
Mexiletine Manufacturing Plant Project Report 2026: Industry Trends, Plant Setup, Machinery, Raw Materials, Investment Opportunities, Cost and Revenue
Mexiletine Manufacturing Plant Project Report (DPR) Summary:
IMARC Group's comprehensive DPR report, titled "Mexiletine Manufacturing Plant Project Report 2026: Industry Trends, Plant Setup, Machinery, Raw Materials, Investment Opportunities, Cost and Revenue," provides a complete roadmap for setting up a mexiletine manufacturing unit. The mexiletine market is driven by the expanding generic drug manufacturing that is improving treatment affordability and accessibility across developed and emerging markets. According to IMARC Group, North America accounts for approximately 35% of the global market.
This feasibility report covers a comprehensive market overview to micro-level information such as unit operations involved, raw material requirements, utility requirements, infrastructure requirements, machinery and technology requirements, manpower requirements, packaging requirements, transportation requirements, etc.
The mexiletine manufacturing plant setup cost is provided in detail covering project economics, capital investments (CapEx), project funding, operating expenses (OpEx), income and expenditure projections, fixed costs vs. variable costs, direct and indirect costs, expected ROI and net present value (NPV), profit and loss account, financial analysis, etc.

Access the Detailed Feasibility Analysis, Request Sample
What is Mexiletine?
Mexiletine is an oral prescription medication primarily classified as a Class 1B antiarrhythmic drug. It is principally prescribed to treat and manage serious, life-threatening ventricular arrhythmias (irregular heartbeats originating in the lower chambers of the heart).The drug functions as a sodium channel blocker. By inhibiting the influx of sodium ions into cardiac myocytes and nerve cells, it slows down overactive electrical impulses and stabilizes the heart's membranes. This action allows the heart to maintain a normal rhythm. Beyond its primary cardiovascular applications, mexiletine is sometimes utilized off-label to manage chronic nerve pain (such as diabetic neuropathy) and reduce muscle stiffness in certain genetic disorders like myotonia.
Key Investment Highlights
- Process Used: Alkylation/ether formation, oxime formation and catalytic hydrogenation to produce mexiletine hydrochloride.
- End-use Industries: Pharmaceutical manufacturing, healthcare, hospitals, clinics, cardiology and neurology care.
- Applications: Used primarily as a sodium-channel-blocking antiarrhythmic and in the management of certain ventricular arrhythmias; it may also be used off-label for neuropathic pain.
Mexiletine Plant Capacity:
The proposed facility is designed with an annual production capacity ranging between 100–500 MT, enabling economies of scale while maintaining operational flexibility.
Mexiletine Plant Profit Margins:
The project demonstrates healthy profitability potential under normal operating conditions. Gross profit margins typically range between 35–45%, supported by stable demand and value-added applications.
- Gross Profit: 35–45%
- Net Profit: 15-22%
Mexiletine Plant Cost Analysis:
The operating cost structure of a mexiletine manufacturing plant is primarily driven by raw material consumption, including chloroacetone, 2,6-dimethylphenol, hydroxylamine, and hydrogen, which accounts for approximately 40–50% of total operating expenses (OpEx).
- Raw Materials: 40–50% of OpEx
- Utilities: 10-15% of OpEx
Financial Projection:
The financial projections for the proposed project have been developed based on realistic assumptions related to capital investment, operating costs, manufacturing capacity utilization, pricing trends, and demand outlook. These projections provide a comprehensive view of the project’s financial viability, ROI, profitability, and long-term sustainability.
Major Applications:
- Pharmaceuticals (active pharmaceutical ingredient for the formulation of antiarrhythmic and local anesthetic medications)
- Healthcare (treatment of ventricular arrhythmias and management of certain cardiac rhythm disorders)
- Medical Research (pharmacological studies involving sodium-channel blockade and cardiac electrophysiology)
- Drug Formulation (development and manufacture of oral pharmaceutical dosage forms, including tablets and capsules)
Why Mexiletine Manufacturing?
✓ Essential Antiarrhythmic Therapeutic Application: Mexiletine is an important Class IB antiarrhythmic medication used primarily for the management of certain ventricular arrhythmias and, in some markets, for other neurological indications such as myotonic disorders, positioning it as a specialized pharmaceutical ingredient with relevance across cardiovascular and neuromuscular care.
✓ Moderate but Justifiable Entry Barriers: Mexiletine manufacturing requires stringent control over chemical synthesis, reaction conditions, purity, impurity profiles and pharmaceutical-grade quality standards. Compliance with GMP requirements, regulatory approvals, analytical testing and consistent batch-to-batch quality creates entry barriers that favour experienced manufacturers with established pharmaceutical production capabilities.
✓ Growing Demand for Specialized Therapeutics: The increasing prevalence of cardiovascular disorders, expanding diagnosis of cardiac arrhythmias and continued demand for treatments for rare neuromuscular conditions support the need for mexiletine and its pharmaceutical formulations. Growing emphasis on specialized and targeted therapies further strengthens opportunities for manufacturers serving niche therapeutic segments.
✓ Regulatory & Healthcare Infrastructure Push: Investments in healthcare infrastructure, expansion of cardiology services, improved access to diagnostic technologies and increasing availability of specialized medicines are supporting demand for established antiarrhythmic therapies such as mexiletine. Strengthening pharmaceutical manufacturing capabilities and domestic API production initiatives also create opportunities for local producers.
✓ Localization and Dependability in Pharmaceutical Supply Chains: Pharmaceutical companies are increasingly seeking reliable API suppliers to reduce supply disruptions, maintain consistent quality and improve procurement resilience. This creates opportunities for regional mexiletine manufacturers with robust sourcing networks, compliant production facilities, strong quality systems and dependable supply capabilities.
Transforming Vision into Reality:
This report provides the comprehensive blueprint needed to transform your mexiletine manufacturing vision into a technologically advanced and highly profitable reality.
Mexiletine Industry Outlook 2026:
The global mexiletine industry is expected to witness steady growth, supported by the rising prevalence of cardiovascular diseases, particularly ventricular arrhythmias, and increasing demand for effective long-term rhythm management therapies. As per the WHO, an estimated 19.8 million people died from cardiovascular diseases in 2022, representing approximately 32% of all global deaths. Mexiletine, an orally administered sodium-channel blocker, continues to play an important role in treating serious ventricular arrhythmias, while its application in myotonic disorders and certain neuropathic conditions is broadening its therapeutic relevance. The growing aging population, increasing incidence of cardiac disorders, and greater adoption of oral antiarrhythmic therapies are anticipated to strengthen demand. Continued clinical research into mexiletine for neuromuscular disorders may further expand its addressable patient population, including potential pediatric applications. Looking ahead, improving healthcare access, wider generic availability, and growing awareness of rare myotonic disorders are expected to create favorable opportunities for manufacturers and pharmaceutical suppliers.
Leading Mexiletine Manufacturers:
Leading manufacturers in the global mexiletine industry include several multinational companies with extensive manufacturing capacities and diverse application portfolios. Key players include:
- Alembic Pharmaceuticals Limited
- AGC Pharma Chemicals
- Willow Birch Pharma
all of which serve end-use sectors such as pharmaceutical manufacturing, healthcare, hospitals, clinics, cardiology and neurology care.
How to Setup a Mexiletine Manufacturing Plant?
Setting up a mexiletine manufacturing plant requires evaluating several key factors, including technological requirements and quality assurance. Some of the critical considerations include:
- Detailed Process Flow: The manufacturing process is a multi-step operation that involves several unit operations, material handling, and quality checks. Below are the main stages involved in the mexiletine manufacturing process flow:
- Unit Operations Involved
- Mass Balance and Raw Material Requirements
- Quality Assurance Criteria
- Technical Tests
- Site Selection: The location must offer easy access to key raw materials such as chloroacetone, 2,6-dimethylphenol, hydroxylamine, and hydrogen. Proximity to target markets will help minimize distribution costs. The site must have robust infrastructure, including reliable transportation, utilities, and waste management systems. Compliance with local zoning laws and environmental regulations must also be ensured.
- Plant Layout Optimization: The layout should be optimized to enhance workflow efficiency, safety, and minimize material handling. Separate areas for raw material storage, manufacturing, quality control, and finished goods storage must be designated. Space for future expansion should be incorporated to accommodate business growth.
- Equipment Selection: High-quality, corrosion-resistant machinery tailored for mexiletine manufacturing must be selected. Essential equipment includes reaction vessels, stirred reactors, heating and cooling systems, condensers, filtration units, oxime reaction vessels, hydrogenation reactors, hydrogen supply systems, solvent recovery units, crystallization tanks, centrifuges, vacuum dryers, milling equipment, and pharmaceutical-grade packaging machines. All machinery must comply with industry standards for safety, efficiency, and reliability.
- Raw Material Sourcing: Reliable suppliers must be secured for raw materials like chloroacetone, 2,6-dimethylphenol, hydroxylamine, and hydrogen to ensure consistent manufacturing quality. Minimizing transportation costs by selecting nearby suppliers is essential. Sustainability and supply chain risks must be assessed, and long-term contracts should be negotiated to stabilize pricing and ensure a steady supply.
- Safety and Environmental Compliance: Safety protocols must be implemented throughout the manufacturing process of mexiletine. Advanced monitoring systems should be installed to detect leaks or deviations in the process. Effluent treatment systems are necessary to minimize environmental impact and ensure compliance with emission standards.
- Quality Assurance Systems: A comprehensive quality management system should be implemented across all stages of operations to ensure consistent product and service standards. Appropriate testing, monitoring, and validation processes must be established to evaluate performance, safety, reliability, and compliance with applicable regulatory and industry requirements. Standard operating procedures (SOPs), documentation protocols, and traceability mechanisms should be maintained to support transparency, risk management, and continuous improvement. Regular audits, inspections, and corrective action frameworks should also be integrated to enhance overall operational excellence.
Project Economics:
Establishing and operating a mexiletine manufacturing plant involves various cost components, including:
- Capital Investment: The total capital investment depends on plant capacity, technology, and location. This investment covers land acquisition, site preparation, and necessary infrastructure.
- Equipment Costs: Equipment costs, such as those for reaction vessels, stirred reactors, heating and cooling systems, condensers, filtration units, oxime reaction vessels, hydrogenation reactors, hydrogen supply systems, solvent recovery units, crystallization tanks, centrifuges, vacuum dryers, milling equipment, and pharmaceutical-grade packaging machines, represent a significant portion of capital expenditure. The scale of manufacturing and automation level will determine the total cost of machinery.
- Raw Material Expenses: Raw materials, including chloroacetone, 2,6-dimethylphenol, hydroxylamine, and hydrogen, are a major part of operating costs. Long-term contracts with reliable suppliers will help mitigate price volatility and ensure a consistent supply of materials.
- Infrastructure and Utilities: Costs associated with land acquisition, construction, and utilities (electricity, water, steam) must be considered in the financial plan.
- Operational Costs: Ongoing expenses for labor, maintenance, quality control, and environmental compliance must be accounted for. Optimizing processes and providing staff training can help control these operational costs.
- Financial Planning: A detailed financial analysis, including income projections, expenditures, and break-even points, must be conducted. This analysis aids in securing funding and formulating a clear financial strategy.
Capital Expenditure (CapEx) and Operational Expenditure (OpEx) Analysis:
Capital Investment (CapEx): Machinery costs account for the largest portion of the total capital expenditure. The cost of land and site development, including charges for land registration, boundary development, and other related expenses, forms a substantial part of the overall investment. This allocation ensures a solid foundation for safe and efficient plant operations.
Operating Expenditure (OpEx): In the first year of operations, the operating cost for the mexiletine manufacturing plant is projected to be significant, covering raw materials, utilities, depreciation, taxes, packing, transportation, and repairs and maintenance. By the fifth year, the total operational cost is expected to increase substantially due to factors such as inflation, market fluctuations, and potential rises in the cost of key materials. Additional factors, including supply chain disruptions, rising consumer demand, and shifts in the global economy, are expected to contribute to this increase.
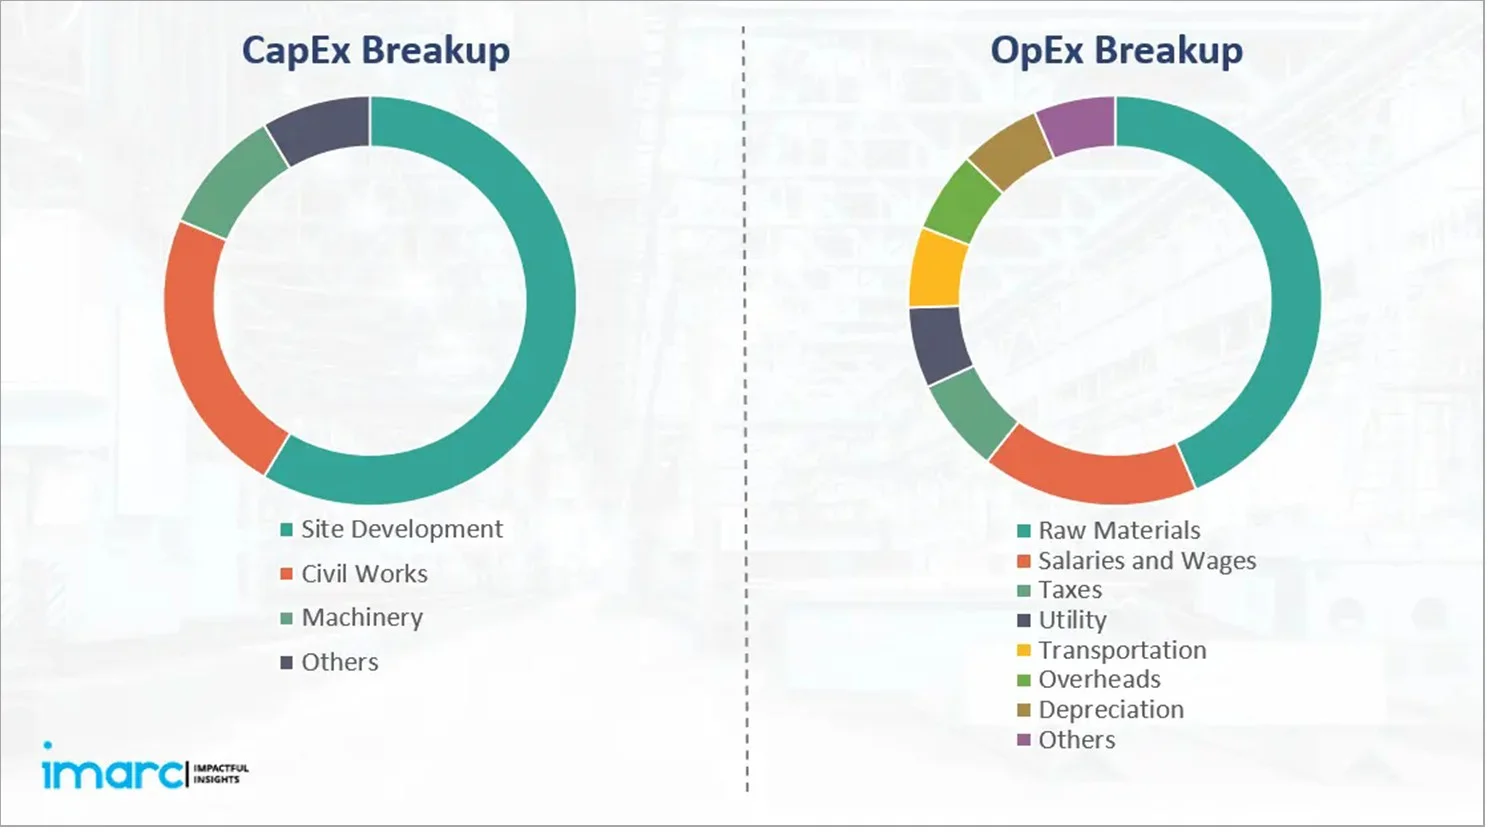
Capital Expenditure Breakdown:
| Particulars | Cost (in US$) |
|---|---|
| Land and Site Development Costs | XX |
| Civil Works Costs | XX |
| Machinery Costs | XX |
| Other Capital Costs | XX |
To access CapEx Details, Request Sample
Operational Expenditure Breakdown:
| Particulars | In % |
|---|---|
| Raw Material Cost | 40-50% |
| Utility Cost | 10-15% |
| Transportation Cost | XX |
| Packaging Cost | XX |
| Salaries and Wages | XX |
| Depreciation | XX |
| Taxes | XX |
| Other Expenses | XX |
To access OpEx Details, Request Sample
Profitability Analysis:
| Particulars | Unit | Year 1 | Year 2 | Year 3 | Year 4 | Year 5 | Average |
|---|---|---|---|---|---|---|---|
| Total Income | US$ | XX | XX | XX | XX | XX | XX |
| Total Expenditure | US$ | XX | XX | XX | XX | XX | XX |
| Gross Profit | US$ | XX | XX | XX | XX | XX | XX |
| Gross Margin | % | XX | XX | XX | XX | XX | 35-45% |
| Net Profit | US$ | XX | XX | XX | XX | XX | XX |
| Net Margin | % | XX | XX | XX | XX | XX | 15-22% |
To access Financial Analysis, Request Sample
Latest Industry Developments:
- December 2025: A research study published in Next Research detailed the reengineering of mexiletine into novel analogs named JME-173 and JME-209. These chemical modifications successfully suppressed the standard anesthetic liabilities of the parent drug while significantly enhancing anti-inflammatory and antispasmodic properties, specifically targeting difficult-to-treat severe asthma.
Report Coverage:
| Report Features | Details |
|---|---|
| Product Name | Mexiletine |
| Report Coverage | Detailed Process Flow: Unit Operations Involved, Quality Assurance Criteria, Technical Tests, Mass Balance, and Raw Material Requirements Land, Location and Site Development: Selection Criteria and Significance, Location Analysis, Project Planning and Phasing of Development, Environmental Impact, Land Requirement and Costs Plant Layout: Importance and Essentials, Layout, Factors Influencing Layout Plant Machinery: Machinery Requirements, Machinery Costs, Machinery Suppliers (Provided on Request) Raw Materials: Raw Material Requirements, Raw Material Details and Procurement, Raw Material Costs, Raw Material Suppliers (Provided on Request) Packaging: Packaging Requirements, Packaging Material Details and Procurement, Packaging Costs, Packaging Material Suppliers (Provided on Request) Other Requirements and Costs: Transportation Requirements and Costs, Utility Requirements and Costs, Energy Requirements and Costs, Water Requirements and Costs, Human Resource Requirements and Costs Project Economics: Capital Costs, Techno-Economic Parameters, Income Projections, Expenditure Projections, Product Pricing and Margins, Taxation, Depreciation Financial Analysis: Liquidity Analysis, Profitability Analysis, Payback Period, Net Present Value, Internal Rate of Return, Profit and Loss Account, Uncertainty Analysis, Sensitivity Analysis, Economic Analysis Other Analysis Covered in The Report: Market Trends and Analysis, Market Segmentation, Market Breakup by Region, Price Trends, Competitive Landscape, Regulatory Landscape, Strategic Recommendations, Case Study of a Successful Venture |
| Currency | US$ (Data can also be provided in the local currency) |
| Customization Scope | The report can also be customized based on the requirement of the customer |
| Post-Sale Analyst Support | 10-12 Weeks |
| Delivery Format | PDF and Excel through email (We can also provide the editable version of the report in PPT/Word format on special request) |
Key Questions Answered in This Report?
- How has the mexiletine market performed so far and how will it perform in the coming years?
- What is the market segmentation of the global mexiletine market?
- What is the regional breakup of the global mexiletine market?
- What are the price trends of various feedstocks in the mexiletine industry?
- What is the structure of the mexiletine industry and who are the key players?
- What are the various unit operations involved in a mexiletine manufacturing plant?
- What is the total size of land required for setting up a mexiletine manufacturing plant?
- What is the layout of a mexiletine manufacturing plant?
- What are the machinery requirements for setting up a mexiletine manufacturing plant?
- What are the raw material requirements for setting up a mexiletine manufacturing plant?
- What are the packaging requirements for setting up a mexiletine manufacturing plant?
- What are the transportation requirements for setting up a mexiletine manufacturing plant?
- What are the utility requirements for setting up a mexiletine manufacturing plant?
- What are the human resource requirements for setting up a mexiletine manufacturing plant?
- What are the infrastructure costs for setting up a mexiletine manufacturing plant?
- What are the capital costs for setting up a mexiletine manufacturing plant?
- What are the operating costs for setting up a mexiletine manufacturing plant?
- What should be the pricing mechanism of the final product?
- What will be the income and expenditures for a mexiletine manufacturing plant?
- What is the time required to break even?
- What are the profit projections for setting up a mexiletine manufacturing plant?
- What are the key success and risk factors in the mexiletine industry?
- What are the key regulatory procedures and requirements for setting up a mexiletine manufacturing plant?
- What are the key certifications required for setting up a mexiletine manufacturing plant?
Report Customization
While we have aimed to create an all-encompassing mexiletine plant project report, we acknowledge that individual stakeholders may have unique demands. Thus, we offer customized report options that cater to your specific requirements. Our consultants are available to discuss your business requirements, and we can tailor the report's scope accordingly. Some of the common customizations that we are frequently requested to make by our clients include:
- The report can be customized based on the location (country/region) of your plant.
- The plant’s capacity can be customized based on your requirements.
- Plant machinery and costs can be customized based on your requirements.
- Any additions to the current scope can also be provided based on your requirements.
Why Buy IMARC Reports?
- The insights provided in our reports enable stakeholders to make informed business decisions by assessing the feasibility of a business venture.
- Our extensive network of consultants, raw material suppliers, machinery suppliers and subject matter experts spans over 100+ countries across North America, Europe, Asia Pacific, South America, Africa, and the Middle East.
- Our cost modeling team can assist you in understanding the most complex materials. With domain experts across numerous categories, we can assist you in determining how sensitive each component of the cost model is and how it can affect the final cost and prices.
- We keep a constant track of land costs, construction costs, utility costs, and labor costs across 100+ countries and update them regularly.
- Our client base consists of over 3000 organizations, including prominent corporations, governments, and institutions, who rely on us as their trusted business partners. Our clientele varies from small and start-up businesses to Fortune 500 companies.
- Our strong in-house team of engineers, statisticians, modeling experts, chartered accountants, architects, etc. have played a crucial role in constructing, expanding, and optimizing sustainable manufacturing plants worldwide.
Need more help?
- Speak to our experienced analysts for insights on the current market scenarios.
- Include additional segments and countries to customize the report as per your requirement.
- Gain an unparalleled competitive advantage in your domain by understanding how to utilize the report and positively impacting your operations and revenue.
- For further assistance, please connect with our analysts.


Factory Setup Services
IMARC Group's factory setup services streamline the entire establishment process, ensuring efficient planning, seamless execution, and optimal operational readiness for your manufacturing facility.


Site Selection Services
IMARC Group's site selection services optimize location choices for businesses, ensuring strategic, cost-effective, and efficient manufacturing operations.


Factory Audit Services
IMARC Group's plant audit services offer comprehensive evaluations of your industrial facility's health, efficiency, and regulatory compliance.


Regulatory Approvals, and Licensing Services
IMARC Group's regulatory approval and licensing services ensure businesses meet all compliance requirements, facilitating smooth and timely market entry.
 Inquire Before Buying
 Speak to an Analyst
 Request Brochure
 Request Customization
Related Reports

Frequently Asked Questions
Our feasibility studies assess several key factors to provide a detailed evaluation of your project's potential. The study includes a pricing analysis of feedstocks, helping to understand industry profit margins and cost variations. Detailed insights into mass balance, unit operations, raw material requirements, and the manufacturing process flow are also provided to ensure a clear understanding of the production setup.
The study also covers critical elements such as location analysis, environmental impact, plant layout, and costs associated with land, machinery, raw materials, packaging, transportation, utilities, and human resources. The project economics section provides an in-depth analysis of capital expenditure (CapEx), operating expenditure (OpEx), income projections, taxation, depreciation, liquidity, profitability, payback period, net present value (NPV), uncertainty, and sensitivity analysis.
Additionally, IMARC Group's feasibility studies address regulatory procedures, financial assistance, and necessary certifications, ensuring all legal and compliance requirements are met. By covering these aspects, IMARC Group's feasibility studies support informed decision-making, risk reduction, and the overall viability of your business.
Yes, our site identification services include a thorough assessment of potential sites based on proximity to raw materials, ensuring cost-effective and timely supply chain operations. We also consider access to infrastructure, such as transportation networks, utilities, and technology, which are essential for smooth plant operations. Labor availability is another key factor we analyze to ensure that the site has access to a skilled workforce. Additionally, we evaluate the environmental impact to ensure compliance with regulations and sustainable practices. By integrating these factors, we provide a comprehensive site evaluation to identify the optimal location for your new plant, supporting your strategic goals and operational efficiency.
Yes, our regulatory approvals and licensing services are made specifically to support companies in effectively and efficiently navigating the ever-changing regulatory environment. We start by carefully evaluating your company's requirements as well as the unique regulatory framework that applies to your sector. After that, you are assisted by our team of professionals throughout the whole process of securing the necessary industrial permits, business licenses, and environmental clearances.
Additionally, we help with industry-specific regulatory licensing so that your company complies with all sector-specific regulations. To further safeguard your brand and innovations from the outset, we also offer support for intellectual property rights (IPR) registrations and licensing. We manage the required documentation and communicate with pertinent authorities on your behalf by utilizing our deep industry experience and painstaking attention to detail. This allows you to focus on building and growing your business while we take care of the regulatory complexities. Partnering with us ensures that your business is fully compliant and ready to thrive from the start.
Our skilled engineering staff specializes in designing efficient and effective plant layouts that meet your unique needs. We begin with a comprehensive process design to ensure the best possible workflow and use of resources.
Our services include careful equipment selection, ensuring that your plant design incorporates the most suitable and advanced machinery. We also focus on meticulous layout planning, strategically arranging workstations and equipment to optimize output and reduce operational bottlenecks. Furthermore, our facility design takes into account every important factor, such as regulatory compliance, scalability, and safety.
By leveraging our expertise, we ensure that your plant layout not only meets your current operational needs but is also adaptable to future growth and technological advancements. Our goal is to create a well-organized, efficient, and compliant facility that enhances your overall operational efficiency and supports your business objectives.
Yes, our raw material and machinery sourcing services are designed to identify and connect you with reliable and affordable providers. We leverage our extensive network and industry expertise to source high-quality raw materials and advanced machinery that meet your specific requirements.
We also conduct supplier audits and evaluations so that you get the best value for your investment. We evaluate potential suppliers on the basis of cost, quality, reliability, and delivery timelines. We also make sure that all the legal requirements are met, including customs, tax regulations, labor laws, and import/export laws, to ensure you are fully compliant.
When you choose to work with us, you gain access to a list of suppliers pre-screened for affordability and reliability, helping you optimize your procurement process and reduce overall operational costs. It is our goal to assist you in establishing a new plant effectively and economically, ensuring long-term success and sustainability.
IMARC Group can effectively manage the construction of your new facility through our comprehensive construction management services. Our dedicated construction management team oversees the entire construction phase, ensuring that all activities are executed according to plan and within the specified timeline. We manage contractors, coordinating their efforts to ensure smooth and efficient workflow on-site.
Furthermore, our team pays great attention to the progress of the construction work, and we conduct site reviews and quality control to ensure that the construction work is done to the highest standards. We resolve any problems as they arise, thus avoiding any form of delay and keeping the project on schedule. When you work with us, you can be assured that your new facility will be constructed to the highest standards that will enable you to concentrate on your core business activities.
Yes, our distributor identification services are designed to connect companies with trusted distributors who meet high standards of reliability, performance, and ethical practices. We leverage our vast network of vetted distributors across various industries and regions to find the best match for your business needs.
Our process begins with a careful analysis of your particular needs and business goals. We then carry out rigorous research and due diligence to identify the distributors that have market reach and the capability to manage your product lines effectively. Our thorough vetting process involves the distributors' background checks and performance history reviews to ensure that they meet industry standards and have a proven track record.
Also, we ensure compliance with the relevant legislation and regulations to avoid legal issues that may affect the functioning of the company. Once potential distributors are identified, we organize business meetings, as well as handle all logistics to facilitate productive discussions. We provide continuous support throughout the partnership, including performance monitoring and logistics coordination, to ensure the success and optimization of your distribution networks in the long run.
Yes, our factory audit services provide a systematic and thorough evaluation of your plant's performance across various critical parameters. Our experienced auditors utilize industry best practices to conduct detailed inspections, focusing on safety, quality, efficiency, compliance, and sustainability.
Our audits assess safety protocols to ensure a secure working environment, evaluate quality standards to enhance product satisfaction and optimize processes to increase productivity and reduce costs. Compliance checks ensure adherence to relevant regulations, mitigating legal risks, and our sustainability assessments recommend eco-friendly practices to minimize environmental impact.
Our holistic approach delivers actionable insights through detailed audit reports, offering clear recommendations for continuous improvement. By partnering with us, you gain valuable insights into your plant's operations, enabling you to drive enhancements, achieve operational excellence, and maintain a competitive edge.
Yes, our contract manufacturer identification services are designed to assist businesses in navigating the complex landscape of contract manufacturing. We start by defining the ideal contract manufacturer through in-depth discussions with our clients, followed by extensive research to identify potential candidates.
Once potential manufacturers are identified, we conduct a rigorous evaluation and vetting process to ensure they meet high standards of quality, reliability, and compliance with relevant regulations. Our team handles the pre-screening process, arranging meetings between our clients and interested candidates, and managing all logistics to facilitate productive discussions.
We have strict performance monitoring and quality control checks to ensure the manufacturers remain at par with your expectations and contribute positively to your business throughout the partnership lifecycle. Through our expertise and extensive network, we ensure that you partner with capable and credible contract manufacturers, who help you drive efficiency, quality, and growth in your production processes.
IMARC Group offers a comprehensive suite of marketing and sales services dedicated to helping businesses increase revenues and effectively sell products. Our performance marketing services focus on data-driven campaigns that maximize return on investment, utilizing programmatic advertising and retargeting techniques to reach the right audience at the right time. We enhance your online presence through SEO and SMO, driving organic traffic and improving your digital footprint.
The lead generation strategies we use target high-quality quality leads that convert into loyal clients, while our brand promotion strategies including influencer marketing and creative designing enhance the visibility and credibility of your brand. Our social media management services assist you in engaging with your audience, establishing relationships with them, and driving conversions through targeted campaigns.
By partnering with IMARC Group, you benefit from our approach that is tailored to your business needs and unique objectives. Our strategies cover all aspects of digital marketing so that you can reach your target audience consistently, along with our ongoing support and optimization to keep your campaigns effective and relevant. Our cutting edge and performance driven marketing services help you gain the competitive advantage and ensure long-term success.
Choose your plan
*Please note that the prices mentioned below are starting prices for each bundle type. Kindly contact our team for further details.*
Single User License
- 1 User License, Access on 2 Devices
- PDF Report + Excel Dataset (Password Protected)
- Lifetime Access
- No Printing Rights
- 10% Free Report Customization
- 10–12 Weeks of Analyst Support
Five User License
- Access for 5 Users, 2 Devices per User
- PDF Report + Excel Dataset (Password Protected)
- Lifetime Access
- Dedicated Account Manager
- 12–14 Weeks of Analyst Support
- No Printing Rights
- 15% Free Report Customization
- 25% Discount on Your Next Purchase
Corporate User License
- Unlimited User Access (Within Your Organization)
- PDF Report + Excel Dataset
- Lifetime Access
- Dedicated Account Manager
- 14–20 Weeks of Analyst Support
- No Printing Rights
- 20% Free Report Customization
- 30% Discount on Your Next Purchase
Essential Insights
What's included:
3 reports
- Lifetime Access
- PDF Reports
- Excel Datasets
- 2 Weeks of Free Analyst Support
- 2 User Licenses
- Access on 2 Devices
- Printing Rights
- Complimentary PowerPoint (PPT) Version
- Complimentary License Upgrade
Professional Access
What's included:
5 reports
- Lifetime Access
- PDF Reports
- Excel Datasets
- 8 Weeks of Free Analyst Support
- 2 User Licenses
- Access on 2 Devices
- Printing Rights
- Complimentary PowerPoint (PPT) Version
- Complimentary License Upgrade
Business Advantage
What's included:
8 reports
- Lifetime Access
- PDF Reports
- Excel Datasets
- 14 Weeks of Free Analyst Support
- 2 User Licenses
- Access on 2 Devices
- Printing Rights
- Complimentary PowerPoint (PPT) Version
- Complimentary License Upgrade
Enterprise Intelligence
What's included:
10 reports
- Lifetime Access
- PDF Reports
- Excel Datasets
- 20 Weeks of Free Analyst Support
- 2 User Licenses
- Access on 2 Devices
- Printing Rights
- Complimentary PowerPoint (PPT) Version
- Complimentary License Upgrade