PET Preform Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
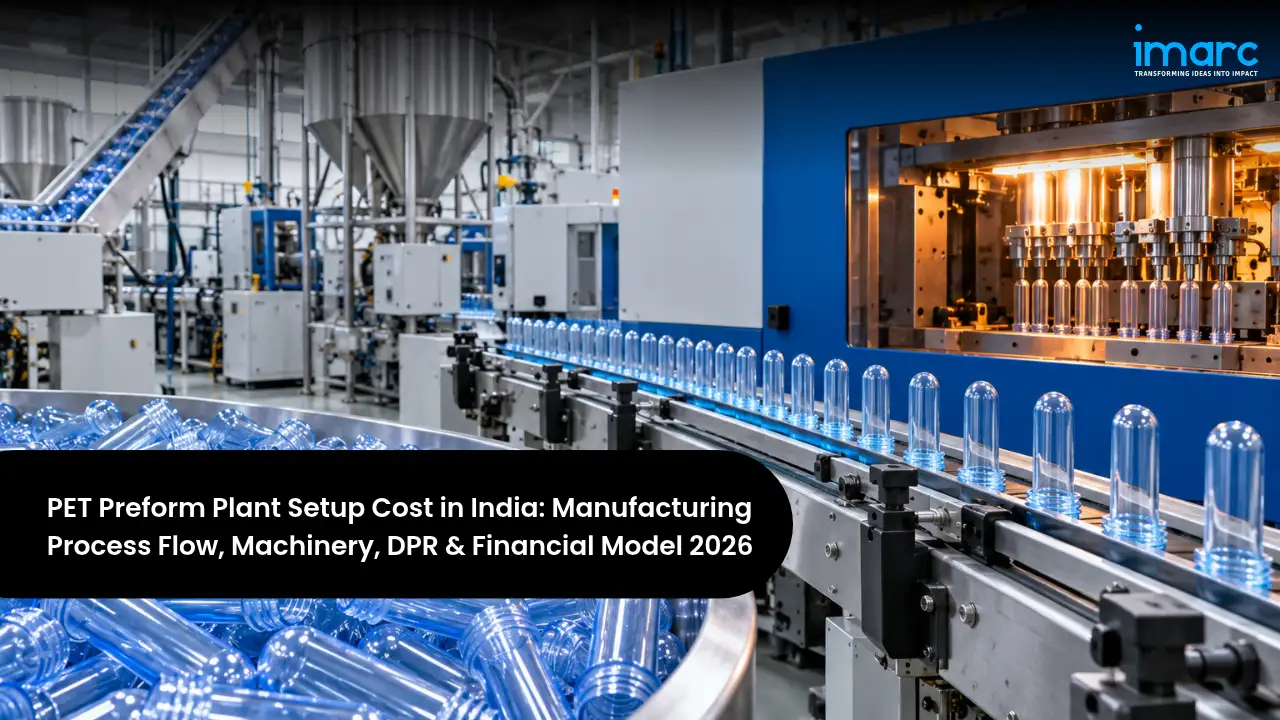
PET preforms are test-tube-shaped mouldings of polyethylene terephthalate with a finished threaded neck, which bottlers heat and stretch-blow into bottles for drinking water, soft drinks, juices, edible oil, dairy, pharmaceuticals, personal care, and household products. Preforms are compact and easy to transport, so they are usually made in dedicated injection moulding plants and shipped to bottling lines across a region. The global PET preform market was valued at about USD 17.5 billion in 2025 and is projected to reach USD 25.8 billion by 2034, and India's wider PET packaging market was about USD 1.5 billion in 2024. Rising packaged water and beverage consumption, growth in edible oil and FMCG packaging, and new rules requiring recycled PET in packaging make PET Preform Manufacturing Plant Setup in India a steady opportunity for plastics processors and packaging investors.
Investment depends mainly on capacity, the number of injection systems and mould cavities, the neck finishes and weights produced, drying and cooling systems, automation, and whether the plant processes recycled PET. The PET Preform Manufacturing Plant Cost ranges from about INR 8–15 crore for a small unit of 2,000 to 3,000 tonnes a year with one or two machines to INR 50–90 crore for a plant of 10,000 to 15,000 tonnes a year with several high-cavitation systems, and INR 200–350 crore for a large facility of 40,000 tonnes a year or more with 128 to 144 cavity systems and recycled PET handling. Resin makes up 75 to 85% of operating cost and utilities 10 to 15%, so PET resin prices, cycle time, and rejection rates shape profitability. A well-run plant typically earns a gross margin of 20 to 30% and a net margin of 8 to 12%.
This guide is written for investors exploring how to start a PET Preform manufacturing plant in India. It focuses on a plant of about 12,000 tonnes a year producing water, carbonated soft drink, edible oil, and FMCG preforms in standard neck finishes for bottlers and brand owners, and also explains small units and large facilities. It covers products and markets, the demand outlook, the production process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, recycled content and other approvals, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Global Preform Market (2025) | About USD 17.50 Billion |
| Global Market Forecast (2034) | USD 25.78 Billion, 4.4% CAGR |
| India PET Packaging Market (2024) | About USD 1.5 Billion |
| Recycled Content (FY2026-27) | 40% for food-contact PET |
| Typical Plant Capacity | 50,000 – 100,000 Tonnes a Year |
| Indicative Total Investment | INR 8 Crore to 350 Crore |
The snapshot shows a large, steadily growing packaging market, with beverages the dominant end use and West and Central India the leading region. New recycled content rules are reshaping raw material sourcing, and preform makers that can process food-grade recycled PET will be better placed with brand owners. The wide investment range reflects a real choice between a small unit, a mid-sized multi-machine plant, and a large high-cavitation facility. The sections below work through that choice.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Water, CSD, oil, pharma, FMCG preforms |
| Plant Capacity | 2,000 – 40,000+ Tonnes per year |
| Total Project Investment | INR 8–15 Crore (small unit) to 200–350 Crore (large plant) |
| Payback Period | 4 – 5 Years |
| Net Profit Margin | 8 – 12% |
| IRR | 15 – 22% |
| Preferred States | Gujarat, Maharashtra, Uttar Pradesh, Tamil Nadu, West Bengal, Telangana |
| Key Requirement | Resin supply, moulds, bottler contracts |
These ranges provide a realistic frame for early planning, but actual returns depend on PET resin prices, which follow crude oil and PTA and MEG markets, the cost and availability of food-grade recycled PET, cycle times and mould cavitation, rejection rates, freight to bottlers, seasonal beverage demand, and competition from bottlers who make their own preforms. A site-specific PET Preform Feasibility Report narrows each of these assumptions to your chosen products, capacity, location, and customers.
Table of Contents
- What is PET Preform Manufacturing?
- Why is PET Preform Manufacturing Growing in India?
- PET Preform Manufacturing Process Flow
- Raw Materials Required for PET Preform Manufacturing
- Location, Land & Infrastructure
- PET Preform Manufacturing Machinery and Equipment
- PET Preform Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for PET Preform Manufacturing in India
- Recent Developments in the India PET Preform Manufacturing Industry
- How a PET Preform Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is PET Preform Manufacturing?
A preform is the intermediate form of a PET bottle. Dried PET resin is melted and injected into a multi-cavity mould, where it forms a thick-walled tube with a fully formed neck, thread, and support ring. The body is later reheated and stretch-blow-moulded into the final bottle shape, while the neck stays unchanged and must fit the cap exactly. Preforms are defined by weight, typically from about 9 g for small water bottles to over 50 g for large oil and soft drink containers, and by neck finish, such as standard soft drink, water, and wide-mouth finishes. Clarity, weight accuracy, neck dimensions, low acetaldehyde, and minimal loss of intrinsic viscosity decide quality.
Commercially, preforms are sold to packaged drinking water bottlers, soft drink and juice bottlers, edible oil packers, dairy companies, pharmaceutical and personal care companies, household product makers, and liquor and alcoholic beverage producers. A PET Preform Manufacturing Plant can serve all these segments by changing moulds and neck finishes. Buyers value consistent weight and dimensions, clarity, freedom from defects, compatibility with their blowing machines and caps, reliable supply in peak season, and competitive prices.
- Water: Lightweight preforms for drinking water.
- Carbonated Drinks: Pressure-resistant preforms for CSD.
- Edible Oil & Food: Larger preforms for oil and sauces.
- Pharma & FMCG: Wide-mouth and specialty preforms.
The Main Preform Types and Applications
Choosing the product mix is the most important commercial decision, because it determines moulds, machines, resin grades, and customers:
| Preform Type | Description | Key Property | Primary Demand |
|---|---|---|---|
| Water Preforms | 9 – 25 g, short neck | Light weight | Water bottlers |
| CSD Preforms | PCO neck | Pressure resistance | Soft drinks |
| Edible Oil Preforms | 30 – 90 g | Strength | Oil packers |
| Hot-Fill Preforms | Heat-set neck | Heat resistance | Juices |
| Wide-Mouth Preforms | Jar necks | Easy filling | Food, FMCG |
| Pharma Preforms | Small, coloured | Light protection | Syrups, tablets |
These choices shape the whole plant. Water and soft drink preforms are high-volume, price-sensitive products that need high-cavitation systems and fast cycle times, while edible oil, hot-fill, wide-mouth, and pharma preforms use different moulds, resin grades, and sometimes colours, and are made in smaller lots at better margins. Most new entrants therefore start with water and edible oil preforms in standard neck finishes, and add soft drink, hot-fill, and specialty preforms as their moulds, quality systems, and customer base grow.
Why is PET Preform Manufacturing Growing in India?
Key Growth Drivers in India and Export Markets
Demand is supported by rising consumption of packaged drinks and foods and by shifts in packaging rules:
- Packaged water: Bottled water demand keeps growing in cities, towns, and travel hubs.
- Beverages: Soft drink, juice, and dairy brands are expanding their bottling capacity.
- Edible oil and FMCG: More oils, sauces, and household products move into PET bottles.
- Recycled content rules: Mandatory recycled PET content creates demand for rPET-capable preform makers.
- Exports: Indian preforms are supplied to South Asia, the Middle East, and Africa.
India-Specific Market Opportunity
| Segment | Market Context | Manufacturing Role |
|---|---|---|
| Water Bottlers | Many regional brands | Light preforms |
| Beverage Majors | Franchise bottlers | CSD preforms |
| Edible Oil Packers | Shift to PET | Large preforms |
| FMCG & Pharma | Brand owners | Specialty preforms |
The strongest opportunity for new entrants lies in reliable regional supply to the many water and beverage bottlers that do not make their own preforms, in edible oil and FMCG preforms with better margins, and in rPET-blend preforms for brand owners meeting recycled content targets. Producers that combine competitive resin sourcing, efficient high-cavitation moulding, and dependable delivery will be best placed to grow.
PET Preform Manufacturing Process Flow
Understanding the process helps you plan equipment, layout, and where cost and quality are decided. The flow runs from resin receipt and testing through blending with recycled PET and masterbatch, drying, injection moulding with hot runner moulds, in-mould and post-mould cooling, inspection, counting and packing, and storage to dispatch. Drying and melt control decide clarity and viscosity loss, while mould design and cycle time decide output and cost.
The PET Preform Manufacturing Process Flow
The sequence below reflects a plant using virgin and recycled PET. Plants using only virgin resin skip the recycled PET blending step.
| Unit Operation | Key Activity |
|---|---|
| Resin Receipt | IV, moisture checked |
| Blending | Virgin, rPET, colour |
| Drying | Below 50 ppm moisture |
| Melting | Screw at 270 – 290 °C |
| Injection | Hot runner mould |
| Mould Cooling | Chilled water |
| Post-Mould Cooling | Robot cooling tubes |
| Inspection | Vision, weight |
| Counting & Packing | Octabins, cartons |
| Storage & Dispatch | Dust-free stores |
Two factors decide profitability across this flow. The first is resin efficiency, because resin is most of the cost, so accurate preform weights, low reject rates, and careful drying that prevents viscosity loss directly protect margins. The second is cycle time and uptime, since a high-cavitation system running a few seconds faster per cycle, with little downtime for mould changes and maintenance, can produce many more preforms from the same capital.
Raw Materials Required for PET Preform Manufacturing
The main raw material is bottle-grade PET resin with intrinsic viscosity usually between 0.76 and 0.84 dl/g, increasingly blended with food-grade recycled PET, along with colour masterbatches, acetaldehyde scavengers and other additives where needed, and packaging such as octabins, cartons, and liners.
| Raw Material | Role in Product | India Sourcing | % of OpEx |
|---|---|---|---|
| Virgin PET Resin | Main input | Domestic producers | 55–65% |
| Food-Grade rPET | Recycled content | Domestic recyclers | 12–18% |
| Masterbatch & Additives | Colour, AA control | Domestic suppliers | 1–3% |
| Packaging | Octabins, cartons | Domestic suppliers | 2–3% |
| Mould Spares | Wear parts | Domestic, imported | 1–2% |
PET resin is by far the largest cost, and its price moves with crude oil and with the prices of PTA and MEG, its building blocks. Contracts with domestic resin producers, approved food-grade rPET suppliers, pricing linked to resin indices with bottlers, and careful inventory management through seasonal peaks help manage cost and supply risk.
Location, Land & Infrastructure
Site selection for a preform plant is driven by proximity to bottlers and brand owners, access to PET resin and rPET suppliers, and reliable power for injection moulding and chillers. Other factors include good road links for frequent deliveries, availability of skilled machine operators and mould technicians, and state incentives for plastics processing. Because preforms are light but bulky and bottlers want just-in-time supply, locating within a few hundred kilometres of bottling clusters is usually the best option.
Choosing the Best Location for PET Preform Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Gujarat | Resin plants, FMCG | Raw material |
| Maharashtra | Large bottling base | Demand |
| Uttar Pradesh | Northern bottlers | Large market |
| Tamil Nadu | Southern beverages | Demand, ports |
| West Bengal | Haldia resin plant | Eastern market |
| Telangana | Hyderabad bottlers | Central south |
Gujarat combines domestic PET resin production with large FMCG and edible oil industries, while Maharashtra and Uttar Pradesh host many water and beverage bottlers. Tamil Nadu and Telangana serve fast-growing southern markets, and West Bengal offers resin supply from Haldia and access to eastern markets. The final choice should weigh customer proximity, resin access, power cost, and land cost.
Quality, Safety and Environmental Systems
Preforms for food and beverages must meet Indian food-contact standards for PET and migration limits, and recycled PET must come from FSSAI-approved processes and meet the relevant standard for recycled plastics, with recycled content labelled where required. A credible plant needs a laboratory for intrinsic viscosity, acetaldehyde, weight, dimensions, and stress testing, vision inspection on every line, and batch traceability of resin and rPET. Safety focuses on hot moulds, high-pressure hydraulics, robots, and electrical systems. Environmental systems cover regrinding and recycling of rejects, dust-free storage, and energy-efficient chillers. An experienced PET Preform Manufacturing Consultant in India can help plan products, moulds, machines, and approvals so the plant meets regulatory and customer requirements from the start.
Infrastructure Requirements (12,000 TPA Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 2 – 4 acres | Industrial area |
| Moulding Hall | Injection systems | Clean, cool |
| Resin Store | Silos, bags | Dry storage |
| Chiller Plant | Process cooling | Energy efficient |
| Utilities | Power, compressed air | 2 – 3 MW load |
| Finished Goods Store | Octabins | Dust-free |
| QC Laboratory | IV, AA, dimensions | Food-contact tests |
Reliable power, an efficient chiller plant, and a clean, cool moulding hall are the most important infrastructure requirements, since injection moulding and cooling run continuously. Dry resin storage, dust-free finished goods stores, a capable laboratory, and good road access for frequent dispatches complete the core needs.
PET Preform Manufacturing Machinery and Equipment
The equipment set covers resin handling, blending, drying, injection moulding, cooling, inspection, packing, and utilities. Injection moulding systems and hot runner moulds account for most of the machinery budget.
| Equipment | Function | Key Specification |
|---|---|---|
| Resin Silos & Conveying | Store, feed resin | Vacuum conveying |
| Blender & Dosing | Mix rPET, colour | Gravimetric |
| Dehumidifying Dryer | Dry resin | Low dew point |
| Crystalliser | Prepare rPET | For flakes |
| Injection System | Mould preforms | High cavitation |
| Hot Runner Mould | Form preforms | 48 – 144 cavities |
| Post-Mould Cooling | Cool preforms | Robot take-out |
| Chillers | Cool moulds | Water cooled |
| Air Compressors | Supply air | Oil-free |
| Vision Inspection | Detect defects | Automatic |
| QC Instruments | Test quality | IV, AA, polariscope |
Machinery should follow the product plan. A small unit needs one or two injection machines with 32 to 48 cavity moulds, a dryer, a chiller, and manual packing, while a mid-sized plant adds several dedicated preform systems with 72 to 96 cavity hot runner moulds, central resin conveying, vision inspection, and automatic packing. Large facilities add 128 to 144 cavity systems, recycled PET crystallisers and blending, and full automation, and a good stock of mould spares is essential at every scale.
PET Preform Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a plant of about 12,000 tonnes a year in India. The final PET Preform Investment Cost for your project will depend on capacity, number of systems and cavities, mould range, recycled PET handling, land cost, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Injection Systems | 40–50% | Machines, robots |
| Moulds & Tooling | 12–18% | Hot runner moulds |
| Utilities & Chillers | 8–12% | Cooling, power, air |
| Buildings & Civil Works | 10–14% | Hall, stores |
| Land & Site Development | 4–7% | Land and approvals |
| Working Capital | 10–15% | Resin, receivables |
Injection systems and moulds make up most of the fixed capital, and each new neck finish or weight needs its own mould. Working capital is significant because resin is bought in large lots and bottlers build stock before summer. Because of this, a detailed PET Preform Business Plan should model sales by preform type and customer, resin and rPET prices, cycle times and cavitation, rejection rates, power costs, seasonal demand, credit terms, and working capital together, so that funding supports the business through peak and off-peak seasons.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials & Packaging | 75–85% | PET resin, rPET |
| Utilities (power) | 10–15% | Moulding, chillers |
| Labour | 2–3% | Operators, technicians |
| Maintenance & Moulds | 1–2% | Spares, servicing |
| Logistics | 1–2% | Deliveries to bottlers |
| Overheads & Testing | 1–2% | Quality, admin |
With resin making up most of the cost, margins depend on the conversion charge over resin, weight accuracy, rejection rates, power use, and capacity utilisation. A good operating model tracks resin consumption per thousand preforms, cycle times, uptime, rejects, power per tonne, and realised conversion margins by customer, and tests results against higher resin prices, weaker summer demand, or price competition.
Financial Analysis and Profitability
Based on analysis of a 12,000 TPA plant, the financial profile is moderate and steady, supported by large and growing beverage and FMCG demand, but returns depend heavily on conversion margins, utilisation, and resin management. The profitability of PET Preform manufacturing business in India improves markedly with high-cavitation systems and fast cycles, low rejects, energy-efficient chillers, long-term supply contracts with bottlers, resin-linked pricing, and a growing share of edible oil, specialty, and rPET-blend preforms.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 20–30% | Conversion driven |
| Net Profit Margin | 8–12% | After depreciation, taxes |
| Payback Period | 4–5 Years | Machine intensive |
| IRR (Internal Rate of Return) | 15–22% | Higher for specialty |
| Capacity Utilization (stable ops) | 70–85% | Seasonal peaks |
| Break-even Capacity Utilization | 45–55% | Moderate fixed costs |
Customer mix and utilisation decide where a plant lands within these ranges. Edible oil, hot-fill, pharma, and coloured preforms earn better conversion charges than lightweight water preforms, which compete mainly on price. Plants with annual contracts and steady off-season demand from oil and FMCG customers use their machines better than those relying only on summer beverage demand.
Returns can be strengthened by investing in high-cavitation, energy-efficient systems, lightweighting designs that save resin for customers, adding rPET blending to meet brand owners' recycled content needs, diversifying into oil, FMCG, and pharma preforms, and signing resin-linked annual contracts.
Key Risks and Mitigation
The main risks are resin price swings, seasonal demand, competition from bottlers making their own preforms, price pressure from other converters, changes in recycled content rules, and quality claims. Price risk is reduced by resin-linked contracts; seasonal risk by diversifying into non-beverage customers; competition risk by service, quality, and specialty products; regulatory risk by building rPET capability early; and quality risk by strong inspection. Promoters often work with a PET Preform Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for PET Preform Manufacturing in India
Approvals for a preform plant centre on plastic waste and recycled content rules, food-contact compliance, and factory requirements, along with standard business registrations. Promoters setting up a PET Preform Manufacturing Plant in India generally need the following:
- EPR Registration: Registration on the CPCB portal as a producer of plastic packaging under the waste rules.
- Food-Contact Compliance: Compliance with Indian food-contact standards and FSSAI packaging rules.
- Recycled PET Use: Sourcing rPET from FSSAI-approved recyclers and labelling recycled content.
- Pollution Control: Consent to Establish and Operate from the state pollution control board.
- Customer Audits: Approvals and audits by beverage and FMCG brand owners.
- Factory & Fire: Factory license, building plan approval, and fire NOC.
- Business & Trade Registrations: Business registration, GST, Udyam, trademark, and Import Export Code.
Customer approvals and food-contact compliance are usually on the critical path, since large bottlers and brand owners will not buy preforms without audits and test results. Starting trials with target customers during commissioning shortens the time from investment decision to regular orders.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, products, state pollution control categories, customer specifications, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India PET Preform Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- Recycled content rule: In April 2026, amended plastic waste rules required at least 40% recycled content in food-contact PET packaging for FY2026-27, up from 30% in 2025-26.
- rPET capacity: In April 2026, industry estimated India had 15 to 18 food-grade rPET plants with about 300,000 tonnes of capacity.
- Food-grade rPET: In April 2025, FSSAI issued guidelines and a logo for using recycled PET in food packaging.
- Industry investment: In September 2024, IVL Dhunseri and Dhunseri Ventures formed a joint venture with Varun Beverages to build PET recycling plants in India.
The common thread is a rapid shift toward recycled PET in packaging, backed by rules and new recycling capacity. New entrants who build rPET blending capability, efficient moulding, and close bottler relationships will be best placed to grow.
How a PET Preform Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from market demand and product selection to resin sourcing, machine and mould selection, plant design, approvals, and economics. It helps investors decide the right products, capacity, and location, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed PET Preform Financial Model covering sales by preform type and customer, resin and rPET prices, cycle times and cavitation, weights and rejects, power and chiller costs, mould costs, labour, logistics, seasonal demand, working capital, debt servicing, cash flows, break-even, return on investment, and payback under different price and volume scenarios. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a PET Preform Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a preform project, a strong DPR also clarifies the product and customer strategy, the machine and mould plan, the resin and rPET sourcing approach, and the recycled content and food-contact compliance path, which together are the factors most likely to decide success. By testing margins against resin prices, utilisation, and competition, the report turns a steady packaging opportunity into a plan that lenders and partners can trust.
Frequently Asked Questions
What are the first steps to set up a PET preform manufacturing plant in India?
Start by choosing your products and customers, such as water preforms for regional bottlers or oil preforms for packers. Then commission a feasibility study and DPR, select injection systems and moulds, secure virgin and recycled PET supply, choose a site near bottling clusters, obtain EPR registration and other approvals, install drying, moulding, and cooling equipment, and complete customer trials.
How much does it cost to set up a PET preform manufacturing plant in India?
Investment ranges from about INR 8–15 crore for a small unit of 2,000 to 3,000 tonnes a year to INR 50–90 crore for a plant of 10,000 to 15,000 tonnes a year, and INR 200–350 crore for a large facility of 40,000 tonnes a year or more.
What are the main steps in making PET preforms?
The flow runs from resin receipt and blending through drying, melting, injection into hot runner moulds, mould and post-mould cooling, inspection, counting and packing, and storage and dispatch.
Which machinery does a PET preform manufacturing plant need?
Key equipment includes resin silos and conveying, blenders, dehumidifying dryers, crystallisers for rPET, injection systems, hot runner moulds, post-mould cooling robots, chillers, air compressors, vision inspection, and quality testing instruments.
What raw materials are used for PET preform manufacturing?
The main raw material is bottle-grade PET resin, increasingly blended with food-grade recycled PET, along with colour masterbatches, additives, and packaging such as octabins and cartons.
How profitable is PET preform manufacturing in India?
A well-run plant typically earns a 20 to 30% gross margin and an 8 to 12% net margin, with payback in about 4 to 5 years. Profitability depends on conversion margins, utilisation, rejects, power costs, and product mix.
Which approvals does a PET preform manufacturing plant need in India?
Typical approvals include EPR registration on the CPCB portal, food-contact compliance, use of FSSAI-approved rPET, pollution control consents, customer audits, factory and fire approvals, and GST, Udyam, trademark, and Import Export Code registrations.
How do I get a feasibility study or DPR for a PET preform manufacturing project?
A detailed feasibility study and DPR covers market demand, products, resin sourcing, machines and moulds, plant design, approvals, and full financials. Investors usually engage a PET Preform Manufacturing Feasibility Study Consultant with experience in plastics and packaging projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Biodegradable tableware covers plates, bowls, trays, cups, food containers, clamshells, and cutlery made from plant-based materials such as sugarcane bagasse, bamboo and wheat straw fibre, areca palm leaves, paper, wood, and certified compostable bioplastics.
Setting up a Corrugated Box Manufacturing Plant in India is a high-demand, packaging-driven venture, powered by the country's booming e-commerce, FMCG, and export sectors, and the steady shift toward recyclable paper-based packaging.
Setting up a Pallets Manufacturing Plant in India is a high-demand, logistics-driven venture, powered by the country's booming warehousing, e-commerce, and organized-retail sectors, and the steady formalization of supply chains after GST.
The GCC biodegradable food service disposables market size is undergoing a remarkable change as environmental sustainability takes center stage in regional business and regulatory agendas. Throughout the Gulf Cooperation Council nations, which include countries like Saudi Arabia, the UAE, Qatar, Kuwait, Oman, and Bahrain, significant players within the food service packaging sector are powerfully embracing novel packaging solutions that not only reduce environmental impact but also cater to modern-day consumers' needs for convenience and efficiency.
PVC blisters packaging is a type of thermoforming packaging wherein polyvinyl chloride (PVC) material is heated to mold it into packaging cavities to securely place individual items inside, which is then closed with either aluminum foil or paper-based lidding materials. PVC packaging exhibits clarity, strength, and moldability, making it possible to view the individual items while also protecting them against external damage.
A PET bottle is a type of rigid packaging packaging that is produced using a thermoplastic called polyethylene terephthalate, also known as polyester. The production of a PET bottle involves an injection stretch-blow molding technique that provides a lightweight and durable package with high clarity, strength, and impermeability.
Paper cups are a type of beverage container made mostly from paperboard. The paperboard gives the container strength. The lining of the paperboard varies and usually consists of waterborne coatings, bio-based coatings, and polymer coatings. This facilitates the paper cup to hold hot and cold fluids for an amount of time. Paper cups come in various sizes and different wall structures. This makes the paper cup functional for the desired purpose and environment.
Bagasse kraft paper is a green packaging material made from bagasse, the fibrous byproduct that is left when juice is extracted from sugarcane. Kraft paper is generally produced traditionally using wood pulp via the sulfate process, but bagasse offers a sustainable, non-wood source used in promoting green manufacturing and less reliance on forest resources. Bagasse fibers have high cellulose, moderate fiber length, and good bonding properties, making them ideal for manufacturing strong and long-lasting kraft paper. Production includes bagasse collection from sugar mills, purification to eliminate impurities, and processing into pulp either by chemical or mechanical pulping.
Bagasse biodegradable cutlery is made from the fibrous material remaining after extracting sugarcane stalk juice, a low-value agricultural residue also known as bagasse. The material is harvested from sugar mills, washed, pulped and mechanically molded into wet-molded forms; those wet parts are dried, pressed in heat-resistant molds and thermally cured to create rigid, food-grade spoons, forks and knives that are grease- and water-resistant but not covered with plastic coatings.
The global food packaging market is evolving as consumer expectations, sustainability concerns, and technological advancements redefine the way food is kept safe, secure, and delivered. Packaging is no longer merely a container; it has transformed into a critical enabler that drives purchase decisions, improves product shelf life, and communicates brand values. As demand for ready-to-eat, convenience, and packaged foods grows, packaging has emerged to convey sustainability, safety, and innovation.
Aluminum foil is a flexible, thin, and extremely versatile aluminum sheet that has gained universal application in different industries owing to its superior barrier, thermal, and mechanical characteristics. Usually made by rolling aluminum slabs or ingots into extremely thin sheets, aluminum foil is 0.006 mm to 0.2 mm thick.
Glass bottles are rigid, non-porous, and chemically inert packages commonly employed in the packing of beverages, foods, drugs, cosmetics, and specialty chemicals. Constructed mainly from silica sand, soda ash, and limestone, glass bottles are prized for their preservation of product purity, inhibition of chemical leaching, and retention of flavor character.
The corrugated box industry is powered by its versatility, strength, and sustainability, rendering it crucial for shipping, storage, and retail packaging. Crafted from kraft paper, the boxes are strong, cushioned, and protective, serving e-commerce, food & beverage, electronics, and pharmaceuticals industries. Online retailing demand, sustainability drives, and innovation in packaging are driving the growth of the market.
Aluminium cans are common packaging solutions in the food, beverage, and industrial sectors because they are strong, lightweight, and highly recyclable. They ensure product freshness by shielding contents from light, air, and pathogens thanks to their exceptional barrier qualities. Because of its limitless recyclability and little environmental impact, aluminium cans have become the favoured option as sustainability awareness has grown.