Sodium-Ion Battery Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
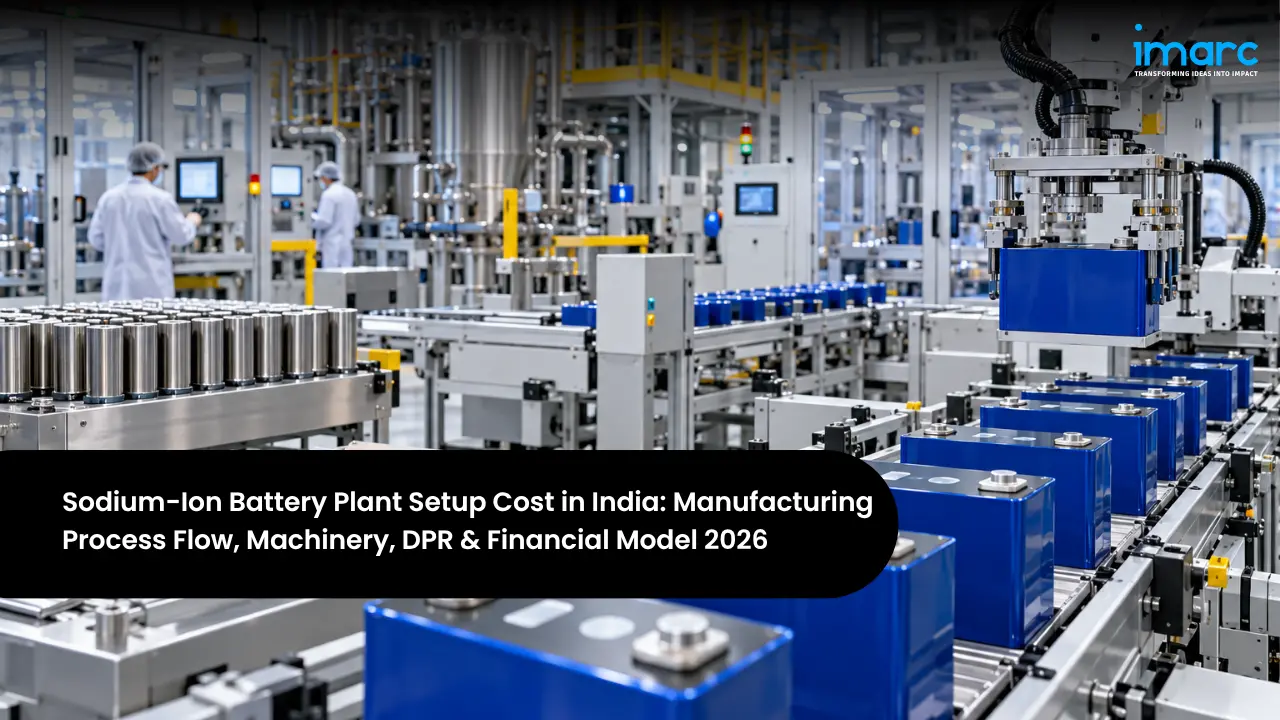
Sodium-ion batteries are emerging as a practical complement to lithium-ion technology. They work on the same principle, shuttling ions between a cathode and an anode, but use sodium, which is abundant, inexpensive, and available within India, in place of lithium. They also avoid cobalt and nickel, and use aluminium instead of copper as the anode current collector. That makes them attractive for energy storage systems, two- and three-wheelers, backup power, and low-temperature applications where cost, safety, and supply security matter more than maximum energy density. For India, which imports almost all its lithium and battery cells, a Sodium-Ion Battery Manufacturing Plant Setup in India offers a route to battery production built on a more domestic raw material base.
Investment depends above all on capacity, chemistry, and cell format, and on how much of the materials chain the plant makes itself. Sodium-ion cells can be produced on equipment very similar to lithium-ion lines, with dry rooms, precision coating, and formation systems, so capital needs are substantial. The Sodium-Ion Battery Manufacturing Plant Cost ranges from about INR 150 crore for a pilot line of a few hundred MWh to INR 2,000–5,000 crore for a commercial plant of 2 to 5 GWh. Cathode materials, hard carbon, electrolyte, and separators account for most of the operating cost, and energy is the next largest item. Yield, material sourcing, and customer adoption are therefore the decisions that shape profitability. At stable operations, a well-run plant can deliver a gross margin of 30 to 40% and a net profit margin of 12 to 18%, with payback typically within 4 to 7 years.
This guide is written for investors trying to understand how to start a Sodium-Ion Battery manufacturing plant in India. It covers the main chemistries and cell formats and their markets, the demand outlook, the production process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, the approvals involved, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Global Sodium-Ion Battery Market (2025) | USD 600.9 Million |
| Projected Global Market (2033) | USD 1,426.5 Million, 11.6% CAGR |
| Leading Region | Asia Pacific, about 42% share |
| Typical Energy Density | 100–160 Wh/kg |
| Indicative Total Investment | INR 150–5,000 Crore (pilot to 5 GWh) |
| Typical Payback Period | 4–7 Years |
The snapshot shows a young but fast-growing market in which Asia Pacific leads, driven by cost sensitivity and supply security. Sodium-ion stores less energy per kilogram than lithium-ion, so it competes best where weight matters less, such as stationary storage, two- and three-wheelers, and backup power, and where safety, low-temperature performance, and material cost matter more. India does not yet have a published standalone market size for sodium-ion, and commercial production is still at an early stage. The wide investment range reflects a genuine choice between a pilot or demonstration line to prove cells with customers and a commercial plant serving energy storage and mobility buyers at scale. The sections below work through that choice.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Sodium-ion cells in cylindrical, prismatic, or pouch formats |
| Total Project Investment | INR 150 – 5,000 Crore (capacity-dependent) |
| Payback Period | 4 – 7 Years |
| Net Profit Margin | 12 – 18% |
| IRR | 14 – 20% |
| Preferred States | Gujarat, Maharashtra, Tamil Nadu, Karnataka, Telangana, Uttar Pradesh |
| Key Approvals | Environmental clearance, SPCB consents, BIS where applicable, EPR under battery waste rules |
| Key Requirement | Proven cell technology, material supply, and customer qualification |
These ranges provide a realistic frame for early planning, but actual returns depend on chemistry and format, technology partner terms, cathode and hard carbon costs, yield during ramp-up, and how quickly storage and mobility customers adopt the technology. A site-specific Sodium-Ion Battery Feasibility Report narrows each of these assumptions to your chosen chemistry, format, customers, location, and capacity.
Table of Contents
- What is Sodium-Ion Battery Manufacturing?
- Why is Sodium-Ion Battery Manufacturing Growing in India?
- Sodium-Ion Battery Manufacturing Process Flow
- Raw Materials Required for Sodium-Ion Battery Manufacturing
- Location, Land & Infrastructure
- Sodium-Ion Battery Manufacturing Machinery and Equipment
- Sodium-Ion Battery Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Sodium-Ion Battery Manufacturing in India
- Recent Developments in the India Sodium-Ion Battery Manufacturing Industry
- How a Sodium-Ion Battery Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Sodium-Ion Battery Manufacturing?
A sodium-ion battery stores energy by moving sodium ions between a cathode and an anode through a liquid electrolyte, with a porous separator keeping the two electrodes apart. Cathodes are typically layered metal oxides, polyanionic compounds, or Prussian blue analogues, while the anode is usually hard carbon, which can be made from biomass such as coconut shells or other agricultural residues. Manufacturing covers electrode production, cell assembly, and formation and testing, following much the same sequence as lithium-ion cell making but with different materials, formation protocols, and in many cases water-based anode processing.
Commercially, the business targets applications where cost, safety, and supply security outweigh the need for the highest energy density. A Sodium-Ion Battery Manufacturing Plant can supply battery energy storage system integrators, electric two- and three-wheeler makers, telecom and UPS providers, inverter and home backup brands, and industrial users who need batteries that perform well in heat and cold. Because the technology is newer, early customers usually test and qualify cells in pilot deployments before committing to volume orders.
- Energy Storage: Cells for grid, commercial, and residential storage systems paired with solar and wind.
- Two & Three-Wheelers: Cost-effective cells for urban electric mobility and fleet vehicles.
- Telecom, UPS & Inverters: Safe, long-life replacements for lead-acid backup batteries.
- Low-Temperature & Industrial Uses: Batteries for cold regions, start-stop systems, and industrial equipment.
The Main Sodium-Ion Chemistries and Formats
Choosing the cathode chemistry and cell format is the most important commercial decision, because it determines technology partners, materials, machinery, and customers:
| Chemistry / Format | Description | Key Property | Primary Demand |
|---|---|---|---|
| Layered Oxide Cathode | Sodium transition-metal oxides | Higher energy density | Mobility and storage |
| Polyanionic Cathode | Phosphate-based compounds such as NVP | Long cycle life and stability | Storage and industrial |
| Prussian Blue Analogues | Low-cost framework materials | Low cost and fast charging | Storage and backup power |
| Cylindrical Cells | Standard round formats | Mature, automated production | 2W, tools, backup packs |
| Prismatic & Pouch Cells | Large-format rectangular or pouch | Good pack integration | Energy storage and EVs |
These choices shape the whole plant. Layered oxides offer the best energy density for mobility, polyanionic materials favour long life for storage, and Prussian blue analogues promise the lowest cost. Many Indian projects are expected to begin with a pilot or demonstration line producing one chemistry in a standard format for energy storage and backup applications, then scale up as cells are qualified, costs fall, and customers commit to larger volumes.
Why is Sodium-Ion Battery Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
Demand is supported by the growth of renewable energy, the electrification of transport, and the need to reduce dependence on imported lithium:
- Energy storage growth: Rising solar and wind capacity requires large, low-cost battery storage for grid stability.
- Supply security: Sodium is abundant and India has a large soda ash industry, reducing reliance on imported lithium, cobalt, and nickel.
- Cost and safety: Cheaper materials, aluminium current collectors, and good thermal stability suit price-sensitive applications.
- Climate suitability: Good performance across a wide temperature range suits Indian heat and cold regions.
- Policy support: Advanced cell manufacturing incentives and state battery policies encourage domestic production.
India-Specific Market Opportunity
| Segment | India Market Context | Manufacturing Role |
|---|---|---|
| Grid & Renewable Storage | Large storage tenders and solar growth | Long-life prismatic storage cells |
| Electric Two & Three-Wheelers | Largest EV segment by volume | Cost-effective mobility cells |
| Telecom & Data Backup | Lead-acid replacement across towers and sites | Safe backup power cells |
| Home Inverters & UPS | Large replacement market | Low-cost, durable cells |
The strongest early opportunity lies in energy storage and backup power, where sodium-ion's lower energy density matters least and its cost, safety, and temperature tolerance matter most. Securing pilot deployments with storage integrators, telecom operators, or inverter brands, and converting them into long-term supply agreements, is the most reliable way to build volumes while the technology matures.
Sodium-Ion Battery Manufacturing Process Flow
Understanding the process helps you plan machinery, dry room area, and where yield and cost are decided. Production follows a continuous, highly automated sequence from electrode manufacturing through cell assembly to formation and testing. Moisture and contamination must be tightly controlled, so assembly and filling take place in dry rooms.
The Sodium-Ion Battery Manufacturing Process Flow
The sequence below reflects prismatic and cylindrical cell production. Pouch lines follow the same electrode steps but use stacking and laminated pouch sealing. A key difference from lithium-ion is that both electrodes use aluminium foil, and the hard carbon anode is often processed with water-based binders.
| Unit Operation | Key Activity |
|---|---|
| Material Preparation & Mixing | Cathode, hard carbon, binders, and additives mixed into slurries |
| Electrode Coating & Drying | Slurries coated on aluminium foil and dried |
| Calendering | Electrodes pressed to precise thickness and density |
| Slitting & Vacuum Drying | Electrodes cut to width and dried to remove moisture |
| Winding or Stacking | Cathode, separator, and anode assembled into a cell core |
| Tab Welding & Casing | Tabs welded and core inserted into can or pouch |
| Electrolyte Filling & Sealing | Sodium-salt electrolyte injected and cell sealed |
| Formation | First controlled charge cycles to build the interface layer |
| Ageing & Degassing | Cells rested, monitored, and degassed where needed |
| Grading, Testing & Packing | Capacity, resistance, and safety checks before dispatch |
Two factors decide profitability across this flow. The first is yield: pilot sodium-ion lines often start with yields of around 60 to 80%, well below mature lithium-ion plants, and every rejected cell carries the full cost of its materials, so process control and inline inspection are critical. The second is energy use, because coating, drying, dry rooms, and formation consume large amounts of power; water-based anode processing, heat recovery, and energy-regenerative formation equipment help reduce operating cost.
Raw Materials Required for Sodium-Ion Battery Manufacturing
The main inputs are cathode active materials, hard carbon for the anode, a sodium-salt electrolyte such as NaPF6, separator film, aluminium foil for both electrodes, binders and conductive additives, and cans, casings, pouches, and tabs. Because materials make up most of the cost and their quality directly sets cell performance, a qualified and stable supplier base is central to project planning.
| Raw Material | Role in Cell | India Sourcing | % of OpEx |
|---|---|---|---|
| Cathode Active Material | Stores sodium, sets energy density | Largely imported; local synthesis possible | 22–30% |
| Hard Carbon Anode | Hosts sodium during charging | Imported; biomass-based local production emerging | 10–14% |
| Electrolyte (NaPF6-based) | Carries sodium ions | Largely imported | 7–10% |
| Separator | Keeps electrodes apart safely | Largely imported | 5–8% |
| Aluminium Foil | Current collector for both electrodes | Domestic and imported | 3–5% |
| Cans, Casings, Tabs & Binders | Housing and connections | Domestic and imported | 4–6% |
Sodium-ion's material base is one of its strongest advantages in India. Sodium precursors such as soda ash are produced domestically at scale, aluminium is available locally, and hard carbon can be made from agricultural residues such as coconut shells and rice husk. Supply chains for battery-grade cathode materials, hard carbon, and electrolytes are still small, however, so early plants often import them. A phased localisation plan, including local cathode synthesis or hard carbon production, can improve margins and supply security as volumes grow.
Location, Land & Infrastructure
Site selection for a sodium-ion plant is shaped by access to reliable power, proximity to energy storage and mobility customers, access to sodium precursors and biomass for hard carbon, port access for imported materials and equipment, availability of engineers and technicians, and state incentives. Water supply and room for future expansion are also important.
Choosing the Best Location for Sodium-Ion Battery Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Gujarat (Jamnagar, Sanand & Bharuch) | Battery gigafactory and soda ash base | Precursors, ports, and incentives |
| Maharashtra (Pune region) | Battery technology and automotive hub | Talent, R&D, and customers |
| Tamil Nadu (Chennai & Krishnagiri) | EV and electronics manufacturing hub | Customers, ports, and biomass |
| Karnataka (Bengaluru region) | Battery and energy technology base | Talent and start-up ecosystem |
| Telangana (Hyderabad region) | Growing battery manufacturing corridor | Land, power, and incentives |
| Uttar Pradesh & NCR | Large North Indian demand centre | Proximity to inverter and EV markets |
Gujarat stands out because it combines India's largest soda ash producers, major battery investments, ports, and strong industrial policy. Maharashtra and Karnataka offer battery technology talent and research partners, Tamil Nadu brings EV customers and biomass for hard carbon, and Telangana and Uttar Pradesh offer land, incentives, and access to large regional markets. The final choice should weigh power availability and tariffs, incentives, customer proximity, and material logistics.
Quality, Safety and Technology Partnerships
Cell quality depends on consistent materials, tightly controlled processes, and rigorous testing of capacity, internal resistance, cycle life, and safety under abuse conditions. Because sodium-ion is a newer technology, performance data, standards, and customer specifications are still evolving, which makes independent testing and transparent data especially important for winning customer trust. Most new entrants license technology or partner with a developer that has proven chemistry. An experienced Sodium-Ion Battery Manufacturing Consultant in India can help evaluate technology partners, plan dry room and quality systems, and prepare the plant for customer qualification.
Infrastructure Requirements (1–2 GWh Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 15 – 50 acres | Room for phased capacity expansion |
| Electrode Production Hall | Clean, temperature-controlled area | Long coating lines need large bays |
| Dry Rooms | Low-humidity assembly and filling areas | Energy-intensive dehumidification |
| Formation & Ageing Area | Large racks with fire protection | Strict fire safety design |
| Utilities & Solvent Handling | Chillers, compressed air, solvent recovery | Lower solvent load with aqueous anodes |
| Power Requirement | 10 – 40 MW | Reliable, preferably renewable supply |
| Testing & R&D Laboratory | Cell testing and material analysis | Core to customer qualification |
Dry rooms, electrode coating lines, formation areas, and a strong testing laboratory are the defining infrastructure needs. Power reliability is critical because interruptions can scrap material in process, and renewable power agreements can lower both cost and carbon footprint. Fire safety design for formation, ageing, and storage areas should be planned from the start, even though sodium-ion cells are generally considered to have a good safety profile.
Sodium-Ion Battery Manufacturing Machinery and Equipment
The equipment set covers electrode manufacturing, cell assembly, formation and testing, and supporting utilities. Much of it is the same type of equipment used for lithium-ion cells, which allows proven suppliers to be used, though settings, drying conditions, and formation protocols are adapted to sodium-ion materials. The main items are summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Slurry Mixers | Mix cathode and anode slurries | Planetary or continuous mixing |
| Coating & Drying Machines | Coat electrodes and dry them | Precise coating weight and long ovens |
| Solvent Recovery System | Recover cathode processing solvent | High recovery efficiency |
| Calendering Machines | Press electrodes to target density | Tight thickness control |
| Slitting & Notching Machines | Cut electrodes to size | Burr-free cutting, laser or die |
| Vacuum Drying Ovens | Remove residual moisture | Controlled temperature and vacuum |
| Winding or Stacking Machines | Assemble cell cores | High speed and alignment accuracy |
| Tab & Laser Welding Systems | Weld tabs and seal cans | Ultrasonic and laser welding |
| Electrolyte Filling & Sealing Machines | Fill and seal cells | Operated inside dry rooms |
| Formation, Ageing & Grading Systems | Condition, test, and sort cells | Energy-regenerative cyclers |
| Dry Room & Dehumidification Units | Maintain low humidity | Stable dew point control |
Machinery should follow the chemistry, format, and capacity plan. A pilot line prioritises flexibility for process development and customer samples, while a commercial line prioritises speed, automation, and yield. Integrated manufacturing execution systems, inline vision inspection, and energy-regenerative formation equipment improve yield and reduce cost, and because sodium-ion lines resemble lithium-ion lines, some plants design for flexibility to produce both chemistries.
Sodium-Ion Battery Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a commercial-scale sodium-ion facility in India. The final Sodium-Ion Battery Investment Cost for your project will depend on capacity, chemistry and format, the equipment and technology partner chosen, whether cathode or hard carbon is made in-house, the extent of dry room and utility infrastructure, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 50–60% | Electrode, assembly, formation, and test lines |
| Dry Rooms, Clean Areas & MEP | 10–15% | Dehumidification, HVAC, and fire systems |
| Land & Buildings | 10–15% | Production halls, warehouses, and offices |
| Utilities & Solvent Recovery | 4–7% | Power, chillers, water, and solvent systems |
| IT, MES & Testing Laboratory | 3–6% | Traceability, process control, and cell testing |
| Technology, Pre-operative & Contingency | 6–10% | Licensing, DPR, validation, and buffer |
| Working Capital | 5–8% | Materials and receivables |
Machinery dominates the capital budget, and much of it is imported, so currency movements and supplier lead times affect project cost and schedule. Because customer adoption of sodium-ion is still building, phasing capacity is especially important. A detailed Sodium-Ion Battery Business Plan should model a pilot or first phase, ramp-up yields, technology fees, incentives, and customer qualification timelines together, so that funding matches the real path from trial production to profitable volume.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials (cathode, hard carbon, electrolyte, separator, foil) | 60–70% | Local sourcing can lower costs over time |
| Utilities (power, dry rooms, water) | 15–20% | Coating, drying, and formation are energy-intensive |
| Labour & Technical Staff | 4–7% | Engineers and trained operators |
| Maintenance & Spares | 2–4% | Imported spares for specialised equipment |
| Quality, Testing & Scrap Handling | 2–4% | Higher during ramp-up |
| Logistics & Overheads | 1–3% | Import handling and administration |
With materials making up most of the cost and utilities the next largest item, margins depend on material pricing, production yield, and energy efficiency. A good operating model tracks cost per kWh, yield at each process stage, energy use per kWh, and scrap rates, and tests how margins respond when material prices move, when yields improve more slowly than planned, or when lithium-ion prices fall and narrow sodium-ion's cost advantage.
Financial Analysis and Profitability
Based on analysis of a commercial-scale sodium-ion facility, the financial profile is attractive at stable operation, supported by lower material costs and supply security, but depends heavily on ramp-up and market adoption. The profitability of Sodium-Ion Battery manufacturing business in India improves markedly with high yields, long-term storage and mobility contracts, incentives, and localisation of cathode and hard carbon materials.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 30–40% | Higher with good yields and local materials |
| Net Profit Margin | 12–18% | After depreciation and Indian corporate taxes |
| Payback Period | 4–7 Years | Faster with quick ramp-up and offtake |
| IRR (Internal Rate of Return) | 14–20% | Higher with incentives and localisation |
| Capacity Utilization (stable ops) | 65–85% | Depends on customer adoption |
| Break-even Capacity Utilization | 50–60% | High fixed costs and depreciation |
Yield, utilisation, and pricing against lithium iron phosphate cells decide where a plant lands within these ranges. A plant that ramps up slowly or cannot fill capacity can make losses in its early years, while one that reaches target yields quickly and sells most of its output under long-term agreements can earn healthy returns. Because sodium-ion competes directly with LFP in storage and mobility, its cost advantage must be maintained as lithium prices move.
Returns can be strengthened by choosing a proven technology partner, starting with a well-sized first phase, securing pilot deployments that convert into volume orders, localising cathode and hard carbon supply, capturing PLI and state incentives, and investing in energy-efficient equipment. Consistent performance data and safety records are what earn trust from storage developers and vehicle makers.
Key Risks and Mitigation
The main risks are technology and ramp-up risk, slower-than-expected market adoption, competition from falling lithium-ion prices, immature material supply chains, and evolving standards. Technology risk is reduced through experienced partners and pilot validation; market risk by early customer agreements and a focus on storage and backup applications; price risk by continuous cost reduction and localisation; and standards risk by independent testing and certification. Promoters often work with a Sodium-Ion Battery Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for Sodium-Ion Battery Manufacturing in India
Approvals for a sodium-ion plant combine environmental and industrial clearances with hazardous material, fire safety, and product certification requirements. Promoters setting up a Sodium-Ion Battery Manufacturing Plant in India generally need the following:
- Environmental Clearance: Environmental clearance from the state or central authority where applicable, based on project scale and category.
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, covering solvent emissions and effluents.
- Hazardous Materials & Waste: Hazardous waste authorisation and, where applicable, PESO approval for solvent and flammable material storage.
- Product Certification: BIS and automotive certification where applicable to the target application, as standards for sodium-ion cells continue to evolve.
- Battery Waste Management Rules: Extended Producer Responsibility registration for batteries placed on the market.
- Factory, Fire & Business Registrations: Factory license, Fire NOC, GST, Udyam, IEC for imports and exports, and EPF and ESI registrations.
- Incentive Approvals: PLI and state incentive approvals where the project is eligible.
Environmental clearance, pollution consents, and fire approvals are usually on the critical path for construction and start-up, while product certification and customer qualification take place during trial production. Because standards for sodium-ion are still developing, early engagement with testing laboratories and certification bodies helps avoid delays in reaching commercial sales.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, chemistry, cell format, target applications, export markets, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Sodium-Ion Battery Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- Reliance and Faradion: Reliance acquired UK-based sodium-ion developer Faradion in 2022 and plans to use sodium-ion alongside LFP at its Jamnagar battery gigafactory, with an early focus on energy storage.
- KPIT and Trentar partnership: In February 2025, KPIT Technologies selected Trentar Energy Solutions to commercialise its sodium-ion technology, with plans for a 3 GWh manufacturing facility.
- Global market growth: The global sodium-ion battery market reached about USD 600.9 million in 2025 and is expected to grow at about 11.6% a year to 2033.
- Global commercialisation: Leading international cell makers have begun commercial sodium-ion production for storage and vehicles, helping build supply chains and customer confidence.
The common thread is a technology moving from research into early commercial production, with India's largest groups and technology companies taking positions. New entrants who secure proven technology, early customers, and a phased investment plan will be best placed as sodium-ion gains ground in storage and mobility through the decade.
How a Sodium-Ion Battery Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from market demand and chemistry selection to plant design, machinery, technology partnerships, and economics. It helps investors decide the right chemistry, format, and phasing, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Sodium-Ion Battery Financial Model covering revenue by application and customer segment, material cost per kWh, ramp-up yields, energy and utility costs, incentives, working capital, cash flows, break-even, return on investment, and payback. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a Sodium-Ion Battery Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a sodium-ion project, a strong DPR also clarifies the technology partnership, the material localisation roadmap, the phasing from pilot to commercial scale, and the customer adoption strategy, which together are the factors most likely to decide success. By modelling ramp-up realistically and testing margins against LFP price competition, yield shortfalls, and delays, the report turns an emerging-technology opportunity into a plan that lenders and partners can trust.
Frequently Asked Questions
What are the first steps to set up a sodium-ion battery manufacturing plant in India?
Start by choosing your chemistry, cell format, capacity, and target applications, and identify a technology partner. Then commission a feasibility study and DPR, secure land with reliable power in a supportive state, obtain environmental and pollution clearances, build electrode halls, dry rooms, and formation areas, install production lines, recruit and train technical staff, and begin customer qualification and product certification.
How much does it cost to set up a sodium-ion battery manufacturing plant in India?
Investment ranges from about INR 150 crore for a pilot line of a few hundred MWh to INR 2,000–5,000 crore for a commercial plant of 2 to 5 GWh, depending on chemistry, format, equipment, and infrastructure. Process equipment, dry rooms, and utilities are the largest components.
What are the main steps in sodium-ion battery manufacturing?
The flow runs from material preparation and slurry mixing through electrode coating and drying, calendering, slitting and vacuum drying, winding or stacking, tab welding and casing, electrolyte filling and sealing, formation, ageing and degassing, and final grading, testing, and packing.
Which machinery does a sodium-ion battery manufacturing plant need?
Key equipment includes slurry mixers, coating and drying machines, solvent recovery systems, calendering machines, slitting and notching machines, vacuum drying ovens, winding or stacking machines, tab and laser welding systems, electrolyte filling and sealing machines, formation, ageing, and grading systems, and dry room dehumidification units.
What raw materials are used to make sodium-ion batteries?
The main inputs are cathode materials such as layered oxides, polyanionic compounds, or Prussian blue analogues, hard carbon for the anode, sodium-salt electrolyte, separator film, aluminium foil for both electrodes, binders and conductive additives, and cans, casings, pouches, and tabs.
How profitable is sodium-ion battery manufacturing in India?
At stable operation, a well-run plant typically earns a 30 to 40% gross margin and a 12 to 18% net margin, with payback in about 4 to 7 years. Profitability depends heavily on yields, utilisation, customer adoption, and pricing against lithium iron phosphate cells, and the ramp-up period can be loss-making.
Which approvals does a sodium-ion battery manufacturing plant need in India?
Typical approvals include environmental clearance where applicable, State Pollution Control Board consents, hazardous waste authorisation, PESO approval where applicable, BIS or automotive certification where applicable, EPR registration under the Battery Waste Management Rules, a factory license and Fire NOC, and GST, Udyam, IEC, and labour registrations.
How do I get a feasibility study or DPR for a sodium-ion battery manufacturing project?
A detailed feasibility study and DPR covers market demand, chemistry and format strategy, technology partners, plant design, approvals, and full financials. Investors usually engage a Sodium-Ion Battery Manufacturing Feasibility Study Consultant with experience in battery and advanced manufacturing projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Few industries in India have scaled as quickly as solar manufacturing. Backed by ambitious renewable energy targets, a rooftop programme for households, import duties on foreign modules, and the Approved List of Models and Manufacturers (ALMM), domestic module capacity has multiplied in just a few years.
Setting up an Electrical Panel Manufacturing Plant in India is a fabrication-and-assembly venture powered by heavy grid modernisation, a fast-growing renewable-energy build-out, rising industrial and commercial construction, and the spread of automation across factories and buildings.
Saudi Arabia has turned its power transition into one of the world's largest procurement programmes, and international developers, lenders, and equipment makers are following the tenders.
Setting up a Battery Manufacturing Plant in India is a high-demand, energy-driven venture, powered by the country's booming automotive sector, huge power-backup market, and the fast-growing shift to electric vehicles and renewable storage.
Setting up a Liquefied Natural Gas (LNG) Manufacturing Plant in India is a capital-intensive, strategically important venture, powered by the country's push toward a gas-based economy, the shift to cleaner fuels in transport and industry, and rising demand for LNG as a truck, bus, and industrial fuel.
The India carbon credit market is moving from a voluntary, project-by-project trade into a regulated national system with binding targets, a central registry, and exchange-based price discovery. According to IMARC Group, the market was valued at USD 33.69 Billion in 2025, grew to USD 44.42 Billion in 2026, and is projected to reach USD 405.47 Billion by 2034, expanding at a CAGR of 31.84% (2026–2034).
Setting up a Syngas Production Plant in India is a capital-intensive but strategically valuable venture, driven by the country's push for cleaner industrial fuels, coal and biomass utilization, and chemical self-reliance. Syngas, or synthesis gas, is a mixture of hydrogen and carbon monoxide produced by gasifying carbon-rich feedstocks, and it serves as a versatile building block for power, chemicals, hydrogen, and synthetic fuels. With abundant biomass, coal, and waste feedstock and growing policy support for gasification, India offers a favourable environment for new plants.
Setting up a Battery Energy Storage System Manufacturing Plant in India is a capital-efficient, high-growth venture, driven by the country's renewable energy expansion, grid modernization, and supportive storage policies. As solar and wind capacity scales up and the grid needs to balance variable generation, battery energy storage systems have become essential infrastructure.
Setting up a Lithium-ion Battery Recycling Plant in India is a capital-intensive but high-potential venture. India's rapid rise as a major electric-vehicle market, its large consumer-electronics base, and its fast-growing energy-storage sector are together creating one of the deepest and fastest-expanding pools of end-of-life lithium-ion batteries in the world.
Solar glass is a type of specialty glass that has high transmittance and is designed exclusively for use in solar energy systems. Unlike regular flat glass, solar glass is designed to have maximum light transmission with minimal losses due to reflection and absorption.
A solar inverter is a vital component in solar photovoltaic (PV) systems, responsible for transforming the direct current (DC) electricity produced by solar panels into alternating current (AC) electricity. This AC power is then suitable for use by the electrical grid, various appliances, and industrial equipment.
Australia has firmly established itself as a dominant force in the global liquefied natural gas (LNG) market, maintaining its position as one of the world's leading exporters. The country's strategic geographical location in the Asia-Pacific region, combined with substantial natural gas reserves, has enabled it to become a critical energy supplier to rapidly growing Asian economies, particularly China, Japan, and South Korea.
Japan's lead acid battery market stands as a cornerstone of the nation's energy storage infrastructure, demonstrating remarkable resilience and adaptability in an era dominated by rapid technological evolution. Despite the global shift toward lithium-ion technologies, the Japanese lead acid battery sector continues to thrive, driven by its unmatched cost-effectiveness, proven reliability, and exceptional recyclability.
Green hydrogen is the cleanest form of hydrogen available, as it is produced through water electrolysis using the electricity generated from renewable energy sources such as solar, wind, or hydropower. Carbon dioxide emissions are zero since no fossil fuels are used. Essentially, an electrolyzer is used in the electrolysis process to split water molecules into hydrogen and oxygen. The resulting hydrogen is refined by purification, compression, or liquefaction and then fed into various applications. Green hydrogen is considered a cornerstone of the global energy transition because it can store renewable energy, decarbonize hard-to-abate sectors, and serve as a sustainable alternative to fossil-fuel-based hydrogen.
Japan’s thermal power plant industry remains a crucial pillar of the nation’s energy infrastructure, providing a stable and reliable source of electricity for both industrial and residential consumption. Thermal power generation, which primarily involves the combustion of fossil fuels such as coal, natural gas, and oil, continues to play a key role despite increasing investments in renewable energy.
An electrical panel, also called a distribution board or switchboard, is an important installation in electrical infrastructure that acts as the main center for the distribution, control, and protection of electrical power within residential, commercial, and industrial systems. It acts as the point at which electrical energy is received from the utility or a source of power generation and is distributed to various circuits and equipment in an organized manner.
The global oil and gas EPC market is currently experiencing a remarkable transformation as it positions itself at the intersection of traditional energy demands and technological innovation. As of 2024, the market is demonstrating robust growth, reaching USD 52.9 Billion in 2024, depending on regional scope and market segmentation approaches. This substantial market base is supporting a major number of capital projects worldwide, including offshore platform projects and onshore installations that are collectively shaping the energy landscape.
Bamboo pellets are a biomass fuel type created through the compression of bamboo residues like shavings, sawdust, and chips into thick cylindrical pellets. They are an environmentally friendly substitute for conventional fossil fuels like natural gas and coal. Due to the fast growth rate and high biomass yield of bamboo, it has become one of the most renewable raw materials for the production of bioenergy.
Biomass briquettes are dense, solid fuel blocks made of compressed organic waste materials like sawdust, agricultural wastes, wood shavings, coconut shells, rice husk, or herbaceous biomass. The briquetting process usually involves drying the biomass to lower the moisture content (usually down to 10-15%), grinding or milling for a fine particle size uniformity, and then compressing under high pressure with or without a binding agent.
Biogas is a renewable energy form generated by the anaerobic fermentation of organic matter including agricultural residues, animal waste, municipal solid waste, sewage sludge, and food waste. Microorganisms in the absence of oxygen break down organic substances in the process and produce a gaseous mixture of mainly methane (CH4) and carbon dioxide (CO2), with traces of hydrogen sulfide (H2S) and water vapor.
A battery is an electrochemical energy storage system that transforms chemical energy into electrical energy by way of redox reactions between its electrodes and electrolyte. It consists of a single or multiple electrochemical cells, each having a positive electrode (cathode), a negative electrode (anode), and an electrolyte for ion transfer. Batteries are categorically divided into primary (non-rechargeable) and secondary (rechargeable) types.
The global energy landscape is undergoing a seismic transformation, with green hydrogen emerging as one of the most promising solutions to achieve deep decarbonization across sectors. Far from a niche technology, green hydrogen is emerging as a critical pillar of the future energy system, offering a pathway to a sustainable and resilient economy.
Transmission line towers are essential support components of transmission lines installed on overhead to distribute high-voltage electricity over long distances. Towers are made of galvanized steel, primarily, and are designed to tolerate mechanical stress, environmental loads, and electrical safety. Some of the important characteristics of transmission line towers are high structural strength, corrosion resistance, adaptability for modular design, and high service life. They are normally produced in lattice form (tubular or free-standing towers) or tubular form, with types including suspension towers, tension towers, angle towers, and terminal towers based on use.
The energy storage revolution is here, and it's powered by graphene. While the world struggles with the limitations of conventional lithium-ion batteries, a new technology is emerging that promises to shatter every performance barrier we've accepted as unchangeable.
Australia is undergoing a significant energy transformation, underscoring the growing role of renewable energy sources. These sources are key to combating climate change by reducing greenhouse gas emissions, the primary cause of global warming and air pollution. Beyond environmental benefits, renewable energy strengthens energy security by diversifying power sources and reducing dependence on volatile fossil fuel imports, contributing to greater energy independence.
Learn how to plan capital investment, manage raw material costs, post manufacturing cost and optimize operations for setting up solar panel plant.
Battery Energy Storage System (BESS) represents a power grid technology that stores electricity to enhance electric power grid reliability while increasing operational efficiency. BESS permits battery recharging during periods of low demand or extra grid supply capacity. BESS provides three principal operational functionalities which include power grid stabilization during supply disruptions, control of energy supply variations, and integration of intermittent renewable generation from wind and solar resources.
China's economic presence is expanding globally, and Latin America and the Caribbean (LAC) have become a focal point for its investments, especially within the energy sector. The region, rich in natural resources and experiencing rising energy demands, offers strategic opportunities for Chinese energy giants looking to invest and expand. LAC is currently leading a transformative movement towards sustainable energy. From 2015 to 2022, the region increased its renewable energy capacity by an impressive 51%, now generating 64% of its electricity from renewables such as hydropower, wind, and solar. This shift addresses the global demand for cleaner energy while supporting local economic growth and enhancing energy security.
Hydrogen is a clean, renewable, and widely available energy source that can be produced through various methods. Production techniques such as coal gasification, steam methane reforming, electrolysis, and thermochemical processes highlight its versatility. Hydrogen is essential in several critical sectors, including methanol and ammonia production, petroleum refining, transportation, power generation, as well as in electronics, metal industries, and as a rocket propellant. The increasing concern over carbon emissions and greenhouse gases has led to a shift towards cleaner fuel options. Hydrogen is recognized for its cleanliness and versatility as an energy carrier. Additionally, supportive government initiatives and favorable policies are driving the growth of hydrogen production globally.
Hydrogen is a clean, renewable, and abundant energy source derived from various methods. Its applications span across transportation, heating, and power generation. Diverse production methods, including coal gasification, steam methane reforming, electrolysis, and thermochemical processes, contribute to its versatility. Hydrogen plays a pivotal role in crucial sectors like methanol and ammonia production, petroleum refining, transportation, power generation, as well as in electronics, metal industries, and as a rocket propellant.
A floating solar farm is a renewable energy installation in which solar panels are mounted on floating structures in water bodies such as lakes, reservoirs, ponds, or even the sea. This technology, also known as a floating photovoltaic (PV) system, or “floatovoltaics,” enables solar power generation in areas with limited available land or where land use is restricted for other purposes. Floating solar farms offer various benefits, including improved solar panel efficiency through cooling, land conservation, reduction of evaporation and algae growth, and integration with hydropower facilities to generate both solar and hydroelectric power in the same location.
Nuclear power utilizes nuclear reactions to generate heat, which is then converted into electricity. This energy is released from the nucleus—the core of atoms composed of protons and neutrons. Nuclear power can be derived from nuclear fission, nuclear decay, and nuclear fusion reactions. Across the globe, nuclear power plants predominantly use the fission of uranium and plutonium to produce electricity. The heat generated from fission is used to create steam, which drives turbines connected to generators. Nuclear power offers several advantages over fossil fuels, such as minimal greenhouse gas emissions and a higher energy density, meaning a small amount of nuclear fuel produces a large amount of energy.