Biomass Briquettes Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
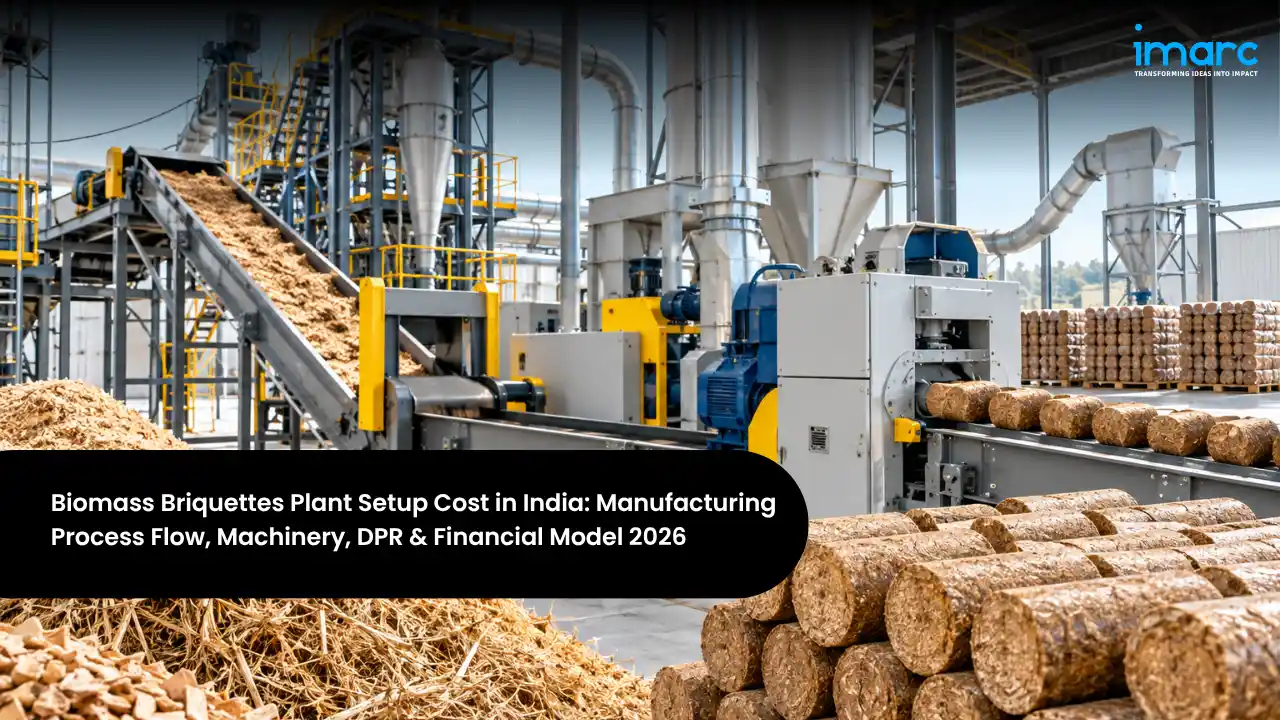
Biomass briquettes, often called white coal, are dense blocks of compressed agricultural and forestry residues that burn cleanly in industrial boilers, furnaces, and power plants. India produces hundreds of millions of tonnes of crop residues every year, much of which is burnt in fields, while industries are under pressure to replace coal and firewood with cleaner fuels. Mandatory biomass co-firing in thermal power plants, air quality rules in the NCR, and rising demand from textile, food processing, chemical, and pharmaceutical boilers are creating steady buyers for densified biomass. Together these trends make Biomass Briquettes Manufacturing Plant Setup in India an accessible and impactful opportunity in renewable fuels.
Investment depends above all on capacity, the type of residue, and how much of the collection and drying chain the plant owns. A small unit with one briquetting press near a sawmill or groundnut processing cluster is a modest project, while a plant processing paddy straw needs balers, large storage yards, dryers, and multiple presses. The Biomass Briquettes Manufacturing Plant Cost ranges from about INR 0.5–2 crore for a small unit of 1 to 2 tonnes per hour (TPH) to INR 5–15 crore for a plant of 3 to 6 TPH with drying and grinding, and INR 25–60 crore for an integrated paddy straw plant of 10 to 20 TPH with its own baling fleet and a pellet line. Raw materials make up 40 to 50% of operating cost and utilities another 25 to 35%, so residue sourcing, moisture control, and power cost shape profitability. A well-run plant typically earns a gross margin of 25 to 35% and a net margin of 10 to 15%.
This guide is written for investors exploring how to start a Biomass Briquettes manufacturing plant in India. It focuses on a plant converting agro-residues and wood waste into briquettes for industrial boilers, and also explains small sawdust units, paddy straw plants, and pellet lines for power plant co-firing. It covers products and markets, the demand outlook, the production process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, approvals, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Global Biomass Briquette Market (2025) | USD 1.14 Billion |
| Projected Global Market (2034) | USD 2.37 Billion, 8.5% CAGR |
| Thermal Power Co-firing Mandate | 5% biomass, plus 2% in NCR plants |
| Biomass Co-fired in Power Plants | 6.10 Million Tonnes (to June 2026) |
| Power Plants Using Biomass | 75 thermal power plants |
| Indicative Total Investment | INR 0.5 Crore to 60 Crore |
The snapshot shows a growing global market and an Indian market shaped strongly by policy, with power plants now using millions of tonnes of biomass and industries moving away from coal in polluted regions. Supply of reliable, quality densified biomass still lags demand in many areas. The wide investment range reflects a real choice between a small briquetting unit, a mid-sized plant with drying, and an integrated straw-based facility. The sections below work through that choice.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Agro-residue and sawdust briquettes, paddy straw briquettes, optional pellets |
| Plant Capacity | 5,000 – 30,000 Tonnes per year |
| Total Project Investment | INR 0.5 Crore (small unit) to 25–60 Crore (integrated) |
| Payback Period | 2 – 4 Years |
| Net Profit Margin | 10 – 15% |
| IRR | 18 – 25% |
| Preferred States | Punjab, Haryana, Uttar Pradesh, Gujarat, Maharashtra, Madhya Pradesh |
| Key Requirement | Assured residue supply, low moisture, and long-term fuel buyers |
These ranges provide a realistic frame for early planning, but actual returns depend on residue availability and prices through the year, moisture content, power cost, the selling price relative to coal, long-term contracts with industries or power plants, and storage losses. A site-specific Biomass Briquettes Feasibility Report narrows each of these assumptions to your chosen feedstock, capacity, location, and customers.
Table of Contents
- What are Biomass Briquettes Manufacturing?
- Why is Biomass Briquettes Manufacturing Growing in India?
- Biomass Briquettes Manufacturing Process Flow
- Raw Materials Required for Biomass Briquettes Manufacturing
- Location, Land & Infrastructure
- Biomass Briquettes Manufacturing Machinery and Equipment
- Biomass Briquettes Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Biomass Briquettes Manufacturing in India
- Recent Developments in the India Biomass Briquettes Manufacturing Industry
- How a Biomass Briquettes Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What are Biomass Briquettes Manufacturing?
Biomass briquettes are cylindrical blocks, typically 60 to 90 mm in diameter, made by compressing dried and ground biomass under high pressure. The heat and pressure soften the natural lignin in the material, which binds the particles together without added glue. Briquettes are three to five times denser than loose residue, have uniform size and moisture, and deliver a calorific value of roughly 3,500 to 4,500 kcal per kg depending on the feedstock, which makes them easy to store, transport, and burn in boilers designed for coal or wood. Pellets are a smaller, denser form of the same idea, used mainly in power plants and smaller burners.
Commercially, briquettes are sold to industries that need steam or heat, either directly or through fuel traders. A Biomass Briquettes Manufacturing Plant can supply textile processing units, food and dairy plants, rice and solvent extraction mills, chemical and pharmaceutical factories, paper mills, brick kilns, hotels and laundries, and thermal power plants that co-fire biomass. Buyers value consistent calorific value, low moisture and ash, reliable supply through the year, and a price below coal or firewood on a heat basis.
- Industrial Boilers: Textile, food, dairy, chemical, and pharmaceutical plants.
- Thermal Power Plants: Co-firing with coal under national and NCR mandates.
- Process Heat Users: Brick kilns, foundries, and dryers.
- Commercial Users: Hotels, laundries, and community kitchens.
The Main Briquette Types and Applications
Choosing the feedstock and product is the most important commercial decision, because it determines machinery, drying needs, fuel quality, and customers:
| Briquette Type | Feedstock | Key Property | Primary Demand |
|---|---|---|---|
| Sawdust Briquettes | Sawdust and wood waste | High calorific value | Industrial boilers |
| Groundnut Shell Briquettes | Groundnut shells | Low moisture, high heat | Boilers in Gujarat |
| Agro-Residue Briquettes | Mustard, cotton, soybean residues | Abundant feedstock | Industrial boilers |
| Paddy Straw Briquettes | Rice straw | Reduces stubble burning | NCR industries, power plants |
| Mixed Briquettes | Blended residues | Stable year-round supply | Large industrial buyers |
| Biomass Pellets | Same residues, finer form | High density, uniform | Power plant co-firing |
These choices shape the whole plant. Sawdust and groundnut shell briquettes need little drying and command higher prices, while straw and stalk briquettes rely on abundant, cheap residue but need balers, shredders, dryers, and large storage. Paddy straw has high ash and silica content, which affects boilers, so buyers often blend it with other residues. Most new entrants therefore start with locally abundant, low-moisture residues for nearby industrial boilers, and add straw processing or pellet lines once supply chains and customers are established.
Why is Biomass Briquettes Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
Demand is supported by co-firing mandates, air quality rules, industrial fuel switching, and the need to manage crop residues:
- Power plant co-firing: Coal-based plants must co-fire 5% biomass, with an extra 2% in NCR plants, creating demand for millions of tonnes of densified biomass.
- Air quality rules: Industries in the NCR and other polluted regions must use cleaner approved fuels, favouring biomass over coal and firewood.
- Stubble burning control: Paddy straw management programmes encourage turning residues into fuel.
- Industrial decarbonisation: Companies with sustainability targets are replacing coal in boilers with biomass.
- Cost advantage: Briquettes are often cheaper than coal on a heat basis near residue-rich areas.
India-Specific Market Opportunity
| Segment | India Market Context | Manufacturing Role |
|---|---|---|
| Industrial Boilers | Large base of coal and wood users | Agro-residue and sawdust briquettes |
| Thermal Power Plants | Co-firing mandates and tenders | Briquettes and pellets |
| NCR Industries | Clean fuel requirements | Paddy straw briquettes |
| Brick Kilns & Foundries | Fuel switching from coal | Low-cost briquettes |
| Commercial Users | Hotels and laundries | Bagged briquettes |
The strongest opportunity for new entrants lies in supplying industrial boilers within a short distance of residue-rich areas, in long-term contracts with large industries that are switching from coal, and in paddy straw processing in Punjab, Haryana, and western Uttar Pradesh where policy support is strongest. Producers that secure year-round feedstock, control moisture and quality, and sign long-term supply agreements will be best placed to grow.
Biomass Briquettes Manufacturing Process Flow
Understanding the process helps you plan equipment, storage, and where cost and quality are decided. Production runs from biomass collection and baling through receipt and storage, shredding, drying, grinding, screening and blending, briquetting, cooling, and quality checks to storage and dispatch. Moisture control and particle size decide briquette strength and output, while residue cost, power, and drying fuel are the largest controllable costs.
The Biomass Briquettes Manufacturing Process Flow
The sequence below reflects a plant processing mixed agro-residues with drying. A sawdust or groundnut shell unit often skips shredding and needs little or no drying.
| Unit Operation | Key Activity |
|---|---|
| Collection & Baling | Residues gathered and baled |
| Receipt & Storage | Weighing, moisture checks, stacking |
| Shredding | Bales and stalks chopped |
| Drying | Moisture reduced to 8–12% |
| Grinding | Hammer mills reduce particle size |
| Screening & Blending | Oversize removed, residues mixed |
| Briquetting | Compressed in piston or screw press |
| Cooling | Briquettes cooled and hardened |
| Cutting & Quality Testing | Length, density, moisture checks |
| Storage & Dispatch | Covered storage, loose or bagged |
Two factors decide profitability across this flow. The first is moisture control, because wet feedstock produces weak briquettes, damages dies, and wastes energy, so good storage, drying, and incoming checks are essential. The second is press uptime and power use, since dies and rams wear quickly with abrasive residues, so maintenance, hardened parts, and well-sized grinding keep output high and power per tonne low.
Raw Materials Required for Biomass Briquettes Manufacturing
The main inputs are agricultural residues such as groundnut shells, mustard and cotton stalks, soybean husk, paddy straw, sugarcane trash, and bagasse, together with forestry and industrial residues such as sawdust and wood chips. No binder is needed in most cases. Because residues are seasonal and scattered, collection, storage, and year-round supply are central to project planning.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Agro-Residues (stalks, husks, shells) | Main feedstock | Farmers, mandis, traders | 30–38% |
| Sawdust & Wood Waste | High-energy feedstock | Sawmills, furniture units | 5–8% |
| Paddy Straw | Feedstock in rice belts | Farmers via balers | Varies |
| Collection & Freight | Baling and transport | Own fleet or aggregators | 4–6% |
| Bags & Consumables | Packing and press parts | Domestic | 1–2% |
India has abundant residues, but they are available only after harvest and spread over large areas, so supply can be tight and prices can rise late in the season. Contracts with farmer groups and aggregators, owning balers and storage, buying in season and storing under cover, blending several residues, and locating near agro-processing units that generate residues at one site help manage cost and supply risk.
Location, Land & Infrastructure
Site selection for a briquetting plant is driven by the availability of residues within a short radius, distance to industrial and power plant customers, land for large covered storage, reliable power, and state support for residue management and renewable fuels. Because residues are bulky and briquettes are low-value per tonne, short transport distances on both sides are essential. As a rule of thumb, most plants source residues within about 50 to 100 km and sell briquettes within a similar distance, so the best sites sit between agricultural belts and industrial clusters, close to good roads.
Choosing the Best Location for Biomass Briquettes Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Punjab & Haryana | Paddy straw and NCR demand | Policy support and buyers |
| Uttar Pradesh | Straw, cane trash, industries | Large feedstock and demand |
| Gujarat | Groundnut shells, cotton stalks | Strong industrial boiler market |
| Maharashtra | Cotton, soybean, bagasse | Industrial clusters |
| Madhya Pradesh | Soybean husk and mustard | Low-cost residues |
| Rajasthan | Mustard stalk and husk | Abundant dry residues |
Punjab, Haryana, and western Uttar Pradesh combine huge paddy straw volumes with strong policy support and NCR demand, while Gujarat offers groundnut shells and cotton stalks close to a large industrial boiler market. Maharashtra, Madhya Pradesh, and Rajasthan provide abundant cotton, soybean, and mustard residues. The final choice should weigh residue supply, customer distance, storage land, and power availability.
Quality, Safety and Environmental Systems
Briquettes must meet customer specifications for calorific value, moisture, ash, size, and density, and power plant supplies follow the quality norms in co-firing contracts, so regular testing is essential. A credible plant needs a basic laboratory with a moisture meter, bomb calorimeter, and ash testing, along with incoming material checks and batch records. Safety focuses on fire risk in large biomass stores, dust explosions in grinding, and moving machinery, while environmental systems cover dust collection, dryer emissions, and ash disposal. An experienced Biomass Briquettes Manufacturing Consultant in India can help plan feedstock strategy, plant layout, and fire safety so the plant meets customer and regulatory requirements from the start.
Infrastructure Requirements (5 TPH Briquetting Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 3 – 8 acres | Mostly raw material storage |
| Raw Material Yard | Covered sheds and open stacks | Several months of stock |
| Process Shed | Dryer, mills, and presses | Dust extraction |
| Finished Goods Storage | Covered, ventilated | Protects from moisture |
| Power Supply | HT or LT connection, 0.5 – 1 MW | Presses and hammer mills |
| Fire Safety | Hydrants, spacing, detection | Critical for biomass stores |
| Weighbridge & Roads | Truck access | High truck movements |
Large covered storage for residues and finished briquettes is the most important infrastructure requirement, since the plant must hold several months of feedstock after harvest. A reliable power supply for presses and mills, strong fire protection, and a weighbridge with good truck access complete the core needs.
Biomass Briquettes Manufacturing Machinery and Equipment
The equipment set covers residue collection, size reduction, drying, grinding, briquetting, cooling, handling, and testing. Briquetting presses, dryers, and hammer mills account for most of the machinery budget. The main items are summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Balers & Tractors | Collect straw and stalks | Square or round balers |
| Shredders & Chaff Cutters | Cut bales and stalks | Heavy-duty blades |
| Conveyors & Feeders | Move material | Belt and screw conveyors |
| Rotary or Flash Dryer | Reduce moisture | Biomass-fired hot air |
| Hammer Mills | Grind residues | Screen size 6–8 mm |
| Cyclones & Bag Filters | Collect dust | Dust and fire control |
| Briquetting Presses | Compress biomass | Piston or screw type |
| Cooling Conveyors | Cool briquettes | Air-cooled tracks |
| Weighing & Bagging | Pack product | Loose or bagged dispatch |
| Testing Equipment | Check quality | Moisture meter, calorimeter |
| Fire Protection System | Protect stores | Hydrants and detectors |
Machinery should follow the feedstock and capacity plan. A sawdust or groundnut shell unit needs mainly a hammer mill, conveyors, and presses, while a straw plant adds balers, shredders, and dryers. Mechanical piston presses suit high outputs and varied residues, screw presses give denser briquettes for some feedstocks, and a pellet mill line can be added to serve power plants.
Biomass Briquettes Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a 5 TPH briquetting plant with drying in India. The final Biomass Briquettes Investment Cost for your project will depend on capacity, feedstock, the need for balers and dryers, storage size, land cost, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 40–50% | Presses, dryer, mills, conveyors |
| Collection Equipment | 8–12% | Balers, tractors, trailers |
| Civil Works & Sheds | 15–20% | Process and storage sheds |
| Land & Site Development | 8–12% | Land, yards, roads |
| Electrical & Fire Safety | 5–8% | Power connection, hydrants |
| Working Capital | 10–15% | Seasonal residue stocks |
Machinery and storage dominate the capital budget, and working capital is significant because residues must be bought and stored in season for use through the year. Because feedstock prices, briquette prices, and coal prices move independently, a detailed Biomass Briquettes Business Plan should model seasonal purchasing, storage losses, moisture, power cost, selling prices relative to coal, and customer contracts together, so that funding supports a full year of operation without cash strain.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials | 40–50% | Residue prices are seasonal |
| Utilities (power, dryer fuel) | 25–35% | Presses and mills use most power |
| Labour | 8–12% | Operators and handling staff |
| Maintenance & Spares | 4–6% | Dies, rams, hammer replacement |
| Transport & Selling | 4–6% | Delivery to customers |
| Overheads | 2–4% | Administration and insurance |
With raw materials and power making up most of the cost, margins depend on residue prices, moisture, power tariffs, press uptime, and selling prices. A good operating model tracks feedstock cost per tonne of output, moisture loss, power per tonne, die and ram life, storage losses, and realised prices by customer, and tests how margins respond when residue prices spike or coal prices fall.
Financial Analysis and Profitability
Based on analysis of a 5 TPH plant, the financial profile is attractive, supported by low capital needs, strong policy support, and growing demand from industries and power plants, but returns depend on securing feedstock at the right price and selling consistently. The profitability of Biomass Briquettes manufacturing business in India improves markedly with a location close to both residues and buyers, low-moisture feedstock, efficient presses, long-term supply contracts, and access to co-firing tenders.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 25–35% | Depends on residue cost |
| Net Profit Margin | 10–15% | After depreciation and taxes |
| Payback Period | 2–4 Years | Low capital intensity |
| IRR (Internal Rate of Return) | 18–25% | Higher with long-term contracts |
| Capacity Utilization (stable ops) | 60–80% | Seasonal feedstock limits |
| Break-even Capacity Utilization | 40–50% | Moderate fixed costs |
Feedstock security and customer contracts decide where a plant lands within these ranges. Plants with assured residues and long-term buyers run at high utilisation and earn steady margins, while those buying residue at peak prices or relying on spot sales face swings. Sawdust and groundnut shell briquettes usually earn better prices, while straw briquettes rely on policy-driven demand and support schemes.
Returns can be strengthened by integrating collection, storing residues efficiently, blending feedstocks for consistent quality, adding a pellet line for power plants, selling under long-term contracts indexed to coal prices, and earning carbon credits where available.
Key Risks and Mitigation
The main risks are seasonal feedstock shortages and price spikes, high moisture, fire in storage, falling coal prices, payment delays from power plants, and inconsistent quality. Supply risk is reduced through farmer contracts and in-season buying; moisture risk by covered storage and drying; fire risk by spacing and fire systems; price risk by contracts linked to coal prices; payment risk by diversified customers; and quality risk by blending and testing. Promoters often work with a Biomass Briquettes Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for Biomass Briquettes Manufacturing in India
Approvals for a briquetting plant are relatively simple but must cover pollution control, fire safety, and land use. Promoters setting up a Biomass Briquettes Manufacturing Plant in India generally need the following:
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, with the category depending on the state and process.
- Land Use Approval: Conversion of agricultural land for industrial use where required.
- Fire Safety: Fire NOC covering biomass storage, with hydrants, detection, and safe stacking.
- Factory License: Factory license under the Occupational Safety, Health and Working Conditions Code, 2020 and building approval as applicable.
- Power Connection: Electricity connection approval from the distribution company.
- Customer Empanelment: Vendor registration with power plants and industrial buyers for co-firing and fuel supply.
- Business & Trade Registrations: Company incorporation, GST, Udyam registration, and EPF and ESI registrations.
Land use approval and pollution control consent are usually on the critical path, while vendor empanelment with power plants can take several months. Planning approvals, feedstock arrangements, and customer contracts in parallel shortens the time from investment decision to the first supplies.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, feedstock, customer specifications, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Biomass Briquettes Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- Co-firing policy: In November 2025, the Ministry of Power notified a policy requiring 5% biomass co-firing across coal plants, with an extra 2% of torrefied charcoal in NCR plants and 50% locally sourced paddy straw for NCR plants.
- Enforcement: In December 2025, CAQM issued penalties of INR 61.85 crore to six thermal power plants near Delhi for missing co-firing targets in 2024-25.
- Rising biomass use: By June 2026, thermal power plants had co-fired about 6.10 million tonnes of biomass, with 75 plants participating.
- State programmes: In July 2025, the Goa Energy Development Agency launched a project to convert biomass into briquettes.
The common thread is strong policy support, stricter enforcement, and rising use of biomass by power plants and industries. New entrants who secure reliable residue supply, consistent quality, and long-term buyers will be best placed to capture this growth.
How a Biomass Briquettes Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from market demand and feedstock assessment to plant design, machinery, storage, approvals, and economics. It helps investors decide the right feedstock, capacity, and customer mix, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Biomass Briquettes Financial Model covering revenue by customer, seasonal feedstock purchases and prices, moisture and storage losses, power and labour costs, maintenance, working capital, debt servicing, cash flows, break-even, return on investment, and payback under different feedstock and price scenarios. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a Biomass Briquettes Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a briquetting project, a strong DPR also clarifies the feedstock catchment and collection plan, storage design, customer contracts, and fire safety, which together are the factors most likely to decide success. By testing margins against residue price swings, coal prices, and seasonal supply, the report turns a policy-driven opportunity into a plan that lenders and partners can trust.
Frequently Asked Questions
What are the first steps to set up a biomass briquettes manufacturing plant in India?
Start by surveying residue availability and prices within a short radius, and identifying industrial and power plant buyers. Then commission a feasibility study and DPR, secure land with storage space and power, select presses and dryers, arrange collection and storage, obtain pollution control and fire approvals, and sign supply agreements with customers.
How much does it cost to set up a biomass briquettes manufacturing plant in India?
Investment ranges from about INR 0.5–2 crore for a small unit of 1 to 2 TPH to INR 5–15 crore for a plant of 3 to 6 TPH with drying and grinding, and INR 25–60 crore for an integrated paddy straw plant of 10 to 20 TPH with its own baling fleet and a pellet line.
What are the main steps in biomass briquettes manufacturing?
The flow runs from collection and baling through receipt and storage, shredding, drying, grinding, screening and blending, briquetting, cooling, cutting and quality testing, and storage and dispatch.
Which machinery does a biomass briquettes manufacturing plant need?
Key equipment includes balers and tractors, shredders and chaff cutters, conveyors and feeders, a rotary or flash dryer, hammer mills, cyclones and bag filters, briquetting presses, cooling conveyors, weighing and bagging equipment, testing equipment, and a fire protection system.
What raw materials are used to make biomass briquettes?
Common raw materials include groundnut shells, mustard and cotton stalks, soybean husk, paddy straw, sugarcane trash, bagasse, sawdust, and wood waste. Most briquettes need no binder, since natural lignin binds the particles under heat and pressure.
How profitable is biomass briquettes manufacturing in India?
A well-run plant typically earns a 25 to 35% gross margin and a 10 to 15% net margin, with payback in about 2 to 4 years. Profitability depends on residue cost, moisture, power cost, utilisation, and long-term customer contracts.
Which approvals does a biomass briquettes manufacturing plant need in India?
Typical approvals include pollution control consents, land use conversion where needed, Fire NOC, a factory license, an electricity connection, vendor empanelment with power plants and industries, and GST, Udyam, and labour registrations.
How do I get a feasibility study or DPR for a biomass briquettes manufacturing project?
A detailed feasibility study and DPR covers feedstock assessment, market demand, plant design, approvals, and full financials. Investors usually engage a Biomass Briquettes Manufacturing Feasibility Study Consultant with experience in biomass and renewable fuel projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Lead-acid batteries start every car, truck, and two-wheeler, back up telecom towers, data centres, and homes through inverters and UPS systems, and store energy for solar installations. Almost all of the lead, plastic, and acid in a used battery can be recovered, and India already meets more than 80% of its lead demand from recycling.
Fuel cells turn hydrogen into electricity with water as the only exhaust, which makes them one of the most important technologies in India's clean energy transition. They power hydrogen buses, trucks, and trains, provide backup power for telecom towers and data centres, and supply off-grid and distributed electricity where diesel generators are used today.
India's cities generate well over a lakh tonnes of municipal solid waste every day, and much of it still ends up in overflowing dumpsites that release methane, catch fire, and pollute land and water.
Every solar power system needs an inverter to convert the direct current produced by solar panels into alternating current that homes, businesses, and the grid can use.
Sodium-ion batteries are emerging as a practical complement to lithium-ion technology. They work on the same principle, shuttling ions between a cathode and an anode, but use sodium, which is abundant, inexpensive, and available within India, in place of lithium.
Few industries in India have scaled as quickly as solar manufacturing. Backed by ambitious renewable energy targets, a rooftop programme for households, import duties on foreign modules, and the Approved List of Models and Manufacturers (ALMM), domestic module capacity has multiplied in just a few years.
Setting up an Electrical Panel Manufacturing Plant in India is a fabrication-and-assembly venture powered by heavy grid modernisation, a fast-growing renewable-energy build-out, rising industrial and commercial construction, and the spread of automation across factories and buildings.
Saudi Arabia has turned its power transition into one of the world's largest procurement programmes, and international developers, lenders, and equipment makers are following the tenders.
Setting up a Battery Manufacturing Plant in India is a high-demand, energy-driven venture, powered by the country's booming automotive sector, huge power-backup market, and the fast-growing shift to electric vehicles and renewable storage.
Setting up a Liquefied Natural Gas (LNG) Manufacturing Plant in India is a capital-intensive, strategically important venture, powered by the country's push toward a gas-based economy, the shift to cleaner fuels in transport and industry, and rising demand for LNG as a truck, bus, and industrial fuel.
The India carbon credit market is moving from a voluntary, project-by-project trade into a regulated national system with binding targets, a central registry, and exchange-based price discovery. According to IMARC Group, the market was valued at USD 33.69 Billion in 2025, grew to USD 44.42 Billion in 2026, and is projected to reach USD 405.47 Billion by 2034, expanding at a CAGR of 31.84% (2026–2034).
Setting up a Syngas Production Plant in India is a capital-intensive but strategically valuable venture, driven by the country's push for cleaner industrial fuels, coal and biomass utilization, and chemical self-reliance. Syngas, or synthesis gas, is a mixture of hydrogen and carbon monoxide produced by gasifying carbon-rich feedstocks, and it serves as a versatile building block for power, chemicals, hydrogen, and synthetic fuels. With abundant biomass, coal, and waste feedstock and growing policy support for gasification, India offers a favourable environment for new plants.
Setting up a Battery Energy Storage System Manufacturing Plant in India is a capital-efficient, high-growth venture, driven by the country's renewable energy expansion, grid modernization, and supportive storage policies. As solar and wind capacity scales up and the grid needs to balance variable generation, battery energy storage systems have become essential infrastructure.
Setting up a Lithium-ion Battery Recycling Plant in India is a capital-intensive but high-potential venture. India's rapid rise as a major electric-vehicle market, its large consumer-electronics base, and its fast-growing energy-storage sector are together creating one of the deepest and fastest-expanding pools of end-of-life lithium-ion batteries in the world.
Solar glass is a type of specialty glass that has high transmittance and is designed exclusively for use in solar energy systems. Unlike regular flat glass, solar glass is designed to have maximum light transmission with minimal losses due to reflection and absorption.
A solar inverter is a vital component in solar photovoltaic (PV) systems, responsible for transforming the direct current (DC) electricity produced by solar panels into alternating current (AC) electricity. This AC power is then suitable for use by the electrical grid, various appliances, and industrial equipment.
Australia has firmly established itself as a dominant force in the global liquefied natural gas (LNG) market, maintaining its position as one of the world's leading exporters. The country's strategic geographical location in the Asia-Pacific region, combined with substantial natural gas reserves, has enabled it to become a critical energy supplier to rapidly growing Asian economies, particularly China, Japan, and South Korea.
Japan's lead acid battery market stands as a cornerstone of the nation's energy storage infrastructure, demonstrating remarkable resilience and adaptability in an era dominated by rapid technological evolution. Despite the global shift toward lithium-ion technologies, the Japanese lead acid battery sector continues to thrive, driven by its unmatched cost-effectiveness, proven reliability, and exceptional recyclability.
Green hydrogen is the cleanest form of hydrogen available, as it is produced through water electrolysis using the electricity generated from renewable energy sources such as solar, wind, or hydropower. Carbon dioxide emissions are zero since no fossil fuels are used. Essentially, an electrolyzer is used in the electrolysis process to split water molecules into hydrogen and oxygen. The resulting hydrogen is refined by purification, compression, or liquefaction and then fed into various applications. Green hydrogen is considered a cornerstone of the global energy transition because it can store renewable energy, decarbonize hard-to-abate sectors, and serve as a sustainable alternative to fossil-fuel-based hydrogen.
Japan’s thermal power plant industry remains a crucial pillar of the nation’s energy infrastructure, providing a stable and reliable source of electricity for both industrial and residential consumption. Thermal power generation, which primarily involves the combustion of fossil fuels such as coal, natural gas, and oil, continues to play a key role despite increasing investments in renewable energy.
An electrical panel, also called a distribution board or switchboard, is an important installation in electrical infrastructure that acts as the main center for the distribution, control, and protection of electrical power within residential, commercial, and industrial systems. It acts as the point at which electrical energy is received from the utility or a source of power generation and is distributed to various circuits and equipment in an organized manner.
The global oil and gas EPC market is currently experiencing a remarkable transformation as it positions itself at the intersection of traditional energy demands and technological innovation. As of 2024, the market is demonstrating robust growth, reaching USD 52.9 Billion in 2024, depending on regional scope and market segmentation approaches. This substantial market base is supporting a major number of capital projects worldwide, including offshore platform projects and onshore installations that are collectively shaping the energy landscape.
Bamboo pellets are a biomass fuel type created through the compression of bamboo residues like shavings, sawdust, and chips into thick cylindrical pellets. They are an environmentally friendly substitute for conventional fossil fuels like natural gas and coal. Due to the fast growth rate and high biomass yield of bamboo, it has become one of the most renewable raw materials for the production of bioenergy.
Biomass briquettes are dense, solid fuel blocks made of compressed organic waste materials like sawdust, agricultural wastes, wood shavings, coconut shells, rice husk, or herbaceous biomass. The briquetting process usually involves drying the biomass to lower the moisture content (usually down to 10-15%), grinding or milling for a fine particle size uniformity, and then compressing under high pressure with or without a binding agent.
Biogas is a renewable energy form generated by the anaerobic fermentation of organic matter including agricultural residues, animal waste, municipal solid waste, sewage sludge, and food waste. Microorganisms in the absence of oxygen break down organic substances in the process and produce a gaseous mixture of mainly methane (CH4) and carbon dioxide (CO2), with traces of hydrogen sulfide (H2S) and water vapor.
A battery is an electrochemical energy storage system that transforms chemical energy into electrical energy by way of redox reactions between its electrodes and electrolyte. It consists of a single or multiple electrochemical cells, each having a positive electrode (cathode), a negative electrode (anode), and an electrolyte for ion transfer. Batteries are categorically divided into primary (non-rechargeable) and secondary (rechargeable) types.
The global energy landscape is undergoing a seismic transformation, with green hydrogen emerging as one of the most promising solutions to achieve deep decarbonization across sectors. Far from a niche technology, green hydrogen is emerging as a critical pillar of the future energy system, offering a pathway to a sustainable and resilient economy.
Transmission line towers are essential support components of transmission lines installed on overhead to distribute high-voltage electricity over long distances. Towers are made of galvanized steel, primarily, and are designed to tolerate mechanical stress, environmental loads, and electrical safety. Some of the important characteristics of transmission line towers are high structural strength, corrosion resistance, adaptability for modular design, and high service life. They are normally produced in lattice form (tubular or free-standing towers) or tubular form, with types including suspension towers, tension towers, angle towers, and terminal towers based on use.
The energy storage revolution is here, and it's powered by graphene. While the world struggles with the limitations of conventional lithium-ion batteries, a new technology is emerging that promises to shatter every performance barrier we've accepted as unchangeable.
Australia is undergoing a significant energy transformation, underscoring the growing role of renewable energy sources. These sources are key to combating climate change by reducing greenhouse gas emissions, the primary cause of global warming and air pollution. Beyond environmental benefits, renewable energy strengthens energy security by diversifying power sources and reducing dependence on volatile fossil fuel imports, contributing to greater energy independence.
Learn how to plan capital investment, manage raw material costs, post manufacturing cost and optimize operations for setting up solar panel plant.
Battery Energy Storage System (BESS) represents a power grid technology that stores electricity to enhance electric power grid reliability while increasing operational efficiency. BESS permits battery recharging during periods of low demand or extra grid supply capacity. BESS provides three principal operational functionalities which include power grid stabilization during supply disruptions, control of energy supply variations, and integration of intermittent renewable generation from wind and solar resources.
China's economic presence is expanding globally, and Latin America and the Caribbean (LAC) have become a focal point for its investments, especially within the energy sector. The region, rich in natural resources and experiencing rising energy demands, offers strategic opportunities for Chinese energy giants looking to invest and expand. LAC is currently leading a transformative movement towards sustainable energy. From 2015 to 2022, the region increased its renewable energy capacity by an impressive 51%, now generating 64% of its electricity from renewables such as hydropower, wind, and solar. This shift addresses the global demand for cleaner energy while supporting local economic growth and enhancing energy security.
Hydrogen is a clean, renewable, and widely available energy source that can be produced through various methods. Production techniques such as coal gasification, steam methane reforming, electrolysis, and thermochemical processes highlight its versatility. Hydrogen is essential in several critical sectors, including methanol and ammonia production, petroleum refining, transportation, power generation, as well as in electronics, metal industries, and as a rocket propellant. The increasing concern over carbon emissions and greenhouse gases has led to a shift towards cleaner fuel options. Hydrogen is recognized for its cleanliness and versatility as an energy carrier. Additionally, supportive government initiatives and favorable policies are driving the growth of hydrogen production globally.
Hydrogen is a clean, renewable, and abundant energy source derived from various methods. Its applications span across transportation, heating, and power generation. Diverse production methods, including coal gasification, steam methane reforming, electrolysis, and thermochemical processes, contribute to its versatility. Hydrogen plays a pivotal role in crucial sectors like methanol and ammonia production, petroleum refining, transportation, power generation, as well as in electronics, metal industries, and as a rocket propellant.
A floating solar farm is a renewable energy installation in which solar panels are mounted on floating structures in water bodies such as lakes, reservoirs, ponds, or even the sea. This technology, also known as a floating photovoltaic (PV) system, or “floatovoltaics,” enables solar power generation in areas with limited available land or where land use is restricted for other purposes. Floating solar farms offer various benefits, including improved solar panel efficiency through cooling, land conservation, reduction of evaporation and algae growth, and integration with hydropower facilities to generate both solar and hydroelectric power in the same location.
Nuclear power utilizes nuclear reactions to generate heat, which is then converted into electricity. This energy is released from the nucleus—the core of atoms composed of protons and neutrons. Nuclear power can be derived from nuclear fission, nuclear decay, and nuclear fusion reactions. Across the globe, nuclear power plants predominantly use the fission of uranium and plutonium to produce electricity. The heat generated from fission is used to create steam, which drives turbines connected to generators. Nuclear power offers several advantages over fossil fuels, such as minimal greenhouse gas emissions and a higher energy density, meaning a small amount of nuclear fuel produces a large amount of energy.