Aluminum Air EV Battery Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
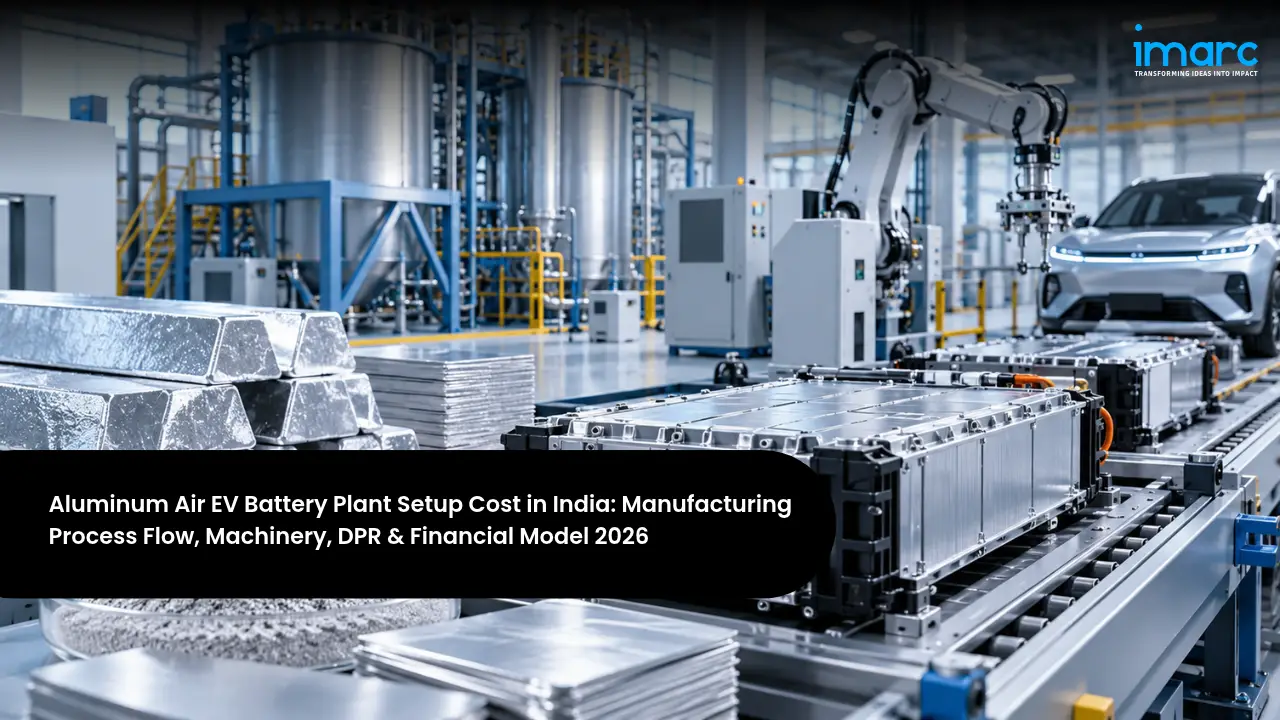
Aluminum-air batteries generate electricity by reacting aluminum plates with oxygen from the air in a water-based electrolyte. Aluminum has a very high theoretical energy density, and instead of being recharged from a socket, spent plates are swapped for fresh ones while the aluminum hydroxide produced is recycled into new aluminum. The technology is still in early commercial use, mainly as backup power for telecom towers and data centres and as a range extender for electric vehicles. The global aluminum-air EV battery market was valued at about USD 96 million in 2025 and is projected to grow at nearly 14% a year to 2034. India's aluminum industry, EV ambitions, and pilots by Indian Oil, Phinergy, and Hindalco make Aluminum Air EV Battery Manufacturing Plant Setup in India an emerging opportunity for investors willing to take on technology risk.
Investment depends mainly on scale, technology access, in-house cathode and plate production, and testing capability. The Aluminum Air EV Battery Manufacturing Plant Cost ranges from about INR 15–30 crore for a pilot line of 500 to 1,000 systems a year to INR 80–150 crore for a commercial plant of about 5,000 systems a year with cathode, plate, and stack lines, and INR 400–700 crore for a large integrated facility of 25,000 systems a year or more with plate production and recycling partnerships. Raw materials make up 50 to 60% of operating cost and utilities 15 to 25%. IMARC's analysis points to a gross margin of 35 to 50% and a net margin of 15 to 30%, but these depend on reaching commercial volumes, which few producers have yet achieved.
This guide is written for investors exploring how to start an Aluminum Air EV Battery manufacturing plant in India. It focuses on a commercial plant of about 5,000 systems a year producing aluminum-air power modules for telecom and data centre backup and EV range extenders, together with a recurring business in replacement aluminum plates and recycling, and also explains pilot lines and large integrated facilities. It covers technology and markets, process flow, machinery, location, costs, approvals, and how a DPR and financial model turn this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Global Market (2025) | About USD 95.83 Million |
| Global Market Forecast (2034) | USD 304.32 Million, 13.7% CAGR |
| Technology Stage | Early commercial, pilot scale |
| Main Fuel | Aluminum plates, recyclable |
| Typical Plant Capacity | 5,000+ Systems a Year |
| Indicative Total Investment | INR 15 Crore to 700 Crore |
The snapshot shows a small but fast-growing market at an early stage of commercial use. Most current deployments are stationary backup systems replacing diesel generators, while EV applications remain in trials. The wide investment range reflects a real choice between a pilot line, a commercial plant, and a large integrated facility, with technology access and customer pilots mattering as much as capital. The sections below work through that choice.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Backup modules, EV range extenders |
| Plant Capacity | 500 – 25,000+ Systems Per Year |
| Total Project Investment | INR 15–30 Crore (pilot line) to 400–700 Crore (integrated) |
| Payback Period | 5 – 8 Years |
| Net Profit Margin | 15 – 30% (IMARC, at scale) |
| IRR | 14 – 22% |
| Preferred States | Odisha, Uttar Pradesh, Maharashtra, Tamil Nadu, Karnataka, Gujarat |
| Key Requirement | Technology license, aluminum supply, pilots |
These ranges should be read with caution. Actual returns depend on access to proven technology, the cost of aluminum fuel per kilowatt-hour, cathode life, recycling logistics, customer adoption beyond pilots, competition from lithium-ion and sodium-ion batteries, and the pace of regulatory approvals for vehicle use. A site-specific Aluminum Air EV Battery Feasibility Report tests each of these assumptions against your chosen technology route, applications, capacity, location, and customers.
Table of Contents
- What is an Aluminum Air EV Battery Manufacturing?
- Why is Aluminum Air EV Battery Manufacturing Growing in India?
- Aluminum Air EV Battery Manufacturing Process Flow
- Raw Materials Required for Aluminum Air EV Battery Manufacturing
- Location, Land & Infrastructure
- Aluminum Air EV Battery Manufacturing Machinery and Equipment
- Aluminum Air EV Battery Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Aluminum Air EV Battery Manufacturing in India
- Recent Developments in the India Aluminum Air EV Battery Manufacturing Industry
- How an Aluminum Air EV Battery Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is an Aluminum Air EV Battery Manufacturing?
An aluminum-air cell has three main parts: an anode made of a specially alloyed aluminum plate, an air cathode that lets oxygen from the air in while keeping liquid electrolyte from leaking out, and an alkaline or saline electrolyte between them. As the cell works, the aluminum is gradually converted to aluminum hydroxide, releasing electrons that power the load. Small amounts of alloying elements such as tin, indium, or gallium reduce unwanted corrosion that would otherwise waste aluminum and release hydrogen. Cells are stacked into modules with pumps to circulate electrolyte, scrubbers to remove carbon dioxide from incoming air, heat management, and power electronics to deliver steady output.
Because the aluminum is consumed, these systems behave more like a fuel-based generator than a rechargeable battery. Customers buy or lease the system and then pay for replacement aluminum plates, while spent electrolyte and aluminum hydroxide are collected for recycling into new aluminum. An Aluminum Air EV Battery Manufacturing Plant therefore earns revenue from both system sales and a recurring fuel and recycling service. Buyers value long run time, low weight, zero on-site emissions, fast refuelling, reliable operation, and a total cost competitive with diesel generators or lithium-ion batteries.
- Telecom Backup: Power for towers during grid outages.
- Data Centre Backup: Clean alternative to diesel generators.
- EV Range Extenders: Extra range alongside lithium-ion packs.
- Remote & Defence Power: Off-grid and portable energy.
The Main Applications and Product Types
Choosing the application is the most important commercial decision, because it determines system design, certifications, partners, and the speed of adoption:
| Application | Description | Key Property | Primary Demand |
|---|---|---|---|
| Telecom Backup | 3 – 10 kW modules | Long run time | Tower companies |
| Data Centre Backup | Large generator units | Zero emissions | Data centres |
| EV Range Extender | Vehicle-mounted packs | High energy density | Buses, trucks, cars |
| Off-Grid Power | Portable units | Light weight | Remote sites |
| Defence & Emergency | Rugged systems | Silent operation | Armed forces |
| Replacement Plates | Aluminum fuel | Recurring revenue | All users |
These choices shape the whole plant. Stationary backup systems are the most commercially advanced, with simpler safety approvals and customers who value replacing diesel, while vehicle range extenders need compact designs, crash and safety testing, and vehicle homologation. Most new entrants therefore start with telecom and data centre backup modules and a plate supply service, and move into EV range extenders as vehicle trials, approvals, and refuelling networks mature.
Why is Aluminum Air EV Battery Manufacturing Growing in India?
Key Growth Drivers in India and Export Markets
Interest is supported by decarbonisation goals, the search for alternatives to diesel and imported lithium, and India's aluminum base:
- Diesel replacement: Telecom towers and data centres want clean backup without diesel.
- Energy security: Aluminum is produced in India, reducing reliance on imported lithium.
- EV range: High energy density can extend range for buses and trucks.
- Circular economy: Spent material can be recycled into new aluminum.
- Exports: Backup systems can serve data centres and telecoms abroad.
India-Specific Market Opportunity
| Segment | Market Context | Manufacturing Role |
|---|---|---|
| Telecom Towers | Large tower base | Backup modules |
| Data Centres | Rapid capacity growth | Generator units |
| Commercial EVs | Bus and truck trials | Range extenders |
| Defence & Remote | Off-grid needs | Rugged systems |
| Aluminum Recycling | Smelter partners | Fuel cycle |
The strongest near-term opportunity lies in replacing diesel generators at telecom towers and data centres, where pilots are already under way, and in building the aluminum plate supply and recycling chain with smelters. EV range extenders are a longer-term opportunity that depends on vehicle trials and refuelling infrastructure. Producers that secure proven technology, strong aluminum partners, and early anchor customers will be best placed to grow.
Aluminum Air EV Battery Manufacturing Process Flow
Understanding the process helps you plan equipment, layout, and where cost and quality are decided. The flow runs from aluminum alloy plate preparation through air cathode material mixing, coating and pressing, drying and lamination, cell frame moulding, cell and stack assembly, system integration with pumps, scrubbers, and electronics, and testing to packing and dispatch, with a separate loop for recycling spent material.
The Aluminum Air EV Battery Manufacturing Process Flow
The sequence below reflects a plant that makes its own air cathodes and finishes purchased alloy plates. Integrated plants also cast and roll the aluminum alloy.
| Unit Operation | Key Activity |
|---|---|
| Plate Preparation | Alloy plates cut, cleaned |
| Cathode Mixing | Carbon, catalyst, binder |
| Coating & Pressing | On metal mesh |
| Drying & Lamination | Gas diffusion layer |
| Frame Moulding | Cell housings |
| Cell Assembly | Anode, cathode, seals |
| Stack Assembly | Cells, electrolyte paths |
| System Integration | Pumps, scrubber, BMS |
| Testing | Leak, discharge, safety |
| Packing & Dispatch | Systems and plates |
Two factors decide profitability across this flow. The first is air cathode performance and life, because cathodes are the most technical and costly part of the cell, and longer-lasting, higher-power cathodes lower cost per kilowatt-hour across many plate replacements. The second is aluminum utilisation, since corrosion and incomplete use of the plate waste costly fuel and generate hydrogen, so alloy design, electrolyte management, and system control strongly affect the economics customers see.
Raw Materials Required for Aluminum Air EV Battery Manufacturing
The main inputs are high-purity aluminum alloy plates with small additions of elements such as tin, indium, or gallium, air cathode materials including carbon, catalysts, PTFE binder, and nickel or steel mesh, electrolyte chemicals such as potassium hydroxide and additives, plastic cell frames and housings, pumps, heat exchangers, and carbon dioxide scrubbers, and electronics such as battery management systems and DC-DC converters.
| Raw Material | Role in Product | India Sourcing | % of OpEx |
|---|---|---|---|
| Aluminum Alloy Plates | Anode fuel | Smelters, rollers | 25–32% |
| Cathode Materials | Oxygen reaction | Mostly imported | 10–14% |
| Electrolyte Chemicals | Ion transport | Domestic suppliers | 3–5% |
| Frames & Balance of System | Housings, pumps | Domestic vendors | 6–8% |
| Electronics | Control, conversion | Domestic, imported | 6–9% |
Aluminum plates are the largest recurring cost, and their price follows aluminum markets plus alloying and rolling charges, while catalysts and specialised cathode materials are often imported. Partnerships with aluminum producers for alloy plates and recycling, local development of cathode materials, and long-term supply agreements help manage cost and supply risk.
Location, Land & Infrastructure
Site selection for this plant is driven by access to aluminum smelters and rolling mills for alloy plates and recycling, proximity to telecom, data centre, and automotive customers, and availability of engineers in electrochemistry and power electronics. Other factors include reliable power for testing, chemical storage approvals, good logistics for the plate exchange and recycling loop, and state incentives for EV and battery manufacturing.
Choosing the Best Location for Aluminum Air EV Battery Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Odisha | Major smelters | Aluminum, recycling |
| Uttar Pradesh | Renukoot smelter, NCR | Metal and markets |
| Maharashtra | Pune auto cluster | Vehicle partners |
| Tamil Nadu | Chennai auto, EVs | EV ecosystem |
| Karnataka | Bengaluru tech | Engineering talent |
| Gujarat | EV and battery parks | Incentives, ports |
Odisha and Uttar Pradesh host large aluminum smelters that can supply plates and take back aluminum hydroxide, while Maharashtra and Tamil Nadu offer automotive partners for range extender trials. Karnataka provides engineering talent in batteries and electronics, and Gujarat offers EV manufacturing incentives and port access. The final choice should weigh aluminum access, customer proximity, talent, incentives, and land cost.
Quality, Safety and Environmental Systems
Systems must be tested for power output, run time, electrolyte leakage, hydrogen release, thermal behaviour, and electrical safety, and vehicle systems need homologation testing under applicable automotive standards. A credible plant needs a cathode testing laboratory, discharge test benches, environmental chambers, leak testers, and full traceability of cathodes, plates, and stacks. Safety focuses on caustic electrolyte handling, hydrogen ventilation during testing, and high-current electrical work. Environmental systems cover collection and recycling of spent electrolyte and aluminum hydroxide, and treatment of chemical wastewater. An experienced Aluminum Air EV Battery Manufacturing Consultant in India can help plan technology access, product design, testing, and approvals so the plant meets regulatory and customer requirements from the start.
Infrastructure Requirements (5,000 Systems a Year)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 3 – 6 acres | Industrial zone |
| Cathode Line | Mixing, coating, pressing | Dust control |
| Plate Finishing | Cutting, treatment | Near metal supply |
| Assembly Hall | Cells, stacks, systems | Clean, organised |
| Utilities | Power, water | 1 – 2 MW load |
| Test Area | Discharge, safety | Hydrogen venting |
| Recycling Yard | Spent material | Return logistics |
A capable cathode production line, a safe and well-ventilated test area, and organised logistics for the plate exchange and recycling loop are the most important infrastructure requirements. An R&D laboratory, chemical storage, and good road access for customer deliveries complete the core needs.
Aluminum Air EV Battery Manufacturing Machinery and Equipment
The equipment set covers plate preparation, cathode production, frame moulding, cell and stack assembly, system integration, testing, and electrolyte handling. Cathode production equipment, test systems, and assembly lines account for most of the machinery budget.
| Equipment | Function | Key Specification |
|---|---|---|
| Plate Cutting Line | Size anode plates | Shear, punch |
| Surface Treatment | Clean plates | Chemical line |
| Planetary Mixer | Mix cathode paste | Vacuum |
| Coating Machine | Coat mesh | Precision |
| Roll Press | Compact cathodes | Calender |
| Drying Oven | Cure cathodes | Controlled |
| Injection Moulding | Make frames | Engineering plastics |
| Welding Systems | Join components | Laser, ultrasonic |
| Assembly Line | Build stacks | Semi-automatic |
| Discharge Test Benches | Test systems | Electronic loads |
| Environmental Chamber | Stress testing | Heat, humidity |
Machinery should follow the product plan. A pilot line needs small mixers, a coater, a roll press, manual assembly benches, and test benches, often with cathodes supplied by a technology partner, while a commercial plant adds automated cathode lines, frame moulding, semi-automatic stack assembly, and full test systems. Large facilities add aluminum alloy casting and rolling links, automated system integration, and recycling partnerships, and precise cathode production equipment is essential at every scale.
Aluminum Air EV Battery Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a commercial plant of about 5,000 systems a year in India. The final Aluminum Air EV Battery Investment Cost for your project will depend on technology licensing, scale, cathode and plate production depth, testing facilities, land cost, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 35–45% | Cathode, assembly, test |
| Technology & R&D | 12–18% | License, lab, validation |
| Buildings & Civil Works | 12–16% | Production, test areas |
| Land & Site Development | 4–7% | Land and approvals |
| Pilots & Pre-operative | 5–8% | Field trials |
| Working Capital | 15–20% | Plates, receivables |
Machinery and technology costs make up most of the capital, and early customer pilots add cost before volume sales begin. Working capital covers aluminum plate stock, systems on trial, and receivables from large customers. Because revenue builds slowly as pilots convert into orders, a detailed Aluminum Air EV Battery Business Plan should model system sales and leases, plate and recycling revenue, aluminum prices, cathode life, pilot timelines, customer adoption, and working capital together, so that funding carries the business through the early commercial phase.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials | 50–60% | Plates, cathodes |
| Utilities (power, water) | 15–25% | Testing, production |
| Labour & Engineering | 8–12% | Technicians, R&D |
| Logistics & Recycling | 4–6% | Plate exchange loop |
| Maintenance | 2–3% | Equipment upkeep |
| Overheads & Royalties | 3–5% | Technology fees |
With materials and utilities making up most of the cost, margins depend on aluminum prices, cathode cost and life, plate utilisation, recycling credits, and production yields. A good operating model tracks cost per kilowatt-hour delivered to customers, cathode life, aluminum utilisation, yield, recycling value, and realised prices for systems and plates, and tests margins against higher aluminum prices, shorter cathode life, or slower adoption.
Financial Analysis and Profitability
Based on analysis of a 5,000 systems a year plant, the financial profile is promising but uncertain, supported by strong interest in diesel replacement and recurring plate revenue, but highly dependent on technology performance and customer adoption. The profitability of the Aluminum Air EV Battery manufacturing business in India improves markedly with proven, licensed technology, long cathode life, high aluminum utilisation, smelter partnerships for plates and recycling, anchor customers in telecom and data centres, and a growing base of installed systems that buy replacement plates.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 35–50% | IMARC, at scale |
| Net Profit Margin | 15–30% | IMARC, at scale |
| Payback Period | 5–8 Years | Early-stage market |
| IRR (Internal Rate of Return) | 14–22% | Adoption dependent |
| Capacity Utilization (stable ops) | 40–70% | Pilot to scale |
| Break-even Capacity Utilization | 40–50% | High fixed costs |
Adoption speed and the recurring fuel business decide where a plant lands within these ranges. The margins above assume commercial scale and should be treated as targets rather than early-year results.
Returns can be strengthened by licensing proven technology, partnering with smelters on plates and recycling, focusing first on diesel replacement where economics are clearest, offering systems on lease with fuel contracts, using EV and clean energy incentives where eligible, and building intellectual property in cathodes.
Key Risks and Mitigation
The main risks are technology maturity and performance, competition from fast-improving lithium-ion and sodium-ion batteries, high cost per kilowatt-hour of aluminum fuel, slow customer adoption, recycling logistics, hydrogen and caustic safety issues, and dependence on foreign technology. Technology risk is reduced by licensing proven designs and extensive field trials; cost risk by smelter partnerships and recycling credits; market risk by focusing on diesel replacement; safety risk by robust design and testing; and dependence risk by building local R&D. Promoters often work with an Aluminum Air EV Battery Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for Aluminum Air EV Battery Manufacturing in India
Approvals for this plant centre on chemical handling, battery waste rules, product safety, and vehicle homologation, along with standard business registrations. Promoters setting up an Aluminum Air EV Battery Manufacturing Plant in India generally need the following:
- Pollution Control: Consent to Establish and Operate covering electrolyte and chemical handling.
- Battery Waste Rules: Producer registration and recycling obligations under the Battery Waste Management Rules.
- Vehicle Homologation: Testing at ARAI or ICAT under applicable automotive standards for EV applications.
- Product Safety: Electrical and safety testing for stationary systems as customers require.
- Technology Agreements: Technology license, patents, and import approvals for equipment and materials.
- Factory & Fire: Factory license, fire NOC, and hydrogen safety measures for test areas.
- Business & Trade Registrations: Business registration, GST, Udyam, trademark, and Import Export Code.
Technology agreements, customer validation, and vehicle homologation are usually on the critical path, since products cannot be sold at scale without proven performance and approvals. Starting with stationary applications while vehicle approvals progress shortens the time from investment decision to first revenue.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, products, state pollution control categories, customer specifications, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Aluminum Air EV Battery Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- Data centre backup: In August 2025, Phinergy partnered with US electrical contractor Rosendin to roll out aluminum-air backup generators for data centres.
- Emergency power: In February 2025, the New York Power Authority and Phinergy received a USD 1.5 million grant to demonstrate an alternative to emergency generators.
- Telecom pilots in India: In September 2023, Indus Towers signed an agreement with IOC Phinergy to deploy 300 aluminum-air energy systems at its tower sites.
- Aluminum supply chain: In July 2022, Hindalco signed an agreement with Phinergy and IOC Phinergy to develop aluminum plates and recycle spent material in India.
The common thread is growing commercial interest in stationary backup, early pilots in India, and the build-up of an aluminum supply and recycling chain. New entrants who secure proven technology, aluminum partners, and anchor customers will be best placed to grow.
How an Aluminum Air EV Battery Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from market demand and application choice to technology access, aluminum supply, plant design, approvals, and economics. It helps investors decide the right applications, scale, and location, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Aluminum Air EV Battery Financial Model covering system sales and leasing, recurring plate and recycling revenue, aluminum and cathode costs, technology fees, production yields, pilot and adoption timelines, labour, logistics, working capital, debt servicing, cash flows, break-even, return on investment, and payback under different adoption and price scenarios. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint an Aluminum Air EV Battery Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For an emerging technology like this, a strong DPR also clarifies the technology route, the aluminum supply and recycling plan, the first target applications, and the approval path, which together are the factors most likely to decide success. By testing results against slower adoption, higher costs, and competing batteries, the report turns a promising but early opportunity into a plan that lenders and partners can judge with confidence.
Frequently Asked Questions
What are the first steps to set up an aluminum air EV battery manufacturing plant in India?
Start by choosing your applications, such as telecom backup or EV range extenders, and securing access to proven technology through licensing or partnership. Then commission a feasibility study and DPR, line up aluminum plate and recycling partners, run field pilots with anchor customers, select a site near aluminum supply or customers, obtain approvals, and build cathode, assembly, and test facilities.
How much does it cost to set up an aluminum air EV battery manufacturing plant in India?
Investment ranges from about INR 15–30 crore for a pilot line of 500 to 1,000 systems a year to INR 80–150 crore for a commercial plant of about 5,000 systems a year, and INR 400–700 crore for a large integrated facility of 25,000 systems a year or more.
What are the main steps in making aluminum air EV battery?
The flow runs from aluminum alloy plate preparation through cathode mixing, coating and pressing, drying and lamination, frame moulding, cell and stack assembly, system integration, testing, and packing, with a separate loop for recycling spent material.
Which machinery does an aluminum air EV battery manufacturing plant need?
Key equipment includes plate cutting and surface treatment lines, planetary mixers, coating machines, roll presses, drying ovens, injection moulding machines, laser and ultrasonic welders, assembly lines, discharge test benches, and environmental chambers.
What raw materials are used for aluminum air EV battery?
The main inputs are aluminum alloy plates, air cathode materials such as carbon, catalysts, PTFE, and metal mesh, potassium hydroxide electrolyte, plastic frames and housings, pumps and scrubbers, and electronics.
How profitable is an aluminum air EV battery manufacturing plant in India?
IMARC's analysis indicates a 35 to 50% gross margin and a 15 to 30% net margin at commercial scale, but early years are likely to be loss-making or low margin while pilots convert into orders. Profitability depends on technology performance, aluminum costs, recycling, and adoption.
Which approvals does an aluminum air EV battery manufacturing plant need in India?
Typical approvals include pollution control consents, battery waste management registration, vehicle homologation for EV use, product safety testing, technology agreements, factory and fire approvals, and GST, Udyam, trademark, and Import Export Code registrations.
How do I get a feasibility study or DPR for an aluminum air EV battery manufacturing project?
A detailed feasibility study and DPR covers market demand, applications, technology access, aluminum supply, plant design, approvals, and full financials. Investors usually engage an Aluminum Air EV Battery Manufacturing Feasibility Study Consultant with experience in battery and clean energy projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

LED bulbs use light-emitting diodes mounted on a metal-core circuit board, powered by a small electronic driver and housed in a plastic and aluminium body with a diffuser and a standard B22 or E27 cap.
Inverters convert direct current from batteries or solar panels into the alternating current used by homes, shops, and factories.
Electrical control panels are steel enclosures that house circuit breakers, contactors, relays, busbars, meters, drives, and controllers to distribute power and control motors, machines, and processes safely.
Microchips, or integrated circuits and semiconductor devices, are the building blocks of phones, computers, vehicles, appliances, power systems, telecom networks, and defence equipment.
Resistors are the most widely used electronic components, found by the dozens or hundreds in almost every circuit board, from phones, laptops, and televisions to vehicles, appliances, telecom equipment, power electronics, medical devices, and defence systems.
Rare earth magnets, mainly neodymium-iron-boron (NdFeB) and samarium-cobalt, are the strongest permanent magnets made, and they sit at the heart of electric vehicle motors, wind turbine generators, electronics, industrial automation, medical devices, and defence systems. India imported over 53,000 tonnes of rare earth permanent magnets in 2024-25 and has almost no domestic production, while demand is expected to double by 2030.
Wires and cables carry power and signals through every home, office, factory, railway, data centre, and solar park, and India's market has grown to about USD 10 billion as construction, power transmission, renewable energy, and industrial investment have expanded.
Heat exchangers are among the most widely used pieces of engineering equipment in the world. Refineries, petrochemical and fertiliser plants, power stations, pharmaceutical and food factories, HVAC systems, and data centers all depend on them to heat, cool, condense, and recover energy from process streams.
India's trucks and buses rarely rest. They carry freight across highway corridors, move goods from ports and factories, and ferry millions of passengers every day, often under heavy loads and tough road conditions.
Silicon wafers are the thin, precisely sliced discs and squares on which solar cells and computer chips are built. India has rapidly become a major assembler of solar modules and is now building cell capacity, but almost all of the wafers those cells need are still imported.
Every video call, UPI payment, and 5G connection in India ultimately travels over glass. Fiber optic cables carry the country's data between cities, into mobile towers and data centres, and increasingly right into homes through fiber-to-the-home connections.
Setting up an Air Conditioner Manufacturing Plant in India is an assembly-driven, high-volume consumer durable venture, powered by rising household incomes, extreme summers, rapid urbanisation, and one of the lowest room air-conditioning penetration rates among large economies.
Setting up a High Voltage Cable Manufacturing Plant in India is a capital-intensive, high-value venture, powered by the country's massive power-transmission expansion, renewable-energy build-out, and the shift toward underground cabling in cities.
Setting up a Copper Cable Manufacturing Plant in India is a high-demand, infrastructure-driven venture, powered by the country's construction boom, rapid electrification, and steady industrial and appliance demand.
Setting up a Junction Box Manufacturing Plant in India is a high-demand, infrastructure-driven venture, powered by the country's construction boom, rapid electrification, and expanding solar and industrial sectors.
Setting up an Electric Cable Manufacturing Plant in India is a high-demand, infrastructure-linked venture, powered by the country's rapid growth in power, construction, renewable energy, and electrification. Cables and wires are essential to every building, factory, grid, and vehicle, giving an Electric Cable Manufacturing Plant a large and steadily growing market.
Setting up a Semiconductor Fabrication Manufacturing Plant in India is a highly capital-intensive but strategically transformative venture, driven by the country's semiconductor mission, deep policy incentives, and a vast import-substitution opportunity. Semiconductors are the foundation of every modern electronic and digital product, yet India currently imports almost all of its chip requirement.
Setting up a PCB Manufacturing Plant in India is a capital-intensive but strategically timed venture, driven by the country's electronics manufacturing push, strong policy incentives, and a large import-substitution opportunity. Printed circuit boards are the backbone of every electronic product, yet India still imports the overwhelming majority of its PCB requirement.
The Indian PCB (Printed Circuit Board) Market is emerging as the physical backbone of the country's electronics manufacturing ambitions. The market reached USD 7.27 Billion in 2025 and is projected to reach USD 25.48 Billion by 2034, growing at a CAGR of 14.96% (2026–2034), a total addressable market expansion driven by the Production Linked Incentive (PLI) scheme, 5G infrastructure rollout, and rising domestic consumer electronics demand.
Setting up an E-waste Recycling Plant in India is a capital-intensive but high-potential venture, driven by the country's soaring volume of discarded electronics, tightening Extended Producer Responsibility regulations, and the rising value of recovered metals. India is now among the world's largest generators of electronic waste, yet only a small share is processed through formal, compliant channels, leaving a large, policy-backed opportunity for organized recyclers who can capture volumes shifting from the informal sector.
Global semiconductor demand across automotive, data centers, and defense, highlighting market segmentation, key applications, regional dynamics, and industry shifts.
The hearables market represents one of the most dynamic segments within consumer electronics and wearable technology. These intelligent audio devices have evolved beyond simple wireless earbuds into multifunctional platforms combining premium audio with health monitoring, artificial intelligence, and seamless digital connectivity.
A smart washing machine is a sophisticated home appliance that incorporates advanced digital features such as connectivity, sensor technology, and automated controls for improved efficiency, convenience, and user control. In contrast to traditional washing machines, smart washing machines come pre-installed with advanced features such as Wi-Fi connectivity, smart load detection, smart detergent dispensing, and voice-control capability.
A smartphone is a portable electronic device that combines sophisticated capabilities in computer processing, wireless communication, multimedia entertainment, and internet access. Smartphones are distinct from other mobile phones in that their operation involves highly sophisticated platforms of operation that are capable of supporting multiple applications, multitasking, and connectivity with internet platforms.
Semiconductor manufacturing is a highly specialized industrial process that involves the design, fabrication, and assembly of semiconductor devices including integrated circuits (ICs), memory chips, sensors, and discrete components. The process transforms raw semiconductor materials, primarily silicon, into sophisticated electronic components through a combination of physical and chemical processing steps, such as wafer fabrication, photolithography, doping, etching, thin-film deposition, and packaging.
The retail landscape is experiencing a profound transformation as self-checkout systems emerge as critical infrastructure components reshaping consumer experiences and operational efficiency globally. These automated solutions enable customers to independently scan, bag, and pay for purchases without cashier assistance, representing a fundamental shift in modern commerce.
The webcams market is experiencing unprecedented transformation as digital communication becomes the cornerstone of modern business, education, and healthcare. Global webcam industry dynamics are being reshaped by technological innovation and evolving workplace models.
As smartphones become a way of life for most Filipinos, the market has changed dramatically and expectations from consumers are higher than ever before. With the demand for smartphones growing, there is a significant change in consumer shopping habits with more emphasis on using online platforms for shopping. This change is closely interlinked with the fast growth of the Philippines e-commerce market, both bringing opportunities and challenges to the stakeholders of the smartphone industry.
As technology continues to advance, lighting has transformed from a basic necessity into a strategic enabler of innovation, efficiency, and sustainability. The evolution from incandescent bulbs to LEDs, smart systems, and intelligent lighting networks represents not just technological change but a redefinition of how energy, design, and functionality intersect in the built environment.
An LED light is an illuminating device that utilizes Light Emitting Diodes as its source of light, generating light through a semiconductor-based process called electroluminescence. When electrical current flows across the semiconductor material of the diode, electrons emit energy as photons and thus produce highly efficient and concentrated illumination.
An LED bulb is a solid-state lighting device that uses Light Emitting Diodes (LEDs) as its illumination source. Different from incandescent or fluorescent lamps, light in LED bulbs is produced by electroluminescence, a process where the passing of an electric current through a semiconductor material emits photons directly. This process is highly energy-efficient, with a far larger percentage of the electricity being converted to usable light and very little heat generated in the process.
The junction box, generally made from plastic, metal, or composite materials, houses wire connections, terminations, and protective components to allow the safe distribution and routing of electrical circuits. The junction box will provide insulation, mechanical protection, and a secure environment to avoid accidental contact with live electrical parts, moisture intrusion, or dust accumulation.
The Japan power electronics market is poised to grow substantially, driven by rising demand in automotive, energy, industrial automation, and infrastructure sectors. According to IMARC Group, the Japan power electronics market is studied from 2019 to 2024 with projections extending to 2033.
Japan's printed circuit board (PCB) industry is the world leader in technology innovation, enabling consumer electronics, automotive, and next-generation communication system development. As a key enabler of modern electronic products, PCBs provide the essential building blocks for embedding semiconductors, sensors, and microchips into miniaturized, high-performance devices. Japan, through its world-class manufacturing base and engineering expertise, remains the hub of the global PCB supply chain.
Aluminum-Air (Al-Air) battery is a new energy storage technology that has attracted interest as a future alternative to conventional lithium-ion batteries, specifically for electric vehicle (EV) use. As opposed to normal rechargeable batteries, the Al-Air battery is a metal-air electrochemical cell with aluminum as the anode, oxygen from the ambient air as the cathode reactant, and a liquid electrolyte (commonly sodium hydroxide or potassium hydroxide) as the medium through which the reaction occurs.
Aluminium wire is an essential industrial commodity commonly employed in power transmission, electrical distribution, building construction, and manufacturing processes owing to its high conductivity-to-weight ratio, resistance to corrosion, and cost advantage over copper. Produced by methods including continuous casting, rolling, and drawing, aluminum wire is available in various grades and alloys to serve the wide demands, from overhead transmission conductors and building wiring to automotive harnesses and electronic applications.
Air conditioners are electromechanical devices used to control indoor climate by extracting heat and humidity and ensuring optimum air circulation. Generally consisting of a compressor, condenser, evaporator, refrigerant fluid, filters, fans, and electronic controls, air conditioners work based on the principle of heat exchange, moving heat from indoor areas to the external environment. Contemporary units come in diverse configurations, such as split systems, window units, central air systems, and portable models, supporting respective residential, commercial, and industrial applications. Some of the major characteristics are efficiency in cooling, energy use, noise rating, and environmental footprint in relation to refrigerant type.
E-waste, or electronic waste, is electrical and electronic equipment that has been discarded, such as computers, cell phones, television sets, servers, and household appliances. It is among the world's fastest-growing streams of waste, consisting of a heterogeneous combination of metals, plastics, glass, and toxic substances. E-waste contains valuable metals like copper, aluminum, gold, silver, palladium, and rare earth elements, in addition to toxic materials like lead, mercury, cadmium, and brominated flame retardants.
Polished silicon wafers are very pure, ultra-flat semiconductor substrates that are produced from high-quality single-crystal silicon. The wafers act as the material base for making integrated circuits, power devices, and MEMS (Microelectromechanical Systems). The wafers are made of monocrystalline silicon ingots using the Czochralski or Float-Zone process, from which the wafers are cut, lapped, etched, and polished to atomic-scale flatness and defect-free surfaces.
AI is revolutionizing Japan’s semiconductor industry by boosting innovation and efficiency across the entire value chain. Advanced artificial intelligence (AI)-powered Electronic Design Automation (EDA) tools significantly shorten chip design cycles, improving performance and energy efficiency.
Recent projections indicate that Australia semiconductor market, including services, is growing at a steady compound annual growth rate as the nation deepens its tech infrastructure. The importance of semiconductors spans electronics, defense systems, telecommunications, and emerging AI applications, which position the local ecosystem as strategically vital for growth.
Fiber optic cables are high-tech communications cables that carry information like bursts of light along extremely thin glass or plastic strands, providing high-speed, high-bandwidth connectivity with little loss of signal. Fiber optic cables make up the foundation of contemporary telecommunications, carrying internet, cloud computing, 5G networks, and smart infrastructure.
CAT (Category) cables are twisted-pair Ethernet cables utilized for copper-based wired network communications, varying from CAT5e to CAT8 standards. The cables carry data through copper conductors, but with different speeds (up to 40 Gbps for CAT8) and bandwidths, supporting networks such as LANs, data centers, and smart buildings.
India's semiconductor industry is undergoing a revolutionary phase driven by rising demand from industries like consumer electronics, automotive technologies, industrial automation, and telecom infrastructure.
USB data cables are critical elements of contemporary digital connectivity, enabling high-speed and consistent data transfer and power supply for a broad scope of electronic products. They provide the foundation for charging and synchronizing smartphones, tablets, laptops, and other peripherals, with significant applications in consumer electronics, industrial automation, and new technologies. With technologies like USB-C, the cables today carry faster data speeds, more power output, and universal compatibility, making them essential in a world that is connected.
Thin-film-transistor (TFT) liquid-crystal display (LCD) is a type of display technology used in many electronic devices, such as smartphones, tablets, laptops, and televisions (TVs). A backlight, colour filters, a thin-film transistor array, and a liquid crystal layer are among the layers that make up this flat-panel display. TFT LCDs are made to produce sharp images with superb viewing angles, strong contrast, and accurate colour reproduction. They are made up of thousands of tiny transistors that regulate how much light enters each pixel. This makes it possible for the display to generate crisp, detailed images at rapid refresh rates. TFT LCD technology's low power consumption is one of its main benefits, which makes it perfect for battery-operated gadgets.
Polycrystalline solar photovoltaic (PV) modules are a key component of solar energy systems, harnessing sunlight and converting it into electricity through the photovoltaic effect. These modules are composed of multiple interconnected solar cells, each made from polycrystalline silicon. Polycrystalline solar panels are renowned for their efficiency, affordability, and versatility, making them a popular choice for various applications such as solar installations, commercial and industrial projects, off-grid systems and solar farms.
The LED chip is the core component of an LED bulb, comprising semiconductor layers that enable the free flow of protons and electrons. Employed in all LED lighting fixtures—from bulbs to tubes—the LED chip fundamentally determines light quality, with variations in brightness, voltage, and wavelength. These chips are manufactured through a process called MOCVD (metal-organic chemical vapor deposition), which creates the semiconductor layers that facilitate electric flow. Major applications of these chips include backlighting, illumination, automotive lighting, signs, and signals.
Semiconductors are crucial components in the modern electronics industry, used in electronic equipment and devices to manage and control the flow of electricity. They are found in consumer items like smartphones, wearables, smart TVs, and advanced equipment used in industrial applications, defense, and aerospace. Semiconductors are further divided into four broad categories: optoelectronics, discrete components, integrated circuits, and sensors. Memory devices, logic devices, analog ICs, MPUs, discrete power devices, MCUs, and sensors are some of the major components of semiconductors.