Power Cable Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
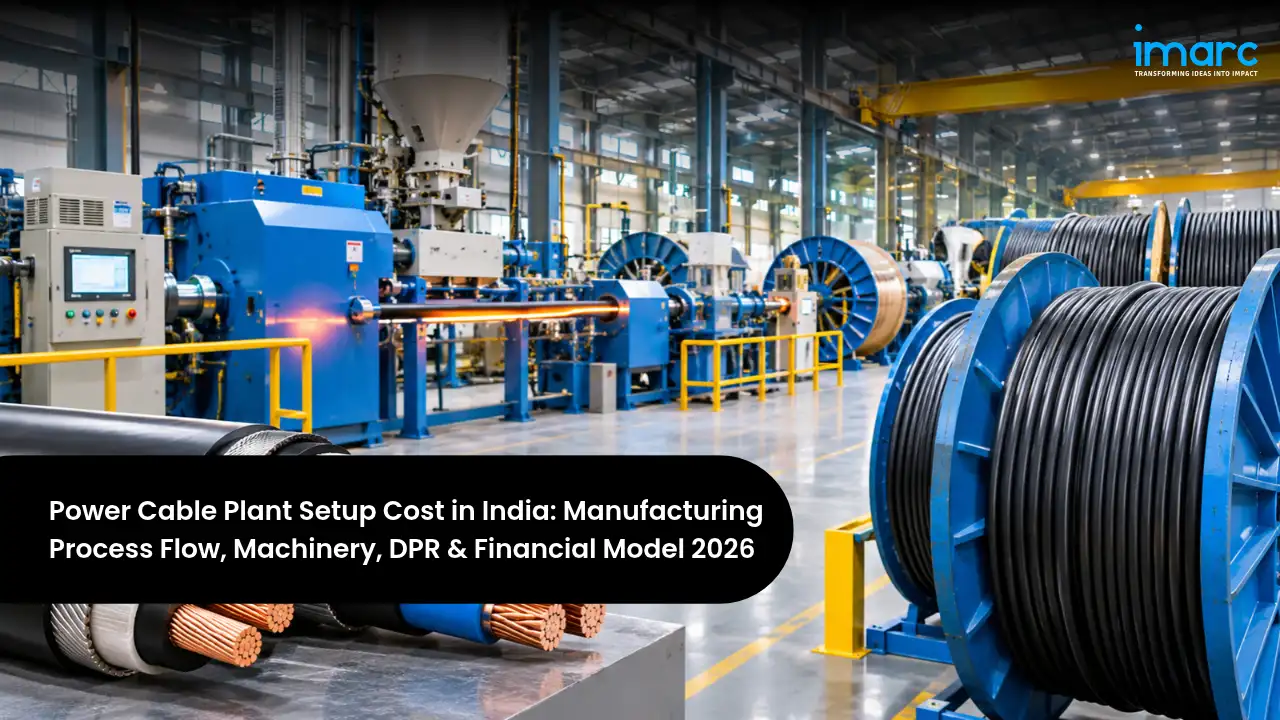
Setting up a Power Cable Manufacturing Plant in India puts an investor directly in the path of one of the country's largest infrastructure build-outs. Transmission and distribution networks are being expanded and modernised, renewable energy capacity is growing rapidly, cities are moving overhead lines underground, and data centres, metros, and industrial corridors all need reliable cabling. Every one of these projects runs on low-voltage, medium-voltage, and high-voltage power cables, and the domestic industry has been adding capacity steadily to keep up.
The overall Power Cable Manufacturing Plant Cost depends on the voltage range, conductor material, capacity, and how much of the process is integrated, with total investment for a typical LT and MV plant ranging from INR 30 crore to INR 250 crore, and considerably more for extra-high-voltage capability. Copper and aluminium make up the bulk of operating cost, so metal procurement and price pass-through are the decisions that matter most commercially. At healthy utilisation, a well-run Indian plant earns a net profit margin of 5 to 9% and an IRR of 15 to 22%, with payback usually within 4 to 6 years.
This guide is written for promoters and investors evaluating how to start a power cable manufacturing plant in India. It explains the main cable categories, the demand outlook, the production flow, the machinery and raw materials involved, location and infrastructure planning, a detailed cost and returns breakdown, the certifications and approvals required, and how a DPR turns all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Voltage Segments | Low, medium, high, and extra-high voltage |
| Conductor Materials | Copper and aluminium |
| Indicative Total Investment | INR 30–250 Crore (LT and MV) |
| Typical Payback Period | 4–6 Years |
The snapshot reflects a large, steadily growing market driven by public and private infrastructure spending rather than short-term consumer trends. Demand is broad, spanning utilities, renewable developers, EPC contractors, industry, and real estate, and quality certification acts as a strong filter on competition. The investment range reflects the choice between a focused LT plant and a larger facility with continuous vulcanisation lines for medium- and high-voltage cables.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | LT, MV, and HT power cables, PVC and XLPE |
| Total Project Investment | INR 30 – 250 Crore (LT and MV) |
| Payback Period | 4 – 6 Years |
| Net Profit Margin | 5 – 9% |
| IRR | 15 – 22% |
| Best Locations | Gujarat, Maharashtra, Haryana, Rajasthan, Uttarakhand, Tamil Nadu |
| Mandatory Approvals | BIS License, Utility Approvals, Factory License, SPCB, Fire NOC |
| Key Requirement | Metal price management and utility vendor approvals |
These parameters give a practical starting point for evaluation. Margins in cables are moderate in percentage terms, but high asset turnover and steady order books make returns on capital attractive when the plant is run well. A site-specific Power Cable Feasibility Report refines these figures to your voltage range, conductor mix, capacity, and target customers.
Table of Contents
- What is Power Cable Manufacturing?
- Why is Power Cable Manufacturing Growing in India?
- Power Cable Manufacturing Process Flow
- Raw Materials Required for Power Cable Manufacturing
- Location, Land & Infrastructure
- Power Cable Manufacturing Machinery and Equipment
- Power Cable Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Power Cable Manufacturing in India
- Recent Developments in the India Power Cable Manufacturing Industry
- How Power Cable Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Power Cable Manufacturing?
A power cable carries electrical energy from generation sources through transmission and distribution networks to end users. It is built in layers: a copper or aluminium conductor, insulation such as PVC or cross-linked polyethylene (XLPE), semiconducting screens and metallic screens for medium and higher voltages, an inner sheath, armouring for mechanical protection, and an outer sheath. Power cable manufacturing is the process of producing these layers to precise dimensions and electrical properties, then testing the finished cable against national and utility standards.
From a business perspective, the attraction is the breadth and durability of demand. Power utilities, transmission companies, renewable project developers, EPC contractors, railways and metros, industrial plants, data centres, and real estate developers all buy power cables, often through recurring tenders and framework contracts. A manufacturer with certified products, utility approvals, and reliable delivery can build a diversified and repeatable order book.
- Low-Voltage (LT) Cables: Cables up to 1.1 kV with PVC or XLPE insulation, used in buildings, industry, and distribution networks.
- Medium-Voltage (MV/HT) Cables: XLPE cables from 3.3 kV to 33 kV for utility distribution, renewable plants, and industrial substations.
- High and Extra-High-Voltage Cables: XLPE cables from 66 kV upward for transmission links, urban substations, and large projects.
- Special Power Cables: Fire-resistant, low-smoke, halogen-free, solar, and aerial bunched cables for specific applications.
Main Cable Categories by Voltage and Use
Deciding which categories the plant will produce is the foundational choice, because it drives machinery, testing infrastructure, and investment:
| Cable Type | Description | Key Property | Primary Demand |
|---|---|---|---|
| LT PVC / XLPE | Up to 1.1 kV | High volume, broad use | Buildings, industry, distribution |
| MV XLPE | 3.3 kV to 33 kV | Screened, CCV-made | Utilities, solar, wind, industry |
| HV / EHV XLPE | 66 kV and above | Highest technical barrier | Transmission and urban grids |
| Aerial Bunched | Insulated overhead conductors | Loss and theft reduction | Distribution utilities |
This decision shapes the entire factory. An LT plant can be built around extrusion, armouring, and sheathing lines with silane or PVC insulation, while MV cables need a continuous catenary vulcanisation line with triple extrusion and partial discharge testing. HV and EHV capability needs vertical or long catenary lines, very clean insulation handling, and specialised high-voltage test bays. Many new entrants start with LT and MV cables, build utility approvals and customer relationships, and then invest in higher voltages.
Why is Power Cable Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
India's power cable demand is underpinned by long-term infrastructure programmes rather than short cycles. IMARC Group values the Indian power cables market at USD 6.4 billion in 2025 and expects it to reach USD 9.7 billion by 2034:
- Transmission build-out: Transmission and distribution capex of around INR 9 trillion is expected through 2032 to integrate renewable energy and strengthen the grid.
- Distribution modernisation: The Revamped Distribution Sector Scheme, with sanctions of about INR 2.77 lakh crore, is funding loss reduction, network upgrades, and smart metering.
- Renewable energy: Large solar, wind, and hybrid parks need MV collection cables and HV evacuation links, supporting the 500 GW non-fossil capacity target for 2030.
- Urban undergrounding and fire safety: Cities, metros, airports, and high-rise buildings are adopting underground and fire-resistant, low-smoke cables.
- Data centres and industry: Rapid data centre growth, EV charging, and new manufacturing capacity are lifting demand for LT and MV power cables.
India-Specific Market Opportunity
| Segment | India Market Context | Manufacturing Role |
|---|---|---|
| Power Distribution | RDSS-funded network upgrades | LT, MV, and aerial bunched cables |
| Transmission | Large T&D capex pipeline | HV and EHV cables |
| Renewable Energy | Solar, wind, and hybrid parks | MV collection and solar cables |
| Infrastructure & Real Estate | Metros, airports, buildings | Fire-safe LT and MV cables |
| Industry & Data Centres | New plants and campuses | LT and MV power cables |
The strongest opportunity lies in a plant that serves several of these segments rather than depending on one. Utility tenders provide large volumes, renewable and data centre projects add steady private demand, and fire-safe and special cables carry better margins. A manufacturer that earns approvals with major utilities and EPC contractors early can build a resilient order book across cycles.
Power Cable Manufacturing Process Flow
Understanding the process helps you plan machinery, floor layout, and cost drivers. Cable production is a sequence of drawing, stranding, extrusion, and protective layering steps, each adding a precisely controlled layer to the conductor. The flow below reflects an armoured XLPE power cable; LT PVC cables follow a shorter version of the same sequence.
Step-by-Step Power Cable Manufacturing Process
Copper or aluminium rod is drawn into wire, stranded and compacted into a conductor, insulated, screened where required, laid up into multi-core form, then sheathed, armoured, and finally tested before being wound onto drums. Smooth material flow between these stages, and drum handling between machines, have a large effect on productivity in a cable plant.
| Unit Operation | Key Activity |
|---|---|
| Rod Breakdown & Wire Drawing | Copper or aluminium rod drawn to wire |
| Annealing | Wire softened for flexibility (copper) |
| Stranding & Compacting | Wires stranded into round or sector conductors |
| Insulation Extrusion | PVC or XLPE applied; triple extrusion for MV |
| Curing / Cross-linking | Silane curing (LT) or CCV dry curing (MV/HV) |
| Metallic Screening | Copper tape or wire screen applied (MV/HV) |
| Laying Up | Cores twisted together with fillers |
| Inner Sheath & Armouring | Bedding sheath and steel wire or strip armour |
| Outer Sheathing | PVC or special compound outer jacket |
| Testing & Drumming | Routine and type tests, then drum packing |
Two factors decide profitability across this flow. First, material efficiency: copper and aluminium are so expensive that small over-dimensioning of conductors or insulation adds up quickly, so precise process control directly improves margin. Second, first-time quality: MV and HV cables must pass partial discharge and high-voltage tests, and a failed length means costly rework or scrap. Routine testing of every drum, along with periodic type testing at accredited laboratories, is what keeps BIS licenses and utility approvals in good standing.
Raw Materials Required for Power Cable Manufacturing
The main inputs are copper or aluminium rod for the conductor, polymers for insulation and sheathing, and steel for armouring. Because metals account for most of the cost and their prices move with international commodity markets, procurement strategy and the ability to pass on price changes are central to the business.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Copper / Aluminium Rod | Conductor | Domestic smelters and imports | 55–70% |
| XLPE & Semiconductive Compounds | Insulation and screens | Domestic and imported | 6–10% |
| PVC & Special Sheathing Compounds | Inner and outer sheaths | Domestic compounders | 4–7% |
| GI Wire / Steel Strip | Armouring | Domestic steel suppliers | 3–6% |
| Copper Tape, Fillers & Drums | Screens, fillers, packing | Domestic suppliers | 3–6% |
With metals dominating cost, most cable makers link selling prices to copper and aluminium benchmarks through price variation clauses in tenders and contracts, and many hedge or buy against confirmed orders. India has a strong domestic aluminium base and growing copper refining capacity, but high-grade XLPE and semiconductive compounds for MV and HV cables are still partly imported, so qualifying more than one supplier protects both cost and continuity.
Location, Land & Infrastructure
Site selection is a key early decision in any Power Cable Manufacturing Plant Setup in India, because cables are heavy and shipped on bulky drums, and freight costs add up quickly. Proximity to major consumption regions, good road access for oversized loads, reliable power, and a supply of skilled machine operators usually matter more than proximity to raw materials.
Best Location for Power Cable Manufacturing Plant Setup in India
| State | Why It Works | Key Advantage |
|---|---|---|
| Gujarat | Halol, Vadodara, and nearby clusters | Large cable ecosystem and ports |
| Maharashtra | Pune, Nashik, and Mumbai region | Market access and engineering base |
| Haryana | NCR industrial belt | Northern market and logistics |
| Rajasthan | Bhiwadi and Neemrana estates | Land availability and NCR access |
| Uttarakhand | Haridwar and Roorkee estates | Established cable and electrical units |
| Tamil Nadu | Chennai and Hosur corridor | Southern utility and industrial demand |
The strongest locations combine an existing electrical and cable ecosystem, good highway connectivity for drum transport, and access to large utility and industrial demand centres. Western India, led by Gujarat and Maharashtra, hosts many of the largest cable plants, while the NCR belt and Uttarakhand serve the northern market and Tamil Nadu serves the south. Because freight is significant, many manufacturers choose a location close to their main customers and add regional depots as they grow.
BIS Certification and Testing Requirements
Certification is a basic condition for selling power cables in India. Under the Cables (Quality Control) Order, 2020, PVC insulated heavy-duty cables to IS 1554 and XLPE insulated cables to IS 7098, along with aerial bunched and other listed cables, must carry the BIS Standard Mark under license. Utilities and large EPC contractors also require vendor approval, which typically involves factory inspection and type tests at an accredited laboratory such as CPRI. In practice, a plant needs a well-equipped in-house laboratory with high-voltage AC testing, partial discharge measurement for MV cables, conductor resistance testing, and material testing, along with documented quality systems. Designing the test bay and quality processes into the plant from the start is far easier than adding them later.
Infrastructure Requirements (Mid-Sized Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 20,000 – 60,000 sq. meters | Long sheds for CCV and drum yards |
| Production Sheds | High-bay sheds with cranes | Space for long extrusion lines |
| Power Requirement | 2 – 8 MW | Extrusion and drawing are power-intensive |
| Testing Laboratory | HV test bay and PD lab | Needed for BIS and utility approvals |
| Cooling Water System | Recirculating cooling | For extrusion and drawing lines |
| Drum Yard & Warehousing | Open and covered storage | Large finished-goods footprint |
| Material Handling | EOT cranes and forklifts | Heavy drums and coils |
Infrastructure for a cable plant centres on long, high-bay production sheds, robust power supply, cooling water, and generous space for drums. MV and HV lines in particular need long buildings or tall towers, which should be planned from the outset even if the first phase is LT-focused. Under-sizing the drum yard and crane capacity is a common mistake that limits output as order volumes grow.
Power Cable Manufacturing Machinery and Equipment
The machinery set covers wire drawing, stranding, extrusion, curing, armouring, and testing, and the line-up depends on the voltage range and conductor materials. Lines must deliver precise dimensions and consistent quality over long continuous runs, since cable lengths can run to several kilometres per drum. The core machinery is summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Rod Breakdown Machine | Draw rod into wire | Multi-die, high speed |
| Annealer | Soften copper wire | In-line resistance annealing |
| Rigid / Bunching Stranders | Strand and compact conductors | Round and sector shapes |
| Insulation Extrusion Line | Apply PVC or XLPE | Precise diameter control |
| CCV Line (Triple Extrusion) | MV and HV insulation and curing | Dry curing, catenary design |
| Copper Tape Screening Machine | Apply metallic screen | Uniform overlap |
| Laying-Up Machine | Twist cores together | Drum twister type |
| Armouring Machine | Apply steel wire or strip | Multi-bobbin |
| Sheathing Extrusion Line | Inner and outer sheaths | With printing and marking |
| HV Test & PD Equipment | Routine and type testing | Partial discharge measurement |
Equipment selection should follow your product range rather than the other way around. An LT-focused plant can start with drawing, stranding, extrusion, armouring, and sheathing lines, while MV capability hinges on the CCV line, which is the single largest equipment investment and the main determinant of MV capacity. Test equipment is often under-budgeted, yet it is essential for BIS licenses, utility approvals, and customer confidence.
Power Cable Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below summarise the capital and operating cost structure of a mid-sized LT and MV cable facility in India, based on industry analysis. The total Power Cable Investment Cost for a specific project depends on voltage range, capacity, conductor mix, level of integration, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Land, Building & Sheds | 18–25% | Land, high-bay sheds, and civil works |
| Plant & Machinery | 35–45% | Drawing, stranding, extrusion, CCV, armouring |
| Testing Laboratory | 4–7% | HV test bay and PD lab |
| Utilities & Material Handling | 5–8% | Power, cooling, cranes |
| Pre-operative & Contingency | 3–6% | Engineering, DPR, and buffer |
| Working Capital | 20–30% | Metal inventory and receivables |
Working capital is unusually large in cables, because copper and aluminium inventory is costly and utility and EPC customers often take extended payment terms. Machinery, led by the CCV line for MV cables, forms the other major block. These elements are modelled carefully in a Power Cable Business Plan so that funding needs reflect real metal prices and customer credit periods.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials (metals, polymers) | 75–85% | Copper and aluminium dominate |
| Power & Utilities | 3–5% | Extrusion and drawing |
| Labour & Skilled Manpower | 3–5% | Operators, QC, and maintenance |
| Packing & Freight | 3–5% | Drums and heavy transport |
| Maintenance & Overheads | 2–4% | Line upkeep and plant overheads |
| Quality, Testing & Approvals | 1–2% | Type tests and certification |
With raw materials making up the vast majority of operating cost, this is fundamentally a metals-and-conversion business. Profitability depends on managing metal price risk, keeping conversion costs low, and controlling material usage per kilometre of cable. A sound model should track metal content per product, price pass-through arrangements, and working capital cycles closely.
Financial Analysis and Profitability
Based on analysis of a mid-sized facility, the financial profile is steady and asset-efficient, supported by long-term infrastructure demand and certification-driven entry barriers. The profitability of power cable manufacturing business in India improves with a higher share of MV and special cables, strong utility approvals, tight metal price management, and disciplined working capital.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 12–20% | Higher for MV and special cables |
| Net Profit Margin | 5–9% | After depreciation and Indian corporate taxes |
| Payback Period | 4–6 Years | Faster with strong order book |
| IRR (Internal Rate of Return) | 15–22% | Driven by high asset turnover |
| Capacity Utilization (stable ops) | 70–85% | Tenders and frameworks support volume |
| Break-even Capacity Utilization | 45–60% | Broad infrastructure demand |
Product mix and working capital management most determine outcomes. A plant making only commodity LT cables competes mainly on price, while one with MV, fire-safe, and solar cables and approvals with major utilities earns better margins and steadier orders. Because metal inventory and receivables tie up so much capital, collection discipline and price-variation clauses are as important to returns as production efficiency.
Returns can be strengthened by expanding into MV and special cables, winning approvals with utilities, transmission companies, and large EPC contractors, using price-variation contracts and hedging to manage metal risk, optimising conductor and insulation dimensions, and keeping receivable cycles short.
Key Risks and Mitigation
The principal risks are copper and aluminium price volatility, long receivable cycles with utilities and contractors, intense price competition in LT cables, and quality failures that can lead to loss of approvals. Metal risk is mitigated by price-linked contracts and back-to-back buying; credit risk by customer diversification and receivable discipline; competitive risk by moving up the voltage and specialty ladder; and quality risk by strong process control and testing. A manufacturer that treats metal management, approvals, and working capital as core priorities is far better placed to sustain returns.
Licenses and Approvals for Power Cable Manufacturing in India
Power cables are a regulated electrical product and are usually sold to utilities and large buyers with their own approval processes. Promoters planning a new plant generally need the following before commencing commercial supply:
- BIS Certification: Product licenses under the Cables (Quality Control) Order, 2020 for cables covered by IS 1554, IS 7098, and other listed standards.
- Type Testing and Utility Approvals: Type tests at accredited laboratories such as CPRI, and vendor approvals with utilities, transmission companies, and EPC contractors.
- Factory License: Factory establishment and industrial operation approval under the Occupational Safety, Health and Working Conditions Code, 2020.
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board (CTE and CTO).
- Quality Management Certification: ISO 9001 and related certifications commonly required by utilities and export customers.
- Business & Tax Registration: Company incorporation, GST registration, Udyam registration, and an Import Export Code.
- Fire Safety & Labour Registrations: Fire NOC, and employee welfare registrations such as EPF and ESI.
BIS licenses and utility vendor approvals sit on the critical path, because without them the plant cannot participate in most tenders. Type tests require finished samples, so they should be scheduled immediately after trial production. Many first-time promoters engage a Power Cable Manufacturing Consultant in India to plan certification, type testing, and vendor registration alongside commissioning, which can bring forward the first tender wins by several months.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, product range, voltage class, target customers, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Power Cable Manufacturing Industry
Several current trends give useful context for investors considering this industry:
- Transmission and distribution capex cycle: Analysts expect around INR 9 trillion of T&D investment through 2032, with an expanding HVDC pipeline and continued RDSS-funded distribution upgrades.
- Capacity expansion by leading players: Established cable manufacturers are adding MV, HV, and EHV capacity to meet rising utility and renewable demand, signalling confidence in the long-term outlook.
- Fire-safe and data centre cabling: Fire-resistant, low-smoke, and halogen-free cables are gaining share in metros, airports, high-rise buildings, and the fast-growing data centre segment.
The common thread is a long infrastructure cycle with demand moving toward higher voltages and higher specifications. For a new entrant, the clear implication is to build certified, efficient capacity with a path into MV and special cables, and to secure utility and EPC approvals early so the plant can participate fully in the investment wave.
How Power Cable Manufacturing Project Report and DPR Helps Investors
A detailed project report and DPR provides a structured roadmap for the facility, covering market demand, product and voltage selection, process design, machinery, plant layout, utilities, certification pathway, and economics. It helps investors choose the right capacity and product mix, estimate capital expenditure (CapEx) and operating expenditure (OpEx), assess profitability, and identify risks before implementation.
At its core sits a Power Cable Financial Model with product-wise revenues, metal-linked cost build-up, working capital cycles, cash flow projections, break-even analysis, return on investment (ROI), and payback calculations. Lenders pay particular attention to metal price assumptions and receivable periods, so these must be realistic. Many investors work with a Power Cable Plant Project Report Consultant in India or a Power Cable Manufacturing Feasibility Study Consultant to prepare and validate these documents for bank appraisal.
For a cable project specifically, a strong DPR also clarifies the voltage roadmap, the LT-versus-MV product mix, the certification and vendor approval plan, and the metal risk strategy, which are the factors most likely to decide success. By testing returns against metal price swings, slower approvals, and longer collection cycles, the report turns a competitive but well-supported opportunity into a plan that lenders and partners can back with confidence.
Frequently Asked Questions
How to start a power cable manufacturing plant in India?
Begin by choosing your voltage range and product mix, then commission a feasibility study and DPR. Secure land with good highway access, install drawing, stranding, extrusion, armouring, and testing lines, obtain BIS licenses and pollution consents, complete type tests, and register as an approved vendor with utilities and EPC contractors.
What is the power cable manufacturing plant setup cost in India?
An LT and MV cable plant typically needs INR 30 crore to INR 250 crore, depending on capacity and product range, with HV and EHV capability requiring significantly more. Machinery and working capital are the largest cost items.
What is the process flow for making power cables?
The flow runs from rod breakdown and wire drawing through annealing, stranding and compacting, insulation extrusion and curing, metallic screening, laying up, inner sheathing, armouring, outer sheathing, and finally routine testing and drumming.
What machinery is needed for a power cable manufacturing factory?
Key machines include a rod breakdown machine, annealer, stranders, insulation extrusion lines, a CCV line for MV cables, copper tape screening, laying-up and armouring machines, sheathing lines, and high-voltage and partial discharge test equipment.
What raw materials are used to make power cables?
The main materials are copper or aluminium rod for conductors, XLPE and semiconductive compounds for insulation and screens, PVC or special compounds for sheaths, galvanised steel wire or strip for armour, copper tape, fillers, and cable drums.
Is a power cable business profitable in India?
Yes. A well-run plant typically earns a 5 to 9% net margin and a 15 to 22% IRR, with payback in 4 to 6 years. Returns improve with MV and special cables, utility approvals, metal price pass-through, and tight working capital management.
What licenses are required for a power cable manufacturing unit in India?
A plant needs BIS licenses under the Cables Quality Control Order, type test certificates and utility vendor approvals, a Factory License, State Pollution Control Board consents, a Fire NOC, ISO certification, and GST, Udyam, and labour registrations.
Which state is best for a power cable manufacturing plant?
Gujarat, Maharashtra, Haryana, Rajasthan, Uttarakhand, and Tamil Nadu are popular choices. The right location depends on your target customers, freight distances for heavy drums, power availability, and state incentives.
How do I get a feasibility study or DPR for a power cable manufacturing plant?
A professionally prepared DPR covers market assessment, product and voltage selection, technical design, certification pathway, costs, and financial projections suitable for bank appraisal. Many promoters work with a Power Cable Business Plan Consultant in India to prepare it and align it with lender and subsidy requirements.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Servos are precision electric motors fitted with a position sensor, called an encoder, and paired with an electronic drive that controls speed, torque, and position very accurately.
PVC-insulated wires and cables are made by drawing copper or aluminium rod into fine conductors, annealing and stranding them, and covering them with coloured PVC insulation and, for multi-core cables, an outer PVC sheath and sometimes steel armour.
Portable chargers are compact battery packs made from lithium-ion or lithium-polymer cells, a charging and protection circuit board, ports or wireless coils, and a plastic or metal casing.
Small electric cooking and food preparation products, such as mixer grinders, induction cooktops, electric kettles, air fryers, hand blenders, and sandwich makers, are made by moulding plastic bodies, forming steel and aluminium parts, winding motors or fitting heating elements, assembling control boards, and wiring and testing each unit for safety.
Aluminum-air batteries generate electricity by reacting aluminum plates with oxygen from the air in a water-based electrolyte. Aluminum has a very high theoretical energy density, and instead of being recharged from a socket, spent plates are swapped for fresh ones while the aluminum hydroxide produced is recycled into new aluminum.
LED bulbs use light-emitting diodes mounted on a metal-core circuit board, powered by a small electronic driver and housed in a plastic and aluminium body with a diffuser and a standard B22 or E27 cap.
Inverters convert direct current from batteries or solar panels into the alternating current used by homes, shops, and factories.
Electrical control panels are steel enclosures that house circuit breakers, contactors, relays, busbars, meters, drives, and controllers to distribute power and control motors, machines, and processes safely.
Microchips, or integrated circuits and semiconductor devices, are the building blocks of phones, computers, vehicles, appliances, power systems, telecom networks, and defence equipment.
Resistors are the most widely used electronic components, found by the dozens or hundreds in almost every circuit board, from phones, laptops, and televisions to vehicles, appliances, telecom equipment, power electronics, medical devices, and defence systems.
Rare earth magnets, mainly neodymium-iron-boron (NdFeB) and samarium-cobalt, are the strongest permanent magnets made, and they sit at the heart of electric vehicle motors, wind turbine generators, electronics, industrial automation, medical devices, and defence systems. India imported over 53,000 tonnes of rare earth permanent magnets in 2024-25 and has almost no domestic production, while demand is expected to double by 2030.
Wires and cables carry power and signals through every home, office, factory, railway, data centre, and solar park, and India's market has grown to about USD 10 billion as construction, power transmission, renewable energy, and industrial investment have expanded.
Heat exchangers are among the most widely used pieces of engineering equipment in the world. Refineries, petrochemical and fertiliser plants, power stations, pharmaceutical and food factories, HVAC systems, and data centers all depend on them to heat, cool, condense, and recover energy from process streams.
India's trucks and buses rarely rest. They carry freight across highway corridors, move goods from ports and factories, and ferry millions of passengers every day, often under heavy loads and tough road conditions.
Silicon wafers are the thin, precisely sliced discs and squares on which solar cells and computer chips are built. India has rapidly become a major assembler of solar modules and is now building cell capacity, but almost all of the wafers those cells need are still imported.
Every video call, UPI payment, and 5G connection in India ultimately travels over glass. Fiber optic cables carry the country's data between cities, into mobile towers and data centres, and increasingly right into homes through fiber-to-the-home connections.
Setting up an Air Conditioner Manufacturing Plant in India is an assembly-driven, high-volume consumer durable venture, powered by rising household incomes, extreme summers, rapid urbanisation, and one of the lowest room air-conditioning penetration rates among large economies.
Setting up a High Voltage Cable Manufacturing Plant in India is a capital-intensive, high-value venture, powered by the country's massive power-transmission expansion, renewable-energy build-out, and the shift toward underground cabling in cities.
Setting up a Copper Cable Manufacturing Plant in India is a high-demand, infrastructure-driven venture, powered by the country's construction boom, rapid electrification, and steady industrial and appliance demand.
Setting up a Junction Box Manufacturing Plant in India is a high-demand, infrastructure-driven venture, powered by the country's construction boom, rapid electrification, and expanding solar and industrial sectors.
Setting up an Electric Cable Manufacturing Plant in India is a high-demand, infrastructure-linked venture, powered by the country's rapid growth in power, construction, renewable energy, and electrification. Cables and wires are essential to every building, factory, grid, and vehicle, giving an Electric Cable Manufacturing Plant a large and steadily growing market.
Setting up a Semiconductor Fabrication Manufacturing Plant in India is a highly capital-intensive but strategically transformative venture, driven by the country's semiconductor mission, deep policy incentives, and a vast import-substitution opportunity. Semiconductors are the foundation of every modern electronic and digital product, yet India currently imports almost all of its chip requirement.
Setting up a PCB Manufacturing Plant in India is a capital-intensive but strategically timed venture, driven by the country's electronics manufacturing push, strong policy incentives, and a large import-substitution opportunity. Printed circuit boards are the backbone of every electronic product, yet India still imports the overwhelming majority of its PCB requirement.
The Indian PCB (Printed Circuit Board) Market is emerging as the physical backbone of the country's electronics manufacturing ambitions. The market reached USD 7.27 Billion in 2025 and is projected to reach USD 25.48 Billion by 2034, growing at a CAGR of 14.96% (2026–2034), a total addressable market expansion driven by the Production Linked Incentive (PLI) scheme, 5G infrastructure rollout, and rising domestic consumer electronics demand.
Setting up an E-waste Recycling Plant in India is a capital-intensive but high-potential venture, driven by the country's soaring volume of discarded electronics, tightening Extended Producer Responsibility regulations, and the rising value of recovered metals. India is now among the world's largest generators of electronic waste, yet only a small share is processed through formal, compliant channels, leaving a large, policy-backed opportunity for organized recyclers who can capture volumes shifting from the informal sector.
Global semiconductor demand across automotive, data centers, and defense, highlighting market segmentation, key applications, regional dynamics, and industry shifts.
The hearables market represents one of the most dynamic segments within consumer electronics and wearable technology. These intelligent audio devices have evolved beyond simple wireless earbuds into multifunctional platforms combining premium audio with health monitoring, artificial intelligence, and seamless digital connectivity.
A smart washing machine is a sophisticated home appliance that incorporates advanced digital features such as connectivity, sensor technology, and automated controls for improved efficiency, convenience, and user control. In contrast to traditional washing machines, smart washing machines come pre-installed with advanced features such as Wi-Fi connectivity, smart load detection, smart detergent dispensing, and voice-control capability.
A smartphone is a portable electronic device that combines sophisticated capabilities in computer processing, wireless communication, multimedia entertainment, and internet access. Smartphones are distinct from other mobile phones in that their operation involves highly sophisticated platforms of operation that are capable of supporting multiple applications, multitasking, and connectivity with internet platforms.
Semiconductor manufacturing is a highly specialized industrial process that involves the design, fabrication, and assembly of semiconductor devices including integrated circuits (ICs), memory chips, sensors, and discrete components. The process transforms raw semiconductor materials, primarily silicon, into sophisticated electronic components through a combination of physical and chemical processing steps, such as wafer fabrication, photolithography, doping, etching, thin-film deposition, and packaging.
The retail landscape is experiencing a profound transformation as self-checkout systems emerge as critical infrastructure components reshaping consumer experiences and operational efficiency globally. These automated solutions enable customers to independently scan, bag, and pay for purchases without cashier assistance, representing a fundamental shift in modern commerce.
The webcams market is experiencing unprecedented transformation as digital communication becomes the cornerstone of modern business, education, and healthcare. Global webcam industry dynamics are being reshaped by technological innovation and evolving workplace models.
As smartphones become a way of life for most Filipinos, the market has changed dramatically and expectations from consumers are higher than ever before. With the demand for smartphones growing, there is a significant change in consumer shopping habits with more emphasis on using online platforms for shopping. This change is closely interlinked with the fast growth of the Philippines e-commerce market, both bringing opportunities and challenges to the stakeholders of the smartphone industry.
As technology continues to advance, lighting has transformed from a basic necessity into a strategic enabler of innovation, efficiency, and sustainability. The evolution from incandescent bulbs to LEDs, smart systems, and intelligent lighting networks represents not just technological change but a redefinition of how energy, design, and functionality intersect in the built environment.
An LED light is an illuminating device that utilizes Light Emitting Diodes as its source of light, generating light through a semiconductor-based process called electroluminescence. When electrical current flows across the semiconductor material of the diode, electrons emit energy as photons and thus produce highly efficient and concentrated illumination.
An LED bulb is a solid-state lighting device that uses Light Emitting Diodes (LEDs) as its illumination source. Different from incandescent or fluorescent lamps, light in LED bulbs is produced by electroluminescence, a process where the passing of an electric current through a semiconductor material emits photons directly. This process is highly energy-efficient, with a far larger percentage of the electricity being converted to usable light and very little heat generated in the process.
The junction box, generally made from plastic, metal, or composite materials, houses wire connections, terminations, and protective components to allow the safe distribution and routing of electrical circuits. The junction box will provide insulation, mechanical protection, and a secure environment to avoid accidental contact with live electrical parts, moisture intrusion, or dust accumulation.
The Japan power electronics market is poised to grow substantially, driven by rising demand in automotive, energy, industrial automation, and infrastructure sectors. According to IMARC Group, the Japan power electronics market is studied from 2019 to 2024 with projections extending to 2033.
Japan's printed circuit board (PCB) industry is the world leader in technology innovation, enabling consumer electronics, automotive, and next-generation communication system development. As a key enabler of modern electronic products, PCBs provide the essential building blocks for embedding semiconductors, sensors, and microchips into miniaturized, high-performance devices. Japan, through its world-class manufacturing base and engineering expertise, remains the hub of the global PCB supply chain.
Aluminum-Air (Al-Air) battery is a new energy storage technology that has attracted interest as a future alternative to conventional lithium-ion batteries, specifically for electric vehicle (EV) use. As opposed to normal rechargeable batteries, the Al-Air battery is a metal-air electrochemical cell with aluminum as the anode, oxygen from the ambient air as the cathode reactant, and a liquid electrolyte (commonly sodium hydroxide or potassium hydroxide) as the medium through which the reaction occurs.
Aluminium wire is an essential industrial commodity commonly employed in power transmission, electrical distribution, building construction, and manufacturing processes owing to its high conductivity-to-weight ratio, resistance to corrosion, and cost advantage over copper. Produced by methods including continuous casting, rolling, and drawing, aluminum wire is available in various grades and alloys to serve the wide demands, from overhead transmission conductors and building wiring to automotive harnesses and electronic applications.
Air conditioners are electromechanical devices used to control indoor climate by extracting heat and humidity and ensuring optimum air circulation. Generally consisting of a compressor, condenser, evaporator, refrigerant fluid, filters, fans, and electronic controls, air conditioners work based on the principle of heat exchange, moving heat from indoor areas to the external environment. Contemporary units come in diverse configurations, such as split systems, window units, central air systems, and portable models, supporting respective residential, commercial, and industrial applications. Some of the major characteristics are efficiency in cooling, energy use, noise rating, and environmental footprint in relation to refrigerant type.
E-waste, or electronic waste, is electrical and electronic equipment that has been discarded, such as computers, cell phones, television sets, servers, and household appliances. It is among the world's fastest-growing streams of waste, consisting of a heterogeneous combination of metals, plastics, glass, and toxic substances. E-waste contains valuable metals like copper, aluminum, gold, silver, palladium, and rare earth elements, in addition to toxic materials like lead, mercury, cadmium, and brominated flame retardants.
Polished silicon wafers are very pure, ultra-flat semiconductor substrates that are produced from high-quality single-crystal silicon. The wafers act as the material base for making integrated circuits, power devices, and MEMS (Microelectromechanical Systems). The wafers are made of monocrystalline silicon ingots using the Czochralski or Float-Zone process, from which the wafers are cut, lapped, etched, and polished to atomic-scale flatness and defect-free surfaces.
AI is revolutionizing Japan’s semiconductor industry by boosting innovation and efficiency across the entire value chain. Advanced artificial intelligence (AI)-powered Electronic Design Automation (EDA) tools significantly shorten chip design cycles, improving performance and energy efficiency.
Recent projections indicate that Australia semiconductor market, including services, is growing at a steady compound annual growth rate as the nation deepens its tech infrastructure. The importance of semiconductors spans electronics, defense systems, telecommunications, and emerging AI applications, which position the local ecosystem as strategically vital for growth.
Fiber optic cables are high-tech communications cables that carry information like bursts of light along extremely thin glass or plastic strands, providing high-speed, high-bandwidth connectivity with little loss of signal. Fiber optic cables make up the foundation of contemporary telecommunications, carrying internet, cloud computing, 5G networks, and smart infrastructure.
CAT (Category) cables are twisted-pair Ethernet cables utilized for copper-based wired network communications, varying from CAT5e to CAT8 standards. The cables carry data through copper conductors, but with different speeds (up to 40 Gbps for CAT8) and bandwidths, supporting networks such as LANs, data centers, and smart buildings.
India's semiconductor industry is undergoing a revolutionary phase driven by rising demand from industries like consumer electronics, automotive technologies, industrial automation, and telecom infrastructure.
USB data cables are critical elements of contemporary digital connectivity, enabling high-speed and consistent data transfer and power supply for a broad scope of electronic products. They provide the foundation for charging and synchronizing smartphones, tablets, laptops, and other peripherals, with significant applications in consumer electronics, industrial automation, and new technologies. With technologies like USB-C, the cables today carry faster data speeds, more power output, and universal compatibility, making them essential in a world that is connected.
Thin-film-transistor (TFT) liquid-crystal display (LCD) is a type of display technology used in many electronic devices, such as smartphones, tablets, laptops, and televisions (TVs). A backlight, colour filters, a thin-film transistor array, and a liquid crystal layer are among the layers that make up this flat-panel display. TFT LCDs are made to produce sharp images with superb viewing angles, strong contrast, and accurate colour reproduction. They are made up of thousands of tiny transistors that regulate how much light enters each pixel. This makes it possible for the display to generate crisp, detailed images at rapid refresh rates. TFT LCD technology's low power consumption is one of its main benefits, which makes it perfect for battery-operated gadgets.
Polycrystalline solar photovoltaic (PV) modules are a key component of solar energy systems, harnessing sunlight and converting it into electricity through the photovoltaic effect. These modules are composed of multiple interconnected solar cells, each made from polycrystalline silicon. Polycrystalline solar panels are renowned for their efficiency, affordability, and versatility, making them a popular choice for various applications such as solar installations, commercial and industrial projects, off-grid systems and solar farms.
The LED chip is the core component of an LED bulb, comprising semiconductor layers that enable the free flow of protons and electrons. Employed in all LED lighting fixtures—from bulbs to tubes—the LED chip fundamentally determines light quality, with variations in brightness, voltage, and wavelength. These chips are manufactured through a process called MOCVD (metal-organic chemical vapor deposition), which creates the semiconductor layers that facilitate electric flow. Major applications of these chips include backlighting, illumination, automotive lighting, signs, and signals.
Semiconductors are crucial components in the modern electronics industry, used in electronic equipment and devices to manage and control the flow of electricity. They are found in consumer items like smartphones, wearables, smart TVs, and advanced equipment used in industrial applications, defense, and aerospace. Semiconductors are further divided into four broad categories: optoelectronics, discrete components, integrated circuits, and sensors. Memory devices, logic devices, analog ICs, MPUs, discrete power devices, MCUs, and sensors are some of the major components of semiconductors.