Recycled Aluminium Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
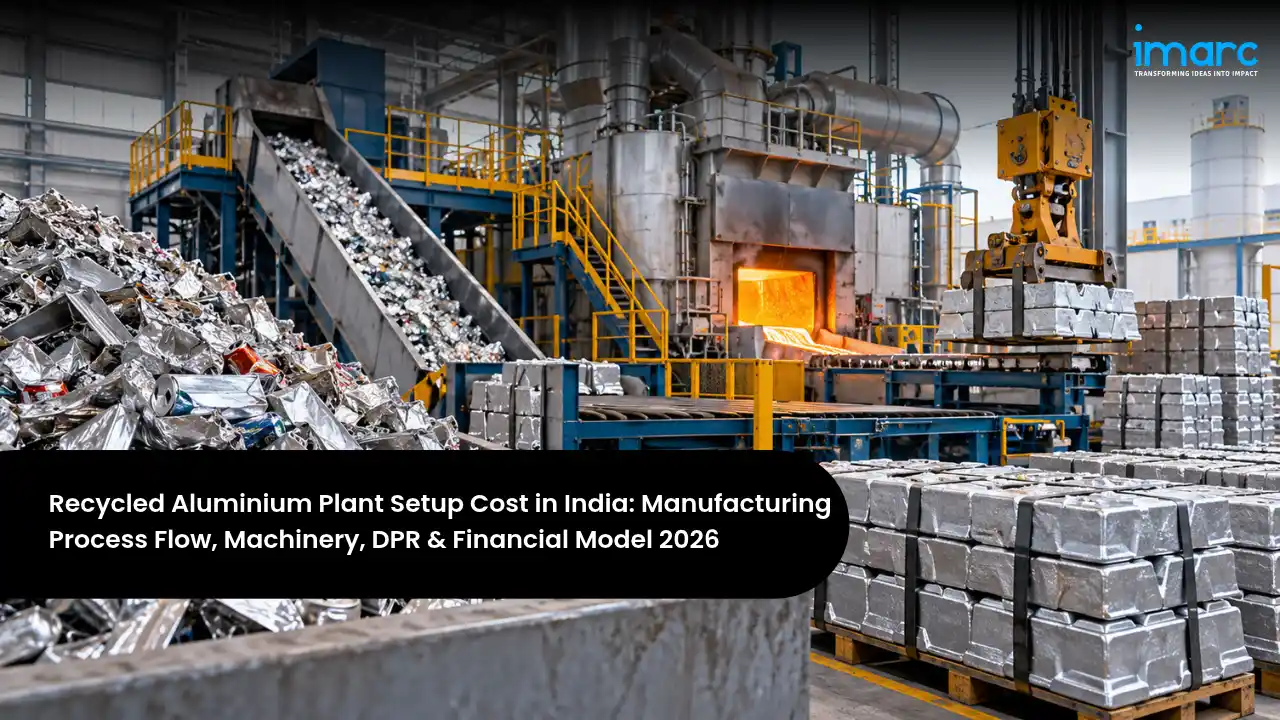
Recycled, or secondary, aluminium is made by melting aluminium scrap and refining it into alloy ingots, billets, and liquid metal, using about 95% less energy than making primary aluminium from bauxite. It feeds automotive die-casting, extrusions, castings, steel deoxidation, and packaging. India produced nearly 2.2 million tonnes of secondary aluminium in 2025-26, meeting around 35% of the country's aluminium needs, and imported nearly 2 million tonnes of scrap in 2025, making it one of the world's largest scrap buyers. With fast-growing vehicle production, lightweighting, and pressure to cut carbon emissions, Recycled Aluminium Manufacturing Plant Setup in India is an attractive opportunity in the metals and circular economy space.
Investment depends above all on scale, scrap preparation, and the products made. A small unit melting sorted scrap in a rotary furnace and casting ingots is a modest project, an integrated plant with shredding, sorting, decoating, multiple furnaces, and alloy casting is a substantial investment, and a large plant supplying billets, slabs, or liquid metal to rolling and extrusion mills needs much more capital. The Recycled Aluminium Manufacturing Plant Cost ranges from about INR 8–20 crore for a small unit of 3,000 to 6,000 tonnes a year to INR 80–200 crore for an integrated plant of 30,000 to 60,000 tonnes a year, and INR 500–1,000 crore for a large plant of 1 to 2 lakh tonnes a year. Raw materials, mainly scrap, make up 80 to 85% of operating cost, so scrap buying, metal recovery, and alloy pricing shape profitability. A well-run plant typically earns a gross margin of 15 to 25% and a net margin of 5 to 10%.
This guide is written for investors exploring how to start a Recycled Aluminium manufacturing plant in India. It focuses on an integrated plant of about 50,000 tonnes a year making die-casting alloy ingots and liquid metal for automotive and engineering foundries, and also explains small ingot units and large plants making billets and slabs. It covers products and markets, the demand outlook, the recycling process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, approvals, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Global Recycled Aluminium Market (2025) | USD 54.46 Billion |
| Projected Global Market (2034) | USD 94.39 Billion, 6.3% CAGR |
| India Secondary Aluminium Output (FY26) | Nearly 2.2 Million Tonnes |
| Share of India Aluminium Consumption | Around 35% |
| India Aluminium Scrap Imports (2025) | Nearly 2 Million Tonnes |
| Indicative Total Investment | INR 8 Crore to 1,000 Crore |
The snapshot shows a fast-growing global market and an Indian industry that has more than doubled its output in a decade, but still depends on imports for 80 to 85% of its scrap. Rising vehicle production, demand for low-carbon metal, and growing domestic scrap from end-of-life vehicles and buildings support long-term growth. The wide investment range reflects a real choice between a small ingot unit, an integrated alloy plant, and a large plant making billets and slabs. The sections below work through that choice.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Die-casting alloy ingots, liquid metal, billets, slabs, and deox aluminium |
| Plant Capacity | 3,000 – 2,00,000 Tonnes Per yYear |
| Total Project Investment | INR 8–20 Crore (small unit) to 500–1,000 Crore (large plant) |
| Payback Period | 4 – 6 Years |
| Net Profit Margin | 5 – 10% |
| IRR | 14 – 20% |
| Preferred States | Gujarat, Haryana, Tamil Nadu, Maharashtra, Rajasthan, Uttarakhand |
| Key Requirement | Reliable scrap supply, good sorting, and auto and foundry customers |
These ranges provide a realistic frame for early planning, but actual returns depend on scrap prices and availability, import duty and export restrictions in supplier countries, metal recovery rates, energy costs, alloy premiums over the London Metal Exchange price, customer approvals, and environmental compliance costs. A site-specific Recycled Aluminium Feasibility Report narrows each of these assumptions to your chosen products, capacity, location, and customers.
Table of Contents
- What is Recycled Aluminium Manufacturing?
- Why is Recycled Aluminium Manufacturing Growing in India?
- Recycled Aluminium Manufacturing Process Flow
- Raw Materials Required for Recycled Aluminium Manufacturing
- Location, Land & Infrastructure
- Recycled Aluminium Manufacturing Machinery and Equipment
- Recycled Aluminium Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Recycled Aluminium Manufacturing in India
- Recent Developments in the India Recycled Aluminium Manufacturing Industry
- How a Recycled Aluminium Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Recycled Aluminium Manufacturing?
Recycled aluminium is produced by collecting aluminium scrap, such as old castings, extrusion and sheet scrap, used beverage cans, wheels, wires, and production offcuts, then sorting, cleaning, melting, and refining it into new metal. Because aluminium can be recycled again and again without losing its properties, recycled metal can replace primary aluminium in most uses. The metal's chemistry is adjusted by adding silicon, copper, magnesium, and other elements to make standard alloys, and impurities and gases are removed before casting. Recycling uses only a small fraction of the energy needed to make primary aluminium, so it greatly reduces costs and carbon emissions.
Commercially, recycled aluminium is sold as alloy ingots, liquid metal delivered hot to nearby foundries, extrusion billets, rolling slabs, and deoxidation products for steel plants, usually under monthly or term contracts priced against the LME. A Recycled Aluminium Manufacturing Plant can supply automotive and two-wheeler die-casting foundries, engineering and electrical casting makers, extrusion and rolling mills, steel plants needing deoxidisers, and export buyers. Buyers value consistent chemistry, low inclusions and gas, reliable delivery, and competitive pricing.
- Automotive Die-Casting: Alloy ingots and liquid metal for engine and body parts.
- Engineering Castings: Alloys for pumps, motors, and appliances.
- Extrusion & Rolling: Billets and slabs from clean, sorted scrap.
- Steel Industry: Deoxidation aluminium in notch bars and shots.
The Main Recycled Aluminium Products and Applications
Choosing the product range is the most important commercial decision, because it determines scrap grades, equipment, and customers:
| Product | Description | Key Property | Primary Demand |
|---|---|---|---|
| Die-Casting Alloy Ingots | ADC12, LM6, LM24 grades | Castability | Auto and two-wheeler parts |
| Liquid Metal | Molten alloy delivered hot | Saves remelting cost | Nearby foundries |
| Extrusion Billets | 6000-series alloys | Formability | Windows, profiles |
| Rolling Slabs | Sheet-grade alloys | Clean, low iron | Rolling mills |
| Deox Aluminium | Notch bars, cubes, shots | Oxygen removal | Steel plants |
| Remelt Ingots | General-purpose ingots | Flexible use | Smaller foundries |
These choices shape the whole plant. Die-casting alloys are the largest segment in India and can use mixed scrap with careful alloying, while billets and slabs need clean, well-sorted scrap and higher-grade casting equipment. Liquid metal supply saves energy for both the recycler and the foundry but requires customers close by. Most new entrants therefore start with die-casting alloy ingots for automotive and engineering foundries, and add liquid metal, billets, or deox products once their sourcing and quality systems are established.
Why is Recycled Aluminium Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
Demand is supported by vehicle production, lightweighting, decarbonisation, and infrastructure growth:
- Automotive growth: Cars, two-wheelers, and commercial vehicles use large volumes of cast aluminium parts.
- Lightweighting and EVs: Electric and fuel-efficient vehicles use more aluminium to save weight.
- Low-carbon metal: Buyers and export markets increasingly prefer metal with low carbon emissions.
- Construction and electrical: Extrusions, conductors, and appliances need more aluminium.
- Domestic scrap growth: Vehicle scrappage and rising consumption are increasing scrap generation at home.
India-Specific Market Opportunity
| Segment | India Market Context | Manufacturing Role |
|---|---|---|
| Automotive Castings | Large and growing output | Die-casting alloys |
| Two-Wheelers | World's largest market | Alloy ingots and liquid metal |
| Building & Construction | Rising extrusion demand | Extrusion billets |
| Steel Industry | Growing steel output | Deox aluminium |
| Exports | Low-carbon metal demand | Certified recycled alloys |
The strongest opportunity for new entrants lies in supplying certified alloys and liquid metal to automotive foundries in major auto hubs, in billets and slabs from carefully sorted scrap, and in low-carbon recycled metal for export customers. Producers that secure scrap supply, control chemistry tightly, and invest in clean, efficient furnaces will be best placed to grow.
Recycled Aluminium Manufacturing Process Flow
Understanding the process helps you plan equipment, layout, and where cost and quality are decided. Production runs from scrap receipt and inspection through sorting, shredding, decoating, melting, alloying, fluxing and degassing, and filtration to casting and testing and dispatch. Sorting and melting decide metal recovery, while scrap cost, energy, and melt losses are the largest controllable costs.
The Recycled Aluminium Manufacturing Process Flow
The sequence below reflects an integrated alloy recycling plant. Billet and slab plants use cleaner scrap and add direct-chill casting and homogenising.
| Unit Operation | Key Activity |
|---|---|
| Scrap Receipt & Inspection | Weighed, graded, sampled |
| Sorting | Magnets, eddy current, sensors |
| Shredding | Scrap reduced in size |
| Decoating & Drying | Paint, oil, moisture removed |
| Melting | Rotary or reverb furnace |
| Alloying | Chemistry adjusted |
| Fluxing & Degassing | Gas and oxides removed |
| Filtration | Inclusions filtered out |
| Casting | Ingots or liquid metal |
| Testing & Dispatch | Chemistry checked, shipped |
Two factors decide profitability across this flow. The first is metal recovery, because every percentage point of aluminium lost to dross and oxidation is lost margin, so good sorting, decoating, the right furnace for each scrap type, and dross recovery maximise the metal obtained from every tonne of scrap. The second is chemistry and energy control, since accurate alloying with the least expensive additions and efficient, well-insulated furnaces with heat recovery keep both material and fuel costs down.
Raw Materials Required for Recycled Aluminium Manufacturing
The main inputs are imported and domestic aluminium scrap in many grades, alloying elements such as silicon, copper, and magnesium, fluxes and degassing gases, and some primary aluminium for chemistry correction. Scrap is by far the largest cost, its price moves with the LME and global scrap markets, and most of it is imported, so scrap buying is central to project planning.
| Raw Material | Role in Product | India Sourcing | % of OpEx |
|---|---|---|---|
| Imported Aluminium Scrap | Main metal source | Middle East, US, Europe, Asia | 55–62% |
| Domestic Scrap | Local metal source | Dealers, industry, vehicles | 15–20% |
| Alloying Elements | Silicon, copper, magnesium | Domestic and imported | 4–6% |
| Fluxes & Degassing Gases | Cleaning the melt | Domestic suppliers | 1–2% |
| Primary Aluminium | Chemistry correction | Domestic smelters | 1–3% |
India relies on imports for most of its aluminium scrap, so supply can be disrupted by export restrictions, freight costs, and import duty. Buying from several countries, building domestic collection networks with dealers and vehicle recyclers, signing tolling agreements with industrial customers for their process scrap, and using sensor-based sorting to upgrade mixed scrap help manage cost and supply risk.
Location, Land & Infrastructure
Site selection for an aluminium recycling plant is driven by proximity to ports for imported scrap, closeness to automotive and engineering foundries for alloy and liquid metal sales, and the availability of fuel and power. Other factors include industrial estates that permit secondary metal processing, environmental clearance capacity, skilled workers, and state incentives.
Choosing the Best Location for Recycled Aluminium Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Gujarat | Mundra and Kandla ports | Imported scrap access |
| Haryana | Faridabad and Gurugram | Auto foundry customers |
| Tamil Nadu | Chennai auto corridor | Customers and ports |
| Maharashtra | Pune and Mumbai region | Auto hub and JNPT port |
| Rajasthan | Bhiwadi industrial area | Near Delhi NCR market |
| Uttarakhand | Pantnagar and Haridwar | Two-wheeler and auto plants |
Gujarat offers the best access to imported scrap through its ports, while Haryana, Tamil Nadu, and Maharashtra place plants close to India's largest automotive and engineering foundry clusters. Rajasthan's Bhiwadi and Uttarakhand's industrial areas serve northern vehicle makers. The final choice should weigh scrap logistics, customer proximity, fuel and power cost, environmental approvals, and incentives.
Quality, Safety and Environmental Systems
Recycled aluminium must meet customer and standard specifications for alloy chemistry, gas content, inclusions, and mechanical properties, with automotive customers requiring tight control and full traceability. A credible plant needs an optical emission spectrometer for every melt, gas and inclusion testing, lot traceability from scrap to ingot, and ISO 9001, 14001, and 45001 certification, with IATF 16949 for automotive supply. Safety is critical because molten metal can explode on contact with moisture, so scrap must be dry, and furnaces and ladles must be handled with care, while environmental systems must control dust, fumes, and dioxins from coated scrap, and manage dross and salt cake properly. An experienced Recycled Aluminium Manufacturing Consultant in India can help plan furnace selection, pollution control, and layout so the plant meets customer and regulatory requirements from the start.
Infrastructure Requirements (50,000 TPA Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 8 – 12 acres | Industrial estate permitting recycling |
| Scrap Yard | Covered storage by grade | Keeps scrap dry |
| Melting Shed | Furnaces and casting | High roof, good ventilation |
| Fuel & Power | Gas or oil, HT connection | Furnace fuel supply |
| Pollution Control | Bag filters, afterburners | Essential for consent |
| Dross Handling | Cooling and processing area | Recover metal from dross |
| Laboratory | Spectrometer and testing | Every melt tested |
Dry, covered scrap storage and effective pollution control are the most important infrastructure requirements, since wet scrap is dangerous to melt and emissions control decides whether the plant can operate. A reliable fuel supply, a well-ventilated melting shed, dross handling, and good road access to ports and customers complete the core needs.
Recycled Aluminium Manufacturing Machinery and Equipment
The equipment set covers scrap preparation, melting, refining, casting, dross processing, testing, and pollution control. Furnaces, shredders and sorters, casting machines, and pollution control systems account for most of the machinery budget. The main items are summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Scrap Shredder | Reduce scrap size | Heavy-duty rotor |
| Magnetic & Eddy Current Separators | Remove iron, separate metals | Continuous |
| Sensor-based Sorter | Sort by alloy | XRF or LIBS |
| Decoating Kiln | Remove coatings and oil | With afterburner |
| Rotary Tilting Furnace | Melt mixed and dirty scrap | Salt or salt-free |
| Reverberatory Furnace | Melt and hold metal | Large batches |
| Degassing Unit | Remove hydrogen | Rotary degasser |
| Ingot Casting Machine | Cast alloy ingots | Automatic stacking |
| Liquid Metal Ladles | Deliver hot metal | Insulated transport |
| Dross Processing Unit | Recover metal from dross | Press or rotary |
| Spectrometer & APC System | Test and control emissions | OES, bag filters |
Machinery should follow the scrap mix and product plan. A small unit needs mainly a rotary furnace, a holding furnace, a casting line, a spectrometer, and a bag filter, while an integrated plant adds shredding, sensor-based sorting, decoating, degassing, liquid metal logistics, and dross recovery. Billet and slab plants add direct-chill casting and homogenising furnaces, and modern burners, heat recovery, and salt-free melting improve both costs and environmental performance.
Recycled Aluminium Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for an integrated alloy recycling plant of about 50,000 tonnes a year in India. The final Recycled Aluminium Investment Cost for your project will depend on capacity, scrap preparation, furnace types, products, pollution control, land cost, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 50–60% | Shredding, furnaces, casting |
| Civil Works & Sheds | 12–16% | Scrap yard, melting shed |
| Pollution Control | 8–12% | Bag filters, afterburners, stacks |
| Land & Site Development | 5–8% | Industrial land |
| Pre-operative & Licenses | 2–3% | Approvals, trials, audits |
| Working Capital | 15–20% | Scrap stocks and receivables |
Machinery and pollution control dominate the fixed investment, while working capital is large because scrap is costly, imported shipments take weeks to arrive, and automotive customers pay on credit. Because scrap and alloy prices both follow the LME but with different lags and premiums, a detailed Recycled Aluminium Business Plan should model scrap purchases by grade and origin, metal recovery, alloy prices and premiums, energy costs, import duty, inventory, hedging, and payment terms together, so that funding supports steady operation through metal price cycles.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials | 80–85% | Aluminium scrap dominates |
| Utilities (fuel, power) | 10–15% | Furnace fuel and electricity |
| Labour | 2–3% | Furnace and casting crews |
| Maintenance & Refractories | 1–2% | Furnace relining |
| Logistics | 1–2% | Scrap and ingot freight |
| Overheads | 0.5–1% | Administration and testing |
With scrap making up most of the cost, margins depend on buying the right grades at the right price, metal recovery, alloy premiums, energy efficiency, and price risk management. A good operating model tracks scrap cost against the LME, metal recovery by scrap grade, fuel use per tonne, dross generation and recovery, alloying cost per tonne, and realised premiums by customer, and tests how margins respond when scrap prices rise faster than alloy prices.
Financial Analysis and Profitability
Based on analysis of a 50,000 TPA integrated recycling plant, the financial profile is sound, supported by strong automotive demand, energy savings over primary metal, and growing interest in low-carbon aluminium, but returns depend on scrap buying and metal recovery. The profitability of Recycled Aluminium manufacturing business in India improves markedly with reliable scrap sourcing, high metal recovery, liquid metal supply to nearby foundries, long-term contracts with automotive customers, and a richer mix of billets, slabs, and certified low-carbon alloys.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 15–25% | Depends on scrap spread |
| Net Profit Margin | 5–10% | After depreciation and taxes |
| Payback Period | 4–6 Years | Working capital heavy |
| IRR (Internal Rate of Return) | 14–20% | Higher with value-added products |
| Capacity Utilization (stable ops) | 70–85% | Scrap availability |
| Break-even Capacity Utilization | 50–60% | Thin unit margins |
Scrap buying and product mix decide where a plant lands within these ranges. Plants with secure scrap supply, high recovery, and value-added products such as liquid metal, billets, and certified alloys earn healthier margins, while those selling standard ingots compete on thin spreads with many recyclers. Established Indian recyclers often report net margins at the lower end of the range, so scale and efficiency matter.
Returns can be strengthened by building domestic scrap networks, investing in sorting and decoating to use cheaper scrap, supplying liquid metal to nearby foundries, recovering metal from dross, adding billets and slabs, and selling certified low-carbon metal to export and premium customers. Tolling agreements, under which customers supply their own scrap and pay a conversion fee, can also keep furnaces busy with little price risk.
Key Risks and Mitigation
The main risks are scrap supply disruptions and export bans in supplier countries, scrap and LME price swings, import duty, low metal recovery from poor scrap, environmental compliance, molten metal safety, and customer concentration in the automotive sector. Supply risk is reduced by diversifying origins and domestic sourcing; price risk by hedging and LME-linked pricing; recovery risk by sorting and decoating; compliance risk by strong pollution control; safety risk by dry scrap and training; and customer risk by broadening segments. Promoters often work with a Recycled Aluminium Business Plan Consultant in India to test these scenarios before committing capital. Lenders pay close attention to how scrap stocks are financed and protected against metal price falls, so a clear buying and hedging policy agreed before start-up strengthens the case for funding.
Licenses and Approvals for Recycled Aluminium Manufacturing in India
Approvals for an aluminium recycling plant are significant because secondary metal processing is a polluting activity and imported scrap is regulated. Promoters setting up a Recycled Aluminium Manufacturing Plant in India generally need the following:
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, with strict emission norms.
- Hazardous Waste Authorisation: Authorisation for handling dross, salt cake, and scrap imports under the hazardous and other wastes rules.
- Scrap Import Compliance: Import Export Code, pre-shipment inspection certificates, and customs clearance for metal scrap.
- Product Standards: BIS and customer specifications for alloys, and BIS certification where products are under quality control orders.
- Factory License & Safety: Factory license with provisions for furnaces and molten metal, and fire NOC.
- Quality Certifications: ISO 9001, 14001, and 45001, and IATF 16949 for automotive customers.
- Business & Trade Registrations: Business registration, GST, and Udyam where eligible.
Pollution control consent and hazardous waste authorisation are usually on the critical path, since the plant cannot melt scrap without them, while customer approvals decide how quickly sales grow. Planning approvals, pollution control design, scrap sourcing, and early customer sampling in parallel shortens the time from investment decision to commercial production.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, products, state pollution control categories, customer specifications, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Recycled Aluminium Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- Duty debate: In July 2026, the Material Recycling Association of India urged the government to remove the 2.5% import duty on aluminium scrap, noting that secondary output has grown to nearly 2.2 million tonnes and imports meet 80 to 85% of scrap needs.
- Supply disruption: From June to October 2026, several Gulf countries restricted aluminium scrap exports, disrupting about 4 lakh tonnes, or nearly 20%, of India's imports and pushing importers toward new sources.
- Sector listing: In June 2026, CMR Green Technologies, with about 6.15 lakh tonnes of capacity across 13 plants in eight states, listed on the stock exchanges.
- Recycling push: Hindalco plans to quadruple its aluminium recycling capacity by FY30 as part of a INR 43,000 crore expansion programme.
The common thread is fast growth in secondary aluminium, rising investment by large players, and continuing challenges in scrap supply and import costs. New entrants who secure diverse scrap sources, recover metal efficiently, and build strong automotive relationships will be best placed to grow.
How a Recycled Aluminium Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from market demand and product selection to scrap sourcing, process design, machinery, pollution control, approvals, and economics. It helps investors decide the right products, capacity, and level of scrap preparation, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Recycled Aluminium Financial Model covering scrap purchases by grade and origin, metal recovery, revenue by product and customer, alloying, fuel, power, labour, logistics, import duty, working capital, hedging, debt servicing, cash flows, break-even, return on investment, and payback under different price and supply scenarios. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a Recycled Aluminium Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For an aluminium recycling project, a strong DPR also clarifies the scrap sourcing strategy, the furnace and pollution control design, the customer and approval plan, and the approach to price risk, which together are the factors most likely to decide success. By testing margins against scrap price swings, supply disruptions, and recovery rates, the report turns a growing circular economy opportunity into a plan that lenders and partners can trust.
Frequently Asked Questions
What are the first steps to set up a recycled aluminium manufacturing plant in India?
Start by choosing your products and target customers, and by studying scrap availability, prices, and competition. Then commission a feasibility study and DPR, secure land in an estate that permits secondary metal processing, design pollution control, obtain consents and hazardous waste authorisation, install furnaces, casting, and testing equipment, arrange scrap imports and domestic sourcing, and begin sampling with foundries.
How much does it cost to set up a recycled aluminium manufacturing plant in India?
Investment ranges from about INR 8–20 crore for a small unit of 3,000 to 6,000 tonnes a year to INR 80–200 crore for an integrated plant of 30,000 to 60,000 tonnes a year, and INR 500–1,000 crore for a large plant of 1 to 2 lakh tonnes a year.
What are the main steps in recycled aluminium manufacturing?
The flow runs from scrap receipt and inspection through sorting, shredding, decoating and drying, melting, alloying, fluxing and degassing, filtration, casting, and testing and dispatch.
Which machinery does a recycled aluminium manufacturing plant need?
Key equipment includes a scrap shredder, magnetic and eddy current separators, a sensor-based sorter, a decoating kiln, rotary and reverberatory furnaces, a degassing unit, an ingot casting machine, liquid metal ladles, a dross processing unit, and a spectrometer and air pollution control system.
What raw materials are used to make recycled aluminium?
The main raw materials are imported and domestic aluminium scrap, alloying elements such as silicon, copper, and magnesium, fluxes and degassing gases, and small amounts of primary aluminium.
How profitable is recycled aluminium manufacturing in India?
A well-run plant typically earns a 15 to 25% gross margin and a 5 to 10% net margin, with payback in about 4 to 6 years. Profitability depends on scrap prices, metal recovery, product mix, and energy costs.
Which approvals does a recycled aluminium manufacturing plant need in India?
Typical approvals include pollution control consents, hazardous waste authorisation, scrap import compliance, product standards, a factory license and fire NOC, quality certifications, and GST and Udyam registrations.
How do I get a feasibility study or DPR for a recycled aluminium manufacturing project?
A detailed feasibility study and DPR covers scrap sourcing, market demand, plant design, pollution control, approvals, and full financials. Investors usually engage a Recycled Aluminium Manufacturing Feasibility Study Consultant with experience in metals and recycling projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

The Australia Power Industry is the physical foundation of one of the developed world's most coal-reliant electricity systems, which is precisely why its transition now ranks among the largest infrastructure investment programmes in the country's history.
Every solar panel is connected by cables built to survive 25 years or more of sun, heat, rain, and high DC voltage. India added a record 44.6 GW of solar capacity in 2025-26, taking cumulative solar capacity past 150 GW, and rooftop programmes such as PM Surya Ghar are adding millions of smaller systems.
Biomass briquettes, often called white coal, are dense blocks of compressed agricultural and forestry residues that burn cleanly in industrial boilers, furnaces, and power plants.
Lead-acid batteries start every car, truck, and two-wheeler, back up telecom towers, data centres, and homes through inverters and UPS systems, and store energy for solar installations. Almost all of the lead, plastic, and acid in a used battery can be recovered, and India already meets more than 80% of its lead demand from recycling.
Fuel cells turn hydrogen into electricity with water as the only exhaust, which makes them one of the most important technologies in India's clean energy transition. They power hydrogen buses, trucks, and trains, provide backup power for telecom towers and data centres, and supply off-grid and distributed electricity where diesel generators are used today.
India's cities generate well over a lakh tonnes of municipal solid waste every day, and much of it still ends up in overflowing dumpsites that release methane, catch fire, and pollute land and water.
Every solar power system needs an inverter to convert the direct current produced by solar panels into alternating current that homes, businesses, and the grid can use.
Sodium-ion batteries are emerging as a practical complement to lithium-ion technology. They work on the same principle, shuttling ions between a cathode and an anode, but use sodium, which is abundant, inexpensive, and available within India, in place of lithium.
Few industries in India have scaled as quickly as solar manufacturing. Backed by ambitious renewable energy targets, a rooftop programme for households, import duties on foreign modules, and the Approved List of Models and Manufacturers (ALMM), domestic module capacity has multiplied in just a few years.
Setting up an Electrical Panel Manufacturing Plant in India is a fabrication-and-assembly venture powered by heavy grid modernisation, a fast-growing renewable-energy build-out, rising industrial and commercial construction, and the spread of automation across factories and buildings.
Saudi Arabia has turned its power transition into one of the world's largest procurement programmes, and international developers, lenders, and equipment makers are following the tenders.
Setting up a Battery Manufacturing Plant in India is a high-demand, energy-driven venture, powered by the country's booming automotive sector, huge power-backup market, and the fast-growing shift to electric vehicles and renewable storage.
Setting up a Liquefied Natural Gas (LNG) Manufacturing Plant in India is a capital-intensive, strategically important venture, powered by the country's push toward a gas-based economy, the shift to cleaner fuels in transport and industry, and rising demand for LNG as a truck, bus, and industrial fuel.
The India carbon credit market is moving from a voluntary, project-by-project trade into a regulated national system with binding targets, a central registry, and exchange-based price discovery. According to IMARC Group, the market was valued at USD 33.69 Billion in 2025, grew to USD 44.42 Billion in 2026, and is projected to reach USD 405.47 Billion by 2034, expanding at a CAGR of 31.84% (2026–2034).
Setting up a Syngas Production Plant in India is a capital-intensive but strategically valuable venture, driven by the country's push for cleaner industrial fuels, coal and biomass utilization, and chemical self-reliance. Syngas, or synthesis gas, is a mixture of hydrogen and carbon monoxide produced by gasifying carbon-rich feedstocks, and it serves as a versatile building block for power, chemicals, hydrogen, and synthetic fuels. With abundant biomass, coal, and waste feedstock and growing policy support for gasification, India offers a favourable environment for new plants.
Setting up a Battery Energy Storage System Manufacturing Plant in India is a capital-efficient, high-growth venture, driven by the country's renewable energy expansion, grid modernization, and supportive storage policies. As solar and wind capacity scales up and the grid needs to balance variable generation, battery energy storage systems have become essential infrastructure.
Setting up a Lithium-ion Battery Recycling Plant in India is a capital-intensive but high-potential venture. India's rapid rise as a major electric-vehicle market, its large consumer-electronics base, and its fast-growing energy-storage sector are together creating one of the deepest and fastest-expanding pools of end-of-life lithium-ion batteries in the world.
Solar glass is a type of specialty glass that has high transmittance and is designed exclusively for use in solar energy systems. Unlike regular flat glass, solar glass is designed to have maximum light transmission with minimal losses due to reflection and absorption.
A solar inverter is a vital component in solar photovoltaic (PV) systems, responsible for transforming the direct current (DC) electricity produced by solar panels into alternating current (AC) electricity. This AC power is then suitable for use by the electrical grid, various appliances, and industrial equipment.
Australia has firmly established itself as a dominant force in the global liquefied natural gas (LNG) market, maintaining its position as one of the world's leading exporters. The country's strategic geographical location in the Asia-Pacific region, combined with substantial natural gas reserves, has enabled it to become a critical energy supplier to rapidly growing Asian economies, particularly China, Japan, and South Korea.
Japan's lead acid battery market stands as a cornerstone of the nation's energy storage infrastructure, demonstrating remarkable resilience and adaptability in an era dominated by rapid technological evolution. Despite the global shift toward lithium-ion technologies, the Japanese lead acid battery sector continues to thrive, driven by its unmatched cost-effectiveness, proven reliability, and exceptional recyclability.
Green hydrogen is the cleanest form of hydrogen available, as it is produced through water electrolysis using the electricity generated from renewable energy sources such as solar, wind, or hydropower. Carbon dioxide emissions are zero since no fossil fuels are used. Essentially, an electrolyzer is used in the electrolysis process to split water molecules into hydrogen and oxygen. The resulting hydrogen is refined by purification, compression, or liquefaction and then fed into various applications. Green hydrogen is considered a cornerstone of the global energy transition because it can store renewable energy, decarbonize hard-to-abate sectors, and serve as a sustainable alternative to fossil-fuel-based hydrogen.
Japan’s thermal power plant industry remains a crucial pillar of the nation’s energy infrastructure, providing a stable and reliable source of electricity for both industrial and residential consumption. Thermal power generation, which primarily involves the combustion of fossil fuels such as coal, natural gas, and oil, continues to play a key role despite increasing investments in renewable energy.
An electrical panel, also called a distribution board or switchboard, is an important installation in electrical infrastructure that acts as the main center for the distribution, control, and protection of electrical power within residential, commercial, and industrial systems. It acts as the point at which electrical energy is received from the utility or a source of power generation and is distributed to various circuits and equipment in an organized manner.
The global oil and gas EPC market is currently experiencing a remarkable transformation as it positions itself at the intersection of traditional energy demands and technological innovation. As of 2024, the market is demonstrating robust growth, reaching USD 52.9 Billion in 2024, depending on regional scope and market segmentation approaches. This substantial market base is supporting a major number of capital projects worldwide, including offshore platform projects and onshore installations that are collectively shaping the energy landscape.
Bamboo pellets are a biomass fuel type created through the compression of bamboo residues like shavings, sawdust, and chips into thick cylindrical pellets. They are an environmentally friendly substitute for conventional fossil fuels like natural gas and coal. Due to the fast growth rate and high biomass yield of bamboo, it has become one of the most renewable raw materials for the production of bioenergy.
Biomass briquettes are dense, solid fuel blocks made of compressed organic waste materials like sawdust, agricultural wastes, wood shavings, coconut shells, rice husk, or herbaceous biomass. The briquetting process usually involves drying the biomass to lower the moisture content (usually down to 10-15%), grinding or milling for a fine particle size uniformity, and then compressing under high pressure with or without a binding agent.
Biogas is a renewable energy form generated by the anaerobic fermentation of organic matter including agricultural residues, animal waste, municipal solid waste, sewage sludge, and food waste. Microorganisms in the absence of oxygen break down organic substances in the process and produce a gaseous mixture of mainly methane (CH4) and carbon dioxide (CO2), with traces of hydrogen sulfide (H2S) and water vapor.
A battery is an electrochemical energy storage system that transforms chemical energy into electrical energy by way of redox reactions between its electrodes and electrolyte. It consists of a single or multiple electrochemical cells, each having a positive electrode (cathode), a negative electrode (anode), and an electrolyte for ion transfer. Batteries are categorically divided into primary (non-rechargeable) and secondary (rechargeable) types.
The global energy landscape is undergoing a seismic transformation, with green hydrogen emerging as one of the most promising solutions to achieve deep decarbonization across sectors. Far from a niche technology, green hydrogen is emerging as a critical pillar of the future energy system, offering a pathway to a sustainable and resilient economy.
Transmission line towers are essential support components of transmission lines installed on overhead to distribute high-voltage electricity over long distances. Towers are made of galvanized steel, primarily, and are designed to tolerate mechanical stress, environmental loads, and electrical safety. Some of the important characteristics of transmission line towers are high structural strength, corrosion resistance, adaptability for modular design, and high service life. They are normally produced in lattice form (tubular or free-standing towers) or tubular form, with types including suspension towers, tension towers, angle towers, and terminal towers based on use.
The energy storage revolution is here, and it's powered by graphene. While the world struggles with the limitations of conventional lithium-ion batteries, a new technology is emerging that promises to shatter every performance barrier we've accepted as unchangeable.
Australia is undergoing a significant energy transformation, underscoring the growing role of renewable energy sources. These sources are key to combating climate change by reducing greenhouse gas emissions, the primary cause of global warming and air pollution. Beyond environmental benefits, renewable energy strengthens energy security by diversifying power sources and reducing dependence on volatile fossil fuel imports, contributing to greater energy independence.
Learn how to plan capital investment, manage raw material costs, post manufacturing cost and optimize operations for setting up solar panel plant.
Battery Energy Storage System (BESS) represents a power grid technology that stores electricity to enhance electric power grid reliability while increasing operational efficiency. BESS permits battery recharging during periods of low demand or extra grid supply capacity. BESS provides three principal operational functionalities which include power grid stabilization during supply disruptions, control of energy supply variations, and integration of intermittent renewable generation from wind and solar resources.
China's economic presence is expanding globally, and Latin America and the Caribbean (LAC) have become a focal point for its investments, especially within the energy sector. The region, rich in natural resources and experiencing rising energy demands, offers strategic opportunities for Chinese energy giants looking to invest and expand. LAC is currently leading a transformative movement towards sustainable energy. From 2015 to 2022, the region increased its renewable energy capacity by an impressive 51%, now generating 64% of its electricity from renewables such as hydropower, wind, and solar. This shift addresses the global demand for cleaner energy while supporting local economic growth and enhancing energy security.
Hydrogen is a clean, renewable, and widely available energy source that can be produced through various methods. Production techniques such as coal gasification, steam methane reforming, electrolysis, and thermochemical processes highlight its versatility. Hydrogen is essential in several critical sectors, including methanol and ammonia production, petroleum refining, transportation, power generation, as well as in electronics, metal industries, and as a rocket propellant. The increasing concern over carbon emissions and greenhouse gases has led to a shift towards cleaner fuel options. Hydrogen is recognized for its cleanliness and versatility as an energy carrier. Additionally, supportive government initiatives and favorable policies are driving the growth of hydrogen production globally.
Hydrogen is a clean, renewable, and abundant energy source derived from various methods. Its applications span across transportation, heating, and power generation. Diverse production methods, including coal gasification, steam methane reforming, electrolysis, and thermochemical processes, contribute to its versatility. Hydrogen plays a pivotal role in crucial sectors like methanol and ammonia production, petroleum refining, transportation, power generation, as well as in electronics, metal industries, and as a rocket propellant.
A floating solar farm is a renewable energy installation in which solar panels are mounted on floating structures in water bodies such as lakes, reservoirs, ponds, or even the sea. This technology, also known as a floating photovoltaic (PV) system, or “floatovoltaics,” enables solar power generation in areas with limited available land or where land use is restricted for other purposes. Floating solar farms offer various benefits, including improved solar panel efficiency through cooling, land conservation, reduction of evaporation and algae growth, and integration with hydropower facilities to generate both solar and hydroelectric power in the same location.
Nuclear power utilizes nuclear reactions to generate heat, which is then converted into electricity. This energy is released from the nucleus—the core of atoms composed of protons and neutrons. Nuclear power can be derived from nuclear fission, nuclear decay, and nuclear fusion reactions. Across the globe, nuclear power plants predominantly use the fission of uranium and plutonium to produce electricity. The heat generated from fission is used to create steam, which drives turbines connected to generators. Nuclear power offers several advantages over fossil fuels, such as minimal greenhouse gas emissions and a higher energy density, meaning a small amount of nuclear fuel produces a large amount of energy.