P.C.C. Electric Poles Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
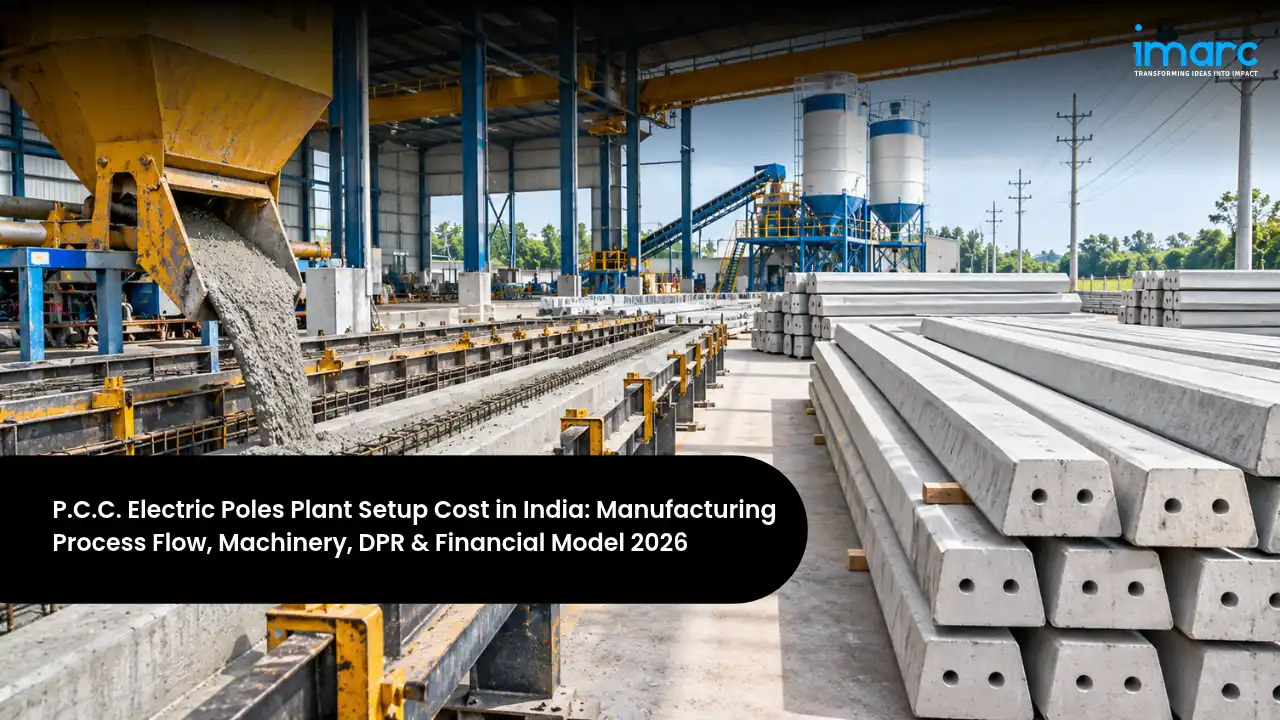
A P.C.C. Electric Poles Manufacturing Plant Setup in India supplies the backbone of the country's power distribution network. Prestressed cement concrete (P.C.C.) poles are made by casting high-strength concrete around high-tensile steel wires that are stretched before casting and released once the concrete has hardened, which puts the concrete into compression and gives a slender, strong, and durable pole. They are the standard support for low-tension and 11 kV lines across India, and are also used for 33 kV lines, rural electrification, agricultural feeders, street lighting, and telecom cables, because they cost less than steel poles, do not rust, need little maintenance, and are made close to where they are installed.
The overall P.C.C. Electric Poles Manufacturing Plant Cost depends mainly on capacity, the number of long-line casting beds and moulds, the level of mechanisation in batching, tensioning, and handling, whether steam curing is used, the size of the casting and stacking yard, and working capital for raw materials and delayed tender payments. A mechanised plant producing 1,00,000 to 1,50,000 poles a year typically needs INR 15 crore to INR 30 crore, while a semi-mechanised unit of 30,000 to 60,000 poles a year can start at around INR 4 crore to INR 10 crore. Raw materials account for 55 to 65% of operating cost, and IMARC Group benchmarks point to gross margins of 20 to 30% and net margins of 7 to 14%.
This guide is written for precast concrete producers, electrical contractors and EPC companies, cement and steel traders, and investors exploring how to start a P.C.C. Electric Poles Manufacturing Plant in India. It explains pole types and buyers, demand drivers, the production process, machinery and raw materials, site and yard planning, a detailed cost and returns breakdown, the approvals and vendor registrations involved, and how a DPR pulls these elements into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Global Utility Poles Market | USD 51.6 Billion (2025) |
| Global Market Outlook | USD 65.6 Billion by 2034, 2.63% CAGR |
| Asia-Pacific Share of P.C.C. Pole Market | About 47% |
| RDSS Loss Reduction Works Sanctioned | INR 1.53 Lakh Crore (2026) |
| Indicative Total Investment | INR 15–30 Crore (1,00,000–1,50,000 poles a year) |
| Typical Payback Period | 4–6 Years |
The snapshot shows a large global utility pole market in which Asia-Pacific is the biggest region for prestressed concrete poles according to IMARC Group. In India, demand is driven mainly by public spending on distribution networks, especially the Revamped Distribution Sector Scheme (RDSS), feeder separation and agricultural feeder solarisation, rural and urban network expansion, and replacement of damaged poles. Because poles are heavy and costly to transport, most plants serve DISCOMs and contractors within a few hundred kilometres.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | 7.5 m, 8 m, 9 m and 11 m P.C.C. poles for LT, 11 kV and 33 kV lines; street lighting poles |
| Total Project Investment | INR 15 – 30 Crore (mechanised); INR 4 – 10 Crore (semi-mechanised) |
| Payback Period | 4 – 6 Years |
| Net Profit Margin | 7 – 14% (IMARC benchmark) |
| IRR | 16 – 22% |
| Best Locations | Uttar Pradesh, Bihar, Madhya Pradesh, Rajasthan, West Bengal, Andhra Pradesh |
| Mandatory Approvals | DISCOM Vendor Registration & Type Test, BIS License (where required), SPCB Consents, Factory License, GST, Udyam |
| Key Requirement | IS 1678 compliant quality, DISCOM approvals, and working capital for tender payment cycles |
These figures offer a practical frame for early evaluation. Returns depend on winning DISCOM and contractor orders, maintaining consistent quality that passes inspection and transverse load tests, controlling cement and steel wire costs, keeping moulds and casting beds fully utilised, and managing receivables from government buyers. A capacity- and market-specific P.C.C. Electric Poles Feasibility Report refines these numbers before capital is committed.
Table of Contents
- What is P.C.C. Electric Poles Manufacturing?
- Why is P.C.C. Electric Poles Manufacturing Growing in India?
- P.C.C. Electric Poles Manufacturing Process Flow
- Raw Materials Required for P.C.C. Electric Poles Manufacturing
- Location, Land & Infrastructure
- P.C.C. Electric Poles Manufacturing Machinery and Equipment
- P.C.C. Electric Poles Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for P.C.C. Electric Poles Manufacturing in India
- Recent Developments in the India P.C.C. Electric Poles Manufacturing Industry
- How P.C.C. Electric Poles Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is P.C.C. Electric Poles Manufacturing?
P.C.C. poles are usually made by the long-line pretensioning method. High-tensile steel wires are laid along a casting bed fitted with steel moulds, anchored at both ends, and stretched to a specified force with hydraulic jacks. Concrete of high strength and low water content is placed in the moulds and compacted by vibration, then cured with water or steam. Once the concrete reaches the required transfer strength, the wires are released and cut, transferring the prestress into the concrete, and the poles are lifted out, cured further, inspected, and tested. A P.C.C. Electric Poles Manufacturing Plant therefore combines concrete batching, wire tensioning, casting and compaction, curing, handling, and quality testing.
Poles are bought mainly by state distribution companies, electricity departments, and the EPC contractors who build distribution lines under government schemes, as well as by municipal bodies, railways, telecom operators, and industrial users. Orders are usually won through tenders on state portals and the Government e-Marketplace, and buyers expect conformity with IS 1678, prior vendor approval, successful type and acceptance tests, timely delivery, and competitive pricing.
- LT Line Poles: 7.5 m and 8 m poles for low-tension distribution in villages and towns.
- 11 kV Line Poles: 8 m and 9 m poles for primary distribution and feeder lines.
- 33 kV and Heavy-Duty Poles: 9 m and 11 m poles with higher working loads.
- Street Lighting and Telecom Poles: Poles for street lights, cable networks, and fencing.
Main Pole Types in P.C.C. Pole Production
The product mix shapes moulds, raw material use, and margins:
| Pole Type | Description | Key Feature | Primary Buyer |
|---|---|---|---|
| 7.5 m / 8 m P.C.C. Poles | Standard LT distribution poles | Highest volume | DISCOMs, rural electrification |
| 9 m P.C.C. Poles | 11 kV distribution poles | Feeder and network expansion | DISCOMs, EPC contractors |
| 11 m P.C.C. Poles | 33 kV and long-span poles | Higher working load | DISCOMs, industrial users |
| Street Light Poles | Lighting supports | Urban and highway projects | Municipalities, contractors |
| Telecom & Fencing Poles | Lighter poles | Diversified demand | Telecom, railways, private users |
Most plants focus on the high-volume 8 m and 9 m poles that dominate DISCOM tenders, while adding 11 m and special poles to widen their customer base. Because the same casting beds can produce several pole lengths with different moulds, flexible mould planning lets producers follow changes in tender demand.
Why is P.C.C. Electric Poles Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
Demand for P.C.C. poles in India is driven by public investment in distribution networks and rising electricity use. IMARC Group values the global utility poles market at USD 51.6 billion in 2025, with Asia-Pacific accounting for about 47% of the prestressed concrete pole market:
- Distribution sector reform: RDSS loss reduction works include new and reconductored lines, feeder bifurcation, and aerial bunched cable, all of which need poles.
- Agricultural feeders: Feeder separation and solarisation under PM-KUSUM require new and upgraded agricultural lines.
- Network expansion: New housing, industrial areas, and urban growth extend LT and 11 kV networks.
- Replacement demand: Old, damaged, and storm-hit poles need regular replacement.
- Cost and durability: P.C.C. poles are cheaper than steel, rust-free, and need little maintenance.
India-Specific Market Opportunity
| Segment | India Market Context | Product Role |
|---|---|---|
| DISCOM Distribution Works | RDSS and state schemes | 8 m and 9 m poles |
| Agricultural Feeders | Feeder separation and solarisation | LT and 11 kV poles |
| Urban Infrastructure | Street lighting and city networks | Lighting and distribution poles |
| Industrial Users | Plant and estate networks | 11 m and heavy-duty poles |
The strongest position for a P.C.C. Electric Poles Manufacturing Plant in India is a mechanised, quality-certified plant located close to DISCOM demand centres, with approved vendor status in one or more states and relationships with the EPC contractors executing distribution projects. Because demand depends on public spending cycles, plants that serve several states and customer types are more resilient.
P.C.C. Electric Poles Manufacturing Process Flow
Understanding the P.C.C. Electric Poles Manufacturing Process helps promoters plan casting beds, moulds, equipment, and quality control. Pole strength and durability depend on correct wire tensioning, concrete strength and water-cement ratio, proper compaction, adequate curing before detensioning, accurate dimensions and cover to steel, and careful handling. The flow below reflects a typical mechanised long-line plant.
Step-by-Step Pole Production Flow
Moulds are cleaned and oiled, and high-tensile wires are laid along the casting bed with spacers and anchored at both ends. The wires are tensioned with hydraulic jacks, concrete is batched, mixed, placed, and vibrated, and the poles are cured until the concrete reaches transfer strength. The wires are then released and cut, the poles are demoulded, stacked, and cured further, and samples are tested before dispatch.
| Unit Operation | Key Activity |
|---|---|
| Material Testing | Check cement, wire, aggregates, water |
| Mould Preparation | Clean, oil, and align steel moulds |
| Wire Laying | Place high-tensile wires and spacers |
| Tensioning | Stretch wires with hydraulic jacks |
| Batching & Mixing | Produce high-strength concrete |
| Casting & Vibration | Place and compact concrete |
| Curing | Water or steam curing to transfer strength |
| Detensioning & Demoulding | Release wires, cut, lift poles |
| Stacking & Final Curing | Stack and cure in yard |
| Testing, Marking & Dispatch | Transverse load test, inspection, loading |
Two factors decide profitability. The first is bed and mould utilisation each casting bed produces a fixed number of poles per cycle, so faster curing, quick mould turnaround, and continuous order flow directly raise output and spread fixed costs. The second is material cost and quality control: cement and high-tensile wire make up most of the cost, so accurate mix design, correct wire quantity, low breakage and rejection rates, and consistent test results protect margins and vendor approvals.
Raw Materials Required for P.C.C. Electric Poles Manufacturing
The main inputs are cement, high-tensile steel wire, coarse and fine aggregates, water, and small items such as earthing wire and admixtures. Steel wire and cement are the largest cost items.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| High-Tensile Steel Wire (4 mm) | Prestressing reinforcement | Domestic wire manufacturers | 22–28% |
| Cement (OPC 53 Grade) | Binder for high-strength concrete | Domestic cement plants and dealers | 18–22% |
| Coarse Aggregate | Concrete strength | Local crushers and quarries | 6–8% |
| Fine Aggregate (Sand) | Concrete filler | Local river or manufactured sand | 3–5% |
| Earthing Wire, Fittings & Admixtures | Earthing, workability | Domestic suppliers | 2–4% |
High-tensile wire must meet the relevant Indian Standards and be tested for strength and relaxation, while cement, aggregates, and water must meet concrete specifications to achieve the high strength needed for prestressing. Cement and steel prices move with market cycles, and sand availability varies by state, so contracts with reliable suppliers, testing of each lot, and price variation clauses in tenders where available help manage cost and quality.
Location, Land & Infrastructure
Location shapes access to customers, raw materials, labour, and transport. The best location for P.C.C. Electric Poles manufacturing plant setup lies close to major DISCOM project areas and contractor bases, with nearby cement plants or dealers, aggregate quarries, good road access for long trailers, reliable power and water, and enough flat land for casting beds and stacking yards.
Preferred States for P.C.C. Pole Plants in India
| State | Why It Works | Key Advantage |
|---|---|---|
| Uttar Pradesh | Largest distribution network and RDSS works | High pole demand |
| Bihar | Rapid network expansion and strengthening | Strong DISCOM demand |
| Madhya Pradesh | Agricultural feeders and rural networks | Feeder separation demand |
| Rajasthan | Large area, agricultural and solar feeders | PM-KUSUM and network expansion |
| West Bengal | Dense distribution networks | Steady replacement and expansion |
| Andhra Pradesh | Agricultural and urban network upgrades | Southern market access |
Uttar Pradesh and Bihar have some of the largest distribution networks and strengthening programmes, while Madhya Pradesh and Rajasthan have extensive agricultural and rural feeders linked to feeder separation and solarisation. West Bengal and Andhra Pradesh offer steady demand for network upgrades and replacement. Because transport adds significantly to the delivered cost of poles, many producers set up plants in more than one state to serve tenders efficiently.
Quality and Testing Requirements
P.C.C. poles must comply with IS 1678 for prestressed concrete poles for overhead power, traction, and telecom lines, with testing as per IS 2905, along with the technical specifications of each DISCOM. Key controls include testing of cement, aggregates, and wire, regular concrete cube tests, verification of wire tension, checks on dimensions and cover, and transverse strength tests on sample poles during type testing and acceptance inspections. Many DISCOMs inspect production and witness tests before dispatch, so documented quality systems and a well-equipped laboratory are essential.
Infrastructure Requirements (Mechanised Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 5 – 10 acres | Casting beds and stacking yard |
| Casting Beds | Long-line beds with anchor blocks | Covered or open sheds |
| Stacking Yard | Hardened, well-drained | Curing and storage of poles |
| Power Requirement | 250 – 500 kW | Batching, vibrators, cranes |
| Water Supply | Mixing and curing | Borewell or municipal supply |
| Steam Curing System | Boiler and curing covers | Faster mould turnaround |
| Quality Laboratory | Cube testing, transverse load test rig | Type and acceptance tests |
Infrastructure for a P.C.C. pole plant centres on long-line casting beds with strong anchor blocks, a batching plant, material storage, a large hardened yard for curing and stacking, gantry cranes or forklifts for handling, steam curing where used, and a laboratory with a pole testing rig. Planning space for additional beds and longer poles from the outset supports future growth.
P.C.C. Electric Poles Manufacturing Machinery and Equipment
Machinery for P.C.C. poles is widely manufactured in India, including batching plants, moulds, tensioning equipment, and handling systems. The main equipment is summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Concrete Batching Plant | Weigh and batch materials | Automatic, accurate dosing |
| Pan or Planetary Mixer | Mix high-strength concrete | Low water-cement ratio |
| Long-Line Casting Beds | Hold moulds and anchors | With end anchor blocks |
| Steel Pole Moulds | Shape poles | 7.5 m, 8 m, 9 m, 11 m sizes |
| Hydraulic Tensioning Jacks | Stretch steel wires | Calibrated pressure gauges |
| Wire Decoilers & Cutting Machines | Prepare high-tensile wire | Accurate lengths |
| Vibrators | Compact concrete | Needle and shutter vibrators |
| Steam Curing System | Accelerate curing | Boiler, pipes, covers |
| Gantry Cranes & Handling Equipment | Lift and stack poles | Gantry, EOT, forklifts |
| Testing Equipment | Check quality and strength | Cube testing machine, transverse load rig |
Equipment selection should follow capacity and product range. The number of casting beds and moulds largely determines output, while steam curing can shorten the casting cycle and raise bed utilisation. Many promoters begin with a few beds, manual handling, and water curing, then add automatic batching, steam curing, and gantry cranes as orders grow.
P.C.C. Electric Poles Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below summarise the capital and operating cost structure of a mechanised P.C.C. pole plant in India. The final P.C.C. Electric Poles Investment Cost for a specific project depends on capacity, number of beds and moulds, mechanisation, curing method, land costs, and working capital for raw materials and receivables.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 28–36% | Batching, tensioning, vibrators, curing, cranes |
| Moulds & Casting Beds | 12–16% | Steel moulds, beds, anchor blocks |
| Land & Yard Development | 10–14% | Land, levelling, hardened yard |
| Civil Works & Sheds | 10–14% | Sheds, stores, laboratory, offices |
| Pre-operative & Contingency | 4–6% | Type testing, approvals, trials |
| Working Capital | 18–24% | Materials, finished poles, receivables |
Machinery, moulds, and yard development form most of the fixed investment, while working capital is significant because government buyers and contractors often take several months to pay. A P.C.C. Electric Poles Business Plan models these components so that capacity, mechanisation, and financing rest on realistic numbers.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials | 55–65% | Steel wire and cement dominate |
| Utilities | 10–14% | Power, water, steam |
| Labour | 9–12% | Casting crews, operators, supervisors |
| Transport & Logistics | 8–12% | Delivery to project sites |
| Maintenance & Moulds | 2–4% | Mould repair, equipment upkeep |
| Testing & Overheads | 2–3% | Inspection, admin, insurance |
With materials making up most of operating cost, profitability depends on cement and wire prices, mix efficiency, rejection rates, bed utilisation, and freight to project sites. A sound financial model should test margins against raw material price increases, lower order flow, tender price competition, payment delays, and transport costs.
Financial Analysis and Profitability
P.C.C. pole manufacturing offers steady returns for efficient producers with reliable order books. The profitability of P.C.C. Electric Poles manufacturing business in India improves with approved vendor status in several states, high bed and mould utilisation, efficient material use, low rejection rates, a plant location close to project sites, and disciplined management of receivables.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 20–30% | IMARC benchmark |
| Net Profit Margin | 7–14% | After depreciation and Indian corporate taxes |
| Payback Period | 4–6 Years | Depends on order flow |
| IRR (Internal Rate of Return) | 16–22% | Sensitive to utilisation and payments |
| Capacity Utilization (stable ops) | 60–80% | Linked to tender wins |
| Break-even Capacity Utilization | 45–55% | Competitive tender pricing |
Order flow is the decisive factor. P.C.C. poles are a tender-driven product with many competing producers, so margins depend on winning enough orders at viable prices, keeping the plant busy through scheme cycles, and being paid on time. Plants with approvals in several states, strong contractor relationships, and efficient operations are best placed to earn the benchmark margins.
Returns can be strengthened by locating near large DISCOM project areas, registering as an approved vendor in multiple states, using steam curing to raise bed utilisation, optimising mix design and wire use, adding 11 m and special poles, using MSME benefits in public procurement, and supplying EPC contractors as well as DISCOMs directly.
Key Risks and Mitigation
The main risks are dependence on government schemes and tenders, delayed payments, intense price competition, cement and steel wire price swings, high transport costs, and quality failures during inspection. Demand risk is reduced by serving several states and customer types; payment risk through careful selection of buyers and contract terms; price risk through supplier contracts and price variation clauses; logistics risk through plants close to demand; and quality risk through strict testing and documentation.
Licenses and Approvals for P.C.C. Electric Poles Manufacturing in India
A P.C.C. pole unit requires business, industrial, environmental, quality, and vendor approvals. Promoters typically need the following before supplying customers:
- Business Registration: Company or firm incorporation, GST registration, and Udyam registration for MSME benefits in public procurement.
- Factory License: Registration under the Occupational Safety, Health and Working Conditions Code, 2020 or the applicable state labour code, with an approved plant layout.
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, covering dust and boiler emissions.
- BIS License: Certification of conformity with IS 1678 where required by buyers or applicable regulations.
- DISCOM Vendor Registration and Type Testing: Approved vendor status with state utilities, including plant inspection and type tests on sample poles.
- Tender Portal Registrations: Registration on the Government e-Marketplace and state procurement portals.
- Boiler Registration, Fire NOC and Labour Registrations: Steam boiler registration where steam curing is used, fire safety approval, and EPF and ESI registrations.
DISCOM vendor approval and type testing usually sit on the critical path, since poles cannot be supplied to utilities without them. Engaging a P.C.C. Electric Poles Manufacturing Consultant in India can help promoters choose the right capacity and location, plan the plant and yard, prepare for type tests, and obtain vendor approvals.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, product range, capacity, target customers, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India P.C.C. Electric Poles Manufacturing Industry
Several recent developments are shaping the Indian power distribution and pole industry:
- RDSS extension and sanctions: The Revamped Distribution Sector Scheme, with a total outlay of about INR 3.04 lakh crore, has been extended to March 2028, and in August 2026 the government reported about INR 1.53 lakh crore of sanctioned loss reduction infrastructure works, a major source of demand for distribution poles.
- Higher budget support: The Union Budget for FY 2026–27 raised the Ministry of Power's allocation by about 39% over the previous year's revised estimate, with nearly INR 18,000 crore directed to RDSS and allied schemes.
- PM-KUSUM extension and next phase: In July 2026, the government reported 13.11 GW of solar capacity installed under PM-KUSUM by March 2026 against a 34.8 GW target, with projects that signed power purchase agreements by December 2025 given until March 2027, while a successor scheme focused on feeder-level solarisation is being prepared.
Together these point to sustained public investment in distribution networks and agricultural feeders over the next few years, supporting steady demand for P.C.C. poles. For new entrants, success depends on vendor approvals, consistent quality, efficient operations, and careful management of payment cycles.
How P.C.C. Electric Poles Manufacturing Project Report and DPR Helps Investors
A detailed P.C.C. Electric Poles Project Report gives investors a structured roadmap covering demand from DISCOMs and schemes in target states, tender and vendor approval requirements, product mix, raw material sourcing, process design, machinery, plant and yard layout, utilities, quality systems, and economics. It helps promoters choose the right capacity and mechanisation level, estimate capital expenditure (CapEx) and operating expenditure (OpEx), assess profitability, and identify risks before implementation.
At the core of the DPR is a P.C.C. Electric Poles Financial Model covering pole-wise volumes and tender prices, cement, wire, and aggregate consumption, bed cycle times and utilisation, labour, utility, transport, and testing costs, working capital for receivables, cash flow projections, break-even, return on investment (ROI), and payback. Because returns depend on order flow and payment cycles, lenders expect sensitivity analysis, which is why many promoters engage a P.C.C. Electric Poles Plant Project Report Consultant in India to prepare bank-ready documents.
For a P.C.C. pole project specifically, a strong DPR also answers the questions that matter most: which states and DISCOMs to target, how quickly vendor approvals can be obtained, how many beds and moulds are needed, whether steam curing is worthwhile, and how returns hold up if tender prices fall, payments are delayed, or raw material prices rise. An experienced P.C.C. Electric Poles Manufacturing Feasibility Study Consultant tests these scenarios so that the final plan is one lenders and partners can back with confidence.
Frequently Asked Questions
How do I set up a P.C.C. electric poles manufacturing plant in India?
Start by studying DISCOM demand and tender requirements in your target states, then commission a feasibility study and DPR. Acquire land near project areas, build casting beds and a yard, install batching, tensioning, curing, and handling equipment, obtain factory and pollution approvals, complete type testing and vendor registration, and begin bidding for tenders.
What is the cost of setting up a P.C.C. electric poles manufacturing plant in India?
A mechanised plant producing 1,00,000 to 1,50,000 poles a year typically needs INR 15 crore to INR 30 crore, while a semi-mechanised unit of 30,000 to 60,000 poles a year can start at around INR 4 crore to INR 10 crore.
How are P.C.C. electric poles made?
High-tensile steel wires are laid in moulds on a long-line casting bed and stretched with hydraulic jacks. High-strength concrete is placed and vibrated, the poles are cured until the concrete is strong enough, the wires are released and cut, and the poles are demoulded, cured further, tested, and dispatched.
What machinery is needed for a P.C.C. electric poles manufacturing plant?
Key equipment includes a concrete batching plant and mixer, long-line casting beds, steel pole moulds, hydraulic tensioning jacks, wire decoilers and cutters, vibrators, a steam curing system, gantry cranes or forklifts, and testing equipment such as a cube testing machine and a transverse load rig.
What raw materials are used in P.C.C. electric poles?
The main inputs are high-tensile steel wire, OPC 53 grade cement, coarse and fine aggregates, water, earthing wire, fittings, and admixtures.
Is a P.C.C. electric poles manufacturing business profitable in India?
Benchmark figures point to a 7 to 14% net margin and an IRR of around 16 to 22%, with payback in 4 to 6 years. Profitability depends mainly on order flow, tender prices, bed utilisation, raw material costs, and timely payments.
What licenses are needed for a P.C.C. electric poles manufacturing unit in India?
A unit typically needs company, GST, and Udyam registration, a Factory License, State Pollution Control Board consents, a BIS license where required, DISCOM vendor registration with type testing, tender portal registrations, and boiler, fire, and labour registrations.
Which state is best for a P.C.C. electric poles manufacturing plant?
Uttar Pradesh, Bihar, Madhya Pradesh, Rajasthan, West Bengal, and Andhra Pradesh are strong options. The best site is close to large DISCOM project areas, with good access to cement, aggregates, and roads.
How do I get a feasibility study or DPR for a P.C.C. electric poles manufacturing plant?
A professionally prepared DPR covers demand and tender analysis, vendor approval requirements, technical design, costs, and financial projections for bank appraisal. Many promoters work with a P.C.C. Electric Poles Business Plan Consultant in India to prepare it and align it with lender requirements.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Yes, India's intensifying heat is one of the clearest demand signals behind the India air conditioning market, which IMARC Group values at USD 6.15 Billion in 2025 and USD 7.07 Billion in 2026. The market is projected to reach USD 21.59 Billion by 2034, growing at a CAGR of 14.98% during 2026-2034.
An Alkaline Battery Manufacturing Plant Setup in India addresses a product used in almost every home, office, and clinic, yet until recently made almost entirely abroad.
An LED Light Manufacturing Plant Setup in India taps into one of the largest and most mature consumer electrical markets in the country.
An LED Chip Manufacturing Plant Setup in India addresses one of the biggest gaps in the country's lighting and display supply chain. India assembles hundreds of millions of LED bulbs, battens, panels, and displays every year, yet almost all LED chips, the tiny semiconductor dies that actually emit light, are imported, mainly from China, Taiwan, and South Korea.
A Smartphone Manufacturing Plant Setup in India places an investor inside one of the country's biggest industrial success stories of the past decade.
A Smart Watch Manufacturing Plant Setup in India serves one of the world's largest wearables markets. Indian consumers buy tens of millions of smartwatches every year, and domestic brands have shifted much of their production from imports to local contract manufacturers.
The India Semiconductor Market has moved past the stage of ambition documents and into the stage of concrete assets, approved sites and dated delivery milestones. The India Semiconductor Market size reached USD 59.78 Billion in 2025, expanded to USD 73.00 Billion in 2026, and is projected to reach USD 180.20 Billion by 2034, growing at a CAGR of 11.95% over the 2026-2034 forecast period.
A genset combines an engine, usually diesel or gas, with an alternator that converts its motion into electricity, mounted on a steel base frame with a fuel tank, exhaust and emission after-treatment, a control panel, and in most cases a soundproof acoustic enclosure.
Setting up a Power Cable Manufacturing Plant in India puts an investor directly in the path of one of the country's largest infrastructure build-outs.
Servos are precision electric motors fitted with a position sensor, called an encoder, and paired with an electronic drive that controls speed, torque, and position very accurately.
PVC-insulated wires and cables are made by drawing copper or aluminium rod into fine conductors, annealing and stranding them, and covering them with coloured PVC insulation and, for multi-core cables, an outer PVC sheath and sometimes steel armour.
Portable chargers are compact battery packs made from lithium-ion or lithium-polymer cells, a charging and protection circuit board, ports or wireless coils, and a plastic or metal casing.
Small electric cooking and food preparation products, such as mixer grinders, induction cooktops, electric kettles, air fryers, hand blenders, and sandwich makers, are made by moulding plastic bodies, forming steel and aluminium parts, winding motors or fitting heating elements, assembling control boards, and wiring and testing each unit for safety.
Aluminum-air batteries generate electricity by reacting aluminum plates with oxygen from the air in a water-based electrolyte. Aluminum has a very high theoretical energy density, and instead of being recharged from a socket, spent plates are swapped for fresh ones while the aluminum hydroxide produced is recycled into new aluminum.
LED bulbs use light-emitting diodes mounted on a metal-core circuit board, powered by a small electronic driver and housed in a plastic and aluminium body with a diffuser and a standard B22 or E27 cap.
Inverters convert direct current from batteries or solar panels into the alternating current used by homes, shops, and factories.
Electrical control panels are steel enclosures that house circuit breakers, contactors, relays, busbars, meters, drives, and controllers to distribute power and control motors, machines, and processes safely.
Microchips, or integrated circuits and semiconductor devices, are the building blocks of phones, computers, vehicles, appliances, power systems, telecom networks, and defence equipment.
Resistors are the most widely used electronic components, found by the dozens or hundreds in almost every circuit board, from phones, laptops, and televisions to vehicles, appliances, telecom equipment, power electronics, medical devices, and defence systems.
Rare earth magnets, mainly neodymium-iron-boron (NdFeB) and samarium-cobalt, are the strongest permanent magnets made, and they sit at the heart of electric vehicle motors, wind turbine generators, electronics, industrial automation, medical devices, and defence systems. India imported over 53,000 tonnes of rare earth permanent magnets in 2024-25 and has almost no domestic production, while demand is expected to double by 2030.
Wires and cables carry power and signals through every home, office, factory, railway, data centre, and solar park, and India's market has grown to about USD 10 billion as construction, power transmission, renewable energy, and industrial investment have expanded.
Heat exchangers are among the most widely used pieces of engineering equipment in the world. Refineries, petrochemical and fertiliser plants, power stations, pharmaceutical and food factories, HVAC systems, and data centers all depend on them to heat, cool, condense, and recover energy from process streams.
India's trucks and buses rarely rest. They carry freight across highway corridors, move goods from ports and factories, and ferry millions of passengers every day, often under heavy loads and tough road conditions.
Silicon wafers are the thin, precisely sliced discs and squares on which solar cells and computer chips are built. India has rapidly become a major assembler of solar modules and is now building cell capacity, but almost all of the wafers those cells need are still imported.
Every video call, UPI payment, and 5G connection in India ultimately travels over glass. Fiber optic cables carry the country's data between cities, into mobile towers and data centres, and increasingly right into homes through fiber-to-the-home connections.
Setting up an Air Conditioner Manufacturing Plant in India is an assembly-driven, high-volume consumer durable venture, powered by rising household incomes, extreme summers, rapid urbanisation, and one of the lowest room air-conditioning penetration rates among large economies.
Setting up a High Voltage Cable Manufacturing Plant in India is a capital-intensive, high-value venture, powered by the country's massive power-transmission expansion, renewable-energy build-out, and the shift toward underground cabling in cities.
Setting up a Copper Cable Manufacturing Plant in India is a high-demand, infrastructure-driven venture, powered by the country's construction boom, rapid electrification, and steady industrial and appliance demand.
Setting up a Junction Box Manufacturing Plant in India is a high-demand, infrastructure-driven venture, powered by the country's construction boom, rapid electrification, and expanding solar and industrial sectors.
Setting up an Electric Cable Manufacturing Plant in India is a high-demand, infrastructure-linked venture, powered by the country's rapid growth in power, construction, renewable energy, and electrification. Cables and wires are essential to every building, factory, grid, and vehicle, giving an Electric Cable Manufacturing Plant a large and steadily growing market.
Setting up a Semiconductor Fabrication Manufacturing Plant in India is a highly capital-intensive but strategically transformative venture, driven by the country's semiconductor mission, deep policy incentives, and a vast import-substitution opportunity. Semiconductors are the foundation of every modern electronic and digital product, yet India currently imports almost all of its chip requirement.
Setting up a PCB Manufacturing Plant in India is a capital-intensive but strategically timed venture, driven by the country's electronics manufacturing push, strong policy incentives, and a large import-substitution opportunity. Printed circuit boards are the backbone of every electronic product, yet India still imports the overwhelming majority of its PCB requirement.
The Indian PCB (Printed Circuit Board) Market is emerging as the physical backbone of the country's electronics manufacturing ambitions. The market reached USD 7.27 Billion in 2025 and is projected to reach USD 25.48 Billion by 2034, growing at a CAGR of 14.96% (2026–2034), a total addressable market expansion driven by the Production Linked Incentive (PLI) scheme, 5G infrastructure rollout, and rising domestic consumer electronics demand.
Setting up an E-waste Recycling Plant in India is a capital-intensive but high-potential venture, driven by the country's soaring volume of discarded electronics, tightening Extended Producer Responsibility regulations, and the rising value of recovered metals. India is now among the world's largest generators of electronic waste, yet only a small share is processed through formal, compliant channels, leaving a large, policy-backed opportunity for organized recyclers who can capture volumes shifting from the informal sector.
Global semiconductor demand across automotive, data centers, and defense, highlighting market segmentation, key applications, regional dynamics, and industry shifts.
The hearables market represents one of the most dynamic segments within consumer electronics and wearable technology. These intelligent audio devices have evolved beyond simple wireless earbuds into multifunctional platforms combining premium audio with health monitoring, artificial intelligence, and seamless digital connectivity.
A smart washing machine is a sophisticated home appliance that incorporates advanced digital features such as connectivity, sensor technology, and automated controls for improved efficiency, convenience, and user control. In contrast to traditional washing machines, smart washing machines come pre-installed with advanced features such as Wi-Fi connectivity, smart load detection, smart detergent dispensing, and voice-control capability.
A smartphone is a portable electronic device that combines sophisticated capabilities in computer processing, wireless communication, multimedia entertainment, and internet access. Smartphones are distinct from other mobile phones in that their operation involves highly sophisticated platforms of operation that are capable of supporting multiple applications, multitasking, and connectivity with internet platforms.
Semiconductor manufacturing is a highly specialized industrial process that involves the design, fabrication, and assembly of semiconductor devices including integrated circuits (ICs), memory chips, sensors, and discrete components. The process transforms raw semiconductor materials, primarily silicon, into sophisticated electronic components through a combination of physical and chemical processing steps, such as wafer fabrication, photolithography, doping, etching, thin-film deposition, and packaging.
The retail landscape is experiencing a profound transformation as self-checkout systems emerge as critical infrastructure components reshaping consumer experiences and operational efficiency globally. These automated solutions enable customers to independently scan, bag, and pay for purchases without cashier assistance, representing a fundamental shift in modern commerce.
The webcams market is experiencing unprecedented transformation as digital communication becomes the cornerstone of modern business, education, and healthcare. Global webcam industry dynamics are being reshaped by technological innovation and evolving workplace models.
As smartphones become a way of life for most Filipinos, the market has changed dramatically and expectations from consumers are higher than ever before. With the demand for smartphones growing, there is a significant change in consumer shopping habits with more emphasis on using online platforms for shopping. This change is closely interlinked with the fast growth of the Philippines e-commerce market, both bringing opportunities and challenges to the stakeholders of the smartphone industry.
As technology continues to advance, lighting has transformed from a basic necessity into a strategic enabler of innovation, efficiency, and sustainability. The evolution from incandescent bulbs to LEDs, smart systems, and intelligent lighting networks represents not just technological change but a redefinition of how energy, design, and functionality intersect in the built environment.
An LED light is an illuminating device that utilizes Light Emitting Diodes as its source of light, generating light through a semiconductor-based process called electroluminescence. When electrical current flows across the semiconductor material of the diode, electrons emit energy as photons and thus produce highly efficient and concentrated illumination.
An LED bulb is a solid-state lighting device that uses Light Emitting Diodes (LEDs) as its illumination source. Different from incandescent or fluorescent lamps, light in LED bulbs is produced by electroluminescence, a process where the passing of an electric current through a semiconductor material emits photons directly. This process is highly energy-efficient, with a far larger percentage of the electricity being converted to usable light and very little heat generated in the process.
The junction box, generally made from plastic, metal, or composite materials, houses wire connections, terminations, and protective components to allow the safe distribution and routing of electrical circuits. The junction box will provide insulation, mechanical protection, and a secure environment to avoid accidental contact with live electrical parts, moisture intrusion, or dust accumulation.
The Japan power electronics market is poised to grow substantially, driven by rising demand in automotive, energy, industrial automation, and infrastructure sectors. According to IMARC Group, the Japan power electronics market is studied from 2019 to 2024 with projections extending to 2033.
Japan's printed circuit board (PCB) industry is the world leader in technology innovation, enabling consumer electronics, automotive, and next-generation communication system development. As a key enabler of modern electronic products, PCBs provide the essential building blocks for embedding semiconductors, sensors, and microchips into miniaturized, high-performance devices. Japan, through its world-class manufacturing base and engineering expertise, remains the hub of the global PCB supply chain.
Aluminum-Air (Al-Air) battery is a new energy storage technology that has attracted interest as a future alternative to conventional lithium-ion batteries, specifically for electric vehicle (EV) use. As opposed to normal rechargeable batteries, the Al-Air battery is a metal-air electrochemical cell with aluminum as the anode, oxygen from the ambient air as the cathode reactant, and a liquid electrolyte (commonly sodium hydroxide or potassium hydroxide) as the medium through which the reaction occurs.
Aluminium wire is an essential industrial commodity commonly employed in power transmission, electrical distribution, building construction, and manufacturing processes owing to its high conductivity-to-weight ratio, resistance to corrosion, and cost advantage over copper. Produced by methods including continuous casting, rolling, and drawing, aluminum wire is available in various grades and alloys to serve the wide demands, from overhead transmission conductors and building wiring to automotive harnesses and electronic applications.
Air conditioners are electromechanical devices used to control indoor climate by extracting heat and humidity and ensuring optimum air circulation. Generally consisting of a compressor, condenser, evaporator, refrigerant fluid, filters, fans, and electronic controls, air conditioners work based on the principle of heat exchange, moving heat from indoor areas to the external environment. Contemporary units come in diverse configurations, such as split systems, window units, central air systems, and portable models, supporting respective residential, commercial, and industrial applications. Some of the major characteristics are efficiency in cooling, energy use, noise rating, and environmental footprint in relation to refrigerant type.
E-waste, or electronic waste, is electrical and electronic equipment that has been discarded, such as computers, cell phones, television sets, servers, and household appliances. It is among the world's fastest-growing streams of waste, consisting of a heterogeneous combination of metals, plastics, glass, and toxic substances. E-waste contains valuable metals like copper, aluminum, gold, silver, palladium, and rare earth elements, in addition to toxic materials like lead, mercury, cadmium, and brominated flame retardants.
Polished silicon wafers are very pure, ultra-flat semiconductor substrates that are produced from high-quality single-crystal silicon. The wafers act as the material base for making integrated circuits, power devices, and MEMS (Microelectromechanical Systems). The wafers are made of monocrystalline silicon ingots using the Czochralski or Float-Zone process, from which the wafers are cut, lapped, etched, and polished to atomic-scale flatness and defect-free surfaces.
AI is revolutionizing Japan’s semiconductor industry by boosting innovation and efficiency across the entire value chain. Advanced artificial intelligence (AI)-powered Electronic Design Automation (EDA) tools significantly shorten chip design cycles, improving performance and energy efficiency.
Recent projections indicate that Australia semiconductor market, including services, is growing at a steady compound annual growth rate as the nation deepens its tech infrastructure. The importance of semiconductors spans electronics, defense systems, telecommunications, and emerging AI applications, which position the local ecosystem as strategically vital for growth.
Fiber optic cables are high-tech communications cables that carry information like bursts of light along extremely thin glass or plastic strands, providing high-speed, high-bandwidth connectivity with little loss of signal. Fiber optic cables make up the foundation of contemporary telecommunications, carrying internet, cloud computing, 5G networks, and smart infrastructure.
CAT (Category) cables are twisted-pair Ethernet cables utilized for copper-based wired network communications, varying from CAT5e to CAT8 standards. The cables carry data through copper conductors, but with different speeds (up to 40 Gbps for CAT8) and bandwidths, supporting networks such as LANs, data centers, and smart buildings.
India's semiconductor industry is undergoing a revolutionary phase driven by rising demand from industries like consumer electronics, automotive technologies, industrial automation, and telecom infrastructure.
USB data cables are critical elements of contemporary digital connectivity, enabling high-speed and consistent data transfer and power supply for a broad scope of electronic products. They provide the foundation for charging and synchronizing smartphones, tablets, laptops, and other peripherals, with significant applications in consumer electronics, industrial automation, and new technologies. With technologies like USB-C, the cables today carry faster data speeds, more power output, and universal compatibility, making them essential in a world that is connected.
Thin-film-transistor (TFT) liquid-crystal display (LCD) is a type of display technology used in many electronic devices, such as smartphones, tablets, laptops, and televisions (TVs). A backlight, colour filters, a thin-film transistor array, and a liquid crystal layer are among the layers that make up this flat-panel display. TFT LCDs are made to produce sharp images with superb viewing angles, strong contrast, and accurate colour reproduction. They are made up of thousands of tiny transistors that regulate how much light enters each pixel. This makes it possible for the display to generate crisp, detailed images at rapid refresh rates. TFT LCD technology's low power consumption is one of its main benefits, which makes it perfect for battery-operated gadgets.
Polycrystalline solar photovoltaic (PV) modules are a key component of solar energy systems, harnessing sunlight and converting it into electricity through the photovoltaic effect. These modules are composed of multiple interconnected solar cells, each made from polycrystalline silicon. Polycrystalline solar panels are renowned for their efficiency, affordability, and versatility, making them a popular choice for various applications such as solar installations, commercial and industrial projects, off-grid systems and solar farms.
The LED chip is the core component of an LED bulb, comprising semiconductor layers that enable the free flow of protons and electrons. Employed in all LED lighting fixtures—from bulbs to tubes—the LED chip fundamentally determines light quality, with variations in brightness, voltage, and wavelength. These chips are manufactured through a process called MOCVD (metal-organic chemical vapor deposition), which creates the semiconductor layers that facilitate electric flow. Major applications of these chips include backlighting, illumination, automotive lighting, signs, and signals.
Semiconductors are crucial components in the modern electronics industry, used in electronic equipment and devices to manage and control the flow of electricity. They are found in consumer items like smartphones, wearables, smart TVs, and advanced equipment used in industrial applications, defense, and aerospace. Semiconductors are further divided into four broad categories: optoelectronics, discrete components, integrated circuits, and sensors. Memory devices, logic devices, analog ICs, MPUs, discrete power devices, MCUs, and sensors are some of the major components of semiconductors.