Pharmaceutical Manufacturing Plant Setup in India: Cost, Process Flow, Machinery, DPR & Financial Guide 2026
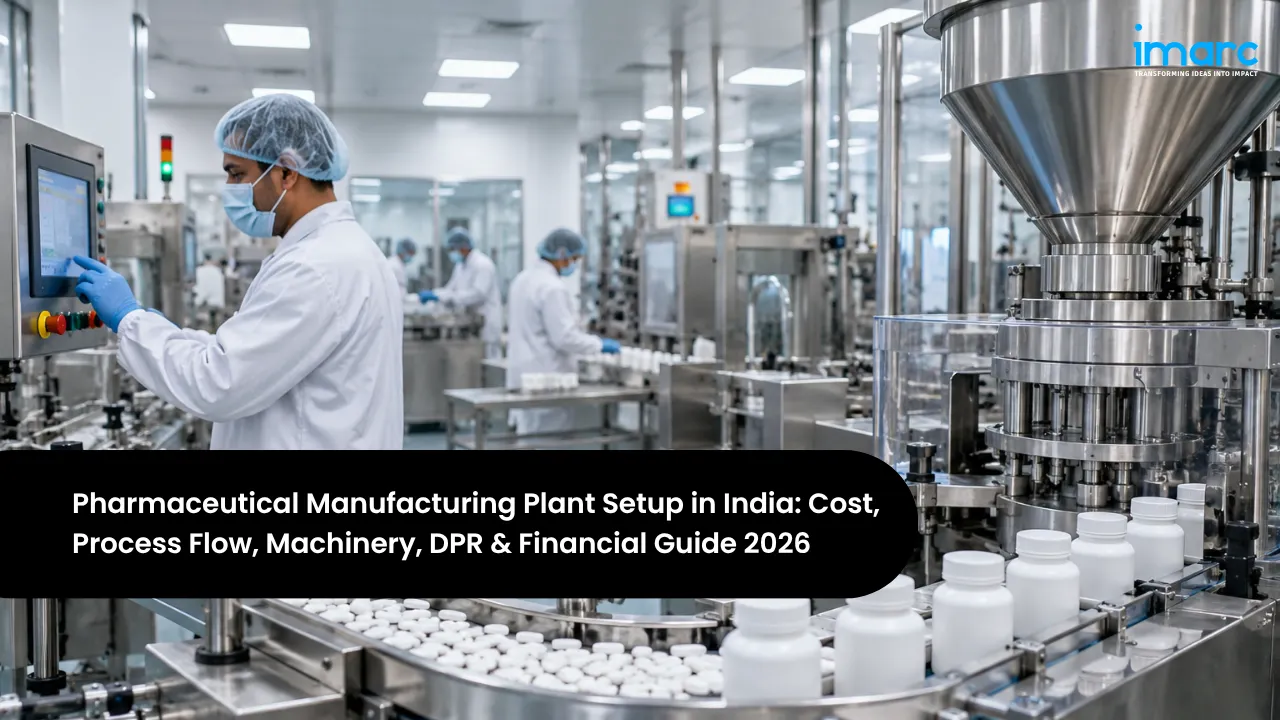
Setting up a Pharmaceutical Manufacturing Plant in India is a high-potential, strategically strong venture, powered by the country's position as the pharmacy of the world and one of the largest generic drug producers globally. India's deep formulation expertise, cost competitiveness, and vast domestic and export demand make a pharmaceutical manufacturing unit setup in India one of the most attractive opportunities in the healthcare sector. A well-run plant converts active ingredients and excipients into finished, quality-assured medicines for domestic use and export.
The Pharmaceutical Manufacturing Plant Cost and Investment depends on dosage forms, capacity, and the level of automation and compliance, with total investment for a typical unit ranging from INR 25 crore to INR 250 crore. Raw materials, chiefly active pharmaceutical ingredients, account for the largest share of operating costs, so procurement and quality control are the most important financial decisions in the project. At healthy capacity utilisation, a well-run Indian plant delivers a net profit margin of 12 to 22% and an IRR of 16 to 26%, with payback typically achieved within 4 to 6 years.
This guide is written for investors and entrepreneurs asking how to start a pharmaceutical manufacturing plant in India. It covers what the business involves, why demand is rising, the process flow, the machinery and raw materials required, location and infrastructure planning, a detailed cost and financial breakdown, the licenses you must secure, and how a project report and DPR turns all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| India Position | Among the world's largest generic drug producers |
| Primary Dosage Forms | Tablets, capsules, liquids, injectables |
| Key Markets | Domestic and export (US, Africa, EU, Asia) |
| Pharmaceutical Production Capacity | Sized by dosage form and demand |
| Indicative Total Investment | INR 25–250 Crore |
| Typical Payback Period | 4–6 Years |
The snapshot captures why this sector attracts strong investor interest: a globally competitive industry, deep formulation know-how, and vast domestic and export demand. The wide investment range reflects a genuine choice of dosage forms and scale, from a focused solid-dosage unit to a multi-line facility spanning tablets, capsules, liquids, and beyond. The rest of this guide unpacks that decision in detail.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Dosage Forms | Tablets, capsules, liquids, injectables |
| Total Project Investment | INR 25 – 250 Crore |
| Payback Period | 4 – 6 Years |
| Net Profit Margin | 12 – 22% |
| IRR | 16 – 26% |
| Best Locations | Himachal, Gujarat, Telangana, Maharashtra, Sikkim |
| Mandatory Approvals | Drug Licence, GMP, Factory Licence, CPCB/SPCB, Fire NOC |
| Key Requirement | GMP-compliant facility and QC |
These indicative parameters give a realistic frame for early feasibility work. The returns are attractive, but they depend on securing quality raw materials, building a fully GMP-compliant facility, and winning approvals and customers in regulated markets. A well-prepared Pharmaceutical Manufacturing Plant Feasibility Study tightens each of these numbers to your specific location, dosage forms, and capacity.
Table of Contents
- What is Pharmaceutical Manufacturing?
- Why is Pharmaceutical Manufacturing Growing in India?
- Pharmaceutical Manufacturing Process Flow
- Raw Materials Required for Pharmaceutical Manufacturing
- Location, Land & Infrastructure
- Pharmaceutical Manufacturing Machinery and Equipment
- Pharmaceutical Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Pharmaceutical Manufacturing Plant in India
- Recent Developments in the India Pharmaceutical Manufacturing Industry
- How a Pharmaceutical Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Pharmaceutical Manufacturing?
Pharmaceutical Manufacturing is the production of finished medicines by converting active pharmaceutical ingredients and excipients into safe, effective, quality-assured dosage forms such as tablets, capsules, and liquids. A pharmaceutical plant carries out formulation, processing, and packaging under strict quality and hygiene controls, so that every batch meets regulatory and therapeutic standards. The activity sits at the heart of healthcare, turning raw chemical ingredients into medicines that patients and markets depend on.
From a business perspective, what makes pharmaceutical manufacturing attractive in India is the combination of world-class formulation capability, cost competitiveness, and enormous domestic and export demand. Every hospital, pharmacy, and export buyer seeking reliable, affordable, compliant medicines is a potential customer. A manufacturer that meets quality standards and builds regulatory approvals is positioned to serve markets where India already holds a leading global position.
- Solid Dosage Forms: Tablets and capsules, the highest-volume category, produced on granulation, compression, and encapsulation lines.
- Liquid Formulations: Syrups, suspensions, and oral liquids requiring mixing, filtration, and filling under controlled conditions.
- Injectables & Sterile: Sterile products demanding the highest cleanroom classes and rigorous validation.
- Topicals & Others: Ointments, creams, and specialty forms that broaden a plant's product range.
The Main Dosage-Form Routes in Pharmaceutical Manufacturing
Understanding which dosage forms your plant will produce is the foundational decision, because it drives equipment, cleanroom design, and compliance:
| Dosage Form | Description | Key Property | Primary Demand |
|---|---|---|---|
| Tablets | Compressed solid doses | High volume, efficient | Broad domestic and export |
| Capsules | Filled hard or soft capsules | Flexible dosing | Wide therapeutic use |
| Liquids | Syrups and suspensions | Paediatric and elderly use | Strong domestic demand |
| Injectables | Sterile parenteral products | Highest compliance | Hospitals and export |
This choice shapes the entire facility, because a Tablet and Capsule Manufacturing Plant needs granulation, compression, and encapsulation lines, while a Liquid Pharmaceutical Manufacturing Plant needs mixing, filtration, and filling systems, and injectables demand the strictest sterile environments. Many Indian entrants begin with a solid-dosage line, the largest and most efficient category, and add liquid or specialty capability as they build approvals and markets. The dosage-form decision drives everything from machinery to the level of investment required.
Why is Pharmaceutical Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
India's pharmaceutical manufacturing sector is being propelled by several structural factors that combine strong domestic demand with global export leadership. Few industries enjoy this alignment of scale, capability, and policy support:
- Global generic leadership: India is among the largest suppliers of generic medicines worldwide, with established access to regulated and emerging markets and a strong quality reputation.
- Rising domestic healthcare demand: Growing population, income, insurance coverage, and chronic-disease prevalence are steadily expanding domestic medicine consumption.
- Cost competitiveness: Lower manufacturing and development costs make Indian plants highly competitive for both domestic supply and export.
- Policy and PLI support: Production-linked incentives and manufacturing schemes actively support domestic pharmaceutical and bulk-drug production and localization.
- Export and outsourcing demand: Global demand for affordable medicines and contract manufacturing continues to create strong export and partnership opportunities.
India-Specific Market Opportunity
| Segment | India Market Context | Manufacturing Role |
|---|---|---|
| Generics | Global generic leadership | Core high-volume production |
| Domestic Healthcare | Large, growing patient base | Broad medicine supply |
| Exports | Regulated and emerging markets | Compliant, competitive supply |
| Contract Manufacturing | Growing outsourcing demand | Capacity for brand owners |
| Chronic & Specialty | Rising disease burden | Higher-value formulations |
The strongest opportunity lies in building a compliant, efficient plant positioned for both domestic supply and export or contract manufacturing. A producer that achieves the right approvals and quality systems can serve regulated markets, brand owners, and the large domestic sector alike. Moving into chronic-disease and specialty formulations, where demand and margins are rising, further strengthens a plant's competitive position in a large and growing market.
Pharmaceutical Manufacturing Process Flow
Understanding the process helps you plan equipment, cleanroom infrastructure, and the main cost drivers. Pharmaceutical production is a precise, quality-controlled operation carried out in classified clean areas, where every step is documented and validated to meet regulatory standards. The flow differs by dosage form but follows a common logic of dispensing, processing, forming, and packaging under strict control.
The Pharmaceutical Formulation Manufacturing Process
For solid dosage forms, materials move from weighing through granulation, drying, blending, compression or filling, coating, and packaging, with quality checks at each stage. Setting up this pharma production line setup in India requires careful equipment selection and cleanroom design so that the flow meets both efficiency and compliance goals, since a poorly planned layout raises both contamination risk and running cost.
| Unit Operation | Key Activity |
|---|---|
| Dispensing | Raw materials weighed in controlled conditions |
| Granulation | Wet or dry granulation of the blend |
| Drying | Granules dried to required moisture |
| Blending | Granules blended with lubricants and excipients |
| Compression / Filling | Tablets compressed or capsules filled |
| Coating | Tablets coated for protection or release |
| Quality Control | In-process and finished-product testing |
| Packaging | Blister, strip, or bottle packaging |
| Labelling & Serialization | Labelling and track-and-trace coding |
| Warehousing & Dispatch | Storage and dispatch to markets |
Two points determine profitability across this flow. First, quality and yield are decisive, because a batch that fails testing is a costly loss and regulatory standards are non-negotiable, so process control and documentation govern outcomes. Second, an unbroken clean, validated environment protects both product quality and market approval. Liquid manufacturing follows a parallel flow of mixing, filtration, filling, and packaging under the same disciplined controls. Across both routes, thorough documentation and batch records are not paperwork for their own sake but the evidence regulators rely on to approve every release.
Raw Materials Required for Pharmaceutical Manufacturing
The main inputs are active pharmaceutical ingredients and excipients, and securing consistent, quality-approved supply is the single biggest determinant of a plant's viability. Because active ingredients dominate cost and directly affect quality and compliance, a reliable, qualified supplier network is central to project planning, alongside packaging materials that meet regulatory requirements.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Active Pharmaceutical Ingredients | Therapeutic active substance | Domestic bulk-drug and imports | 45–60% |
| Excipients | Binders, fillers, coatings | Domestic and imported suppliers | 8–15% |
| Packaging Materials | Blister foil, bottles, cartons | Domestic packaging suppliers | 8–15% |
| Solvents & Process Aids | Processing inputs | Domestic chemical suppliers | 3–8% |
| Quality & Testing Consumables | QC and validation | Specialty suppliers | 2–5% |
Because active ingredients are such a large and quality-critical share of cost, supplier qualification and procurement strategy are the biggest levers on both profitability and compliance. India has a strong bulk-drug base but still imports certain key ingredients, so building qualified, reliable supplier relationships and holding appropriate stock protects both cost and continuity. Approved packaging and testing consumables round out the inputs a compliant plant needs to release every batch confidently.
Location, Land & Infrastructure
Where you set up your Pharmaceutical Manufacturing Plant in India significantly affects access to talent, suppliers, incentives, and export logistics. Because pharmaceutical production demands classified cleanrooms, controlled utilities, and strict environmental compliance, infrastructure quality and pharma-cluster location shape site selection more than raw-material proximity.
Best States for Pharmaceutical Manufacturing Plant Setup in India
| State | Why It Works | Key Advantage |
|---|---|---|
| Himachal Pradesh | Baddi pharma cluster | Incentives and ecosystem |
| Gujarat | Strong pharma and chemical base | Suppliers and logistics |
| Telangana | Hyderabad pharma hub | Talent and bulk-drug base |
| Maharashtra | Large pharma industry | Market and talent access |
| Sikkim & Uttarakhand | Incentive-backed clusters | Tax and cost advantages |
| Andhra Pradesh | Growing pharma and API base | Land, power, and supply |
The strongest locations combine an established pharmaceutical ecosystem, skilled talent, reliable utilities, and supportive incentives. Himachal, Gujarat, and Telangana lead for their clusters, supplier bases, and talent, while incentive-backed states such as Sikkim and Uttarakhand offer cost advantages. Because compliance and utilities are central, the quality of infrastructure and access to skilled pharmaceutical professionals should weigh most heavily in the final choice, alongside effluent and environmental capacity.
GMP and Quality Control Requirements
Meeting Good Manufacturing Practice and quality-control standards is not optional but foundational, because regulators and markets require it before a plant can produce and sell medicines. This means classified cleanrooms with controlled air handling, validated water systems, documented procedures, trained personnel, and a fully equipped quality-control laboratory that can test and release every batch to specification. Building the facility to GMP standards from the outset, in line with Schedule M and WHO-GMP expectations, is essential both for regulatory approval and for access to regulated export markets, and retrofitting these requirements later is far more costly than designing them in from the start.
Infrastructure Requirements (Mid-Sized Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 3,000 – 10,000 sq. meters | Industrial or pharma-zone plot |
| Cleanrooms & HVAC | Classified clean areas | Core to GMP compliance |
| Water System | Purified water and WFI | Validated pharma-grade water |
| Power Requirement | 500 kW – 2 MW | Stable supply with backup |
| Quality Control Laboratory | Fully equipped QC lab | For testing and release |
| Effluent Treatment Plant | Mandatory | Pharma effluent compliance |
| Warehousing | Controlled storage | For materials and finished goods |
Infrastructure for a pharmaceutical plant centres on cleanrooms, validated water, HVAC, and quality-control facilities, because product quality and regulatory approval depend on all of them. These systems represent a large share of capital cost and are inspected closely by regulators, so under-provisioning them is both a compliance and a commercial risk. Building adequate cleanroom, water, and laboratory capacity from the start supports both scaling and the standards that regulated markets demand.
Pharmaceutical Manufacturing Machinery and Equipment
The equipment set spans dispensing, processing, forming, packaging, and testing, and the line-up depends heavily on the dosage forms produced. Because pharmaceutical processing is compliance-critical, machinery must be validated, easy to clean, and GMP-compliant. The machinery required for pharmaceutical manufacturing plant operations, from raw-material dispensing through finished-product testing, is summarized below.
| Equipment | Function | Key Specification |
|---|---|---|
| Dispensing Booth | Weigh materials safely | Controlled, contained airflow |
| Rapid Mixer Granulator | Granulate the blend | High-shear mixing |
| Fluid Bed Dryer | Dry granules | Controlled drying |
| Blender | Blend granules and excipients | Uniform blending |
| Compression Machine | Compress tablets | High-speed, precise |
| Capsule Filling Machine | Fill capsules | Accurate dosing |
| Coating Machine | Coat tablets | Uniform film coating |
| Liquid Mixing & Filling Line | Produce and fill liquids | For oral liquid products |
| Blister / Strip Packing | Package solid doses | High-speed packaging |
| QC Lab Instruments | Test and release products | HPLC, dissolution, and analysis |
Equipment selection should follow your dosage forms rather than the other way around. A solid-dosage line needs granulation, compression, coating, and packaging, while liquids need mixing and filling, and injectables add sterile and validation-heavy equipment. Quality-control laboratory instruments are essential and easy to under-budget, because the ability to test and release every batch to specification is what allows a plant to operate and to access regulated markets.
Pharmaceutical Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below give you a breakdown of both the upfront capital investment and the ongoing operating costs, based on industry analysis of a mid-sized facility in India. The actual setup cost for your specific project, and the wider Pharmaceutical Manufacturing Investment Cost, will depend on your chosen location, dosage forms, capacity, and level of automation and compliance.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Cleanrooms, HVAC & Building | 25–35% | Classified areas and construction |
| Plant & Machinery | 30–40% | Processing, forming, and packaging lines |
| Water System & Utilities | 8–12% | Purified water and utilities |
| Quality Control Laboratory | 6–10% | Testing instruments and lab |
| Effluent & Safety Systems | 4–7% | ETP and safety compliance |
| Pre-operative & Contingency | 5–8% | Engineering, DPR, and buffer |
| Working Capital | 10–15% | Raw materials and receivables |
The CapEx profile is unusual in that cleanrooms, HVAC, and the water system are as significant as the process machinery, because GMP compliance is built into the facility itself. Working capital is also important, since active ingredients are costly and must often be procured ahead of sales. These elements are modelled in detail in the Pharmaceutical Manufacturing Business Plan and Financial Model so that dosage-form and scale choices rest on realistic numbers.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials (APIs, excipients) | 50–65% | Largest cost; active ingredients dominate |
| Labour & Skilled Manpower | 10–15% | Production, QA, and QC staff |
| Power & Utilities | 6–10% | HVAC and processing are energy-intensive |
| Quality & Compliance | 5–10% | Testing, validation, and audits |
| Packaging & Consumables | 4–8% | Compliant packaging materials |
| Maintenance & Overheads | 4–8% | Equipment and facility upkeep |
With raw materials, chiefly active ingredients, dominating operating cost, this is fundamentally a procurement-and-quality business, and margin depends on sourcing well and maintaining high yield and compliance. Operating costs move with active-ingredient prices and quality requirements, so a financial model should track these closely and stress-test margins against material price swings and batch yields, which are the biggest variables, while valuing the higher realizations that regulated markets can command.
Financial Analysis and Profitability
Based on analysis of a mid-sized pharmaceutical facility in India, the financial profile is strong, supported by large domestic and export demand, cost competitiveness, and the value of compliant, quality-assured production. Because raw materials and compliance drive economics, the Pharmaceutical Manufacturing Plant ROI and Profitability improves markedly with efficient sourcing, high yield, strong utilisation, and access to regulated markets.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 35–55% | Driven by product mix and market |
| Net Profit Margin | 12–22% | After depreciation and Indian corporate taxes |
| Payback Period | 4–6 Years | Faster with export and specialty products |
| IRR (Internal Rate of Return) | 16–26% | Higher for regulated-market and specialty output |
| Capacity Utilization (stable ops) | 70–85% | Approvals and contracts protect utilisation |
| Break-even Capacity Utilization | 50–65% | Strong demand supports throughput |
Product mix, utilisation, and market access are the factors that most determine outcomes, because a plant supplying regulated markets and specialty products earns far more than one making only basic generics for a crowded domestic segment. An operator with approvals, contracts, and reliable supply can run comfortably above break-even, while one facing regulatory or demand gaps will see margins swing. This is why compliance, approvals, and market access are as central to the financial model as the machinery itself.
There are several ways to strengthen returns in the Indian context: securing regulated-market and export approvals, moving into higher-value chronic and specialty formulations, adding contract manufacturing to fill capacity, sourcing active ingredients efficiently, and running at high utilisation to spread fixed costs. Strong quality systems that avoid batch failures and regulatory issues further protect profitability.
Key Risks and Mitigation
The principal risks are active-ingredient price and supply volatility, regulatory and quality compliance, and intense competition. Supply risk is mitigated by qualified, diversified suppliers and appropriate stock; compliance risk is mitigated by robust GMP systems, trained staff, and rigorous quality control; and competitive risk is mitigated by product differentiation, regulated-market access, and efficiency. A manufacturer that treats sourcing, compliance, and market access as core priorities is far better placed to sustain the returns the model promises.
Licenses and Approvals for Pharmaceutical Manufacturing Plant in India
The approvals for this business are central and demanding, because medicines are strictly regulated for safety and quality. Manufacturers planning to establish a Pharmaceutical Manufacturing Plant in India generally need to obtain the following before commencing operations, and drug and GMP approvals are especially important:
- Drug Manufacturing Licence: Manufacturing licence from the State Drug Controller and CDSCO oversight for producing medicines.
- GMP Certification: Good Manufacturing Practice certification, including WHO-GMP for regulated export markets.
- Factory Licence: Factory establishment and industrial operation approval under the Factories Act.
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board (CTE and CTO).
- Product & Export Approvals: Product registrations and market-specific approvals for domestic sale and export.
- Business & Tax Registration: Company incorporation, GST registration, and Udyam registration.
- Fire Safety & Labour Registrations: Fire NOC, and employee welfare registrations such as EPF and ESI.
For a pharmaceutical plant, the drug manufacturing licence and GMP certification are the critical items and should be pursued early, in parallel with facility construction, because production cannot begin without them and export markets demand documented compliance. Engaging a consultant familiar with pharmaceutical regulations is usually worth the cost, since approval gaps can delay a completed plant. Sequencing approvals well, alongside supplier qualification, can shave months off the project timeline.
Note: The exact approvals, registrations, licences, and certification requirements may vary depending on factors such as plant location, dosage forms, target markets, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Pharmaceutical Manufacturing Industry
A few structural trends give useful context for investors considering entry into this industry:
- Policy support and localization: Production-linked incentives and bulk-drug schemes continue to support domestic manufacturing and reduce dependence on imported active ingredients.
- Quality and compliance focus: Rising global scrutiny of quality is pushing Indian manufacturers toward stronger GMP systems and higher-standard facilities, which favours well-built plants.
- Specialty and biosimilar growth: Growing demand for complex generics, specialty drugs, and biosimilars is opening higher-value opportunities beyond basic formulations.
The common thread is a maturing, quality-focused industry backed by strong policy and global demand. For a new entrant, the implication is clear: the window to establish compliant capacity and secure approvals and markets is open, and those who build quality, compliance, and higher-value capability into their model from the start will be best placed as standards and demand rise through the decade.
How a Pharmaceutical Manufacturing Project Report and DPR Helps Investors
A comprehensive project report and DPR provides a structured roadmap for establishing the facility by evaluating every aspect of the venture, from market demand and dosage forms to machinery selection, cleanroom design, and economics. It helps investors determine the optimal product mix and capacity, estimate capital expenditure (CapEx) and operating expenditure (OpEx), assess profitability, and identify potential risks before implementation.
The report also brings together a detailed Pharmaceutical Manufacturing Financial Model with revenue forecasts, production costs, cash flow analysis, break-even assessment, return on investment (ROI), and payback period calculations. These insights enable investors, lenders, and stakeholders to make informed decisions and evaluate the long-term viability of the project. Many investors engage a Pharmaceutical Manufacturing Plant Business Consultant in India or a Pharmaceutical Manufacturing Plant Project Consultant to prepare and validate these documents.
For a pharmaceutical project specifically, a strong DPR also clarifies the dosage-form and compliance strategy, the sourcing plan, and the regulatory and approval pathway, which are the factors most likely to determine success. By modelling utilisation against realistic demand and testing margins against active-ingredient price swings, the report turns a demanding but high-value opportunity into an executable plan that lenders and partners can trust.
Frequently Asked Questions
How to start a pharmaceutical manufacturing plant in India?
Begin by choosing your dosage forms and capacity, then prepare a feasibility study and DPR, secure land in a pharma cluster, build a GMP-compliant facility with cleanrooms and a QC lab, arrange machinery and qualified suppliers, and obtain the drug manufacturing licence and GMP certification. A detailed project report maps each step for your target setup.
What is the Pharmaceutical Manufacturing Plant Setup Cost in India?
It typically ranges from INR 25 crore to INR 250 crore, while the wider Pharmaceutical Manufacturing Plant Cost and Investment depends on dosage forms, capacity, and compliance level. Cleanrooms, machinery, and utilities are the largest parts of CapEx.
What is the pharmaceutical manufacturing process flow?
For solid dosage forms the flow runs from dispensing through granulation, drying, blending, compression or capsule filling, coating, in-process and finished-product quality control, packaging, labelling, and dispatch. Liquid products follow a parallel flow of mixing, filtration, filling, and packaging under the same controls.
What machinery is required for a pharmaceutical manufacturing plant?
The Pharmaceutical Manufacturing Machinery and Equipment includes a dispensing booth, rapid mixer granulator, fluid bed dryer, blender, compression machine, capsule filling machine, coating machine, liquid mixing and filling line, blister or strip packing, and quality-control laboratory instruments such as HPLC and dissolution testers.
What raw materials are required for pharmaceutical manufacturing?
The Raw Materials Required for Pharmaceutical Manufacturing are chiefly active pharmaceutical ingredients and excipients, which together dominate cost, along with compliant packaging materials, solvents and process aids, and quality-control consumables.
What is the Pharmaceutical Manufacturing Plant ROI and Profitability in India?
It is strong, with a typical 12 to 22% net profit margin and a 16 to 26% IRR, and a 4 to 6 year payback at healthy utilization. Returns improve with regulated-market access, higher-value and specialty products, efficient sourcing, and strong quality systems, though margins track active-ingredient prices.
What licenses and approvals are needed for a pharmaceutical manufacturing unit setup in India?
The Licenses and Approvals for Pharmaceutical Manufacturing Plant operations include a drug manufacturing licence with CDSCO oversight, GMP and WHO-GMP certification, a Factory Licence, State Pollution Control Board consents, product and export approvals, a Fire NOC, and GST, Udyam, and labour registrations.
How do I get a feasibility study or DPR for a pharmaceutical plant?
A Pharmaceutical Manufacturing Plant Feasibility Study and DPR covers the full plant setup and financials. Many investors engage a Pharmaceutical Manufacturing Plant Business Consultant in India or a Pharmaceutical Manufacturing Plant Project Consultant to prepare and validate it.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

The Dental 3D Printing Market is attracting renewed investor attention because the technology has moved from a promising adjunct to a default production method inside dental laboratories and clinics.
Vitamin water is a functional, non-carbonated beverage that is created by the fortification of purified water with a combination of vitamins, minerals, and sometimes electrolytes, along with natural or artificial flavors and sweeteners. It is placed in a category between bottled water and carbonated soft drinks, providing hydration with a functional twist.
Vitamin B12, or cobalamin, is a water-soluble vitamin that contains the metal cobalt and is a micronutrient required by the human body. It acts as a coenzyme in the synthesis of DNA, the production of red blood cells, and the functioning of the nervous system.
Japan's dietary supplements industry has become one of the most advanced and innovation-led industries in the world. It is at the nexus of science, culture, and consumer health awareness.
A syringe is a medical instrument that is used to inject fluids into the body or to withdraw fluids from the body. A syringe usually has a cylindrical body, a plunger that moves inside the body to generate pressure or suction, and a nozzle to which a needle can be attached.
Cosmetic surgery in Australia today has evolved into a significant element of the greater beauty and wellness economy. Changing cultural attitudes, advances in medical aesthetics, and the rise of social media over the last ten years have reconstituted the ways in which cosmetic surgery is perceived and undertaken by Australians.
The contact lenses market represents a dynamic segment of the global vision care industry, characterized by continuous innovation and expanding demographic demand.
Brazil's diagnostic imaging equipment market stands at a pivotal moment as Latin America's largest and most dynamic healthcare arena. With substantial investments in hospital modernization, regulatory reforms, and artificial intelligence adoption, the market is transforming rapidly. As providers transition from analog to AI-ready platforms, Brazil emerges as a critical destination for medical device manufacturers seeking growth through the next decade.
The Indian healthcare space has indeed been changing. Telemedicine has emerged as one of the most important drivers of this change. Driving this transformation is the increased adoption of digital tools, growing patient awareness, and the pressing need to make healthcare more accessible across diverse geographies.
The Australia medical aesthetics industry size reached USD 396.4 Million in 2025. Looking forward, the market is expected to reach USD 784.8 Million by 2034, exhibiting a growth rate (CAGR) of 7.89% during 2026-2034. Over the last ten years, the medical aesthetic industry in Australia has transformed from a niche beauty service into a mainstream part of healthcare and wellness.
A rapid diagnostic test (RDT) kit is a medical device designed to quickly detect specific biomarkers, antigens, antibodies, or nucleic acids linked to diseases—typically within minutes and without the need for sophisticated laboratory equipment. These kits often use lateral flow assays, immunochromatographic strips, or rapid molecular testing methods to deliver fast and reliable results.
The Philippines pharmaceutical industry stands as one of Southeast Asia's most dynamic and rapidly expanding healthcare markets in the ASEAN region. With a market valuation reaching USD 3.36 Billion in 2025, the sector demonstrates resilience and tremendous growth potential.
Pharmaceuticals are medical products, substances, or formulations involved in the development, manufacture, and regulation for the prevention, diagnosis, treatment, and management of diseases in humans as well as animals.
The Australia aged care industry stands at a pivotal juncture as the nation grapples with demographic shifts that are reshaping the landscape of elderly care services. With an aging population that continues to expand, Australia faces both unprecedented challenges and remarkable opportunities in delivering quality care to its senior citizens.
The Indian vaccines industry holds an unparalleled position globally, often celebrated as the pharmacy of the world due and its massive production scale and capabilities. It reached INR 113.7 Billion in 2024 according to IMARC Group and it is projected to grow at a CAGR of 8.8% from 2025-2033.
The medical imaging market has reached a transformational phase, driven both by rapid technological advancements and growing demands for precision-driven diagnostics. As health systems worldwide come under increasing pressure to improve patient outcomes while minimizing procedural risks and optimizing clinical workflows, medical imaging has become one of the most important cornerstones of modern medicine.
India’s medical devices industry is on a sustained growth trajectory driven by expanding hospital infrastructure, rising chronic disease burden, stronger local manufacturing supported by government incentives, and a rapidly growing shift toward portable and home care devices.
Pectin represents a naturally occurring polysaccharide mainly extracted from cell walls of fruits (mainly from citrus peel and apple pomace). It is a soluble dietary fiber and a hydrocolloid with gelling, thickening, and stabilizing properties. It is mostly composed of galacturonic acid units.
Paracetamol, also referred to as acetaminophen, is an analgesic and antipyretic compound that is commonly used worldwide for the treatment of mild to moderate pain and the management of fever. The mechanism of action occurs mainly in the central nervous system, where it inhibits the mechanisms that regulate pain and body temperature, but lacks anti-inflammatory properties.
The Australia wellness tourism industry has emerged as a critical segment of the country’s broader travel and hospitality sector. It reflects a growing global emphasis on health, self-care, and holistic well-being, capturing the attention of travelers seeking experiences that combine relaxation, rejuvenation, and personal growth.
The Brazil cardiovascular devices market represents a crucial segment in the country’s healthcare ecosystem, addressing one of the leading causes of morbidity and mortality: cardiovascular diseases. Conditions such as heart attacks, stroke, arrhythmias, and heart failure require ongoing medical intervention and advanced heart disease treatment solutions. With the rising prevalence of cardiovascular disorders, demand for comprehensive cardiac care equipment and innovative treatment modalities is increasing.
India's Ayurvedic products market is experiencing remarkable transformation as consumers increasingly prioritize holistic wellness and natural remedies over conventional alternatives. The convergence of traditional healing wisdom with modern consumer preferences has created a dynamic landscape where herbal medicines, chemical-free personal care products, and immunity-boosting supplements are becoming household staples.
Nicotine pouches are small, smokeless oral delivery products of nicotine, free from tobacco, designed to allow for controlled release of the active principle without burning, vaporizing, or use of traditional tobacco leaves. It consists of a small pouch that contains a matrix made basically from plant fibers, flavorings, pH adjusters, and stabilizers impregnated with nicotine, encased in a permeable material permitting the gradual absorption of the product via the oral mucosa.
The pharmaceutical industry in Japan is among the most advanced globally, recognized for combining innovation, high-quality standards, and patient-centered care. Its extensive value chain includes drug discovery, clinical trials, manufacturing, distribution, marketing, and post-market surveillance. Serving both domestic and international markets, Japanese pharmaceutical companies are respected for regulatory compliance, safety, and reliability, establishing them as trusted global collaborators in drug development.
The pharmaceutical industry in Japan is among the most advanced globally, recognized for combining innovation, high-quality standards, and patient-centered care. Its extensive value chain includes drug discovery, clinical trials, manufacturing, distribution, marketing, and post-market surveillance. Serving both domestic and international markets, Japanese pharmaceutical companies are respected for regulatory compliance, safety, and reliability, establishing them as trusted global collaborators in drug development.
The global healthcare IT industry is on a remarkable upswing, fueled by the surge in preventive care, digital health platforms, and smarter patient management systems. According to IMARC Group, the market hit USD 363.15 Billion in 2024, a clear sign of worldwide adoption. An aging population, the growing comfort with remote care, and the push toward personalized medicine are all speeding this momentum.
The global endoscopy devices market is on a sharp growth path, fueled by the shift toward minimally invasive procedures, the need for early diagnosis, and cutting-edge imaging technologies. IMARC Group reported the market hit USD 50.01 Billion in 2024, underscoring its worldwide acceptance.
The global business-to-business (B2B) payments landscape is experiencing a fundamental transformation that is reshaping how enterprises conduct financial transactions across borders and industries. The market, valued at approximately 1,189.6 Billion in 2024, is projecting remarkable growth with expectations to reach USD 2,189.0 Billion by 2033, exhibiting a CAGR of 7% from 2025-2033. This exponential expansion is signaling a paradigm shift in commercial finance, driven by technological innovation, changing business expectations, and the urgent need for more efficient payment infrastructures.
The smart medical devices market is entering a decade defined by connected care, real-time diagnostics, and patient empowerment. Valued at USD 45.9 Billion in 2024, the market is projected to reach USD 82 Billion by 2033, expanding at a compound annual growth rate (CAGR) of 6.33% between 2025 and 2033 by IMARC Group. This steady rise reflects growing confidence in data-driven healthcare systems, integration of IoT in medical environments, and the increasing role of artificial intelligence in clinical decision-making.
Active Pharmaceutical Ingredients (APIs) are the bioactive molecules of any drug used in pharmaceuticals, which cause the desired therapeutic action in the body of a human being. APIs are the central core of all drugs, chemical or biological and are responsible for the efficacy, strength, and safety of the drug. APIs are synthesized by various complex chemical synthesis, fermentation, biotechnological, or extraction processes based on the type of drug.
A bio medical incinerator is a high-temperature combustion system specialized for biomedical waste disposal by hospitals, clinics, laboratories, and research institutions. Biomedical waste usually consists of infectious waste, pathological waste, sharps, pharmaceuticals, and contaminated disposables that are very hazardous to human health and the environment if not treated.
Obesity, once viewed primarily as a lifestyle choice, is now widely recognized as a complex and chronic disease characterized by excessive body fat accumulation. Its global prevalence is escalating at an alarming rate posing a significant and growing challenge to public health systems worldwide.
Gonorrhea, a sexually transmitted infection caused by the bacterium Neisseria gonorrhoeae, is a major public health issue globally. Reports show that over one million new cases of curable STIs are contracted every day by individuals aged 15 to 49 years, with the majority being asymptomatic.
The 7 major allergic conjunctivitis markets reached a value of USD 2.1 Billion in 2024. Looking forward, IMARC Group expects the 7MM to reach USD 2.9 Billion by 2035, exhibiting a growth rate (CAGR) of 3.00% during 2025-2035.
The healthcare sector is changing rapidly because of the growing demand for better ways to manage chronic diseases. As we move toward 2025 and beyond, digital tools are playing an important role in dealing with conditions like diabetes, heart disease, cancer, and respiratory problems.
The global multivitamin gummies market consists of chewable dietary supplements that are charged with key vitamins and minerals aimed at maintaining general health and wellness. The gummies present a handy, enjoyable, and easy-to-swallow option to classic pills or tablets, hence are predominantly preferred by children and adults who do not like taking pills.
India's pharmaceutical sector is evolving rapidly, supported by the integration of artificial intelligence (AI) across the value chain. As of 2023, India ranked as the third-largest pharmaceutical producer by volume, accounting for 20% of global generic drug exports.
As Lung Cancer Awareness continues to build global momentum in 2025, Artificial Intelligence (AI) is proving to be a transformative force—not only in clinical diagnostics but also in public education and preventive health efforts. Given that lung cancer remains one of the world’s deadliest cancers, accounting for over 1.8 million deaths each year and a five-year survival rate of just 28.4%, the integration of AI marks a critical turning point.
Observed on May 19, Hepatitis Testing Day 2025 emphasizes the need to "Test. Treat. Eliminate," highlighting the gap in diagnosing hepatitis B and C, which cause over 1.3 million deaths annually. Hepatitis remains a major global health threat, on par with HIV, tuberculosis, and malaria. The growing viral hepatitis market <Viral Hepatitis Market Size | Share, Trends - 2034 > reflects rising demand for better diagnostics, treatments, and integrated care. The WHO warns that without faster testing and treatment, the goal of eliminating hepatitis by 2030 may not be achieved, with disparities in diagnostics, particularly in low- and middle-income countries, hindering progress.
Observed on May 8, World Ovarian Cancer Day 2025 carries the theme “No Woman Left Behind,” reinforcing the urgent need to close the gaps in access, diagnosis, treatment, and care across all regions and socioeconomic groups. Ovarian cancer remains one of the deadliest gynecological cancers, often detected too late due to vague symptoms and limited screening tools. The World Ovarian Cancer Coalition projects a 55% rise in annual cases and nearly 70% more deaths by 2050, with the heaviest burden falling on low- and middle-income countries. Equitable access to early diagnostics, genetic testing, and targeted therapies is critical.
In clinics around the world, a concerning pattern is becoming increasingly evident: a growing number of patients are experiencing wheezing, breathlessness, and persistent coughing. This surge reflects a broader global trend. According to the World Health Organization (WHO), more than 260 million people are currently living with asthma, making it one of the most widespread and persistent chronic respiratory conditions globally.
Observed on April 25, World Malaria Day 2025 carries the theme “Accelerating Equity in Malaria Prevention and Cure,” underscoring the urgent need to reach communities still lacking access to life-saving vaccines and diagnostics. While global malaria death rates have seen modest declines, the disease continues to claim the life of one child every minute, highlighting the critical need for swift, equity-driven action
Sulfamethoxazole is a common synthetic antibacterial that is a member of the sulfonamide class of antibiotics. This substance plays a very significant role in modern medicine due to the amazing capabilities offered by the substance for curing infections and bacterial diseases. Trimethoprim and sulfamethoxazole are frequently used together to create the well-known antibiotic co-trimoxazole, which is well-known for its potency against a variety of bacterial infections. It works by preventing the manufacture of folic acid, which is necessary for the growth of bacteria. Sulfamethoxazole is an essential part of modern antibiotic therapy since it has been used to treat lung infections, urinary tract infections, and other common bacterial illnesses.
Healthcare consumables are necessary medical supplies used for patient treatment, diagnostics, and cleanliness in clinics, hospitals, and home care settings. These consist of supplies such as surgical masks, bandages, gloves, syringes, catheters, and disinfectants. Usually, they are disposable or single use to preserve sterility and stop infections. Healthcare consumables are an essential component of the global healthcare ecosystem and are in high demand due to expanding healthcare needs, an increase in operations, infection control measures, and technological improvements.
Catheters are flexible, tubular medical devices designed to access various body cavities, organs, or blood vessels for diagnostic or therapeutic purposes. They can be broadly classified into types based on their application, including urinary catheters, cardiac catheters, and intravenous (IV) catheters. Catheters are commonly used in diverse healthcare settings for managing chronic conditions, enabling fluid drainage, delivering medications, or facilitating minimally invasive surgeries.
Bioinformatics involves applying computational techniques and tools to study and understand biological systems at the molecular level. It is a field of study that combines mathematics, biology, computer science, and statistics to research genomic data and biological networks. The goal is to interpret information from large biological data sets, such as DNA sequences, protein structures, gene expressions, and other high-throughput experimental data. This field provides various products and services, such as knowledge management tools, bioinformatics platforms, and services.
A non-animal model refers to an experimental system or method used in scientific research or testing that does not involve the use of animals. These models are developed to simulate biological processes, test hypotheses, or study diseases without the need for live animals. The aim is often to reduce the reliance on animal testing, which has ethical implications and raises concerns about animal welfare.
Cell therapy involves the transplantation and manipulation of living cells to replace and repair damaged tissue. Its primary branches include stem cell therapy and non-stem cell therapy. Stem cell therapy utilizes stem cells to repair, replace, or rejuvenate damaged or diseased cells and tissues as they possess the ability to differentiate into various specialized cell types, making them valuable for regenerative medicine. Non-stem cell-based therapies typically involve somatic cells isolated from the human body. These cells are propagated, expanded, selected, and then administered to patients for curative, preventive, or diagnostic purposes. On the other hand, gene therapy seeks to treat diseases by introducing, replacing, or inactivating genes within cells.