Automotive Forging Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
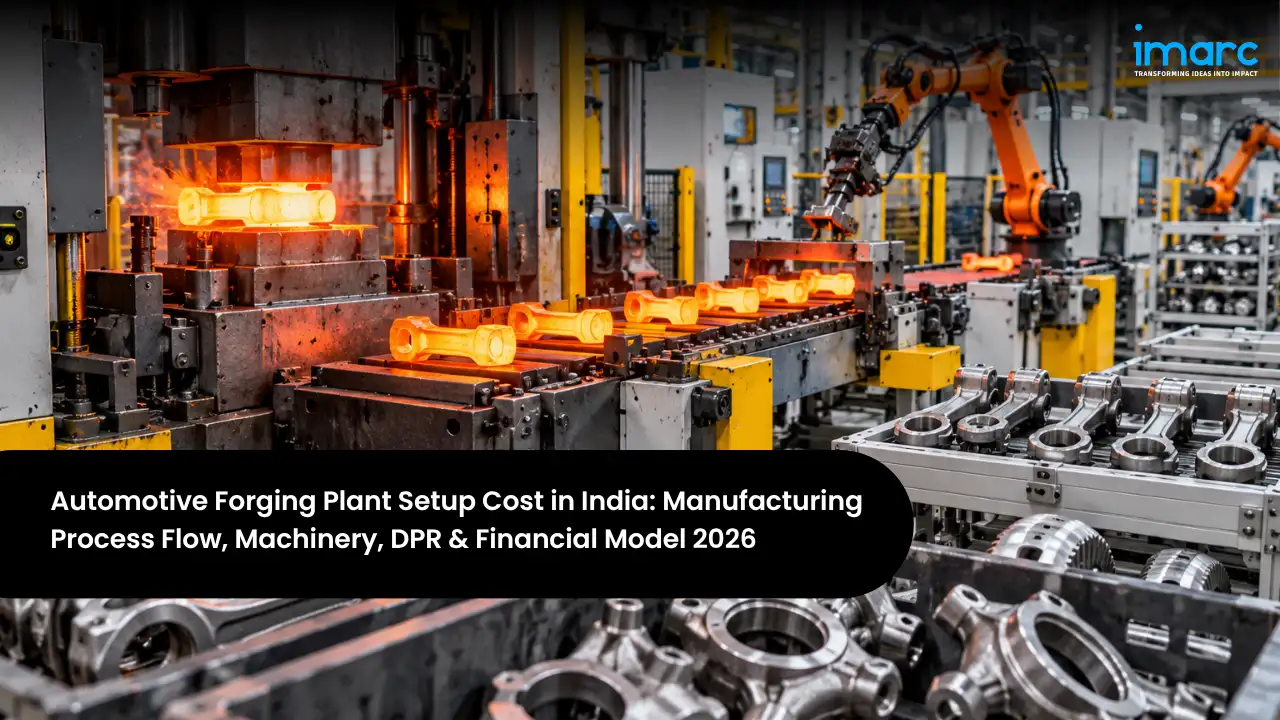
Every vehicle on the road depends on forged parts. Crankshafts, connecting rods, steering knuckles, axle beams, gears, and hubs are forged because the process gives steel a continuous grain flow and the strength to survive millions of load cycles. India has become the world's second-largest producer of forgings, supplying domestic vehicle makers and exporting to Europe, North America, and Asia. For investors, an Automotive Forging Plant Setup in India offers entry into a strategic, export-capable engineering industry, though one that demands heavy equipment, skilled die design, and certified quality systems.
Investment depends on capacity, press sizes, the range of components produced, and whether heat treatment and machining are carried out in-house. For a closed-die forging plant of roughly 5,000 to 30,000 tonnes a year, the Automotive Forging Plant Cost ranges from about INR 50 crore to INR 500 crore. Steel billets make up the largest share of operating cost, followed by energy for heating and heat treatment, so material sourcing, yield, and energy efficiency are the decisions that shape profitability. At healthy utilisation, a well-run plant can deliver a net profit margin of 10 to 15% and an IRR of 15 to 22%, with payback typically within 4 to 6 years.
This guide is written for investors trying to understand how to start an Automotive Forging plant in India. It covers the main component families and markets, the demand outlook, the production flow, machinery and raw materials, site and infrastructure planning, a detailed cost and financial breakdown, the approvals and certifications involved, and how a DPR turns all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| India Forging Market (2026) | USD 6.12 Billion, 7.10% CAGR to 2034 |
| Annual Forging Production | About 2.9 Million Tonnes (capacity 4.8 Million Tonnes) |
| Global Position | World’s second-largest producer of forgings |
| Export Share | About 30% of production exported |
| Indicative Total Investment | INR 50–500 Crore (5,000–30,000 TPA) |
| Typical Payback Period | 4–6 Years |
The snapshot shows a large, globally competitive industry with meaningful spare capacity and a strong export orientation. Closed-die forging, which accounts for most automotive parts, dominates the market, and demand continues to grow with vehicle production and global sourcing shifts toward India. The wide investment range reflects a genuine choice between a focused plant with a few mid-sized presses serving local customers and a large facility with heavy presses, automated lines, and integrated machining for export programmes. The sections below work through that choice.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Engine, transmission, chassis, suspension, and driveline forgings |
| Total Project Investment | INR 50 – 500 Crore (5,000–30,000 TPA) |
| Payback Period | 4 – 6 Years |
| Net Profit Margin | 10 – 15% |
| IRR | 15 – 22% |
| Preferred States | Maharashtra, Punjab, Haryana, Tamil Nadu, Jharkhand, Gujarat |
| Key Approvals | Factory License, SPCB consents, IATF 16949, customer PPAP approvals, Fire NOC |
| Key Requirement | Right press capacity, die design capability, and OEM approvals |
These ranges give a realistic frame for early planning, but actual returns depend on steel prices, forging yield, press utilisation, die life, and the time needed to win customer approvals. A site-specific Automotive Forging Feasibility Report narrows each of these assumptions to your chosen components, press line-up, location, and capacity.
Table of Contents
- What is Automotive Forging?
- Why is Automotive Forging Growing in India?
- Automotive Forging Process Flow
- Raw Materials Required for Automotive Forging
- Location, Land & Infrastructure
- Automotive Forging Machinery and Equipment for a Forging Plant
- Automotive Forging Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Automotive Forging in India
- Recent Developments in the India Automotive Forging Industry
- How an Automotive Forging Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Automotive Forging?
Automotive forging is the shaping of heated metal, usually steel and increasingly aluminium, into strong, near-net-shape components using compressive force from presses or hammers. In closed-die forging, a heated billet is plastically deformed between precision dies using a press, hammer or other forging equipment until the material fills the die cavity, after which excess material is trimmed away. The process aligns the metal's grain flow with the part's shape, giving forged components superior strength, toughness, and fatigue resistance compared with castings or machined bar stock.
Commercially, forging sits at the heart of the auto component supply chain. A well-run Automotive Forging Plant can supply vehicle makers and their tier-one suppliers with raw or machined forgings for passenger vehicles, commercial vehicles, two-wheelers, and tractors, and can serve export customers seeking reliable, cost-competitive suppliers. Long-term component programmes with approved customers provide steady volumes, while engineering capability and consistent quality protect the relationship.
- Engine Components: Crankshafts, connecting rods, and camshafts for internal combustion engines.
- Transmission Parts: Gear blanks, shafts, flanges, and synchroniser parts.
- Chassis & Suspension: Steering knuckles, control arms, axle beams, and spindles.
- Driveline & Hub Parts: Yokes, constant-velocity joint parts, wheel hubs, and flanges.
The Main Automotive Forging Product Families
Choosing which component families to produce is the most important commercial decision, because it determines press sizes, die technology, heat treatment, and target customers:
| Product Family | Description | Key Property | Primary Demand |
|---|---|---|---|
| Engine Forgings | Crankshafts and connecting rods | High fatigue strength | PV, CV, and two-wheeler engines |
| Transmission Forgings | Gear blanks, shafts, flanges | Precision and toughness | Gearboxes and axles |
| Chassis & Suspension Forgings | Knuckles, arms, axle beams | Safety-critical strength | All vehicle segments |
| Driveline Forgings | Yokes, CV joint parts, hubs | Wear resistance | PV and CV drivelines |
| Aluminium Forgings | Lightweight suspension and EV parts | Low weight, high strength | Premium and electric vehicles |
Product choice shapes the whole plant. Heavy crankshafts and front axle beams need large presses and long heating lines, while smaller gear blanks and flanges suit high-speed presses with automated handling. Aluminium forgings require separate heating and heat treatment practices. Many new entrants begin with transmission and driveline forgings, which have broad demand across vehicle types and are less exposed to the long-term shift away from combustion engines, then add chassis and aluminium parts as customer approvals grow.
Why is Automotive Forging Growing in India?
Key Growth Drivers in the Indian Market
Demand is supported by vehicle production growth at home and India's rising role in global component supply:
- Rising vehicle production: Growth in passenger vehicles, commercial vehicles, two-wheelers, and tractors increases demand for forged components.
- Global sourcing shift: Vehicle makers and tier-one suppliers in Europe and North America are diversifying supply toward India.
- Lightweighting: Automakers are seeking lighter, stronger parts, driving demand for optimised steel and aluminium forgings.
- Electric vehicles: EVs still need chassis, suspension, and driveline forgings, and new e-axle and motor components create fresh opportunities.
- Non-automotive diversification: Railways, defense, construction equipment, and energy offer additional outlets for forging capacity.
India-Specific Market Opportunity
| Segment | India Market Context | Manufacturing Role |
|---|---|---|
| Domestic OEMs | Growing vehicle production | Raw and machined forgings |
| Tier-One Suppliers | Expanding component programmes | Contract forging supply |
| Export Customers | About 30% of output exported | Certified, cost-competitive supply |
| EV Programmes | New platforms and e-axles | Lightweight and precision forgings |
| Non-Auto Sectors | Railways, defense, off-highway | Diversified volumes |
The strongest opportunity lies in combining steady domestic OEM and tier-one business with export programmes, supported by in-house heat treatment and machining that allow the plant to deliver finished, ready-to-fit components. Producers who plan early for electrification by building capability in chassis, driveline, and aluminium forgings will be better protected as engine-related demand gradually changes.
Automotive Forging Process Flow
Understanding the flow helps you plan presses, furnaces, and where cost and quality are decided. Automotive forging is a hot working process followed by heat treatment, finishing, and inspection, with every step controlled to ensure that each part meets strict dimensional and metallurgical requirements. Die design, heating accuracy, and heat treatment together determine both yield and part performance.
The Automotive Forging Process Flow
The sequence below reflects a typical closed-die steel forging line. Plants offering machined forgings add CNC machining cells after heat treatment and inspection.
| Unit Operation | Key Activity |
|---|---|
| Billet Receipt & Inspection | Steel grade, chemistry, and defects checked |
| Cutting | Billets sheared or sawn to precise weights |
| Induction Heating | Billets heated uniformly to forging temperature |
| Pre-Forming | Material distributed by rolling or busting |
| Closed-Die Forging | Part formed in dies on press or hammer |
| Trimming & Piercing | Flash removed and holes punched |
| Heat Treatment | Normalising or hardening and tempering |
| Shot Blasting | Scale removed and surface cleaned |
| Inspection & Testing | Crack detection, dimensions, and hardness |
| Machining, Packing & Dispatch | Optional machining, protection, and shipment |
Two factors decide profitability across this flow. The first is material yield: steel is the largest cost, and flash, scale, and rejected parts all waste it, so optimised billet weights, well-designed dies, and simulation-led process development pay back quickly. The second is die life and uptime, because forging dies are expensive and presses are the most valuable assets in the plant; good die design, controlled lubrication, and quick die changes keep output high and cost per part low.
Raw Materials Required for Automotive Forging
The main input is alloy and micro-alloyed steel in the form of billets or bars, supported by die steel for tooling, aluminium billets for lightweight parts, forging lubricants, shot blasting media, and packaging. Because steel dominates cost and its quality directly affects forging performance, reliable supply of certified grades from qualified mills is central to project planning.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Alloy & Micro-Alloyed Steel Billets | Primary forging material | Domestic special steel mills | 60–70% |
| Aluminium Billets (optional) | Lightweight forgings | Domestic and imported | 0–8% |
| Die Steel Blocks | Forging dies | Domestic and imported | 3–5% |
| Forging Lubricants | Die lubrication and release | Domestic and imported | 1–2% |
| Shot Media & Consumables | Cleaning and finishing | Domestic suppliers | 1–2% |
| Packaging & Rust Preventives | Protection during transit | Domestic suppliers | 1–2% |
India has a strong base of special and alloy steel mills, which helps keep supply reliable and lead times manageable. Because steel prices follow global commodity cycles, most forging contracts include raw material price adjustment clauses, and securing these terms with customers is one of the most important steps in protecting margins. Die steel quality also matters greatly, since longer die life directly reduces cost per part.
Location, Land & Infrastructure
Site selection for a forging plant is shaped by proximity to vehicle makers and tier-one customers, access to steel suppliers, availability of skilled forging and die-making talent, reliable power, and logistics to export ports. Forging also generates noise and vibration, so plants are best located in designated industrial areas.
Choosing the Best Location for Automotive Forging Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Maharashtra (Pune & Chakan) | India’s leading forging and auto cluster | Customers, talent, and suppliers |
| Punjab (Ludhiana) | Strong forging base for CVs and tractors | Skilled workforce and cost advantage |
| Haryana (Gurugram & Faridabad) | Large auto component ecosystem | Proximity to northern OEMs |
| Tamil Nadu (Chennai & Coimbatore) | Major auto manufacturing hub | OEM demand and port access |
| Jharkhand (Jamshedpur) | Steel and CV manufacturing base | Steel supply and heavy forging |
| Gujarat (Rajkot & Ahmedabad) | Engineering and forging cluster | Ports and industrial incentives |
Pune and the wider Maharashtra cluster remain the natural first choice, with the country's deepest pool of forging expertise, die makers, and auto customers. Ludhiana and Faridabad serve northern commercial vehicle and tractor makers, Chennai offers strong OEM demand and export access, and Jamshedpur combines steel supply with heavy forging experience. The final choice should balance customer proximity, steel logistics, skilled labour, power cost, and state incentives.
Quality Systems, Safety and Environmental Controls
Automotive forgings are often safety-critical, so customers require certified quality systems, full traceability from steel heat number to finished part, and rigorous testing. That means IATF 16949 certification, process validation through PPAP, spectrometer checks on incoming steel, controlled heating and heat treatment, magnetic particle crack detection, hardness and microstructure testing, and CMM inspection. On the plant side, noise and vibration control, furnace emissions management, safe handling of hot parts, and worker safety systems are essential. An experienced Automotive Forging Consultant in India can help plan the press line-up, die shop, quality system, and environmental controls so the plant can win customer approvals quickly.
Infrastructure Requirements (Mid-Sized Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 5 – 20 acres | Space for billet yard and expansion |
| Forge Shop | Heavy foundations for presses and hammers | Vibration isolation required |
| Power Requirement | 3 – 15 MW | Induction heating is a major load |
| Heat Treatment Section | Continuous and batch furnaces | Separate from forging area |
| Die Shop | CNC machining and EDM for dies | Core to die life and quality |
| Quality Laboratory | Metallurgical and dimensional testing | Supports IATF and PPAP |
| Cranes & Handling | EOT cranes and manipulators | Safe movement of billets and dies |
Heavy press foundations, high-capacity power, and an in-house die shop are the defining infrastructure needs. Foundations and power must be planned for the largest press the plant may eventually install, since adding them later is costly. A well-equipped die shop shortens development time for new parts and reduces dependence on outside tool rooms, which is often decisive in winning new programmes.
Automotive Forging Machinery and Equipment for a Forging Plant
The equipment set covers billet preparation, heating, forging, trimming, heat treatment, finishing, machining, die making, and inspection. Press and hammer selection is the central investment decision, because tonnage and type determine the size and complexity of parts the plant can produce. The main items are summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Billet Shearing / Sawing Machines | Cut billets to weight | Accurate, high-speed cutting |
| Induction Billet Heaters | Heat billets for forging | Temperature-controlled, energy-efficient |
| Roll Forging / Reducer Rolls | Pre-form billets | Improves material distribution |
| Mechanical / Hot Forging Presses | Form parts in closed dies | Typically 1,000 to 6,300 tonnes |
| Forging Hammers & Screw Presses | Form complex or large parts | Counterblow or drop hammers |
| Trimming & Piercing Presses | Remove flash and punch holes | Integrated with forging line |
| Heat Treatment Furnaces | Normalise, harden, and temper | Continuous and batch types |
| Shot Blasting Machines | Clean and finish surfaces | Hanger or tumble type |
| Die Shop Equipment | Make and repair dies | CNC machining centres and EDM |
| CNC Machining Cells (optional) | Deliver machined forgings | Turning and milling centres |
| Inspection Equipment | Test and verify parts | MPI crack detection, CMM, spectrometer |
Machinery should follow the product plan and customer requirements. A plant focused on smaller transmission parts can use high-speed mechanical presses with automated transfer, while heavy crankshafts and axle beams need large presses or hammers with long heating lines. Automation, including robotic handling between heating, forging, and trimming, improves consistency and safety, and simulation software for die design shortens development time for new parts.
Automotive Forging Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a mid-sized automotive forging facility in India. The final Automotive Forging Investment Cost for your project will depend on press tonnage and number, heat treatment and machining integration, automation, location, and target capacity.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 55–65% | Presses, heaters, furnaces, and machining |
| Land, Buildings & Foundations | 12–18% | Forge shop, heavy foundations, and warehouse |
| Power & Utilities | 6–10% | Substation, compressed air, and cooling |
| Die Shop & Tooling | 4–7% | Die-making equipment and initial dies |
| Quality Lab & Metrology | 2–4% | Metallurgical and dimensional testing |
| Pre-operative & Contingency | 4–6% | Engineering, DPR, approvals, buffer |
| Working Capital | 8–12% | Steel inventory and customer receivables |
Presses and heating equipment dominate the capital budget, and choosing the right tonnage and configuration is the most important investment decision. Heavy foundations and power infrastructure also represent a meaningful share and should be sized for future growth. A detailed Automotive Forging Business Plan should model the press line-up, die development costs, and customer approval timelines together, since new plants often take a year or more to reach stable volumes with approved parts.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials (steel billets, die steel) | 70–80% | Steel dominates; often price-linked |
| Power & Fuel | 10–15% | Induction heating and furnaces |
| Labour & Skilled Manpower | 5–8% | Forgers, die makers, and inspectors |
| Die Maintenance & Consumables | 2–4% | Die repair, lubricants, and shot |
| Freight & Packaging | 2–3% | Heavy shipments and export packing |
| Maintenance & Overheads | 2–3% | Press upkeep and administration |
With steel making up the large majority of operating cost, margins depend on securing raw material price pass-through in customer contracts, maximising yield, and keeping energy use per tonne low. A good operating model tracks input weight per part, scrap and rejection rates, energy per tonne, and die cost per piece, and tests how margins respond when steel or power prices change.
Financial Analysis and Profitability
Based on analysis of a mid-sized forging facility, the financial profile is sound, supported by long-term component programmes, export demand, and India's cost competitiveness. The profitability of Automotive Forging business in India improves markedly with high press utilisation, strong yields, raw material price pass-through, in-house machining, and a diversified customer base across vehicle segments and export markets.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 15–25% | Higher for machined and complex forgings |
| Net Profit Margin | 10–15% | After depreciation and Indian corporate taxes |
| Payback Period | 4–6 Years | Includes customer approval period |
| IRR (Internal Rate of Return) | 15–22% | Higher with export programmes |
| Capacity Utilization (stable ops) | 65–85% | Depends on approved part portfolio |
| Break-even Capacity Utilization | 50–60% | High fixed and depreciation costs |
Product mix, customer base, and utilisation decide where a plant lands within these ranges. A plant supplying simple raw forgings to a few domestic customers will sit near the lower end, while one delivering machined, complex, or safety-critical parts to multiple OEMs and export customers can earn noticeably more per tonne. Because presses are expensive, keeping them busy across shifts is essential to returns.
Returns can be strengthened by winning long-term programmes with raw material price adjustment clauses, adding in-house machining to capture more value, diversifying into export, EV, and non-automotive customers, investing in automation and simulation to raise yield, and maintaining a strong die shop that shortens development time. Consistent quality and on-time delivery build the trust that leads to repeat programmes.
Key Risks and Mitigation
The main risks are steel price volatility, cyclical swings in vehicle production, customer concentration, and the long-term shift away from engine components as electric vehicles grow. Price risk is reduced through pass-through clauses; cyclical risk by serving multiple vehicle segments and export markets; concentration risk by diversifying customers; and technology risk by building capability in chassis, driveline, and aluminium forgings. Promoters often work with an Automotive Forging Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for Automotive Forging in India
Approvals for a forging plant combine industrial and environmental registrations with the quality certifications and customer approvals that open the door to automotive business. Promoters setting up an Automotive Forging Plant in India generally need the following:
- Factory License: Registration and plan approval under the Occupational Safety, Health and Working Conditions Code, 2020, with attention to heavy machinery safety.
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, covering furnace emissions, noise, vibration, and wastewater.
- Hazardous Waste Authorisation: Authorisation for used oils, quench media, and other regulated wastes.
- Power Connection Approvals: HT connection and Electrical Inspectorate approval for high-load equipment.
- Quality Certifications: IATF 16949, ISO 14001, and ISO 45001, typically required by vehicle makers and tier-one suppliers.
- Customer Approvals: Part-by-part approval through PPAP and customer audits before series supply.
- Business, Tax, Fire & Labour Registrations: Company incorporation, GST, Udyam, IEC for exports, Fire NOC, and EPF and ESI registrations.
Pollution consent, the factory license, and power approvals are usually on the critical path for construction, while IATF certification and customer PPAP approvals determine when the plant can begin series supply. Planning quality systems and sample development in parallel with installation, and engaging target customers early, can shorten the time from commissioning to revenue considerably.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, component types, target customers, export markets, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Automotive Forging Industry
Several recent developments give useful context for investors considering this market:
- Global standing: India now produces about 2.9 million tonnes of forgings a year from an installed capacity of about 4.8 million tonnes, making it the world’s second-largest producer.
- Export orientation: Around 30% of production is exported, mainly to Europe, North America, and Asia.
- Lightweighting and aluminium: Automakers are increasingly asking for lighter forged parts, driving investment in optimised steel designs and aluminium forging lines.
- Industry 4.0 adoption: Leading forgers are adopting automation, digital simulation, and data-driven process control to improve yield and consistency.
The common thread is an industry moving up the value chain, from raw forgings toward precision, lightweight, and machined components for global customers. New entrants who invest in the right presses, strong die design, certified quality systems, and a diversified customer base will be best placed as India's role in global automotive supply chains grows through the decade.
How an Automotive Forging Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from market demand and product selection to press line-up, heat treatment, layout, certification, and economics. It helps investors decide the right capacity and component mix, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Automotive Forging Financial Model covering revenue by component and customer, input weight and yield assumptions, steel price pass-through, energy and die costs, ramp-up and approval timelines, cash flows, break-even, return on investment, and payback. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint an Automotive Forging Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a forging project, a strong DPR also clarifies the press selection, the die development strategy, the machining make-or-buy decision, and the customer acquisition plan, which together are the factors most likely to decide success. By modelling utilisation against realistic programme wins and testing margins against steel and power price swings, the report turns a capital-intensive opportunity into a plan that lenders and partners can trust.
Frequently Asked Questions
What are the first steps to set up an automotive forging plant in India?
Start by identifying target components, customers, and capacity, then commission a feasibility study and DPR. Next, secure land in an auto cluster with adequate power, select presses and heating equipment, set up a die shop and quality laboratory, obtain the factory license, pollution consent, and power approvals, pursue IATF certification, and begin sample development and PPAP with target customers.
How much does it cost to set up an automotive forging plant in India?
A closed-die forging plant of roughly 5,000 to 30,000 tonnes a year typically needs INR 50 crore to INR 500 crore, depending on press tonnage and number, heat treatment and machining integration, and automation. Presses, heating equipment, and foundations are the largest components.
What are the main steps in automotive forging?
The flow runs from billet receipt and inspection through cutting, induction heating, pre-forming, closed-die forging, trimming and piercing, heat treatment, shot blasting, crack detection and inspection, and optional machining before packing and dispatch.
Which machinery does an automotive forging plant need?
Key equipment includes billet shearing or sawing machines, induction billet heaters, roll forging machines, mechanical or hot forging presses, forging hammers and screw presses, trimming presses, heat treatment furnaces, shot blasting machines, die shop equipment, optional CNC machining cells, and inspection equipment such as MPI, CMMs, and spectrometers.
What raw materials are used in automotive forging?
The main input is alloy and micro-alloyed steel billets, with aluminium billets for lightweight parts, die steel blocks for tooling, forging lubricants, shot blasting media, and rust preventives and packaging.
How profitable is automotive forging in India?
A well-run plant typically earns a 10 to 15% net margin and a 15 to 22% IRR, with payback in 4 to 6 years including the customer approval period. Profitability improves with machined and complex parts, export programmes, raw material pass-through, and high press utilisation, while margins track steel and energy prices.
Which licenses does an automotive forging plant need in India?
Typical approvals include a factory license, State Pollution Control Board consents, hazardous waste authorisation, HT power approvals, IATF 16949 and ISO certifications, customer PPAP approvals, a Fire NOC, and GST, Udyam, IEC, and labour registrations.
How do I get feasibility study or DPR for an automotive forging project?
A detailed feasibility study and DPR covers market demand, component and customer strategy, press selection, plant design, approvals, and full financials. Investors usually engage an Automotive Forging Feasibility Study Consultant with experience in auto component and metal-forming projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Setting up an Automotive Components Manufacturing Plant in India is a high-potential, export-capable venture, powered by the country's large automobile industry, deep supplier base, and growing role as a global sourcing hub for auto parts.
The global automotive lead-acid battery market reached USD 13.89 Billion in 2025 and is projected to reach USD 16.60 Billion by 2034, growing at a CAGR of 1.94% (2026–2034).
Setting up an Electric Scooter Manufacturing Plant in India is a capital-efficient, high-growth venture, driven by the country's rapid shift to electric mobility, supportive EV policies, and surging demand for affordable, clean urban transport. As two-wheelers dominate Indian roads and buyers move from petrol to battery-powered scooter manufacturing, an EV Scooter Manufacturing Plant is one of the most accessible and strategically timed entry points into the electric vehicle economy.
Capital is flowing into the united states used car market because structural affordability pressure, digital retail maturity, and a record-old national vehicle fleet have converged into a genuinely investable thesis.
The Europe Tire Market reached a volume of 458.89 Million Units in 2025 and is projected to reach 565.69 Million Units by 2034, growing at a CAGR of 2.35% (2026–2034).
A strategic analysis of how PLI policies and localization drive global OEM investments. India’s EV battery market hits USD 15,898.31 Million by 2034 (21.7% CAGR).
A tyre is circular in shape and made of a combination of rubber materials that fit perfectly over a circular rim on a wheel, providing traction, load-carrying capabilities, shock absorption, and directional stability. As such, tyres are engineered materials composed of a combination of natural or synthetic materials. They are composed of a combination of materials such as rubber, a combination of materials such as steel or textile, and various chemical materials, among others.
A tractor is a self-propelled, torque-requiring vehicle intended primarily for pulling power at low speeds for agricultural, industrial, and utility purposes. It functions as a mobile power source that can be used for towing, pushing, lifting, or driving a variety of agricultural implements through mechanical, hydraulic, or power take-off systems. Tractors are designed with powerful propulsion systems, sturdy frames, and versatile coupling systems for use on different terrains and under heavy loads.
The electric boat and ship market size is experiencing unparalleled growth as the marine industry embraces electrification on a large scale across different geographies. As sustainability is becoming a strategic priority, with each passing day, more and more marine operators look to electric propulsion technologies as alternatives aimed at cutting down emissions, improving operational efficiencies, and enabling greener ports.
The GCC car rental market has emerged as a critical component of the region's transportation ecosystem, driven by robust tourism activity, expanding business travel, and a substantial expatriate population. Countries across the Gulf Cooperation Council are witnessing unprecedented demand for flexible mobility solutions that cater to diverse customer segments. The GCC car rental market size was valued at USD 1.65 Billion in 2024 as governments prioritize infrastructure development and sustainable tourism initiatives.
The Indian automotive sector has formed a vital part of the country's industrial and economic development for a long period. Over the years, the industry has transformed significantly, influenced by changes in technology, global trends, and consumer preference. Among the various factors shaping its trajectory, government policies have emerged as a decisive force driving growth, innovation, and competitiveness in the India auto parts manufacturing industry.
The India motorcycle tires market continues to evolve in response to changing mobility preferences, rising urbanization, and the growing significance of two-wheelers as essential transportation assets for millions of riders. As per sources, the India motorcycle tires market size reached USD 933.66 Million in 2024. The market is projected to reach USD 2,419.36 Million by 2033, exhibiting a growth rate (CAGR) of 10.3% during 2025-2033.
The Saudi Arabia tire market is undergoing a significant transformation driven by the nation’s economic diversification, rapid urbanization, and growing vehicle ownership. As one of the largest automotive hubs in the Middle East, Saudi Arabia is witnessing increasing demand for both passenger and commercial vehicle tires across urban and industrial regions.
One of the world's most dynamic and quickly changing markets, India's automotive industry is undergoing revolutionary changes in both the new and used car markets. Despite general economic uncertainty, the used car industry has shown remarkable resilience and growth potential, making it a particularly vibrant part of this ecosystem.
One of the world's most vibrant and quickly growing automobile markets is India's passenger car sector. From technological innovation to economic development, a number of interrelated factors have contributed to the sector's remarkable transformation. For stakeholders looking to take advantage of the enormous opportunities in this dynamic market, it is imperative that they comprehend these growth drivers.
India's truck industry is at a turning point in its development, driven by extensive government policies that are changing the commercial vehicle market. The industry, which is the foundation of the country's logistics ecosystem, is gaining previously unheard-of momentum thanks to smart regulatory frameworks and forward-thinking legislative initiatives. A fundamental change in truck operations on Indian highways is being sparked by government initiatives ranging from infrastructure development to emission standards, digitalization, and financial incentives.
The electric rickshaw sector in India has experienced a significant upheaval in recent years and is now a vital part of the country's sustainable transportation network. Strategic government policies aimed at hastening the adoption of clean mobility solutions have played a major role in orchestrating this evolution. India's larger vision of sustainable urbanization is in line with the electric rickshaw industry, which combines social development objectives, economic opportunities, and environmental imperatives.
Transportation in India is undergoing a spectacular change with the advent of electric two-wheelers that are quite an enticing alternative to traditional fuel-powered ones. This change is not merely an act of technological transformation, but an indication of how millions of Indians will think about city mobility, eco-awareness, and economic effectiveness.
As one of the world's leading industrial powerhouses, Japan has long been recognized for its commitment to technological innovation and manufacturing precision. The industry for industrial automation components—encompassing sensors, controllers, actuators, drives, robotics, and human-machine interfaces—represents the backbone of modern manufacturing infrastructure.
The Australian brakes and clutches industry plays a vital role in ensuring vehicle performance, safety, and efficiency across both automotive and industrial segments. As the nation transitions toward electric mobility and smarter manufacturing systems, the demand for advanced braking and clutch mechanisms is rising significantly.
The Philippines automotive wiring harness industry stands at a transformative juncture, driven by technological innovations that are reshaping vehicle electrical architectures worldwide. As vehicles evolve into sophisticated mobile computing platforms, the wiring harness, the circulatory system transmitting electrical power and data throughout modern automobiles, has become increasingly complex and critical to vehicle performance.
Japan's hybrid vehicles market stands as a global benchmark for sustainable mobility innovation, demonstrating remarkable growth and technological leadership. The market achieved a valuation of USD 33.57 Billion in 2024. Japan's hybrid vehicle (HV) market is one of the most established globally, originating with pioneering models like the Toyota Prius. It currently represents a significant portion of the country's automotive sales.
The Japan warehouse robotics market is a highly dynamic and rapidly expanding segment of the global automation industry. The market, valued at USD 414.0 Million in 2024, is on a sharp growth trajectory. Its growth is fueled by critical domestic factors, including a severe labor shortage, the rapid expansion of e-commerce, and Japan's strategic position as a world-leading robotics manufacturer.
The UK is rapidly evolving into a dynamic hub for autonomous vehicle research, testing, and early-stage deployments. A strong ecosystem comprising academic institutions, technology start-ups, automakers, and mobility service providers fosters continuous innovation. Supported by a skilled workforce specializing in software, sensing, robotics, and transportation systems, the nation has become a fertile ground for experimentation.
Japan’s transportation landscape is on the brink of a major shift, with robo taxis, autonomous, driverless vehicles designed for passenger and goods transport, emerging as a practical mobility solution. The Japan robo taxi market reached USD 83.2 Million in 2024 . This remarkable expansion reflects Japan’s broader move toward smart mobility, sustainability, and automation.
The Japan electric truck market is experiencing transformative growth as the nation accelerates toward sustainable transportation and carbon neutrality. As a leading automotive manufacturing hub, Japan is witnessing unprecedented momentum in commercial vehicle electrification, driven by stringent environmental regulations, technological innovation, and strategic government support. The electric truck industry represents a critical component of Japan's commitment to achieving 100% electrified vehicle sales by 2035 and carbon neutrality by 2050.
An EV charging station represents the necessary main infrastructure that allows electrical energy to be transferred from the power grid into electric vehicles to enable their use for transportation. Unlike conventional fueling stations that offer liquid fuels, EV charging stations provide electric power through the use of standardized connectors and smart control systems. The core components include a power conversion unit, which transforms alternating current from the grid into direct current for the vehicle battery; a charging controller controlling communication between the charger and the EV; and a connector or plug matched to the vehicle's charging interface.
An electric scooter is a two-wheeled vehicle powered by an electric motor and rechargeable battery, aimed at offering the means for efficient, eco-friendly, and cost-effective urban mobility. Apart from the traditional scooters that are powered by internal combustion engines, the electric scooters make use of lithium-ion or lead-acid batteries that feed an electric supply to a BLDC motor, which drives the wheels either directly or via a belt or chain mechanism.
Electric bikes, commonly referred to as e-bikes, are one of the most transformational innovations in modern personal mobility, combining conventional bicycle mechanics with advanced electric propulsion technology. At the heart of e-bikes are an electric motor, a rechargeable battery, and a control system that add assistance to the rider while pedaling, making cycling easier, faster, and more accessible across varied terrains. Based on their design, they can be further categorized into pedal-assist, throttle-controlled, or hybrid models, each providing different levels of rider control and engagement of the motor.
The micro-mobility industry has emerged as a transformative force in urban transportation, revolutionizing how people navigate cities worldwide. According to IMARC, the global micro-mobility market size was valued at USD 63.10 Billion in 2024. Looking forward, IMARC Group estimates the market to reach USD 204.83 Billion by 2033, exhibiting a CAGR of 12.86% from 2025-2033.
India's electric vehicle (EV) revolution is accelerating at a breakneck speed, powered by a strategic combination of government incentives, infrastructure investments, and manufacturing policies that are transforming the automotive landscape. The IMARC Group forecasts that the Indian electric car market reached USD 963 Million in 2024.
The diesel engine industry is standing at a transformative crossroads. As global markets are pushing for sustainability, stricter emissions compliance, and cutting-edge innovations, diesel powertrains are facing both immense pressure and promising potential.
The global tire market is a multi-billion-dollar industry, driven by the growing demand for vehicles across emerging economies and the replacement tire segment in developed countries. The global tire market is expected to grow at a compound annual growth rate (CAGR) of 4.70% between 2025 and 2033. The industry is heavily influenced by factors such as technological advancements, raw material prices, environmental regulations, and consumer preferences.
Australia's electric vehicle (EV) sector is experiencing swift expansion, fueled by increasing interest in eco-friendly transportation alternatives. In 2024, sales of battery electric and plug-in hybrid vehicles hit an all-time high, totaling around 114,000 units.
The electric bus industry is the part of the transportation sector that deals with the production and installation of buses that run completely or partially on electricity, employing battery packs or fuel cells in place of conventional diesel or gasoline engines. The buses deliver lower greenhouse gas emissions, lesser noise levels, and enhanced energy efficiency, and thus they are a prime solution for environmentally friendly public transport.
India's electric vehicle market is undergoing a profound transformation, impelled by green priorities, economic imperatives, and changing consumer trends. With rising concerns about air pollution and fossil fuel dependence, electric mobility has become a strategic option for India's transport industry. Policy clarity, technology development, and an emerging ecosystem of makers and suppliers are driving this market shift.
The global electric vehicle market size was valued at USD 755 Billion in 2024. The global EV market is rapidly expanding, driven by technological advancements, government incentives, stricter emission regulations, rising fuel costs, extended battery range, growing environmental consciousness, and significant investments in charging and production infrastructure.
Electric Vehicles, or EVs, are vehicles operated partially or wholly by electrical power, generally with rechargeable battery packs as their fuel. In contrast to conventional internal combustion engine cars, EVs emit no tailpipe emissions, making them a cleaner, environmentally friendly transportation choice. EVs comprise Battery Electric Vehicles (BEVs), Plug-in Hybrid Electric Vehicles (PHEVs), and Hybrid Electric Vehicles (HEVs), and are gaining ground in passenger, commercial, and two-wheeler segments owing to developments in battery technology, charging infrastructure, and policy support.
Aluminum alloy wheels are high-performance, lightweight, and durable components widely used in the automotive industry. Their superior strength-to-weight ratio enhances vehicle efficiency, fuel economy, and handling, making them a preferred choice for both passenger and commercial vehicles. Beyond their functional benefits, aluminum alloy wheels contribute to vehicle aesthetics, offering sleek designs and customization options that appeal to consumers. Their corrosion resistance and thermal conductivity further enhance braking performance and longevity. With increasing demand for fuel-efficient and stylish vehicles, aluminum alloy wheels play a crucial role in the global automotive sector, catering to OEMs, aftermarket suppliers, and performance vehicle manufacturers.
A tyre is a crucial component of a vehicle, serving as the outer covering of a wheel. Its main purposes are to support the vehicle's weight, provide traction for movement, and act as a flexible cushion that absorbs shocks from the road. Usually composed of rubber, tires are strengthened with steel and cloth. Tires for cars, trucks, motorbikes, bicycles, and other vehicles have different designs and compositions depending on the vehicle type and its intended usage. To improve stability and grip, they have a tread pattern on the outside.
Electric kick scooters are small, battery-operated personal transportation vehicles intended for short-distance and urban movement. They offer an economical and environmentally responsible substitute for conventional modes of mobility thanks to their electric engine, rechargeable battery, and lightweight frame. The need for sustainable transportation options, traffic congestion, and growing urbanisation have all contributed to their rise in popularity. Electric kick scooters are now the go-to option for last-mile connectivity and personal commuting because to developments in battery technology, connectivity features, and government programs encouraging micro-mobility.
An automotive wiring harness is an organized assembly of electrical wires, connectors, and terminals that transmit power and signals across a vehicle’s electrical system. It guarantees effective communication between several parts, including the engine control unit, lighting, and sensors. Wiring harnesses are intended to increase vehicle performance and safety by lowering the possibility of short circuits. By maximising electrical connectivity and lowering wire complexity, they are utilised in both conventional and electric automobiles and are essential to contemporary automotive technology.
In an automotive braking system, brake pads are the most important parts since they are engineered to contact the brake rotor to produce friction, thus stopping or slowing down a vehicle in virtually any driving condition safely and efficiently. The key way of classifying these pads is according to their material types: low metallic, ceramic, organic, and semi-metallic.
Tires are essential components of vehicles designed to provide traction, support, and absorb road shocks. Primarily made of rubber, tires consist of treads, belts, and sidewalls that work together to offer grip, stability, and durability. Modern tires come in various types – such as all-season, winter, and performance tires – each engineered for specific driving conditions. The two major tire categories are radial and bias tires, and they are available in different sizes to suit various vehicle types, including passenger cars, light commercial vehicles, medium and heavy commercial vehicles, two-wheelers, and off-road vehicles.
Electric Vehicles (EVs) are powered by electric motors instead of traditional internal combustion engines (ICEs). Electric motors propel EVs by utilizing electricity stored in rechargeable batteries or other energy storage systems. They produce lower or zero tailpipe emissions, reduce air pollution and greenhouse gas (GHG) emissions, and help in mitigating climate change. Electric vehicles consist of various components, such as battery cells and packs, reducers, fuel stacks, power control units, power conditioners, air compressors, humidifiers, motors, on-board chargers, battery management systems, and others. EVs are classified into four types based on propulsion, outlined below.
Saudi Arabia is the second-largest producer and exporter of crude oil and holds the second-largest proven oil reserves in the world, with around 267 billion barrels. The country's oil sector is a significant part of its economy, accounting for 75% of government revenue and approximately 90% of exports. However, due to the volatility of oil prices and the potential for economic instability, Saudi Arabia is increasingly focusing on non-oil activities to reduce its dependency on the oil sector. Non-oil commodities tend to have more stable prices, providing protection against these fluctuations and strengthening the country's social, economic, and financial sectors.