Paracetamol Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
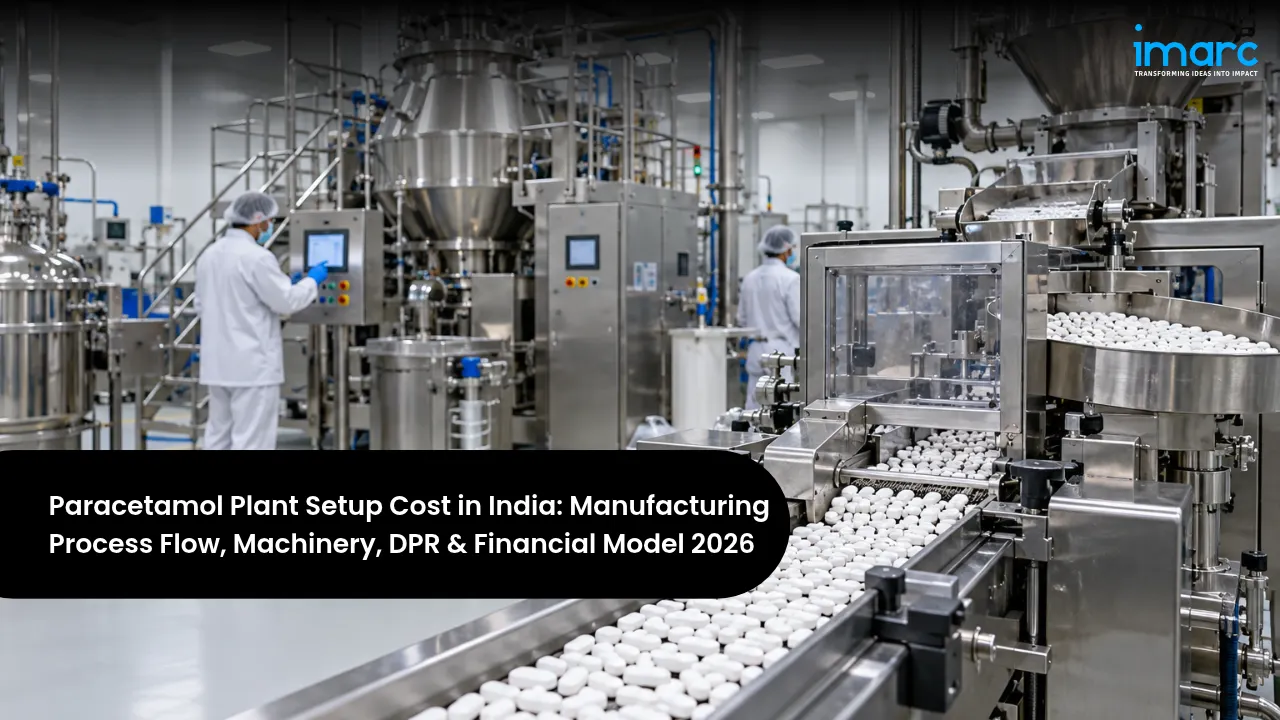
Paracetamol, also called acetaminophen, is one of the world's most widely used medicines for pain and fever, sold in tablets, syrups, suspensions, injections, and combination products. The active pharmaceutical ingredient (API) is made by acetylating para-aminophenol (PAP) with acetic anhydride, then purifying, crystallising, drying, and milling the product to pharmacopoeial standards. The global paracetamol market was valued at about USD 810 million in 2025, and India is one of its largest producers, with leading plants of up to 24,000 tonnes a year and new PAP capacity built under the bulk drug PLI scheme to reduce reliance on imported starting materials. Together these factors make Paracetamol Manufacturing Plant Setup in India an attractive opportunity for API makers, chemical companies, and pharmaceutical groups.
Investment depends mainly on capacity, the regulatory markets targeted, and the degree of backward and forward integration. A GMP API unit buying PAP is the most accessible project, a larger plant with direct compression granules and approvals for regulated markets is a moderate investment, and an integrated complex making its own PAP needs much more capital. The Paracetamol Manufacturing Plant Cost ranges from about INR 25–60 crore for a unit of 600 to 1,500 tonnes a year to INR 80–180 crore for a plant of 3,000 to 6,000 tonnes a year, and INR 500–900 crore for an integrated complex of 15,000 tonnes a year or more with PAP production. Raw materials make up 50 to 60% of operating cost, so PAP and acetic anhydride prices shape profitability. A well-run plant typically earns a gross margin of 35 to 40% and a net margin of 18 to 30%, although prices move sharply through the cycle.
This guide is written for investors exploring how to start a Paracetamol manufacturing plant in India. It focuses on a GMP API plant of about 5,000 tonnes a year making pharmacopoeial and direct compression grades for domestic formulators and export buyers, and also explains smaller units and integrated complexes. It covers products and markets, the demand outlook, the production process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, drug and environmental approvals, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Global Paracetamol Market (2025) | About USD 810 Million |
| Global Forecast (2034) | USD 1,161.9 Million, 4.1% CAGR |
| Leading Indian Plant Capacity | About 24,000 Tonnes a Year |
| PAP Capacity under PLI | About 25,500 Tonnes a Year |
| Typical New Plant Capacity | About 5,000 Tonnes a Year |
| Indicative Total Investment | INR 25 Crore to 900 Crore |
The snapshot shows a large, mature market where India is already a major supplier, with recent investment focused on securing domestic PAP and acetic anhydride so producers depend less on imports. Demand is steady because paracetamol is an essential medicine, but prices swing with raw material costs and competition, so cost position and integration decide who earns good returns. The wide investment range reflects a real choice between a focused API unit, a larger regulated-market plant, and an integrated complex. The sections below work through that choice.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | API, DC granules, fine and dense grades |
| Plant Capacity | 600 – 15,000+ Tonnes per year |
| Total Project Investment | INR 25–60 Crore (small unit) to 500–900 Crore (integrated) |
| Payback Period | 3 – 5 Years |
| Net Profit Margin | 18 – 30% |
| IRR | 18 – 28% |
| Preferred States | Gujarat, Telangana, Andhra Pradesh, Maharashtra, Himachal Pradesh, Tamil Nadu |
| Key Requirement | PAP supply, GMP compliance, approvals |
These ranges provide a realistic frame for early planning, but actual returns depend on PAP and acetic anhydride prices, yields and acetic acid recovery, selling prices that move with global supply, regulatory approvals for export markets, environmental compliance costs, and competition from established Indian and Chinese producers. A site-specific Paracetamol Feasibility Report narrows each of these assumptions to your chosen capacity, grades, integration level, location, and customers.
Table of Contents
- What is Paracetamol Manufacturing?
- Why is Paracetamol Manufacturing Growing in India?
- Paracetamol Manufacturing Process Flow
- Raw Materials Required for Paracetamol Manufacturing
- Location, Land & Infrastructure
- Paracetamol Manufacturing Machinery and Equipment
- Paracetamol Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Paracetamol Manufacturing in India
- Recent Developments in the India Paracetamol Manufacturing Industry
- How a Paracetamol Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Paracetamol Manufacturing?
Paracetamol API is a white crystalline powder, chemically N-acetyl-para-aminophenol, that must meet the Indian, British, European, or United States Pharmacopoeia for assay, related substances such as free PAP, loss on drying, heavy metals, and residual solvents. It is produced in bulk by chemical synthesis and sold to formulation companies that turn it into tablets, capsules, syrups, suspensions, effervescent products, and injections. Because tablets often contain 500 to 1,000 mg of paracetamol, physical properties such as particle size, bulk density, and flow matter as much as purity, which is why many producers also make granulated grades ready for direct compression.
Commercially, the API is sold to domestic formulators, contract manufacturers, government and hospital suppliers through formulators, and export buyers in regulated and emerging markets. A Paracetamol Manufacturing Plant can supply large generic and branded formulation companies, contract manufacturers, combination product makers, and importers in the United States, Europe, Africa, Latin America, and Asia. Buyers value consistent purity, low free PAP and colour, reliable particle size, regulatory documentation such as drug master files and certificates of suitability, and competitive, reliable supply.
- Tablets & Capsules: The largest use, from plain to combination products.
- Liquids & Suspensions: Syrups and drops for children.
- Injectables: Intravenous paracetamol for hospitals.
- Combination Products: Cold, flu, and pain combinations.
The Main Paracetamol Grades and Applications
Choosing the grade range is the most important commercial decision, because it determines finishing equipment, approvals, and customers:
| Grade | Description | Key Property | Primary Demand |
|---|---|---|---|
| Pharmacopoeial API | IP, BP, EP, USP grade | Standard purity | Formulators |
| DC Granules | Pre-granulated API | Ready to compress | Large tablet makers |
| Fine Powder | Small particle size | Fast dissolution | Suspensions, sachets |
| Dense Grade | Larger crystals | Good flow | Wet granulation |
| Injectable Grade | High purity | Low impurities | IV infusions |
| Premixes | Blends with other APIs | Convenience | Combination products |
These choices shape the whole plant. Standard API needs reaction, crystallisation, drying, and milling sections, while DC granules need granulation, drying, and blending lines with tighter control of particle size and hardness. Injectable grades need extra purification and cleaner finishing areas, and regulated-market grades need full documentation and audit-ready systems. Most new entrants therefore start with pharmacopoeial API for domestic and emerging markets, and add DC granules, special grades, and regulated-market approvals as their quality systems and customer base grow.
Why is Paracetamol Manufacturing Growing in India?
Key Growth Drivers in India and Export Markets
Demand is supported by population growth, wider access to medicines, and the need for secure supply of essential drugs:
- Essential medicine: Paracetamol is a first-line treatment for pain and fever worldwide.
- Growing healthcare access: Expanding health coverage in India and emerging markets raises medicine use.
- Self-medication and OTC sales: Over-the-counter use keeps volumes high.
- Supply security: Governments and buyers want reliable sources outside a few countries.
- New formats: Injectables, suspensions, and combinations add value.
India-Specific Market Opportunity
| Segment | Market Context | Manufacturing Role |
|---|---|---|
| Domestic Formulators | Large generic industry | API and DC grades |
| Regulated Exports | US and EU buyers | DMF and CEP-backed API |
| Emerging Markets | Africa, Asia, LatAm | Competitive API |
| Special Grades | Injectables, suspensions | High-purity, fine grades |
| Supply Security | PAP self-reliance | Integrated production |
The strongest opportunity for new entrants lies in cost-competitive API for domestic formulators and emerging markets, in DC granules and special grades that earn better prices, and in integrated production that secures PAP and acetic anhydride supply. Producers that combine low costs, strong compliance, and reliable delivery will be best placed to grow.
Paracetamol Manufacturing Process Flow
Understanding the process helps you plan equipment, layout, and where cost and quality are decided. Production runs from raw material testing through acetylation, crude crystallisation, centrifugation, purification, recrystallisation, drying, milling and sieving, and quality testing to packing and release. Reaction control and purification decide colour and impurity levels, while acetic acid recovery and yields decide cost.
The Paracetamol Manufacturing Process Flow
The sequence below reflects an API plant buying PAP. Integrated complexes first make PAP, usually by hydrogenating nitrobenzene.
| Unit Operation | Key Activity |
|---|---|
| Raw Material Testing | PAP and anhydride checked |
| Acetylation | PAP reacted with anhydride |
| Crude Crystallisation | Crude product separated |
| Centrifugation | Crystals separated |
| Purification | Carbon treatment |
| Recrystallisation | Pure crystals formed |
| Drying | Fluid bed drying |
| Milling & Sieving | Sized to grade |
| Quality Testing | Pharmacopoeial tests |
| Packing & Release | Drums released |
Two factors decide profitability across this flow. The first is yield and purity, because careful control of reaction temperature, carbon treatment, and crystallisation converts more PAP into on-specification API with low colour and free PAP, while poor control raises reprocessing and rejections. The second is recovery and energy efficiency, since recovering acetic acid from mother liquors, recycling water, and using steam and cooling efficiently can lower cost per kilogram significantly in a business where prices are set by global competition.
Raw Materials Required for Paracetamol Manufacturing
The main inputs are para-aminophenol and acetic anhydride, along with activated carbon, antioxidants and process aids, purified water, and packaging such as HDPE drums with liners. India now produces PAP under the bulk drug PLI scheme and acetic anhydride domestically, but some PAP is still imported, so securing supply is central to planning.
| Raw Material | Role in Product | India Sourcing | % of OpEx |
|---|---|---|---|
| Para-Aminophenol (PAP) | Key starting material | PLI plants, imports | 38–45% |
| Acetic Anhydride | Acetylating agent | Domestic producers | 8–12% |
| Activated Carbon | Purification | Domestic suppliers | 1–2% |
| Antioxidants & Aids | Colour control | Domestic suppliers | 1–2% |
| Packaging | Drums and liners | Domestic suppliers | 1–2% |
PAP is the largest and most volatile cost, and its price follows nitrobenzene, hydrogen, and Chinese supply. Long-term contracts with domestic PAP producers, qualifying more than one source, recovering acetic acid for sale or reuse, and, for larger players, integrating into PAP or acetic anhydride help manage cost and supply risk.
Location, Land & Infrastructure
Site selection for a paracetamol plant is driven by access to PAP and acetic anhydride, the availability of a notified chemical or pharmaceutical zone with environmental capacity, proximity to formulation customers and ports, and incentives under state pharmaceutical policies and bulk drug parks. Other factors include reliable steam and power, water availability, skilled chemists and GMP-trained staff, and common effluent infrastructure. Because bulk drug plants need environmental clearance and generate process effluent, locating in an established pharmaceutical or chemical cluster can make approvals and effluent management easier. Nearness to existing API producers also gives access to experienced staff, service providers, and testing laboratories.
Choosing the Best Location for Paracetamol Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Gujarat | Vadodara, Dahej, Ankleshwar | PAP, chemicals, ports |
| Telangana | Hyderabad bulk drug hub | API skills, ecosystem |
| Andhra Pradesh | Visakhapatnam, Kakinada park | Ports, bulk drug park |
| Maharashtra | Tarapur and Aurangabad | Chemicals and pharma |
| Himachal Pradesh | Una bulk drug park | Incentives |
| Tamil Nadu | Chennai pharma base | Ports and customers |
Gujarat combines domestic PAP and acetic anhydride producers with chemical infrastructure and ports, while Telangana's Hyderabad cluster has deep API skills and an established supplier base. Andhra Pradesh offers ports and a bulk drug park, Maharashtra has a strong chemical and pharma base, Himachal Pradesh offers a bulk drug park with incentives, and Tamil Nadu has ports and formulation customers. The final choice should weigh raw material access, environmental capacity, incentives, talent, and logistics.
Quality, Safety and Environmental Systems
Paracetamol API must meet pharmacopoeial specifications and be made under good manufacturing practices, including the revised Schedule M in India and the GMP standards expected by regulated-market buyers and inspectors. A credible plant needs a quality control laboratory with HPLC, GC, and particle size analysis, validated processes and cleaning, stability studies, change control, and full batch documentation, along with drug master files and certificates of suitability for export markets. Safety focuses on handling acetic anhydride, hydrogen in PAP plants, solvents, and dust. Environmental systems cover process effluent, acetic acid recovery, and solid waste. An experienced Paracetamol Manufacturing Consultant in India can help plan process design, GMP layout, regulatory filings, and environmental systems so the plant meets regulatory and customer requirements from the start.
Infrastructure Requirements (5,000 TPA Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 5 – 10 acres | Chemical or pharma zone |
| Production Block | Reaction, crystallisation | GMP design |
| Finishing Area | Drying, milling, packing | Controlled clean area |
| Tank Farm | Anhydride and acetic acid | Bunded storage |
| Utilities | Steam, chilled water, power | 2 – 3 MW load |
| QC Laboratory | Batch testing | Pharmacopoeial tests |
| Effluent Treatment | ETP, ZLD where required | Consent requirement |
A GMP-compliant production and finishing block with a capable quality control laboratory is the most important infrastructure requirement, since it decides regulatory approvals and customer audits. Reliable steam and chilled water, safe storage for acetic anhydride, efficient effluent treatment, and good road and port access complete the core needs.
Paracetamol Manufacturing Machinery and Equipment
The equipment set covers reaction, crystallisation, separation, purification, drying, milling, sieving, blending, packing, acid recovery, utilities, and testing. Reactors, crystallisers, centrifuges, dryers, and the acetic acid recovery system account for most of the machinery budget. The main items are summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Acetylation Reactor | React PAP | SS or glass-lined |
| Crystalliser | Form crystals | Jacketed, cooled |
| Centrifuge | Separate crystals | Basket or pusher |
| Carbon Treatment Vessel | Remove colour | Agitated |
| Filter | Remove carbon | Closed sparkler |
| Fluid Bed Dryer | Dry API | GMP design |
| Multimill & Sifter | Size product | Stainless steel |
| Blender | Homogenise batches | Double cone |
| Acid Recovery Unit | Recover acetic acid | Distillation column |
| Utility Systems | Steam, chilled, purified water | Boiler, chillers |
| QC Instruments | Test quality | HPLC, GC, PSD |
Machinery should follow the product plan. A small unit needs a few reactors, crystallisers, centrifuges, a dryer, a mill, and a basic laboratory, while a larger plant adds continuous or larger-batch equipment, DC granulation lines, automated blending, acetic acid recovery, and a full regulated-market laboratory. Integrated complexes add hydrogenation reactors and catalyst handling for PAP, and stainless steel, closed-transfer equipment helps meet GMP expectations.
Paracetamol Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a GMP API plant of about 5,000 tonnes a year in India. The final Paracetamol Investment Cost for your project will depend on capacity, grade range, regulatory markets, integration into PAP, effluent systems, land cost, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 40–50% | Reactors, dryers, recovery |
| Buildings & GMP Fit-out | 15–20% | Production and finishing |
| Utilities & ETP | 10–15% | Steam, chillers, effluent |
| Land & Site Development | 5–8% | Land and approvals |
| Pre-operative & Validation | 3–5% | Validation, DMF, audits |
| Working Capital | 10–15% | PAP stocks, receivables |
Machinery, GMP buildings, and utilities make up most of the capital budget, and validation and regulatory filings are important because export customers will not buy until approvals are in place. Working capital covers PAP stocks, finished API inventory, and credit to formulators and importers. Because prices move with global supply and approvals take time, a detailed Paracetamol Business Plan should model sales by grade and market, PAP and anhydride prices, yields and acid recovery, approval timelines, and working capital together, so that funding supports the business through price cycles.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials & Packaging | 50–60% | PAP and anhydride |
| Utilities (steam, power, water) | 20–25% | Crystallisation, drying |
| Labour | 5–8% | Chemists and operators |
| Maintenance | 2–4% | Equipment upkeep |
| Effluent Treatment | 2–4% | ETP and recovery |
| Overheads & QC | 3–5% | Testing, regulatory |
With raw materials and utilities making up most of the cost, margins depend on PAP prices, yields, acetic acid recovery, energy efficiency, and realised selling prices. A good operating model tracks PAP consumption per kilogram of API, batch yields, steam and power use, recovery rates, capacity use, and realised prices by grade and market, and tests margins against higher PAP prices, lower API prices, and slower export approvals.
Financial Analysis and Profitability
Based on analysis of a 5,000 TPA API plant, the financial profile is attractive at mid-cycle prices, supported by steady demand and India's strong position, but returns depend on raw material costs, selling prices, and regulatory approvals. The profitability of Paracetamol manufacturing business in India improves markedly with secure PAP supply, high yields and acid recovery, efficient utilities, a good share of DC granules and special grades, approvals for regulated markets, and long-term supply contracts with formulators.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 35–40% | Raw material driven |
| Net Profit Margin | 18–30% | Varies through cycle |
| Payback Period | 3–5 Years | Moderate capital needs |
| IRR (Internal Rate of Return) | 18–28% | Higher with integration |
| Capacity Utilization (stable ops) | 70–90% | Steady demand |
| Break-even Capacity Utilization | 40–50% | Price dependent |
Cost position and market mix decide where a plant lands within these ranges. Integrated producers with captive PAP and strong export approvals earn steadier margins, while units buying PAP at spot prices and selling mostly in competitive domestic markets see much larger swings. DC granules, injectable grades, and regulated-market sales typically carry better margins than standard API.
Returns can be strengthened by securing PAP through long-term contracts or integration, maximising acetic acid recovery, investing in energy efficiency, obtaining DMFs and certificates of suitability, adding DC granules and special grades, and building long-term relationships with large formulators.
Key Risks and Mitigation
The main risks are swings in PAP and API prices, competition from large Indian and Chinese producers, regulatory inspection findings, environmental compliance, acetic anhydride controls, and demand dips after seasonal peaks. Price risk is reduced through contracts and integration; competition risk by cost leadership and special grades; regulatory risk by strong GMP systems; environmental risk by efficient effluent treatment and recovery; and demand risk by a balanced domestic and export customer base. Promoters often work with a Paracetamol Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for Paracetamol Manufacturing in India
Approvals for a paracetamol plant cover drug regulation, environmental clearance, controlled chemicals, and factory requirements, since it is a bulk drug made by chemical synthesis. Promoters setting up a Paracetamol Manufacturing Plant in India generally need the following:
- Drug Manufacturing License: License from the State Drug Controller under the Drugs and Cosmetics Rules, with compliance to the revised Schedule M GMP requirements.
- Environmental Clearance: Clearance for bulk drug manufacture under item 5(f) of the EIA Notification 2006, followed by Consent to Establish and Operate.
- Controlled Substance Registration: Registration for handling acetic anhydride, which is a controlled substance under the NDPS rules.
- Hazardous Chemicals & Waste: Compliance with the hazardous chemical rules and authorisation for hazardous wastes.
- Factory, Boiler & Fire Safety: Factory license, boiler registration, and fire NOC.
- Export Approvals: WHO-GMP, written confirmation for the EU, US DMF, and European certificate of suitability as required.
- Business & Trade Registrations: Business registration, GST, Udyam, and Import Export Code.
The drug manufacturing license, environmental clearance, and regulatory approvals for export markets are usually on the critical path, since sales cannot start without them. Preparing the EIA, GMP documentation, and regulatory filings in parallel with construction shortens the time from investment decision to first sales.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, products, state pollution control categories, customer specifications, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Paracetamol Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- Backward integration: In November 2025, Farmson Basic Drugs opened a INR 300 crore acetic anhydride plant at Nandesari, Vadodara, as part of its move to become a fully integrated paracetamol producer.
- Domestic PAP capacity: Under the bulk drug PLI scheme, Meghmani and Sadhana Nitro Chem have installed about 13,500 and 12,000 tonnes a year of PAP capacity, reducing reliance on imports.
- Price cycles: A May 2025 rating report noted that Meghmani, with 24,000 tonnes a year of paracetamol capacity, saw paracetamol revenue fall 48% in 2024-25 on lower volumes and a 19% drop in realisations.
- New formulations: In July 2025, Akums Drugs and Pharmaceuticals launched a paracetamol oral suspension of 500 mg per 5 ml in India.
The common thread is that India is strengthening its paracetamol supply chain through backward integration, while price cycles reward producers with low costs and secure raw materials. New entrants who secure PAP, run efficient GMP plants, and build strong customer relationships will be best placed to grow.
How a Paracetamol Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from market demand and grade selection to raw material sourcing, plant design, approvals, and economics. It helps investors decide the right capacity, integration level, and location, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Paracetamol Financial Model covering revenue by grade and market, PAP, acetic anhydride, utility, and packaging costs, yields and acid recovery, labour, effluent treatment, working capital, debt servicing, cash flows, break-even, return on investment, and payback under different price and volume scenarios. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a Paracetamol Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a paracetamol project, a strong DPR also clarifies the raw material and integration strategy, the GMP and regulatory plan, the environmental design, and the customer and market strategy, which together are the factors most likely to decide success. By testing margins against PAP prices, API price cycles, and approval timelines, the report turns a steady, competitive opportunity into a plan that lenders and partners can trust.
Frequently Asked Questions
What are the first steps to set up a paracetamol manufacturing plant in India?
Start by choosing your capacity, grades, and target markets, and whether you will buy PAP or make it. Then commission a feasibility study and DPR, secure PAP and acetic anhydride supply, select a site in a chemical or pharmaceutical zone, apply for environmental clearance, a drug manufacturing license, and controlled substance registration, build a GMP plant, validate processes, and begin supplying formulators while preparing export filings.
How much does it cost to set up a paracetamol manufacturing plant in India?
Investment ranges from about INR 25–60 crore for a unit of 600 to 1,500 tonnes a year to INR 80–180 crore for a plant of 3,000 to 6,000 tonnes a year, and INR 500–900 crore for an integrated complex of 15,000 tonnes a year or more with PAP production.
What are the main steps in making paracetamol?
The flow runs from raw material testing through acetylation of PAP with acetic anhydride, crude crystallisation, centrifugation, carbon purification, recrystallisation, drying, milling and sieving, quality testing, and packing and release.
Which machinery does a paracetamol manufacturing plant need?
Key equipment includes acetylation reactors, crystallisers, centrifuges, carbon treatment vessels, filters, fluid bed dryers, multimills and sifters, blenders, acetic acid recovery units, utility systems, and laboratory instruments such as HPLC and GC.
What raw materials are used to make paracetamol?
The main raw materials are para-aminophenol and acetic anhydride, along with activated carbon, antioxidants and process aids, purified water, and packaging materials.
How profitable is paracetamol manufacturing in India?
A well-run plant typically earns a 35 to 40% gross margin and an 18 to 30% net margin at mid-cycle prices, with payback in about 3 to 5 years. Profitability depends on PAP prices, yields, selling prices, and regulatory approvals.
Which approvals does a paracetamol manufacturing plant need in India?
Typical approvals include a drug manufacturing license with revised Schedule M compliance, environmental clearance and pollution control consents, controlled substance registration for acetic anhydride, hazardous chemical and waste compliance, a factory license, boiler registration, fire NOC, export approvals, and GST, Udyam, and Import Export Code registrations.
How do I get a feasibility study or DPR for a paracetamol manufacturing project?
A detailed feasibility study and DPR covers market demand, grades, raw materials, plant design, approvals, and full financials. Investors usually engage a Paracetamol Manufacturing Feasibility Study Consultant with experience in bulk drug and chemical projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Ayurveda is India's traditional system of medicine, and Ayurvedic medicines are made from herbs, minerals, and natural bases such as ghee, oils, honey, and jaggery, following classical texts and modern quality standards.
The Europe Medical Cannabis Industry has moved decisively from a patchwork of national pilot programmes into a credentialed pharmaceutical market with prescriptions, import quotas, reimbursement pathways and EU-GMP supply chains. According to IMARC Group, the market reached USD 3,060.0 Million in 2025 and is projected to reach USD 13,161.29 Million by 2034, expanding at a CAGR of 17.60% (2026–2034).
Workplace wellbeing in Asia-Pacific has shifted from a discretionary benefit to something employers are measured on, by regulators, insurers, and the talent market alike. According to IMARC Group, the Corporate Wellness Market was valued at USD 75.0 Billion in 2025 and is projected to reach USD 129.5 Billion by 2034, growing at a CAGR of 6.07% (2026–2034).
The Europe Digital Health Industry has become the continent's principal answer to a demographic and fiscal problem that hospitals alone cannot solve: ageing populations, rising chronic-disease burdens and persistent clinical staff shortages, set against public health budgets that cannot expand at the same pace as demand.
For two decades India bought most of its medical technology from abroad. The government's own assessment put import dependence at more than 85% of the market in 2020, and the country's role was that of a large consumer rather than a producer. That position is now changing, as incentive schemes, multinational localization, and domestic innovation turn the Indian medical devices sector into a manufacturing and export base.
Rapid diagnostic tests deliver results in minutes, without laboratory equipment, at a clinic, pharmacy, field camp, or at home. Lateral flow tests for malaria, dengue, typhoid, HIV, hepatitis, syphilis, pregnancy, fertility, drugs of abuse, and cardiac markers have become an essential part of India's healthcare system, especially in primary care and rural areas where laboratories are scarce.
Setting up a Generic Injectables Manufacturing Plant in India is a high-value, highly regulated venture, powered by the country's position as the pharmacy of the world, growing global demand for affordable injectables, and a wave of patent expiries opening new products to generic competition.
Setting up a Pharmaceutical Manufacturing Plant in India is a high-potential, strategically strong venture, powered by the country's position as the pharmacy of the world and one of the largest generic drug producers globally. India's deep formulation expertise, cost competitiveness, and vast domestic and export demand make a pharmaceutical manufacturing unit setup in India one of the most attractive opportunities in the healthcare sector.
The Dental 3D Printing Market is attracting renewed investor attention because the technology has moved from a promising adjunct to a default production method inside dental laboratories and clinics.
Vitamin water is a functional, non-carbonated beverage that is created by the fortification of purified water with a combination of vitamins, minerals, and sometimes electrolytes, along with natural or artificial flavors and sweeteners. It is placed in a category between bottled water and carbonated soft drinks, providing hydration with a functional twist.
Vitamin B12, or cobalamin, is a water-soluble vitamin that contains the metal cobalt and is a micronutrient required by the human body. It acts as a coenzyme in the synthesis of DNA, the production of red blood cells, and the functioning of the nervous system.
Japan's dietary supplements industry has become one of the most advanced and innovation-led industries in the world. It is at the nexus of science, culture, and consumer health awareness.
A syringe is a medical instrument that is used to inject fluids into the body or to withdraw fluids from the body. A syringe usually has a cylindrical body, a plunger that moves inside the body to generate pressure or suction, and a nozzle to which a needle can be attached.
Cosmetic surgery in Australia today has evolved into a significant element of the greater beauty and wellness economy. Changing cultural attitudes, advances in medical aesthetics, and the rise of social media over the last ten years have reconstituted the ways in which cosmetic surgery is perceived and undertaken by Australians.
The contact lenses market represents a dynamic segment of the global vision care industry, characterized by continuous innovation and expanding demographic demand.
Brazil's diagnostic imaging equipment market stands at a pivotal moment as Latin America's largest and most dynamic healthcare arena. With substantial investments in hospital modernization, regulatory reforms, and artificial intelligence adoption, the market is transforming rapidly. As providers transition from analog to AI-ready platforms, Brazil emerges as a critical destination for medical device manufacturers seeking growth through the next decade.
The Indian healthcare space has indeed been changing. Telemedicine has emerged as one of the most important drivers of this change. Driving this transformation is the increased adoption of digital tools, growing patient awareness, and the pressing need to make healthcare more accessible across diverse geographies.
The Australia medical aesthetics industry size reached USD 396.4 Million in 2025. Looking forward, the market is expected to reach USD 784.8 Million by 2034, exhibiting a growth rate (CAGR) of 7.89% during 2026-2034. Over the last ten years, the medical aesthetic industry in Australia has transformed from a niche beauty service into a mainstream part of healthcare and wellness.
A rapid diagnostic test (RDT) kit is a medical device designed to quickly detect specific biomarkers, antigens, antibodies, or nucleic acids linked to diseases—typically within minutes and without the need for sophisticated laboratory equipment. These kits often use lateral flow assays, immunochromatographic strips, or rapid molecular testing methods to deliver fast and reliable results.
The Philippines pharmaceutical industry stands as one of Southeast Asia's most dynamic and rapidly expanding healthcare markets in the ASEAN region. With a market valuation reaching USD 3.36 Billion in 2025, the sector demonstrates resilience and tremendous growth potential.
Pharmaceuticals are medical products, substances, or formulations involved in the development, manufacture, and regulation for the prevention, diagnosis, treatment, and management of diseases in humans as well as animals.
The Australia aged care industry stands at a pivotal juncture as the nation grapples with demographic shifts that are reshaping the landscape of elderly care services. With an aging population that continues to expand, Australia faces both unprecedented challenges and remarkable opportunities in delivering quality care to its senior citizens.
The Indian vaccines industry holds an unparalleled position globally, often celebrated as the pharmacy of the world due and its massive production scale and capabilities. It reached INR 113.7 Billion in 2024 according to IMARC Group and it is projected to grow at a CAGR of 8.8% from 2025-2033.
The medical imaging market has reached a transformational phase, driven both by rapid technological advancements and growing demands for precision-driven diagnostics. As health systems worldwide come under increasing pressure to improve patient outcomes while minimizing procedural risks and optimizing clinical workflows, medical imaging has become one of the most important cornerstones of modern medicine.
India’s medical devices industry is on a sustained growth trajectory driven by expanding hospital infrastructure, rising chronic disease burden, stronger local manufacturing supported by government incentives, and a rapidly growing shift toward portable and home care devices.
Pectin represents a naturally occurring polysaccharide mainly extracted from cell walls of fruits (mainly from citrus peel and apple pomace). It is a soluble dietary fiber and a hydrocolloid with gelling, thickening, and stabilizing properties. It is mostly composed of galacturonic acid units.
Paracetamol, also referred to as acetaminophen, is an analgesic and antipyretic compound that is commonly used worldwide for the treatment of mild to moderate pain and the management of fever. The mechanism of action occurs mainly in the central nervous system, where it inhibits the mechanisms that regulate pain and body temperature, but lacks anti-inflammatory properties.
The Australia wellness tourism industry has emerged as a critical segment of the country’s broader travel and hospitality sector. It reflects a growing global emphasis on health, self-care, and holistic well-being, capturing the attention of travelers seeking experiences that combine relaxation, rejuvenation, and personal growth.
The Brazil cardiovascular devices market represents a crucial segment in the country’s healthcare ecosystem, addressing one of the leading causes of morbidity and mortality: cardiovascular diseases. Conditions such as heart attacks, stroke, arrhythmias, and heart failure require ongoing medical intervention and advanced heart disease treatment solutions. With the rising prevalence of cardiovascular disorders, demand for comprehensive cardiac care equipment and innovative treatment modalities is increasing.
India's Ayurvedic products market is experiencing remarkable transformation as consumers increasingly prioritize holistic wellness and natural remedies over conventional alternatives. The convergence of traditional healing wisdom with modern consumer preferences has created a dynamic landscape where herbal medicines, chemical-free personal care products, and immunity-boosting supplements are becoming household staples.
Nicotine pouches are small, smokeless oral delivery products of nicotine, free from tobacco, designed to allow for controlled release of the active principle without burning, vaporizing, or use of traditional tobacco leaves. It consists of a small pouch that contains a matrix made basically from plant fibers, flavorings, pH adjusters, and stabilizers impregnated with nicotine, encased in a permeable material permitting the gradual absorption of the product via the oral mucosa.
The pharmaceutical industry in Japan is among the most advanced globally, recognized for combining innovation, high-quality standards, and patient-centered care. Its extensive value chain includes drug discovery, clinical trials, manufacturing, distribution, marketing, and post-market surveillance. Serving both domestic and international markets, Japanese pharmaceutical companies are respected for regulatory compliance, safety, and reliability, establishing them as trusted global collaborators in drug development.
The pharmaceutical industry in Japan is among the most advanced globally, recognized for combining innovation, high-quality standards, and patient-centered care. Its extensive value chain includes drug discovery, clinical trials, manufacturing, distribution, marketing, and post-market surveillance. Serving both domestic and international markets, Japanese pharmaceutical companies are respected for regulatory compliance, safety, and reliability, establishing them as trusted global collaborators in drug development.
The global healthcare IT industry is on a remarkable upswing, fueled by the surge in preventive care, digital health platforms, and smarter patient management systems. According to IMARC Group, the market hit USD 363.15 Billion in 2024, a clear sign of worldwide adoption. An aging population, the growing comfort with remote care, and the push toward personalized medicine are all speeding this momentum.
The global endoscopy devices market is on a sharp growth path, fueled by the shift toward minimally invasive procedures, the need for early diagnosis, and cutting-edge imaging technologies. IMARC Group reported the market hit USD 50.01 Billion in 2024, underscoring its worldwide acceptance.
The global business-to-business (B2B) payments landscape is experiencing a fundamental transformation that is reshaping how enterprises conduct financial transactions across borders and industries. The market, valued at approximately 1,189.6 Billion in 2024, is projecting remarkable growth with expectations to reach USD 2,189.0 Billion by 2033, exhibiting a CAGR of 7% from 2025-2033. This exponential expansion is signaling a paradigm shift in commercial finance, driven by technological innovation, changing business expectations, and the urgent need for more efficient payment infrastructures.
The smart medical devices market is entering a decade defined by connected care, real-time diagnostics, and patient empowerment. Valued at USD 45.9 Billion in 2024, the market is projected to reach USD 82 Billion by 2033, expanding at a compound annual growth rate (CAGR) of 6.33% between 2025 and 2033 by IMARC Group. This steady rise reflects growing confidence in data-driven healthcare systems, integration of IoT in medical environments, and the increasing role of artificial intelligence in clinical decision-making.
Active Pharmaceutical Ingredients (APIs) are the bioactive molecules of any drug used in pharmaceuticals, which cause the desired therapeutic action in the body of a human being. APIs are the central core of all drugs, chemical or biological and are responsible for the efficacy, strength, and safety of the drug. APIs are synthesized by various complex chemical synthesis, fermentation, biotechnological, or extraction processes based on the type of drug.
A bio medical incinerator is a high-temperature combustion system specialized for biomedical waste disposal by hospitals, clinics, laboratories, and research institutions. Biomedical waste usually consists of infectious waste, pathological waste, sharps, pharmaceuticals, and contaminated disposables that are very hazardous to human health and the environment if not treated.
Obesity, once viewed primarily as a lifestyle choice, is now widely recognized as a complex and chronic disease characterized by excessive body fat accumulation. Its global prevalence is escalating at an alarming rate posing a significant and growing challenge to public health systems worldwide.
Gonorrhea, a sexually transmitted infection caused by the bacterium Neisseria gonorrhoeae, is a major public health issue globally. Reports show that over one million new cases of curable STIs are contracted every day by individuals aged 15 to 49 years, with the majority being asymptomatic.
The 7 major allergic conjunctivitis markets reached a value of USD 2.1 Billion in 2024. Looking forward, IMARC Group expects the 7MM to reach USD 2.9 Billion by 2035, exhibiting a growth rate (CAGR) of 3.00% during 2025-2035.
The healthcare sector is changing rapidly because of the growing demand for better ways to manage chronic diseases. As we move toward 2025 and beyond, digital tools are playing an important role in dealing with conditions like diabetes, heart disease, cancer, and respiratory problems.
The global multivitamin gummies market consists of chewable dietary supplements that are charged with key vitamins and minerals aimed at maintaining general health and wellness. The gummies present a handy, enjoyable, and easy-to-swallow option to classic pills or tablets, hence are predominantly preferred by children and adults who do not like taking pills.
India's pharmaceutical sector is evolving rapidly, supported by the integration of artificial intelligence (AI) across the value chain. As of 2023, India ranked as the third-largest pharmaceutical producer by volume, accounting for 20% of global generic drug exports.
As Lung Cancer Awareness continues to build global momentum in 2025, Artificial Intelligence (AI) is proving to be a transformative force—not only in clinical diagnostics but also in public education and preventive health efforts. Given that lung cancer remains one of the world’s deadliest cancers, accounting for over 1.8 million deaths each year and a five-year survival rate of just 28.4%, the integration of AI marks a critical turning point.
Observed on May 19, Hepatitis Testing Day 2025 emphasizes the need to "Test. Treat. Eliminate," highlighting the gap in diagnosing hepatitis B and C, which cause over 1.3 million deaths annually. Hepatitis remains a major global health threat, on par with HIV, tuberculosis, and malaria. The growing viral hepatitis market <Viral Hepatitis Market Size | Share, Trends - 2034 > reflects rising demand for better diagnostics, treatments, and integrated care. The WHO warns that without faster testing and treatment, the goal of eliminating hepatitis by 2030 may not be achieved, with disparities in diagnostics, particularly in low- and middle-income countries, hindering progress.
Observed on May 8, World Ovarian Cancer Day 2025 carries the theme “No Woman Left Behind,” reinforcing the urgent need to close the gaps in access, diagnosis, treatment, and care across all regions and socioeconomic groups. Ovarian cancer remains one of the deadliest gynecological cancers, often detected too late due to vague symptoms and limited screening tools. The World Ovarian Cancer Coalition projects a 55% rise in annual cases and nearly 70% more deaths by 2050, with the heaviest burden falling on low- and middle-income countries. Equitable access to early diagnostics, genetic testing, and targeted therapies is critical.
In clinics around the world, a concerning pattern is becoming increasingly evident: a growing number of patients are experiencing wheezing, breathlessness, and persistent coughing. This surge reflects a broader global trend. According to the World Health Organization (WHO), more than 260 million people are currently living with asthma, making it one of the most widespread and persistent chronic respiratory conditions globally.
Observed on April 25, World Malaria Day 2025 carries the theme “Accelerating Equity in Malaria Prevention and Cure,” underscoring the urgent need to reach communities still lacking access to life-saving vaccines and diagnostics. While global malaria death rates have seen modest declines, the disease continues to claim the life of one child every minute, highlighting the critical need for swift, equity-driven action
Sulfamethoxazole is a common synthetic antibacterial that is a member of the sulfonamide class of antibiotics. This substance plays a very significant role in modern medicine due to the amazing capabilities offered by the substance for curing infections and bacterial diseases. Trimethoprim and sulfamethoxazole are frequently used together to create the well-known antibiotic co-trimoxazole, which is well-known for its potency against a variety of bacterial infections. It works by preventing the manufacture of folic acid, which is necessary for the growth of bacteria. Sulfamethoxazole is an essential part of modern antibiotic therapy since it has been used to treat lung infections, urinary tract infections, and other common bacterial illnesses.
Healthcare consumables are necessary medical supplies used for patient treatment, diagnostics, and cleanliness in clinics, hospitals, and home care settings. These consist of supplies such as surgical masks, bandages, gloves, syringes, catheters, and disinfectants. Usually, they are disposable or single use to preserve sterility and stop infections. Healthcare consumables are an essential component of the global healthcare ecosystem and are in high demand due to expanding healthcare needs, an increase in operations, infection control measures, and technological improvements.
Catheters are flexible, tubular medical devices designed to access various body cavities, organs, or blood vessels for diagnostic or therapeutic purposes. They can be broadly classified into types based on their application, including urinary catheters, cardiac catheters, and intravenous (IV) catheters. Catheters are commonly used in diverse healthcare settings for managing chronic conditions, enabling fluid drainage, delivering medications, or facilitating minimally invasive surgeries.
Bioinformatics involves applying computational techniques and tools to study and understand biological systems at the molecular level. It is a field of study that combines mathematics, biology, computer science, and statistics to research genomic data and biological networks. The goal is to interpret information from large biological data sets, such as DNA sequences, protein structures, gene expressions, and other high-throughput experimental data. This field provides various products and services, such as knowledge management tools, bioinformatics platforms, and services.
A non-animal model refers to an experimental system or method used in scientific research or testing that does not involve the use of animals. These models are developed to simulate biological processes, test hypotheses, or study diseases without the need for live animals. The aim is often to reduce the reliance on animal testing, which has ethical implications and raises concerns about animal welfare.
Cell therapy involves the transplantation and manipulation of living cells to replace and repair damaged tissue. Its primary branches include stem cell therapy and non-stem cell therapy. Stem cell therapy utilizes stem cells to repair, replace, or rejuvenate damaged or diseased cells and tissues as they possess the ability to differentiate into various specialized cell types, making them valuable for regenerative medicine. Non-stem cell-based therapies typically involve somatic cells isolated from the human body. These cells are propagated, expanded, selected, and then administered to patients for curative, preventive, or diagnostic purposes. On the other hand, gene therapy seeks to treat diseases by introducing, replacing, or inactivating genes within cells.