Rice Husk Ash Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
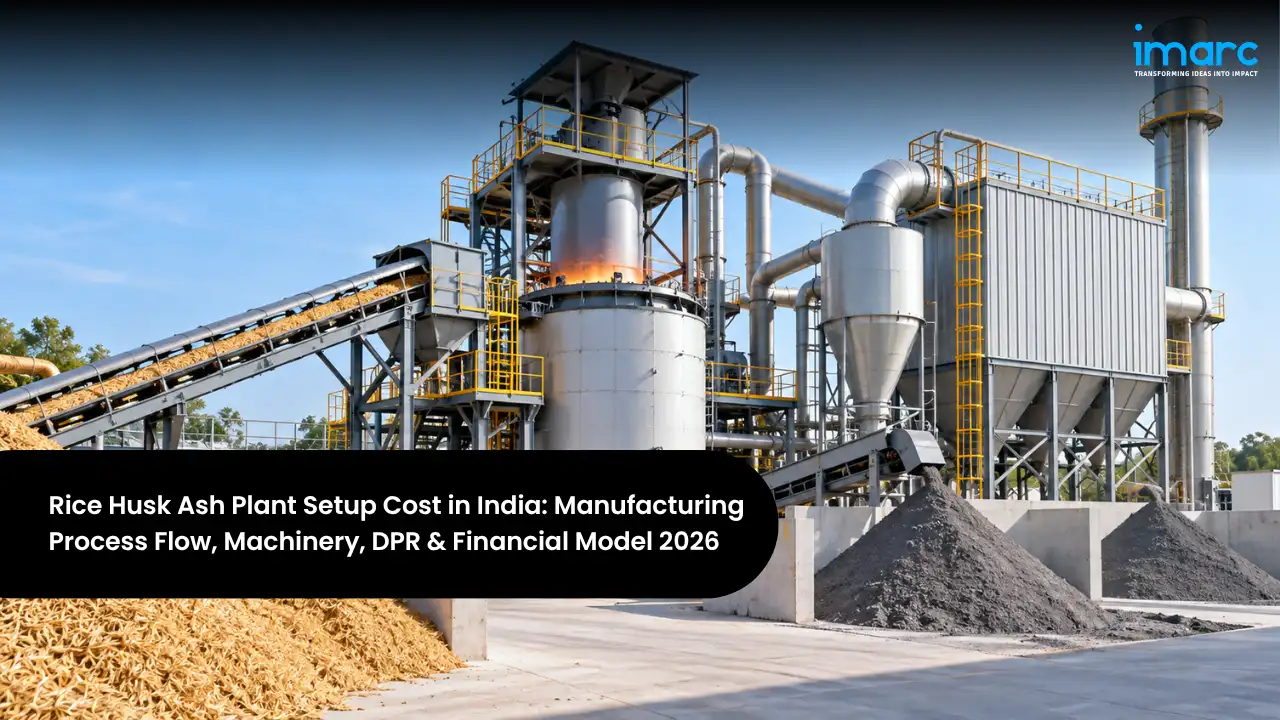
Rice husk ash (RHA) is the residue left when rice husk is burned, and when the burning is properly controlled it is one of the richest natural sources of amorphous silica, typically 85 to 95% silica by weight. Steel plants use it as an insulating cover on molten steel, concrete and cement makers use it as a highly reactive pozzolan that improves strength and durability, and chemical producers extract silica from it for sodium silicate and precipitated silica. India produced a record 154 million tonnes of rice in 2025-26, and husk makes up about a fifth of every tonne of paddy milled, giving the country an enormous and renewable raw material base. Growing steel output, demand for greener construction materials, and export opportunities together make Rice Husk Ash Manufacturing Plant Setup in India an attractive value-added agro-industrial business.
Investment depends above all on the process and scale. A unit that collects ash from rice mill boilers and then screens, grinds, and packs it is a small project, while a plant that burns husk in a controlled-combustion furnace to produce consistent high-silica ash, recovers the heat, and grinds and classifies the product needs more capital, and an integrated complex adding power generation or silica chemicals is larger still. The Rice Husk Ash Manufacturing Plant Cost ranges from about INR 1–3 crore for an ash processing unit of 2,000 to 5,000 tonnes a year to INR 8–25 crore for a controlled-combustion plant of 5,000 to 15,000 tonnes a year, and INR 60–150 crore for an integrated plant with heat recovery power and silica products. Utilities make up 50 to 60% of operating cost and rice husk 10 to 20%, so energy efficiency, husk sourcing, and product quality shape profitability. A well-run plant typically earns a gross margin of 40 to 50% and a net margin of 20 to 35%.
This guide is written for investors weighing how to start a Rice Husk Ash manufacturing plant in India. It focuses on a controlled-combustion plant producing steel-grade and high-reactivity RHA, and also explains silica extraction and other value-added uses. It covers products and markets, the demand outlook, the production process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, approvals, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Global RHA Market (2025) | USD 2.98 Billion |
| Projected Global Market (2034) | USD 4.63 Billion, 5.0% CAGR |
| India Rice Production (2025-26) | Record 154.02 Million Tonnes |
| Husk Share of Paddy | About 20% by weight |
| Silica Content of Quality RHA | About 85 – 95% |
| Indicative Total Investment | INR 1 Crore to 150 Crore |
The snapshot shows a steadily growing global market and an Indian raw material base that is among the largest in the world. Much of India's husk is still burned in rice mill boilers or brick kilns with little control, producing ash of uneven quality that is often dumped. Plants that burn husk under controlled conditions, or that collect and upgrade boiler ash consistently, can turn this waste into a specified product for steel, construction, and chemical buyers. The wide investment range reflects a real choice between simple ash processing, a controlled-combustion RHA plant, and an integrated energy and silica complex. The sections below work through that choice.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Steel-grade RHA, high-reactivity RHA, white silica ash, agricultural grades |
| Plant Capacity | 5,000 – 15,000 Tonnes of ash per year (controlled combustion) |
| Total Project Investment | INR 1 Crore (ash processing) to 60–150 Crore (integrated plant) |
| Payback Period | 2 – 4 Years |
| Net Profit Margin | 20 – 35% |
| IRR | 22 – 30% |
| Preferred States | Punjab, West Bengal, Chhattisgarh, Odisha, Andhra Pradesh, Uttar Pradesh |
| Key Requirement | Steady husk supply, controlled burning, and steel or cement buyers |
These ranges provide a realistic frame for early planning, but actual returns depend on husk availability and price, combustion control and ash quality, energy recovery, product mix, freight to steel plants, cement plants, and ports, and the strength of buyer relationships. A site-specific Rice Husk Ash Feasibility Report narrows each of these assumptions to your chosen process, products, capacity, location, and customers.
Table of Contents
- What is Rice Husk Ash Manufacturing?
- Why is Rice Husk Ash Manufacturing Growing in India?
- Rice Husk Ash Manufacturing Process Flow
- Raw Materials Required for Rice Husk Ash Manufacturing
- Location, Land & Infrastructure
- Rice Husk Ash Manufacturing Machinery and Equipment
- Rice Husk Ash Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Rice Husk Ash Manufacturing in India
- Recent Developments in the India Rice Husk Ash Manufacturing Industry
- How a Rice Husk Ash Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Rice Husk Ash Manufacturing?
Rice husk is the hard outer covering of the rice grain, removed during milling. It contains a high proportion of silica, which plants absorb from the soil, along with cellulose and lignin that burn as fuel. When husk is burned, the organic matter is consumed and the silica remains as ash, making up about 15 to 20% of the husk's weight. The temperature and duration of burning decide the ash's properties: controlled burning at roughly 600 to 700°C keeps the silica amorphous and highly reactive, while uncontrolled burning at higher temperatures turns it crystalline and less useful, and incomplete burning leaves black ash with more carbon.
Commercially, RHA serves several industries. A Rice Husk Ash Manufacturing Plant can supply integrated and secondary steel plants and foundries, cement and ready-mix concrete producers, precast and construction chemical companies, refractory and insulation makers, sodium silicate and precipitated silica producers, rubber, paint, and plastics compounders, farms and horticulture, and export markets in the Middle East, Southeast Asia, and Europe. Buyers value consistent silica content, low and controlled carbon, fine and uniform particle size, and reliable supply.
- Steel Industry: Insulating cover for ladles and tundishes that keeps molten steel hot.
- Cement & Concrete: Reactive pozzolan that replaces part of the cement and improves durability.
- Silica Chemicals: Feedstock for sodium silicate and precipitated silica.
- Refractories & Agriculture: Insulating bricks, castables, and silicon-rich soil conditioners.
The Main RHA Products and Grades
Choosing the product mix is the most important commercial decision, because it determines combustion control, grinding, capital cost, and customers:
| Product / Grade | Description | Key Property | Primary Demand |
|---|---|---|---|
| Steel-Grade RHA | Powder or granules with some carbon | Low thermal conductivity | Steel plants and foundries |
| High-Reactivity RHA | Finely ground amorphous ash | Strong pozzolanic activity | Cement and ready-mix concrete |
| White Silica Ash | Low-carbon, high-silica ash | Above 90% silica | Sodium silicate and silica makers |
| Refractory & Insulation Grade | Ash for bricks and castables | Heat insulation | Refractory and kiln users |
| Agricultural Grade | Coarser ash or blends | Silicon and potassium supply | Farms and horticulture |
| Filler Grade | Very fine silica filler | Reinforcement and bulk | Rubber, paints, plastics |
These choices shape the whole plant. Steel-grade RHA is the largest established market and tolerates some carbon, making it a natural starting product, while high-reactivity RHA for concrete and white silica ash for chemicals need tighter combustion control and finer grinding but earn higher prices. Most new entrants therefore begin with steel-grade ash for domestic and export buyers, then add high-reactivity grades for concrete and cement as their process control and testing capabilities mature.
Why is Rice Husk Ash Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
Demand is supported by steel and construction growth, the push for sustainable materials, abundant feedstock, and export interest:
- Growing steel production: India produced about 170 million tonnes of crude steel in 2025-26, and every ladle and tundish needs insulating cover material.
- Green construction materials: Partial replacement of cement with reactive RHA lowers carbon emissions while improving concrete strength and durability.
- Abundant raw material: Record rice harvests generate tens of millions of tonnes of husk each year, much of it under-used.
- Waste valorisation: Pollution control boards and rice mills seek better ways to handle husk and boiler ash than dumping.
- Export demand: Steel makers in the Middle East, Asia, and Europe import RHA, and India is a leading supplier.
India-Specific Market Opportunity
| Segment | India Market Context | RHA Role |
|---|---|---|
| Steel Plants & Foundries | Rapid capacity growth | Steel-grade insulating ash |
| Cement & Ready-Mix Concrete | Large and growing construction sector | High-reactivity pozzolan |
| Silica Chemicals | Demand for precipitated silica in tyres | White silica ash feedstock |
| Refractories & Insulation | Steel and kiln industries | Insulating bricks and castables |
The strongest opportunity for new entrants lies in producing consistent, specified ash from controlled combustion, rather than variable boiler ash, and selling it under supply contracts to steel plants, cement and concrete producers, and exporters. Producers that test every batch, offer granulated and finely ground grades, and recover energy from husk burning will be best placed as buyers look for reliable, sustainable silica sources.
Rice Husk Ash Manufacturing Process Flow
Understanding the process helps you plan equipment, energy use, and where cost and quality are decided. Production runs from husk procurement and storage through cleaning, controlled combustion, heat recovery, ash cooling and collection, grinding, classification, testing, and packing. Combustion temperature and time determine silica form and carbon content, while grinding energy and husk cost are the largest controllable costs.
The Rice Husk Ash Manufacturing Process Flow
The sequence below reflects a controlled-combustion plant with heat recovery. A processing-only unit collects ash from rice mill boilers and begins at screening and grinding, while silica plants add alkaline digestion, filtration, and precipitation after the ash is produced.
| Unit Operation | Key Activity |
|---|---|
| Husk Procurement & Storage | Husk received from mills and stored dry |
| Cleaning & Feeding | Stones and dust removed, husk fed steadily |
| Controlled Combustion | Husk burned at about 600–700°C |
| Heat Recovery | Hot gases raise steam or heat for drying |
| Ash Cooling & Collection | Ash cooled and captured by cyclones and filters |
| Carbon Control | Ash burned further for white grades if needed |
| Grinding | Ash milled to the required fineness |
| Classification & Sieving | Particles sized for each grade |
| Quality Testing | Silica, carbon, fineness, and reactivity checked |
| Packing & Dispatch | Bagged or granulated, then shipped |
Two factors decide profitability across this flow. The first is combustion control: steady husk feeding, correct temperature, and adequate residence time produce amorphous, low-variability ash that commands premium prices, while poor control yields crystalline or high-carbon ash with limited markets. The second is energy use, because grinding and air handling consume most of the power, so efficient mills and classifiers and recovering heat from combustion for steam or power sharply improve margins.
Raw Materials Required for Rice Husk Ash Manufacturing
The main input is rice husk bought from rice mills, either delivered loose or baled, with moisture and contamination checked on arrival. Processing units may instead buy ash from rice mill boilers and biomass power plants. Other inputs are packaging materials, binders for granulated grades, grinding media, and water. Because husk is also in demand as boiler fuel and for biomass pellets, secure supply contracts with nearby mills are central to project planning.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Rice Husk | Source of silica and heat | Rice mills in paddy belts | 8–15% |
| Boiler Ash (processing route) | Alternative feed for upgrading | Rice mills and biomass plants | Replaces husk |
| Packaging (HDPE and jumbo bags) | Product packing | Domestic suppliers | 2–3% |
| Binders & Additives | Granules for steel grade | Domestic suppliers | 0.5–1% |
| Grinding Media & Consumables | Milling and maintenance | Domestic suppliers | 0.5–1% |
India's rice belts in Punjab, Haryana, Uttar Pradesh, West Bengal, Andhra Pradesh, Telangana, Chhattisgarh, Odisha, and Tamil Nadu generate husk at thousands of mills, giving plants many sourcing options. Prices rise when demand from boilers, power plants, and pellet makers grows, so long-term agreements with clusters of mills, on-site storage to cover the off-season, and in some cases integration with rice milling help manage cost and supply risk.
Location, Land & Infrastructure
Site selection for an RHA plant is shaped by proximity to rice mill clusters for husk supply, distance to steel plants, cement and concrete producers, and ports, land for husk storage, reliable power, and access to roads for bulk transport. Because husk is bulky and light, the plant should sit close to mills, while finished ash is denser and travels more economically to buyers.
Choosing the Best Location for Rice Husk Ash Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Punjab & Haryana | Large rice milling clusters | Husk supply and northern buyers |
| West Bengal | Largest rice producer, steel plants | Husk, steel buyers, and Kolkata port |
| Chhattisgarh & Odisha | Rice bowl plus steel and cement | Husk and major industrial buyers |
| Andhra Pradesh & Telangana | Rice belt and cement clusters | Husk, cement buyers, and ports |
| Uttar Pradesh | Large paddy output | Husk and northern construction demand |
| Tamil Nadu | Parboiled rice mills | Husk and export ports |
Chhattisgarh, Odisha, and West Bengal stand out because they combine large rice output with steel, sponge iron, and cement industries nearby, keeping both husk and product freight short. Punjab and Haryana offer dense milling clusters, Andhra Pradesh and Telangana combine rice with cement clusters and ports, and Tamil Nadu suits export-oriented plants. The final choice should weigh husk availability and price, buyer proximity, port access, land, and power.
Quality, Safety and Environmental Systems
Steel, cement, and chemical buyers specify silica content, loss on ignition or carbon, fineness, moisture, and reactivity, so a credible plant needs a laboratory for chemical analysis, particle size, and pozzolanic activity testing, batch records, and certificates of analysis for every lot. Husk is combustible and stored in large volumes, so fire prevention, detection, and fighting systems are essential. Fine ash is a dust hazard, so enclosed handling, cyclones and bag filters, worker respiratory protection, and controlled stack emissions are needed to meet pollution control standards. An experienced Rice Husk Ash Manufacturing Consultant in India can help plan combustion technology, heat recovery, quality systems, and buyer qualification so the plant meets specifications from the start.
Infrastructure Requirements (Controlled-Combustion RHA Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 2 – 6 acres | Large covered husk storage |
| Husk Storage Shed | Covered, ventilated storage | Fire safety and moisture control |
| Furnace & Heat Recovery Area | Combustor and boiler or dryer | Space for future power unit |
| Grinding & Packing Building | Mills, classifiers, and packing | Enclosed dust-controlled area |
| Power Supply | HT connection, 0.3 – 1 MW | Grinding and fans are main loads |
| Pollution Control | Cyclones and bag filters | Stack monitoring as required |
| Finished Goods Store | Covered storage and loading | Truck and container access |
Covered husk storage with good fire protection and a well-designed combustion and heat recovery section are the most important infrastructure requirements, since they decide both safety and ash quality. The plant also needs an enclosed grinding and packing building with dust control, reliable power, and covered finished goods storage with easy truck and container loading.
Rice Husk Ash Manufacturing Machinery and Equipment
The equipment set covers husk handling, combustion, heat recovery, ash collection, grinding, classification, packing, and pollution control. The combustion furnace, heat recovery unit, and grinding mills account for most of the machinery budget. The main items are summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Husk Conveyors & Feeders | Move and meter husk | Steady, controlled feed rate |
| Pre-Cleaning Screens | Remove stones and dust | Protects furnace and mills |
| Controlled-Combustion Furnace | Burn husk to ash | Fluidised bed or cyclonic, temperature control |
| Heat Recovery Boiler or Hot Air Unit | Recover energy | Steam for process or power |
| Ash Cooler | Cool hot ash | Prevents further crystallisation |
| Cyclones & Bag Filters | Collect ash and clean gases | Meets emission norms |
| Ball Mill or Pulveriser | Grind ash | Fine and consistent output |
| Air Classifier & Vibro Sifter | Size particles | Separate grades |
| Granulator (optional) | Make steel-grade granules | Low-dust product |
| Packing Machine | Fill bags and jumbo bags | Accurate weighing |
| Testing Laboratory | Analyse ash quality | Silica, LOI, fineness, reactivity |
Machinery should follow the product and capacity plan. A processing unit needs mainly screens, mills, classifiers, and packing, while a controlled-combustion plant adds the furnace, heat recovery, and gas cleaning equipment that ensure consistent quality. Furnaces with accurate temperature control, efficient mills, and good dust collection raise product value, cut energy use, and keep the plant within emission limits.
Rice Husk Ash Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a mid-sized controlled-combustion RHA plant in India. The final Rice Husk Ash Investment Cost for your project will depend on capacity, combustion technology, the scale of heat recovery or power generation, grinding fineness, any silica chemical line, the level of automation, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 45–55% | Furnace, heat recovery, mills, classifiers, packing |
| Pollution Control | 8–12% | Cyclones, bag filters, stack |
| Civil Works & Buildings | 12–16% | Husk shed, process building, stores |
| Land & Site Development | 6–10% | Land, roads, and yards |
| Utilities & Fire Safety | 3–5% | Power, water, fire protection |
| Pre-operative & Contingency | 4–6% | Engineering, DPR, commissioning, buffer |
| Working Capital | 6–10% | Husk stocks, finished goods, receivables |
Machinery and buildings dominate the capital budget, with husk storage and pollution control taking a meaningful share. Working capital is moderate, though plants often build husk stocks during the milling season to cover lean months, and export orders can tie up inventory in transit. Because husk prices, ash quality, and buyer contracts decide margins, a detailed Rice Husk Ash Business Plan should model husk supply and seasonal prices, energy recovery value, product mix, freight, and buyer terms together, so that funding supports steady year-round operation.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials (husk, packaging) | 10–20% | Husk prices vary by season and region |
| Utilities (power, auxiliary fuel) | 50–60% | Grinding and fans dominate |
| Labour | 8–12% | Operators and handling crews |
| Logistics | 6–10% | Freight to buyers and ports |
| Maintenance & Refractory | 5–7% | Furnace linings and mill wear |
| Overheads & Testing | 2–4% | Laboratory and administration |
With utilities and husk making up most of the cost, margins depend on energy efficiency, husk price, ash yield, and the share of premium grades. A good operating model tracks husk cost per tonne of ash, power consumption per tonne, ash yield, rejection rates, energy recovery credits, and freight per tonne, and tests how margins respond when husk prices rise, when power tariffs change, or when buyers tighten specifications.
Financial Analysis and Profitability
Based on analysis of a mid-sized controlled-combustion RHA plant, the financial profile is attractive, supported by low-cost raw material, modest capital needs, and steady demand from steel and construction, but returns depend on consistent quality and secure husk supply. The profitability of Rice Husk Ash manufacturing business in India improves markedly with long-term husk contracts, efficient combustion and grinding, heat recovery, premium high-reactivity and silica grades, and supply contracts with steel plants, cement producers, and exporters.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 40–50% | Low raw material cost |
| Net Profit Margin | 20–35% | After depreciation and Indian corporate taxes |
| Payback Period | 2–4 Years | Faster with energy recovery |
| IRR (Internal Rate of Return) | 22–30% | Higher with premium grades |
| Capacity Utilization (stable ops) | 65–85% | Depends on husk supply |
| Break-even Capacity Utilization | 35–45% | Moderate fixed costs |
Quality and supply decide where a plant lands within these ranges. Plants producing consistent, tested ash under contract with steel and cement buyers earn healthy margins, while plants selling variable ash on the spot market face low prices and rejections. High-reactivity and white silica grades command premiums, and steam or power from heat recovery can offset a large part of energy costs.
Returns can be strengthened by integrating with rice mills or biomass power plants, recovering heat for steam or power, investing in temperature-controlled combustion and efficient grinding, qualifying products with cement and concrete companies, building export relationships, and adding silica chemical lines as volumes grow.
Key Risks and Mitigation
The main risks are rising husk prices due to competing demand from boilers, power plants, and pellet makers, inconsistent ash quality, dependence on a few steel buyers, freight costs, and fire and dust hazards. Supply risk is reduced through long-term mill contracts and storage; quality risk by controlled combustion and testing; buyer risk by serving steel, construction, chemical, and export markets; freight risk by locating near buyers or ports; and safety risk by strong fire and dust controls. Promoters often work with a Rice Husk Ash Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for Rice Husk Ash Manufacturing in India
Approvals for an RHA plant combine pollution control requirements for combustion and dust with industrial, boiler, and fire safety permits. Promoters setting up a Rice Husk Ash Manufacturing Plant in India generally need the following:
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, covering combustion emissions and dust.
- Boiler Registration: Registration and inspection under the Boilers Act where steam is raised from heat recovery.
- Power Approvals: Industrial power connection, and approvals for captive or grid-connected generation where power is produced.
- Factory & Fire Approvals: Factory license under the Occupational Safety, Health and Working Conditions Code, 2020, building approval, and Fire NOC covering husk storage.
- Local Permits: Industrial land use approval and trade license from the local authority.
- Export Registrations: IEC and relevant export promotion council membership for overseas sales.
- Business & Tax Registrations: Company incorporation, GST, Udyam where applicable, and EPF and ESI registrations.
Pollution consents and fire approvals are usually on the critical path, together with boiler registration where heat recovery is used, while buyer qualification and sample testing are needed before regular orders. Planning approvals and buyer trials in parallel with plant construction shortens the time from investment decision to commercial operations.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, combustion and heat recovery systems, product types, export markets, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Rice Husk Ash Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- Record raw material base: In May 2026, the Third Advance Estimates put India’s 2025-26 rice production at a record 154.02 million tonnes, expanding husk availability.
- Steel growth: India’s crude steel production reached about 170 million tonnes in 2025-26, supporting demand for steel-grade insulating ash.
- Concrete research: Studies published in November 2025 confirmed that reactive RHA can replace 10–20% of cement while improving strength, and used machine learning to predict the strength of RHA concrete.
- Competition for husk: Biomass co-firing in coal power plants and growing pellet production are raising demand and prices for husk, making secure supply contracts more important.
The common thread is abundant feedstock, steady industrial demand, and growing interest in RHA as a low-carbon construction material, balanced by rising competition for husk. Producers who secure supply, control quality, and serve several markets will be best placed to grow.
How a Rice Husk Ash Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from husk availability and buyer demand to plant design, machinery, energy recovery, approvals, and economics. It helps investors decide the right process, products, and capacity, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Rice Husk Ash Financial Model covering revenue by grade and customer, husk supply and seasonal prices, ash yield, power and fuel costs, heat recovery credits, labour and freight, working capital, debt servicing, cash flows, break-even, return on investment, and payback under different price and supply scenarios. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a Rice Husk Ash Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For an RHA project, a strong DPR also clarifies the husk sourcing strategy, the combustion and heat recovery design, the product and buyer plan, and the phasing of value-added grades, which together are the factors most likely to decide success. By testing margins against husk price increases, quality issues, and slower sales, the report turns an agro-waste opportunity into a plan that lenders and partners can trust.
Frequently Asked Questions
What are the first steps to set up a rice husk ash manufacturing plant in India?
Start by mapping husk availability from nearby rice mills and identifying steel, cement, and export buyers, then choose process, products, and capacity. Next, commission a feasibility study and DPR, secure land with storage space, obtain pollution consents, boiler registration where needed, and fire approvals, install the furnace, heat recovery, grinding, and packing equipment, sign husk supply contracts, and qualify samples with buyers.
How much does it cost to set up a rice husk ash manufacturing plant in India?
Investment ranges from about INR 1–3 crore for an ash processing unit of 2,000 to 5,000 tonnes a year to INR 8–25 crore for a controlled-combustion plant of 5,000 to 15,000 tonnes a year, and INR 60–150 crore for an integrated plant with heat recovery power and silica products.
What are the main steps in a rice husk ash manufacturing?
The flow runs from husk procurement and storage through cleaning and feeding, controlled combustion, heat recovery, ash cooling and collection, carbon control, grinding, classification and sieving, quality testing, and packing and dispatch.
Which machinery does a rice husk ash manufacturing plant need?
Key equipment includes husk conveyors and feeders, pre-cleaning screens, a controlled-combustion furnace, a heat recovery boiler or hot air unit, an ash cooler, cyclones and bag filters, ball mills or pulverisers, air classifiers and sifters, an optional granulator, packing machines, and a testing laboratory.
What raw materials are used to make rice husk ash?
The main input is rice husk from rice mills, or boiler ash for processing-only units, along with packaging materials, binders for granulated grades, grinding media, and water.
How profitable is a rice husk ash manufacturing in India?
A well-run plant typically earns a 40 to 50% gross margin and a 20 to 35% net margin, with payback in about 2 to 4 years. Profitability depends on husk price and supply, ash quality, energy efficiency, product mix, and freight.
Which approvals does a rice husk ash manufacturing plant need in India?
Typical approvals include State Pollution Control Board consents, boiler registration where steam is raised, power approvals, a factory license, Fire NOC, local permits, IEC for exports, and GST and labour registrations.
How do I get a feasibility study or DPR for a rice husk ash manufacturing project?
A detailed feasibility study and DPR covers husk supply, buyer demand, process and product strategy, plant design, approvals, and full financials. Investors usually engage a Rice Husk Ash Manufacturing Feasibility Study Consultant with experience in biomass and industrial minerals projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Concrete poles carry most of India's low-tension and 11 kV distribution lines, as well as street lights, rural feeders, and telecom cables. They are strong, durable, resistant to rust, rot, and termites, need almost no maintenance, and cost less than steel poles, which makes them the default choice for state power distribution companies.
Crushed stone aggregates and manufactured sand are the most widely used construction materials after water. They form the bulk of concrete, the base layers of roads and runways, railway ballast, and the fill under buildings, factories, and ports.
Almost every industrial process generates heat that has to be removed. Power plants, steel mills, refineries, chemical and pharmaceutical units, food processors, plastics moulders, and now data centers all rely on cooling towers, chillers, and heat rejection equipment running around the clock.
Steel is the backbone of India's economic growth. Buildings, bridges, railways, highways, ports, power plants, automobiles, machinery, and household appliances all depend on it. India is the world's second-largest steel producer, and crude steel output reached about 170 million tonnes in 2025-26.
Ready mix concrete (RMC) is concrete batched in a central plant to a precise, engineered mix design and delivered to construction sites in transit mixers, ready to pour.
Open a modular kitchen cabinet, a wardrobe shutter, or an office workstation in India today and there is a good chance it is made from medium density fibreboard.
India is the world's second-largest producer of ceramic tiles, and walking through any new apartment, mall, hospital, or metro station shows why. Tiles have replaced mosaic, stone, and plain cement floors in homes across the country, while large-format glazed vitrified slabs are now standard in premium projects.
Setting up a TMT Bar Manufacturing Plant in India is a high-demand, infrastructure-driven venture, powered by the country's massive construction and housing boom, government infrastructure spending, and steady urbanisation.
Setting up a Cement Manufacturing Plant in India is a capital-intensive, high-demand venture, powered by the country's massive infrastructure programme, housing boom, and status as the world's second-largest cement producer.
Setting up a PVC Panel Manufacturing Plant in India is a high-demand, construction-driven venture, powered by the country's building boom, fast-growing interior and renovation market, and the shift away from plywood and plaster toward affordable, waterproof panels.
Setting up an Electric Motor Manufacturing Plant in India is a high-value, engineering-driven venture, powered by the country's industrial expansion, energy-efficiency push, and the rise of electric vehicles and automation.
Setting up an Iron Ore Pellets Manufacturing Plant in India is a capital-intensive, high-demand venture, powered by the country's ambitious steel-capacity expansion, the shift toward value-added iron ore, and rising demand from blast furnaces and sponge iron units.
The Saudi Arabia construction market has emerged as one of the most closely watched construction economies in the world. The market reached USD 101.4 Billion in 2025 and is projected to reach USD 140.4 Billion by 2034, expanding at a compound annual growth rate (CAGR) of 3.6% between 2026 and 2034.
A WPC (Wood Plastic Composite) door is a type of composite door made from a combination of wood fibers or wood flour and thermoplastic resins like PVC, polyethylene, or polypropylene, with additives to improve durability and processability. The resulting composite material is then extruded or molded into door panels and frames, providing the attractive look of wood and the strength and water-resistance of plastic.
UPVC windows refer to window frames and window assemblies manufactured from ‘unplasticized polyvinyl chloride,’ which is a relatively rigid and strong thermoplastic substance. While PVC is a flexible material that requires the addition of a softening substance called a plasticizer to be formed into a durable performance material, PVC window frames and UPVC window assemblies, for instance, do not display such requirements due to the presence of unplasticizers, a component of the material that provides enhanced strength, stability, and resistance to the elements such as UV radiation, moisture, and temperature changes.
The Saudi Arabia factoring market represents a critical component of the Kingdom's evolving financial services landscape, offering businesses an increasingly popular alternative to traditional bank lending. Factoring, which involves the sale of accounts receivable to a third-party financial institution at a discount, has emerged as a vital mechanism for improving liquidity, managing cash flow, and mitigating credit risk across diverse industry sectors.
The GCC bridge construction market represents a vital component of the region's ambitious infrastructure transformation agenda, serving as a cornerstone for enhanced mobility, economic integration, and sustainable urban development across the Gulf states.
The Australia industrial couplings industry stands at a transformative juncture in 2025, propelled by technological advancement and surging demand across critical sectors. As mechanical devices connecting two shafts to transmit power and torque, industrial couplings form the backbone of machinery operations in manufacturing, mining, automotive, and energy sectors.
The Saudi Arabia real estate market stands at a pivotal juncture in its evolution, representing one of the most dynamic and transformative sectors within the Kingdom's economy. With this country having a very ambitious agenda of economic diversification and modernization, the real estate business has come out as one of the pillars of this transformation.
Steel is an alloy that consists of iron and carbon in addition to trace amounts of other elements like manganese, silicon, chromium, and nickel. The amount of carbon in steel is usually less than two percent and is an important factor in determining the strength, hardness, and ductility of steel.
Saudi Arabia’s precast concrete market reached USD 1.2 Billion in 2024 as per the IMARC Group, clear proof that off-site construction is rapidly becoming the Kingdom’s go-to building solution. With residential, commercial, and major infrastructure projects multiplying, developers are increasingly turning to precast building solutions to keep pace.
The GCC cold storage construction market represents critical infrastructure underpinning regional food security, pharmaceutical distribution, and temperature-sensitive logistics across the Arabian Peninsula. As Gulf Cooperation Council nations diversify their economies and reduce hydrocarbon dependence, robust cold chain infrastructure has emerged as a cornerstone of sustainable development planning.
PVC panels are lightweight, durable building materials made from polyvinyl chloride using extrusion or molding processes. They are available as rigid or semi-rigid sheets designed primarily for wall and ceiling cladding, partitions, and decorative finishes. Known for their excellent resistance to moisture, chemicals, termites, and corrosion, PVC panels offer a smooth surface and a clean, polished look that’s easy to maintain. Available in an extensive range of colors, textures, and patterns, these panels serve as a practical alternative to traditional materials like wood, plaster, or tiles.
Ready mix concrete (RMC) is a precisely engineered construction material produced in a controlled environment within a batching plant and delivered to construction sites in a freshly mixed, plastic state. It is formulated by combining cement, aggregates, water, and chemical or mineral admixtures in carefully proportioned quantities to achieve specific performance characteristics. Unlike site-mixed concrete, RMC ensures consistent quality, uniformity, and superior workability through automated production and quality control processes.
The construction industry across the Gulf Cooperation Council (GCC) member states is at the core of a monumental economic transformation. Far exceeding traditional building activities, the sector now serves as the principal vehicle for national economic diversification strategies, moving these nations beyond reliance on oil revenues.
Paver blocks are precast construction material made basically from cement, aggregates, sand, and pigments for constructing surfacing. They are produced in standardized shape and thickness, allowing each unit to interlock to form a strong, load-bearing surface with no need for continuous concrete pouring. Paver blocks possess high compressive strength, abrasion resistance, and are easy to lay and maintain.
The Brazil ceramic tiles market has witnessed stable growth, reflecting broader trends in the construction and building materials industries of the country. The Brazil ceramic tiles market size was valued at USD 1.6 Billion in 2025. The market is expected to reach USD 2.2 Billion by 2034, exhibiting a CAGR of 3.91% during 2026-2034.
MDF is an engineered wood product produced by breaking down hardwood or softwood residuals into wood fibers, which are then combined with resin binders under heat and pressure. MDF exhibits a homogeneous density, a smooth surface, and fine texture, ensuring a much more workable material compared to natural wood.
Float glass is a type of flat glass that is manufactured by floating molten glass on a bed of molten tin. This produces a smooth, uniform surface and consistent thickness. The float process was developed by Pilkington in the 1950s and revolutionized glassmaking because it enabled the production of large, flawless sheets of glass without needing polishing or grinding. The basic raw materials used-silica sand, soda ash, limestone, and dolomite-are heated in the furnace to a very high temperature, then continuously poured onto the tin bath, where the molten glass spreads out into an even layer. It cools and solidifies into a perfectly flat and perfectly transparent sheet. As it provides optical clarity and strength and is easily processed into coated, laminated, or toughened forms, float glass is used as a basic product for various applications, ranging from architectural and automotive to industrial applications.
ERW steel pipes can be identified as one of the most important categories of welded pipes and find wide applications in infrastructure, construction, and other industries because of their precision, cost-effectiveness, and reliability. The raw material to produce these pipes is either hot-rolled or cold-rolled steel coils that are longitudinally formed and welded by the application of high-frequency electric resistance welding.
Drill bits are specifically designed cutting instruments intended to produce cylindrical holes in various materials, ranging from soft woods and plastics to hardened steels, stone, and rock. Although they seem straightforward, drill bits consist of various specialized shapes, coatings, and materials that are designed to suit the cutting characteristics of the intended material and the requirements of the drilling task.
Concrete is among the most widely used construction materials in the world due to its strength, versatility, and durability. It is a composite material largely made of cement, water, aggregates-sand, gravel, or crushed stone-and in some cases, admixtures which give special properties to the concrete.
Clay bricks are one of the oldest and most extensively used construction materials in the globe, appreciated for their strength, durability, insulation against heat, and beauty. They are produced mainly from natural clay and shale, which are fashioned, dried, and subjected to high-temperature firing to produce a hard, dense material that can resist multiple environmental and structural stresses. The mix generally consists of alumina, silica, lime, iron oxide, and magnesia that collectively decide the color, texture, and performance properties of the brick.
Metal beam crash barriers and high mast light poles are essential infrastructural features providing security and visibility on highways, city roads, and industrial sites. Metal beam crash barriers or guardrails are made of galvanized steel beams, typically W-beam or Thrie-beam, that are designed to dissipate the impact energy on impact with a vehicle and minimize death and damage to vehicles.
Laminated plywood is an engineered wood material that is produced by laminating several layers of thin veneers of wood together with powerful adhesives and covering them with a protective or decorative laminate sheet. This amalgamation not only increases the strength of the plywood but also its beauty, which is why it is extremely versatile for use in furniture, cabinetry, floors, paneling, and interior design.
Ductile iron pipes (DIP) are a key part of new water and wastewater infrastructure, providing enhanced performance capabilities over older piping materials. Cast from ductile cast iron, a material that has the strength of steel combined with the resistance to corrosion of cast iron, these pipes are designed to endure high-pressure use while still being flexible enough to absorb stress without cracking.
The real estate sector plays a critical role in driving economic growth and shaping communities. It significantly contributes to national economies by generating jobs, influencing investment flows, and boosting government revenues through taxes. Beyond these economic benefits, real estate development directly affects the quality of life by creating homes, enhancing infrastructure, and revitalizing urban areas.
Gypsum boards, also referred to as drywall or plasterboard, are lightweight, strong and fireproof building materials that are frequently used for partitions, walls and ceilings. Constructed from a gypsum core encased in paper liners, they provide improved acoustics, cost effectiveness, and speedy installation. Gypsum boards are favoured in industrial, commercial, and residential construction because of its environmentally beneficial qualities, ability to withstand moisture, and ability to insulate against heat. They are an essential part of efficient and sustainable construction methods because of their adaptability to contemporary building processes.
A frameless shower door is a modern and aesthetically appealing bathroom fixture that has gained popularity for its sleek and minimalist design. They are constructed without the bulky metal framing that surrounds the glass panels and are typically made from thick, tempered glass that is securely attached to the wall and floor using hinges or brackets.