MIG Welding Wire Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
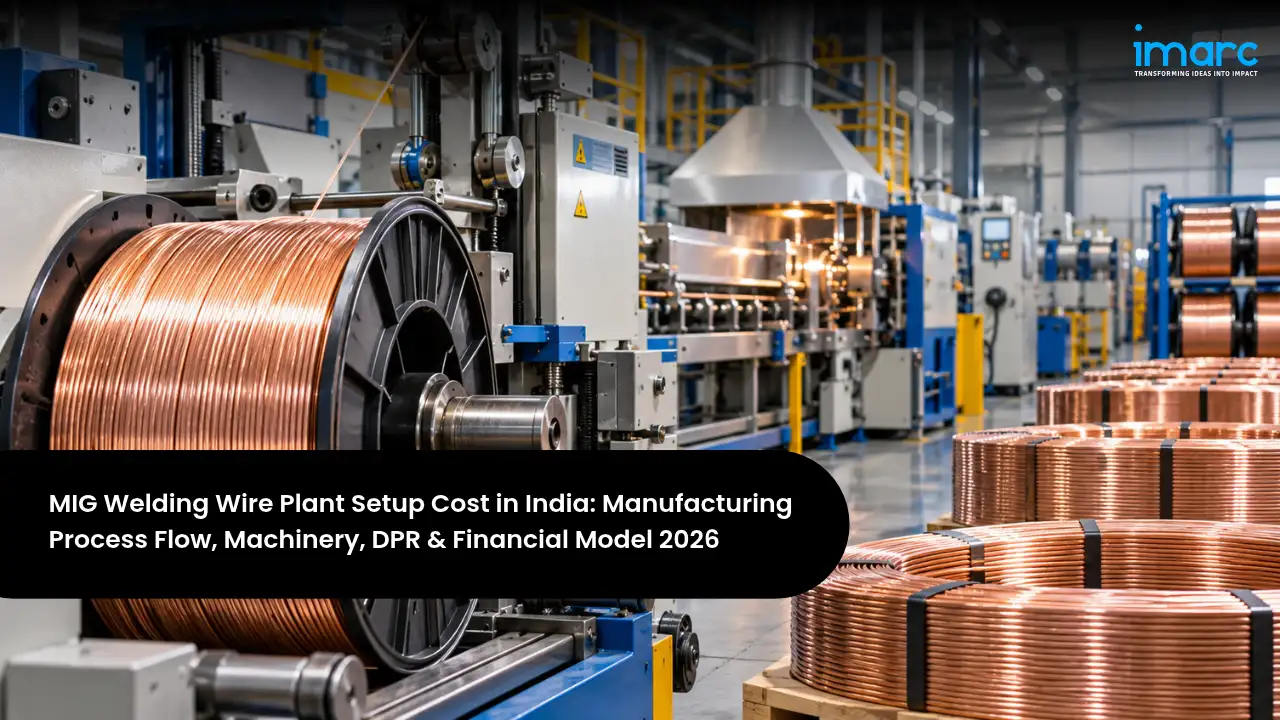
MIG welding wire is a continuous solid wire, usually 0.8 to 1.6 mm in diameter, that is fed through a welding gun and melted by an electric arc under a shielding gas to join metals. The most common type in India is copper-coated mild steel wire for gas-shielded arc welding of structural steel, widely used in fabrication, construction, automobiles, railways, shipbuilding, and capital goods. Compared with stick electrodes, MIG welding is faster, more productive, and suited to automation and robots. India's welding consumables market was valued at about USD 1.32 billion in 2025 and is projected to grow at around 5.8% a year, supported by infrastructure spending, manufacturing growth, and renewable energy projects. Together these factors make MIG Welding Wire Manufacturing Plant Setup in India an attractive opportunity for wire drawers, steel companies, and welding product makers.
Investment depends mainly on capacity, the range of wire types, the level of automation in drawing and winding, and the coating and effluent systems. The MIG Welding Wire Manufacturing Plant Cost ranges from about INR 10–25 crore for a small plant of 2,400 to 6,000 tonnes a year to INR 40–90 crore for a plant of 10,000 to 25,000 tonnes a year, and INR 150–300 crore for a large multi-product plant of 50,000 tonnes a year or more that also makes stainless, aluminium, and flux-cored wires. Wire rod makes up most of the operating cost, so steel prices, drawing efficiency, and product mix shape profitability. A well-run plant typically earns a gross margin of 18 to 25% and a net margin of 7 to 12%.
This guide is written for investors exploring how to start a MIG Welding Wire manufacturing plant in India. It focuses on a plant of about 12,000 tonnes a year making copper-coated and bright mild steel MIG wires on spools and drums for fabricators, automotive companies, and dealers, and also explains small plants and large multi-product facilities. It covers products and markets, the demand outlook, the production process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, BIS and other approvals, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| India Welding Consumables Market (2025) | About USD 1,322.9 Million |
| Market Forecast (2034) | USD 2,221 Million, 5.76% CAGR |
| Largest Product Segment (2025) | Stick Electrodes, 34.5% |
| BIS Standard for MIG Wire | IS 6419, Mandatory under QCO |
| Typical Plant Capacity | 10,000 – 25,000 Tonnes a Year |
| Indicative Total Investment | INR 10 Crore to 300 Crore |
The snapshot shows a large, growing consumables market in which MIG wires are steadily gaining share from stick electrodes as fabricators adopt faster semi-automatic and robotic welding. Mandatory BIS certification for gas-shielded welding wires has raised quality standards and favours organised producers. The wide investment range reflects a real choice between a small plant, a mid-sized dedicated plant, and a large multi-product facility. The sections below work through that choice.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Copper-coated, bright, stainless, aluminium wires |
| Plant Capacity | 2,400 – 50,000+ Tonnes per year |
| Total Project Investment | INR 10–25 Crore (small plant) to 150–300 Crore (large plant) |
| Payback Period | 4 – 6 Years |
| Net Profit Margin | 7 – 12% |
| IRR | 15 – 22% |
| Preferred States | Gujarat, Maharashtra, Tamil Nadu, Haryana, Jharkhand, Punjab |
| Key Requirement | BIS license, wire rod supply, dealer network |
These ranges provide a realistic frame for early planning, but actual returns depend on wire rod prices and quality, drawing speeds and yields, coating quality, die and lubricant costs, the mix of standard and specialty wires, dealer and OEM pricing, and competition from established Indian brands and imports. A site-specific MIG Welding Wire Feasibility Report narrows each of these assumptions to your chosen products, capacity, location, and customers.
Table of Contents
- What is MIG Welding Wire Manufacturing?
- Why is MIG Welding Wire Manufacturing Growing in India?
- MIG Welding Wire Manufacturing Process Flow
- Raw Materials Required for MIG Welding Wire Manufacturing
- Location, Land & Infrastructure
- MIG Welding Wire Manufacturing Machinery and Equipment
- MIG Welding Wire Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for MIG Welding Wire Manufacturing in India
- Recent Developments in the India MIG Welding Wire Manufacturing Industry
- How a MIG Welding Wire Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is MIG Welding Wire Manufacturing?
MIG welding wire is a consumable electrode made by drawing steel wire rod down to a precise diameter, cleaning it, usually coating it with a thin layer of copper, and winding it in neat layers on spools or into drums. The wire carries welding current and melts into the joint, so its chemistry, diameter tolerance, surface cleanliness, and winding quality all affect arc stability, feeding, spatter, and weld strength. The standard mild steel grade contains controlled manganese and silicon to remove oxygen from the weld, and the copper coating improves electrical contact and protects the wire from rust. Stainless steel, aluminium, and flux-cored wires serve more specialised applications.
Commercially, MIG wire is sold to fabricators, construction and structural steel contractors, automobile and auto component makers, railway and shipbuilding yards, capital goods and engineering companies, and through welding equipment dealers, usually in 15 kg spools for manual welding and 250 kg or larger drums for robots. A MIG Welding Wire Manufacturing Plant can supply these customers directly and through dealers, along with OEMs who sell wire under their own brands. Buyers value consistent diameter and cast, smooth feeding, low spatter, clean copper coating, BIS certification, and dependable delivery.
- Structural Fabrication: Buildings, bridges, towers, and pre-engineered structures.
- Automotive: Robotic welding of car and two-wheeler components.
- Heavy Engineering: Rail, shipbuilding, boilers, and capital goods.
- Renewable Energy: Solar structures and wind towers.
The Main MIG Welding Wire Types and Applications
Choosing the product range is the most important commercial decision, because it determines raw materials, process lines, and customers:
| Wire Type | Description | Key Property | Primary Demand |
|---|---|---|---|
| Copper-Coated MS | Mild steel, copper coated | General purpose | Fabrication, auto |
| Bright MS Wire | Uncoated mild steel | Low fume, clean | Robotic lines |
| Stainless Steel | 308L, 316L grades | Corrosion resistance | Food, pharma, chemical |
| Aluminium | 4043, 5356 grades | Light metals | Rail coaches, marine |
| Flux-Cored | Tubular wire with flux | High deposition | Shipbuilding, heavy |
| Low-Alloy Grades | Alloyed steel wires | Higher strength | Boilers, pressure parts |
These choices shape the whole plant. Copper-coated and bright mild steel wires share most of the drawing and winding line, while stainless steel needs different dies, lubricants, and cleaning, and aluminium needs separate, very clean handling. Flux-cored wires need a forming and filling line in addition to drawing. Most new entrants therefore start with copper-coated mild steel wire, the highest-volume product, add bright wire and drums for robotic users, and move into stainless, aluminium, and flux-cored wires as their skills and customer base grow.
Why is MIG Welding Wire Manufacturing Growing in India?
Key Growth Drivers in India and Export Markets
Demand is supported by infrastructure, manufacturing, automation, and renewable energy:
- Infrastructure investment: Large public capital spending on roads, railways, bridges, and buildings increases structural fabrication.
- Manufacturing growth: Production-linked incentives and new factories raise welding in automobiles, electronics, and capital goods.
- Shift to MIG welding: Fabricators move from stick electrodes to faster, more productive MIG processes.
- Automation and robotics: Automotive and component makers use robots that need high-quality wire in drums.
- Renewable energy: Solar mounting structures and wind towers use large volumes of welding wire.
India-Specific Market Opportunity
| Segment | Market Context | Manufacturing Role |
|---|---|---|
| Infrastructure | Steel structures | Mild steel solid wire |
| Automotive | Robotic welding | Bright wire, drums |
| Renewable Energy | Solar and wind | Solid and flux-cored |
| Shipbuilding & Rail | Heavy fabrication | Flux-cored, aluminium |
The strongest opportunity for new entrants lies in copper-coated and bright mild steel wire for fabricators and automotive users in industrial clusters, in drum supply for robotic lines, and in replacing imported specialty wires. Producers that combine consistent quality, BIS compliance, and strong dealer and OEM relationships will be best placed to grow.
MIG Welding Wire Manufacturing Process Flow
Understanding the process helps you plan equipment, layout, and where cost and quality are decided. Production runs from wire rod receipt through descaling, rough drawing, fine drawing, cleaning, copper coating, skin-pass drawing, and layer winding to quality testing and packing. Drawing practice decides diameter accuracy and surface finish, while cleaning, coating, and winding decide how smoothly the wire feeds and welds.
The MIG Welding Wire Manufacturing Process Flow
The sequence below reflects a plant making copper-coated mild steel wire. Bright wire skips the coating step but needs extra surface treatment.
| Unit Operation | Key Activity |
|---|---|
| Wire Rod Receipt | Chemistry and size checked |
| Descaling | Scale removed |
| Rough Drawing | Reduced in stages |
| Fine Drawing | Drawn to 0.8 – 1.6 mm |
| Cleaning | Lubricant removed |
| Copper Coating | Thin copper layer |
| Skin-Pass Drawing | Final size and finish |
| Layer Winding | Precision spooling |
| Quality Testing | Size, cast, chemistry |
| Packing & Dispatch | Spools, drums, cartons |
Two factors decide profitability across this flow. The first is drawing efficiency and yield, because high drawing speeds, good dies and lubricants, and few wire breaks raise output per machine and reduce scrap, which matters when wire rod is most of the cost. The second is surface and winding quality, since poorly cleaned or unevenly coated wire causes feeding problems, spatter, and complaints, while precise layer winding and correct cast and helix allow trouble-free use on semi-automatic and robotic equipment.
Raw Materials Required for MIG Welding Wire Manufacturing
The main input is low-carbon wire rod with controlled manganese and silicon, typically 5.5 mm in diameter, along with drawing lubricants and dies, cleaning and copper coating chemicals, plastic or metal spools, drums, and cartons. Indian steel mills produce suitable wire rod, though some specialty grades and stainless and aluminium feedstock are imported.
| Raw Material | Role in Product | India Sourcing | % of OpEx |
|---|---|---|---|
| Wire Rod | Base metal | Steel mills, imports | 62–70% |
| Lubricants & Dies | Drawing | Domestic, imports | 3–5% |
| Copper & Chemicals | Coating | Domestic suppliers | 2–3% |
| Spools & Drums | Winding, bulk packs | Domestic suppliers | 3–5% |
| Cartons & Packaging | Moisture protection | Domestic suppliers | 1–2% |
Wire rod is by far the largest cost, and its price follows domestic steel prices. Long-term arrangements with steel mills for consistent welding-grade rod, testing every heat for chemistry, buying in quantities that match production, and managing die life help control cost and quality. Pricing linked to steel price movements protects margins when rod prices rise.
Location, Land & Infrastructure
Site selection for a MIG wire plant is driven by access to wire rod from steel mills, proximity to fabrication, automotive, and engineering clusters, reliable power for drawing machines, and environmental capacity for cleaning and coating effluent. Other factors include availability of skilled operators, good road connectivity, and nearness to dealers and OEM customers. Because finished wire is sold through dealer networks and directly to large users across regions, a central location with good logistics can help a plant reach several markets. Industrial areas with common effluent treatment facilities also make it easier to manage coating and rinse water.
Choosing the Best Location for MIG Welding Wire Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Gujarat | Steel and engineering hubs | Wire rod, demand |
| Maharashtra | Pune and Aurangabad auto | Automotive demand |
| Tamil Nadu | Chennai auto, heavy industry | Demand and ports |
| Haryana | Gurugram and Manesar auto | Automotive demand |
| Jharkhand | Steel mills nearby | Wire rod supply |
| Punjab | Ludhiana engineering cluster | MSME demand |
Gujarat and Jharkhand offer good access to wire rod from steel producers, while Maharashtra, Tamil Nadu, and Haryana put plants close to the largest automotive and engineering clusters. Punjab's Ludhiana cluster has many small fabricators and engineering units that buy through dealers. The final choice should weigh wire rod supply, customer proximity, power cost, environmental approvals, and land cost.
Quality, Safety and Environmental Systems
MIG wires for structural steel must carry the BIS mark under the welding rods and electrodes quality control order, which requires testing to IS 6419 for chemistry, mechanical properties of the weld metal, diameter, and winding. Large users and classification societies also test weld quality and audit suppliers. A credible plant needs a laboratory for wire diameter, cast and helix, copper coating weight, surface cleanliness, and chemistry, along with weld testing facilities, batch traceability, and ISO 9001 certification. Safety focuses on moving wire and drawing machines, acid and chemical handling, and heavy coils. Environmental systems cover treatment of acid, copper, and rinse water, and disposal of sludge and spent lubricants. An experienced MIG Welding Wire Manufacturing Consultant in India can help plan product mix, line design, BIS certification, and effluent systems so the plant meets regulatory and customer requirements from the start.
Infrastructure Requirements (12,000 TPA Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 3 – 5 acres | Industrial area |
| Drawing Hall | Rough and fine drawing | Crane, ventilation |
| Coating Section | Cleaning and coating | Fume extraction |
| Winding & Packing | Spooling lines | Clean, dry area |
| Utilities | Power, water, air | 1.5 – 3 MW load |
| QC Laboratory | Wire and weld tests | BIS testing |
| Warehouse | Rod and finished goods | Dry storage |
Reliable power for drawing machines and a well-designed cleaning and coating section with effluent treatment are the most important infrastructure requirements, since they decide output and environmental approvals. Clean, dry winding and packing areas, a capable laboratory, and good road access complete the core needs.
MIG Welding Wire Manufacturing Machinery and Equipment
The equipment set covers descaling, drawing, cleaning, coating, finishing, winding, drum filling, effluent treatment, and testing. Drawing machines, the copper coating line, and precision layer winders account for most of the machinery budget. The main items are summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Descaling Unit | Remove scale | Bending and brushing |
| Rough Drawing Machine | Reduce rod | Multi-block, dry |
| Fine Drawing Machine | Draw to final size | Wet, high speed |
| Annealing Furnace | Soften wire | Optional, continuous |
| Cleaning Line | Clean wire | Electrolytic type |
| Copper Coating Line | Apply copper | Chemical or electrolytic |
| Skin-Pass Unit | Final finish | Precision die |
| Layer Winding Machine | Wind spools | Precision layering |
| Drum Filling Machine | Fill bulk drums | Twist-free |
| Effluent Treatment | Treat rinse water | Copper and acid removal |
| QC Instruments | Test wire | Micrometer, spectrometer |
Machinery should follow the product plan. A small plant needs a descaler, a rough and a fine drawing machine, a combined cleaning and coating line, and a few layer winders, while a mid-sized plant adds several high-speed drawing lines, automated coating, drum filling for robotic users, and a full weld testing laboratory. Large plants add stainless and aluminium lines, flux-cored wire forming and filling, and automated packing, and good dies and lubricants are as important as the machines themselves.
MIG Welding Wire Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a plant of about 12,000 tonnes a year in India. The final MIG Welding Wire Investment Cost for your project will depend on capacity, wire types, automation, coating and effluent systems, land cost, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 50–60% | Drawing, coating, winding |
| Building & Civil Works | 15–20% | Halls and warehouse |
| Land & Site Development | 5–10% | Land and approvals |
| ETP & Utilities | 5–8% | Effluent, power, air |
| Pre-operative & BIS | 2–4% | Trials, certification |
| Working Capital | 12–18% | Wire rod, receivables |
Machinery makes up the largest share of the capital budget, and working capital is significant because wire rod is bought in large lots and dealers and OEMs often expect credit. Because margins depend on the spread between wire rod and finished wire prices, a detailed MIG Welding Wire Business Plan should model sales by product, pack, channel, and region, wire rod prices, yields, die and lubricant costs, dealer margins, and payment terms together, so that funding supports the business through steel price cycles.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials & Packaging | 70–80% | Wire rod, spools |
| Utilities (power, water) | 5–8% | Drawing machines |
| Labour | 4–6% | Operators, technicians |
| Dies & Consumables | 2–4% | Dies, lubricants |
| Logistics | 3–5% | Dealers and OEMs |
| Overheads & Marketing | 3–5% | Brand and admin |
With wire rod making up most of the cost, margins depend on the conversion spread, yields, drawing speeds, and product mix. A good operating model tracks wire rod cost per tonne of finished wire, yield and scrap rates, power use per tonne, die life, capacity use, and realised prices by product and channel, and tests margins against higher rod prices, lower selling prices, or slower collections.
Financial Analysis and Profitability
Based on analysis of a 12,000 TPA plant, the financial profile is moderate but steady, supported by recurring demand from fabrication and manufacturing, but returns depend on the conversion spread, efficiency, and brand strength. The profitability of the MIG Welding Wire manufacturing business in India improves markedly with steady wire rod supply, high drawing speeds and yields, consistent quality that wins OEM approvals, a strong dealer network, a growing share of bright wire, drums, and specialty grades, and pricing linked to steel prices.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 18–25% | Conversion spread driven |
| Net Profit Margin | 7–12% | After finance and taxes |
| Payback Period | 4–6 Years | Moderate capital needs |
| IRR (Internal Rate of Return) | 15–22% | Higher for specialty wires |
| Capacity Utilization (stable ops) | 65–85% | Industrial demand |
| Break-even Capacity Utilization | 45–55% | Thin unit margins |
Product mix and brand strength decide where a plant lands within these ranges. Plants with OEM approvals, robotic-grade drum supply, and specialty wires earn better margins, while units selling only standard spools through dealers compete mainly on price. Stainless, aluminium, and flux-cored wires typically carry much higher margins than mild steel wire.
Returns can be strengthened by securing consistent wire rod, investing in high-speed drawing and precise winding, winning approvals from automotive, railway, and shipbuilding customers, adding drums and specialty wires, building strong dealer relationships, and linking prices to steel prices.
Key Risks and Mitigation
The main risks are wire rod price swings, competition from large Indian brands and imports, quality complaints, BIS compliance failures, environmental issues from coating effluent, credit risk with dealers, and slowdowns in construction and manufacturing. Price risk is reduced through steel-linked pricing; competition risk by quality, service, and specialty products; quality risk by strong testing; regulatory risk by maintaining BIS compliance; environmental risk by good effluent treatment; and credit risk by careful dealer selection. Promoters often work with a MIG Welding Wire Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for MIG Welding Wire Manufacturing in India
Approvals for a MIG wire plant cover product certification, environmental requirements, and customer approvals. Promoters setting up a MIG Welding Wire Manufacturing Plant in India generally need the following:
- BIS Certification: BIS license to IS 6419 under the Welding Rods and Electrodes (Quality Control) Order, 2023.
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, covering cleaning and coating effluent.
- Hazardous Waste Authorisation: Authorisation for spent acids, copper sludge, and used lubricants.
- Factory License & Fire Safety: Factory license, building approval, and fire NOC.
- Customer Approvals: Approvals from classification societies for shipbuilding, and from railway and other large users.
- Quality Certification: ISO 9001 and automotive customer audits for robotic-grade supply.
- Business & Trade Registrations: Business registration, GST, Udyam, trademark, and Import Export Code.
BIS certification and pollution control consents are usually on the critical path, since BIS-marked wire is mandatory for sale and the coating line cannot run without consents. Preparing BIS applications, testing arrangements, and effluent designs in parallel with construction shortens the time from investment decision to first sales.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, products, state pollution control categories, customer specifications, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India MIG Welding Wire Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- Mandatory BIS certification: In July 2023, the government notified the Welding Rods and Electrodes (Quality Control) Order, 2023, making BIS certification mandatory for gas-shielded welding wires to IS 6419 and covered electrodes, phased in from 2024.
- Renewable energy build-out: In 2024-25, India added 29.52 GW of renewable capacity, including 23.83 GW of solar, increasing welding for mounting structures and wind towers.
- Infrastructure spending: The Union Budget 2025-26 set public capital expenditure at INR 11.21 lakh crore, supporting structural fabrication demand.
- Manufacturing investment: By March 2025, investments under production-linked incentive schemes across 14 sectors exceeded INR 1.76 lakh crore, encouraging automated welding.
The common thread is strong demand from infrastructure, renewables, and manufacturing, combined with higher quality standards. New entrants who build efficient, BIS-certified plants and develop strong dealer and OEM relationships will be best placed to grow.
How a MIG Welding Wire Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from market demand and product selection to wire rod sourcing, plant design, certification, channels, and economics. It helps investors decide the right products, capacity, and location, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed MIG Welding Wire Financial Model covering revenue by product, pack, channel, and region, wire rod, coating, die, lubricant, and packaging costs, yields, power use, labour, logistics, working capital, debt servicing, cash flows, break-even, return on investment, and payback under different steel price and demand scenarios. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a MIG Welding Wire Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a MIG wire project, a strong DPR also clarifies the product and channel strategy, the wire rod sourcing plan, the BIS and customer approval path, and the effluent design, which together are the factors most likely to decide success. By testing margins against steel prices, conversion spreads, and competition, the report turns a steady, growing opportunity into a plan that lenders and partners can trust.
Frequently Asked Questions
What are the first steps to set up a MIG welding wire manufacturing plant in India?
Start by choosing your products, such as copper-coated or bright mild steel wire, and your channels, including dealers and OEMs. Then commission a feasibility study and DPR, secure welding-grade wire rod supply, select a site near customers and steel mills, obtain pollution control consents, install drawing, coating, and winding lines, apply for BIS certification, and build dealer and OEM relationships.
How much does it cost to set up a MIG welding wire manufacturing plant in India?
Investment ranges from about INR 10–25 crore for a small plant of 2,400 to 6,000 tonnes a year to INR 40–90 crore for a plant of 10,000 to 25,000 tonnes a year, and INR 150–300 crore for a large multi-product plant of 50,000 tonnes a year or more.
What are the main steps in making MIG welding wire?
The flow runs from wire rod receipt through descaling, rough drawing, fine drawing, cleaning, copper coating, skin-pass drawing, layer winding, quality testing, and packing and dispatch.
Which machinery does a MIG welding wire manufacturing plant need?
Key equipment includes descaling units, rough and fine drawing machines, optional annealing furnaces, cleaning and copper coating lines, skin-pass units, layer winding machines, drum filling machines, effluent treatment, and testing instruments.
What raw materials are used to make MIG welding wire?
The main raw materials are welding-grade low-carbon wire rod, drawing lubricants and dies, cleaning and copper coating chemicals, spools and drums, and cartons and packaging.
How profitable is MIG welding wire manufacturing in India?
A well-run plant typically earns an 18 to 25% gross margin and a 7 to 12% net margin, with payback in about 4 to 6 years. Profitability depends on the conversion spread, yields, product mix, and brand strength.
Which approvals does a MIG welding wire manufacturing plant need in India?
Typical approvals include BIS certification to IS 6419, pollution control consents, hazardous waste authorisation, a factory license and fire NOC, customer and classification society approvals, ISO 9001, and GST, Udyam, trademark, and Import Export Code registrations.
How do I get a feasibility study or DPR for a MIG welding wire manufacturing project?
A detailed feasibility study and DPR covers market demand, products, raw materials, plant design, certifications, channels, and full financials. Investors usually engage a MIG Welding Wire Manufacturing Feasibility Study Consultant with experience in wire and welding products to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Gypsum board, also called plasterboard or drywall, is a panel made of a set gypsum core sandwiched between two sheets of heavy paper.
Steel forgings are strong, reliable metal parts made by shaping heated steel under the force of presses and hammers, which refines the grain structure and gives far better strength and fatigue resistance than casting or machining from bar.
PVC boards, mainly PVC foam boards and WPC boards, are lightweight, waterproof, termite-proof sheets used as an alternative to plywood and MDF in kitchens, bathrooms, wardrobes, furniture, partitions, signage, and interiors.
Laminated veneer lumber, or LVL, is an engineered wood product made by bonding thin wood veneers with their grain running in the same direction, producing straight, strong, and dimensionally stable members from fast-growing plantation timber.
Fly ash bricks turn a waste product from coal-fired power plants into strong, uniform building blocks that need no firing in a kiln. India's thermal power plants generated about 340 million tonnes of fly ash in 2024-25, and government rules require building projects within 300 km of these plants to use ash-based bricks and blocks where they are priced competitively.
Nuts and bolts hold together almost everything that is built or manufactured, from cars, tractors, and two-wheelers to bridges, towers, railways, machinery, and household appliances.
Precast elements are cast in a factory under controlled conditions and then transported to site, where they are lifted into place like the parts of a kit. India's construction sector is turning to this method to build faster, with better quality and less dependence on site labour.
Rice husk ash (RHA) is the residue left when rice husk is burned, and when the burning is properly controlled it is one of the richest natural sources of amorphous silica, typically 85 to 95% silica by weight.
Concrete poles carry most of India's low-tension and 11 kV distribution lines, as well as street lights, rural feeders, and telecom cables. They are strong, durable, resistant to rust, rot, and termites, need almost no maintenance, and cost less than steel poles, which makes them the default choice for state power distribution companies.
Crushed stone aggregates and manufactured sand are the most widely used construction materials after water. They form the bulk of concrete, the base layers of roads and runways, railway ballast, and the fill under buildings, factories, and ports.
Almost every industrial process generates heat that has to be removed. Power plants, steel mills, refineries, chemical and pharmaceutical units, food processors, plastics moulders, and now data centers all rely on cooling towers, chillers, and heat rejection equipment running around the clock.
Steel is the backbone of India's economic growth. Buildings, bridges, railways, highways, ports, power plants, automobiles, machinery, and household appliances all depend on it. India is the world's second-largest steel producer, and crude steel output reached about 170 million tonnes in 2025-26.
Ready mix concrete (RMC) is concrete batched in a central plant to a precise, engineered mix design and delivered to construction sites in transit mixers, ready to pour.
Open a modular kitchen cabinet, a wardrobe shutter, or an office workstation in India today and there is a good chance it is made from medium density fibreboard.
India is the world's second-largest producer of ceramic tiles, and walking through any new apartment, mall, hospital, or metro station shows why. Tiles have replaced mosaic, stone, and plain cement floors in homes across the country, while large-format glazed vitrified slabs are now standard in premium projects.
Setting up a TMT Bar Manufacturing Plant in India is a high-demand, infrastructure-driven venture, powered by the country's massive construction and housing boom, government infrastructure spending, and steady urbanisation.
Setting up a Cement Manufacturing Plant in India is a capital-intensive, high-demand venture, powered by the country's massive infrastructure programme, housing boom, and status as the world's second-largest cement producer.
Setting up a PVC Panel Manufacturing Plant in India is a high-demand, construction-driven venture, powered by the country's building boom, fast-growing interior and renovation market, and the shift away from plywood and plaster toward affordable, waterproof panels.
Setting up an Electric Motor Manufacturing Plant in India is a high-value, engineering-driven venture, powered by the country's industrial expansion, energy-efficiency push, and the rise of electric vehicles and automation.
Setting up an Iron Ore Pellets Manufacturing Plant in India is a capital-intensive, high-demand venture, powered by the country's ambitious steel-capacity expansion, the shift toward value-added iron ore, and rising demand from blast furnaces and sponge iron units.
The Saudi Arabia construction market has emerged as one of the most closely watched construction economies in the world. The market reached USD 101.4 Billion in 2025 and is projected to reach USD 140.4 Billion by 2034, expanding at a compound annual growth rate (CAGR) of 3.6% between 2026 and 2034.
A WPC (Wood Plastic Composite) door is a type of composite door made from a combination of wood fibers or wood flour and thermoplastic resins like PVC, polyethylene, or polypropylene, with additives to improve durability and processability. The resulting composite material is then extruded or molded into door panels and frames, providing the attractive look of wood and the strength and water-resistance of plastic.
UPVC windows refer to window frames and window assemblies manufactured from ‘unplasticized polyvinyl chloride,’ which is a relatively rigid and strong thermoplastic substance. While PVC is a flexible material that requires the addition of a softening substance called a plasticizer to be formed into a durable performance material, PVC window frames and UPVC window assemblies, for instance, do not display such requirements due to the presence of unplasticizers, a component of the material that provides enhanced strength, stability, and resistance to the elements such as UV radiation, moisture, and temperature changes.
The Saudi Arabia factoring market represents a critical component of the Kingdom's evolving financial services landscape, offering businesses an increasingly popular alternative to traditional bank lending. Factoring, which involves the sale of accounts receivable to a third-party financial institution at a discount, has emerged as a vital mechanism for improving liquidity, managing cash flow, and mitigating credit risk across diverse industry sectors.
The GCC bridge construction market represents a vital component of the region's ambitious infrastructure transformation agenda, serving as a cornerstone for enhanced mobility, economic integration, and sustainable urban development across the Gulf states.
The Australia industrial couplings industry stands at a transformative juncture in 2025, propelled by technological advancement and surging demand across critical sectors. As mechanical devices connecting two shafts to transmit power and torque, industrial couplings form the backbone of machinery operations in manufacturing, mining, automotive, and energy sectors.
The Saudi Arabia real estate market stands at a pivotal juncture in its evolution, representing one of the most dynamic and transformative sectors within the Kingdom's economy. With this country having a very ambitious agenda of economic diversification and modernization, the real estate business has come out as one of the pillars of this transformation.
Steel is an alloy that consists of iron and carbon in addition to trace amounts of other elements like manganese, silicon, chromium, and nickel. The amount of carbon in steel is usually less than two percent and is an important factor in determining the strength, hardness, and ductility of steel.
Saudi Arabia’s precast concrete market reached USD 1.2 Billion in 2024 as per the IMARC Group, clear proof that off-site construction is rapidly becoming the Kingdom’s go-to building solution. With residential, commercial, and major infrastructure projects multiplying, developers are increasingly turning to precast building solutions to keep pace.
The GCC cold storage construction market represents critical infrastructure underpinning regional food security, pharmaceutical distribution, and temperature-sensitive logistics across the Arabian Peninsula. As Gulf Cooperation Council nations diversify their economies and reduce hydrocarbon dependence, robust cold chain infrastructure has emerged as a cornerstone of sustainable development planning.
PVC panels are lightweight, durable building materials made from polyvinyl chloride using extrusion or molding processes. They are available as rigid or semi-rigid sheets designed primarily for wall and ceiling cladding, partitions, and decorative finishes. Known for their excellent resistance to moisture, chemicals, termites, and corrosion, PVC panels offer a smooth surface and a clean, polished look that’s easy to maintain. Available in an extensive range of colors, textures, and patterns, these panels serve as a practical alternative to traditional materials like wood, plaster, or tiles.
Ready mix concrete (RMC) is a precisely engineered construction material produced in a controlled environment within a batching plant and delivered to construction sites in a freshly mixed, plastic state. It is formulated by combining cement, aggregates, water, and chemical or mineral admixtures in carefully proportioned quantities to achieve specific performance characteristics. Unlike site-mixed concrete, RMC ensures consistent quality, uniformity, and superior workability through automated production and quality control processes.
The construction industry across the Gulf Cooperation Council (GCC) member states is at the core of a monumental economic transformation. Far exceeding traditional building activities, the sector now serves as the principal vehicle for national economic diversification strategies, moving these nations beyond reliance on oil revenues.
Paver blocks are precast construction material made basically from cement, aggregates, sand, and pigments for constructing surfacing. They are produced in standardized shape and thickness, allowing each unit to interlock to form a strong, load-bearing surface with no need for continuous concrete pouring. Paver blocks possess high compressive strength, abrasion resistance, and are easy to lay and maintain.
The Brazil ceramic tiles market has witnessed stable growth, reflecting broader trends in the construction and building materials industries of the country. The Brazil ceramic tiles market size was valued at USD 1.6 Billion in 2025. The market is expected to reach USD 2.2 Billion by 2034, exhibiting a CAGR of 3.91% during 2026-2034.
MDF is an engineered wood product produced by breaking down hardwood or softwood residuals into wood fibers, which are then combined with resin binders under heat and pressure. MDF exhibits a homogeneous density, a smooth surface, and fine texture, ensuring a much more workable material compared to natural wood.
Float glass is a type of flat glass that is manufactured by floating molten glass on a bed of molten tin. This produces a smooth, uniform surface and consistent thickness. The float process was developed by Pilkington in the 1950s and revolutionized glassmaking because it enabled the production of large, flawless sheets of glass without needing polishing or grinding. The basic raw materials used-silica sand, soda ash, limestone, and dolomite-are heated in the furnace to a very high temperature, then continuously poured onto the tin bath, where the molten glass spreads out into an even layer. It cools and solidifies into a perfectly flat and perfectly transparent sheet. As it provides optical clarity and strength and is easily processed into coated, laminated, or toughened forms, float glass is used as a basic product for various applications, ranging from architectural and automotive to industrial applications.
ERW steel pipes can be identified as one of the most important categories of welded pipes and find wide applications in infrastructure, construction, and other industries because of their precision, cost-effectiveness, and reliability. The raw material to produce these pipes is either hot-rolled or cold-rolled steel coils that are longitudinally formed and welded by the application of high-frequency electric resistance welding.
Drill bits are specifically designed cutting instruments intended to produce cylindrical holes in various materials, ranging from soft woods and plastics to hardened steels, stone, and rock. Although they seem straightforward, drill bits consist of various specialized shapes, coatings, and materials that are designed to suit the cutting characteristics of the intended material and the requirements of the drilling task.
Concrete is among the most widely used construction materials in the world due to its strength, versatility, and durability. It is a composite material largely made of cement, water, aggregates-sand, gravel, or crushed stone-and in some cases, admixtures which give special properties to the concrete.
Clay bricks are one of the oldest and most extensively used construction materials in the globe, appreciated for their strength, durability, insulation against heat, and beauty. They are produced mainly from natural clay and shale, which are fashioned, dried, and subjected to high-temperature firing to produce a hard, dense material that can resist multiple environmental and structural stresses. The mix generally consists of alumina, silica, lime, iron oxide, and magnesia that collectively decide the color, texture, and performance properties of the brick.
Metal beam crash barriers and high mast light poles are essential infrastructural features providing security and visibility on highways, city roads, and industrial sites. Metal beam crash barriers or guardrails are made of galvanized steel beams, typically W-beam or Thrie-beam, that are designed to dissipate the impact energy on impact with a vehicle and minimize death and damage to vehicles.
Laminated plywood is an engineered wood material that is produced by laminating several layers of thin veneers of wood together with powerful adhesives and covering them with a protective or decorative laminate sheet. This amalgamation not only increases the strength of the plywood but also its beauty, which is why it is extremely versatile for use in furniture, cabinetry, floors, paneling, and interior design.
Ductile iron pipes (DIP) are a key part of new water and wastewater infrastructure, providing enhanced performance capabilities over older piping materials. Cast from ductile cast iron, a material that has the strength of steel combined with the resistance to corrosion of cast iron, these pipes are designed to endure high-pressure use while still being flexible enough to absorb stress without cracking.
The real estate sector plays a critical role in driving economic growth and shaping communities. It significantly contributes to national economies by generating jobs, influencing investment flows, and boosting government revenues through taxes. Beyond these economic benefits, real estate development directly affects the quality of life by creating homes, enhancing infrastructure, and revitalizing urban areas.
Gypsum boards, also referred to as drywall or plasterboard, are lightweight, strong and fireproof building materials that are frequently used for partitions, walls and ceilings. Constructed from a gypsum core encased in paper liners, they provide improved acoustics, cost effectiveness, and speedy installation. Gypsum boards are favoured in industrial, commercial, and residential construction because of its environmentally beneficial qualities, ability to withstand moisture, and ability to insulate against heat. They are an essential part of efficient and sustainable construction methods because of their adaptability to contemporary building processes.
A frameless shower door is a modern and aesthetically appealing bathroom fixture that has gained popularity for its sleek and minimalist design. They are constructed without the bulky metal framing that surrounds the glass panels and are typically made from thick, tempered glass that is securely attached to the wall and floor using hinges or brackets.