Blood Collection Tube Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
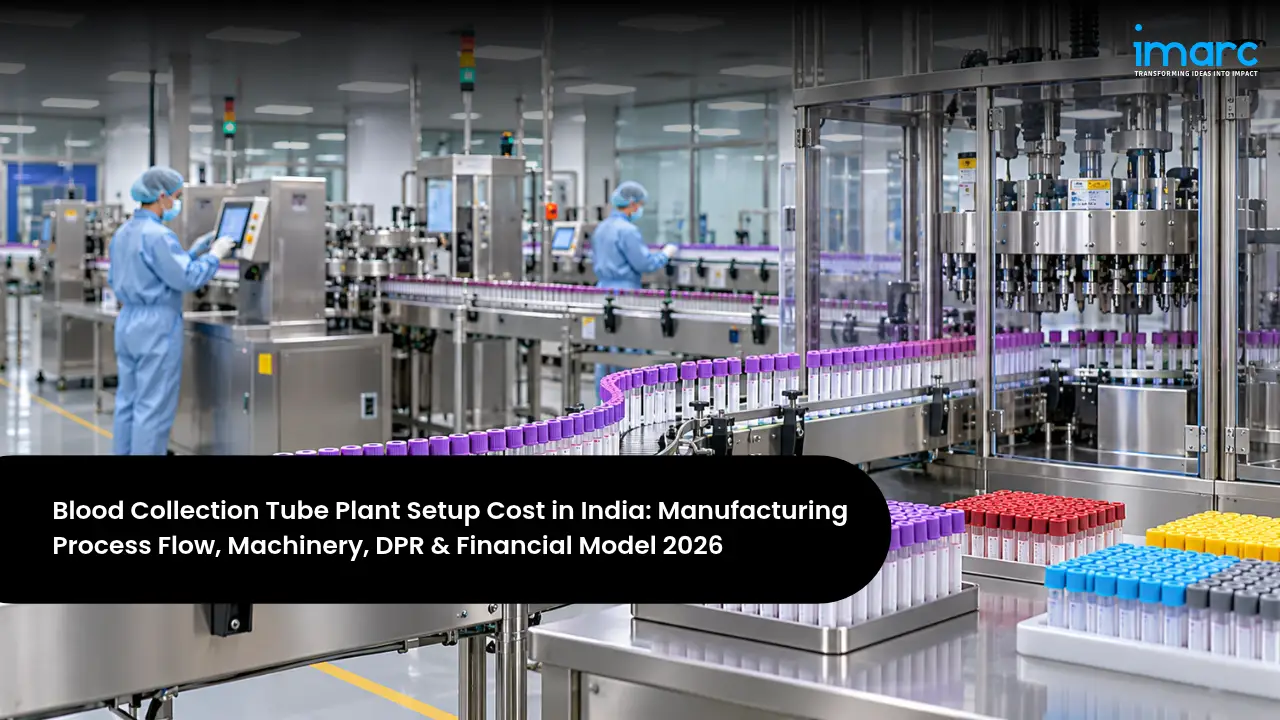
A Blood Collection Tube Manufacturing Plant Setup in India supplies one of the most widely used consumables in healthcare. Evacuated blood collection tubes are sealed plastic tubes with a precise internal vacuum and a colour-coded closure, pre-filled with additives suited to each test: clot activators and separator gel for serum chemistry, EDTA for haematology, sodium citrate for coagulation, heparin for plasma tests, and sodium fluoride for glucose. Every blood test in hospitals, pathology laboratories, diagnostic chains, blood banks, and home collection services begins with one of these tubes. India's expanding diagnostics sector, rising chronic disease burden, preventive health check-ups, and policy push to reduce medical device imports make domestic tube manufacturing an attractive opportunity.
The overall Blood Collection Tube Manufacturing Plant Cost depends mainly on annual capacity, high-cavitation injection moulding machines and moulds for PET tubes and closures, additive dosing and drying systems, automatic vacuum capping and assembly lines, cleanroom area, labelling, inspection, and packing equipment, sterilisation arrangements, quality control laboratories and validation, and working capital for resin, stoppers, additives, and distributor credit. A plant producing about 100 million tubes a year typically needs INR 35 crore to INR 60 crore in fixed assets, or about INR 45 crore to INR 75 crore including working capital, while a smaller semi-automatic unit of 20 to 30 million tubes a year using bought-in tubes and closures can start at around INR 6 crore to INR 12 crore. IMARC Group puts typical capacities at 50 to 200 million tubes a year, with gross margins of 40 to 50% and net margins of 15 to 20%.
This guide is written for medical device manufacturers, diagnostics companies, plastic moulders entering healthcare, distributors, and investors exploring how to start a Blood Collection Tube manufacturing plant in India. It explains product types and end users, demand drivers, the production flow, machinery and raw materials, site selection in medical device clusters, a detailed cost and returns breakdown, the medical device licensing and quality approvals involved, and how a DPR pulls these elements into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Global Blood Collection Tube Market (2025) | USD 6.50 Billion |
| Global Market Outlook | USD 11.39 Billion by 2034, 6.43% CAGR |
| India Medical Devices Market (2026 estimate) | USD 20.23 Billion, projected USD 31.85 Billion by 2034 |
| Typical Plant Capacity | 50–200 Million Tubes a Year |
| Indicative Total Investment | INR 45–75 Crore (100 Million tubes a year, incl. working capital) |
The snapshot shows a growing global market, according to IMARC Group. Blood collection tubes are high-volume, repeat-purchase consumables with steady demand from every part of the healthcare system, and the government's focus on medical device self-reliance supports domestic producers that can match imported products on quality and price.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Serum and gel separator tubes, EDTA tubes, sodium citrate tubes, heparin tubes, fluoride tubes, paediatric and micro tubes |
| Total Project Investment | INR 45 – 75 Crore incl. working capital (100 million tubes a year); INR 6 – 12 Crore (20–30 Million tubes a year) |
| Payback Period | 3 – 5 Years |
| Net Profit Margin | 15 – 20% (IMARC benchmark) |
| IRR | 20 – 26% |
| Best Locations | Andhra Pradesh, Telangana, Tamil Nadu, Gujarat, Haryana, Himachal Pradesh |
| Mandatory Approvals | CDSCO / State Medical Device Manufacturing License (MDR 2017), ISO 13485, SPCB Consents, Factory License |
| Key Requirement | Precise vacuum and additive control, validated sterilisation, and strong diagnostic lab relationships |
These figures offer a practical frame for early evaluation. Returns depend on consistent draw volume and vacuum retention, accurate additive dosing, validated sterilisation, regulatory approvals, high-speed automated production, competitive pricing against imports, and supply contracts with hospitals, diagnostic chains, distributors, and government buyers. A capacity- and product-specific Blood Collection Tube Feasibility Report refines these numbers before capital is committed.
Table of Contents
- What is Blood Collection Tube Manufacturing?
- Why is Blood Collection Tube Manufacturing Growing in India?
- Blood Collection Tube Manufacturing Process Flow
- Raw Materials Required for Blood Collection Tube Manufacturing
- Location, Land & Infrastructure
- Blood Collection Tube Manufacturing Machinery and Equipment
- Blood Collection Tube Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Blood Collection Tube Manufacturing in India
- Recent Developments in the India Blood Collection Tube Manufacturing Industry
- How Blood Collection Tube Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Blood Collection Tube Manufacturing?
Blood collection tube manufacturing combines precision plastic moulding, additive processing, vacuum assembly, and medical-grade quality control. Medical-grade PET is dried and injection moulded into tubes on high-cavitation hot-runner moulds, while plastic caps are moulded and fitted with butyl rubber stoppers. In a cleanroom, additives are applied to the tubes: EDTA is sprayed and dried as a fine coating, sodium citrate and other liquids are dosed precisely, clot activators are coated on the inner wall, and separator gel is dispensed into serum and plasma tubes. Tubes are then evacuated to a set vacuum and capped in a vacuum chamber, which fixes the volume of blood each tube will draw. Finished tubes are labelled with lot, expiry, and fill lines, packed in racks and cartons, sterilised, usually by gamma irradiation, and tested before release. A Blood Collection Tube Manufacturing Plant therefore integrates moulding, cleanroom additive processing, vacuum capping, labelling, sterilisation, and quality control.
Tubes are sold to hospitals, pathology laboratories, diagnostic chains, blood banks, research laboratories, home sample collection services, government health programmes, and distributors, as well as export markets. Buyers expect accurate draw volumes, reliable vacuum over the shelf life, correct additive concentrations, no haemolysis or interference with test results, clean, break-resistant tubes, clear labelling, regulatory compliance, and dependable supply at competitive prices.
- Serum and Gel Separator Tubes: For clinical chemistry, serology, and immunology tests.
- EDTA Tubes: For haematology tests such as complete blood counts.
- Sodium Citrate Tubes: For coagulation tests and ESR.
- Heparin and Fluoride Tubes: For plasma chemistry and glucose testing.
Main Product Types in Blood Collection Tube Production
The product mix shapes additive systems, validation, and margins:
| Product Type | Description | Key Feature | Primary Use |
|---|---|---|---|
| Clot Activator / Gel Separator Tubes | Silica coating, separator gel | Clean serum separation | Clinical chemistry, serology |
| K2 / K3 EDTA Tubes | Spray-dried EDTA coating | Highest volume | Haematology, CBC |
| Sodium Citrate Tubes | Liquid citrate, precise ratio | Strict fill accuracy | Coagulation, ESR |
| Lithium Heparin Tubes | Heparin coating, optional gel | Plasma chemistry | Emergency and routine chemistry |
| Sodium Fluoride / Oxalate Tubes | Glycolysis inhibitor | Stable glucose results | Glucose and lactate testing |
Many new entrants start with plain, clot activator, and EDTA tubes, which make up the bulk of volume, then add gel separator, citrate, heparin, and fluoride tubes, paediatric and micro tubes, and complete blood collection systems with needles and holders as validation, regulatory approvals, and customer relationships mature.
Why is Blood Collection Tube Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
Demand for blood collection tubes is driven by diagnostic testing growth, chronic disease, preventive health, and the push to replace imports. IMARC Group expects the global market to grow at 6.43% a year from 2026 to 2034:
- Diagnostics expansion: Hospital laboratories and organised diagnostic chains are expanding rapidly across cities and smaller towns.
- Chronic disease burden: India has over 101 million diabetics and around 315 million people with high blood pressure, requiring regular blood tests.
- Preventive and home testing: Health check-ups and home sample collection are increasing test volumes.
- Shift from syringes to vacuum systems: Evacuated tubes improve sample quality, safety, and laboratory efficiency compared with syringe collection.
- Medical device self-reliance: Government policy encourages domestic manufacturing to reduce a large medical device import bill.
End-User Market Opportunity
| End User | Demand Driver | Product Role |
|---|---|---|
| Hospitals | Inpatient and outpatient testing | Full tube range |
| Diagnostic Chains & Pathology Labs | Organised testing growth | High-volume EDTA, serum, gel tubes |
| Home Collection & Preventive Health | Convenience testing | Complete collection systems |
| Government Health Programmes | Public hospitals, screening | Tenders for standard tubes |
| Blood Banks & Research | Screening, studies | Specialty and plain tubes |
The strongest position for a Blood Collection Tube Manufacturing Plant in India combines automated, high-speed production, consistent quality that laboratories trust, a complete range of tube types, regulatory approvals and ISO 13485 certification, competitive pricing, and strong relationships with diagnostic chains, hospitals, distributors, and government buyers. Producers that also offer needles and holders can sell complete collection systems.
Blood Collection Tube Manufacturing Process Flow
Understanding the Blood Collection Tube Manufacturing Process helps promoters plan moulding, cleanroom operations, vacuum capping, sterilisation, layout, staffing, and quality control. Product performance depends on tube dimensional accuracy and clarity, precise additive dosing and drying, correct vacuum level and seal integrity, reliable stoppers, validated sterilisation, and rigorous testing. The flow below reflects a typical automated PET tube plant.
Step-by-Step Blood Collection Tube Production Flow
PET resin is dried and moulded into tubes, and caps are moulded and fitted with rubber stoppers. Tubes are inspected, then additives are sprayed, dosed, or dispensed and dried in a cleanroom. Tubes are evacuated and capped under vacuum, labelled, packed, sterilised, and tested for draw volume, vacuum, additive content, and sterility before release.
| Unit Operation | Key Activity |
|---|---|
| Resin Drying & Tube Moulding | Mould PET tubes |
| Cap & Stopper Preparation | Mould caps, fit stoppers |
| Tube Inspection | Vision checks for defects |
| Additive Preparation | Prepare EDTA, citrate, gel, activators |
| Additive Dosing & Coating | Spray, dose, or dispense additives |
| Drying | Dry coated additives |
| Vacuum Evacuation & Capping | Set draw volume, seal tube |
| Labelling & Packing | Lot, expiry, fill line, racks |
| Sterilisation | Gamma irradiation |
| Quality Testing & Release | Draw volume, vacuum, sterility |
Two factors decide profitability. The first is quality consistency laboratories switch suppliers only when they trust that draw volumes, additive concentrations, and sample quality are consistent, so precise dosing, vacuum control, and validated processes are the foundation of sales. The second is automation and scale: tubes sell at low unit prices in very high volumes, so high-speed moulding and assembly, low rejection rates, and high utilisation determine unit cost and margins.
Raw Materials Required for Blood Collection Tube Manufacturing
The main inputs are medical-grade PET resin, polyethylene or polypropylene for caps, butyl rubber stoppers, additives such as EDTA, sodium citrate, heparin, clot activators, separator gel, and sodium fluoride, labels, and packaging. IMARC Group estimates raw materials at 45 to 50% of operating cost, primarily PET or glass, and utilities at 12 to 15%.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Medical-Grade PET Resin | Tube body | Domestic and imported resin suppliers | 14–18% |
| Butyl Rubber Stoppers | Seal and vacuum retention | Domestic and imported | 8–11% |
| PE / PP Resin for Caps | Colour-coded closures | Domestic petrochemical producers | 4–6% |
| Additives (EDTA, Citrate, Heparin, Gel, Activators, Fluoride) | Sample preservation and separation | Specialty chemical suppliers | 6–9% |
| Labels, Racks, Trays & Cartons | Identification and packing | Domestic suppliers | 4–6% |
Medical-grade PET and caps are available from domestic suppliers, while specialised butyl stoppers, separator gels, and some high-purity additives are partly imported, so qualifying reliable suppliers, maintaining certificates of analysis, and testing every lot are essential. Long-term supply agreements and dual sourcing for stoppers and gel reduce supply risk and support consistent product performance.
Location, Land & Infrastructure
Location shapes access to medical device infrastructure, skilled staff, and customers. The best location for Blood Collection Tube manufacturing plant setup lies in a medical device park or pharmaceutical and plastics cluster with common testing and sterilisation facilities, reliable power and purified water, a trained workforce familiar with cleanroom operations, and good logistics to major diagnostic markets.
Preferred States for Blood Collection Tube Plants in India
| State | Why It Works | Key Advantage |
|---|---|---|
| Andhra Pradesh | AMTZ medical device park in Visakhapatnam | Common facilities, testing, incentives |
| Telangana | Medical devices park near Hyderabad | Life sciences ecosystem |
| Tamil Nadu | Chennai medical device and plastics cluster | Automated tube manufacturing base |
| Gujarat | Medical device and pharma clusters | Industry presence, ports |
| Haryana | Faridabad and NCR medical consumables cluster | Established device makers, NCR market |
| Himachal Pradesh | Medical device park at Nalagarh | Incentives, pharma ecosystem |
Andhra Pradesh and Telangana host dedicated medical device parks with shared testing, sterilisation, and regulatory support, while Tamil Nadu's Chennai region already hosts automated blood collection tube manufacturing. Gujarat, Haryana, and Himachal Pradesh offer established pharmaceutical and medical consumables ecosystems and state incentives. Access to contract gamma sterilisation and accredited testing laboratories is an important factor in site selection.
Quality, Regulatory and Cleanroom Requirements
Blood collection tubes are medical devices that must be manufactured under an ISO 13485 quality management system and licensed under India's Medical Devices Rules, 2017, with performance aligned to international standards for venous blood specimen containers such as ISO 6710. Additive processing and assembly take place in classified cleanrooms, and sterilisation must be validated. Key controls include incoming material testing, in-process checks of dimensions and additive dosing, vacuum and draw volume testing, seal integrity and leak tests, sterility and bioburden testing, stability studies for shelf life, and full lot traceability with complaint handling and post-market surveillance.
Infrastructure Requirements (100 Million Tubes a Year Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 2 – 3 acres | Factory, warehouse, expansion |
| Factory Building | 4,000 – 6,000 m² | Moulding, assembly, warehouse |
| Cleanroom | 800 – 1,500 m², ISO Class 8 | Additive dosing and assembly |
| Power | 1 – 1.8 MW connected load | Moulding, HVAC, assembly lines |
| Purified Water | 20 – 40 KLD | Additive preparation, cleaning |
| Quality and Microbiology Laboratory | Physical, chemical, sterility tests | Regulatory compliance |
| Warehouse | Raw material and finished goods | Controlled temperature and quarantine areas |
Infrastructure for a blood collection tube plant centres on an injection moulding hall with resin dryers and chillers, a classified cleanroom for additive processing and vacuum capping, labelling and packing lines, quarantine and finished goods warehouses, a quality and microbiology laboratory, HVAC and purified water systems, and arrangements for gamma sterilisation. Planning space for additional moulding and assembly lines and a needle and holder unit supports future growth.
Blood Collection Tube Manufacturing Machinery and Equipment
High-speed injection moulding machines, multi-cavity hot-runner moulds, and fully automatic tube assembly lines are mostly imported from Europe, Japan, and China, while auxiliary equipment, cleanroom systems, and packing machines are widely available in India. The main equipment is summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| PET Injection Moulding Machines & Hot-Runner Moulds | Mould tubes | High cavitation, fast cycles |
| Cap / Closure Moulding Machines | Mould colour-coded caps | Multi-cavity moulds |
| Resin Dryers & Chillers | Prepare resin, cool moulds | Dew point control |
| Vision Inspection Systems | Detect tube and cap defects | Inline cameras |
| Additive Spray, Dosing & Drying Machines | Apply additives | High-precision dosing |
| Gel Dispensing Machines | Dispense separator gel | Accurate volume control |
| Automatic Vacuum Capping & Assembly Lines | Evacuate and seal tubes | Controlled vacuum levels |
| Labelling & Printing Machines | Label and code tubes | Lot, expiry, fill line |
| Rack Loading & Packing Machines | Pack tubes | Racks, trays, cartons |
| Cleanroom HVAC & QC Laboratory Equipment | Control environment, test products | Vacuum testers, sterility testing |
Equipment selection should follow capacity and product range. Moulding capacity and mould quality largely determine tube output and consistency, while dosing and vacuum capping lines determine product performance. Many promoters begin with bought-in tubes or a single moulding line plus semi-automatic dosing and capping for high-volume tube types, adding high-cavitation moulding, fully automatic assembly, and in-house closure production as volumes and approvals grow.
Blood Collection Tube Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below summarise the capital and operating cost structure of a blood collection tube plant producing about 100 million tubes a year in India. The final Blood Collection Tube Investment Cost for a specific project depends on capacity, degree of automation, number of moulds and lines, cleanroom area, sterilisation arrangements, validation and regulatory costs, land and building costs, and working capital for materials and distributor receivables.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Injection Moulding & Moulds | 28–35% | Tube and cap moulding machines, hot-runner moulds |
| Additive Dosing, Assembly & Vacuum Capping | 18–24% | Dosing, drying, gel, capping lines |
| Cleanroom & HVAC | 10–14% | Classified cleanroom, air handling |
| Labelling, Inspection & Packing | 5–8% | Vision systems, labellers, packers |
| QC Laboratory & Validation | 4–6% | Lab equipment, process validation |
| Land & Buildings | 8–12% | Factory, warehouse, offices |
| Working Capital | 12–18% | Materials, finished stock, receivables |
Moulding and automated assembly equipment account for most of the fixed investment, while cleanroom and validation costs are significant for regulatory compliance. A Blood Collection Tube Business Plan models these components so that capacity, product mix, and financing rest on realistic sales, pricing, and regulatory timeline assumptions.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials | 45–50% | PET, stoppers, additives |
| Utilities | 12–15% | Moulding, HVAC, compressed air |
| Labour | 8–12% | Operators, QA, microbiologists |
| Sterilisation | 4–6% | Contract gamma irradiation |
| Sales, Distribution & Regulatory | 6–9% | Distributor margins, tenders, compliance |
| Maintenance & Overheads | 3–5% | Moulds, machines, admin |
With raw materials and utilities forming the largest costs, profitability depends on resin and stopper prices, moulding efficiency, rejection rates, sterilisation costs, product mix, and pricing against imported and domestic competitors. A sound financial model should test margins against lower selling prices in tenders, raw material cost increases, slower regulatory approvals, and longer payment cycles from hospitals and distributors.
Financial Analysis and Profitability
Blood collection tube manufacturing offers strong returns for producers that combine automation, quality, and market access. The profitability of Blood Collection Tube manufacturing business in India improves with high-speed moulding and assembly, low rejection rates, a complete tube range, ISO 13485 and regulatory approvals, export certifications, supply contracts with diagnostic chains and hospitals, participation in government tenders, and the addition of needles and holders for complete collection systems.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 40–50% | IMARC benchmark |
| Net Profit Margin | 15–20% | After depreciation and Indian corporate taxes |
| Payback Period | 3–5 Years | High-volume consumable |
| IRR (Internal Rate of Return) | 20–26% | Sensitive to pricing and utilisation |
| Capacity Utilization (stable ops) | 65–85% | Grows with laboratory approvals |
| Break-even Capacity Utilization | 35–45% | Moderate fixed costs |
Quality trust and scale are the decisive factors. Laboratories are cautious about changing tube suppliers because sample quality affects test results, so manufacturers must demonstrate consistent performance through evaluations and trials, then scale volume through diagnostic chains, hospital groups, and distributors. Automated producers with validated processes and competitive pricing can win share from imports.
Returns can be strengthened by investing in high-cavitation moulds and automatic assembly, validating processes thoroughly, offering a complete range including gel and citrate tubes, adding needles and holders, earning CE marking or other export approvals, partnering with large diagnostic chains, participating in government procurement, locating in medical device parks with shared facilities, and building a strong technical support team for laboratories.
Key Risks and Mitigation
The main risks are quality failures that affect test results, regulatory delays, price pressure in tenders and from imports, dependence on imported stoppers, gels, and moulds, sterilisation capacity constraints, and slow customer adoption. Quality risk is reduced through validated processes and rigorous testing; regulatory risk through early planning and experienced quality teams; price risk through automation and scale; supply risk through dual sourcing; sterilisation risk through contracts with multiple providers; and adoption risk through laboratory trials and technical support.
Licenses and Approvals for Blood Collection Tube Manufacturing in India
A blood collection tube unit requires medical device, quality, environmental, industrial, and business approvals. Promoters typically need the following before starting commercial sales:
- Medical Device Manufacturing License: License under the Medical Devices Rules, 2017, from the State Licensing Authority or CDSCO depending on the device risk class, preceded by a test license for samples.
- ISO 13485 Quality Management System: A quality management system compliant with ISO 13485 and the Fifth Schedule of the Medical Devices Rules.
- Product Standards and Validation: Performance aligned with standards such as ISO 6710, sterilisation validation, cleanroom qualification, and stability studies for shelf life.
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board.
- Factory License and Fire NOC: Factory registration and fire safety approval.
- Export Approvals: CE marking under the EU Medical Device Regulation, US FDA clearance, or other country registrations for export markets.
- Business Registrations: Company incorporation, GST, an Import Export Code, Udyam registration, and Government e-Marketplace registration for public procurement.
The medical device manufacturing license, ISO 13485 certification, and process validation usually sit on the critical path. Engaging a Blood Collection Tube Manufacturing Consultant in India can help promoters select machinery and automation levels, design cleanrooms and validation plans, prepare licensing documentation, and plan market entry with laboratories and distributors.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, product range, capacity, target customers, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Blood Collection Tube Manufacturing Industry
Several recent developments are shaping the Indian blood collection tube and medical device industry:
- Automated tube moulding in India: In September 2024, Kriya Medical Technologies unveiled its ICHOR Medical Molding System at its facility in the Oragadam Industrial Corridor, Chennai, a fully automated system designed to produce 250 million blood collection tubes a year.
- PLI progress for medical devices: In July 2026, the government reported that the PLI scheme for medical devices had 27 approved projects, including 14 MSMEs, with actual investment of Rs 1,153 crore and 23 projects commissioned.
- Import gap remains large: In August 2026, industry analysis estimated India's medical devices market at USD 18.3 billion in 2026, noting that FY 2024–25 imports of USD 8.8 billion were more than double exports of USD 4 billion.
Together these point to growing domestic capability in automated tube production, continued policy support for medical device manufacturing, and a large import gap that domestic producers can address. For new entrants, success depends on quality, automation, regulatory approvals, and strong laboratory relationships.
How Blood Collection Tube Manufacturing Project Report and DPR Helps Investors
A detailed Blood Collection Tube Project Report gives investors a structured roadmap covering demand by end user and region, competition and import trends, product range, process design, machinery and automation, cleanroom and utilities, raw material sourcing, sterilisation, quality systems, regulatory approvals, and economics. It helps promoters choose the right capacity, automation level, and product mix, estimate capital expenditure (CapEx) and operating expenditure (OpEx), assess profitability, and identify risks before implementation.
At the core of the DPR is a Blood Collection Tube Financial Model covering production and sales by tube type, selling prices by channel, resin, stopper, and additive costs, moulding and assembly yields, labour, power, sterilisation, regulatory and validation costs, distribution margins, working capital, cash flow projections, break-even, return on investment (ROI), and payback. Because pricing, utilisation, and regulatory timelines drive returns, lenders expect detailed sensitivity analysis, which is why many promoters engage a Blood Collection Tube Plant Project Report Consultant in India to prepare bank-ready documents.
For a blood collection tube project specifically, a strong DPR also answers the questions that matter most: which tube types and customers to target first, what level of automation suits the planned volume, how sterilisation will be arranged, how long licensing and laboratory evaluations will take, and how returns hold up if tender prices fall or approvals take longer. An experienced Blood Collection Tube Manufacturing Feasibility Study Consultant tests these scenarios so that the final plan is one lenders and partners can back with confidence.
Frequently Asked Questions
How do I set up a blood collection tube manufacturing factory in India?
Start by defining your tube range and target customers, then commission a feasibility study and DPR. Choose a site in a medical device park or healthcare cluster, install moulding, cleanroom dosing, vacuum capping, labelling, and packing equipment, arrange validated sterilisation, implement ISO 13485, obtain the medical device manufacturing license and other approvals, and complete laboratory evaluations before commercial supply.
What is the cost of setting up a blood collection tube manufacturing plant in India?
A plant producing about 100 million tubes a year typically needs INR 35 crore to INR 60 crore in fixed assets, or about INR 45 crore to INR 75 crore including working capital. A smaller semi-automatic unit of 20 to 30 million tubes a year can start at around INR 6 crore to INR 12 crore.
How are blood collection tubes made?
PET is moulded into tubes and caps are fitted with rubber stoppers. In a cleanroom, additives such as EDTA, citrate, clot activators, or gel are applied, then tubes are evacuated and capped under vacuum, labelled, packed, sterilised by gamma irradiation, and tested before release.
What machinery is needed for a blood collection tube manufacturing plant?
Key equipment includes PET injection moulding machines with hot-runner moulds, cap moulding machines, resin dryers and chillers, vision inspection systems, additive spray, dosing, and drying machines, gel dispensers, automatic vacuum capping and assembly lines, labelling machines, packing machines, cleanroom HVAC, and quality control laboratory equipment.
What raw materials are used in blood collection tube manufacturing?
The main inputs are medical-grade PET resin, PE or PP for caps, butyl rubber stoppers, additives such as EDTA, sodium citrate, lithium heparin, clot activators, separator gel, and sodium fluoride, labels, racks, and cartons.
Is blood collection tube manufacturing profitable in India?
Benchmark figures point to a 15 to 20% net margin and an IRR of around 20 to 26%, with payback in 3 to 5 years. Profitability depends mainly on quality consistency, automation, utilisation, pricing, and access to diagnostic laboratories and hospitals.
What licenses are needed for a blood collection tube manufacturing unit in India?
A unit typically needs a medical device manufacturing license under the Medical Devices Rules, 2017, ISO 13485 certification, process and sterilisation validation, State Pollution Control Board consents, a Factory License, a Fire NOC, GST, and export approvals such as CE marking where relevant.
Which state is best for a blood collection tube manufacturing plant?
Andhra Pradesh, Telangana, Tamil Nadu, Gujarat, Haryana, and Himachal Pradesh are strong options. The best site is in a medical device park or healthcare cluster with access to sterilisation, testing facilities, and skilled staff.
How do I get a feasibility study or DPR for a blood collection tube manufacturing plant?
A professionally prepared DPR covers market analysis, product and technical design, regulatory planning, costs, and financial projections for bank appraisal. Many promoters work with a Blood Collection Tube Business Plan Consultant in India to prepare it and align it with lender requirements.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

An HPMC Capsule Manufacturing Plant Setup in India produces plant-based, two-piece hard capsules made from hydroxypropyl methylcellulose, a cellulose derivative obtained from wood pulp or cotton.
A spirulina Manufacturing Plant Setup in India turns sunlight, water, carbon dioxide, and mineral nutrients into one of the most protein-dense foods available.
A Nicotine Pouches Manufacturing Plant Setup in India is one of the most regulation-sensitive projects an investor can consider. Nicotine pouches are small, tobacco-free pouches filled with plant fibres, a nicotine salt, flavours, and sweeteners, placed under the lip so that nicotine is absorbed through the gums.
The medical imaging market is a concentrated, capital-intensive oligopoly in which a handful of global vendors dominate high-value modalities, but the periphery of that structure is now moving. IMARC Group estimates the global medical imaging market at USD 49.0 Billion in 2026, up from USD 46.8 Billion in 2025, and projects it to reach USD 71.2 Billion by 2034, a CAGR of 4.78% during 2026-2034.
IV infusion bags are sterile, flexible plastic bags filled with fluids such as normal saline, dextrose, and Ringer lactate that are dripped directly into a patient's vein to restore fluids, salts, and energy or to dilute medicines.
The global orthopedic prosthetics market is moving away from a replacement-device business model and toward a capability-driven care model, in which fit, function and follow-up data determine whether a device delivers value. According to IMARC Group, the market was valued at USD 2.5 Billion in 2025 and is projected to reach USD 3.5 Billion by 2034, expanding at a CAGR of 3.61% between 2026 and 2034.
Health supplements and functional nutrition products are made by blending vitamins, minerals, proteins, probiotics, and botanical extracts and turning them into tablets, capsules, softgels, powders, gummies, and drinks under food-grade good manufacturing practices.
Generic medicines are copies of off-patent brands that contain the same active ingredient, strength, dosage form, and effect, and are approved on the basis of bioequivalence rather than new clinical trials, so they reach patients at a fraction of the original price.
The UK Health Insurance Market is at an inflection point, shaped by the mounting strain on the National Health Service and a structural shift in how employers and individuals seek to protect their health. According to IMARC Group, the market was valued at USD 67.2 Billion in 2025 to USD 70.9 Billion in 2026 and is projected to reach USD 98.6 Billion by 2034, growing at a CAGR of 4.21% (2026–2034).
Single-use syringes are sterile medical devices made from a moulded plastic barrel and plunger, a rubber gasket, and usually a fine stainless steel needle, and they are used once and discarded to prevent infection.
Absorbent cotton wool is raw cotton that has been cleaned, scoured, and bleached to remove natural waxes, oils, and impurities, then carded into soft, pure white layers that absorb many times their own weight in liquid.
Generic formulations are finished medicines, such as tablets and capsules, that contain the same active ingredient, strength, and effect as an original brand once its patent expires.
IV solutions, also called intravenous fluids or large volume parenterals, are sterile solutions given directly into a patient's vein to restore fluids and electrolytes, provide nutrition, or deliver medicines.
Paracetamol, also called acetaminophen, is one of the world's most widely used medicines for pain and fever, sold in tablets, syrups, suspensions, injections, and combination products.
Ayurveda is India's traditional system of medicine, and Ayurvedic medicines are made from herbs, minerals, and natural bases such as ghee, oils, honey, and jaggery, following classical texts and modern quality standards.
The Europe Medical Cannabis Industry has moved decisively from a patchwork of national pilot programmes into a credentialed pharmaceutical market with prescriptions, import quotas, reimbursement pathways and EU-GMP supply chains. According to IMARC Group, the market reached USD 3,060.0 Million in 2025 and is projected to reach USD 13,161.29 Million by 2034, expanding at a CAGR of 17.60% (2026–2034).
Workplace wellbeing in Asia-Pacific has shifted from a discretionary benefit to something employers are measured on, by regulators, insurers, and the talent market alike. According to IMARC Group, the Corporate Wellness Market was valued at USD 75.0 Billion in 2025 and is projected to reach USD 129.5 Billion by 2034, growing at a CAGR of 6.07% (2026–2034).
The Europe Digital Health Industry has become the continent's principal answer to a demographic and fiscal problem that hospitals alone cannot solve: ageing populations, rising chronic-disease burdens and persistent clinical staff shortages, set against public health budgets that cannot expand at the same pace as demand.
For two decades India bought most of its medical technology from abroad. The government's own assessment put import dependence at more than 85% of the market in 2020, and the country's role was that of a large consumer rather than a producer. That position is now changing, as incentive schemes, multinational localization, and domestic innovation turn the Indian medical devices sector into a manufacturing and export base.
Rapid diagnostic tests deliver results in minutes, without laboratory equipment, at a clinic, pharmacy, field camp, or at home. Lateral flow tests for malaria, dengue, typhoid, HIV, hepatitis, syphilis, pregnancy, fertility, drugs of abuse, and cardiac markers have become an essential part of India's healthcare system, especially in primary care and rural areas where laboratories are scarce.
Setting up a Generic Injectables Manufacturing Plant in India is a high-value, highly regulated venture, powered by the country's position as the pharmacy of the world, growing global demand for affordable injectables, and a wave of patent expiries opening new products to generic competition.
Setting up a Pharmaceutical Manufacturing Plant in India is a high-potential, strategically strong venture, powered by the country's position as the pharmacy of the world and one of the largest generic drug producers globally. India's deep formulation expertise, cost competitiveness, and vast domestic and export demand make a pharmaceutical manufacturing unit setup in India one of the most attractive opportunities in the healthcare sector.
The Dental 3D Printing Market is attracting renewed investor attention because the technology has moved from a promising adjunct to a default production method inside dental laboratories and clinics.
Vitamin water is a functional, non-carbonated beverage that is created by the fortification of purified water with a combination of vitamins, minerals, and sometimes electrolytes, along with natural or artificial flavors and sweeteners. It is placed in a category between bottled water and carbonated soft drinks, providing hydration with a functional twist.
Vitamin B12, or cobalamin, is a water-soluble vitamin that contains the metal cobalt and is a micronutrient required by the human body. It acts as a coenzyme in the synthesis of DNA, the production of red blood cells, and the functioning of the nervous system.
Japan's dietary supplements industry has become one of the most advanced and innovation-led industries in the world. It is at the nexus of science, culture, and consumer health awareness.
A syringe is a medical instrument that is used to inject fluids into the body or to withdraw fluids from the body. A syringe usually has a cylindrical body, a plunger that moves inside the body to generate pressure or suction, and a nozzle to which a needle can be attached.
Cosmetic surgery in Australia today has evolved into a significant element of the greater beauty and wellness economy. Changing cultural attitudes, advances in medical aesthetics, and the rise of social media over the last ten years have reconstituted the ways in which cosmetic surgery is perceived and undertaken by Australians.
The contact lenses market represents a dynamic segment of the global vision care industry, characterized by continuous innovation and expanding demographic demand.
Brazil's diagnostic imaging equipment market stands at a pivotal moment as Latin America's largest and most dynamic healthcare arena. With substantial investments in hospital modernization, regulatory reforms, and artificial intelligence adoption, the market is transforming rapidly. As providers transition from analog to AI-ready platforms, Brazil emerges as a critical destination for medical device manufacturers seeking growth through the next decade.
The Indian healthcare space has indeed been changing. Telemedicine has emerged as one of the most important drivers of this change. Driving this transformation is the increased adoption of digital tools, growing patient awareness, and the pressing need to make healthcare more accessible across diverse geographies.
The Australia medical aesthetics industry size reached USD 396.4 Million in 2025. Looking forward, the market is expected to reach USD 784.8 Million by 2034, exhibiting a growth rate (CAGR) of 7.89% during 2026-2034. Over the last ten years, the medical aesthetic industry in Australia has transformed from a niche beauty service into a mainstream part of healthcare and wellness.
A rapid diagnostic test (RDT) kit is a medical device designed to quickly detect specific biomarkers, antigens, antibodies, or nucleic acids linked to diseases—typically within minutes and without the need for sophisticated laboratory equipment. These kits often use lateral flow assays, immunochromatographic strips, or rapid molecular testing methods to deliver fast and reliable results.
The Philippines pharmaceutical industry stands as one of Southeast Asia's most dynamic and rapidly expanding healthcare markets in the ASEAN region. With a market valuation reaching USD 3.36 Billion in 2025, the sector demonstrates resilience and tremendous growth potential.
Pharmaceuticals are medical products, substances, or formulations involved in the development, manufacture, and regulation for the prevention, diagnosis, treatment, and management of diseases in humans as well as animals.
The Australia aged care industry stands at a pivotal juncture as the nation grapples with demographic shifts that are reshaping the landscape of elderly care services. With an aging population that continues to expand, Australia faces both unprecedented challenges and remarkable opportunities in delivering quality care to its senior citizens.
The Indian vaccines industry holds an unparalleled position globally, often celebrated as the pharmacy of the world due and its massive production scale and capabilities. It reached INR 113.7 Billion in 2024 according to IMARC Group and it is projected to grow at a CAGR of 8.8% from 2025-2033.
The medical imaging market has reached a transformational phase, driven both by rapid technological advancements and growing demands for precision-driven diagnostics. As health systems worldwide come under increasing pressure to improve patient outcomes while minimizing procedural risks and optimizing clinical workflows, medical imaging has become one of the most important cornerstones of modern medicine.
India’s medical devices industry is on a sustained growth trajectory driven by expanding hospital infrastructure, rising chronic disease burden, stronger local manufacturing supported by government incentives, and a rapidly growing shift toward portable and home care devices.
Pectin represents a naturally occurring polysaccharide mainly extracted from cell walls of fruits (mainly from citrus peel and apple pomace). It is a soluble dietary fiber and a hydrocolloid with gelling, thickening, and stabilizing properties. It is mostly composed of galacturonic acid units.
Paracetamol, also referred to as acetaminophen, is an analgesic and antipyretic compound that is commonly used worldwide for the treatment of mild to moderate pain and the management of fever. The mechanism of action occurs mainly in the central nervous system, where it inhibits the mechanisms that regulate pain and body temperature, but lacks anti-inflammatory properties.
The Australia wellness tourism industry has emerged as a critical segment of the country’s broader travel and hospitality sector. It reflects a growing global emphasis on health, self-care, and holistic well-being, capturing the attention of travelers seeking experiences that combine relaxation, rejuvenation, and personal growth.
The Brazil cardiovascular devices market represents a crucial segment in the country’s healthcare ecosystem, addressing one of the leading causes of morbidity and mortality: cardiovascular diseases. Conditions such as heart attacks, stroke, arrhythmias, and heart failure require ongoing medical intervention and advanced heart disease treatment solutions. With the rising prevalence of cardiovascular disorders, demand for comprehensive cardiac care equipment and innovative treatment modalities is increasing.
India's Ayurvedic products market is experiencing remarkable transformation as consumers increasingly prioritize holistic wellness and natural remedies over conventional alternatives. The convergence of traditional healing wisdom with modern consumer preferences has created a dynamic landscape where herbal medicines, chemical-free personal care products, and immunity-boosting supplements are becoming household staples.
Nicotine pouches are small, smokeless oral delivery products of nicotine, free from tobacco, designed to allow for controlled release of the active principle without burning, vaporizing, or use of traditional tobacco leaves. It consists of a small pouch that contains a matrix made basically from plant fibers, flavorings, pH adjusters, and stabilizers impregnated with nicotine, encased in a permeable material permitting the gradual absorption of the product via the oral mucosa.
The pharmaceutical industry in Japan is among the most advanced globally, recognized for combining innovation, high-quality standards, and patient-centered care. Its extensive value chain includes drug discovery, clinical trials, manufacturing, distribution, marketing, and post-market surveillance. Serving both domestic and international markets, Japanese pharmaceutical companies are respected for regulatory compliance, safety, and reliability, establishing them as trusted global collaborators in drug development.
The pharmaceutical industry in Japan is among the most advanced globally, recognized for combining innovation, high-quality standards, and patient-centered care. Its extensive value chain includes drug discovery, clinical trials, manufacturing, distribution, marketing, and post-market surveillance. Serving both domestic and international markets, Japanese pharmaceutical companies are respected for regulatory compliance, safety, and reliability, establishing them as trusted global collaborators in drug development.
The global healthcare IT industry is on a remarkable upswing, fueled by the surge in preventive care, digital health platforms, and smarter patient management systems. According to IMARC Group, the market hit USD 363.15 Billion in 2024, a clear sign of worldwide adoption. An aging population, the growing comfort with remote care, and the push toward personalized medicine are all speeding this momentum.
The global endoscopy devices market is on a sharp growth path, fueled by the shift toward minimally invasive procedures, the need for early diagnosis, and cutting-edge imaging technologies. IMARC Group reported the market hit USD 50.01 Billion in 2024, underscoring its worldwide acceptance.
The global business-to-business (B2B) payments landscape is experiencing a fundamental transformation that is reshaping how enterprises conduct financial transactions across borders and industries. The market, valued at approximately 1,189.6 Billion in 2024, is projecting remarkable growth with expectations to reach USD 2,189.0 Billion by 2033, exhibiting a CAGR of 7% from 2025-2033. This exponential expansion is signaling a paradigm shift in commercial finance, driven by technological innovation, changing business expectations, and the urgent need for more efficient payment infrastructures.
The smart medical devices market is entering a decade defined by connected care, real-time diagnostics, and patient empowerment. Valued at USD 45.9 Billion in 2024, the market is projected to reach USD 82 Billion by 2033, expanding at a compound annual growth rate (CAGR) of 6.33% between 2025 and 2033 by IMARC Group. This steady rise reflects growing confidence in data-driven healthcare systems, integration of IoT in medical environments, and the increasing role of artificial intelligence in clinical decision-making.
Active Pharmaceutical Ingredients (APIs) are the bioactive molecules of any drug used in pharmaceuticals, which cause the desired therapeutic action in the body of a human being. APIs are the central core of all drugs, chemical or biological and are responsible for the efficacy, strength, and safety of the drug. APIs are synthesized by various complex chemical synthesis, fermentation, biotechnological, or extraction processes based on the type of drug.
A bio medical incinerator is a high-temperature combustion system specialized for biomedical waste disposal by hospitals, clinics, laboratories, and research institutions. Biomedical waste usually consists of infectious waste, pathological waste, sharps, pharmaceuticals, and contaminated disposables that are very hazardous to human health and the environment if not treated.
Obesity, once viewed primarily as a lifestyle choice, is now widely recognized as a complex and chronic disease characterized by excessive body fat accumulation. Its global prevalence is escalating at an alarming rate posing a significant and growing challenge to public health systems worldwide.
Gonorrhea, a sexually transmitted infection caused by the bacterium Neisseria gonorrhoeae, is a major public health issue globally. Reports show that over one million new cases of curable STIs are contracted every day by individuals aged 15 to 49 years, with the majority being asymptomatic.
The 7 major allergic conjunctivitis markets reached a value of USD 2.1 Billion in 2024. Looking forward, IMARC Group expects the 7MM to reach USD 2.9 Billion by 2035, exhibiting a growth rate (CAGR) of 3.00% during 2025-2035.
The healthcare sector is changing rapidly because of the growing demand for better ways to manage chronic diseases. As we move toward 2025 and beyond, digital tools are playing an important role in dealing with conditions like diabetes, heart disease, cancer, and respiratory problems.
The global multivitamin gummies market consists of chewable dietary supplements that are charged with key vitamins and minerals aimed at maintaining general health and wellness. The gummies present a handy, enjoyable, and easy-to-swallow option to classic pills or tablets, hence are predominantly preferred by children and adults who do not like taking pills.
India's pharmaceutical sector is evolving rapidly, supported by the integration of artificial intelligence (AI) across the value chain. As of 2023, India ranked as the third-largest pharmaceutical producer by volume, accounting for 20% of global generic drug exports.
As Lung Cancer Awareness continues to build global momentum in 2025, Artificial Intelligence (AI) is proving to be a transformative force—not only in clinical diagnostics but also in public education and preventive health efforts. Given that lung cancer remains one of the world’s deadliest cancers, accounting for over 1.8 million deaths each year and a five-year survival rate of just 28.4%, the integration of AI marks a critical turning point.
Observed on May 19, Hepatitis Testing Day 2025 emphasizes the need to "Test. Treat. Eliminate," highlighting the gap in diagnosing hepatitis B and C, which cause over 1.3 million deaths annually. Hepatitis remains a major global health threat, on par with HIV, tuberculosis, and malaria. The growing viral hepatitis market <Viral Hepatitis Market Size | Share, Trends - 2034 > reflects rising demand for better diagnostics, treatments, and integrated care. The WHO warns that without faster testing and treatment, the goal of eliminating hepatitis by 2030 may not be achieved, with disparities in diagnostics, particularly in low- and middle-income countries, hindering progress.
Observed on May 8, World Ovarian Cancer Day 2025 carries the theme “No Woman Left Behind,” reinforcing the urgent need to close the gaps in access, diagnosis, treatment, and care across all regions and socioeconomic groups. Ovarian cancer remains one of the deadliest gynecological cancers, often detected too late due to vague symptoms and limited screening tools. The World Ovarian Cancer Coalition projects a 55% rise in annual cases and nearly 70% more deaths by 2050, with the heaviest burden falling on low- and middle-income countries. Equitable access to early diagnostics, genetic testing, and targeted therapies is critical.
In clinics around the world, a concerning pattern is becoming increasingly evident: a growing number of patients are experiencing wheezing, breathlessness, and persistent coughing. This surge reflects a broader global trend. According to the World Health Organization (WHO), more than 260 million people are currently living with asthma, making it one of the most widespread and persistent chronic respiratory conditions globally.
Observed on April 25, World Malaria Day 2025 carries the theme “Accelerating Equity in Malaria Prevention and Cure,” underscoring the urgent need to reach communities still lacking access to life-saving vaccines and diagnostics. While global malaria death rates have seen modest declines, the disease continues to claim the life of one child every minute, highlighting the critical need for swift, equity-driven action
Sulfamethoxazole is a common synthetic antibacterial that is a member of the sulfonamide class of antibiotics. This substance plays a very significant role in modern medicine due to the amazing capabilities offered by the substance for curing infections and bacterial diseases. Trimethoprim and sulfamethoxazole are frequently used together to create the well-known antibiotic co-trimoxazole, which is well-known for its potency against a variety of bacterial infections. It works by preventing the manufacture of folic acid, which is necessary for the growth of bacteria. Sulfamethoxazole is an essential part of modern antibiotic therapy since it has been used to treat lung infections, urinary tract infections, and other common bacterial illnesses.
Healthcare consumables are necessary medical supplies used for patient treatment, diagnostics, and cleanliness in clinics, hospitals, and home care settings. These consist of supplies such as surgical masks, bandages, gloves, syringes, catheters, and disinfectants. Usually, they are disposable or single use to preserve sterility and stop infections. Healthcare consumables are an essential component of the global healthcare ecosystem and are in high demand due to expanding healthcare needs, an increase in operations, infection control measures, and technological improvements.
Catheters are flexible, tubular medical devices designed to access various body cavities, organs, or blood vessels for diagnostic or therapeutic purposes. They can be broadly classified into types based on their application, including urinary catheters, cardiac catheters, and intravenous (IV) catheters. Catheters are commonly used in diverse healthcare settings for managing chronic conditions, enabling fluid drainage, delivering medications, or facilitating minimally invasive surgeries.
Bioinformatics involves applying computational techniques and tools to study and understand biological systems at the molecular level. It is a field of study that combines mathematics, biology, computer science, and statistics to research genomic data and biological networks. The goal is to interpret information from large biological data sets, such as DNA sequences, protein structures, gene expressions, and other high-throughput experimental data. This field provides various products and services, such as knowledge management tools, bioinformatics platforms, and services.
A non-animal model refers to an experimental system or method used in scientific research or testing that does not involve the use of animals. These models are developed to simulate biological processes, test hypotheses, or study diseases without the need for live animals. The aim is often to reduce the reliance on animal testing, which has ethical implications and raises concerns about animal welfare.
Cell therapy involves the transplantation and manipulation of living cells to replace and repair damaged tissue. Its primary branches include stem cell therapy and non-stem cell therapy. Stem cell therapy utilizes stem cells to repair, replace, or rejuvenate damaged or diseased cells and tissues as they possess the ability to differentiate into various specialized cell types, making them valuable for regenerative medicine. Non-stem cell-based therapies typically involve somatic cells isolated from the human body. These cells are propagated, expanded, selected, and then administered to patients for curative, preventive, or diagnostic purposes. On the other hand, gene therapy seeks to treat diseases by introducing, replacing, or inactivating genes within cells.