ERW Steel Pipes Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
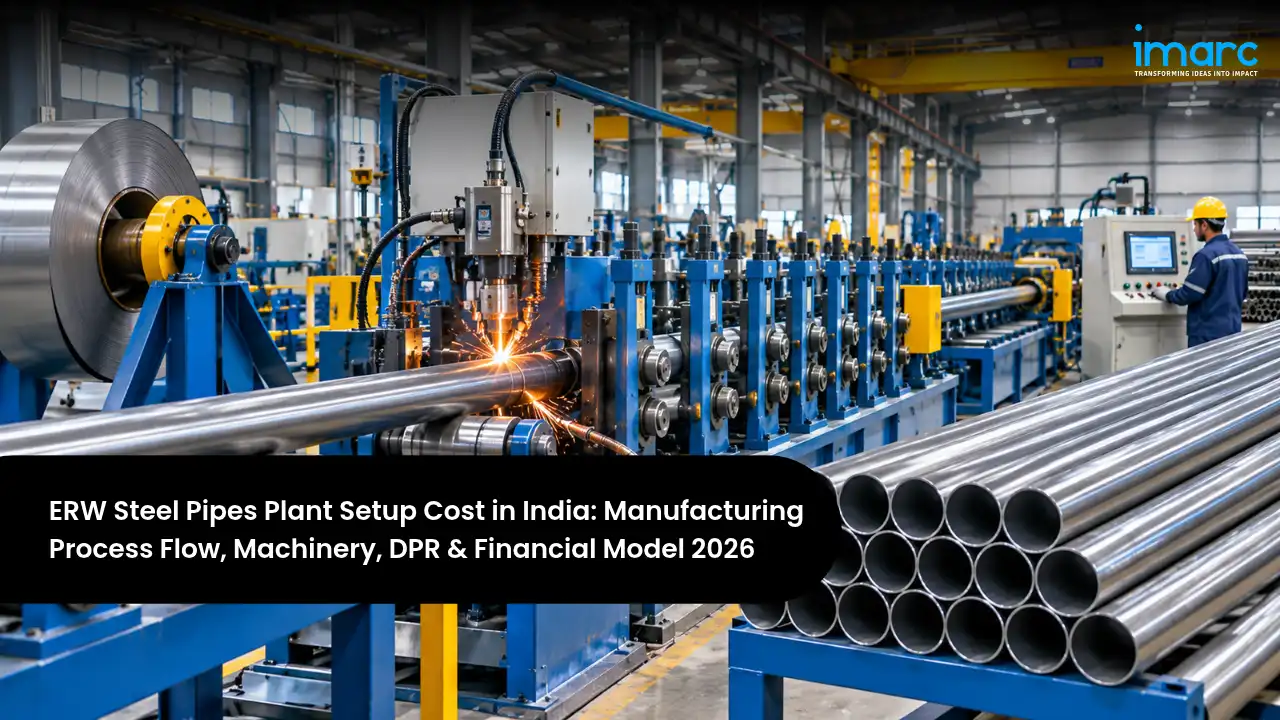
An ERW Steel Pipes Manufacturing Plant Setup in India serves one of the broadest demand bases in the steel value chain. Electric resistance welded (ERW) pipes are made by cold-forming hot-rolled steel strip into a tube and welding the seam with high-frequency current, without any filler metal. The result is an economical, dimensionally accurate pipe or hollow section used in water supply, gas distribution, building structures, scaffolding, solar mounting structures, irrigation, fencing, furniture, automotive parts, and general engineering. ERW products account for roughly half of India's steel pipe market by volume, making them the workhorse of the sector.
The overall ERW Steel Pipes Manufacturing Plant Cost depends mainly on capacity, the size range of the tube mills, and whether the plant adds galvanising, coating, or line pipe testing facilities, with total investment ranging from about INR 15 crore for a compact plant of around 24,000 tonnes a year to INR 150 crore or more for an integrated plant of 1 to 3 lakh tonnes. Hot-rolled steel coil makes up 75 to 85% of operating cost, so margins depend on buying steel well and converting it efficiently. Industry benchmarks point to gross margins of 15 to 25% and net margins of 5 to 10%, with returns driven by volume, product mix, and brand strength.
This guide is written for steel traders, fabricators, secondary steel producers, and investors exploring how to start an ERW Steel Pipes manufacturing plant in India. It covers product types and markets, demand drivers, the forming and welding process, machinery and raw materials, site and infrastructure planning, a detailed cost and returns breakdown, the approvals involved, and how a DPR brings these elements into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| India Steel Pipes Market | About 14.6 Million Tonnes (2025) |
| Market Outlook | About 28.7 Million Tonnes by 2034, 7.41% CAGR |
| ERW Share of Steel Pipes | Around 52% by volume |
| Main Raw Material | Hot-rolled steel coil (HRC) |
| Indicative Total Investment | INR 15–150 Crore |
| Typical Payback Period | 3–5 Years |
The snapshot shows a market expected to nearly double in volume over the next decade, with ERW pipes holding the largest share. Growth is broad-based, spanning construction, water, energy, agriculture, and manufacturing, and leading producers continue to add capacity across regions. The investment range reflects the difference between a single-mill plant serving a regional market and a multi-mill plant with galvanising and large-diameter capability.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Black and GI pipes, hollow sections, water and line pipes, precision tubes |
| Total Project Investment | INR 15 – 150 Crore (24,000–3,00,000 TPA) |
| Payback Period | 3 – 5 Years |
| Net Profit Margin | 5 – 10% |
| IRR | 14 – 20% |
| Best Locations | Uttar Pradesh, Chhattisgarh, Gujarat, Maharashtra, Andhra Pradesh, Punjab & Haryana |
| Mandatory Approvals | BIS License, SPCB Consents, Factory License, Hazardous Waste Authorisation, GST |
| Key Requirement | Steady HRC supply and strong dealer or project network |
These figures provide a practical frame for early evaluation. Returns depend on sourcing HRC at competitive prices, maintaining high mill speeds and yields, building a product mix that includes value-added items such as galvanised pipes and hollow sections, and selling through a strong dealer network and project channels. A capacity- and market-specific ERW Steel Pipes Feasibility Report refines these figures before capital is committed.
Table of Contents
- What is ERW Steel Pipes Manufacturing?
- Why is ERW Steel Pipes Manufacturing Growing in India?
- ERW Steel Pipes Manufacturing Process Flow
- Raw Materials Required for ERW Steel Pipes Manufacturing
- Location, Land & Infrastructure
- ERW Steel Pipes Manufacturing Machinery and Equipment
- ERW Steel Pipes Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for ERW Steel Pipes Manufacturing in India
- Recent Developments in the India ERW Steel Pipes Manufacturing Industry
- How ERW Steel Pipes Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is ERW Steel Pipes Manufacturing?
ERW pipe production begins with hot-rolled steel coil, which is slit into strips of the required width. Each strip is uncoiled, joined end to end, and fed through a series of forming rolls that gradually shape it into an open round tube. The edges are heated by high-frequency induction or contact welding and forged together by squeeze rolls, forming a solid seam. The weld bead is trimmed, the pipe is sized, cut to length, straightened, tested, and finished. An ERW Steel Pipes Manufacturing Plant therefore combines coil processing, continuous roll forming, high-frequency welding, sizing, testing, and optional galvanising or coating in one flow.
Commercially, ERW pipes and tubes sell to a wide range of buyers: dealers and distributors serving plumbing and construction, infrastructure contractors, water utilities, city gas distribution companies, solar EPC firms, fabricators, furniture and automotive component makers, and exporters. Strong brands and wide distribution networks command a premium in this otherwise competitive market.
- Black and GI Pipes: Pipes for water, gas, and general use, supplied plain or hot-dip galvanised for corrosion resistance.
- Hollow Sections: Square and rectangular sections for building structures, sheds, frames, and fabrication.
- Water and Line Pipes: Larger-diameter pipes for water mains, sewage, and oil and gas transport.
- Precision and Mechanical Tubes: Tubes for automotive, furniture, cycles, conveyors, and engineering uses.
Main Product Types in ERW Steel Pipe Production
The product mix determines mill size, finishing lines, and margins:
| Product Type | Description | Key Property | Primary Demand |
|---|---|---|---|
| GI & Black Pipes | Round pipes, plain or galvanised | Corrosion resistance, versatility | Plumbing, construction, irrigation |
| Structural Hollow Sections | Square and rectangular tubes | Strength-to-weight ratio | Buildings, sheds, solar structures |
| Water & Sewage Pipes | Larger-diameter pipes | Pressure rating | Water utilities, municipal projects |
| Line Pipes | API and ISO grade pipes | Weld integrity, toughness | Oil, gas, city gas distribution |
| Precision Tubes | Tight-tolerance tubes | Dimensional accuracy | Automotive, furniture, engineering |
Many new plants begin with GI and black pipes or hollow sections in popular sizes, which sell in large volumes through dealers. As they grow, they add larger-diameter mills, galvanising, coated pipes, and certified line pipes, which earn better margins but require more investment, testing, and certification. Planning mill size ranges with this progression in mind helps avoid early re-equipment.
Why is ERW Steel Pipes Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
Demand for ERW pipes in India is driven by infrastructure, housing, water, and energy programmes. IMARC Group estimates India's steel pipes market at about 14.6 million tonnes in 2025, rising to about 28.7 million tonnes by 2034:
- Construction and structural steel: Hollow sections are increasingly replacing conventional angles and channels in buildings, warehouses, and pre-engineered structures.
- Water infrastructure: Rural and urban water supply programmes need large volumes of water pipes and fittings.
- Gas and energy: City gas distribution, oil and gas pipelines, and emerging hydrogen transport create demand for certified line pipes.
- Solar and renewables: Solar mounting structures use large quantities of galvanised tubes and hollow sections.
- Agriculture and manufacturing: Irrigation, greenhouses, fencing, furniture, and automotive applications add steady demand.
India-Specific Market Opportunity
| Segment | India Market Context | Manufacturing Role |
|---|---|---|
| Housing & Commercial Construction | Urban growth and warehousing | Hollow sections and GI pipes |
| Water Supply Projects | Rural and urban water schemes | Water and GI pipes |
| City Gas & Pipelines | Expanding gas networks | Line pipes to API/ISO standards |
| Solar & Infrastructure | Renewable capacity additions | Galvanised structural tubes |
| Dealer & Retail Market | Plumbing and fabrication | Branded standard pipes |
The strongest position for an ERW Steel Pipes Manufacturing Plant in India combines high-volume dealer sales with project and institutional business in water, gas, and solar. Dealer sales build brand and steady demand, while projects and certified products lift margins. Because freight on steel pipes is significant, regional plants close to both steel suppliers and customers enjoy a clear cost advantage.
ERW Steel Pipes Manufacturing Process Flow
Understanding the ERW Steel Pipes Manufacturing Process helps promoters plan mills, layout, testing, and quality systems. The process is continuous and fast, and the quality of the weld seam is the most critical factor in pipe performance. The flow below reflects a typical plant producing black and galvanised pipes and hollow sections.
Step-by-Step ERW Steel Pipe Manufacturing Process Flow
HR coils are inspected and slit into strips, which are uncoiled, joined, and accumulated for continuous feed. The strip is roll-formed into a tube, high-frequency welded, de-beaded, sized, cut to length, straightened, end-finished, tested, and then galvanised or coated if required before marking and bundling.
| Unit Operation | Key Activity |
|---|---|
| Coil Receipt & Slitting | HR coils inspected and slit to strip width |
| Uncoiling & Strip Joining | Strip ends sheared and welded, accumulated |
| Roll Forming | Strip shaped into open round tube |
| High-Frequency Welding | Edges heated and forged into a seam |
| Bead Removal & Seam Treatment | Weld bead trimmed, seam annealed if required |
| Cooling & Sizing | Pipe sized to final diameter or shape |
| Flying Cut-Off | Continuous pipe cut to length |
| Straightening & End Finishing | Straightened, faced, bevelled or threaded |
| Testing | Hydrostatic and non-destructive testing |
| Galvanising, Marking & Bundling | Optional coating, marking, bundling |
Two factors decide profitability. The first is weld quality and mill speed consistent high-frequency welding, well-maintained forming rolls, and accurate sizing produce sound seams at high line speeds, raising output and reducing rejects. The second is yield: losses from coil ends, cut lengths, trimming, and rejects directly reduce margin when steel makes up most of the cost, so strip width optimisation and good process control are essential. Hydrostatic testing, eddy current or ultrasonic weld inspection, and dimensional checks keep pipes within BIS and customer specifications.
Raw Materials Required for ERW Steel Pipes Manufacturing
The main input is hot-rolled steel coil, supported by zinc for galvanising, coatings and oils, and mill consumables. Steel dominates cost to such an extent that procurement strategy is central to plant economics.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Hot-Rolled Steel Coil (HRC) | Base material | Integrated steel plants and service centres | 72–80% |
| Zinc | Hot-dip galvanising | Domestic zinc producer and imports | 0–8% |
| Coatings, Varnish & Oils | Surface protection | Domestic suppliers | 0.5–1% |
| Mill Consumables | Rolls, impeders, saw blades | Domestic and imported | 1–2% |
| Packaging Materials | Strapping, end caps, labels | Local suppliers | 0.5–1% |
India's large integrated steel producers supply HRC in a wide range of grades and thicknesses, but prices move with global steel markets, iron ore, coking coal, and trade measures. Many pipe makers hedge this risk by buying under contracts, maintaining moderate inventories, and passing price changes on through dealer price lists. For galvanised products, zinc is the second-largest material cost, and efficient zinc use in the galvanising bath improves margins noticeably.
Location, Land & Infrastructure
Steel pipes are heavy and freight-sensitive, so location matters both for incoming coil and outgoing pipes. The best location for ERW Steel Pipes manufacturing plant setup sits near steel producers or service centres, close to major demand centres and dealer networks, with good road and rail connectivity, reliable power, and an industrial workforce familiar with steel processing.
Best Location for ERW Steel Pipes Manufacturing Plant Setup in India
| State | Why It Works | Key Advantage |
|---|---|---|
| Uttar Pradesh | Established tube cluster near NCR | Large northern market and dealer networks |
| Chhattisgarh | Major steel production hub | Proximity to HRC and central markets |
| Gujarat | Steel, port, and pipeline industry base | Line pipe demand and exports |
| Maharashtra | Steel plants and industrial demand | Western market access |
| Andhra Pradesh | Coastal steel and port access | Southern markets and exports |
| Punjab & Haryana | Traditional steel processing belt | Northern demand and skilled workforce |
Uttar Pradesh hosts one of India's largest tube clusters close to the NCR market, Chhattisgarh offers proximity to major steel plants, Gujarat combines steel supply, ports, and pipeline demand, Maharashtra and Andhra Pradesh provide access to large western and southern markets, and Punjab and Haryana have long experience in steel processing. Several leading producers operate multiple regional plants to cut freight, and a new entrant should weigh coil sourcing against proximity to customers.
Quality, Certification and Safety Requirements
ERW pipes must meet Indian Standards such as IS 1239 for steel tubes, IS 3589 for water and sewage pipes, IS 4923 for structural hollow sections, and IS 3601 for mechanical tubes, along with API or ISO specifications for line pipes. Testing includes hydrostatic pressure tests, flattening and bend tests, weld seam inspection, zinc coating checks for galvanised pipes, and dimensional measurement. Galvanising lines involve acids, flux, and molten zinc, so fume extraction, acid handling, and hazardous waste management are essential, along with crane safety and machine guarding throughout the plant.
Infrastructure Requirements (Mid-Sized Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 5 – 15 acres | Coil storage and long pipe handling |
| Production Sheds | Long-bay sheds with EOT cranes | Mill lines and finishing |
| Power Requirement | 2 – 8 MW | HF welders and galvanising |
| Cooling Water System | Recirculating system | For welding and mill cooling |
| Galvanising Plant | Pickling, fluxing, zinc bath | Optional, with fume control |
| Coil and Pipe Storage | Covered and open yards | Heavy-load flooring |
| Testing Laboratory | Mechanical and coating tests | BIS and customer compliance |
Infrastructure for an ERW plant centres on long production bays with overhead cranes, reliable power for high-frequency welders, cooling systems, and large storage areas for coils and finished pipes. Where galvanising is included, separate areas for pickling, fluxing, and zinc baths with fume and effluent control are needed. Planning space for an additional tube mill or a larger-diameter line from the outset supports future growth.
ERW Steel Pipes Manufacturing Machinery and Equipment
ERW machinery is widely available from experienced Indian manufacturers as well as international suppliers, which keeps investment moderate compared with many other steel processes. The tube mill and high-frequency welder are the heart of the plant. The main equipment is summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Slitting Line | Slit coils into strips | Matched to coil width and thickness |
| Uncoiler, Shear & End Welder | Feed and join strips | Continuous operation |
| Strip Accumulator | Store strip for non-stop running | Horizontal or vertical type |
| Forming Mill | Roll-form strip into tube | Size range defines product mix |
| HF Solid-State Welder | Weld the seam | High-frequency induction or contact |
| Scarfing & Seam Annealer | Remove bead, heat-treat seam | Annealer needed for line pipes |
| Sizing Mill & Turk's Head | Final size and shape | Round and hollow sections |
| Flying Cut-Off Saw | Cut to length | Synchronised with line speed |
| Straightener, End Facer & Hydro Tester | Finish and test pipes | Pressure testing to standards |
| NDT, Galvanising Plant & Bundling | Inspection, coating, packing | Eddy current or ultrasonic testing |
Mill selection should follow the target size range: small mills serve thin-wall tubes and furniture sections, medium mills cover the main pipe and hollow section market, and large mills enable water and line pipes. Solid-state HF welders improve weld consistency and energy efficiency, while modern NDT systems are essential for certified products. Many plants run two or more mills to cover a wide size range and keep finishing equipment fully used.
ERW Steel Pipes Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below summarise the capital and operating cost structure of an ERW pipe facility in India. The final ERW Steel Pipes Investment Cost for a specific project depends on capacity, the number and size of tube mills, galvanising and coating facilities, testing and certification needs, and land and building costs.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 35–45% | Slitting line, tube mills, welders, finishing |
| Galvanising & Coating (optional) | 8–15% | Pickling, zinc bath, fume control |
| Land & Buildings | 12–18% | Land, sheds, cranes, storage |
| Utilities & Electricals | 5–8% | Power, cooling, compressors |
| Pre-operative & Contingency | 3–6% | Engineering, DPR, commissioning |
| Working Capital | 18–25% | Steel inventory and receivables |
Working capital is unusually large in this business because steel coil is expensive and both coil and finished pipe inventories must be maintained, while dealers and project customers often buy on credit. Machinery is the largest fixed asset but is moderate compared with sales. An ERW Steel Pipes Business Plan models these components carefully so that capacity, product mix, and financing rest on realistic numbers.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials | 75–85% | HRC dominates, plus zinc |
| Power & Utilities | 5–10% | Welding, galvanising, cranes |
| Labour & Manpower | 3–5% | Mill operators and finishers |
| Consumables & Maintenance | 2–3% | Rolls, blades, spares |
| Freight & Distribution | 2–4% | Heavy product movement |
| Overheads & Marketing | 1–3% | Dealer support and administration |
With steel making up most of operating cost, profitability depends on the spread between HRC prices and pipe selling prices, along with yield and the share of value-added products. A sound financial model should test margins against steel price cycles, zinc costs, and capacity utilisation.
Financial Analysis and Profitability
ERW pipe manufacturing is a volume-driven business with moderate capital intensity and steady demand. The pprofitability of ERW Steel Pipes manufacturing business in India improves with high mill utilisation, strong yields, a growing share of galvanised and structural products, and a recognised brand with wide distribution.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 15–25% | Higher for value-added products |
| Net Profit Margin | 5–10% | After depreciation and Indian corporate taxes |
| Payback Period | 3–5 Years | Moderate capital intensity |
| IRR (Internal Rate of Return) | 14–20% | Sensitive to steel price spreads |
| Capacity Utilization (stable ops) | 65–85% | Linked to dealer and project demand |
| Break-even Capacity Utilization | 40–55% | Thin per-tonne margins |
Per-tonne margins are modest, so returns come from volume and efficient asset use. Leading Indian producers have improved profitability by shifting towards branded structural hollow sections and value-added products, while plants selling only commodity pipes are more exposed to steel price swings. Managing inventory through steel price cycles is as important as running the mills well.
Returns can be strengthened by building a branded product range, adding galvanising and structural hollow sections, pursuing certified water and line pipes, locating near steel suppliers and customers, and using efficient solid-state welders and modern NDT to reduce rejects.
Key Risks and Mitigation
The main risks are steel price volatility, intense competition from large branded players and regional producers, working capital strain, demand swings in construction and government projects, and environmental compliance for galvanising. Steel risk is reduced through procurement contracts and disciplined inventory; competition through branding, quality, and service; working capital risk through sound credit policies and financing; demand risk through a diversified customer base; and compliance risk through proper fume, effluent, and hazardous waste systems.
Licenses and Approvals for ERW Steel Pipes Manufacturing in India
An ERW pipe plant requires product certification, environmental, and industrial approvals. Promoters typically need the following before commencing operations:
- BIS Product License: BIS certification under the applicable quality control orders, with IS 1239 (Part 1) steel tubes already mandatory and further pipe standards proposed for inclusion.
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, especially where galvanising and pickling are included.
- Hazardous Waste Authorisation: Authorisation for spent acid, zinc ash, dross, and sludge under the Hazardous and Other Wastes Rules.
- Factory License: Factory registration and building plan approval under the Occupational Safety, Health and Working Conditions Code, 2020.
- Line Pipe Certifications: API or other third-party certifications where the plant targets oil, gas, or export markets.
- Business, Tax and Trade Registration: Company incorporation, GST, Udyam, trademark registration for the brand, and an Import Export Code for exports or equipment imports.
- Fire NOC and Labour Registrations: Fire safety approval plus EPF and ESI registrations.
BIS licensing and pollution consents sit on the critical path for most projects, and galvanising plants need particular attention to effluent and hazardous waste approvals. Engaging an ERW Steel Pipes Manufacturing Consultant in India can help promoters choose mill sizes, plan certifications, and set up quality and environmental systems alongside construction.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, product range, capacity, target customers, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India ERW Steel Pipes Manufacturing Industry
Several recent developments highlight continued investment and tightening standards in the ERW pipe sector:
- Capacity additions by leading players: Hi-Tech Pipes began commercial production at a greenfield 80,000 TPA unit in Kathua, Jammu and Kashmir, in January 2026, and at its 1.2 lakh TPA Sikandrabad Unit-III in Uttar Pradesh in February 2026, taking its total capacity to about 1 million tonnes a year.
- Wider quality control coverage: A draft Iron and Steel Pipes, Tubes and Fittings Quality Control Order, 2025 proposes mandatory BIS certification for further standards, including IS 3589 water pipes, IS 4923 hollow sections, IS 3601 mechanical tubes, and IS/ISO 3183 line pipes.
- Higher-value ERW products: JTL Industries announced a 3 lakh TPA ERW line aimed at ASTM and API grades in July 2025, while Tata Steel and Welspun Corp developed ERW pipes for high-pressure hydrogen transport in August 2024.
Together these point to a growing market where leading producers are adding capacity and moving up the value chain, while quality regulation is tightening. For new entrants, success depends on efficient regional capacity, BIS-compliant quality, and a product mix that includes value-added and certified pipes.
How ERW Steel Pipes Manufacturing Project Report and DPR Helps Investors
A detailed ERW Steel Pipes Project Report gives investors a structured roadmap covering market demand, product mix, steel sourcing, process design, mill selection, plant layout, utilities, certifications, regulatory pathway, and economics. It helps promoters choose the right capacity and mill sizes, estimate capital expenditure (CapEx) and operating expenditure (OpEx), assess profitability, and identify risks before implementation.
At the heart of the DPR is an ERW Steel Pipes Financial Model covering product-wise volumes and prices, HRC and zinc costs, yields, conversion costs, working capital, cash flow projections, break-even, return on investment (ROI), and payback. Because margins depend on steel price spreads, lenders expect sensitivity analysis, which is why many promoters engage an ERW Steel Pipes Plant Project Report Consultant in India to prepare bank-ready documents.
For an ERW project specifically, a strong DPR also answers the questions that matter most: which size range and products to target, whether to add galvanising at the start, how to manage steel price and inventory risk, and how returns hold up under different spread scenarios. An experienced ERW Steel Pipes Manufacturing Feasibility Study Consultant tests these scenarios so that the final plan is one lenders and partners can back with confidence.
Frequently Asked Questions
How do I set up an ERW steel pipes manufacturing factory in India?
Start by defining your product range and target markets, then commission a feasibility study and DPR. Secure a site near steel suppliers and customers, order slitting, tube mill, welding, and finishing equipment, obtain BIS, pollution, and factory approvals, arrange working capital for steel inventory, and build a dealer and project sales network.
What is the ERW steel pipes manufacturing plant setup cost in India?
Total investment typically ranges from about INR 15 crore for a compact plant of around 24,000 tonnes a year to INR 150 crore or more for an integrated plant of 1 to 3 lakh tonnes, depending on mill sizes, galvanising, and working capital needs.
How are ERW steel pipes made?
HR coils are slit into strips, which are roll-formed into tubes and welded by high-frequency current. The pipes are de-beaded, sized, cut to length, straightened, tested, and optionally galvanised before marking and bundling.
What machinery is needed for an ERW steel pipes manufacturing plant?
Key equipment includes a slitting line, uncoiler, shear and end welder, accumulator, forming mill, HF solid-state welder, scarfing unit, sizing mill, flying cut-off saw, straightener, end facer, hydro tester, NDT equipment, and optionally a galvanising plant.
What raw materials are used in ERW steel pipes?
The main raw material is hot-rolled steel coil, with zinc for galvanised pipes, coatings and oils for surface protection, and mill consumables such as rolls, impeders, and saw blades.
Is ERW steel pipes manufacturing profitable in India?
A well-run plant typically earns a 5 to 10% net margin, with payback in 3 to 5 years. Profitability depends on steel price spreads, mill utilisation, yield, and the share of value-added products.
What licenses are needed for an ERW steel pipes manufacturing unit in India?
A plant typically needs a BIS license for applicable standards, State Pollution Control Board consents, hazardous waste authorisation if galvanising, a Factory License, a Fire NOC, and GST, Udyam, and labour registrations.
Which state is best for an ERW steel pipes manufacturing plant?
Uttar Pradesh, Chhattisgarh, Gujarat, Maharashtra, Andhra Pradesh, and Punjab and Haryana are strong options. The best site balances proximity to steel suppliers with access to major markets and dealer networks.
How do I get a feasibility study or DPR for an ERW steel pipes manufacturing plant?
A professionally prepared DPR covers market assessment, product strategy, technical design, approvals, costs, and financial projections for bank appraisal. Many promoters work with an ERW Steel Pipes Business Plan Consultant in India to prepare it and align it with lender requirements.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

The India Construction Equipment Market stands at a defining crossroads where accelerating infrastructure investment collides with some of the most consequential regulatory changes the sector has ever faced. According to IMARC Group, the market was valued at USD 15.37 Billion in 2025 and is projected to reach USD 29.50 Billion by 2034, growing at a CAGR of 7.52% (2026–2034).
Setting up a WPC Door Manufacturing Plant in India taps into a fast-moving shift in the building materials market. Wood plastic composite (WPC) doors combine wood flour or fibre with PVC or other polymers to create doors and frames that look and work like wood but resist water, termites, rot, and warping.
Setting up a Technical Textiles Manufacturing Plant in India gives investors access to one of the fastest-evolving parts of the textile value chain.
Angle sections are L-shaped profiles made mainly by extruding aluminium alloy billets through a shaped die, then straightening, cutting, and heat treating them.
Japan's construction industry is at an inflection point, and the Japan modular construction market sits at the centre of the response. According to IMARC Group, the Japan modular construction market size increased from USD 18.11 Billion in 2025 to USD 18.85 Billion in 2026 and is projected to reach USD 29.27 Billion by 2034, growing at a compound annual growth rate of 5.65% from 2026 to 2034.
DI pipes are made by treating molten iron with magnesium so that its graphite forms tiny spheres instead of flakes, casting it in spinning water-cooled moulds, and then annealing, zinc coating, cement lining, and testing each pipe.
Gypsum plasterboard is a flat building panel with a core of set gypsum bonded between a face paper and a back paper. Fixed to light steel frames, it creates ceilings, partitions, and wall linings that go up far faster than brick and wet plaster, weigh much less, and resist fire because gypsum holds chemically bound water.
MIG welding wire is a continuous solid wire, usually 0.8 to 1.6 mm in diameter, that is fed through a welding gun and melted by an electric arc under a shielding gas to join metals.
Gypsum board, also called plasterboard or drywall, is a panel made of a set gypsum core sandwiched between two sheets of heavy paper.
Steel forgings are strong, reliable metal parts made by shaping heated steel under the force of presses and hammers, which refines the grain structure and gives far better strength and fatigue resistance than casting or machining from bar.
PVC boards, mainly PVC foam boards and WPC boards, are lightweight, waterproof, termite-proof sheets used as an alternative to plywood and MDF in kitchens, bathrooms, wardrobes, furniture, partitions, signage, and interiors.
Laminated veneer lumber, or LVL, is an engineered wood product made by bonding thin wood veneers with their grain running in the same direction, producing straight, strong, and dimensionally stable members from fast-growing plantation timber.
Fly ash bricks turn a waste product from coal-fired power plants into strong, uniform building blocks that need no firing in a kiln. India's thermal power plants generated about 340 million tonnes of fly ash in 2024-25, and government rules require building projects within 300 km of these plants to use ash-based bricks and blocks where they are priced competitively.
Nuts and bolts hold together almost everything that is built or manufactured, from cars, tractors, and two-wheelers to bridges, towers, railways, machinery, and household appliances.
Precast elements are cast in a factory under controlled conditions and then transported to site, where they are lifted into place like the parts of a kit. India's construction sector is turning to this method to build faster, with better quality and less dependence on site labour.
Rice husk ash (RHA) is the residue left when rice husk is burned, and when the burning is properly controlled it is one of the richest natural sources of amorphous silica, typically 85 to 95% silica by weight.
Concrete poles carry most of India's low-tension and 11 kV distribution lines, as well as street lights, rural feeders, and telecom cables. They are strong, durable, resistant to rust, rot, and termites, need almost no maintenance, and cost less than steel poles, which makes them the default choice for state power distribution companies.
Crushed stone aggregates and manufactured sand are the most widely used construction materials after water. They form the bulk of concrete, the base layers of roads and runways, railway ballast, and the fill under buildings, factories, and ports.
Almost every industrial process generates heat that has to be removed. Power plants, steel mills, refineries, chemical and pharmaceutical units, food processors, plastics moulders, and now data centers all rely on cooling towers, chillers, and heat rejection equipment running around the clock.
Steel is the backbone of India's economic growth. Buildings, bridges, railways, highways, ports, power plants, automobiles, machinery, and household appliances all depend on it. India is the world's second-largest steel producer, and crude steel output reached about 170 million tonnes in 2025-26.
Ready mix concrete (RMC) is concrete batched in a central plant to a precise, engineered mix design and delivered to construction sites in transit mixers, ready to pour.
Open a modular kitchen cabinet, a wardrobe shutter, or an office workstation in India today and there is a good chance it is made from medium density fibreboard.
India is the world's second-largest producer of ceramic tiles, and walking through any new apartment, mall, hospital, or metro station shows why. Tiles have replaced mosaic, stone, and plain cement floors in homes across the country, while large-format glazed vitrified slabs are now standard in premium projects.
Setting up a TMT Bar Manufacturing Plant in India is a high-demand, infrastructure-driven venture, powered by the country's massive construction and housing boom, government infrastructure spending, and steady urbanisation.
Setting up a Cement Manufacturing Plant in India is a capital-intensive, high-demand venture, powered by the country's massive infrastructure programme, housing boom, and status as the world's second-largest cement producer.
Setting up a PVC Panel Manufacturing Plant in India is a high-demand, construction-driven venture, powered by the country's building boom, fast-growing interior and renovation market, and the shift away from plywood and plaster toward affordable, waterproof panels.
Setting up an Electric Motor Manufacturing Plant in India is a high-value, engineering-driven venture, powered by the country's industrial expansion, energy-efficiency push, and the rise of electric vehicles and automation.
Setting up an Iron Ore Pellets Manufacturing Plant in India is a capital-intensive, high-demand venture, powered by the country's ambitious steel-capacity expansion, the shift toward value-added iron ore, and rising demand from blast furnaces and sponge iron units.
The Saudi Arabia construction market has emerged as one of the most closely watched construction economies in the world. The market reached USD 101.4 Billion in 2025 and is projected to reach USD 140.4 Billion by 2034, expanding at a compound annual growth rate (CAGR) of 3.6% between 2026 and 2034.
A WPC (Wood Plastic Composite) door is a type of composite door made from a combination of wood fibers or wood flour and thermoplastic resins like PVC, polyethylene, or polypropylene, with additives to improve durability and processability. The resulting composite material is then extruded or molded into door panels and frames, providing the attractive look of wood and the strength and water-resistance of plastic.
UPVC windows refer to window frames and window assemblies manufactured from ‘unplasticized polyvinyl chloride,’ which is a relatively rigid and strong thermoplastic substance. While PVC is a flexible material that requires the addition of a softening substance called a plasticizer to be formed into a durable performance material, PVC window frames and UPVC window assemblies, for instance, do not display such requirements due to the presence of unplasticizers, a component of the material that provides enhanced strength, stability, and resistance to the elements such as UV radiation, moisture, and temperature changes.
The Saudi Arabia factoring market represents a critical component of the Kingdom's evolving financial services landscape, offering businesses an increasingly popular alternative to traditional bank lending. Factoring, which involves the sale of accounts receivable to a third-party financial institution at a discount, has emerged as a vital mechanism for improving liquidity, managing cash flow, and mitigating credit risk across diverse industry sectors.
The GCC bridge construction market represents a vital component of the region's ambitious infrastructure transformation agenda, serving as a cornerstone for enhanced mobility, economic integration, and sustainable urban development across the Gulf states.
The Australia industrial couplings industry stands at a transformative juncture in 2025, propelled by technological advancement and surging demand across critical sectors. As mechanical devices connecting two shafts to transmit power and torque, industrial couplings form the backbone of machinery operations in manufacturing, mining, automotive, and energy sectors.
The Saudi Arabia real estate market stands at a pivotal juncture in its evolution, representing one of the most dynamic and transformative sectors within the Kingdom's economy. With this country having a very ambitious agenda of economic diversification and modernization, the real estate business has come out as one of the pillars of this transformation.
Steel is an alloy that consists of iron and carbon in addition to trace amounts of other elements like manganese, silicon, chromium, and nickel. The amount of carbon in steel is usually less than two percent and is an important factor in determining the strength, hardness, and ductility of steel.
Saudi Arabia’s precast concrete market reached USD 1.2 Billion in 2024 as per the IMARC Group, clear proof that off-site construction is rapidly becoming the Kingdom’s go-to building solution. With residential, commercial, and major infrastructure projects multiplying, developers are increasingly turning to precast building solutions to keep pace.
The GCC cold storage construction market represents critical infrastructure underpinning regional food security, pharmaceutical distribution, and temperature-sensitive logistics across the Arabian Peninsula. As Gulf Cooperation Council nations diversify their economies and reduce hydrocarbon dependence, robust cold chain infrastructure has emerged as a cornerstone of sustainable development planning.
PVC panels are lightweight, durable building materials made from polyvinyl chloride using extrusion or molding processes. They are available as rigid or semi-rigid sheets designed primarily for wall and ceiling cladding, partitions, and decorative finishes. Known for their excellent resistance to moisture, chemicals, termites, and corrosion, PVC panels offer a smooth surface and a clean, polished look that’s easy to maintain. Available in an extensive range of colors, textures, and patterns, these panels serve as a practical alternative to traditional materials like wood, plaster, or tiles.
Ready mix concrete (RMC) is a precisely engineered construction material produced in a controlled environment within a batching plant and delivered to construction sites in a freshly mixed, plastic state. It is formulated by combining cement, aggregates, water, and chemical or mineral admixtures in carefully proportioned quantities to achieve specific performance characteristics. Unlike site-mixed concrete, RMC ensures consistent quality, uniformity, and superior workability through automated production and quality control processes.
The construction industry across the Gulf Cooperation Council (GCC) member states is at the core of a monumental economic transformation. Far exceeding traditional building activities, the sector now serves as the principal vehicle for national economic diversification strategies, moving these nations beyond reliance on oil revenues.
Paver blocks are precast construction material made basically from cement, aggregates, sand, and pigments for constructing surfacing. They are produced in standardized shape and thickness, allowing each unit to interlock to form a strong, load-bearing surface with no need for continuous concrete pouring. Paver blocks possess high compressive strength, abrasion resistance, and are easy to lay and maintain.
The Brazil ceramic tiles market has witnessed stable growth, reflecting broader trends in the construction and building materials industries of the country. The Brazil ceramic tiles market size was valued at USD 1.6 Billion in 2025. The market is expected to reach USD 2.2 Billion by 2034, exhibiting a CAGR of 3.91% during 2026-2034.
MDF is an engineered wood product produced by breaking down hardwood or softwood residuals into wood fibers, which are then combined with resin binders under heat and pressure. MDF exhibits a homogeneous density, a smooth surface, and fine texture, ensuring a much more workable material compared to natural wood.
Float glass is a type of flat glass that is manufactured by floating molten glass on a bed of molten tin. This produces a smooth, uniform surface and consistent thickness. The float process was developed by Pilkington in the 1950s and revolutionized glassmaking because it enabled the production of large, flawless sheets of glass without needing polishing or grinding. The basic raw materials used-silica sand, soda ash, limestone, and dolomite-are heated in the furnace to a very high temperature, then continuously poured onto the tin bath, where the molten glass spreads out into an even layer. It cools and solidifies into a perfectly flat and perfectly transparent sheet. As it provides optical clarity and strength and is easily processed into coated, laminated, or toughened forms, float glass is used as a basic product for various applications, ranging from architectural and automotive to industrial applications.
ERW steel pipes can be identified as one of the most important categories of welded pipes and find wide applications in infrastructure, construction, and other industries because of their precision, cost-effectiveness, and reliability. The raw material to produce these pipes is either hot-rolled or cold-rolled steel coils that are longitudinally formed and welded by the application of high-frequency electric resistance welding.
Drill bits are specifically designed cutting instruments intended to produce cylindrical holes in various materials, ranging from soft woods and plastics to hardened steels, stone, and rock. Although they seem straightforward, drill bits consist of various specialized shapes, coatings, and materials that are designed to suit the cutting characteristics of the intended material and the requirements of the drilling task.
Concrete is among the most widely used construction materials in the world due to its strength, versatility, and durability. It is a composite material largely made of cement, water, aggregates-sand, gravel, or crushed stone-and in some cases, admixtures which give special properties to the concrete.
Clay bricks are one of the oldest and most extensively used construction materials in the globe, appreciated for their strength, durability, insulation against heat, and beauty. They are produced mainly from natural clay and shale, which are fashioned, dried, and subjected to high-temperature firing to produce a hard, dense material that can resist multiple environmental and structural stresses. The mix generally consists of alumina, silica, lime, iron oxide, and magnesia that collectively decide the color, texture, and performance properties of the brick.
Metal beam crash barriers and high mast light poles are essential infrastructural features providing security and visibility on highways, city roads, and industrial sites. Metal beam crash barriers or guardrails are made of galvanized steel beams, typically W-beam or Thrie-beam, that are designed to dissipate the impact energy on impact with a vehicle and minimize death and damage to vehicles.
Laminated plywood is an engineered wood material that is produced by laminating several layers of thin veneers of wood together with powerful adhesives and covering them with a protective or decorative laminate sheet. This amalgamation not only increases the strength of the plywood but also its beauty, which is why it is extremely versatile for use in furniture, cabinetry, floors, paneling, and interior design.
Ductile iron pipes (DIP) are a key part of new water and wastewater infrastructure, providing enhanced performance capabilities over older piping materials. Cast from ductile cast iron, a material that has the strength of steel combined with the resistance to corrosion of cast iron, these pipes are designed to endure high-pressure use while still being flexible enough to absorb stress without cracking.
The real estate sector plays a critical role in driving economic growth and shaping communities. It significantly contributes to national economies by generating jobs, influencing investment flows, and boosting government revenues through taxes. Beyond these economic benefits, real estate development directly affects the quality of life by creating homes, enhancing infrastructure, and revitalizing urban areas.
Gypsum boards, also referred to as drywall or plasterboard, are lightweight, strong and fireproof building materials that are frequently used for partitions, walls and ceilings. Constructed from a gypsum core encased in paper liners, they provide improved acoustics, cost effectiveness, and speedy installation. Gypsum boards are favoured in industrial, commercial, and residential construction because of its environmentally beneficial qualities, ability to withstand moisture, and ability to insulate against heat. They are an essential part of efficient and sustainable construction methods because of their adaptability to contemporary building processes.
A frameless shower door is a modern and aesthetically appealing bathroom fixture that has gained popularity for its sleek and minimalist design. They are constructed without the bulky metal framing that surrounds the glass panels and are typically made from thick, tempered glass that is securely attached to the wall and floor using hinges or brackets.