Truck Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
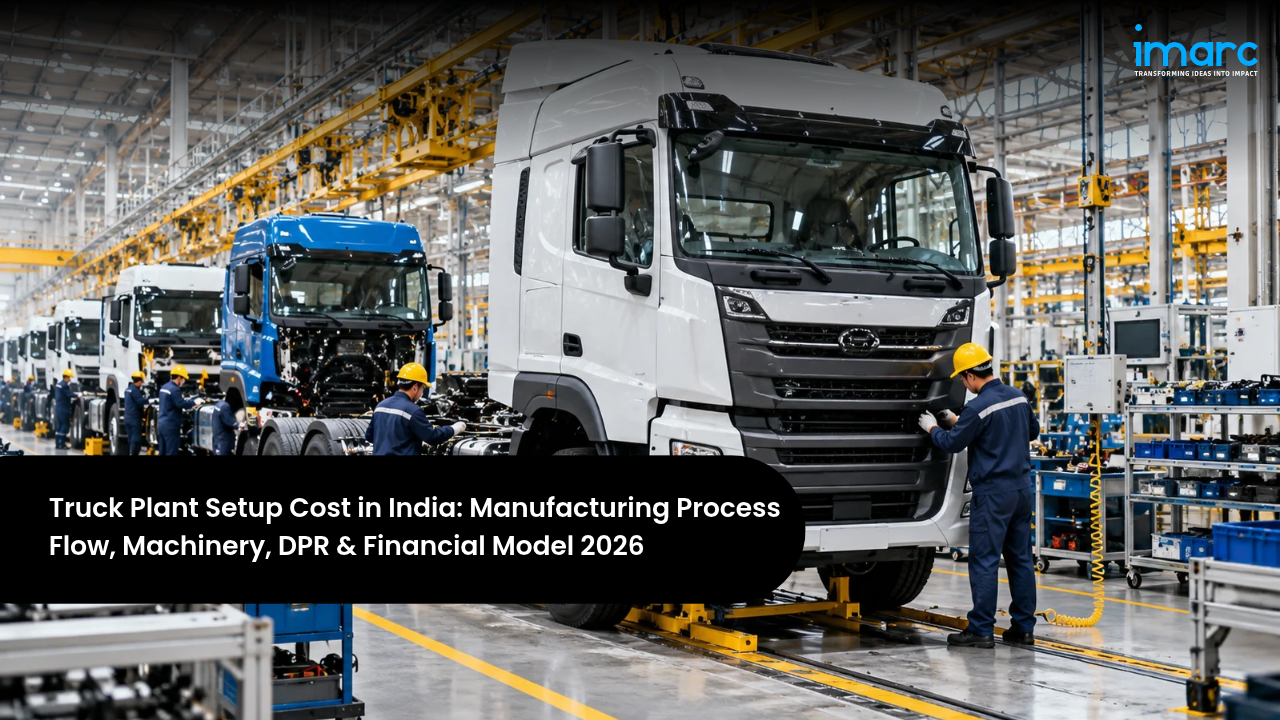
A goods carrier is built on a ladder-frame chassis of heavy steel side members, onto which the engine, gearbox, axles, suspension, brakes, fuel or battery system, and a pressed and welded cab are fitted, before the vehicle is painted, tested, and sent to body builders or customers. Commercial vehicles move most of India's freight, from small light trucks for city deliveries to multi-axle haulers, tippers, and tractor-trailers for highways, mines, and ports. IMARC values India's market at about USD 25.65 billion in 2025 and expects it to reach USD 47.79 billion by 2034, while domestic commercial vehicle volumes grew 12.6% in FY2026 and passed their FY2019 peak. With the GST cut, infrastructure spending, and the shift to cleaner fuels, Truck Manufacturing Plant Setup in India is a large but demanding opportunity for automotive investors.
Investment depends mainly on annual output, the weight classes covered, how much is made in-house, from frames and cabs to engines and axles, the paint process, robotic welding and automation, testing facilities, and whether electric or gas-powered models are included. The Truck Manufacturing Plant Cost ranges from about INR 80–150 crore for an assembly unit making 3,000 to 5,000 light vehicles a year with bought-in powertrains, to INR 900–1,300 crore for an integrated plant of about 15,000 units a year with a press and cab body shop, frame line, paint shop, and final assembly, and INR 3,500–5,000 crore for plants above 50,000 units that also make engines and axles. Materials and components make up 75 to 85% of operating cost, so sourcing and localisation decide competitiveness. IMARC estimates a gross margin of 20 to 30% and a net margin of 8 to 12% for a well-run plant.
This guide is written for investors exploring how to start a Truck manufacturing plant in India. It focuses on an integrated plant of about 15,000 units a year making intermediate and heavy commercial vehicles from about 7.5 to 28 tonnes, including tippers, with in-house frames, cabs, and painting and bought-in or partner-supplied powertrains, selling through dealers to fleet owners, logistics companies, and contractors. It also explains light vehicle assembly units and large integrated plants. It covers products and markets, the demand outlook, the production process flow, machinery and components, location and infrastructure, a detailed cost and financial breakdown, certification and approvals, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| India Market (2025) | About USD 25.65 Billion |
| India Market Forecast (2034) | USD 47.79 Billion, 7.16% CAGR |
| Domestic CV Growth (FY2026) | 12.6%, Above FY2019 Peak |
| GST on Goods Vehicles | 18%, Down from 28% |
| Typical Plant Capacity | 10,000 – 20,000 Units a Year |
| Indicative Total Investment | INR 80 Crore to 5,000 Crore |
The snapshot shows a large, cyclical market enjoying a strong year after the GST cut, with growth expected to moderate in FY2027. The market is led by a few established manufacturers with wide dealer and service networks, so new entrants need a clear niche, strong partners, and reliable after-sales support to win fleet buyers.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | LCV, ICV, HCV, tippers, e-trucks |
| Plant Capacity | 3,000 – 50,000+ Units Per Year |
| Total Project Investment | INR 80–150 Crore (assembly unit) to 900–1,300 Crore (15,000 units) |
| Payback Period | 5 – 7 Years |
| Net Profit Margin | 8 – 12% |
| IRR | 14 – 20% |
| Preferred States | Tamil Nadu, Maharashtra, Jharkhand, Madhya Pradesh, Uttarakhand, Karnataka |
| Key Requirement | Powertrain, dealers, financing |
These ranges provide a realistic frame for early planning, but actual returns depend on steel, engine, axle, and tyre prices, the depth of localisation, freight demand cycles, interest rates and fleet financing, dealer and service reach, the cost of meeting safety and emission rules, competition from established brands, and the working capital tied up in components and dealer stock. A site-specific Truck Feasibility Report narrows each of these assumptions to your chosen capacity, location, product range, and markets.
Table of Contents
- What is Truck Manufacturing?
- Why is Truck Manufacturing Growing in India?
- Truck Manufacturing Process Flow
- Raw Materials Required for Truck Manufacturing
- Location, Land & Infrastructure
- Truck Manufacturing Machinery and Equipment
- Truck Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Truck Manufacturing in India
- Recent Developments in the India Truck Manufacturing Industry
- How a Truck Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Truck Manufacturing?
Goods vehicles are grouped by gross vehicle weight into light, intermediate, medium, and heavy classes, and by configuration into rigid vehicles with two to five axles, tippers with dump bodies, and tractor-trailers that pull separate trailers. Each is built around a steel ladder frame carrying a diesel, gas, or electric powertrain, a gearbox, front and rear axles with leaf or air suspension, air brakes on heavier models, and a cab that now must offer air-conditioning for drivers in heavier classes. Payload, fuel economy, uptime, durability, driver comfort, and total cost of ownership decide value.
Commercially, the vehicles are sold through dealers to fleet operators and transporters, logistics and e-commerce companies, cement, steel, and mining firms, construction contractors, government departments, and small owner-operators who usually buy on loans, with body builders adding cargo boxes, tankers, and tipper bodies, and exports going to Africa, the Middle East, and South Asia. A Truck Manufacturing Plant can serve all these buyers by offering several weight classes and wheelbases on common platforms. Buyers value low running costs, reliability, easy financing, quick service, and strong resale value.
- Logistics: Fleets and transporters.
- Construction: Tippers and mixers.
- Industry: Cement, steel, mining.
- Exports: Africa, Middle East, SAARC.
The Main Products and Applications
Choosing the product range is the most important commercial decision, because it determines frames, cabs, powertrains, and margins:
| Product | Description | Key Property | Primary Demand |
|---|---|---|---|
| Light (up to 7.5 t) | Small goods carriers | City friendly | E-commerce, FMCG |
| Intermediate (7.5–18 t) | Mid-size rigid | Versatile | Regional haulage |
| Heavy Rigid (18–49 t) | Multi-axle | High payload | Long haul, cement |
| Tractor-Trailers | Articulated | Highest payload | Containers, steel |
| Tippers | Dump bodies | Rugged build | Mining, construction |
| Electric & LNG | Clean powertrains | Low emissions | Ports, city logistics |
These choices shape the whole project. Intermediate and tipper segments offer room for focused entrants with lower engineering demands, while heavy haulers and tractor-trailers need powerful engines and long-distance service networks, and electric and LNG models need partnerships and charging or fuelling support.
Why is Truck Manufacturing Growing in India?
Key Growth Drivers in India and Export Markets
Demand is supported by infrastructure spending, freight growth, and policy changes:
- Infrastructure: Roads, ports, and construction keep tipper and haulage demand strong.
- GST cut: The rate on goods vehicles fell from 28% to 18% in September 2025.
- Logistics growth: E-commerce and organised logistics need modern fleets.
- Replacement: Ageing fleets and scrappage rules support new purchases.
- Clean fuels: Electric and LNG models gain support for city and port use.
India-Specific Market Opportunity
| Segment | Market Context | Manufacturing Role |
|---|---|---|
| Fleet Operators | Organised logistics | Reliable haulers |
| Construction | Infrastructure push | Tippers |
| City Logistics | E-commerce growth | Light, electric |
| Ports & Mines | Short-haul duty | Electric, LNG |
The strongest opportunity for new entrants lies in focused segments such as tippers, intermediate vehicles, and electric models for ports and cities, in exports to price-sensitive markets, and in partnerships with global brands seeking Indian production. Makers that combine proven powertrains, local sourcing, financing tie-ups, and dependable service will be best placed to grow.
Truck Manufacturing Process Flow
Understanding the process helps you plan equipment, layout, and where cost and quality are decided. The flow runs from frame fabrication and cab pressing and welding through pretreatment and painting, chassis assembly with axles and suspension, fitting the engine and gearbox, trimming the cab with seats, dashboard, and air-conditioning, mounting the cab on the chassis, adding wiring and fluids, and wheel alignment, brake and emission testing, road testing, and pre-delivery inspection. Frame accuracy and cab welding decide strength and safety, while paint quality and assembly discipline decide durability and reliability.
The Truck Manufacturing Process Flow
The sequence below reflects an integrated plant with its own frame, cab, and paint shops. Assembly units start at chassis assembly with bought-in frames and painted cabs.
| Unit Operation | Key Activity |
|---|---|
| Frame Fabrication | Side, cross members |
| Cab Body Shop | Pressing, welding |
| Painting | Pretreatment, ED, topcoat |
| Chassis Assembly | Axles, suspension |
| Powertrain Fitment | Engine, gearbox |
| Cab Trim | Seats, AC, dashboard |
| Cab Mounting | Cab to chassis |
| Fluids & Electricals | Wiring, filling |
| End-of-Line Testing | Brakes, emissions |
| Road Test & PDI | Test track |
Two factors decide profitability across this flow. The first is sourcing and localisation, because bought-in components make up most of the cost, so local suppliers for frames, cabs, axles, and electricals, common platforms across weight classes, and long-term powertrain agreements directly set the cost of each vehicle. The second is quality and uptime in the field, since fleet buyers judge brands on breakdowns and service, so robust welding, corrosion protection, and thorough end-of-line testing decide repeat orders and long-term returns.
Raw Materials Required for Truck Manufacturing
The main inputs are high-strength steel for frames and cab panels, engines with exhaust aftertreatment, gearboxes, front and rear axles, suspension parts, brake systems, tyres and wheels, fuel tanks or battery packs, wiring harnesses, air-conditioning units, seats and trim, glass, and paint.
| Input | Role in Vehicle | India Sourcing | % of OpEx |
|---|---|---|---|
| Engine & Aftertreatment | Power, emissions | Engine makers, partners | 22–26% |
| Transmission & Axles | Drive train | Gear, axle makers | 16–20% |
| Frame & Cab Steel | Structure | Steel mills, pressings | 12–16% |
| Tyres & Wheels | Running gear | Tyre makers | 8–10% |
| Electricals & Trim | Wiring, AC, seats | Local suppliers | 8–10% |
Powertrains are the largest costs and the most important technical choice, so long-term agreements with engine and axle makers, or technology partnerships, are essential for new entrants.
Location, Land & Infrastructure
Site selection for a commercial vehicle plant is driven by access to mature automotive supplier clusters, skilled workers, steel supply, and good road, rail, and port links for dispatching large finished vehicles. Other factors include large land for press, body, paint, and assembly shops and a test track, reliable power, water for the paint shop, closeness to body builders, and state incentives on capital, power, and employment. Locating in an established automotive corridor cuts logistics costs and supplier lead times.
Choosing the Best Location for Truck Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Tamil Nadu | Hosur, Oragadam | Major CV cluster |
| Maharashtra | Pune, Chakan | Auto suppliers |
| Jharkhand | Jamshedpur | Steel, CV base |
| Madhya Pradesh | Pithampur | Central location |
| Uttarakhand | Pantnagar | Northern market |
| Karnataka | Dharwad, Bengaluru | Engineering talent |
Tamil Nadu and Maharashtra host the largest clusters of commercial vehicle makers and suppliers, while Jharkhand, Madhya Pradesh, and Uttarakhand offer established plants and central or northern market access. The final choice should weigh supplier access, markets, labour, logistics, and incentives.
Quality, Safety and Homologation Systems
Every model must be type approved under the Central Motor Vehicle Rules by an authorised agency such as ARAI or ICAT, meet Bharat Stage VI emission norms, and comply with safety rules on braking, lighting, cab strength, and air-conditioned cabins for heavier classes. A credible plant needs frame and cab gauging, weld testing, paint thickness and corrosion checks, engine and electrical diagnostics, and end-of-line testing of brakes, alignment, and emissions, together with conformity of production audits and IATF 16949 or ISO 9001 systems. Safety in the plant focuses on presses, welding, heavy lifting, and paint shop fire risk. Environmental systems cover paint shop emissions, pretreatment effluent, and waste oils. An experienced Truck Manufacturing Consultant in India can help plan capacity, product range, powertrain partnerships, and homologation so the plant meets regulatory and customer requirements from the start.
Infrastructure Requirements (15,000 Units a Year)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Plant Land | 80 – 120 acres | Test track space |
| Built-up Area | 5 – 7 lakh sq ft | Press to assembly |
| Power Supply | 10 – 15 MVA | Presses, paint |
| Paint Shop | ED and topcoat | ETP needed |
| Test Track | Brakes, gradient | Road testing |
| Dispatch Yard | Large parking | Body builders |
| Utilities | Air, water, gas | Reliable supply |
A well-laid-out press, body, and paint shop, a flowing final assembly line, and a proper test track are the most important infrastructure requirements, since they decide both output and product reliability.
Truck Manufacturing Machinery and Equipment
The equipment set covers pressing, welding, frame building, painting, assembly, fastening, filling, and testing. The press and body shop and the paint shop account for most of the investment, followed by assembly lines and test facilities.
| Equipment | Function | Key Specification |
|---|---|---|
| Press Lines | Form cab panels | Tandem presses |
| Robotic Welding Cells | Weld cabs | Spot, MIG |
| Frame Line | Build chassis frames | Riveting, bolting |
| ED Paint Line | Corrosion coating | Dip tanks, ovens |
| Topcoat Booths | Final paint | Spray, ovens |
| Chassis Conveyor | Assemble chassis | Floor conveyor |
| Cab Trim Line | Fit interiors | Overhead conveyor |
| Fastening Systems | Torque control | DC nutrunners |
| Fluid Filling | Fill fluids | Automatic |
| Alignment & Brake Testers | Check vehicles | Roller testers |
| Emission Test Bay | Check exhaust | BS VI equipment |
Machinery should follow the project plan. A light vehicle assembly unit buys painted cabs and frames and needs only assembly lines, fastening tools, filling stations, and test equipment, while a 15,000 unit plant adds press lines, robotic welding, a frame line, an ED paint shop, and a test track, and large plants add engine and axle manufacturing.
Truck Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for an integrated plant making about 15,000 units a year in India. The final Truck Investment Cost for your project will depend on capacity, weight classes, depth of in-house manufacturing, automation, paint process, testing, land cost, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Press & Cab Body Shop | 20–25% | Presses, robots |
| Frame & Chassis Line | 12–15% | Frames, conveyors |
| Paint Shop | 18–22% | ED, topcoat |
| Final Assembly & Testing | 12–15% | Lines, test bays |
| Land, Buildings & Utilities | 15–20% | Shops, test track |
| Pre-operatives & Working Capital | 8–12% | Parts stock, tooling |
Body, paint, and assembly shops make up most of the capital, while working capital is heavy because powertrains and parts are bought ahead and dealers hold stock. Because of this, a detailed Truck Business Plan should model steel and component prices, powertrain supply terms, localisation, product mix by weight class, dealer margins, retail financing, freight cycles, emission and safety compliance costs, exports, receivables, and financing costs together, so that funding supports the plant through ramp-up and demand cycles.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Materials & Components | 75–85% | Powertrain led |
| Utilities | 5–8% | Power, paint ovens |
| Labour | 4–6% | Skilled assemblers |
| Warranty & Service | 2–3% | Field support |
| Logistics & Dealer Support | 2–4% | Freight, marketing |
| Overheads & Compliance | 2–3% | Testing, audits |
With components making up most of the cost, margins depend on sourcing, localisation, and pricing power. A good operating model tracks material cost per vehicle by model, labour hours per vehicle, warranty claims, dealer stock, and realised prices, and tests results against a freight slowdown, higher interest rates, or new compliance costs.
Financial Analysis and Profitability
Based on analysis of a 15,000 unit plant, the financial profile is capital and working capital intensive, with healthy margins in strong years but clear exposure to freight and interest rate cycles. The profitability of the Truck manufacturing business in India improves markedly with a focused product range, reliable powertrain partners, deep localisation, a wide dealer and service network, fleet financing tie-ups, aftermarket parts sales, exports, and early presence in electric and LNG models.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 20–30% | Component cost driven |
| Net Profit Margin | 8–12% | After depreciation, taxes |
| Payback Period | 5–7 Years | Capital intensive |
| IRR (Internal Rate of Return) | 14–20% | Cycle dependent |
| Capacity Utilization (stable ops) | 55–75% | Freight cycles |
| Break-even Capacity Utilization | 45–55% | High fixed costs |
Distribution and the freight cycle decide where a plant lands within these ranges. Makers with strong networks, fleet relationships, and aftermarket income earn steady returns, while those with limited reach struggle to fill capacity in a market led by large brands.
Returns can be strengthened by selling spare parts and service contracts, offering body-building partnerships, entering export markets, adding electric and LNG models, and sharing platforms with bus or defence vehicle programmes.
Key Risks and Mitigation
The main risks are cyclical freight demand, strong competition from established brands, powertrain supply, rising steel and component costs, changing emission and safety rules, and dealer credit. Cycle risk is reduced by exports and a mix of segments; competition by niche focus and service; powertrain risk by long-term partnerships; cost risk by localisation; regulatory risk by early compliance planning; and credit risk by financing partners. Promoters often work with a Truck Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for Truck Manufacturing in India
Approvals for a commercial vehicle plant centre on type approval, emission and safety compliance, and environmental and factory consents, along with incentive registrations and standard business registrations. Promoters setting up a Truck Manufacturing Plant in India generally need the following:
- Type Approval: CMVR certification from ARAI, ICAT, or another authorised agency.
- Emission Norms: Bharat Stage VI certification for diesel and gas models.
- Safety Standards: Compliance with braking, lighting, cab, and AC cabin rules.
- Pollution Control: Consent to Establish and Operate for the paint shop.
- Factory & Fire: Factory license, building plan approval, and fire NOC.
- Electric Models: Battery safety approvals, battery EPR, and PM E-DRIVE registration.
- Business & Trade Registrations: Business registration, GST, Udyam, trademark, and Import Export Code.
Type approval and emission certification are usually on the critical path, followed by pollution consent and dealer onboarding.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, products, state pollution control categories, customer specifications, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Truck Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- GST cut: From 22 September 2025, the GST rate on goods vehicles fell from 28% to 18%, lifting demand.
- Strong demand: In January 2026, domestic CV wholesales rose 27% to 99,544 units, according to ICRA.
- Record year: In FY2026, domestic CV volumes grew 12.6%, with medium, heavy, and light segments above their FY2019 peaks.
- Electric push: In September 2025, Tata Power EV Charging Solutions partnered with VE Commercial Vehicles to support electric trucks.
The common thread is a strong demand upturn after the GST cut, with growth expected to moderate to 4 to 6% in FY2027, and a steady move toward cleaner powertrains. Makers who combine focused products, reliable service, and early investment in new technologies will be best placed to grow.
How a Truck Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from market demand and product strategy to sourcing, process design, plant layout, homologation, approvals, and economics. It helps investors decide the right capacity, location, and product range, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Truck Financial Model covering component and powertrain prices, localisation, labour, utilities, warranty, dealer margins, financing support, compliance costs, product mix, freight cycles, working capital, depreciation, taxes, financing, debt servicing, cash flows, break-even, return on investment, and payback under different demand and price scenarios. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a Truck Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a commercial vehicle project, a strong DPR also clarifies the product range, the powertrain partnerships, the dealer and service plan, and the homologation path, which together are the factors most likely to decide success.
Frequently Asked Questions
What are the first steps to set up a truck manufacturing plant in India?
Start by choosing your segments and markets, such as tippers, intermediate vehicles, or electric models for city logistics. Then commission a feasibility study and DPR, secure land in an automotive cluster, line up powertrain and component partners, design and homologate your models, obtain approvals, build a dealer network, and arrange project financing.
How much does it cost to set up the truck manufacturing plant in India?
Investment ranges from about INR 80–150 crore for a light vehicle assembly unit of 3,000 to 5,000 units a year to INR 900–1,300 crore for an integrated 15,000 unit plant, and INR 3,500–5,000 crore for plants above 50,000 units with engine and axle making.
What are the main steps in truck manufacturing?
The flow runs from frame fabrication and cab body making through painting, chassis assembly, powertrain fitment, cab trim, cab mounting, fluids and electricals, end-of-line testing, and road testing and pre-delivery inspection.
Which machinery does the truck manufacturing plant need?
Key equipment includes press lines, robotic welding cells, a frame line, an ED paint line, topcoat booths, chassis and cab trim conveyors, fastening systems, fluid filling stations, alignment and brake testers, and an emission test bay.
Which components are used for truck manufacturing?
The main components are engines with aftertreatment, gearboxes and axles, frame and cab steel, suspension and brakes, tyres and wheels, wiring harnesses, air-conditioning units, seats, glass, and paint, or battery packs for electric models.
How profitable is truck manufacturing in India?
IMARC estimates a 20 to 30% gross margin and an 8 to 12% net margin for a well-run plant, with payback in about 5 to 7 years. Profitability depends on localisation, volume, dealer reach, and the freight cycle.
Which approvals does the truck manufacturing plant need in India?
Typical approvals include CMVR type approval, Bharat Stage VI emission certification, safety compliance including AC cabins, pollution board consents, factory license and fire NOC, battery approvals for electric models, and GST, Udyam, trademark, and Import Export Code registrations.
How do I get a feasibility study or DPR for the truck manufacturing project?
A detailed feasibility study and DPR covers market and dealers, product range, sourcing, process and layout, homologation, approvals, and full financials. Investors usually engage a Truck Manufacturing Feasibility Study Consultant with experience in automotive and commercial vehicle projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

E-buses run on large lithium-ion battery packs that drive electric traction motors, producing no tailpipe emissions, little noise, and far lower energy and maintenance costs per kilometre than diesel buses.
The Germany Battery Recycling Industry sits where Europe's largest automotive manufacturing base meets its most demanding battery regulation. According to IMARC Group, the market reached USD 814.3 Million in 2025 and is projected to reach USD 1,617.0 Million by 2034, expanding at a CAGR of 7.68% during 2026–2034.
Electric cars are the fastest-growing part of India's passenger vehicle market. Sales roughly doubled in 2025-26, about 6% of new cars sold in the first seven months of 2026 were electric, and more than a dozen models from Indian and global brands now compete across hatchbacks, sedans, and SUVs.
Every electric vehicle needs a charger, and as India's EV fleet grows, so does demand for the equipment that powers it. India registered more than 2.3 million EVs in 2025, public charging stations grew from about 5,000 in 2022 to more than 27,000 by March 2026, and the PM E-DRIVE scheme is funding 72,300 more public chargers by 2028.
Electric vehicles are moving from early adoption to the mainstream in India. Nearly 19 lakh EVs were registered in the first seven months of 2026, and in some segments the shift is already well advanced: more than four in ten new passenger three-wheelers sold in 2026 were electric, while electric two-wheelers, cars, buses, and light commercial vehicles are all gaining share.
Every function in a modern vehicle that moves, from a brake caliper to an air-conditioning flap, depends on an actuator that turns an electronic command into physical motion. The global automotive actuators market size was valued at USD 31.1 Billion in 2025 and is forecast to reach USD 47.3 Billion by 2034, expanding at a compound annual growth rate (CAGR) of 4.62% during 2026–2034, according to IMARC Group.
India is the world's largest two-wheeler market, and it is steadily going electric. Electric scooters, motorcycles, and mopeds offer running costs far below petrol models, suit short urban commutes and delivery work, and are central to the country's clean mobility goals.
Electric bicycles, or e-bikes, combine a conventional bicycle with a small electric motor, a lithium-ion battery, and a controller that assists the rider's pedalling. In India, models limited to 250 watts and 25 km/h do not need registration or a driving license, cost a few paise per kilometre to run, and suit short commutes, fitness riding, students, and last-mile delivery.
Walk into a modern Indian car parts plant, pharmaceutical packing line, or electronics factory and you will see robots welding and palletising, conveyors moving parts between stations, vision cameras checking quality, and control panels coordinating it all.
Tyres are essential to every vehicle on India's roads, from two-wheelers and three-wheelers to cars, buses, trucks, tractors, and off-highway machines.
If the battery is the heart of an electric vehicle, the wiring harness is its nervous system. Every EV needs low-voltage harnesses for lights, sensors, and controls, plus high-voltage harnesses that carry hundreds of volts and high currents between the battery, inverter, motor, and charging port, and dedicated harnesses inside the battery pack that monitor every cell.
Every electric vehicle needs a brain between the battery and the motor. The motor controller, often called the traction inverter in larger vehicles, converts DC power from the battery into precisely controlled AC power for the motor, manages acceleration, regenerative braking, and efficiency, and protects the whole powertrain from faults.
Every vehicle on the road depends on forged parts. Crankshafts, connecting rods, steering knuckles, axle beams, gears, and hubs are forged because the process gives steel a continuous grain flow and the strength to survive millions of load cycles.
Setting up an Automotive Components Manufacturing Plant in India is a high-potential, export-capable venture, powered by the country's large automobile industry, deep supplier base, and growing role as a global sourcing hub for auto parts.
The global automotive lead-acid battery market reached USD 13.89 Billion in 2025 and is projected to reach USD 16.60 Billion by 2034, growing at a CAGR of 1.94% (2026–2034).
Setting up an Electric Scooter Manufacturing Plant in India is a capital-efficient, high-growth venture, driven by the country's rapid shift to electric mobility, supportive EV policies, and surging demand for affordable, clean urban transport. As two-wheelers dominate Indian roads and buyers move from petrol to battery-powered scooter manufacturing, an EV Scooter Manufacturing Plant is one of the most accessible and strategically timed entry points into the electric vehicle economy.
Capital is flowing into the united states used car market because structural affordability pressure, digital retail maturity, and a record-old national vehicle fleet have converged into a genuinely investable thesis.
The Europe Tire Market reached a volume of 458.89 Million Units in 2025 and is projected to reach 565.69 Million Units by 2034, growing at a CAGR of 2.35% (2026–2034).
A strategic analysis of how PLI policies and localization drive global OEM investments. India’s EV battery market hits USD 15,898.31 Million by 2034 (21.7% CAGR).
A tyre is circular in shape and made of a combination of rubber materials that fit perfectly over a circular rim on a wheel, providing traction, load-carrying capabilities, shock absorption, and directional stability. As such, tyres are engineered materials composed of a combination of natural or synthetic materials. They are composed of a combination of materials such as rubber, a combination of materials such as steel or textile, and various chemical materials, among others.
A tractor is a self-propelled, torque-requiring vehicle intended primarily for pulling power at low speeds for agricultural, industrial, and utility purposes. It functions as a mobile power source that can be used for towing, pushing, lifting, or driving a variety of agricultural implements through mechanical, hydraulic, or power take-off systems. Tractors are designed with powerful propulsion systems, sturdy frames, and versatile coupling systems for use on different terrains and under heavy loads.
The electric boat and ship market size is experiencing unparalleled growth as the marine industry embraces electrification on a large scale across different geographies. As sustainability is becoming a strategic priority, with each passing day, more and more marine operators look to electric propulsion technologies as alternatives aimed at cutting down emissions, improving operational efficiencies, and enabling greener ports.
The GCC car rental market has emerged as a critical component of the region's transportation ecosystem, driven by robust tourism activity, expanding business travel, and a substantial expatriate population. Countries across the Gulf Cooperation Council are witnessing unprecedented demand for flexible mobility solutions that cater to diverse customer segments. The GCC car rental market size was valued at USD 1.65 Billion in 2024 as governments prioritize infrastructure development and sustainable tourism initiatives.
The Indian automotive sector has formed a vital part of the country's industrial and economic development for a long period. Over the years, the industry has transformed significantly, influenced by changes in technology, global trends, and consumer preference. Among the various factors shaping its trajectory, government policies have emerged as a decisive force driving growth, innovation, and competitiveness in the India auto parts manufacturing industry.
The India motorcycle tires market continues to evolve in response to changing mobility preferences, rising urbanization, and the growing significance of two-wheelers as essential transportation assets for millions of riders. As per sources, the India motorcycle tires market size reached USD 933.66 Million in 2024. The market is projected to reach USD 2,419.36 Million by 2033, exhibiting a growth rate (CAGR) of 10.3% during 2025-2033.
The Saudi Arabia tire market is undergoing a significant transformation driven by the nation’s economic diversification, rapid urbanization, and growing vehicle ownership. As one of the largest automotive hubs in the Middle East, Saudi Arabia is witnessing increasing demand for both passenger and commercial vehicle tires across urban and industrial regions.
One of the world's most dynamic and quickly changing markets, India's automotive industry is undergoing revolutionary changes in both the new and used car markets. Despite general economic uncertainty, the used car industry has shown remarkable resilience and growth potential, making it a particularly vibrant part of this ecosystem.
One of the world's most vibrant and quickly growing automobile markets is India's passenger car sector. From technological innovation to economic development, a number of interrelated factors have contributed to the sector's remarkable transformation. For stakeholders looking to take advantage of the enormous opportunities in this dynamic market, it is imperative that they comprehend these growth drivers.
India's truck industry is at a turning point in its development, driven by extensive government policies that are changing the commercial vehicle market. The industry, which is the foundation of the country's logistics ecosystem, is gaining previously unheard-of momentum thanks to smart regulatory frameworks and forward-thinking legislative initiatives. A fundamental change in truck operations on Indian highways is being sparked by government initiatives ranging from infrastructure development to emission standards, digitalization, and financial incentives.
The electric rickshaw sector in India has experienced a significant upheaval in recent years and is now a vital part of the country's sustainable transportation network. Strategic government policies aimed at hastening the adoption of clean mobility solutions have played a major role in orchestrating this evolution. India's larger vision of sustainable urbanization is in line with the electric rickshaw industry, which combines social development objectives, economic opportunities, and environmental imperatives.
Transportation in India is undergoing a spectacular change with the advent of electric two-wheelers that are quite an enticing alternative to traditional fuel-powered ones. This change is not merely an act of technological transformation, but an indication of how millions of Indians will think about city mobility, eco-awareness, and economic effectiveness.
As one of the world's leading industrial powerhouses, Japan has long been recognized for its commitment to technological innovation and manufacturing precision. The industry for industrial automation components—encompassing sensors, controllers, actuators, drives, robotics, and human-machine interfaces—represents the backbone of modern manufacturing infrastructure.
The Australian brakes and clutches industry plays a vital role in ensuring vehicle performance, safety, and efficiency across both automotive and industrial segments. As the nation transitions toward electric mobility and smarter manufacturing systems, the demand for advanced braking and clutch mechanisms is rising significantly.
The Philippines automotive wiring harness industry stands at a transformative juncture, driven by technological innovations that are reshaping vehicle electrical architectures worldwide. As vehicles evolve into sophisticated mobile computing platforms, the wiring harness, the circulatory system transmitting electrical power and data throughout modern automobiles, has become increasingly complex and critical to vehicle performance.
Japan's hybrid vehicles market stands as a global benchmark for sustainable mobility innovation, demonstrating remarkable growth and technological leadership. The market achieved a valuation of USD 33.57 Billion in 2024. Japan's hybrid vehicle (HV) market is one of the most established globally, originating with pioneering models like the Toyota Prius. It currently represents a significant portion of the country's automotive sales.
The Japan warehouse robotics market is a highly dynamic and rapidly expanding segment of the global automation industry. The market, valued at USD 414.0 Million in 2024, is on a sharp growth trajectory. Its growth is fueled by critical domestic factors, including a severe labor shortage, the rapid expansion of e-commerce, and Japan's strategic position as a world-leading robotics manufacturer.
The UK is rapidly evolving into a dynamic hub for autonomous vehicle research, testing, and early-stage deployments. A strong ecosystem comprising academic institutions, technology start-ups, automakers, and mobility service providers fosters continuous innovation. Supported by a skilled workforce specializing in software, sensing, robotics, and transportation systems, the nation has become a fertile ground for experimentation.
Japan’s transportation landscape is on the brink of a major shift, with robo taxis, autonomous, driverless vehicles designed for passenger and goods transport, emerging as a practical mobility solution. The Japan robo taxi market reached USD 83.2 Million in 2024 . This remarkable expansion reflects Japan’s broader move toward smart mobility, sustainability, and automation.
The Japan electric truck market is experiencing transformative growth as the nation accelerates toward sustainable transportation and carbon neutrality. As a leading automotive manufacturing hub, Japan is witnessing unprecedented momentum in commercial vehicle electrification, driven by stringent environmental regulations, technological innovation, and strategic government support. The electric truck industry represents a critical component of Japan's commitment to achieving 100% electrified vehicle sales by 2035 and carbon neutrality by 2050.
An EV charging station represents the necessary main infrastructure that allows electrical energy to be transferred from the power grid into electric vehicles to enable their use for transportation. Unlike conventional fueling stations that offer liquid fuels, EV charging stations provide electric power through the use of standardized connectors and smart control systems. The core components include a power conversion unit, which transforms alternating current from the grid into direct current for the vehicle battery; a charging controller controlling communication between the charger and the EV; and a connector or plug matched to the vehicle's charging interface.
An electric scooter is a two-wheeled vehicle powered by an electric motor and rechargeable battery, aimed at offering the means for efficient, eco-friendly, and cost-effective urban mobility. Apart from the traditional scooters that are powered by internal combustion engines, the electric scooters make use of lithium-ion or lead-acid batteries that feed an electric supply to a BLDC motor, which drives the wheels either directly or via a belt or chain mechanism.
Electric bikes, commonly referred to as e-bikes, are one of the most transformational innovations in modern personal mobility, combining conventional bicycle mechanics with advanced electric propulsion technology. At the heart of e-bikes are an electric motor, a rechargeable battery, and a control system that add assistance to the rider while pedaling, making cycling easier, faster, and more accessible across varied terrains. Based on their design, they can be further categorized into pedal-assist, throttle-controlled, or hybrid models, each providing different levels of rider control and engagement of the motor.
The micro-mobility industry has emerged as a transformative force in urban transportation, revolutionizing how people navigate cities worldwide. According to IMARC, the global micro-mobility market size was valued at USD 63.10 Billion in 2024. Looking forward, IMARC Group estimates the market to reach USD 204.83 Billion by 2033, exhibiting a CAGR of 12.86% from 2025-2033.
India's electric vehicle (EV) revolution is accelerating at a breakneck speed, powered by a strategic combination of government incentives, infrastructure investments, and manufacturing policies that are transforming the automotive landscape. The IMARC Group forecasts that the Indian electric car market reached USD 963 Million in 2024.
The diesel engine industry is standing at a transformative crossroads. As global markets are pushing for sustainability, stricter emissions compliance, and cutting-edge innovations, diesel powertrains are facing both immense pressure and promising potential.
The global tire market is a multi-billion-dollar industry, driven by the growing demand for vehicles across emerging economies and the replacement tire segment in developed countries. The global tire market is expected to grow at a compound annual growth rate (CAGR) of 4.70% between 2025 and 2033. The industry is heavily influenced by factors such as technological advancements, raw material prices, environmental regulations, and consumer preferences.
Australia's electric vehicle (EV) sector is experiencing swift expansion, fueled by increasing interest in eco-friendly transportation alternatives. In 2024, sales of battery electric and plug-in hybrid vehicles hit an all-time high, totaling around 114,000 units.
The electric bus industry is the part of the transportation sector that deals with the production and installation of buses that run completely or partially on electricity, employing battery packs or fuel cells in place of conventional diesel or gasoline engines. The buses deliver lower greenhouse gas emissions, lesser noise levels, and enhanced energy efficiency, and thus they are a prime solution for environmentally friendly public transport.
India's electric vehicle market is undergoing a profound transformation, impelled by green priorities, economic imperatives, and changing consumer trends. With rising concerns about air pollution and fossil fuel dependence, electric mobility has become a strategic option for India's transport industry. Policy clarity, technology development, and an emerging ecosystem of makers and suppliers are driving this market shift.
The global electric vehicle market size was valued at USD 755 Billion in 2024. The global EV market is rapidly expanding, driven by technological advancements, government incentives, stricter emission regulations, rising fuel costs, extended battery range, growing environmental consciousness, and significant investments in charging and production infrastructure.
Electric Vehicles, or EVs, are vehicles operated partially or wholly by electrical power, generally with rechargeable battery packs as their fuel. In contrast to conventional internal combustion engine cars, EVs emit no tailpipe emissions, making them a cleaner, environmentally friendly transportation choice. EVs comprise Battery Electric Vehicles (BEVs), Plug-in Hybrid Electric Vehicles (PHEVs), and Hybrid Electric Vehicles (HEVs), and are gaining ground in passenger, commercial, and two-wheeler segments owing to developments in battery technology, charging infrastructure, and policy support.
Aluminum alloy wheels are high-performance, lightweight, and durable components widely used in the automotive industry. Their superior strength-to-weight ratio enhances vehicle efficiency, fuel economy, and handling, making them a preferred choice for both passenger and commercial vehicles. Beyond their functional benefits, aluminum alloy wheels contribute to vehicle aesthetics, offering sleek designs and customization options that appeal to consumers. Their corrosion resistance and thermal conductivity further enhance braking performance and longevity. With increasing demand for fuel-efficient and stylish vehicles, aluminum alloy wheels play a crucial role in the global automotive sector, catering to OEMs, aftermarket suppliers, and performance vehicle manufacturers.
A tyre is a crucial component of a vehicle, serving as the outer covering of a wheel. Its main purposes are to support the vehicle's weight, provide traction for movement, and act as a flexible cushion that absorbs shocks from the road. Usually composed of rubber, tires are strengthened with steel and cloth. Tires for cars, trucks, motorbikes, bicycles, and other vehicles have different designs and compositions depending on the vehicle type and its intended usage. To improve stability and grip, they have a tread pattern on the outside.
Electric kick scooters are small, battery-operated personal transportation vehicles intended for short-distance and urban movement. They offer an economical and environmentally responsible substitute for conventional modes of mobility thanks to their electric engine, rechargeable battery, and lightweight frame. The need for sustainable transportation options, traffic congestion, and growing urbanisation have all contributed to their rise in popularity. Electric kick scooters are now the go-to option for last-mile connectivity and personal commuting because to developments in battery technology, connectivity features, and government programs encouraging micro-mobility.
An automotive wiring harness is an organized assembly of electrical wires, connectors, and terminals that transmit power and signals across a vehicle’s electrical system. It guarantees effective communication between several parts, including the engine control unit, lighting, and sensors. Wiring harnesses are intended to increase vehicle performance and safety by lowering the possibility of short circuits. By maximising electrical connectivity and lowering wire complexity, they are utilised in both conventional and electric automobiles and are essential to contemporary automotive technology.
In an automotive braking system, brake pads are the most important parts since they are engineered to contact the brake rotor to produce friction, thus stopping or slowing down a vehicle in virtually any driving condition safely and efficiently. The key way of classifying these pads is according to their material types: low metallic, ceramic, organic, and semi-metallic.
Tires are essential components of vehicles designed to provide traction, support, and absorb road shocks. Primarily made of rubber, tires consist of treads, belts, and sidewalls that work together to offer grip, stability, and durability. Modern tires come in various types – such as all-season, winter, and performance tires – each engineered for specific driving conditions. The two major tire categories are radial and bias tires, and they are available in different sizes to suit various vehicle types, including passenger cars, light commercial vehicles, medium and heavy commercial vehicles, two-wheelers, and off-road vehicles.
Electric Vehicles (EVs) are powered by electric motors instead of traditional internal combustion engines (ICEs). Electric motors propel EVs by utilizing electricity stored in rechargeable batteries or other energy storage systems. They produce lower or zero tailpipe emissions, reduce air pollution and greenhouse gas (GHG) emissions, and help in mitigating climate change. Electric vehicles consist of various components, such as battery cells and packs, reducers, fuel stacks, power control units, power conditioners, air compressors, humidifiers, motors, on-board chargers, battery management systems, and others. EVs are classified into four types based on propulsion, outlined below.
Saudi Arabia is the second-largest producer and exporter of crude oil and holds the second-largest proven oil reserves in the world, with around 267 billion barrels. The country's oil sector is a significant part of its economy, accounting for 75% of government revenue and approximately 90% of exports. However, due to the volatility of oil prices and the potential for economic instability, Saudi Arabia is increasingly focusing on non-oil activities to reduce its dependency on the oil sector. Non-oil commodities tend to have more stable prices, providing protection against these fluctuations and strengthening the country's social, economic, and financial sectors.