Copper Strips Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
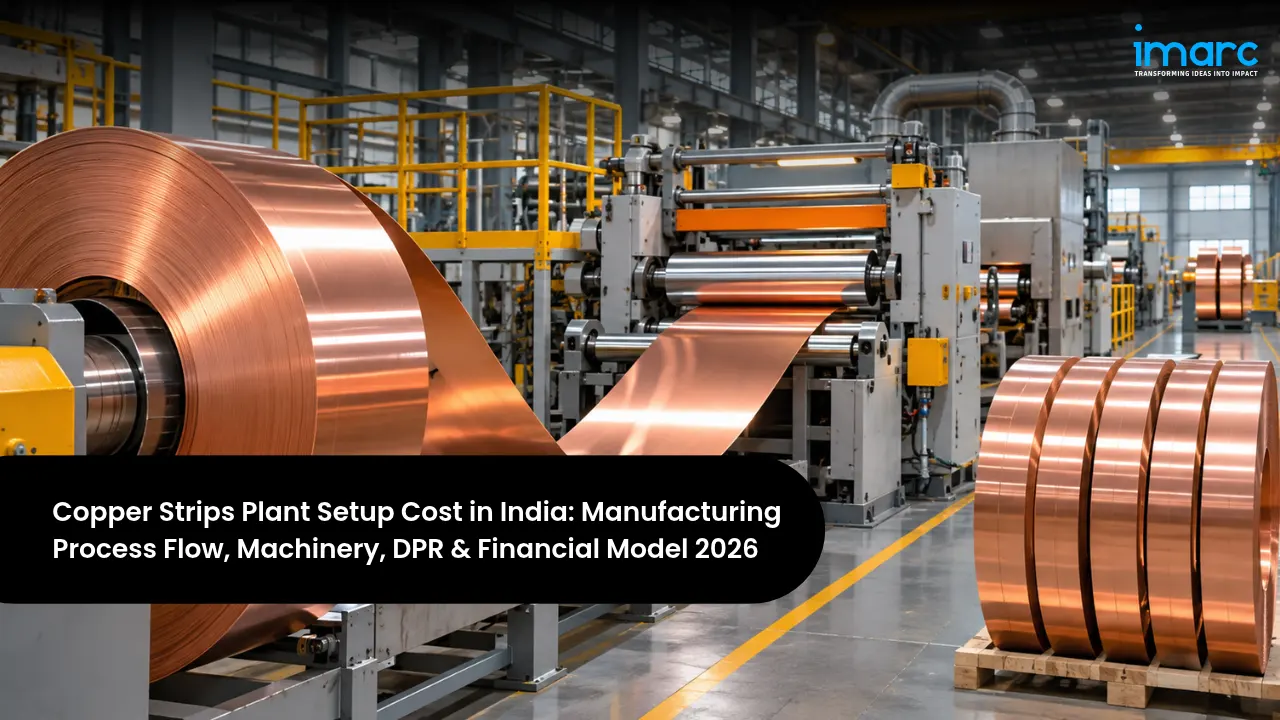
A Copper Strips Manufacturing Plant Setup in India supplies a core material for the country's power, electrical, automotive, and clean energy build-out. Copper strips are flat-rolled copper products, supplied in coils or cut lengths across a range of thicknesses, widths, and tempers. They are used in transformer windings, busbars and switchgear, earthing systems, motors, connectors and terminals, radiators and heat exchangers, solar and battery interconnections, EV components, roofing, and architectural applications. India's copper demand grew 12% in FY 2025–26, led by infrastructure, renewable energy, and transport, and quality control rules now require copper strip for electrical purposes to carry BIS certification, favouring well-equipped domestic producers.
The overall Copper Strips Manufacturing Plant Cost depends mainly on annual capacity, the production route (continuous strip casting and cold rolling, or cake casting with hot and cold rolling), the rolling mill configuration, annealing furnaces and protective atmosphere systems, surface treatment and tinning lines, slitting and finishing equipment, power infrastructure, and especially working capital, because copper metal makes up most of the product value. A plant producing about 15,000 tonnes of copper strips a year typically needs INR 120 crore to INR 200 crore in fixed assets, or about INR 300 crore to INR 450 crore including working capital for copper inventory and receivables, while a smaller re-rolling and slitting unit of 2,000 to 3,000 tonnes a year can start at around INR 40 crore to INR 70 crore including working capital. IMARC Group puts typical capacities at 10,000 to 40,000 tonnes a year, with gross margins of 10 to 18% and net margins of 3 to 8%.
This guide is written for copper and brass processors, cable and conductor makers, transformer and electrical equipment manufacturers, metal traders, and investors exploring how to start a Copper Strips manufacturing plant in India. It explains product types and end uses, demand drivers, the production flow, machinery and raw materials, site selection, a detailed cost and returns breakdown, the BIS and other approvals involved, and how a DPR pulls these elements into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Global Copper Strips Market (2025) | USD 8.50 Billion |
| Global Market Outlook | USD 12.31 Billion by 2034, 4.2% CAGR |
| India Copper Demand (FY 2025–26) | 2,100 Kilotonnes, up 12% |
| India Refined Copper Production (FY 2025–26) | 704 Kilotonnes, up 23%, meeting 58% of demand |
| Typical Plant Capacity | 10,000–40,000 Tonnes a year |
| Indicative Total Investment | INR 300–450 Crore (15,000 TPA, incl. working capital) |
The snapshot shows a steadily growing global market, according to IMARC Group, and strong domestic copper demand, according to the International Copper Association India. Infrastructure accounted for the largest share of incremental demand in FY 2025–26, supported by record solar additions and grid expansion, while domestic refined copper supply is expanding with new smelter capacity, improving the availability of cathode for downstream strip producers.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | ETP and oxygen-free copper strips, busbar flats, earthing strips, tinned strips, thin strips for connectors and solar or battery applications |
| Total Project Investment | INR 300 – 450 Crore incl. working capital (15,000 TPA); INR 40 – 70 Crore (2,000–3,000 TPA re-rolling unit) |
| Payback Period | 5 – 7 Years |
| Net Profit Margin | 3 – 8% (IMARC benchmark) |
| IRR | 14 – 18% |
| Best Locations | Gujarat, Maharashtra, Dadra & Nagar Haveli and Daman & Diu, Haryana, Tamil Nadu, Uttar Pradesh |
| Mandatory Approvals | BIS License (IS 1897), SPCB Consents, Hazardous Waste Authorisation, Factory License, HT Power Connection |
| Key Requirement | Reliable cathode supply, copper price risk management, and tight quality control |
These figures offer a practical frame for early evaluation. Because copper prices are passed through to customers, returns depend mainly on the conversion charge earned per kilogram, metal yield and scrap recovery, rolling and annealing efficiency, energy costs, disciplined hedging of copper price exposure, and long-term supply relationships with transformer, switchgear, and component makers. A capacity- and product-specific Copper Strips Feasibility Report refines these numbers before capital is committed.
Table of Contents
- What is Copper Strips Manufacturing?
- Why is Copper Strips Manufacturing Growing in India?
- Copper Strips Manufacturing Process Flow
- Raw Materials Required for Copper Strips Manufacturing
- Location, Land & Infrastructure
- Copper Strips Manufacturing Machinery and Equipment
- Copper Strips Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Copper Strips Manufacturing in India
- Recent Developments in the India Copper Strips Manufacturing Industry
- How Copper Strips Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Copper Strips Manufacturing?
Copper strip production converts copper cathode into precisely rolled flat products. Cathodes are melted in induction furnaces under a protective cover, and the molten copper is continuously cast into a thick strip or, in larger plants, into cakes that are hot rolled. The cast strip is surface milled to remove defects and then cold rolled in several passes to reduce thickness, with intermediate annealing in bell or continuous furnaces under protective atmosphere to restore ductility. Finish rolling brings the strip to exact gauge, flatness, and temper, after which it is cleaned, optionally tinned or coated, slit to width, levelled, edge conditioned, and tested for electrical conductivity, mechanical properties, and dimensions. A Copper Strips Manufacturing Plant therefore combines melting and casting, rolling, heat treatment, surface treatment, finishing, and metallurgical testing.
Strips are sold to transformer and reactor manufacturers, switchgear and busbar trunking makers, earthing and lightning protection suppliers, motor and generator makers, connector and terminal manufacturers, automotive and EV component suppliers, radiator and heat exchanger producers, solar and battery assemblers, and building and roofing contractors. Buyers expect high electrical conductivity, accurate thickness and width, good flatness and edge quality, the right temper and formability, clean surfaces, BIS-certified material for electrical uses, and reliable delivery at prices linked transparently to copper benchmarks.
- Electrical Copper Strips: For transformer windings, switchgear, and motors.
- Busbar Flats and Earthing Strips: For power distribution and earthing systems.
- High-Conductivity and Oxygen-Free Strips: For electronics, EVs, and demanding applications.
- Tinned and Thin Strips: For connectors, solar ribbons, and battery interconnections.
Main Product Types in Copper Strips Production
The product mix shapes equipment, quality control, and margins:
| Product Type | Description | Key Feature | Primary Market |
|---|---|---|---|
| ETP Copper Strips | Electrolytic tough pitch copper | High conductivity | Transformers, switchgear, motors |
| Busbar Flats & Earthing Strips | Thicker flats and strips | Current carrying capacity | Power distribution, earthing |
| Oxygen-Free Copper Strips | Very low oxygen content | Superior conductivity and formability | Electronics, EV, vacuum devices |
| Tinned / Plated Strips | Tin or other coatings | Corrosion resistance, solderability | Connectors, solar, batteries |
| Thin Precision Strips | Close-tolerance thin gauges | Higher conversion value | Connectors, radiators, shielding |
Many new entrants start with ETP copper strips and busbar flats for transformer, switchgear, and earthing customers, which have steady demand and established specifications, then add thin precision strips, tinned products, and oxygen-free grades as rolling capability, quality systems, and customer approvals mature. Higher-value products earn better conversion margins and reduce dependence on commodity electrical strip.
Why is Copper Strips Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
Demand for copper strips is driven by power infrastructure, renewable energy, electrification of transport, and industrial growth. IMARC Group expects the global copper strips market to grow at 4.2% a year from 2026 to 2034:
- Power transmission and distribution: Grid expansion and new substations need transformers, switchgear, and busbars made with copper strip.
- Renewable energy: Record solar and wind additions increase demand for transformers, inverters, and interconnections.
- Electric vehicles and automotive: EVs use more copper in busbars, battery connections, motors, and charging equipment.
- Buildings and data centres: Commercial real estate, housing, and data centres need switchgear, busbar trunking, and earthing.
- BIS certification: Mandatory BIS certification for electrical copper strip favours certified domestic producers over uncertified imports.
End-Use Market Opportunity
| End Use | Demand Driver | Product Role |
|---|---|---|
| Transformers & Reactors | Grid and renewable expansion | Electrical copper strips |
| Switchgear & Busbar Trunking | Buildings, industry, data centres | Busbar flats, strips |
| Earthing & Lightning Protection | Infrastructure and safety codes | Earthing strips, tinned strips |
| EV, Automotive & Batteries | Electrification of transport | Thin, tinned, OF strips |
| Connectors, Radiators & Electronics | Industrial and consumer growth | Thin precision strips |
The strongest position for a Copper Strips Manufacturing Plant in India combines secure cathode supply, efficient casting and rolling, consistent conductivity and dimensional quality, BIS certification, disciplined copper price risk management, and long-term relationships with transformer, switchgear, and component makers. Producers that can supply thin, precision, and coated strips for EV and electronics customers earn higher conversion margins.
Copper Strips Manufacturing Process Flow
Understanding the Copper Strips Manufacturing Process helps promoters plan casting, rolling, annealing, finishing, layout, staffing, and quality control. Product quality depends on cathode purity, oxygen and hydrogen control during melting, defect-free casting, accurate rolling schedules, controlled annealing under protective atmosphere, clean surface treatment, and precise slitting. The flow below reflects a typical continuous casting and cold rolling plant.
Step-by-Step Copper Strips Production Flow
Copper cathodes are melted in induction furnaces and continuously cast into thick strip, which is surface milled and cold rolled in stages with intermediate annealing. Finish rolling sets the final gauge and temper, and the strip is cleaned, optionally tinned, slit, levelled, tested, and packed in coils or cut lengths.
| Unit Operation | Key Activity |
|---|---|
| Cathode Receiving & Inspection | Check grade and quality |
| Melting | Induction furnace with protective cover |
| Continuous Casting | Cast thick strip or cakes |
| Surface Milling / Hot Rolling | Remove defects, break down cakes |
| Cold Rolling | Reduce thickness in passes |
| Intermediate Annealing | Restore ductility in protective atmosphere |
| Finish Rolling | Final gauge, flatness, temper |
| Cleaning & Surface Treatment | Degrease, pickle, optional tinning |
| Slitting, Levelling & Edge Conditioning | Final width and edge finish |
| Testing & Packing | Conductivity, mechanicals, dimensions |
Two factors decide profitability. The first is the conversion margin: copper metal cost is largely passed through to customers, so profit comes from the conversion charge per kilogram, which depends on product mix, quality, and customer relationships. The second is yield and efficiency: high metal yield, recycling of in-house scrap, low energy use in melting, rolling, and annealing, and high mill utilisation determine how much of that conversion charge becomes profit.
Raw Materials Required for Copper Strips Manufacturing
The main input is copper cathode, supported by in-house and purchased copper scrap, small amounts of alloying elements, protective gases, fluxes and cover materials, rolling oils, and packaging. IMARC Group estimates raw materials at 74 to 82% of operating cost, mainly copper cathode or refined copper, and utilities at 8 to 12%.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Copper Cathode (Grade A) | Main feedstock | Domestic smelters, imports | 70–78% |
| Copper Scrap (Bright, Millberry) | Supplementary feedstock | In-house recycling, scrap dealers | 2–6% |
| Alloying Elements (Tin, Silver, Phosphorus) | Special grades and coatings | Metal suppliers | Below 2% |
| Protective Gases, Charcoal & Fluxes | Melting and annealing atmosphere | Industrial gas and material suppliers | 1–2% |
| Rolling Oils, Chemicals & Packaging | Rolling, cleaning, dispatch | Domestic suppliers | 1–2% |
Copper cathode prices follow international benchmarks such as the LME, and India still relies on imports for a large share of refined copper, although new domestic smelter capacity is improving availability. Plants manage price risk by buying cathode against confirmed orders, using price-linked sales contracts, and hedging on commodity exchanges, while long-term supply agreements with domestic smelters secure consistent quality and volumes.
Location, Land & Infrastructure
Location shapes access to cathode, customers, power, and skilled labour. The best location for Copper Strips manufacturing plant setup lies near copper smelters or major ports for cathode supply, close to clusters of transformer, switchgear, and electrical equipment manufacturers, with reliable and competitively priced high-tension power, good road connectivity, and an industrial zone suited to metal processing.
Preferred States for Copper Strips Plants in India
| State | Why It Works | Key Advantage |
|---|---|---|
| Gujarat | Copper smelters at Dahej and Mundra, Jamnagar metals cluster | Cathode supply, ports |
| Maharashtra | Large electrical equipment and transformer industry | Customers and skills |
| Dadra & Nagar Haveli and Daman & Diu | Silvassa copper and metals cluster | Copper ecosystem |
| Haryana | Electrical OEMs and metal processors in NCR | North India demand |
| Tamil Nadu | Transformer, motor and EV manufacturing | Industrial demand, ports |
| Uttar Pradesh | Growing electrical and electronics base | Large market, incentives |
Gujarat combines domestic copper smelting, ports, and a long-established metals processing cluster, while the Silvassa region hosts copper refining and downstream units. Maharashtra, Tamil Nadu, Haryana, and Uttar Pradesh offer large concentrations of transformer, switchgear, motor, and electrical equipment manufacturers. Because power is a major cost, states and industrial parks with competitive industrial tariffs and reliable supply are preferred.
Product Quality and Standards
Copper strip for electrical purposes must conform to IS 1897 and carry the BIS Standard Mark under the Copper Products Quality Control Order, which specifies chemical composition, electrical conductivity, mechanical properties, dimensions, and tolerances. Customers in automotive, EV, and electronics also require tight thickness and width tolerances, flatness, burr-free edges, and clean surfaces. Key controls include cathode and melt chemistry checks, oxygen control, casting inspection, rolling gauge control, annealing atmosphere monitoring, conductivity and tensile testing, and full coil traceability.
Infrastructure Requirements (15,000 TPA Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 8 – 12 acres | Mill bays, stores, expansion |
| Production Shed | 15,000 – 25,000 m² | Casting, rolling, finishing bays |
| Power | 8 – 15 MW, HT connection | Induction furnaces and mills |
| Protective Gas System | Nitrogen-hydrogen supply | Annealing furnaces |
| Water & Cooling | 100 – 200 KLD, recirculating | Casting and mill cooling |
| Material Handling | EOT cranes, coil handling | Heavy coil movement |
| Laboratory & ETP | Spectrometer, conductivity, tensile; pickling effluent | BIS and customer requirements |
Infrastructure for a copper strips plant centres on a cathode store, melting and casting bay, rolling mill bays with heavy foundations, annealing furnaces with gas supply, cleaning and tinning lines, slitting and finishing areas, overhead cranes, a high-tension substation, cooling towers, an effluent treatment plant, and a metallurgical laboratory. Planning foundations and bay space for an additional finishing mill and slitting line supports future growth.
Copper Strips Manufacturing Machinery and Equipment
Induction furnaces, continuous casting machines, slitting lines, and annealing furnaces are manufactured in India, while high-precision cold rolling and finishing mills with automatic gauge control are often imported from Europe, Japan, or China. The main equipment is summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Induction Melting & Holding Furnaces | Melt cathode and scrap | Protective cover, temperature control |
| Horizontal Continuous Strip Caster | Cast thick strip | Consistent quality, high yield |
| Surface Milling Machine | Remove casting defects | Double-sided milling |
| Hot Rolling Mill (Cake Route) | Break down cast cakes | For large-capacity plants |
| Reversing Cold Rolling Mill | Reduce thickness | 4-high with automatic gauge control |
| Finishing Mill | Final gauge and flatness | Multi-roll precision mill |
| Bell / Continuous Annealing Furnaces | Heat treat strip | Nitrogen-hydrogen atmosphere |
| Cleaning, Pickling & Tinning Line | Surface treatment | Degreasing, pickling, hot-dip or electro tinning |
| Slitting, Levelling & Edge Conditioning Lines | Final width and finish | Precision slitters |
| Laboratory & Packing Equipment | Test and pack coils | Spectrometer, conductivity meter, tensile tester |
Equipment selection should follow capacity, thickness range, and product mix. The cold rolling and finishing mills largely determine gauge accuracy and surface quality, while annealing furnaces determine temper and conductivity. Many promoters begin with continuous strip casting, a reversing cold mill, bell annealing, and slitting for electrical strips, adding a finishing mill, tinning line, and thin-gauge capability as volumes and customer approvals grow.
Copper Strips Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below summarise the capital and operating cost structure of a copper strips plant producing about 15,000 tonnes a year in India. The final Copper Strips Investment Cost for a specific project depends on capacity, production route, mill configuration and origin, annealing and surface treatment systems, power infrastructure, land and building costs, and above all working capital for copper inventory and receivables.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total Project Cost | What It Covers |
|---|---|---|
| Melting & Casting | 9–12% | Induction furnaces, continuous caster, milling |
| Rolling Mills | 14–18% | Cold rolling and finishing mills |
| Annealing & Surface Treatment | 5–7% | Furnaces, gas system, cleaning, tinning |
| Slitting & Finishing | 3–5% | Slitters, levellers, packing |
| Land, Buildings & Cranes | 7–10% | Mill bays, foundations, EOT cranes |
| Utilities | 3–5% | HT substation, cooling, water, ETP |
| Working Capital | 45–58% | Copper inventory, WIP, receivables |
Working capital is the largest component because copper makes up most of the product value and must be held as cathode, work in progress, and finished coils, while customers typically buy on credit. A Copper Strips Business Plan models these components so that capacity, product mix, and financing rest on realistic copper price, conversion charge, and utilisation assumptions.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials | 74–82% | Copper cathode dominates |
| Utilities | 8–12% | Melting, rolling, annealing power |
| Labour | 3–5% | Operators, technicians, metallurgists |
| Consumables | 2–3% | Rolls, oils, gases, cover materials |
| Maintenance | 1–2% | Mills, furnaces, cranes |
| Logistics, Hedging & Overheads | 2–3% | Freight, hedging costs, admin |
With copper making up most of operating cost, profitability depends on conversion charges, metal yield, energy efficiency, product mix, and the cost of financing copper inventory. A sound financial model should test margins against copper price volatility and hedging mismatches, power tariff increases, lower utilisation, competition on conversion charges, and higher interest costs on working capital.
Financial Analysis and Profitability
Copper strip manufacturing is a high-turnover, thin-margin business in which returns depend on efficiency and risk control. The profitability of Copper Strips manufacturing business in India improves with high mill utilisation, strong metal yield and scrap recycling, low energy consumption, disciplined copper price hedging, a mix that includes thin, tinned, and oxygen-free strips, BIS-certified supply to electrical OEMs, and long-term contracts with transformer, switchgear, and EV component makers.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 10–18% | IMARC benchmark |
| Net Profit Margin | 3–8% | After depreciation and Indian corporate taxes |
| Payback Period | 5–7 Years | Working capital intensive |
| IRR (Internal Rate of Return) | 14–18% | Sensitive to conversion charges and utilisation |
| Capacity Utilization (stable ops) | 70–85% | Linked to electrical OEM demand |
| Break-even Capacity Utilization | 50–60% | Thin margins, high turnover |
Conversion margins and risk management are the decisive factors. Because margins are small relative to sales, a few rupees per kilogram in conversion charge, yield, or energy cost make a large difference to returns, and unhedged copper price movements can wipe out profits. Producers that run their mills full, control yield and energy tightly, hedge consistently, and move up the value chain are best placed to earn the expected returns.
Returns can be strengthened by locating near smelters and electrical OEM clusters, securing long-term cathode supply, recycling all process scrap, investing in automatic gauge control and energy-efficient furnaces, adding thin precision, tinned, and oxygen-free products, qualifying with EV, solar, and electronics customers, using rooftop solar to cut power costs, and exporting to markets in the Middle East and Southeast Asia.
Key Risks and Mitigation
The main risks are copper price volatility, high working capital needs and interest costs, dependence on imported cathode, power cost increases, competition on conversion charges, quality failures, and changes in import duties or quality rules. Price risk is reduced through back-to-back buying and hedging; working capital risk through efficient inventory and receivables management; supply risk through domestic smelter contracts; energy risk through efficient equipment and renewable power; competition through product differentiation; and quality risk through BIS-compliant process control.
Licenses and Approvals for Copper Strips Manufacturing in India
A copper strips unit requires quality, environmental, industrial, and business approvals. Promoters typically need the following before starting commercial production:
- BIS License: BIS certification under IS 1897 for copper strip for electrical purposes, mandatory under the Copper Products Quality Control Order.
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, covering furnace emissions and pickling effluent.
- Hazardous Waste Authorisation: Authorisation under the Hazardous and Other Wastes Rules for spent pickling solutions, dross, and sludge.
- Factory License and Safety Approvals: Factory registration, safety approvals for furnaces and cranes, and a Fire NOC.
- PESO License: License for storage of hydrogen, LPG, or other gases used in annealing and heating, where applicable.
- HT Power Connection: High-tension power connection and electrical safety approvals from the state utility and electrical inspectorate.
- Business and Quality Registrations: Company incorporation, GST, an Import Export Code, Udyam registration, and ISO 9001 or IATF 16949 for automotive customers.
BIS certification, pollution consents, and the HT power connection usually sit on the critical path. Engaging a Copper Strips Manufacturing Consultant in India can help promoters select the production route and mill configuration, design an efficient layout, plan copper price risk management, obtain approvals, and secure supply and offtake arrangements.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, product range, capacity, target customers, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Copper Strips Manufacturing Industry
Several recent developments are shaping the Indian copper strips industry:
- BIS certification fully applicable: By 19 April 2025, the Copper Products Quality Control Order requiring copper strip for electrical purposes to conform to IS 1897 and carry the BIS Standard Mark applied to all producers, including small and micro enterprises.
- Domestic copper supply expands: In FY 2025–26, India's primary copper production rose about 25% to around 0.7 million tonnes, with Adani's Kutch Copper smelter contributing output for the first time alongside Hindalco and Vedanta.
- Record copper demand: In October 2026, the International Copper Association India reported that India's copper demand rose 12% to 2,100 kilotonnes in FY 2025–26, led by infrastructure, renewable energy, and transport.
Together these point to strong demand, improving domestic cathode supply, and quality rules that favour certified producers. For new entrants, success depends on efficient rolling, tight quality control, disciplined risk management, and a product mix aligned with power, renewable, and EV customers.
How Copper Strips Manufacturing Project Report and DPR Helps Investors
A detailed Copper Strips Project Report gives investors a structured roadmap covering demand by end use, customer requirements, product mix, cathode supply, production route, machinery, utilities, quality systems, copper price risk management, approvals, and economics. It helps promoters choose the right capacity, route, and product mix, estimate capital expenditure (CapEx) and operating expenditure (OpEx), assess profitability, and identify risks before implementation.
At the core of the DPR is a Copper Strips Financial Model covering production and sales by product, copper price assumptions and pass-through terms, conversion charges, metal yield and scrap recycling, power, labour, consumables, maintenance, hedging costs, working capital for copper inventory and receivables, cash flow projections, break-even, return on investment (ROI), and payback. Because conversion margins and working capital drive returns, lenders expect detailed sensitivity analysis, which is why many promoters engage a Copper Strips Plant Project Report Consultant in India to prepare bank-ready documents.
For a copper strips project specifically, a strong DPR also answers the questions that matter most: where the cathode will come from and on what terms, which customers and products will fill the mill, which production route and mill configuration fit the target thickness range, how copper price exposure will be hedged, and how returns hold up if conversion charges fall, power costs rise, or working capital costs increase. An experienced Copper Strips Manufacturing Feasibility Study Consultant tests these scenarios so that the final plan is one lenders and partners can back with confidence.
Frequently Asked Questions
How do I set up a copper strips manufacturing mill in India?
Start by identifying target customers and products, securing cathode supply, and planning copper price risk management, then commission a feasibility study and DPR. Choose a site near smelters or electrical OEM clusters with reliable HT power, install melting, casting, rolling, annealing, surface treatment, and slitting equipment, obtain BIS, pollution, hazardous waste, and factory approvals, and complete customer qualifications.
What is the cost of setting up a copper strips manufacturing plant in India?
A plant producing about 15,000 tonnes a year typically needs INR 120 crore to INR 200 crore in fixed assets, or about INR 300 crore to INR 450 crore including working capital. A smaller re-rolling and slitting unit of 2,000 to 3,000 tonnes a year can start at around INR 40 crore to INR 70 crore including working capital.
How are copper strips made?
Copper cathodes are melted and continuously cast into thick strip, which is surface milled and cold rolled in passes with intermediate annealing. Finish rolling sets the final gauge and temper, and the strip is cleaned, optionally tinned, slit, levelled, tested, and packed.
What machinery is needed for a copper strips manufacturing plant?
Key equipment includes induction melting and holding furnaces, continuous strip casters, surface milling machines, cold rolling and finishing mills, bell or continuous annealing furnaces, cleaning, pickling, and tinning lines, slitting, levelling, and edge conditioning lines, overhead cranes, and a metallurgical laboratory.
What raw materials are used in manufacturing copper strips?
The main input is Grade A copper cathode, along with copper scrap, small amounts of alloying elements such as tin, silver, and phosphorus, protective gases, charcoal and fluxes, rolling oils, cleaning chemicals, and packaging materials.
Is copper strips manufacturing profitable in India?
Benchmark figures point to a 3 to 8% net margin and an IRR of around 14 to 18%, with payback in 5 to 7 years. Profitability depends mainly on conversion charges, metal yield, energy efficiency, utilisation, copper price hedging, and working capital costs.
What licenses are needed for a copper strips manufacturing unit in India?
A unit typically needs a BIS license under IS 1897, State Pollution Control Board consents, hazardous waste authorisation, a Factory License, a Fire NOC, a PESO license where gases are stored, an HT power connection, GST, and an IEC.
Which state is best for a copper strips manufacturing plant?
Gujarat, Maharashtra, Dadra & Nagar Haveli and Daman & Diu, Haryana, Tamil Nadu, and Uttar Pradesh are strong options. The best site combines cathode access, nearby electrical equipment customers, and competitive industrial power.
How do I get a feasibility study or DPR for a copper strips manufacturing plant?
A professionally prepared DPR covers market and customer analysis, technical design, copper price risk management, approvals, costs, and financial projections for bank appraisal. Many promoters work with a Copper Strips Business Plan Consultant in India to prepare it and align it with lender requirements.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

The Japan real estate market is no longer a purely physical business. Valued at USD 448.31 Billion in 2025, the market is projected to reach USD 576.21 Billion by 2034, expanding at a CAGR of 2.74% during 2026-2034 according to IMARC Group.
A Paver Block Manufacturing Plant Setup in India supplies one of the most widely used building materials in the country's urban and infrastructure boom. Paver blocks are precast concrete units made from cement, stone aggregates, sand, and pigments, pressed and vibrated into interlocking shapes and cured to high strength.
A Copper Pipe Manufacturing Plant Setup in India supplies a material valued for its corrosion resistance, high thermal conductivity, durability, antimicrobial properties, and full recyclability.
A Railway Wagon Manufacturing Plant Setup in India serves one of the country's most important infrastructure priorities: moving more freight by rail. Indian Railways is the world's second-largest freight carrier by volume, and the National Rail Plan aims to raise rail's share of freight from about 27% to 45% by 2030 and double the wagon fleet from around 3 lakh to 6 lakh.
A Medium-Density Fiberboard (MDF) Manufacturing Plant Setup in India gives investors a stake in one of the fastest-changing corners of the wood panel industry. MDF is an engineered board made by breaking plantation wood down into fine fibres, mixing them with resin and wax, and pressing the mat under heat into smooth, uniform panels
A PUF Panel Manufacturing Plant Setup in India serves some of the fastest-moving parts of the construction economy: cold storage, warehousing, pre-engineered buildings, food and pharma processing, clean rooms, and modular structures.
An Engineered Quartz Stone Manufacturing Plant Setup in India places an investor in a sector where the country has become one of the world's major producers. Engineered quartz, often called quartz surfaces or quartz slabs, is made by binding roughly 90% or more crushed natural quartz with polymer resin, pigments, and additives, then compacting the mix under vacuum and vibration into dense, non-porous slabs.
An ERW Steel Pipes Manufacturing Plant Setup in India serves one of the broadest demand bases in the steel value chain. Electric resistance welded (ERW) pipes are made by cold-forming hot-rolled steel strip into a tube and welding the seam with high-frequency current, without any filler metal.
The India Construction Equipment Market stands at a defining crossroads where accelerating infrastructure investment collides with some of the most consequential regulatory changes the sector has ever faced. According to IMARC Group, the market was valued at USD 15.37 Billion in 2025 and is projected to reach USD 29.50 Billion by 2034, growing at a CAGR of 7.52% (2026–2034).
Setting up a WPC Door Manufacturing Plant in India taps into a fast-moving shift in the building materials market. Wood plastic composite (WPC) doors combine wood flour or fibre with PVC or other polymers to create doors and frames that look and work like wood but resist water, termites, rot, and warping.
Setting up a Technical Textiles Manufacturing Plant in India gives investors access to one of the fastest-evolving parts of the textile value chain.
Angle sections are L-shaped profiles made mainly by extruding aluminium alloy billets through a shaped die, then straightening, cutting, and heat treating them.
Japan's construction industry is at an inflection point, and the Japan modular construction market sits at the centre of the response. According to IMARC Group, the Japan modular construction market size increased from USD 18.11 Billion in 2025 to USD 18.85 Billion in 2026 and is projected to reach USD 29.27 Billion by 2034, growing at a compound annual growth rate of 5.65% from 2026 to 2034.
DI pipes are made by treating molten iron with magnesium so that its graphite forms tiny spheres instead of flakes, casting it in spinning water-cooled moulds, and then annealing, zinc coating, cement lining, and testing each pipe.
Gypsum plasterboard is a flat building panel with a core of set gypsum bonded between a face paper and a back paper. Fixed to light steel frames, it creates ceilings, partitions, and wall linings that go up far faster than brick and wet plaster, weigh much less, and resist fire because gypsum holds chemically bound water.
MIG welding wire is a continuous solid wire, usually 0.8 to 1.6 mm in diameter, that is fed through a welding gun and melted by an electric arc under a shielding gas to join metals.
Gypsum board, also called plasterboard or drywall, is a panel made of a set gypsum core sandwiched between two sheets of heavy paper.
Steel forgings are strong, reliable metal parts made by shaping heated steel under the force of presses and hammers, which refines the grain structure and gives far better strength and fatigue resistance than casting or machining from bar.
PVC boards, mainly PVC foam boards and WPC boards, are lightweight, waterproof, termite-proof sheets used as an alternative to plywood and MDF in kitchens, bathrooms, wardrobes, furniture, partitions, signage, and interiors.
Laminated veneer lumber, or LVL, is an engineered wood product made by bonding thin wood veneers with their grain running in the same direction, producing straight, strong, and dimensionally stable members from fast-growing plantation timber.
Fly ash bricks turn a waste product from coal-fired power plants into strong, uniform building blocks that need no firing in a kiln. India's thermal power plants generated about 340 million tonnes of fly ash in 2024-25, and government rules require building projects within 300 km of these plants to use ash-based bricks and blocks where they are priced competitively.
Nuts and bolts hold together almost everything that is built or manufactured, from cars, tractors, and two-wheelers to bridges, towers, railways, machinery, and household appliances.
Precast elements are cast in a factory under controlled conditions and then transported to site, where they are lifted into place like the parts of a kit. India's construction sector is turning to this method to build faster, with better quality and less dependence on site labour.
Rice husk ash (RHA) is the residue left when rice husk is burned, and when the burning is properly controlled it is one of the richest natural sources of amorphous silica, typically 85 to 95% silica by weight.
Concrete poles carry most of India's low-tension and 11 kV distribution lines, as well as street lights, rural feeders, and telecom cables. They are strong, durable, resistant to rust, rot, and termites, need almost no maintenance, and cost less than steel poles, which makes them the default choice for state power distribution companies.
Crushed stone aggregates and manufactured sand are the most widely used construction materials after water. They form the bulk of concrete, the base layers of roads and runways, railway ballast, and the fill under buildings, factories, and ports.
Almost every industrial process generates heat that has to be removed. Power plants, steel mills, refineries, chemical and pharmaceutical units, food processors, plastics moulders, and now data centers all rely on cooling towers, chillers, and heat rejection equipment running around the clock.
Steel is the backbone of India's economic growth. Buildings, bridges, railways, highways, ports, power plants, automobiles, machinery, and household appliances all depend on it. India is the world's second-largest steel producer, and crude steel output reached about 170 million tonnes in 2025-26.
Ready mix concrete (RMC) is concrete batched in a central plant to a precise, engineered mix design and delivered to construction sites in transit mixers, ready to pour.
Open a modular kitchen cabinet, a wardrobe shutter, or an office workstation in India today and there is a good chance it is made from medium density fibreboard.
India is the world's second-largest producer of ceramic tiles, and walking through any new apartment, mall, hospital, or metro station shows why. Tiles have replaced mosaic, stone, and plain cement floors in homes across the country, while large-format glazed vitrified slabs are now standard in premium projects.
Setting up a TMT Bar Manufacturing Plant in India is a high-demand, infrastructure-driven venture, powered by the country's massive construction and housing boom, government infrastructure spending, and steady urbanisation.
Setting up a Cement Manufacturing Plant in India is a capital-intensive, high-demand venture, powered by the country's massive infrastructure programme, housing boom, and status as the world's second-largest cement producer.
Setting up a PVC Panel Manufacturing Plant in India is a high-demand, construction-driven venture, powered by the country's building boom, fast-growing interior and renovation market, and the shift away from plywood and plaster toward affordable, waterproof panels.
Setting up an Electric Motor Manufacturing Plant in India is a high-value, engineering-driven venture, powered by the country's industrial expansion, energy-efficiency push, and the rise of electric vehicles and automation.
Setting up an Iron Ore Pellets Manufacturing Plant in India is a capital-intensive, high-demand venture, powered by the country's ambitious steel-capacity expansion, the shift toward value-added iron ore, and rising demand from blast furnaces and sponge iron units.
The Saudi Arabia construction market has emerged as one of the most closely watched construction economies in the world. The market reached USD 101.4 Billion in 2025 and is projected to reach USD 140.4 Billion by 2034, expanding at a compound annual growth rate (CAGR) of 3.6% between 2026 and 2034.
A WPC (Wood Plastic Composite) door is a type of composite door made from a combination of wood fibers or wood flour and thermoplastic resins like PVC, polyethylene, or polypropylene, with additives to improve durability and processability. The resulting composite material is then extruded or molded into door panels and frames, providing the attractive look of wood and the strength and water-resistance of plastic.
UPVC windows refer to window frames and window assemblies manufactured from ‘unplasticized polyvinyl chloride,’ which is a relatively rigid and strong thermoplastic substance. While PVC is a flexible material that requires the addition of a softening substance called a plasticizer to be formed into a durable performance material, PVC window frames and UPVC window assemblies, for instance, do not display such requirements due to the presence of unplasticizers, a component of the material that provides enhanced strength, stability, and resistance to the elements such as UV radiation, moisture, and temperature changes.
The Saudi Arabia factoring market represents a critical component of the Kingdom's evolving financial services landscape, offering businesses an increasingly popular alternative to traditional bank lending. Factoring, which involves the sale of accounts receivable to a third-party financial institution at a discount, has emerged as a vital mechanism for improving liquidity, managing cash flow, and mitigating credit risk across diverse industry sectors.
The GCC bridge construction market represents a vital component of the region's ambitious infrastructure transformation agenda, serving as a cornerstone for enhanced mobility, economic integration, and sustainable urban development across the Gulf states.
The Australia industrial couplings industry stands at a transformative juncture in 2025, propelled by technological advancement and surging demand across critical sectors. As mechanical devices connecting two shafts to transmit power and torque, industrial couplings form the backbone of machinery operations in manufacturing, mining, automotive, and energy sectors.
The Saudi Arabia real estate market stands at a pivotal juncture in its evolution, representing one of the most dynamic and transformative sectors within the Kingdom's economy. With this country having a very ambitious agenda of economic diversification and modernization, the real estate business has come out as one of the pillars of this transformation.
Steel is an alloy that consists of iron and carbon in addition to trace amounts of other elements like manganese, silicon, chromium, and nickel. The amount of carbon in steel is usually less than two percent and is an important factor in determining the strength, hardness, and ductility of steel.
Saudi Arabia’s precast concrete market reached USD 1.2 Billion in 2024 as per the IMARC Group, clear proof that off-site construction is rapidly becoming the Kingdom’s go-to building solution. With residential, commercial, and major infrastructure projects multiplying, developers are increasingly turning to precast building solutions to keep pace.
The GCC cold storage construction market represents critical infrastructure underpinning regional food security, pharmaceutical distribution, and temperature-sensitive logistics across the Arabian Peninsula. As Gulf Cooperation Council nations diversify their economies and reduce hydrocarbon dependence, robust cold chain infrastructure has emerged as a cornerstone of sustainable development planning.
PVC panels are lightweight, durable building materials made from polyvinyl chloride using extrusion or molding processes. They are available as rigid or semi-rigid sheets designed primarily for wall and ceiling cladding, partitions, and decorative finishes. Known for their excellent resistance to moisture, chemicals, termites, and corrosion, PVC panels offer a smooth surface and a clean, polished look that’s easy to maintain. Available in an extensive range of colors, textures, and patterns, these panels serve as a practical alternative to traditional materials like wood, plaster, or tiles.
Ready mix concrete (RMC) is a precisely engineered construction material produced in a controlled environment within a batching plant and delivered to construction sites in a freshly mixed, plastic state. It is formulated by combining cement, aggregates, water, and chemical or mineral admixtures in carefully proportioned quantities to achieve specific performance characteristics. Unlike site-mixed concrete, RMC ensures consistent quality, uniformity, and superior workability through automated production and quality control processes.
The construction industry across the Gulf Cooperation Council (GCC) member states is at the core of a monumental economic transformation. Far exceeding traditional building activities, the sector now serves as the principal vehicle for national economic diversification strategies, moving these nations beyond reliance on oil revenues.
Paver blocks are precast construction material made basically from cement, aggregates, sand, and pigments for constructing surfacing. They are produced in standardized shape and thickness, allowing each unit to interlock to form a strong, load-bearing surface with no need for continuous concrete pouring. Paver blocks possess high compressive strength, abrasion resistance, and are easy to lay and maintain.
The Brazil ceramic tiles market has witnessed stable growth, reflecting broader trends in the construction and building materials industries of the country. The Brazil ceramic tiles market size was valued at USD 1.6 Billion in 2025. The market is expected to reach USD 2.2 Billion by 2034, exhibiting a CAGR of 3.91% during 2026-2034.
MDF is an engineered wood product produced by breaking down hardwood or softwood residuals into wood fibers, which are then combined with resin binders under heat and pressure. MDF exhibits a homogeneous density, a smooth surface, and fine texture, ensuring a much more workable material compared to natural wood.
Float glass is a type of flat glass that is manufactured by floating molten glass on a bed of molten tin. This produces a smooth, uniform surface and consistent thickness. The float process was developed by Pilkington in the 1950s and revolutionized glassmaking because it enabled the production of large, flawless sheets of glass without needing polishing or grinding. The basic raw materials used-silica sand, soda ash, limestone, and dolomite-are heated in the furnace to a very high temperature, then continuously poured onto the tin bath, where the molten glass spreads out into an even layer. It cools and solidifies into a perfectly flat and perfectly transparent sheet. As it provides optical clarity and strength and is easily processed into coated, laminated, or toughened forms, float glass is used as a basic product for various applications, ranging from architectural and automotive to industrial applications.
ERW steel pipes can be identified as one of the most important categories of welded pipes and find wide applications in infrastructure, construction, and other industries because of their precision, cost-effectiveness, and reliability. The raw material to produce these pipes is either hot-rolled or cold-rolled steel coils that are longitudinally formed and welded by the application of high-frequency electric resistance welding.
Drill bits are specifically designed cutting instruments intended to produce cylindrical holes in various materials, ranging from soft woods and plastics to hardened steels, stone, and rock. Although they seem straightforward, drill bits consist of various specialized shapes, coatings, and materials that are designed to suit the cutting characteristics of the intended material and the requirements of the drilling task.
Concrete is among the most widely used construction materials in the world due to its strength, versatility, and durability. It is a composite material largely made of cement, water, aggregates-sand, gravel, or crushed stone-and in some cases, admixtures which give special properties to the concrete.
Clay bricks are one of the oldest and most extensively used construction materials in the globe, appreciated for their strength, durability, insulation against heat, and beauty. They are produced mainly from natural clay and shale, which are fashioned, dried, and subjected to high-temperature firing to produce a hard, dense material that can resist multiple environmental and structural stresses. The mix generally consists of alumina, silica, lime, iron oxide, and magnesia that collectively decide the color, texture, and performance properties of the brick.
Metal beam crash barriers and high mast light poles are essential infrastructural features providing security and visibility on highways, city roads, and industrial sites. Metal beam crash barriers or guardrails are made of galvanized steel beams, typically W-beam or Thrie-beam, that are designed to dissipate the impact energy on impact with a vehicle and minimize death and damage to vehicles.
Laminated plywood is an engineered wood material that is produced by laminating several layers of thin veneers of wood together with powerful adhesives and covering them with a protective or decorative laminate sheet. This amalgamation not only increases the strength of the plywood but also its beauty, which is why it is extremely versatile for use in furniture, cabinetry, floors, paneling, and interior design.
Ductile iron pipes (DIP) are a key part of new water and wastewater infrastructure, providing enhanced performance capabilities over older piping materials. Cast from ductile cast iron, a material that has the strength of steel combined with the resistance to corrosion of cast iron, these pipes are designed to endure high-pressure use while still being flexible enough to absorb stress without cracking.
The real estate sector plays a critical role in driving economic growth and shaping communities. It significantly contributes to national economies by generating jobs, influencing investment flows, and boosting government revenues through taxes. Beyond these economic benefits, real estate development directly affects the quality of life by creating homes, enhancing infrastructure, and revitalizing urban areas.
Gypsum boards, also referred to as drywall or plasterboard, are lightweight, strong and fireproof building materials that are frequently used for partitions, walls and ceilings. Constructed from a gypsum core encased in paper liners, they provide improved acoustics, cost effectiveness, and speedy installation. Gypsum boards are favoured in industrial, commercial, and residential construction because of its environmentally beneficial qualities, ability to withstand moisture, and ability to insulate against heat. They are an essential part of efficient and sustainable construction methods because of their adaptability to contemporary building processes.
A frameless shower door is a modern and aesthetically appealing bathroom fixture that has gained popularity for its sleek and minimalist design. They are constructed without the bulky metal framing that surrounds the glass panels and are typically made from thick, tempered glass that is securely attached to the wall and floor using hinges or brackets.