Tyre Oil Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
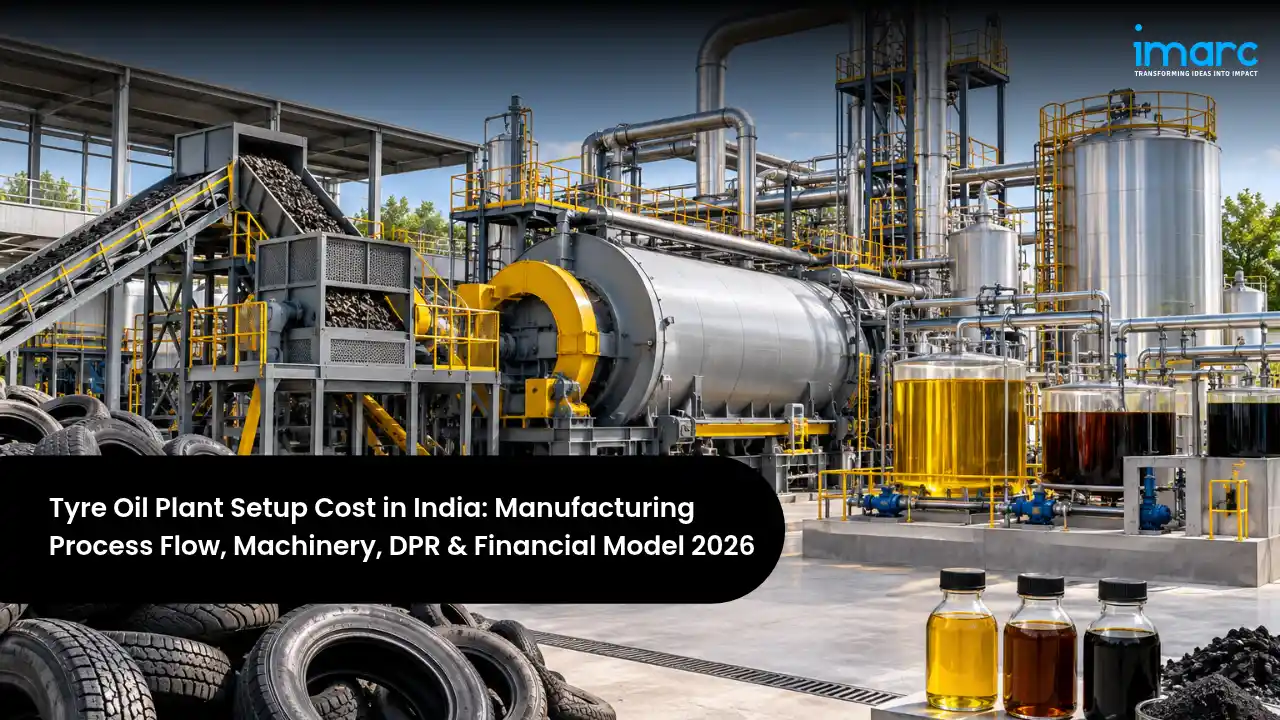
Tyre pyrolysis oil, or TPO, is a dark fuel oil made by heating shredded end-of-life tyres to about 400 to 500°C without oxygen, so that the rubber breaks down into oil vapours, gas, carbon char, and steel wire. The oil is used as a cheaper substitute for furnace oil and light diesel oil in boilers, furnaces, and kilns, and when refined it can be blended into fuels or used as a chemical feedstock, while the char can be milled into recovered carbon black. According to NITI Aayog, India recycled about 3 million tonnes of waste tyres in FY2024, of which about 2.68 million tonnes went to pyrolysis, producing about 1.1 million tonnes of oil. With extended producer responsibility for tyre makers, growing demand for recycled fuels and carbon black, and moves toward national quality standards, Tyre Oil Manufacturing Plant Setup in India is an attractive circular economy opportunity.
Investment depends mainly on daily capacity, whether the plant uses batch or continuous reactors, emission control and monitoring, char refining into carbon black, oil distillation, storage and fire safety, and land and buildings. The Tyre Oil Manufacturing Plant Cost ranges from about INR 2–5 crore for a small batch plant of 10 to 15 tonnes of tyres a day that meets CPCB rules, to INR 50–90 crore for a continuous plant of about 100 tonnes a day with carbon black refining and oil distillation, and INR 200–350 crore for large plants that refine the oil into fuels and chemicals. Waste tyres make up 40 to 50% of operating cost and utilities 25 to 35%. Given low product prices and falling EPR certificate values, a gross margin of 22 to 32% and a net margin of 8 to 15% are realistic for a well-run continuous plant.
This guide is written for investors exploring how to start a Tyre Oil manufacturing plant in India. It focuses on a continuous plant processing about 100 tonnes of tyres a day, or around 30,000 tonnes a year, producing pyrolysis oil for industrial fuel users, recovered carbon black for rubber and plastic makers, and steel wire for recyclers, while earning EPR credits, and also explains small batch plants and large refining plants. It covers products and markets, the demand outlook, the production process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, environmental approvals, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Waste Tyres Recycled (FY2024) | About 3 Million Tonnes |
| Processed by Pyrolysis | About 2.68 Million Tonnes |
| Pyrolysis Oil Produced | About 1.1 Million Tonnes |
| Typical Oil Yield | About 35 – 41% of tyre weight |
| EPR Weightage (Continuous) | 0.8, against 0.5 for batch |
| Indicative Total Investment | INR 2 Crore to 350 Crore |
The snapshot shows that pyrolysis is already India's main way of recycling tyres, but most capacity uses older batch reactors and about 20 to 25% operates outside proper oversight. EPR rules give continuous plants a higher weightage than batch plants, and proposed standards for the oil and carbon black should reward cleaner, better-run facilities.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Pyrolysis oil, carbon black, steel |
| Plant Capacity | 10 – 300+ Tonnes of Tyres a Day |
| Total Project Investment | INR 2–5 Crore (batch plant) to 50–90 Crore (100 TPD continuous plant) |
| Payback Period | 3 – 5 Years |
| Net Profit Margin | 8 – 15% |
| IRR | 18 – 26% |
| Preferred States | Gujarat, Maharashtra, Tamil Nadu, Haryana, Uttar Pradesh, Rajasthan |
| Key Requirement | Pollution consent, steady tyre supply |
These ranges provide a realistic frame for early planning, but actual returns depend on the price and steady supply of waste tyres, the price of fuel oil that pyrolysis oil competes with, the value of EPR certificates, demand and prices for recovered carbon black, oil yield and quality, emission compliance costs, and possible changes in rules on imports, standards, and GST. A site-specific Tyre Oil Feasibility Report narrows each of these assumptions to your chosen capacity, technology, location, and buyers.
Table of Contents
- What is Tyre Oil Manufacturing?
- Why is Tyre Oil Manufacturing Growing in India?
- Tyre Oil Manufacturing Process Flow
- Raw Materials Required for Tyre Oil Manufacturing
- Location, Land & Infrastructure
- Tyre Oil Manufacturing Machinery and Equipment
- Tyre Oil Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Tyre Oil Manufacturing in India
- Recent Developments in the India Tyre Oil Manufacturing Industry
- How a Tyre Oil Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Tyre Oil Manufacturing?
Tyres are made of natural and synthetic rubber, carbon black, steel, and textile. In pyrolysis, the shredded tyres are heated in a sealed reactor without air, so the rubber breaks down into vapours that are cooled into oil, gases that are burned to heat the reactor, carbon char, and steel wire. As a rule of thumb, 100 tonnes of tyres give about 35 to 41 tonnes of oil, 30 to 32 tonnes of char, about 11 tonnes of steel, and the rest as gas. The oil has a heating value close to furnace oil but contains sulphur and must be handled carefully. Oil yield, sulphur and water content, flash point, and char quality decide value.
Commercially, the oil is sold to industries that burn fuel oil, such as ceramic and brick kilns, glass and steel re-rolling units, boilers in textile and food plants, and cement plants, as well as to refiners and chemical buyers for refined grades and to export buyers. A Tyre Oil Manufacturing Plant can serve all these buyers while also selling carbon black, steel, and EPR certificates. Buyers value steady supply, consistent quality, low sulphur and water, and competitive prices.
- Fuel users: Kilns, furnaces, boilers.
- Rubber makers: Recovered carbon black.
- Steel recyclers: Tyre wire.
- Tyre makers: EPR certificates.
The Main Products and Applications
Choosing the product mix is the most important commercial decision, because it determines reactors, refining, and margins:
| Product | Description | Key Property | Primary Demand |
|---|---|---|---|
| Pyrolysis Oil | Crude fuel oil | Cheaper fuel | Boilers, kilns |
| Distilled Oil | Refined fractions | Cleaner burning | Industry, refiners |
| Carbon Black (rCB) | Milled char | Rubber filler | Rubber goods |
| Carbon Char | Raw char | Low-cost fuel | Kilns, cement |
| Steel Wire | Bead and belt wire | Scrap steel | Steel mills |
| Pyrolysis Gas | Non-condensable gas | Process fuel | Own reactor |
These choices shape the whole project. Crude oil and raw char are the simplest products with the lowest prices, while distilled oil and recovered carbon black earn much better prices but need extra equipment, testing, and buyer approvals, and steel wire and gas add steady value.
Why is Tyre Oil Manufacturing Growing in India?
Key Growth Drivers in India and Export Markets
Demand is supported by regulation, fuel costs, and circular economy goals:
- EPR for tyres: Tyre makers must buy recycling certificates for their obligations.
- Fuel costs: Industries look for cheaper alternatives to furnace oil.
- Carbon black demand: Rubber makers seek recovered carbon black to cut emissions.
- Growing tyre waste: More vehicles create more end-of-life tyres every year.
- Exports: Global chemical firms buy refined oil as a feedstock.
India-Specific Market Opportunity
| Segment | Market Context | Manufacturing Role |
|---|---|---|
| Industrial Fuel | Kilns, boilers | Pyrolysis oil |
| Rubber Industry | Green fillers | Recovered carbon |
| Tyre Makers | EPR obligation | Certificates |
| Refiners & Chemicals | Recycled feedstock | Distilled oil |
| Formalisation | Old batch plants | Compliant capacity |
The strongest opportunity lies in replacing polluting batch plants with continuous, well-monitored plants, in refining char into recovered carbon black for rubber and plastic makers, and in distilled oil for chemical buyers. Producers with steady tyre supply, strong emission control, and buyers for higher-value products will be best placed to grow.
Tyre Oil Manufacturing Process Flow
Understanding the process helps you plan equipment, layout, and where cost and quality are decided. The flow runs from receiving and sorting waste tyres, through pulling out the bead wire, shredding the tyres into chips, removing loose steel with magnets, feeding the chips into a sealed reactor, heating them without oxygen, cooling the vapours in condensers to collect oil, cleaning the remaining gas and burning it to heat the reactor, cooling and discharging the char, milling it into carbon black, and storing and dispatching the oil. Heating control decides oil yield, while condensing and gas cleaning decide quality and emissions.
The Tyre Oil Manufacturing Process Flow
The sequence below reflects a continuous plant. Batch plants load whole or cut tyres into rotating reactors, run one cycle, and cool down before unloading.
| Unit Operation | Key Activity |
|---|---|
| Tyre Receiving | Weigh, sort |
| De-beading | Remove bead wire |
| Shredding | Cut into chips |
| Steel Separation | Magnets |
| Feeding | Sealed feeder |
| Pyrolysis | Heat without oxygen |
| Condensation | Cool vapours to oil |
| Gas Cleaning & Reuse | Burn in heater |
| Char Discharge & Milling | Make carbon black |
| Oil Storage & Dispatch | Tanks, tankers |
Two factors decide profitability across this flow. The first is tyre cost and oil yield, because tyres are the main input and their prices have risen with EPR demand, so steady buying, good shredding, and well-controlled heating that gets the most oil from each tonne directly set the margin. The second is the value of by-products, since char sold as raw fuel earns little, while milled and graded carbon black, clean steel, and EPR certificates can add a large share of revenue.
Raw Materials Required for Tyre Oil Manufacturing
The main input is end-of-life tyres from tyre dealers, fleet operators, retreaders, and scrap aggregators, along with start-up fuel such as LPG or the plant's own oil, water for cooling and scrubbing, alkali and other chemicals for gas cleaning and effluent treatment, and bags for carbon black.
| Raw Material | Role in Product | India Sourcing | % of OpEx |
|---|---|---|---|
| Waste Tyres | Feedstock | Dealers, fleets | 40–48% |
| Start-up Fuel | Initial heating | LPG, own oil | 2–4% |
| Water | Cooling, scrubbing | Borewell, supply | 1–2% |
| Chemicals | Gas cleaning, ETP | Domestic suppliers | 1–2% |
| Bags & Packing | Carbon black packs | Domestic suppliers | 1–2% |
Waste tyres are the largest cost, and imports of waste tyres for pyrolysis are not allowed, so plants depend on domestic collection. Long-term agreements with tyre dealers, fleets, and aggregators, and transparent weighing and records for EPR, are essential for steady supply.
Location, Land & Infrastructure
Site selection for a pyrolysis plant is driven by access to large volumes of waste tyres, closeness to industrial users of fuel oil and carbon black, and a site in an industrial area well away from homes, as required by pollution rules. Other factors include state pollution board practices, power and water supply, space for safe tyre storage, and road access for tyre trucks and oil tankers. Locating near cities and transport hubs ensures tyre supply, while locating near kiln and boiler clusters cuts oil delivery costs.
Choosing the Best Location for Tyre Oil Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Gujarat | Morbi, Ahmedabad | Ceramic fuel users |
| Maharashtra | Pune, Nagpur | Fleets, industry |
| Tamil Nadu | Chennai, Coimbatore | Tyre makers |
| Haryana | Panipat, Sonipat | NCR tyre waste |
| Uttar Pradesh | Ghaziabad region | Large tyre waste |
| Rajasthan | Bhiwadi region | Industrial users |
Gujarat combines tyre supply with large ceramic and industrial fuel users, Maharashtra and Tamil Nadu have big fleets and tyre makers, and Haryana, Uttar Pradesh, and Rajasthan sit near the large NCR waste stream and industrial clusters. The final choice should weigh tyre supply, buyers, pollution rules, and land.
Quality, Safety and Environmental Systems
Pyrolysis plants must follow the CPCB standard operating procedure and state pollution board conditions, including closed reactors, proper gas cleaning, safe handling of char and oil, and continuous emission monitoring where required. A credible plant needs a laboratory to test oil for density, viscosity, flash point, water, sulphur, and calorific value, and carbon black for ash, particle size, and surface area, with batch records that support EPR claims. Safety focuses on fire risk from tyres, oil, and gas, reactor pressure, and hot char. Environmental systems cover scrubbers, treatment of pyro-water, odour control, and safe storage. An experienced Tyre Oil Manufacturing Consultant in India can help plan technology, capacity, emission control, and approvals so the plant meets regulatory and buyer requirements from the start.
Infrastructure Requirements (100 TPD Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Plant Land | 4 – 6 acres | Away from homes |
| Tyre Storage | Covered, fire safe | 10 – 15 days stock |
| Process Shed | Reactors, condensers | Hazardous zone |
| Power Supply | 1 – 1.5 MW | DG backup |
| Oil Tank Farm | Above-ground tanks | Licensed storage |
| Emission Control | Scrubbers, OCEMS | CPCB norms |
| Effluent Plant | Pyro-water treatment | Zero discharge |
Safe tyre storage, a well-ventilated process area, licensed oil storage, strong emission control with monitoring, and treatment of pyro-water are the most important infrastructure requirements, since they decide safety, pollution compliance, and the right to keep operating.
Tyre Oil Manufacturing Machinery and Equipment
The equipment set covers de-beading, shredding, steel separation, feeding, pyrolysis, condensing, gas cleaning, char handling and milling, oil refining, and monitoring. The reactors and heating system account for most of the investment, followed by shredding, condensing and gas cleaning, carbon black refining, and safety systems.
| Equipment | Function | Key Specification |
|---|---|---|
| De-beader | Pull bead wire | Hydraulic |
| Tyre Shredder | Cut chips | Twin-shaft |
| Magnetic Separator | Remove steel | Overband |
| Sealed Feeder | Feed reactor | Airlock |
| Continuous Reactor | Heat chips | Rotary or screw |
| Condensers | Recover oil | Shell and tube |
| Gas Scrubber | Clean gas | Alkali wash |
| Char Cooler | Cool char | Water jacketed |
| Carbon Black Mill | Grind char | Fine grinding |
| Distillation Unit | Refine oil | Vacuum type |
| OCEMS | Monitor emissions | Online system |
Machinery should follow the project plan. A small batch plant uses rotating batch reactors, condensers, a scrubber, and oil tanks, while a 100 TPD continuous plant adds shredding, sealed feeding, continuous reactors, carbon black milling, and distillation, and large plants add hydrotreating to make cleaner fuels and chemical feedstocks.
Tyre Oil Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a continuous plant processing about 100 tonnes of tyres a day in India. The final Tyre Oil Investment Cost for your project will depend on capacity, reactor technology, emission control, carbon black and oil refining, storage and safety, land cost, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Shredding & Feeding | 12–15% | De-beader, shredder |
| Pyrolysis Reactors | 30–35% | Reactors, burners |
| Condensing & Gas Cleaning | 12–15% | Condensers, scrubbers |
| Char & Carbon Black | 10–12% | Cooling, milling |
| Tanks, Safety & ETP | 8–10% | Storage, fire, effluent |
| Land, Buildings & Pre-ops | 15–20% | Sheds, fees, trials |
Reactors, shredding, and gas cleaning make up most of the capital, while tyre stocks and oil inventory tie up working capital. Because of this, a detailed Tyre Oil Business Plan should model tyre prices and supply, oil, carbon black, and steel yields and prices, EPR certificate income, emission compliance costs, power and fuel use, possible GST and standards changes, credit terms, and financing costs together, so that funding supports the plant through approvals, commissioning, and market development.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Waste Tyres | 40–50% | Rising with EPR |
| Utilities | 25–30% | Power, fuel |
| Labour | 6–8% | Plant operators |
| Maintenance | 5–7% | Reactor wear |
| Logistics | 4–6% | Tyre collection |
| Compliance & Overheads | 3–5% | Monitoring, audits |
With tyres and utilities making up most of the cost, margins depend on yields, by-product sales, and EPR income. A good operating model tracks oil yield per tonne, carbon black quality and price, fuel use per tonne, plant uptime, and realised prices, and tests results against higher tyre prices, falling fuel oil prices, or lower certificate values.
Financial Analysis and Profitability
Based on analysis of a 100 TPD plant, the financial profile combines moderate capital needs with reasonable margins, supported by EPR rules and industrial fuel demand, though returns depend heavily on tyre prices and by-product values. The profitability of Tyre Oil manufacturing business in India improves markedly with continuous technology that earns higher EPR weightage, refining char into recovered carbon black, distilling oil for higher-value buyers, steady tyre supply contracts, strong emission compliance, and long-term offtake agreements.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 22–32% | Yield driven |
| Net Profit Margin | 8–15% | After depreciation, taxes |
| Payback Period | 3–5 Years | Moderate capital |
| IRR (Internal Rate of Return) | 18–26% | By-product dependent |
| Capacity Utilization (stable ops) | 70–85% | Tyre supply led |
| Break-even Capacity Utilization | 40–50% | Moderate fixed costs |
Technology and product mix decide where a plant lands within these ranges. Continuous plants that sell refined carbon black and oil earn steady returns, while old-style batch plants selling only crude oil and raw char face thin margins and growing regulatory pressure.
Returns can be strengthened by producing recovered carbon black for rubber makers, distilling oil for chemical buyers and exports, using pyrolysis gas to cut fuel costs, and signing long-term tyre supply and EPR agreements with tyre makers.
Key Risks and Mitigation
The main risks are rising tyre prices, falling EPR certificate values due to oversupply, pollution complaints and closure orders, lack of national standards for the oil, fire hazards, and possible changes in import, GST, and end-use rules. Price risk is reduced by supply contracts; certificate risk by not relying on EPR income alone; pollution risk by continuous technology and monitoring; standards risk by testing and buyer specifications; fire risk by strict safety systems; and policy risk by close tracking of rules. Promoters often work with a Tyre Oil Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for Tyre Oil Manufacturing in India
Approvals for a pyrolysis plant centre on pollution control, waste recycling registration under EPR rules, safe storage of oil, and factory and fire safety, along with standard business registrations. Promoters setting up a Tyre Oil Manufacturing Plant in India generally need the following:
- Pollution Control: Consent to Establish and Operate under CPCB norms for tyre pyrolysis.
- Waste Authorisation: Authorisation under the Hazardous and Other Wastes Rules.
- EPR Registration: Registration as a waste tyre recycler on the CPCB portal.
- Oil Storage: PESO license for storing oil above set limits.
- Factory & Fire: Factory license, building plan approval, and fire NOC.
- Monitoring: Online emission monitoring linked to the pollution board where required.
- Business & Trade Registrations: Business registration, GST, Udyam, trademark, and Import Export Code.
Pollution board consent and EPR registration are usually on the critical path, since the plant cannot operate or earn certificates without them.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, products, state pollution control categories, customer specifications, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Tyre Oil Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- Certificate surplus: By September 2025, EPR certificates of 9.2 million tonnes had been generated against 6.2 million tonnes of obligations.
- NITI Aayog study: In January 2026, NITI Aayog found pyrolysis handled about 2.68 million tonnes of tyres a year.
- Chemical feedstock: In February 2026, France formally recognised the oil as a raw material for its chemical industry.
- Proposed reforms: In May 2026, NITI Aayog proposed standards for the oil and carbon black, lower GST, and mandatory emission monitoring.
The common thread is a large and growing recycling industry, an oversupply of certificates, and a clear push toward cleaner technology and quality standards. Producers who combine continuous plants, strong emission control, and higher-value products will be best placed to grow.
How a Tyre Oil Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from feedstock and market strategy to technology choice, process design, plant layout, emission control, approvals, and economics. It helps investors decide the right capacity, location, and technology, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Tyre Oil Financial Model covering tyre volumes and prices, oil, carbon black, steel, and gas yields, product prices, EPR certificate income, utilities, labour, maintenance, logistics, compliance costs, working capital, depreciation, taxes, financing, debt servicing, cash flows, break-even, return on investment, and payback under different tyre price and product price scenarios. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a Tyre Oil Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a pyrolysis project, a strong DPR also clarifies the tyre sourcing plan, the technology partner, the emission control design, and the offtake strategy for oil and carbon black, which together are the factors most likely to decide success.
Frequently Asked Questions
What are the first steps to set up a tyre oil manufacturing plant in India?
Start by choosing the capacity and technology, preferably continuous, and identifying tyre sources and buyers for oil and carbon black. Then commission a feasibility study and DPR, secure land in an industrial area away from homes, obtain pollution board consent and EPR registration, install emission control and monitoring, and arrange project financing.
How much does it cost to set up the tyre oil manufacturing plant in India?
Investment ranges from about INR 2–5 crore for a small compliant batch plant of 10 to 15 tonnes a day to INR 50–90 crore for a 100 TPD continuous plant with carbon black and oil refining, and INR 200–350 crore for large plants that refine oil into fuels and chemicals.
What are the main steps in making tyre oil?
The flow runs from tyre receiving and de-beading through shredding, steel separation, feeding, pyrolysis, condensation, gas cleaning and reuse, char discharge and milling, and oil storage and dispatch.
Which machinery does the tyre oil manufacturing plant need?
Key equipment includes a de-beader, a tyre shredder, a magnetic separator, a sealed feeder, a continuous reactor, condensers, a gas scrubber, a char cooler, a carbon black mill, a distillation unit, and an online emission monitoring system.
What raw materials are used for tyre oil manufacturing?
The main raw material is end-of-life tyres, along with start-up fuel, water for cooling and scrubbing, chemicals for gas cleaning and effluent treatment, and bags for carbon black.
How profitable is tyre oil manufacturing in India?
A well-run continuous plant can expect a 22 to 32% gross margin and an 8 to 15% net margin, with payback in about 3 to 5 years. Profitability depends on tyre prices, oil and carbon black prices, EPR income, and emission compliance.
Which approvals does the tyre oil manufacturing plant need in India?
Typical approvals include pollution board consents under CPCB norms, hazardous waste authorisation, EPR registration as a tyre recycler, a PESO license for oil storage, factory license and fire NOC, emission monitoring, and GST, Udyam, trademark, and Import Export Code registrations.
How do I get a feasibility study or DPR for the tyre oil manufacturing project?
A detailed feasibility study and DPR covers feedstock, markets, technology, process and layout, emission control, approvals, and full financials. Investors usually engage a Tyre Oil Manufacturing Feasibility Study Consultant with experience in waste recycling and energy projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

A farm tractor is built around a frameless chassis in which the engine, clutch housing, gearbox, and rear axle are bolted together to carry the load, with a hydraulic lift and three-point linkage at the back, a power take-off shaft to drive implements, and large rear tyres for traction.
A traction battery is built from lithium-ion cells, each made by coating metal foils with cathode and anode materials, assembling them with a separator and electrolyte inside a sealed case, and charging them for the first time in a controlled formation process.
A goods carrier is built on a ladder-frame chassis of heavy steel side members, onto which the engine, gearbox, axles, suspension, brakes, fuel or battery system, and a pressed and welded cab are fitted, before the vehicle is painted, tested, and sent to body builders or customers.
E-buses run on large lithium-ion battery packs that drive electric traction motors, producing no tailpipe emissions, little noise, and far lower energy and maintenance costs per kilometre than diesel buses.
The Germany Battery Recycling Industry sits where Europe's largest automotive manufacturing base meets its most demanding battery regulation. According to IMARC Group, the market reached USD 814.3 Million in 2025 and is projected to reach USD 1,617.0 Million by 2034, expanding at a CAGR of 7.68% during 2026–2034.
Electric cars are the fastest-growing part of India's passenger vehicle market. Sales roughly doubled in 2025-26, about 6% of new cars sold in the first seven months of 2026 were electric, and more than a dozen models from Indian and global brands now compete across hatchbacks, sedans, and SUVs.
Every electric vehicle needs a charger, and as India's EV fleet grows, so does demand for the equipment that powers it. India registered more than 2.3 million EVs in 2025, public charging stations grew from about 5,000 in 2022 to more than 27,000 by March 2026, and the PM E-DRIVE scheme is funding 72,300 more public chargers by 2028.
Electric vehicles are moving from early adoption to the mainstream in India. Nearly 19 lakh EVs were registered in the first seven months of 2026, and in some segments the shift is already well advanced: more than four in ten new passenger three-wheelers sold in 2026 were electric, while electric two-wheelers, cars, buses, and light commercial vehicles are all gaining share.
Every function in a modern vehicle that moves, from a brake caliper to an air-conditioning flap, depends on an actuator that turns an electronic command into physical motion. The global automotive actuators market size was valued at USD 31.1 Billion in 2025 and is forecast to reach USD 47.3 Billion by 2034, expanding at a compound annual growth rate (CAGR) of 4.62% during 2026–2034, according to IMARC Group.
India is the world's largest two-wheeler market, and it is steadily going electric. Electric scooters, motorcycles, and mopeds offer running costs far below petrol models, suit short urban commutes and delivery work, and are central to the country's clean mobility goals.
Electric bicycles, or e-bikes, combine a conventional bicycle with a small electric motor, a lithium-ion battery, and a controller that assists the rider's pedalling. In India, models limited to 250 watts and 25 km/h do not need registration or a driving license, cost a few paise per kilometre to run, and suit short commutes, fitness riding, students, and last-mile delivery.
Walk into a modern Indian car parts plant, pharmaceutical packing line, or electronics factory and you will see robots welding and palletising, conveyors moving parts between stations, vision cameras checking quality, and control panels coordinating it all.
Tyres are essential to every vehicle on India's roads, from two-wheelers and three-wheelers to cars, buses, trucks, tractors, and off-highway machines.
If the battery is the heart of an electric vehicle, the wiring harness is its nervous system. Every EV needs low-voltage harnesses for lights, sensors, and controls, plus high-voltage harnesses that carry hundreds of volts and high currents between the battery, inverter, motor, and charging port, and dedicated harnesses inside the battery pack that monitor every cell.
Every electric vehicle needs a brain between the battery and the motor. The motor controller, often called the traction inverter in larger vehicles, converts DC power from the battery into precisely controlled AC power for the motor, manages acceleration, regenerative braking, and efficiency, and protects the whole powertrain from faults.
Every vehicle on the road depends on forged parts. Crankshafts, connecting rods, steering knuckles, axle beams, gears, and hubs are forged because the process gives steel a continuous grain flow and the strength to survive millions of load cycles.
Setting up an Automotive Components Manufacturing Plant in India is a high-potential, export-capable venture, powered by the country's large automobile industry, deep supplier base, and growing role as a global sourcing hub for auto parts.
The global automotive lead-acid battery market reached USD 13.89 Billion in 2025 and is projected to reach USD 16.60 Billion by 2034, growing at a CAGR of 1.94% (2026–2034).
Setting up an Electric Scooter Manufacturing Plant in India is a capital-efficient, high-growth venture, driven by the country's rapid shift to electric mobility, supportive EV policies, and surging demand for affordable, clean urban transport. As two-wheelers dominate Indian roads and buyers move from petrol to battery-powered scooter manufacturing, an EV Scooter Manufacturing Plant is one of the most accessible and strategically timed entry points into the electric vehicle economy.
Capital is flowing into the united states used car market because structural affordability pressure, digital retail maturity, and a record-old national vehicle fleet have converged into a genuinely investable thesis.
The Europe Tire Market reached a volume of 458.89 Million Units in 2025 and is projected to reach 565.69 Million Units by 2034, growing at a CAGR of 2.35% (2026–2034).
A strategic analysis of how PLI policies and localization drive global OEM investments. India’s EV battery market hits USD 15,898.31 Million by 2034 (21.7% CAGR).
A tyre is circular in shape and made of a combination of rubber materials that fit perfectly over a circular rim on a wheel, providing traction, load-carrying capabilities, shock absorption, and directional stability. As such, tyres are engineered materials composed of a combination of natural or synthetic materials. They are composed of a combination of materials such as rubber, a combination of materials such as steel or textile, and various chemical materials, among others.
A tractor is a self-propelled, torque-requiring vehicle intended primarily for pulling power at low speeds for agricultural, industrial, and utility purposes. It functions as a mobile power source that can be used for towing, pushing, lifting, or driving a variety of agricultural implements through mechanical, hydraulic, or power take-off systems. Tractors are designed with powerful propulsion systems, sturdy frames, and versatile coupling systems for use on different terrains and under heavy loads.
The electric boat and ship market size is experiencing unparalleled growth as the marine industry embraces electrification on a large scale across different geographies. As sustainability is becoming a strategic priority, with each passing day, more and more marine operators look to electric propulsion technologies as alternatives aimed at cutting down emissions, improving operational efficiencies, and enabling greener ports.
The GCC car rental market has emerged as a critical component of the region's transportation ecosystem, driven by robust tourism activity, expanding business travel, and a substantial expatriate population. Countries across the Gulf Cooperation Council are witnessing unprecedented demand for flexible mobility solutions that cater to diverse customer segments. The GCC car rental market size was valued at USD 1.65 Billion in 2024 as governments prioritize infrastructure development and sustainable tourism initiatives.
The Indian automotive sector has formed a vital part of the country's industrial and economic development for a long period. Over the years, the industry has transformed significantly, influenced by changes in technology, global trends, and consumer preference. Among the various factors shaping its trajectory, government policies have emerged as a decisive force driving growth, innovation, and competitiveness in the India auto parts manufacturing industry.
The India motorcycle tires market continues to evolve in response to changing mobility preferences, rising urbanization, and the growing significance of two-wheelers as essential transportation assets for millions of riders. As per sources, the India motorcycle tires market size reached USD 933.66 Million in 2024. The market is projected to reach USD 2,419.36 Million by 2033, exhibiting a growth rate (CAGR) of 10.3% during 2025-2033.
The Saudi Arabia tire market is undergoing a significant transformation driven by the nation’s economic diversification, rapid urbanization, and growing vehicle ownership. As one of the largest automotive hubs in the Middle East, Saudi Arabia is witnessing increasing demand for both passenger and commercial vehicle tires across urban and industrial regions.
One of the world's most dynamic and quickly changing markets, India's automotive industry is undergoing revolutionary changes in both the new and used car markets. Despite general economic uncertainty, the used car industry has shown remarkable resilience and growth potential, making it a particularly vibrant part of this ecosystem.
One of the world's most vibrant and quickly growing automobile markets is India's passenger car sector. From technological innovation to economic development, a number of interrelated factors have contributed to the sector's remarkable transformation. For stakeholders looking to take advantage of the enormous opportunities in this dynamic market, it is imperative that they comprehend these growth drivers.
India's truck industry is at a turning point in its development, driven by extensive government policies that are changing the commercial vehicle market. The industry, which is the foundation of the country's logistics ecosystem, is gaining previously unheard-of momentum thanks to smart regulatory frameworks and forward-thinking legislative initiatives. A fundamental change in truck operations on Indian highways is being sparked by government initiatives ranging from infrastructure development to emission standards, digitalization, and financial incentives.
The electric rickshaw sector in India has experienced a significant upheaval in recent years and is now a vital part of the country's sustainable transportation network. Strategic government policies aimed at hastening the adoption of clean mobility solutions have played a major role in orchestrating this evolution. India's larger vision of sustainable urbanization is in line with the electric rickshaw industry, which combines social development objectives, economic opportunities, and environmental imperatives.
Transportation in India is undergoing a spectacular change with the advent of electric two-wheelers that are quite an enticing alternative to traditional fuel-powered ones. This change is not merely an act of technological transformation, but an indication of how millions of Indians will think about city mobility, eco-awareness, and economic effectiveness.
As one of the world's leading industrial powerhouses, Japan has long been recognized for its commitment to technological innovation and manufacturing precision. The industry for industrial automation components—encompassing sensors, controllers, actuators, drives, robotics, and human-machine interfaces—represents the backbone of modern manufacturing infrastructure.
The Australian brakes and clutches industry plays a vital role in ensuring vehicle performance, safety, and efficiency across both automotive and industrial segments. As the nation transitions toward electric mobility and smarter manufacturing systems, the demand for advanced braking and clutch mechanisms is rising significantly.
The Philippines automotive wiring harness industry stands at a transformative juncture, driven by technological innovations that are reshaping vehicle electrical architectures worldwide. As vehicles evolve into sophisticated mobile computing platforms, the wiring harness, the circulatory system transmitting electrical power and data throughout modern automobiles, has become increasingly complex and critical to vehicle performance.
Japan's hybrid vehicles market stands as a global benchmark for sustainable mobility innovation, demonstrating remarkable growth and technological leadership. The market achieved a valuation of USD 33.57 Billion in 2024. Japan's hybrid vehicle (HV) market is one of the most established globally, originating with pioneering models like the Toyota Prius. It currently represents a significant portion of the country's automotive sales.
The Japan warehouse robotics market is a highly dynamic and rapidly expanding segment of the global automation industry. The market, valued at USD 414.0 Million in 2024, is on a sharp growth trajectory. Its growth is fueled by critical domestic factors, including a severe labor shortage, the rapid expansion of e-commerce, and Japan's strategic position as a world-leading robotics manufacturer.
The UK is rapidly evolving into a dynamic hub for autonomous vehicle research, testing, and early-stage deployments. A strong ecosystem comprising academic institutions, technology start-ups, automakers, and mobility service providers fosters continuous innovation. Supported by a skilled workforce specializing in software, sensing, robotics, and transportation systems, the nation has become a fertile ground for experimentation.
Japan’s transportation landscape is on the brink of a major shift, with robo taxis, autonomous, driverless vehicles designed for passenger and goods transport, emerging as a practical mobility solution. The Japan robo taxi market reached USD 83.2 Million in 2024 . This remarkable expansion reflects Japan’s broader move toward smart mobility, sustainability, and automation.
The Japan electric truck market is experiencing transformative growth as the nation accelerates toward sustainable transportation and carbon neutrality. As a leading automotive manufacturing hub, Japan is witnessing unprecedented momentum in commercial vehicle electrification, driven by stringent environmental regulations, technological innovation, and strategic government support. The electric truck industry represents a critical component of Japan's commitment to achieving 100% electrified vehicle sales by 2035 and carbon neutrality by 2050.
An EV charging station represents the necessary main infrastructure that allows electrical energy to be transferred from the power grid into electric vehicles to enable their use for transportation. Unlike conventional fueling stations that offer liquid fuels, EV charging stations provide electric power through the use of standardized connectors and smart control systems. The core components include a power conversion unit, which transforms alternating current from the grid into direct current for the vehicle battery; a charging controller controlling communication between the charger and the EV; and a connector or plug matched to the vehicle's charging interface.
An electric scooter is a two-wheeled vehicle powered by an electric motor and rechargeable battery, aimed at offering the means for efficient, eco-friendly, and cost-effective urban mobility. Apart from the traditional scooters that are powered by internal combustion engines, the electric scooters make use of lithium-ion or lead-acid batteries that feed an electric supply to a BLDC motor, which drives the wheels either directly or via a belt or chain mechanism.
Electric bikes, commonly referred to as e-bikes, are one of the most transformational innovations in modern personal mobility, combining conventional bicycle mechanics with advanced electric propulsion technology. At the heart of e-bikes are an electric motor, a rechargeable battery, and a control system that add assistance to the rider while pedaling, making cycling easier, faster, and more accessible across varied terrains. Based on their design, they can be further categorized into pedal-assist, throttle-controlled, or hybrid models, each providing different levels of rider control and engagement of the motor.
The micro-mobility industry has emerged as a transformative force in urban transportation, revolutionizing how people navigate cities worldwide. According to IMARC, the global micro-mobility market size was valued at USD 63.10 Billion in 2024. Looking forward, IMARC Group estimates the market to reach USD 204.83 Billion by 2033, exhibiting a CAGR of 12.86% from 2025-2033.
India's electric vehicle (EV) revolution is accelerating at a breakneck speed, powered by a strategic combination of government incentives, infrastructure investments, and manufacturing policies that are transforming the automotive landscape. The IMARC Group forecasts that the Indian electric car market reached USD 963 Million in 2024.
The diesel engine industry is standing at a transformative crossroads. As global markets are pushing for sustainability, stricter emissions compliance, and cutting-edge innovations, diesel powertrains are facing both immense pressure and promising potential.
The global tire market is a multi-billion-dollar industry, driven by the growing demand for vehicles across emerging economies and the replacement tire segment in developed countries. The global tire market is expected to grow at a compound annual growth rate (CAGR) of 4.70% between 2025 and 2033. The industry is heavily influenced by factors such as technological advancements, raw material prices, environmental regulations, and consumer preferences.
Australia's electric vehicle (EV) sector is experiencing swift expansion, fueled by increasing interest in eco-friendly transportation alternatives. In 2024, sales of battery electric and plug-in hybrid vehicles hit an all-time high, totaling around 114,000 units.
The electric bus industry is the part of the transportation sector that deals with the production and installation of buses that run completely or partially on electricity, employing battery packs or fuel cells in place of conventional diesel or gasoline engines. The buses deliver lower greenhouse gas emissions, lesser noise levels, and enhanced energy efficiency, and thus they are a prime solution for environmentally friendly public transport.
India's electric vehicle market is undergoing a profound transformation, impelled by green priorities, economic imperatives, and changing consumer trends. With rising concerns about air pollution and fossil fuel dependence, electric mobility has become a strategic option for India's transport industry. Policy clarity, technology development, and an emerging ecosystem of makers and suppliers are driving this market shift.
The global electric vehicle market size was valued at USD 755 Billion in 2024. The global EV market is rapidly expanding, driven by technological advancements, government incentives, stricter emission regulations, rising fuel costs, extended battery range, growing environmental consciousness, and significant investments in charging and production infrastructure.
Electric Vehicles, or EVs, are vehicles operated partially or wholly by electrical power, generally with rechargeable battery packs as their fuel. In contrast to conventional internal combustion engine cars, EVs emit no tailpipe emissions, making them a cleaner, environmentally friendly transportation choice. EVs comprise Battery Electric Vehicles (BEVs), Plug-in Hybrid Electric Vehicles (PHEVs), and Hybrid Electric Vehicles (HEVs), and are gaining ground in passenger, commercial, and two-wheeler segments owing to developments in battery technology, charging infrastructure, and policy support.
Aluminum alloy wheels are high-performance, lightweight, and durable components widely used in the automotive industry. Their superior strength-to-weight ratio enhances vehicle efficiency, fuel economy, and handling, making them a preferred choice for both passenger and commercial vehicles. Beyond their functional benefits, aluminum alloy wheels contribute to vehicle aesthetics, offering sleek designs and customization options that appeal to consumers. Their corrosion resistance and thermal conductivity further enhance braking performance and longevity. With increasing demand for fuel-efficient and stylish vehicles, aluminum alloy wheels play a crucial role in the global automotive sector, catering to OEMs, aftermarket suppliers, and performance vehicle manufacturers.
A tyre is a crucial component of a vehicle, serving as the outer covering of a wheel. Its main purposes are to support the vehicle's weight, provide traction for movement, and act as a flexible cushion that absorbs shocks from the road. Usually composed of rubber, tires are strengthened with steel and cloth. Tires for cars, trucks, motorbikes, bicycles, and other vehicles have different designs and compositions depending on the vehicle type and its intended usage. To improve stability and grip, they have a tread pattern on the outside.
Electric kick scooters are small, battery-operated personal transportation vehicles intended for short-distance and urban movement. They offer an economical and environmentally responsible substitute for conventional modes of mobility thanks to their electric engine, rechargeable battery, and lightweight frame. The need for sustainable transportation options, traffic congestion, and growing urbanisation have all contributed to their rise in popularity. Electric kick scooters are now the go-to option for last-mile connectivity and personal commuting because to developments in battery technology, connectivity features, and government programs encouraging micro-mobility.
An automotive wiring harness is an organized assembly of electrical wires, connectors, and terminals that transmit power and signals across a vehicle’s electrical system. It guarantees effective communication between several parts, including the engine control unit, lighting, and sensors. Wiring harnesses are intended to increase vehicle performance and safety by lowering the possibility of short circuits. By maximising electrical connectivity and lowering wire complexity, they are utilised in both conventional and electric automobiles and are essential to contemporary automotive technology.
In an automotive braking system, brake pads are the most important parts since they are engineered to contact the brake rotor to produce friction, thus stopping or slowing down a vehicle in virtually any driving condition safely and efficiently. The key way of classifying these pads is according to their material types: low metallic, ceramic, organic, and semi-metallic.
Tires are essential components of vehicles designed to provide traction, support, and absorb road shocks. Primarily made of rubber, tires consist of treads, belts, and sidewalls that work together to offer grip, stability, and durability. Modern tires come in various types – such as all-season, winter, and performance tires – each engineered for specific driving conditions. The two major tire categories are radial and bias tires, and they are available in different sizes to suit various vehicle types, including passenger cars, light commercial vehicles, medium and heavy commercial vehicles, two-wheelers, and off-road vehicles.
Electric Vehicles (EVs) are powered by electric motors instead of traditional internal combustion engines (ICEs). Electric motors propel EVs by utilizing electricity stored in rechargeable batteries or other energy storage systems. They produce lower or zero tailpipe emissions, reduce air pollution and greenhouse gas (GHG) emissions, and help in mitigating climate change. Electric vehicles consist of various components, such as battery cells and packs, reducers, fuel stacks, power control units, power conditioners, air compressors, humidifiers, motors, on-board chargers, battery management systems, and others. EVs are classified into four types based on propulsion, outlined below.
Saudi Arabia is the second-largest producer and exporter of crude oil and holds the second-largest proven oil reserves in the world, with around 267 billion barrels. The country's oil sector is a significant part of its economy, accounting for 75% of government revenue and approximately 90% of exports. However, due to the volatility of oil prices and the potential for economic instability, Saudi Arabia is increasingly focusing on non-oil activities to reduce its dependency on the oil sector. Non-oil commodities tend to have more stable prices, providing protection against these fluctuations and strengthening the country's social, economic, and financial sectors.