Kraft Paper Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
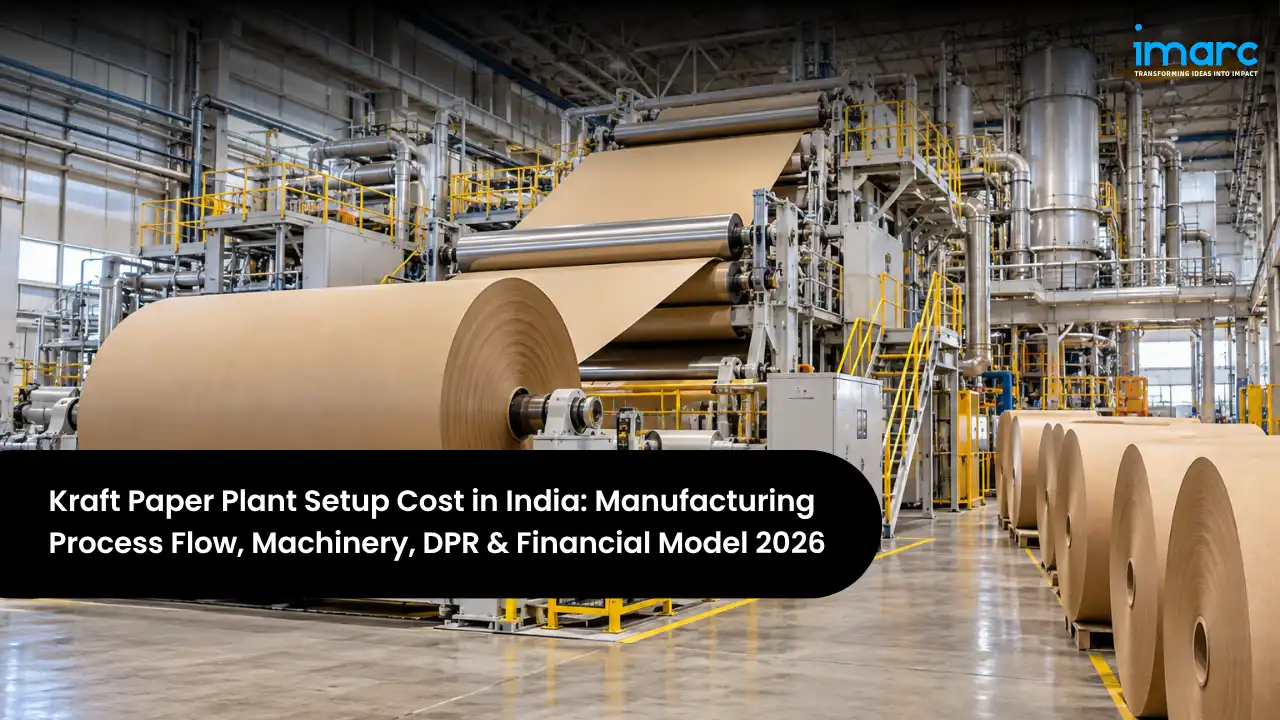
Setting up a Kraft Paper Manufacturing Plant in India is a high-demand, sustainability-driven venture, powered by the country's booming e-commerce, packaging, and corrugated-box industries. Kraft paper is the base material for corrugated boxes and packaging, and demand is rising as businesses shift from plastic to recyclable paper-based packaging. With abundant wood pulp feedstock, strong and growing demand, and proven technology, a Kraft Paper Manufacturing Plant is one of the more dependable opportunities in the paper and packaging economy.
The Kraft Paper Manufacturing Plant Cost depends on capacity, paper grades, and level of automation, with total project investment typically ranging from INR 20 crore to INR 150 crore. Wood pulp, power, and steam are the largest operating inputs, so feedstock and energy management are the most important financial decisions in the project, and together they shape the overall Kraft Paper Investment Cost. At healthy capacity utilization, a well-run plant in India delivers a net profit margin of 8 to 15% and an IRR of 15 to 24%, with payback typically achieved within 4 to 6 years.
This guide is written for investors and entrepreneurs asking how to start a Kraft Paper manufacturing plant in India. It covers what the business involves, why demand is rising, the process flow, the machinery and raw materials required, location and infrastructure planning, a detailed cost and financial breakdown, the licenses you must secure, and how a project report and DPR turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| India Paper & Packaging Market | Large, multi-billion dollar (indicative) |
| Primary Products | Kraft paper for corrugated packaging |
| Projected Market CAGR (2026–2034) | 8–12% (indicative) |
| Typical Plant Capacity | 50–300+ TPD paper output |
| Indicative Total Investment | INR 20–150 Crore |
| Typical Payback Period | 4–6 Years |
The snapshot captures why a Kraft Paper Manufacturing Plant in India attracts strong investor interest: an essential packaging material, broad and growing demand, and abundant wood pulp feedstock. The wide investment range reflects a genuine choice of capacity and grade, from a mid-sized paper unit to a large, integrated plant serving high-volume packaging customers. Because packaging is a repeat-purchase, essential input rather than a discretionary product, the demand base tends to hold up even when the wider economy slows, which is part of why lenders view the sector favourably. The rest of this guide unpacks that decision in detail.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Plant Capacity (Typical) | 50 – 300+ TPD |
| Total Project Investment | INR 20 – 150 Crore |
| Payback Period | 4 – 6 Years |
| Net Profit Margin | 8 – 15% |
| IRR | 15 – 24% |
| Best Locations | Gujarat, Maharashtra, Punjab, UP, Tamil Nadu |
| Mandatory Approvals | CPCB/SPCB, Factory Licence, Fire NOC, GST |
| Primary Revenue | Kraft paper for corrugated boxes |
These indicative parameters give a realistic frame for early feasibility work. The returns are steady, but they depend on securing wood pulp feedstock, managing power and water costs, and building corrugated-box and packaging customers. A well-prepared Kraft Paper Feasibility Report tightens each of these numbers to your specific location, capacity, and paper grades.
Table of Contents
- What is Kraft Paper Manufacturing?
- Why is Kraft Paper Manufacturing Growing in India?
- Kraft Paper Manufacturing Process
- Raw Materials and India Sourcing
- Location, Land & Infrastructure
- Machinery and Equipment Required
- Kraft Paper Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Kraft Paper Manufacturing Plant in India
- Recent Developments in the India Kraft Paper Manufacturing Industry
- How a Kraft Paper Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Kraft Paper Manufacturing?
Kraft paper manufacturing is the production of strong, brown packaging paper by pulping fibre, forming it into a continuous sheet, and drying and reeling it into rolls. The major source for kraft paper manufacturing is wood pulp produced via the sulfate (kraft) pulping process. The output is used primarily to make corrugated boxes and other packaging, where kraft paper is valued for its strength, recyclability, and low cost.
From a business perspective, what makes this sector attractive in India is the combination of surging packaging demand and abundant, low-cost wood pulp feedstock. Every corrugated-box maker, e-commerce packer, and FMCG brand is a potential customer, and a large wood pulp supplier network supplies fibre. A manufacturer that runs efficiently and supplies consistent quality is positioned to serve a large, essential, and fast-growing market driven by the shift to sustainable packaging.
- Corrugated Box Paper: Kraft paper for the corrugated boxes that dominate industrial and e-commerce packaging, the largest demand segment.
- High-BF Kraft: Higher burst-factor paper for heavy-duty and export packaging that commands better prices.
- Liner & Fluting Grades: Liner and fluting papers used in the layers of corrugated board.
- Specialty Kraft: Coloured, laminated, or specialty kraft for niche packaging applications.
The Main Grades in Kraft Paper Manufacturing
Understanding which grades your plant will produce is the foundational decision, because it drives fibre choice, machinery, and value:
| Grade | Typical GSM / BF | Key Property | Primary Demand |
|---|---|---|---|
| Standard Kraft | 100–180 GSM | General strength | Common corrugated boxes |
| High-BF Kraft | High burst factor | Heavy-duty strength | Export and heavy packaging |
| Liner Grade | Surface layer | Smooth, printable | Box outer liners |
| Fluting Grade | Middle layer | Rigidity | Corrugated fluting |
This choice shapes the entire plant, because standard low-GSM kraft is a high-volume commodity while high-burst-factor and specialty grades command better margins but need better fibre and process control. Many Indian entrants begin with standard corrugating grades, the largest and most accessible segment, and move toward higher-BF and specialty paper as they build capability and customers. The grade decision drives everything from machinery to the level of investment required.
Why is Kraft Paper Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
India's kraft paper sector is being propelled by several structural factors that combine booming packaging demand with a sustainability shift. Few products ride as many favourable trends at once:
- E-commerce and packaging boom: Rapid growth in e-commerce and organized retail is driving enormous demand for corrugated boxes and the kraft paper that makes them.
- Shift from plastic to paper: Regulations and consumer preference are pushing packaging from plastic to recyclable paper, expanding kraft demand.
- FMCG and industrial growth: Rising manufacturing and consumer-goods output increases demand for protective packaging across sectors.
- Abundant fibre supply: A large and growing wood pulp supply base provides reliable, low-cost fibre for kraft paper production.
- Circular economy support: Policy and market emphasis on recycling and sustainable packaging favour sustainable paper manufacturing.
India-Specific Market Opportunity
| Segment | India Market Context | Kraft Paper Role |
|---|---|---|
| Corrugated Packaging | Dominant box-making industry | Core raw material |
| E-commerce | Fast-growing online retail | Shipping-box demand |
| FMCG & Industrial | Large goods output | Protective packaging |
| Exports | Packaging for exported goods | High-BF kraft demand |
| Sustainable Packaging | Plastic-to-paper shift | Recyclable material |
The strongest opportunity lies in supplying corrugated-box makers and packaging converters with consistent, competitively priced kraft paper, ideally near both wood pulp supply and box-making clusters. A manufacturer that runs efficiently and maintains quality can lock in steady, high-volume orders from converters. Moving into higher-burst-factor and specialty grades, where margins are better and competition thinner, further strengthens a plant's position in a large, growing market.
Kraft Paper Manufacturing Process
Understanding how paper is actually made helps you plan equipment, feedstock handling, and the main cost drivers. Paper production is a continuous operation that turns fibre into a formed, pressed, and dried sheet, with quality control throughout, and it is both water- and energy-intensive. The typical flow moves wood pulp through pulping and the paper machine to a reeled, cut, and tested product:
The Kraft Paper Manufacturing Process
In this flow, wood pulp is pulped and cleaned into a fibre slurry, refined for strength, formed into a sheet on the paper machine, pressed and dried, then calendered, reeled, and cut for dispatch. Consistent pulp quality and efficient drying are essential to paper that meets strength specifications at a competitive cost.
| Unit Operation | Key Activity |
|---|---|
| Wood Pulp Intake | Wood pulp received and stored |
| Pulping | Wood pulp pulped into a fibre slurry |
| Cleaning & Screening | Contaminants removed from the pulp |
| Refining | Fibre refined for strength and bonding |
| Sheet Formation | Pulp formed into a sheet on the wire |
| Pressing | Water pressed out of the wet sheet |
| Drying | Sheet dried over steam-heated cylinders |
| Calendering | Sheet smoothed and finished |
| Reeling & Cutting | Paper reeled and cut to size |
| Testing & Dispatch | Strength tested, then dispatched to buyers |
width:100%"> Unit Operation Key Activity Wood Pulp Intake Wood pulp received and stored Pulping Wood pulp pulped into a fibre slurry Cleaning & Screening Contaminants removed from the pulp Refining Fibre refined for strength and bonding Sheet Formation Pulp formed into a sheet on the wire Pressing Water pressed out of the wet sheet Drying Sheet dried over steam-heated cylinders Calendering Sheet smoothed and finished Reeling & Cutting Paper reeled and cut to size Testing & Dispatch Strength tested, then dispatched to buyers
Two points determine profitability across this flow. First, fibre yield and quality drive both product strength and material cost, so pulping and refining control directly govern outcomes. Second, the process consumes large amounts of power, steam, and water, so energy and water efficiency are decisive margin levers. Rigorous strength testing, for burst factor and grammage, is what allows a manufacturer to certify paper to customer specifications and win steady converter orders. Because corrugated-box makers run their own machines to tight tolerances, consistent reel quality and reliable delivery matter as much to them as headline price.
Raw Materials and India Sourcing
The main input is fibre, chiefly wood pulp, and securing it at competitive prices and consistent quality is the single biggest determinant of a plant's viability. Because wood pulp dominates cost and its price varies with pulp-market and demand cycles, procurement strategy and a reliable supply network materially affect margin, alongside the chemicals and utilities the process needs.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Wood pulp (virgin/kraft) | Primary fibre source | Wood pulp from domestic mills and imports | 45–60% |
| Process Chemicals | Strength and sizing agents | Domestic chemical suppliers | 5–10% |
| Water | Pulping and forming | Treated water with recycling | 2–5% |
| Packaging & Consumables | Reel packing and wires | Domestic suppliers | 2–5% |
Because wood pulp is such a large and variable share of cost, feedstock strategy is the biggest lever on profitability. India has a large domestic wood pulp supply base supplemented by imports, so supply is available, but prices can swing with demand, making a reliable supplier network and sensible inventory important. Energy is the other major cost, so many plants invest in captive power and steam recovery to protect margins, since power and steam are essential and continuous. Recycling process water and recovering heat from the drying section are common ways to lower both utility bills and the plant's environmental load at the same time.
Location, Land & Infrastructure
Choosing the best location for Kraft Paper manufacturing plant setup significantly affects feedstock and water access, energy costs, and proximity to box-making customers. Being near wood pulp supply, corrugated-box clusters, and reliable water and power shapes site selection, alongside adequate land and effluent-treatment capacity for a water-intensive process.
Best States for Kraft Paper Manufacturing Plant Setup in India
| State | Why It Works | Key Advantage |
|---|---|---|
| Gujarat | Industrial base and ports | Feedstock, imports, and demand |
| Maharashtra | Large packaging demand | Box makers and MIDC zones |
| Punjab | Established paper cluster | Ecosystem and feedstock |
| Uttar Pradesh | Big market and supply | Wood pulp and demand |
| Tamil Nadu | Industrial and export base | Packaging and logistics |
| Telangana & AP | Growing industry base | Land, water, and demand |
The strongest locations combine reliable wood pulp supply and water with proximity to corrugated-box clusters and competitively priced power. Gujarat and Punjab offer strong paper ecosystems and feedstock, while Maharashtra, UP, and Tamil Nadu add large packaging demand and logistics. Because the process is water- and energy-intensive, water availability, effluent capacity, and power cost should weigh heavily in the final choice, alongside land for pulping, the paper machine, and storage.
Infrastructure Requirements (Mid-Sized Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 5,000 – 20,000 sq. meters | Space for machine and storage |
| Paper Machine Hall | Machine-line layout | Length for the paper machine |
| Wood Pulp Storage | Covered storage | Dry storage for bulky feedstock |
| Power & Steam | Captive power and boiler | For drying and operations |
| Water & ETP | Treated water and effluent plant | Mandatory; water-intensive process |
| Testing Laboratory | Paper testing facility | For strength and grammage |
| Finished-Goods Warehouse | Reel storage | For finished paper reels |
Specification India-Specific Note Total Land Area 5,000 – 20,000 sq. meters Space for machine and storage Paper Machine Hall Machine-line layout Length for the paper machine Wood Pulp Storage Covered storage Dry storage for bulky feedstock Power & Steam Captive power and boiler For drying and operations Water & ETP Treated water and effluent plant Mandatory; water-intensive process Testing Laboratory Paper testing facility For strength and grammage Finished-Goods Warehouse Reel storage For finished paper reels
Infrastructure for a kraft paper plant centres on the paper machine, power and steam supply, water and effluent systems, and a testing lab, because output, cost, and compliance depend on all of them. Water treatment and effluent capacity are especially important given how water-intensive papermaking is and how closely regulators scrutinize it. Building adequate power, water, and effluent capacity from the start supports both scaling and the environmental standards the industry must meet. A well-planned machine hall with room to add a second line or wider machine later also makes future expansion far cheaper than retrofitting a cramped site.
Machinery and Equipment Required
The equipment set spans pulping, the paper machine, and finishing, and the line-up scales with capacity and grade range. Because paper quality and efficiency depend on continuous, well-controlled processing, machinery must be robust and well matched to the product. The core machinery, from wood pulp pulping through finished-reel testing, is summarized below.
| Equipment | Function | Key Specification |
|---|---|---|
| Pulper | Pulp wood pulp into slurry | Sized to capacity |
| Cleaning & Screening | Remove contaminants | Multi-stage cleaning |
| Refiner | Develop fibre strength | Controlled refining |
| Paper Machine (Fourdrinier) | Form the paper sheet | Wire, press, and dryer sections |
| Drying Cylinders | Dry the sheet | Steam-heated drying |
| Calender | Smooth and finish paper | Surface finishing |
| Pope Reel | Reel the finished paper | Continuous reeling |
| Rewinder / Cutter | Cut reels to size | Slitting and rewinding |
| Boiler & Power Plant | Supply steam and power | For drying and operations |
| ETP & Lab Equipment | Treat effluent and test paper | Compliance and quality |
Equipment selection should follow your capacity and grade range rather than the other way around. A mid-sized kraft paper plant needs pulping, a paper machine, and finishing, while higher grades and output need better refining, wider machines, and more drying capacity. Power, steam, and effluent systems are central and easy to under-budget, because papermaking's heavy energy and water use mean these utilities determine both cost and the ability to operate within environmental norms.
Kraft Paper Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below give you a breakdown of both the upfront capital investment and the ongoing operating costs, based on industry analysis of a mid-sized facility in India. The actual Kraft Paper Manufacturing Plant Cost for your specific project will depend on your chosen location, capacity, grade range, and level of automation.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Paper Machine & Pulping | 40–50% | Paper machine, pulper, and refining |
| Power & Steam Plant | 12–18% | Captive power and boiler |
| Building & Civil Works | 12–18% | Machine hall and storage |
| Water & Effluent Systems | 6–10% | Water treatment and ETP |
| Pre-operative & Misc. Costs | 4–7% | Engineering fees, DPR, and approvals |
| Contingency Reserve | 5–8% | Standard buffer for cost variability |
| Working Capital | 10–15% | Wood pulp stock and receivables |
The CapEx profile is dominated by the paper machine and pulping line, with the power and steam plant a significant additional investment because papermaking needs continuous energy. Working capital matters because wood pulp must be bought and stocked ahead of production. Under-provisioning power, effluent, or working capital is a common and costly mistake, so all are modelled carefully in the Kraft Paper Business Plan and Financial Model.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Wood Pulp Feedstock | 45–60% | Largest cost; price varies with demand |
| Power & Steam | 15–25% | Drying is highly energy-intensive |
| Labour & Manpower | 6–10% | Machine and plant operators |
| Chemicals & Consumables | 5–10% | Sizing and strength agents |
| Maintenance & Repairs | 3–6% | Continuous-process upkeep |
| Effluent & Compliance | 3–6% | Water treatment and norms |
With wood pulp and energy together dominating operating cost, this is fundamentally a feedstock-and-energy business, and margin depends on cheap fibre, efficient drying, and high yield. Both feedstock and energy prices move over time, so a financial model should track them closely and stress-test margins against wood pulp and power-cost swings, which are the biggest variables, while accounting for the steady demand that packaging provides.
Financial Analysis and Profitability
Based on analysis of a mid-sized kraft paper facility in India, the financial profile is steady, supported by essential, growing packaging demand and abundant wood pulp feedstock. Because feedstock and energy costs drive economics, the ROI of Kraft Paper manufacturing business in India improves markedly with reliable low-cost fibre, efficient power and steam, high utilization, and a move toward higher-value grades.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 15–25% | Driven by fibre and energy costs |
| Net Profit Margin | 8–15% | After depreciation and Indian corporate taxes |
| Payback Period | 4–6 Years | Faster with efficient energy use |
| IRR (Internal Rate of Return) | 15–24% | Higher for high-BF and specialty grades |
| Capacity Utilization (stable ops) | 75–90% | Continuous process favours high run rates |
| Break-even Capacity Utilization | 55–70% | Strong packaging demand supports throughput |
Feedstock cost, energy efficiency, and utilization are the factors that most determine outcomes, because a continuous paper machine must run at high, steady rates to spread its fixed costs and heavy energy base. An operator with reliable fibre supply, efficient captive power, and steady converter demand can run comfortably above break-even, while one exposed to feedstock or power swings will see margins fluctuate. This is why feedstock and energy management are as central to the financial model as the machinery itself.
There are several ways to strengthen returns in the Indian context: securing low-cost wood pulp through a strong supplier network, investing in captive power and steam recovery to cut energy cost, moving into higher-burst-factor and specialty grades, keeping the machine at high utilization, and controlling water and effluent efficiently. Reliable converter relationships further stabilize demand and pricing. Supplying consistent grades on time also helps a plant build long-term contracts with large box makers, which smooths out the volume swings that hurt smaller, spot-market-dependent mills.
Key Risks and Mitigation
The principal risks are wood pulp price volatility, high energy costs, and environmental compliance. Feedstock risk is mitigated by a diversified supplier network and inventory planning; energy risk is mitigated by captive power, steam recovery, and efficient drying; and compliance risk is mitigated by robust effluent treatment and water recycling. A manufacturer that treats feedstock, energy, and compliance as core priorities is far better placed to sustain the returns the model promises.
Licenses and Approvals for Kraft Paper Manufacturing Plant in India
The approvals for this business are important, because papermaking is water- and effluent-intensive and closely regulated for environmental compliance. Manufacturers planning to establish a Kraft Paper Manufacturing Plant generally need to obtain the following before commencing operations, and pollution-control approvals are especially central:
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board (CTE and CTO), central for a water-intensive process.
- Business & Tax Registration: Company or firm incorporation, GST registration, and Udyam (MSME) registration.
- Factory Licence: Registration of the factory and obtaining the applicable licence from the competent State authority in accordance with the Occupational Safety, Health and Working Conditions Code, 2020 (OSHWC Code) and applicable State rules.
- Environmental & Water Approvals: Water usage and effluent-discharge approvals for the plant.
- Boiler & Power Approvals: Approvals for boilers and captive power where applicable.
- Fire Safety NOC: Fire safety and workplace safety compliance for the facility.
- Labour Registrations: Employee welfare and workforce-related registrations such as EPF and ESI.
For a kraft paper plant, pollution-control consents, water and effluent approvals, and boiler approvals are the critical items and should be pursued early, in parallel with construction, because a water-intensive plant cannot operate without them. Engaging a consultant familiar with environmental and boiler regulations is usually worth the cost, since a delayed consent can idle a completed plant. Sequencing approvals well, alongside feedstock and customer development, can shave months off the project timeline.
Note: The exact approvals, registrations, licences, and compliance requirements may vary depending on factors such as plant location, capacity, water use, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Kraft Paper Manufacturing Industry
A few structural trends give useful context for investors considering entry into this industry:
- Packaging and e-commerce growth: Sustained growth in e-commerce and organized retail continues to drive strong demand for corrugated packaging and kraft paper.
- Plastic-to-paper shift: Regulations and consumer preference favouring recyclable packaging are steadily expanding demand for paper-based materials.
- Energy and efficiency focus: Rising energy costs and environmental norms are pushing manufacturers toward captive power, water recycling, and greater efficiency.
The common thread is a market growing with packaging demand and the shift to sustainable materials, with efficiency and compliance increasingly important. For a new entrant, the implication is clear: the window to establish efficient, compliant capacity and build converter relationships is open, and those who build feedstock security, energy efficiency, and quality into their model from the start will be best placed as demand grows through the decade.
How a Kraft Paper Manufacturing Project Report and DPR Helps Investors
A comprehensive Kraft Paper Project Report, prepared as a Detailed Project Report (DPR), provides a structured roadmap for establishing the facility by evaluating every aspect of the venture, from market demand and grade mix to machinery selection, plant layout, and economics. It helps investors determine the optimal capacity and grade range, estimate capital expenditure (CapEx) and operating expenditure (OpEx), assess profitability, and identify potential risks before implementation.
The report also brings together a Kraft Paper Business Plan with revenue forecasts, production costs, cash flow analysis, break-even assessment, return on investment (ROI), and payback period calculations, supported by a detailed Kraft Paper Financial Model. These insights enable investors, lenders, and stakeholders to make informed decisions and evaluate the long-term viability of the project. Many investors engage a Kraft Paper Business Plan Consultant in India or a Kraft Paper Manufacturing Consultant in India to prepare and validate these documents.
For a kraft paper project specifically, a strong DPR also clarifies the feedstock strategy, the energy and grade choices, and the environmental-approval pathway, which are the factors most likely to determine success. By modelling utilization against realistic demand and testing margins against feedstock and energy-cost swings, the report turns a competitive but essential-product opportunity into an executable plan that lenders and partners can trust.
Frequently Asked Questions
How to start a Kraft Paper manufacturing plant in India?
Begin by choosing your capacity and grade range, then prepare a feasibility report and DPR, secure land near feedstock and water, arrange the paper machine and pulping equipment, tie up wood pulp supply and converter customers, and obtain pollution-control and factory approvals. A detailed project report maps each step for your target setup.
What is the Kraft Paper Manufacturing Plant Cost in India?
It typically ranges from INR 20 crore to INR 150 crore depending on capacity, grade range, and automation, and the wider Kraft Paper Investment Cost is dominated by the paper machine and power plant. Machinery and utilities are the largest components.
What is the Kraft Paper Manufacturing Process?
The process runs from wood pulp intake and pulping, through cleaning, refining, sheet formation, pressing, and drying, to calendering, reeling, cutting, strength testing, and dispatch, with quality checks throughout and heavy use of power, steam, and water.
What machinery is required for a kraft paper plant?
Key equipment includes a pulper, cleaning and screening systems, a refiner, a paper machine with wire, press, and dryer sections, a calender, a pope reel, a rewinder or cutter, a boiler and power plant, and effluent-treatment and testing equipment.
What is the best location for Kraft Paper manufacturing plant setup?
The ideal site combines reliable wood pulp supply and water with proximity to corrugated-box clusters and competitively priced power. Gujarat, Maharashtra, Punjab, Uttar Pradesh, and Tamil Nadu are leading choices.
What is the ROI of Kraft Paper manufacturing business in India?
It is steady, with a typical 8 to 15% net profit margin and a 15 to 24% IRR, and a 4 to 6 year payback at healthy utilization. Returns improve with low-cost feedstock, efficient captive power, higher-value grades, and high utilization, though margins track wood pulp and energy prices.
How do I get a project report or feasibility report for a kraft paper plant?
A Kraft Paper Project Report and Kraft Paper Feasibility Report cover the full plant setup and financials. Many investors engage a Kraft Paper Plant Project Report Consultant in India or a Kraft Paper Manufacturing Feasibility Study Consultant to prepare and validate them.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Setting up a Garment Manufacturing Plant in India is a high-demand, employment-generating venture, powered by the country's vast textile base, skilled workforce, and growing role as a global apparel sourcing hub.
The Luxury Fashion Market reached USD 261.0 Billion in 2025 and is projected to reach USD 341.0 Billion by 2034, growing at a CAGR of 3.02% (2026–2034).
Setting up a Container Manufacturing Plant in India is a capital-efficient, high-demand venture powered by the country's fast-growing food, pharmaceutical, FMCG, and industrial packaging sectors.
Bath soap is a body wash product developed primarily to provide personal care. It is made by the alkali saponification, a method that generates soap salts and glycerin in the soap via a reaction between fats or oils and an alkali, such as sodium hydroxide. Bath soaps are made by separating out dirt, sweat, excess oil and microorganisms while helping to remove dirt, sweat, excess oil and water soap from the skin to avoid dirt, extra oil and bacteria and viruses while preserving the balance of both cleansing the skin and compatibility between the application.
Waste tyre recycling can be defined as the organized collection, treatment, and recovery of end-of-life tyres (ELTs) to produce new materials, energy sources, or secondary raw materials. Tyres are made up of vulcanized rubber, steel reinforcement, textiles, and chemical compounds, making them non-biodegradable materials that cannot be easily decomposed.
Wallpaper is a decorative and practical wall covering material used to cover interior surfaces for aesthetic purposes, protection, and ambiance. It is usually made from paper, vinyl, non-woven fibers, textile backing, or a combination of materials, printed or embossed with designs, textures, or solid colors.
The Australian footwear industry is experiencing a remarkable transformation as it navigates a confluence of shifting consumer preferences, technological advancements, and sustainability imperatives.
Tennis ball production is the process of making standardized balls for the game of tennis. The process involves making balls with specific performance and bounce features. A tennis ball is made up of a hollow rubber core that is filled with pressurized air. The core is then covered with a woven felt material.
Soap is a type of cleaning agent made by the chemical reaction of fats or oils and an alkali in a process known as saponification. The chemical reaction transforms triglycerides into soap, also known as fatty acid salts, giving these substances the properties of a surfactant, allowing the substance to be used for the removal of dirt, oil, and bacteria from surfaces.
The size of the global hair oil market has undergone significant transformation with increasing consciousness among consumers to adopt hair care as part of their personal wellness, beyond the realm of mere beauty. Hair oils, being long considered one of the traditional grooming essentials, have transformed into complex formulations to suit various hair types and scalp conditions. Over the past years, lifestyle change, growing awareness related to scalp health, and the rising demand for natural beauty have significantly impacted the consumption pattern in the hair oil segment.
The global online grocery market research landscape has undergone unprecedented changes in recent years, with an upward trend marking the way consumers engage with food retail. There has been a significant expansion in the size of the online grocery market, fuelled by changing consumer preferences, technological advances, and increased convenience associated with digital shopping. Households are showing a growing reliance on online platforms for regular essentials more than ever, making the sector a cornerstone of modern retail.
The UAE’s pet food sector has emerged as one of the most dynamic and lifestyle-influenced consumer categories. While historically smaller and more niche compared to mainstream food and beverage markets, the industry has grown in relevance due to changing demographics, international influences, and shifting consumer priorities. Residents across major cities are embracing pets as companions for emotional well-being and as part of a balanced lifestyle.
The Saudi Arabia road freight transport market represents one of the key building blocks of the economic infrastructure in the Kingdom, providing for cargo movement across various domestic supply chains. It also involves road freight operations, which allow for the distribution of goods-from manufactured goods, consumer goods, and industrial supplies to agricultural produce-across its large and wide geography.
The Saudi Arabia luxury market represents one of the most dynamic and rapidly evolving segments within the Middle Eastern premium retail landscape. As the Kingdom undergoes comprehensive economic diversification and social transformation, luxury consumption patterns are experiencing unprecedented shifts that reflect changing demographics, evolving consumer preferences, and ambitious national development goals.
The Philippines retail sector has become a pluralistic and dynamic environment where old-fashioned stores coexist with high-tech contemporary formats enabled by digital strength. The Philippines retail sector market size reached USD 648.2 Billion in 2025. The market is projected to reach USD 1,223.1 Billion by 2034, exhibiting a growth rate (CAGR) of 7.31% during 2026-2034.
Polyester fabric is a type of synthetic fabric made from polyester fibers. The main source of polyester fibers is petrochemical polymers like polyethylene terephthalate. Polyester fabric is made from processing chips of polymers to produce continuous filaments and staple fibers. The processing of polymers involves heating and melting chips of polymers made from petrochemical materials to produce continuous filaments and staple fibers.
India's gaming industry is rapidly evolving into one of the largest and most dynamic markets in the world. Driven by the increasing adoption of smartphones, affordable internet, and a tech-savvy youth population, gaming is becoming a mainstream form of entertainment.
The beauty landscape in India is undergoing a major transformation propelled by creativity, research, and technology. The India cosmetics market size was valued at USD 15.46 Billion in 2025. Looking forward, the market is expected to reach USD 25.39 Billion by 2034, exhibiting a CAGR of 5.7% from 2026-2034.
The drivers for changing India's textile sector include sustainability, modernization of production, and the introduction of advanced chemical solutions. The India textile market size was valued at USD 152.40 Billion in 2025. The market is projected to reach USD 213.75 Billion by 2034, exhibiting a CAGR of 3.83% from 2026-2034. It places the India textile chemicals market at an important position in this evolution, enabling everything from fiber processing to finishing.
India's consumer landscape is experiencing a profound transformation, driven by rapid digital adoption, evolving consumer preferences, and robust infrastructure development. The shift from traditional brick-and-mortar shopping to digital platforms represents more than a mere change in purchasing channels—it signifies a fundamental restructuring of how businesses engage with consumers and how millions of Indians access goods and services.
The Saudi Arabia deodorants market size continues to evolve as consumers embrace modern grooming habits, premium personal care products, and innovative hygiene solutions. With rising awareness of body care, fragrance layering, and daily freshness, deodorants have become an essential part of both men’s and women’s personal grooming rituals.
Pet foods consist of commercially processed foods that contain nutritional requirements tailored according to their consumption by domesticated pets like dogs, cats, birds, fish, and small animals. The foods contain planned nutritional compositions, such as ingredients like protein, carbohydrate, fat, vitamins, and minerals.
Perfume is a scented liquid composition that contains a mixture of fragrance chemicals, essential oils, aroma chemicals, fixatives, and solvents that are formulated for a pleasing and distinct fragrance emission upon application on human skin or on objects.
Technological advancements and shifting consumer expectations have caused the worldwide washing machine industry to drastically change. Washing machines are becoming indispensable parts of contemporary homes, smoothly integrating into smart home ecosystems from conventional semi-automatic models to fully linked, smart appliances.
Paper plates are disposable food containers, also referred to as tableware, and are made mostly from paperboard, pulp, and materials that are derived from fibers. These plates are designed to be convenient, hygienic, and easy to handle while being moisture and grease-proof, making them ideal for packing different food varieties, ranging from dry foods to moist and greasy food items.
The GCC cigarette lighter market is undergoing a steady phase of expansion due to evolving consumer habits, sustained product demand, and widening distribution channels across the region. In 2024, the GCC cigarette lighter market was valued at USD 197 Million. A key factor shaping industry performance is the rise in convenience-led purchases, driven by widespread retail penetration, duty-free availability, and the continued popularity of smoking-related accessories.
Paint brushes are hand-operated applicator tools, designed and manufactured with great precision, utilizing the capabilities of these tools to apply, spread, and manage liquid paint, along with other forms of paint such as varnishes, stains, lacquers, and surface finishes, onto a desired surface. Paint brushes are commonly manufactured using a series of components, including a handle, a ferrule, and natural or man-made hairs, or a combination of these two. They are also manufactured and designed with different shapes and sizes, according to the viscosity and texture of the paint.
Pan masala is a ready-to-use chewing mixture that is traditionally used as a mouth freshener as well as a digestive aid and is of South Asian origin. It is prepared by mixing different components such as areca nut, catechu, slaked lime, spices, flavoring agents, sweet agents, and aroma agents in specific proportions. It is usually packed ready for use and is different from the betel quid variant that is prepared by using fresh betel leaves. Contemporary formulations of pan masala aim to achieve consistency, shelf life, and standardized flavor so that it can be mass-produced and marketed.
Paper bags can be defined as the final product made from paper-based material such as kraft paper, recycled paper, or specialty paper, used for packing or storing products. Paper bags come in different shapes and sizes with varying strength, ranging from flat-bottom paper bags, gusseted paper bags, and handled paper bags. Paper bags can be biodegradable, can be recycled, and can be made from renewable resources.
The Brazil cosmetics products market represents one of the most vibrant and diverse beauty sectors in Latin America, reflecting a deep-seated cultural emphasis on personal appearance, wellness, and self-care. The Brazilian consumer has long been known for a keen taste for grooming, fashion, and aesthetics, which logically applies to the cosmetics industry. Driven by an expanding middle-class population, an increase in urbanization, and increasing awareness about wellness-oriented lifestyles, the market continues to evolve.
The commercial landscape across the globe is undergoing a seismic shift, driven by technology, changing consumer expectations, and macroeconomic volatility. This transformation is particularly pronounced in high-density, globally connected urban centres like Singapore. Historically a powerhouse of trade and luxury commerce, the nation is now navigating an intricate matrix of digital disruption and soaring operational pressures.
The India confectionery industry has emerged as one of the most dynamic segments within the country's food and beverage sector. Driven by changing consumer preferences, rising disposable incomes, and evolving lifestyles, the market continues to witness remarkable transformation across urban and rural landscapes.
As disposable incomes rise, households are diversifying across investment-grade gold, diamond-studded jewellery, and designer ornaments. Gold, in particular, holds unmatched cultural and economic importance, sustaining demand even through economic fluctuations. Recent indicators show how this cultural attachment continues to translate into measurable investment momentum. Gold demand stood at 135 tonnes in Q2 2025, with a full-year forecast between 600 and 700 tonnes. By mid-2025, India’s total gold holdings reached 66.7 tonnes, with two tonnes added in June and nine tonnes in the first half of the year.
Mobile accessories encompass a wide range of auxiliary products that are intended to complement, protect, enhance, or extend the functional capabilities of smartphones and other portable communication devices. Examples of these accessories include protective cases, screen guards, chargers, power banks, earphones, wireless earbuds, smart wearables, mounts, portable speakers, and connectivity adapters. They enable better usability, device safety, personalization, convenience, and integration with digital ecosystems. Mobile accessories are made from a variety of materials and technologies to meet various performance, durability, and design requirements for different groups of users.
Japan boasts a long and rich culture of traditional board games such as Go and Shogi, which have long been a fundamental component of its culture. The current board game market in Japan, though, is a vibrant mix of these indigenous games and an incredibly diverse range of modern games based on both Western and domestic design schools.
The tobacco industry has long been a cornerstone in world trade and consumer culture, shaping the courses of economies, employment landscapes, and industrial practices for centuries. Even in today's world, with growing awareness regarding health and sustainability, tobacco remains an imposing force in global commerce.
The Australia sportswear industry is experiencing unprecedented momentum, transforming into a multi-billion-dollar powerhouse where fashion, fitness, and lifestyle converge. As health consciousness sweeps the continent and athleisure becomes a wardrobe staple, the Australian market leads a global revolution in performance apparel.
Japan's luxury apparel industry has traditionally been characterized by its profound respect for craftsmanship, quality, and cultural refinement. Japanese consumers have a reverence for art and nuance, preferring items that reflect precision and enduring design over short-lived trends. Over the past decade, Japanese luxury fashion has transcended conventional retailing experiences and assumed a contemporary identity that coalesces international influences with domestic sentiments.
A mattress is a cushioned structure intended to support the human body, either while sleeping, resting, or for therapeutic purposes. It is typically made up of comfort layers, including foam, latex, fiber, or gel, combined with a supportive core, like innerspring coils, high-density foam, or hybrid constructions. Mattresses are designed to evenly distribute body weight to relieve pressure points and ensure proper spinal alignment.
Liquid detergent is a formulated cleaning solution comprising surfactants, solvents, builders, enzymes, pH stabilizers, perfumes, and other additives, which are collectively used for removing dirt, stains, and oils from fabrics, dishes, and different surfaces. Unlike powdered detergents, liquid detergents dissolve immediately in water, allowing even distribution during washing and effective performance in both hot and cold water.
The Japan personal luxury goods industry stands as one of the world’s most crucial and dynamic markets, consistently ranking among the top three globally, alongside the United States and China. In 2024, Japan personal luxury goods market size reached USD 32,060.65 Million in 2024.
The luxury watch industry represents one of the most enduring segments of the global fashion and lifestyle market. Combining precision engineering with timeless craftsmanship, luxury watches continue to hold strong appeal among high-net-worth individuals, collectors, and aspirational consumers. The global luxury watch market size reached USD 29.12 Billion in 2024, reflecting steady growth driven by premiumization, rising consumer demand in emerging economies, and the enduring value of heritage timepieces.
The Vietnam athleisure market stands at a pivotal juncture, experiencing remarkable transformation driven by evolving lifestyles, rising health consciousness, and rapid urbanization. As Vietnamese people are increasingly prioritizing wellness and seeking versatile clothing that seamlessly transitions from gym workouts to casual social settings, the demand for activewear trends has surged dramatically. With lifestyle apparel Vietnam witnessing unprecedented growth and fitness clothing demand reaching new heights, both international brands and homegrown labels are competing vigorously to capture market share in this dynamic sector.
The Philippines conveyor belt market is picking up speed, powered by the country’s industrial growth and focus on automation. According to the IMARC Group, the market reached USD 31.23 Million in 2024, reflecting notable growth across manufacturing, mining, logistics, and food processing. As industries modernize, the need for efficient material handling systems is creating strong momentum for both domestic and imported conveyor solutions.
The US retail market is undergoing a profound transformation, fueled by the integration of artificial intelligence (AI) across multiple business operations. From personalized consumer engagement to predictive inventory management and dynamic pricing strategies, AI is redefining how retailers operate, compete, and deliver value. Increasing consumer expectations for seamless, personalized, and efficient shopping experiences are prompting businesses to embrace AI-driven solutions to optimize performance, reduce costs, and enhance decision-making.
The global beauty and personal care products market is undergoing a profound transformation, driven by technological innovation, evolving consumer expectations, and sustainability-focused practices. Increasing consumer awareness of health, wellness, and ethical sourcing is compelling companies to rethink traditional formulations and adopt advanced manufacturing techniques. Businesses are now integrating biotechnology, artificial intelligence, and data-driven insights into product development, distribution, and marketing strategies.
The Philippines board game market is on a winning streak, fueled by a growing passion for social play, learning, and creative pastimes. According to IMARC Group, the market reached USD 83.39 Million in 2024, reflecting how board gaming is becoming a favorite form of entertainment across generations. Family games, strategy and role-playing titles, and educational options for kids are gaining steady traction, alongside collectible and pop culture–inspired editions.
The Australian fantasy sports industry is entering a phase of heightened momentum, with market size for 2024 reaching approximately USD 810.6 Million, as detailed in a recent report. This market is forecast to grow to USD 2,180.2 Million by 2033, representing a compound annual growth rate (CAGR) of around 10.4 % from 2025 through 2033 .
Australia's textile recycling sector is experiencing a technological renaissance, with 40% of SMEs currently adopting artificial intelligence (AI), marking a 5% increase compared to the previous quarter (July-Sept 2024). The percentage of businesses unaware of how to utilize AI has decreased by 2% to 21%.
Containers are standardized, tough, watertight containers for efficient storage and transportation of goods by ship, rail, and truck without the need for handling the cargo itself. They are the lifeblood of global trade and logistics, allowing for effective intermodal transport. Constructed from high-strength steel, aluminum, or composite materials, they are designed to withstand rigorous marine and environmental elements. The most common types are dry storage containers for general cargo; however, there are also refrigerated (reefers) for perishables, tank containers for liquids and gases, open-top and flat-rack for oversized equipment, and high-cube for voluminous cargo. Standardization, mainly through ISO specifications, allows for seamless compatibility and efficiency throughout global logistics systems.
Carpet is a textile floor covering made of a pile, tufts of yarn or fiber, sewn to a backing for dimensional stability. Carpets are manufactured in various construction forms: tufted (universal across the world, yarn punched through a primary backing and treated with secondary backing), woven (Wilton and Axminster, highly valued for durability and pattern intricacy), needle-felt (bonded fibers for industrial applications), and knotted (hand-made rugs).
Aloe vera gel is a natural concentrate obtained from the parenchyma of the inner leaf of Aloe barbadensis miller, which is valued for its therapeutic, nutritional, and cosmetic uses. The gel mostly comprises water (more than 95%) and polysaccharides, vitamins, minerals, amino acids, enzymes, and antioxidants responsible for its soothing, moisturizing, and healing actions. Renowned for its anti-inflammatory, antimicrobial, and skin-rejuvenating properties, the aloe vera gel finds broad application in personal care cosmetics, pharmaceuticals, food supplements, and beverages.
Aloe vera is a perennial fleshy succulent plant of the species Aloe barbadensis miller, grown worldwide for its nutritional, medicinal, and cosmetic benefits. It has two primary constituents: the transparent inner gel consisting mainly of polysaccharides, vitamins, enzymes, and amino acids; and the yellowish latex, consisting of anthraquinones with powerful laxative properties. Aloe vera gel is highly prized for its emollient, moisturizing, and healing properties and is a common ingredient in skincare, personal care, and pharmaceutical products.
Air purifiers are appliances that enhance indoor air quality by eliminating pollutants like dust, allergens, smoke, volatile organic compounds (VOCs), and microbial particles. They work on various technologies such as HEPA (High-Efficiency Particulate Air) filters, activated carbon filters, UV-C light, ionizers, and photocatalytic oxidation. Their major components are usually fans or blowers, filter media, sensors, electronic controls, and metal or durable plastic housings. Some of the crucial characteristics of air purifiers include efficiency of filtration, airflow, noise levels, power consumption, and filter material durability.
Air coolers are evaporative coolers based on the principle of water evaporation, utilizing a fan or blower to blow cooled air, as opposed to air conditioners, which function based on refrigerant and compressor principles. Air coolers are designed to deliver low-cost and energy-efficient temperature management, mainly applicable to dry and hot climates. They generally consist of a pump, motor, cooling pads, water tank, blower/fan, and electronic control units. Main characteristics are low energy usage, environmental friendliness, portability, and low cost. Production of air coolers typically consists of combining sheet metal or plastic enclosures with motor-driven fans, water distribution networks, and cellulose or aspen cooling pads.
A4 paper, which is one of the most commonly used paper formats around the world, is 210 mm × 297 mm and forms the part of the ISO 216 system. It mainly consists of cellulose fibers obtained from wood pulp, recycled papers, or other fibrous raw materials like bagasse or bamboo. A4 paper contains crucial characteristics like smoothness, even thickness, high opacity, brightness, tensile strength, and durability, which enable it for printing, copying, and writing. The production process includes pulping raw fibers, bleaching for whiteness, refining for increasing fiber bonding, and sheet formation under regulated drying and calendaring.
The manufacturing sector is constantly changing with continuously rising demands for sustainability, innovation, and efficiency. The time comes when companies want to expand their business or venture into new markets.
India's manufacturing industry is experiencing a remarkable transformation and growth in 2025, aiming to establish the nation as a key player in global manufacturing. Supported by governmental initiatives such as the Make in India program and the Production Linked Incentive (PLI) schemes, the sector has drawn significant foreign direct investment (FDI) and encouraged innovation across multiple industries.
India's manufacturing industry is undergoing a turning point in 2025 based on strong government initiatives, a highly skilled and youthful population, and a worldwide trend towards diverse supply chains.
The global tobacco sector remains one of the most mature yet closely scrutinized industries in the world. With demand persisting across both developing and developed markets, cigarette production continues to be a high-volume, technically refined activity governed by extensive regulation and economic influence.
The global vegan cosmetics market is experiencing unprecedented growth, driven by a new wave of conscious consumers who demand beauty products that are not only effective, but also ethical, sustainable, and cruelty-free. This movement is more than just a passing trend; it's a fundamental shift in values that is reshaping the industry.
The global online grocery market has rapidly evolved from a convenience service to a mainstream retail segment, reshaping how consumers shop for everyday essentials. According to the IMARC group report, the market reached a value of USD 710.10 Billion in 2024 and is projected to witness consistent expansion.
The India textile market is picking up serious momentum, supported by smarter tech and changing user preferences. As more buyers look for eco-friendly, premium-quality products, manufacturers are stepping up with automation, digital tools, and flexible production systems.
The global toys market plays a crucial role as toys fundamentally support child development by fostering creativity, cognitive skills, and social interaction. In 2024, the global toys market was valued at USD 113.94 Billion.
The worldwide luxury watch market is poised for sustained growth, driven by rising affluence, aspirational lifestyle, and digital evolution. As consumers place greater importance on exclusivity and craftsmanship, demand for luxury watches is growing in developed as well as emerging markets.
Baby wipes are wet disposable wipes used to clean the tender skin of an infant, mostly when changing diapers. Composed of non-woven materials and embedded with delicate cleansing products, commonly made from water, mild surfactants, moisturizers such as aloe vera, and preservatives baby wipes are made to be delicate, hypoallergenic, and safe for daily use.
A tennis ball is a type of high-performance sporting ball used in both competitive and recreational tennis. On various court surfaces, its rubber core and felt covering provide the best bounce, speed, and durability. Both pressurised and non-pressurized tennis balls are available to accommodate different playing situations and ability levels. Under international regulations, they are crucial for competitions and training, and business expansion is being driven by sustainability and material innovation.
Caramel colour or E150d, is a common food and beverage colouring ingredient that is made by carefully heating food-grade carbohydrates with alkali or acid catalysts. Known as sulfite ammonia caramel, it gives baked items, sauces, soft drinks, and alcoholic beverages a rich brown colour. In food business, it is a preferred option because to its stability, solubility, and capacity to improve aesthetic appeal. Major food regulators across the world have authorised E150d and regulated it for safe consumption.
Kitchen appliances are a diverse category of electrical and mechanical devices that are essential in modern kitchens for various cooking and food preparation tasks. These appliances have revolutionized the way we prepare and cook food, making the process more efficient and convenient. For instance, refrigerators are crucial for storing perishable foods and keeping them fresh. Ovens and stoves are fundamental for baking, roasting, and cooking on open flames or electric coils. Microwaves provide quick heating, cooking, and defrosting, saving time in the kitchen. Dishwashers automate the often-tedious task of cleaning dishes, while blenders and food processors simplify chopping, pureeing, and blending ingredients.
A plastic cigarette lighter is a small portable hand-held device that gives a flame generally used for lighting cigarettes, cigars, candles, and other small things. They are mostly butane-gas fueled, which makes them easily disposable after all the fuel has been depleted. It's manufactured using polycarbonate or polypropylene plastic, so it's very lightweight and affordable.
Tissue paper, made from both virgin and recycled pulp, has become an essential part of daily life for cleaning, dusting, wrapping, and personal use. The industry's expansion is driven by luxurious tissue products, ultra-absorbent paper towels, and rising prices. Favorable factors such as growth in the IT sector, tourism, and MNCs, along with shifts in lifestyle and attitudes towards hygiene, cleanliness, and freshness, have boosted tissue consumption. Institutions like hospitals, malls, office complexes, and F&B chains are major consumers. Government support for sustainable practices has further spurred growth. West and South India are projected to be the largest consumers of tissues due to high foreign tourist influx, growing urbanization, and a hot climate that increases demand for disposable tissues.
While secondary research acts as the base of decision-making for businesses, primary research fills in the gaps that only a nuanced and personalized perspective can deliver. With enormous volumes of data being added daily on search engines, relying on obsolete and unauthentic data could cost businesses heavily. To stay ahead of the curve and make informed decisions, tapping directly into the information gathered through your customers is essential. This helps reveal the drivers of the decision-making process, unveiling unmet needs, and highlighting nascent trends before they take shape.
Consumer behavior mainly includes consumers’ mental, emotional, and behavioral responses toward the buying pattern of products. There are several factors that influence consumer behavior, such as personal, social, cultural, and psychological. Personal factors include the age, gender, and income of the consumer. Social factors like friends and family and cultural factors such as religion and tradition also play an important role in consumer buying patterns. Motivation, perception, and learning about goods and services change consumer preferences and fall under psychological factors.