Textile Recycling Plant Setup Cost in India: Process Flow, Machinery, DPR & Financial Model 2026
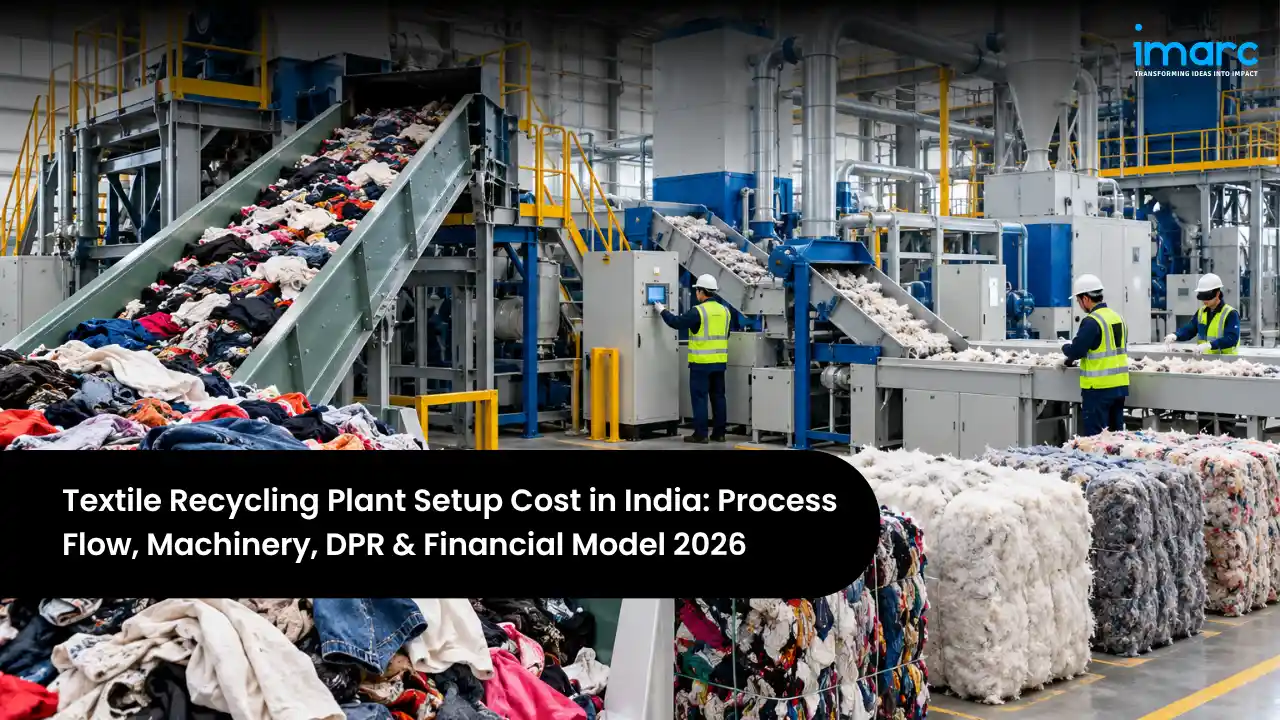
India is one of the world's largest producers and consumers of textiles, and it generates around 7 million tonnes of textile waste every year, from cutting scraps and yarn waste in factories to old clothes and household textiles. India also has a long tradition of textile recycling, with hubs such as Panipat turning old garments into blankets and yarn, and Tiruppur recycling knitwear waste into new fiber. Yet much post-consumer waste is still burned or landfilled, and very little is recycled back into high-quality fiber. Rising waste volumes, global brands' commitments to recycled content, export demand for certified recycled products, and growing policy attention make Textile Recycling Manufacturing Plant Setup in India a significant circular economy opportunity for manufacturers and investors.
Investment depends on the recycling route, the products made, and the scale. Simple mechanical units tear waste into fiber for blankets, felts, and fillings, while recycled-fiber spinning mills turn sorted cotton waste into yarn for new fabrics, and emerging chemical recycling plants break polyester or cotton down to their building blocks. The Textile Recycling Manufacturing Plant Cost ranges from about INR 2–6 crore for a small rag-tearing and fiber unit, through INR 25–80 crore for an integrated recycled-fiber and open-end spinning mill of 5,000 to 20,000 tonnes a year, to INR 200 crore or more for a chemical recycling plant. Textile waste makes up the largest share of operating cost, followed by power, so feedstock sorting, fiber recovery, and product quality are the decisions that shape profitability. At healthy utilisation, a well-run mechanical plant can deliver a gross margin of 30 to 40% and a net profit margin of 10 to 18%, with payback typically within 3 to 5 years.
This guide is written for investors trying to understand how to start a Textile Recycling manufacturing plant in India. It covers the main recycling routes and products, the demand drivers, the process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, the approvals and certifications involved, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| India Textile Waste Generated | About 7 Million Tonnes a year |
| Pre-Consumer vs Post-Consumer | About 42% pre-consumer, 58% post-consumer |
| Mechanical Recycling Units in India | About 900, mainly in Panipat and Tiruppur |
| Global Textile Recycling Market (2025) | USD 5.53 Billion, 2.4% CAGR to 2034 |
| Typical Plant Capacity | 5,000–20,000 Tonnes a year |
| Indicative Total Investment | INR 2–250 Crore |
The snapshot shows a very large waste stream and an established but largely mechanical recycling industry concentrated in a few clusters. Pre-consumer waste from factories is cleaner and easier to recycle and is already mostly recovered, while post-consumer waste is mixed, contaminated, and often lost to landfill or burning, creating room for better collection, sorting, and recycling. The wide investment range reflects a genuine choice between a small mechanical unit making fiber for blankets and felts and a larger recycled yarn or chemical recycling plant supplying brands with certified recycled content. The sections below work through that choice.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Recycled fiber, recycled yarn, blankets, non-woven felts, fillings, and wipers |
| Total Project Investment | INR 2 – 250 Crore (route and scale dependent) |
| Payback Period | 3 – 5 Years |
| Net Profit Margin | 10 – 18% |
| IRR | 16 – 24% |
| Preferred Clusters | Panipat, Tiruppur, Coimbatore, Ludhiana, Surat, Bengaluru, Delhi-NCR |
| Key Approvals | SPCB consents, factory license, Fire NOC, recycled content certifications |
| Key Requirement | Reliable, well-sorted feedstock and efficient fiber recovery |
These ranges provide a realistic frame for early planning, but actual returns depend on the cost and sorting quality of textile waste, fiber recovery and strength, the share of higher-value recycled yarn versus low-value felts and fillings, power costs, and success in winning brand and export customers who pay for certified recycled content. A site-specific Textile Recycling Feasibility Report narrows each of these assumptions to your chosen route, products, location, and capacity.
Table of Contents
- What is Textile Recycling?
- Why is Textile Recycling Manufacturing Growing in India?
- Textile Recycling Manufacturing Process Flow
- Raw Materials Required for Textile Recycling Manufacturing
- Location, Land & Infrastructure
- Textile Recycling Manufacturing Machinery and Equipment
- Textile Recycling Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals Required for Textile Recycling Manufacturing in India
- Recent Developments in the India Textile Recycling Manufacturing Industry
- How a Textile Recycling Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Textile Recycling?
Textile recycling recovers fiber from discarded fabrics and turns it into new products. In mechanical recycling, the most common route in India, waste is sorted by fiber type and colour, trims such as buttons and zips are removed, and the fabric is cut and torn back into fiber. The fiber is cleaned, often blended with some virgin fiber for strength, and then spun into yarn, needle-punched into non-woven felts, or used as filling. Because recycled fibers are shorter, mechanical recycling generally produces coarser yarns. Chemical recycling breaks polyester down into monomers or dissolves cotton into pulp, producing fiber close to virgin quality, but it is still emerging. Sorting accuracy and gentle, efficient fiber opening determine quality and value.
Commercially, recycled textiles serve a wide range of markets. A Textile Recycling Manufacturing Plant can supply yarn to weavers and knitters making denim, towels, home textiles, and apparel, sell blankets and shawls to domestic, institutional, and export buyers, supply non-woven felts and insulation to automotive and furniture makers, provide fillings for mattresses and cushions, and sell wiping cloths to industry. Brands seeking certified recycled content increasingly buy recycled yarn and fabric, often at a premium.
- Recycled Yarn: Open-end yarn from recycled cotton and blends for denim, towels, home textiles, and apparel.
- Blankets & Home Textiles: Blankets, shawls, rugs, and furnishings, a long-standing strength of Panipat.
- Non-Wovens & Insulation: Felts for automotive interiors, furniture, mattresses, and acoustic insulation.
- Fillings & Wipers: Fiber fillings for cushions and mattresses, and industrial wiping cloths.
The Main Recycling Routes and Products
Choosing the recycling route and products is the most important commercial decision, because it determines feedstock, machinery, capital cost, and customers:
| Route / Product | Feedstock | Key Property | Primary Demand |
|---|---|---|---|
| Rag Tearing to Fiber (Shoddy) | Sorted garments and fabric waste | Low capex, established | Blankets, felts, and fillings |
| Recycled Cotton Yarn (OE Spinning) | Colour-sorted cotton waste | No dyeing needed when colour-sorted | Denim, towels, home textiles |
| Non-Woven Felts | Mixed fiber waste | Uses lower-grade fiber | Automotive and furniture |
| Chemical Recycling of Polyester | Polyester-rich waste | Near-virgin quality fiber | Apparel and brand supply chains |
| Wipers & Reuse | Clean cotton garments | Simple processing | Industrial and export markets |
These choices shape the whole plant. Rag-tearing and felting units need modest investment and accept mixed waste, but earn lower prices. Recycled yarn mills need carefully sorted feedstock, carding, and open-end spinning, and they produce higher-value yarn that brands increasingly want. Chemical recycling requires large investment and advanced technology but can handle polyester and blends that mechanical routes cannot. Many new entrants begin with mechanical fiber recovery and open-end spinning of colour-sorted cotton waste, then add non-wovens or partner with chemical recyclers as feedstock systems and customer relationships grow.
Why is Textile Recycling Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
Growth is driven by waste volumes, brand commitments, export demand, and policy attention:
- Large waste volumes: India’s huge textile industry and rising clothing consumption generate millions of tonnes of waste every year.
- Brand commitments: Global and Indian fashion brands have targets to use recycled fibers and reduce waste in their supply chains.
- Export requirements: Export markets, especially in Europe, are moving towards stricter rules on textile waste and recycled content.
- Cost advantage: Recycled fiber from sorted waste can be cheaper than virgin cotton, especially when colour-sorted to avoid dyeing.
- Policy attention: New waste rules and government studies on textile waste are increasing focus on collection and recycling.
India-Specific Market Opportunity
| Segment | India Market Context | Manufacturing Role |
|---|---|---|
| Garment Export Hubs | Large pre-consumer cutting waste | Recycled fiber and yarn |
| Brands & Retailers | Recycled content commitments | Certified recycled yarn and fabric |
| Home Textiles & Blankets | Large domestic and export demand | Recycled blankets and furnishings |
| Automotive & Furniture | Need for felts and insulation | Non-woven products |
The strongest opportunity lies in combining reliable, well-sorted feedstock with certified, traceable recycled products that brands can use in their supply chains. Pre-consumer waste from garment hubs offers cleaner, consistent material, while post-consumer waste represents a much larger, underused resource for operators who can invest in collection and sorting. Certifications for recycled content help open premium export and brand markets.
Textile Recycling Manufacturing Process Flow
Understanding the process helps you plan equipment, layout, and where quality and cost are decided. Mechanical textile recycling runs from waste receipt and sorting through trim removal, cutting, tearing, cleaning, blending, carding, and spinning or felting into finished products. Accurate sorting and careful fiber opening determine fiber length, strength, and the value of the final product.
The Textile Recycling Manufacturing Process Flow
The sequence below reflects a mechanical plant producing recycled cotton yarn by open-end spinning. Felt and blanket plants follow similar opening steps and then use carding and needle-punching or weaving, while chemical recycling plants depolymerise or dissolve sorted waste instead of tearing it.
| Unit Operation | Key Activity |
|---|---|
| Waste Receipt & Inspection | Bales weighed and checked for quality |
| Sorting by Fiber & Colour | Waste sorted manually or with NIR sorters |
| Trim Removal & Cutting | Buttons, zips, and labels removed; fabric cut |
| Tearing & Opening | Fabric torn back into fiber |
| Cleaning & Dust Removal | Fiber cleaned of dust and short fibers |
| Blending | Recycled fiber blended with virgin fiber where needed |
| Carding | Fibers aligned into a sliver |
| Open-End Spinning or Felting | Sliver spun into yarn or formed into felts |
| Winding & Quality Testing | Yarn wound and tested for count and strength |
| Packing & Certification Records | Products packed with recycled content documentation |
Two factors decide profitability across this flow. The first is feedstock sorting: separating waste carefully by fiber type and colour allows the plant to produce coloured yarns without dyeing and to achieve consistent quality, which raises prices and saves water and chemicals. The second is fiber recovery and quality, because aggressive tearing shortens fibers and weakens yarn, so well-maintained tearing and opening lines, optimal blending, and good carding and spinning practice determine how much high-value yarn the plant can produce from each tonne of waste.
Raw Materials Required for Textile Recycling Manufacturing
The main input is textile waste, including pre-consumer cutting waste and yarn waste from factories, and post-consumer garments and household textiles. Other inputs include virgin fibers for blending, small amounts of chemicals or dyes where required, and packaging materials. Because waste is the largest cost and its sorting quality determines product value, reliable sourcing is central to project planning.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Pre- & Post-Consumer Textile Waste | Main fiber source | Garment factories, aggregators, collectors | 34–42% |
| Virgin Fiber for Blending | Add strength to recycled yarn | Domestic cotton and polyester | 4–6% |
| Chemicals & Dyes (if used) | Cleaning or shade correction | Domestic suppliers | 1–2% |
| Packaging Materials | Cones, bags, and bales | Domestic suppliers | 1–2% |
Pre-consumer waste from garment hubs such as Tiruppur, Bengaluru, Delhi-NCR, and Ludhiana is cleaner and more consistent, but competition for it is strong. Post-consumer waste is abundant but mixed, often soiled, and reaches recyclers through informal collection networks. Building partnerships with garment exporters, brands' take-back programmes, municipal and NGO collection systems, and organised aggregators, and investing in sorting, help secure consistent feedstock. Paying for well-sorted, dry material improves yield and quality.
Location, Land & Infrastructure
Site selection for a textile recycling plant is shaped by proximity to waste sources such as garment clusters and collection hubs, closeness to buyers such as weavers, knitters, and home textile makers, availability of skilled workers, reliable power, and established recycling ecosystems with suppliers and service providers.
Choosing the Best Location for Textile Recycling Manufacturing Plant Setup
| Cluster | Why It Works | Key Advantage |
|---|---|---|
| Panipat (Haryana) | World-renowned textile recycling hub | Skills, suppliers, and buyers |
| Tiruppur & Coimbatore (Tamil Nadu) | Knitwear and spinning centre | Pre-consumer waste and OE spinning |
| Ludhiana (Punjab) | Woollen and hosiery industry | Feedstock and markets |
| Surat (Gujarat) | Polyester and synthetic textile hub | Polyester waste and customers |
| Bengaluru & Delhi-NCR | Major garment export centres | Clean pre-consumer waste |
| Erode & Karur (Tamil Nadu) | Home textiles and spinning base | Customers for recycled yarn |
Panipat is the natural choice for blankets and mechanical recycling, offering an unmatched ecosystem of recyclers, machinery suppliers, skilled workers, and buyers. Tiruppur and Coimbatore are ideal for recycled cotton yarn because of their knitwear waste and open-end spinning expertise, while Surat suits polyester-focused recycling. Bengaluru and Delhi-NCR provide clean pre-consumer waste from garment exporters. The final choice should weigh feedstock access, customer proximity, labour, power costs, and the product focus.
Quality, Certification and Worker Safety
Brands and export customers expect recycled products to be consistent and traceable. A credible plant needs careful sorting systems, testing of fiber length, yarn count, and strength, and documentation of feedstock sources and recycled content, often verified through recognised recycled content certifications. Textile recycling creates fiber dust and fire risk, so dust extraction, humidification, fire detection and suppression, and worker protection are essential. An experienced Textile Recycling Manufacturing Consultant in India can help design sorting and processing lines, plan certifications and traceability, and set up safety systems so the plant meets the expectations of brands, auditors, and regulators.
Infrastructure Requirements (Mid-Sized Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 2 – 6 acres | Space for waste and finished goods storage |
| Waste Storage & Sorting Hall | Covered, ventilated area | Fire safety essential |
| Tearing & Opening Section | Rag tearing and opening lines | Dust extraction |
| Spinning or Felting Hall | Carding and spinning or needle-punching | Humidity control for spinning |
| Dust Collection & Humidification | Filters and humidification plant | Worker health and fire safety |
| Power Requirement | 1 – 4 MW | Stable supply with backup |
| Laboratory & Warehouse | Fiber and yarn testing | Supports certification |
Covered waste storage and sorting areas, tearing and opening lines with dust extraction, carding and spinning or felting halls with humidity control, and a testing laboratory are the defining infrastructure needs. Fire safety deserves particular attention because textile waste and fiber are highly flammable, so storage layout, detection, and suppression systems must be planned carefully.
Textile Recycling Manufacturing Machinery and Equipment
The equipment set covers sorting, trim removal, cutting, tearing and opening, cleaning, blending, carding, spinning or felting, and support systems. Tearing lines, carding, and open-end spinning machines account for most of the machinery budget. The main items are summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Sorting Tables & NIR Sorters | Sort waste by fiber and colour | Manual or automated |
| Trim Removal & Cutting Machines | Remove hard parts and cut fabric | Prevents machine damage |
| Rag Tearing Machines | Tear fabric into fiber | Multi-cylinder lines |
| Fiber Openers & Cleaners | Open and clean fiber | Gentle opening to preserve length |
| Blending Bale Openers | Blend recycled and virgin fibers | Accurate blend ratios |
| Carding Machines | Align fibers into sliver | Suited to recycled fiber |
| Open-End Rotor Spinning Machines | Spin coarse and medium yarn | High productivity |
| Needle-Punch Non-Woven Line | Produce felts | For automotive and furniture uses |
| Winding Machines | Wind yarn onto cones | Quality monitoring |
| Balers & Packing Equipment | Pack fiber and products | Export-ready packing |
| Dust Collection, Humidification & QC Lab | Support systems and testing | Fiber and yarn testing instruments |
Machinery should follow the route and product plan. Blanket and felt producers need tearing, carding, and weaving or needle-punching equipment, while recycled yarn mills need gentle opening, good carding, and open-end spinning. Automated colour and fiber sorting improves consistency and reduces labour, and modern tearing lines that preserve fiber length increase the share of high-value yarn.
Textile Recycling Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a mid-sized mechanical recycling plant producing recycled fiber and open-end yarn in India. The final Textile Recycling Investment Cost for your project will depend on the route, capacity, sorting automation, spinning or felting lines, support systems, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 50–60% | Sorting, tearing, carding, spinning or felting |
| Land & Buildings | 15–20% | Storage, processing, and spinning halls |
| Dust Collection & Humidification | 5–8% | Air handling and filtration |
| Utilities & Fire Safety | 4–7% | Power, compressors, and firefighting |
| Laboratory & Handling Equipment | 2–4% | Testing equipment and material handling |
| Pre-operative & Contingency | 3–5% | Installation, trials, DPR, certification |
| Working Capital | 10–15% | Waste inventory and receivables |
Machinery and buildings dominate the capital budget, while dust collection, humidification, and fire safety are essential for worker health and safe operation. Working capital is needed to stock sorted waste, which may be bought seasonally or in large lots, and to extend credit to yarn and fabric buyers. A detailed Textile Recycling Business Plan should model feedstock prices and availability, fiber recovery, product mix, certification premiums, and payment terms together, so that funding matches the real cash cycle of the business.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials (textile waste, virgin fiber) | 40–50% | Clean pre-consumer waste commands higher prices |
| Utilities (power, humidification) | 20–25% | Tearing, carding, and spinning loads |
| Labour | 10–14% | Sorting is labour-intensive |
| Maintenance & Spares | 4–6% | Tearing cylinders and spinning parts |
| Certification & Compliance | 1–3% | Audits and recycled content certification |
| Logistics & Overheads | 4–6% | Waste collection and product dispatch |
With feedstock, power, and labour making up most of the cost, margins depend on buying well-sorted waste at fair prices, recovering as much good fiber as possible, and selling into higher-value segments. A good operating model tracks feedstock cost per kilogram of output, fiber recovery, yarn quality and rejects, power use per kilogram, and the price premium for certified products, and tests how margins respond when waste prices rise or virgin cotton and polyester prices fall.
Financial Analysis and Profitability
Based on analysis of a mid-sized mechanical textile recycling plant, the financial profile is attractive, supported by low-cost feedstock relative to virgin fiber, established domestic markets, and rising brand demand for recycled content. The profitability of Textile Recycling manufacturing business in India improves markedly with good sorting, high fiber recovery, a growing share of recycled yarn and certified products, and long-term relationships with brands and exporters.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 30–40% | Higher for certified recycled yarn |
| Net Profit Margin | 10–18% | After depreciation and Indian corporate taxes |
| Payback Period | 3–5 Years | Faster in established clusters |
| IRR (Internal Rate of Return) | 16–24% | Higher with brand partnerships |
| Capacity Utilization (stable ops) | 65–85% | Depends on feedstock and orders |
| Break-even Capacity Utilization | 40–50% | Moderate fixed costs |
Product mix and feedstock quality decide where a plant lands within these ranges. Low-value fillings and felts from mixed waste earn modest margins and face price competition, while colour-sorted recycled yarn and certified products for brands command better prices. Because recycled fiber competes with virgin cotton and polyester, margins also depend on virgin fiber prices, so diversifying products and customers provides resilience.
Returns can be strengthened by investing in sorting, especially colour sorting that avoids dyeing, partnering with garment exporters and brands for steady feedstock and offtake, obtaining recycled content certifications, producing higher-value yarns and fabrics, and adding non-wovens for automotive and furniture customers. Consistent quality and transparent traceability are what earn long-term business from brands and export buyers.
Key Risks and Mitigation
The main risks are feedstock availability and quality, competition for clean pre-consumer waste, price competition from virgin fibers, fiber dust and fire hazards, and changing brand and export requirements. Feedstock risk is reduced through partnerships and sorting investment; price risk by product diversification and certification premiums; safety risk by dust control and fire protection; and market risk by building relationships with several brands and buyers. Promoters often work with a Textile Recycling Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals Required for Textile Recycling Manufacturing in India
Approvals for a textile recycling plant combine industrial and environmental permissions with fire safety, import, and recycled content certifications. Promoters setting up a Textile Recycling Manufacturing Plant in India generally need the following:
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, with dust control and, where washing or dyeing is involved, effluent treatment.
- Factory License: Registration and plan approval under the Occupational Safety, Health and Working Conditions Code, 2020 and state rules.
- Fire Safety Approval: Fire NOC with detection and suppression systems suited to flammable fiber and waste storage.
- Recycled Content Certifications: Certifications such as recognised global recycled standards and product safety certifications often required by brands and export buyers.
- Import Permissions: Licenses and conditions applicable to imports of used clothing or textile waste, where the business imports feedstock.
- Quality Certifications: ISO 9001 and other quality and social compliance certifications requested by customers.
- Business & Tax Registration: Company incorporation, GST, Udyam, IEC for imports and exports, and EPF and ESI registrations.
Pollution consent, the factory license, and the Fire NOC are usually on the critical path for starting production. Recycled content certifications require documented feedstock sourcing and traceability, so systems should be planned from the start. As India discusses Extended Producer Responsibility for textiles, plants with strong documentation will be well placed for any future requirements.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, recycling route, products, feedstock imports, target customers, export markets, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Textile Recycling Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- Large waste stream: India generates around 7 million tonnes of textile waste a year, with post-consumer waste making up the larger share.
- Mechanical recycling base: India has about 900 mechanical textile recycling units, mainly in Panipat and Tiruppur, but no large-scale chemical recycling plants in operation.
- Policy attention: The Ministry of Textiles published a report on textile waste in February 2026, while textile EPR has not yet been notified.
- New waste rules: The Solid Waste Management Rules, 2026, effective from April 1, 2026, strengthen segregation and recovery requirements that affect textile waste.
The common thread is a vast and under-used waste resource, a strong traditional recycling base, and rising pressure from brands, exports, and regulation. New entrants who invest in sorting, quality, certification, and partnerships across the value chain will be best placed as textile circularity gains momentum through the decade.
How a Textile Recycling Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from feedstock availability and route selection to plant design, machinery, certifications, and economics. It helps investors decide the right route, products, and capacity, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Textile Recycling Financial Model covering feedstock volumes and prices, fiber recovery, product mix and prices, certification premiums, power and labour costs, working capital, cash flows, break-even, return on investment, and payback. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a Textile Recycling Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a textile recycling project, a strong DPR also clarifies the feedstock sourcing and sorting strategy, the product and technology plan, the certification and traceability approach, and the customer strategy, which together are the factors most likely to decide success. By testing margins against waste prices, virgin fiber prices, and demand shifts, the report turns a circular economy opportunity into a plan that lenders and partners can trust.
Frequently Asked Questions
What are the first steps to set up a textile recycling manufacturing plant in India?
Start by choosing your recycling route, products, and capacity, and map feedstock sources and buyers. Then commission a feasibility study and DPR, secure land or a shed in a suitable cluster, obtain pollution consent, factory license, and Fire NOC, install sorting, tearing, carding, and spinning or felting machinery with dust collection, set up testing and traceability systems, and pursue recycled content certifications.
How much does it cost to set up a textile recycling manufacturing plant in India?
Investment ranges from about INR 2–6 crore for a small rag-tearing and fiber unit, through INR 25–80 crore for an integrated recycled-fiber and open-end spinning mill, to INR 200 crore or more for a chemical recycling plant, depending on route, capacity, and products.
What are the main steps in textile recycling?
The flow runs from waste receipt and inspection through sorting by fiber and colour, trim removal and cutting, tearing and opening, cleaning and dust removal, blending, carding, open-end spinning or felting, winding and quality testing, and packing with recycled content documentation.
Which machinery does a textile recycling manufacturing plant need?
Key equipment includes sorting tables and NIR sorters, trim removal and cutting machines, rag tearing machines, fiber openers and cleaners, blending bale openers, carding machines, open-end rotor spinning machines, needle-punch non-woven lines, winding machines, balers, dust collection and humidification systems, and a testing laboratory.
What raw materials are used in textile recycling?
The main input is textile waste, including pre-consumer cutting and yarn waste and post-consumer garments and household textiles, together with virgin fiber for blending, small amounts of chemicals or dyes where needed, and packaging materials.
How profitable is textile recycling manufacturing plant in India?
A well-run mechanical plant typically earns a 30 to 40% gross margin and a 10 to 18% net margin, with payback in 3 to 5 years. Profitability depends on feedstock cost and sorting quality, fiber recovery, product mix, certification premiums, and virgin fiber prices.
Which approvals does a textile recycling manufacturing plant need in India?
Typical approvals include State Pollution Control Board consents, a factory license, a Fire NOC, import permissions where feedstock is imported, recycled content and quality certifications requested by customers, and GST, Udyam, IEC, and labour registrations.
How do I get a feasibility study or DPR for a textile recycling manufacturing project?
A detailed feasibility study and DPR covers feedstock availability, route and product strategy, technology, certifications, approvals, and full financials. Investors usually engage a Textile Recycling Manufacturing Feasibility Study Consultant with experience in textile and recycling projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

India has more than a billion mobile connections, creating a large and recurring market for chargers, cables, protective cases, screen guards, earbuds and other mobile accessories.
The television has quietly become the most connected screen in many Indian homes. Streaming apps, cricket in 4K, YouTube, and voice-controlled content have turned the TV into a smart device, and falling prices, a lower GST rate, and easy online buying have brought smart TVs within reach of millions of first-time buyers.
India is sleeping better, or at least spending more to try. Rising incomes, smaller urban homes, a booming hotel sector, and growing awareness of back health have pushed households away from cotton gaddas toward engineered foam, spring, and hybrid mattresses.
Setting up a Diaper Manufacturing Plant in India is a high-speed converting venture powered by rising hygiene awareness, growing disposable incomes, low current penetration, and expanding demand across baby and adult categories.
Setting up a Liquid Detergent Manufacturing Plant in India is a formulation-and-blending venture with relatively accessible entry capital, powered by rising hygiene awareness, a steady shift from powders to liquids, expanding modern retail, and growing demand across laundry, dishwash, and household cleaning categories.
Setting up a Kraft Paper Manufacturing Plant in India is a high-demand, sustainability-driven venture, powered by the country's booming e-commerce, packaging, and corrugated-box industries. Kraft paper is the base material for corrugated boxes and packaging, and demand is rising as businesses shift from plastic to recyclable paper-based packaging.
Setting up a Garment Manufacturing Plant in India is a high-demand, employment-generating venture, powered by the country's vast textile base, skilled workforce, and growing role as a global apparel sourcing hub.
The Luxury Fashion Market reached USD 261.0 Billion in 2025 and is projected to reach USD 341.0 Billion by 2034, growing at a CAGR of 3.02% (2026–2034).
Setting up a Container Manufacturing Plant in India is a capital-efficient, high-demand venture powered by the country's fast-growing food, pharmaceutical, FMCG, and industrial packaging sectors.
Bath soap is a body wash product developed primarily to provide personal care. It is made by the alkali saponification, a method that generates soap salts and glycerin in the soap via a reaction between fats or oils and an alkali, such as sodium hydroxide. Bath soaps are made by separating out dirt, sweat, excess oil and microorganisms while helping to remove dirt, sweat, excess oil and water soap from the skin to avoid dirt, extra oil and bacteria and viruses while preserving the balance of both cleansing the skin and compatibility between the application.
Waste tyre recycling can be defined as the organized collection, treatment, and recovery of end-of-life tyres (ELTs) to produce new materials, energy sources, or secondary raw materials. Tyres are made up of vulcanized rubber, steel reinforcement, textiles, and chemical compounds, making them non-biodegradable materials that cannot be easily decomposed.
Wallpaper is a decorative and practical wall covering material used to cover interior surfaces for aesthetic purposes, protection, and ambiance. It is usually made from paper, vinyl, non-woven fibers, textile backing, or a combination of materials, printed or embossed with designs, textures, or solid colors.
The Australian footwear industry is experiencing a remarkable transformation as it navigates a confluence of shifting consumer preferences, technological advancements, and sustainability imperatives.
Tennis ball production is the process of making standardized balls for the game of tennis. The process involves making balls with specific performance and bounce features. A tennis ball is made up of a hollow rubber core that is filled with pressurized air. The core is then covered with a woven felt material.
Soap is a type of cleaning agent made by the chemical reaction of fats or oils and an alkali in a process known as saponification. The chemical reaction transforms triglycerides into soap, also known as fatty acid salts, giving these substances the properties of a surfactant, allowing the substance to be used for the removal of dirt, oil, and bacteria from surfaces.
The size of the global hair oil market has undergone significant transformation with increasing consciousness among consumers to adopt hair care as part of their personal wellness, beyond the realm of mere beauty. Hair oils, being long considered one of the traditional grooming essentials, have transformed into complex formulations to suit various hair types and scalp conditions. Over the past years, lifestyle change, growing awareness related to scalp health, and the rising demand for natural beauty have significantly impacted the consumption pattern in the hair oil segment.
The global online grocery market research landscape has undergone unprecedented changes in recent years, with an upward trend marking the way consumers engage with food retail. There has been a significant expansion in the size of the online grocery market, fuelled by changing consumer preferences, technological advances, and increased convenience associated with digital shopping. Households are showing a growing reliance on online platforms for regular essentials more than ever, making the sector a cornerstone of modern retail.
The UAE’s pet food sector has emerged as one of the most dynamic and lifestyle-influenced consumer categories. While historically smaller and more niche compared to mainstream food and beverage markets, the industry has grown in relevance due to changing demographics, international influences, and shifting consumer priorities. Residents across major cities are embracing pets as companions for emotional well-being and as part of a balanced lifestyle.
The Saudi Arabia road freight transport market represents one of the key building blocks of the economic infrastructure in the Kingdom, providing for cargo movement across various domestic supply chains. It also involves road freight operations, which allow for the distribution of goods-from manufactured goods, consumer goods, and industrial supplies to agricultural produce-across its large and wide geography.
The Saudi Arabia luxury market represents one of the most dynamic and rapidly evolving segments within the Middle Eastern premium retail landscape. As the Kingdom undergoes comprehensive economic diversification and social transformation, luxury consumption patterns are experiencing unprecedented shifts that reflect changing demographics, evolving consumer preferences, and ambitious national development goals.
The Philippines retail sector has become a pluralistic and dynamic environment where old-fashioned stores coexist with high-tech contemporary formats enabled by digital strength. The Philippines retail sector market size reached USD 648.2 Billion in 2025. The market is projected to reach USD 1,223.1 Billion by 2034, exhibiting a growth rate (CAGR) of 7.31% during 2026-2034.
Polyester fabric is a type of synthetic fabric made from polyester fibers. The main source of polyester fibers is petrochemical polymers like polyethylene terephthalate. Polyester fabric is made from processing chips of polymers to produce continuous filaments and staple fibers. The processing of polymers involves heating and melting chips of polymers made from petrochemical materials to produce continuous filaments and staple fibers.
India's gaming industry is rapidly evolving into one of the largest and most dynamic markets in the world. Driven by the increasing adoption of smartphones, affordable internet, and a tech-savvy youth population, gaming is becoming a mainstream form of entertainment.
The beauty landscape in India is undergoing a major transformation propelled by creativity, research, and technology. The India cosmetics market size was valued at USD 15.46 Billion in 2025. Looking forward, the market is expected to reach USD 25.39 Billion by 2034, exhibiting a CAGR of 5.7% from 2026-2034.
The drivers for changing India's textile sector include sustainability, modernization of production, and the introduction of advanced chemical solutions. The India textile market size was valued at USD 152.40 Billion in 2025. The market is projected to reach USD 213.75 Billion by 2034, exhibiting a CAGR of 3.83% from 2026-2034. It places the India textile chemicals market at an important position in this evolution, enabling everything from fiber processing to finishing.
India's consumer landscape is experiencing a profound transformation, driven by rapid digital adoption, evolving consumer preferences, and robust infrastructure development. The shift from traditional brick-and-mortar shopping to digital platforms represents more than a mere change in purchasing channels—it signifies a fundamental restructuring of how businesses engage with consumers and how millions of Indians access goods and services.
The Saudi Arabia deodorants market size continues to evolve as consumers embrace modern grooming habits, premium personal care products, and innovative hygiene solutions. With rising awareness of body care, fragrance layering, and daily freshness, deodorants have become an essential part of both men’s and women’s personal grooming rituals.
Pet foods consist of commercially processed foods that contain nutritional requirements tailored according to their consumption by domesticated pets like dogs, cats, birds, fish, and small animals. The foods contain planned nutritional compositions, such as ingredients like protein, carbohydrate, fat, vitamins, and minerals.
Perfume is a scented liquid composition that contains a mixture of fragrance chemicals, essential oils, aroma chemicals, fixatives, and solvents that are formulated for a pleasing and distinct fragrance emission upon application on human skin or on objects.
Technological advancements and shifting consumer expectations have caused the worldwide washing machine industry to drastically change. Washing machines are becoming indispensable parts of contemporary homes, smoothly integrating into smart home ecosystems from conventional semi-automatic models to fully linked, smart appliances.
Paper plates are disposable food containers, also referred to as tableware, and are made mostly from paperboard, pulp, and materials that are derived from fibers. These plates are designed to be convenient, hygienic, and easy to handle while being moisture and grease-proof, making them ideal for packing different food varieties, ranging from dry foods to moist and greasy food items.
The GCC cigarette lighter market is undergoing a steady phase of expansion due to evolving consumer habits, sustained product demand, and widening distribution channels across the region. In 2024, the GCC cigarette lighter market was valued at USD 197 Million. A key factor shaping industry performance is the rise in convenience-led purchases, driven by widespread retail penetration, duty-free availability, and the continued popularity of smoking-related accessories.
Paint brushes are hand-operated applicator tools, designed and manufactured with great precision, utilizing the capabilities of these tools to apply, spread, and manage liquid paint, along with other forms of paint such as varnishes, stains, lacquers, and surface finishes, onto a desired surface. Paint brushes are commonly manufactured using a series of components, including a handle, a ferrule, and natural or man-made hairs, or a combination of these two. They are also manufactured and designed with different shapes and sizes, according to the viscosity and texture of the paint.
Pan masala is a ready-to-use chewing mixture that is traditionally used as a mouth freshener as well as a digestive aid and is of South Asian origin. It is prepared by mixing different components such as areca nut, catechu, slaked lime, spices, flavoring agents, sweet agents, and aroma agents in specific proportions. It is usually packed ready for use and is different from the betel quid variant that is prepared by using fresh betel leaves. Contemporary formulations of pan masala aim to achieve consistency, shelf life, and standardized flavor so that it can be mass-produced and marketed.
Paper bags can be defined as the final product made from paper-based material such as kraft paper, recycled paper, or specialty paper, used for packing or storing products. Paper bags come in different shapes and sizes with varying strength, ranging from flat-bottom paper bags, gusseted paper bags, and handled paper bags. Paper bags can be biodegradable, can be recycled, and can be made from renewable resources.
The Brazil cosmetics products market represents one of the most vibrant and diverse beauty sectors in Latin America, reflecting a deep-seated cultural emphasis on personal appearance, wellness, and self-care. The Brazilian consumer has long been known for a keen taste for grooming, fashion, and aesthetics, which logically applies to the cosmetics industry. Driven by an expanding middle-class population, an increase in urbanization, and increasing awareness about wellness-oriented lifestyles, the market continues to evolve.
The commercial landscape across the globe is undergoing a seismic shift, driven by technology, changing consumer expectations, and macroeconomic volatility. This transformation is particularly pronounced in high-density, globally connected urban centres like Singapore. Historically a powerhouse of trade and luxury commerce, the nation is now navigating an intricate matrix of digital disruption and soaring operational pressures.
The India confectionery industry has emerged as one of the most dynamic segments within the country's food and beverage sector. Driven by changing consumer preferences, rising disposable incomes, and evolving lifestyles, the market continues to witness remarkable transformation across urban and rural landscapes.
As disposable incomes rise, households are diversifying across investment-grade gold, diamond-studded jewellery, and designer ornaments. Gold, in particular, holds unmatched cultural and economic importance, sustaining demand even through economic fluctuations. Recent indicators show how this cultural attachment continues to translate into measurable investment momentum. Gold demand stood at 135 tonnes in Q2 2025, with a full-year forecast between 600 and 700 tonnes. By mid-2025, India’s total gold holdings reached 66.7 tonnes, with two tonnes added in June and nine tonnes in the first half of the year.
Mobile accessories encompass a wide range of auxiliary products that are intended to complement, protect, enhance, or extend the functional capabilities of smartphones and other portable communication devices. Examples of these accessories include protective cases, screen guards, chargers, power banks, earphones, wireless earbuds, smart wearables, mounts, portable speakers, and connectivity adapters. They enable better usability, device safety, personalization, convenience, and integration with digital ecosystems. Mobile accessories are made from a variety of materials and technologies to meet various performance, durability, and design requirements for different groups of users.
Japan boasts a long and rich culture of traditional board games such as Go and Shogi, which have long been a fundamental component of its culture. The current board game market in Japan, though, is a vibrant mix of these indigenous games and an incredibly diverse range of modern games based on both Western and domestic design schools.
The tobacco industry has long been a cornerstone in world trade and consumer culture, shaping the courses of economies, employment landscapes, and industrial practices for centuries. Even in today's world, with growing awareness regarding health and sustainability, tobacco remains an imposing force in global commerce.
The Australia sportswear industry is experiencing unprecedented momentum, transforming into a multi-billion-dollar powerhouse where fashion, fitness, and lifestyle converge. As health consciousness sweeps the continent and athleisure becomes a wardrobe staple, the Australian market leads a global revolution in performance apparel.
Japan's luxury apparel industry has traditionally been characterized by its profound respect for craftsmanship, quality, and cultural refinement. Japanese consumers have a reverence for art and nuance, preferring items that reflect precision and enduring design over short-lived trends. Over the past decade, Japanese luxury fashion has transcended conventional retailing experiences and assumed a contemporary identity that coalesces international influences with domestic sentiments.
A mattress is a cushioned structure intended to support the human body, either while sleeping, resting, or for therapeutic purposes. It is typically made up of comfort layers, including foam, latex, fiber, or gel, combined with a supportive core, like innerspring coils, high-density foam, or hybrid constructions. Mattresses are designed to evenly distribute body weight to relieve pressure points and ensure proper spinal alignment.
Liquid detergent is a formulated cleaning solution comprising surfactants, solvents, builders, enzymes, pH stabilizers, perfumes, and other additives, which are collectively used for removing dirt, stains, and oils from fabrics, dishes, and different surfaces. Unlike powdered detergents, liquid detergents dissolve immediately in water, allowing even distribution during washing and effective performance in both hot and cold water.
The Japan personal luxury goods industry stands as one of the world’s most crucial and dynamic markets, consistently ranking among the top three globally, alongside the United States and China. In 2024, Japan personal luxury goods market size reached USD 32,060.65 Million in 2024.
The luxury watch industry represents one of the most enduring segments of the global fashion and lifestyle market. Combining precision engineering with timeless craftsmanship, luxury watches continue to hold strong appeal among high-net-worth individuals, collectors, and aspirational consumers. The global luxury watch market size reached USD 29.12 Billion in 2024, reflecting steady growth driven by premiumization, rising consumer demand in emerging economies, and the enduring value of heritage timepieces.
The Vietnam athleisure market stands at a pivotal juncture, experiencing remarkable transformation driven by evolving lifestyles, rising health consciousness, and rapid urbanization. As Vietnamese people are increasingly prioritizing wellness and seeking versatile clothing that seamlessly transitions from gym workouts to casual social settings, the demand for activewear trends has surged dramatically. With lifestyle apparel Vietnam witnessing unprecedented growth and fitness clothing demand reaching new heights, both international brands and homegrown labels are competing vigorously to capture market share in this dynamic sector.
The Philippines conveyor belt market is picking up speed, powered by the country’s industrial growth and focus on automation. According to the IMARC Group, the market reached USD 31.23 Million in 2024, reflecting notable growth across manufacturing, mining, logistics, and food processing. As industries modernize, the need for efficient material handling systems is creating strong momentum for both domestic and imported conveyor solutions.
The US retail market is undergoing a profound transformation, fueled by the integration of artificial intelligence (AI) across multiple business operations. From personalized consumer engagement to predictive inventory management and dynamic pricing strategies, AI is redefining how retailers operate, compete, and deliver value. Increasing consumer expectations for seamless, personalized, and efficient shopping experiences are prompting businesses to embrace AI-driven solutions to optimize performance, reduce costs, and enhance decision-making.
The global beauty and personal care products market is undergoing a profound transformation, driven by technological innovation, evolving consumer expectations, and sustainability-focused practices. Increasing consumer awareness of health, wellness, and ethical sourcing is compelling companies to rethink traditional formulations and adopt advanced manufacturing techniques. Businesses are now integrating biotechnology, artificial intelligence, and data-driven insights into product development, distribution, and marketing strategies.
The Philippines board game market is on a winning streak, fueled by a growing passion for social play, learning, and creative pastimes. According to IMARC Group, the market reached USD 83.39 Million in 2024, reflecting how board gaming is becoming a favorite form of entertainment across generations. Family games, strategy and role-playing titles, and educational options for kids are gaining steady traction, alongside collectible and pop culture–inspired editions.
The Australian fantasy sports industry is entering a phase of heightened momentum, with market size for 2024 reaching approximately USD 810.6 Million, as detailed in a recent report. This market is forecast to grow to USD 2,180.2 Million by 2033, representing a compound annual growth rate (CAGR) of around 10.4 % from 2025 through 2033 .
Australia's textile recycling sector is experiencing a technological renaissance, with 40% of SMEs currently adopting artificial intelligence (AI), marking a 5% increase compared to the previous quarter (July-Sept 2024). The percentage of businesses unaware of how to utilize AI has decreased by 2% to 21%.
Containers are standardized, tough, watertight containers for efficient storage and transportation of goods by ship, rail, and truck without the need for handling the cargo itself. They are the lifeblood of global trade and logistics, allowing for effective intermodal transport. Constructed from high-strength steel, aluminum, or composite materials, they are designed to withstand rigorous marine and environmental elements. The most common types are dry storage containers for general cargo; however, there are also refrigerated (reefers) for perishables, tank containers for liquids and gases, open-top and flat-rack for oversized equipment, and high-cube for voluminous cargo. Standardization, mainly through ISO specifications, allows for seamless compatibility and efficiency throughout global logistics systems.
Carpet is a textile floor covering made of a pile, tufts of yarn or fiber, sewn to a backing for dimensional stability. Carpets are manufactured in various construction forms: tufted (universal across the world, yarn punched through a primary backing and treated with secondary backing), woven (Wilton and Axminster, highly valued for durability and pattern intricacy), needle-felt (bonded fibers for industrial applications), and knotted (hand-made rugs).
Aloe vera gel is a natural concentrate obtained from the parenchyma of the inner leaf of Aloe barbadensis miller, which is valued for its therapeutic, nutritional, and cosmetic uses. The gel mostly comprises water (more than 95%) and polysaccharides, vitamins, minerals, amino acids, enzymes, and antioxidants responsible for its soothing, moisturizing, and healing actions. Renowned for its anti-inflammatory, antimicrobial, and skin-rejuvenating properties, the aloe vera gel finds broad application in personal care cosmetics, pharmaceuticals, food supplements, and beverages.
Aloe vera is a perennial fleshy succulent plant of the species Aloe barbadensis miller, grown worldwide for its nutritional, medicinal, and cosmetic benefits. It has two primary constituents: the transparent inner gel consisting mainly of polysaccharides, vitamins, enzymes, and amino acids; and the yellowish latex, consisting of anthraquinones with powerful laxative properties. Aloe vera gel is highly prized for its emollient, moisturizing, and healing properties and is a common ingredient in skincare, personal care, and pharmaceutical products.
Air purifiers are appliances that enhance indoor air quality by eliminating pollutants like dust, allergens, smoke, volatile organic compounds (VOCs), and microbial particles. They work on various technologies such as HEPA (High-Efficiency Particulate Air) filters, activated carbon filters, UV-C light, ionizers, and photocatalytic oxidation. Their major components are usually fans or blowers, filter media, sensors, electronic controls, and metal or durable plastic housings. Some of the crucial characteristics of air purifiers include efficiency of filtration, airflow, noise levels, power consumption, and filter material durability.
Air coolers are evaporative coolers based on the principle of water evaporation, utilizing a fan or blower to blow cooled air, as opposed to air conditioners, which function based on refrigerant and compressor principles. Air coolers are designed to deliver low-cost and energy-efficient temperature management, mainly applicable to dry and hot climates. They generally consist of a pump, motor, cooling pads, water tank, blower/fan, and electronic control units. Main characteristics are low energy usage, environmental friendliness, portability, and low cost. Production of air coolers typically consists of combining sheet metal or plastic enclosures with motor-driven fans, water distribution networks, and cellulose or aspen cooling pads.
A4 paper, which is one of the most commonly used paper formats around the world, is 210 mm × 297 mm and forms the part of the ISO 216 system. It mainly consists of cellulose fibers obtained from wood pulp, recycled papers, or other fibrous raw materials like bagasse or bamboo. A4 paper contains crucial characteristics like smoothness, even thickness, high opacity, brightness, tensile strength, and durability, which enable it for printing, copying, and writing. The production process includes pulping raw fibers, bleaching for whiteness, refining for increasing fiber bonding, and sheet formation under regulated drying and calendaring.
The manufacturing sector is constantly changing with continuously rising demands for sustainability, innovation, and efficiency. The time comes when companies want to expand their business or venture into new markets.
India's manufacturing industry is experiencing a remarkable transformation and growth in 2025, aiming to establish the nation as a key player in global manufacturing. Supported by governmental initiatives such as the Make in India program and the Production Linked Incentive (PLI) schemes, the sector has drawn significant foreign direct investment (FDI) and encouraged innovation across multiple industries.
India's manufacturing industry is undergoing a turning point in 2025 based on strong government initiatives, a highly skilled and youthful population, and a worldwide trend towards diverse supply chains.
The global tobacco sector remains one of the most mature yet closely scrutinized industries in the world. With demand persisting across both developing and developed markets, cigarette production continues to be a high-volume, technically refined activity governed by extensive regulation and economic influence.
The global vegan cosmetics market is experiencing unprecedented growth, driven by a new wave of conscious consumers who demand beauty products that are not only effective, but also ethical, sustainable, and cruelty-free. This movement is more than just a passing trend; it's a fundamental shift in values that is reshaping the industry.
The global online grocery market has rapidly evolved from a convenience service to a mainstream retail segment, reshaping how consumers shop for everyday essentials. According to the IMARC group report, the market reached a value of USD 710.10 Billion in 2024 and is projected to witness consistent expansion.
The India textile market is picking up serious momentum, supported by smarter tech and changing user preferences. As more buyers look for eco-friendly, premium-quality products, manufacturers are stepping up with automation, digital tools, and flexible production systems.
The global toys market plays a crucial role as toys fundamentally support child development by fostering creativity, cognitive skills, and social interaction. In 2024, the global toys market was valued at USD 113.94 Billion.
The worldwide luxury watch market is poised for sustained growth, driven by rising affluence, aspirational lifestyle, and digital evolution. As consumers place greater importance on exclusivity and craftsmanship, demand for luxury watches is growing in developed as well as emerging markets.
Baby wipes are wet disposable wipes used to clean the tender skin of an infant, mostly when changing diapers. Composed of non-woven materials and embedded with delicate cleansing products, commonly made from water, mild surfactants, moisturizers such as aloe vera, and preservatives baby wipes are made to be delicate, hypoallergenic, and safe for daily use.
A tennis ball is a type of high-performance sporting ball used in both competitive and recreational tennis. On various court surfaces, its rubber core and felt covering provide the best bounce, speed, and durability. Both pressurised and non-pressurized tennis balls are available to accommodate different playing situations and ability levels. Under international regulations, they are crucial for competitions and training, and business expansion is being driven by sustainability and material innovation.
Caramel colour or E150d, is a common food and beverage colouring ingredient that is made by carefully heating food-grade carbohydrates with alkali or acid catalysts. Known as sulfite ammonia caramel, it gives baked items, sauces, soft drinks, and alcoholic beverages a rich brown colour. In food business, it is a preferred option because to its stability, solubility, and capacity to improve aesthetic appeal. Major food regulators across the world have authorised E150d and regulated it for safe consumption.
Kitchen appliances are a diverse category of electrical and mechanical devices that are essential in modern kitchens for various cooking and food preparation tasks. These appliances have revolutionized the way we prepare and cook food, making the process more efficient and convenient. For instance, refrigerators are crucial for storing perishable foods and keeping them fresh. Ovens and stoves are fundamental for baking, roasting, and cooking on open flames or electric coils. Microwaves provide quick heating, cooking, and defrosting, saving time in the kitchen. Dishwashers automate the often-tedious task of cleaning dishes, while blenders and food processors simplify chopping, pureeing, and blending ingredients.
A plastic cigarette lighter is a small portable hand-held device that gives a flame generally used for lighting cigarettes, cigars, candles, and other small things. They are mostly butane-gas fueled, which makes them easily disposable after all the fuel has been depleted. It's manufactured using polycarbonate or polypropylene plastic, so it's very lightweight and affordable.
Tissue paper, made from both virgin and recycled pulp, has become an essential part of daily life for cleaning, dusting, wrapping, and personal use. The industry's expansion is driven by luxurious tissue products, ultra-absorbent paper towels, and rising prices. Favorable factors such as growth in the IT sector, tourism, and MNCs, along with shifts in lifestyle and attitudes towards hygiene, cleanliness, and freshness, have boosted tissue consumption. Institutions like hospitals, malls, office complexes, and F&B chains are major consumers. Government support for sustainable practices has further spurred growth. West and South India are projected to be the largest consumers of tissues due to high foreign tourist influx, growing urbanization, and a hot climate that increases demand for disposable tissues.
While secondary research acts as the base of decision-making for businesses, primary research fills in the gaps that only a nuanced and personalized perspective can deliver. With enormous volumes of data being added daily on search engines, relying on obsolete and unauthentic data could cost businesses heavily. To stay ahead of the curve and make informed decisions, tapping directly into the information gathered through your customers is essential. This helps reveal the drivers of the decision-making process, unveiling unmet needs, and highlighting nascent trends before they take shape.
Consumer behavior mainly includes consumers’ mental, emotional, and behavioral responses toward the buying pattern of products. There are several factors that influence consumer behavior, such as personal, social, cultural, and psychological. Personal factors include the age, gender, and income of the consumer. Social factors like friends and family and cultural factors such as religion and tradition also play an important role in consumer buying patterns. Motivation, perception, and learning about goods and services change consumer preferences and fall under psychological factors.