Cigarette Lighter Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
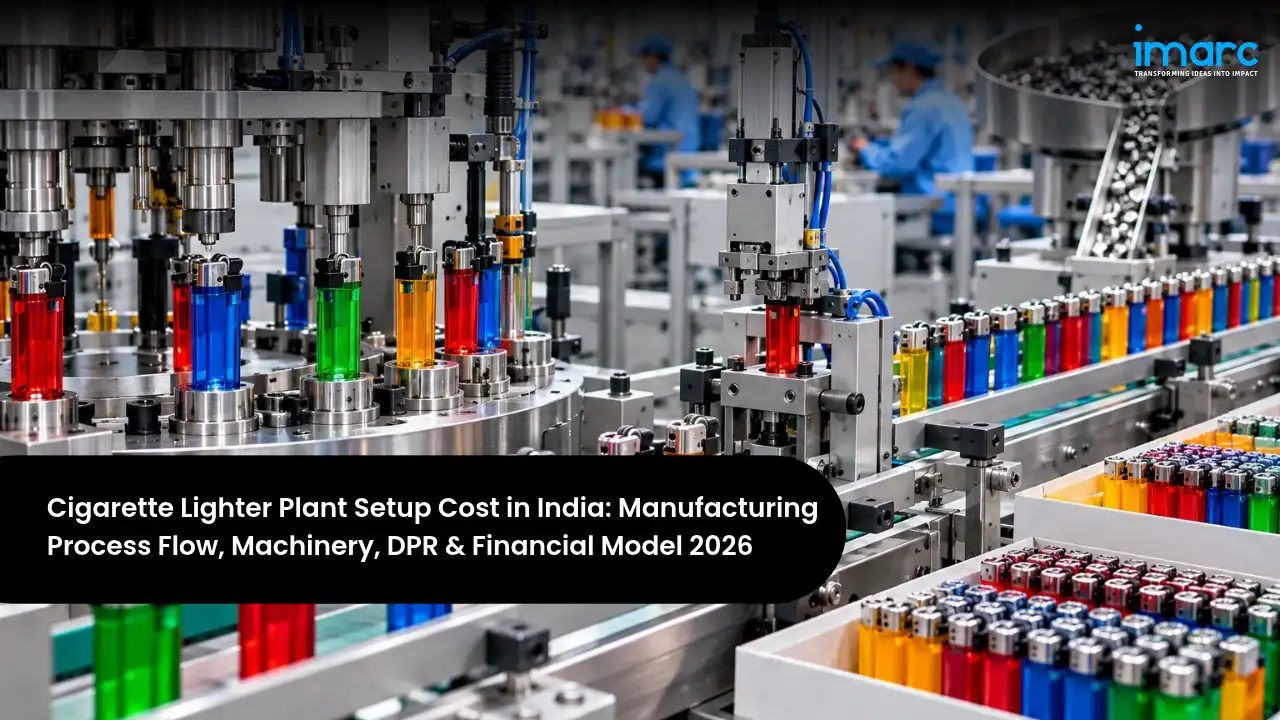
A pocket lighter is a small plastic or metal reservoir of liquefied butane fitted with a valve, a flame adjuster, and an ignition system, either a steel wheel striking a flint or a piezoelectric spark, that releases and lights a controlled flame at the press of a button. Disposable models dominate volumes in Indian shops and kitchens, while refillable, windproof, and long-nozzle utility models serve premium, outdoor, and household markets. IMARC values the global market at about USD 6.63 billion in 2025 and expects it to reach USD 7.80 billion by 2034. In India, imports below INR 20 per piece were banned in June 2023, imports of parts were restricted in October 2024, and all lighters must now meet BIS standards, so Cigarette Lighter Manufacturing Plant Setup in India has become a clear import substitution opportunity for consumer goods and plastics investors.
Investment depends mainly on annual output, whether the plant moulds its own bodies or assembles bought-in parts, the mix of flint, electronic, and refillable models, the level of automation in assembly and gas filling, butane storage and safety systems, and BIS testing facilities. The Cigarette Lighter Manufacturing Plant Cost ranges from about INR 3–8 crore for an assembly unit making 20 to 50 million pieces a year, to INR 35–55 crore for an integrated plant of about 150 million pieces a year with moulding, automated assembly, and gas filling, and INR 80–120 crore for plants above 300 million pieces. Plastics, metal parts, and butane make up 60 to 70% of operating cost, so buying well and keeping rejection rates low decide competitiveness. IMARC estimates a gross margin of 35 to 45% and a net margin of 15 to 20% for a well-run plant.
This guide is written for investors exploring how to start a Cigarette Lighter manufacturing plant in India. It focuses on an integrated plant making about 150 million disposable flint and electronic lighters a year, roughly 500,000 pieces a day, with in-house moulding of bodies, automated assembly, butane filling, and BIS testing, selling through distributors, modern retail, and exports, and also explains smaller assembly units and larger plants. It covers products and markets, the demand outlook, the production process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, certification and approvals, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Global Market (2025) | About USD 6.63 Billion |
| Global Market Forecast (2034) | USD 7.80 Billion, 1.8% CAGR |
| Import Rule (June 2023) | Banned Below INR 20 CIF per Piece |
| Parts Imports (2023-24) | USD 4.86 Million, Now Restricted |
| Typical Plant Capacity | 100 – 300 Million Units a Year |
| Indicative Total Investment | INR 3 Crore to 120 Crore |
The snapshot shows a mature global market with slow growth, but a much more favourable picture in India, where trade and quality rules have closed the door on cheap imports. Domestic producers now supply the low-price segment that imports used to fill, and the BIS requirement rewards plants that invest in proper testing and safety.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Flint, electronic, refillable, utility |
| Plant Capacity | 20 – 300+ Million Units per Year |
| Total Project Investment | INR 3–8 Crore (assembly unit) to 35–55 Crore (150 million units) |
| Payback Period | 3 – 5 Years |
| Net Profit Margin | 15 – 20% |
| IRR | 20 – 28% |
| Preferred States | Tamil Nadu, Gujarat, Uttar Pradesh, Maharashtra, Haryana, West Bengal |
| Key Requirement | BIS license, PESO approval, distribution |
These ranges provide a realistic frame for early planning, but actual returns depend on resin and butane prices, the cost and availability of valves, piezo units, and metal parts now that part imports are restricted, moulding and assembly rejection rates, the product mix, distributor margins, BIS testing costs, export demand, and the working capital tied up in stock and trade credit. A site-specific Cigarette Lighter Feasibility Report narrows each of these assumptions to your chosen capacity, location, product mix, and buyers.
Table of Contents
- What is a Cigarette Lighter Manufacturing?
- Why is Cigarette Lighter Manufacturing Growing in India?
- Cigarette Lighter Manufacturing Process Flow
- Raw Materials Required for Cigarette Lighter Manufacturing
- Location, Land & Infrastructure
- Cigarette Lighter Manufacturing Machinery and Equipment
- Cigarette Lighter Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Cigarette Lighter Manufacturing in India
- Recent Developments in the Cigarette Lighter Manufacturing Industry
- How a Cigarette Lighter Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is a Cigarette Lighter Manufacturing?
A pocket lighter stores a few grams of liquefied butane under pressure in a moulded body, usually made of acrylonitrile styrene or acetal for strength and clarity. Pressing the lever opens a small valve, gas passes through a filter and burner, and a spark from a flint wheel or a piezo unit lights it, while a spring closes the valve when the lever is released. Each piece must not leak, must shut off reliably, must keep the flame within safe height limits, and must survive drops and heat. Leak rate, flame height, shut-off reliability, number of lights per fill, and finish decide value.
Commercially, lighters are sold through distributors to paan shops, grocery stores, and kiosks, through modern retail and e-commerce, to households for lighting gas stoves and lamps, to brands that order custom-printed promotional pieces, and to importers in Africa, the Gulf, and South Asia. A Cigarette Lighter Manufacturing Plant can serve all these channels by changing body colours, prints, ignition types, and packaging on the same lines. Buyers value low price, safe and reliable lighting, attractive designs, and steady supply.
- Retail: Paan shops, grocery, kiosks.
- Households: Gas stoves, lamps, candles.
- Promotional: Custom printed pieces.
- Exports: Africa, Gulf, South Asia.
The Main Products and Applications
Choosing the product mix is the most important commercial decision, because it determines moulds, assembly lines, components, and margins:
| Product Type | Description | Key Property | Primary Demand |
|---|---|---|---|
| Flint Disposable | Spark wheel | Lowest cost | Mass retail |
| Electronic Disposable | Piezo ignition | Easy lighting | Retail, kitchens |
| Refillable Pocket | Refill valve | Reusable | Premium retail |
| Windproof Jet | Turbo flame | Works in wind | Outdoor users |
| Utility Lighter | Long nozzle | Safe reach | Gas stoves, candles |
| Promotional | Custom printed | Brand visibility | Corporates, FMCG |
These choices shape the whole project. Flint and electronic disposables give high volumes at low prices through wide distribution, while refillable, jet, and utility models earn better margins but need extra parts, stronger bodies, and more testing.
Why is Cigarette Lighter Manufacturing Growing in India?
Key Growth Drivers in India
Demand for domestic production is supported by trade rules, quality standards, and steady consumer use:
- Import ban: Imports below INR 20 CIF per piece have been prohibited since June 2023.
- Parts curbs: Restrictions on part imports since October 2024 favour integrated plants.
- BIS standard: All lighters must meet IS/ISO 9994 and carry the BIS mark.
- Household use: More LPG and piped gas homes use lighters for stoves.
- Exports: Low-cost producers can serve Africa, the Gulf, and neighbours.
India-Specific Market Opportunity
| Segment | Market Context | Manufacturing Role |
|---|---|---|
| Retail Outlets | Mass market | Disposable volume |
| Kitchen Use | LPG households | Utility models |
| Import Substitution | Ban below INR 20 | Domestic supply |
| Promotional | Branded orders | Custom printing |
The strongest opportunity for new entrants lies in supplying BIS-certified disposables to the mass market that imports used to serve, in utility models for kitchens, and in printed promotional pieces. Producers that combine in-house moulding, domestic component supply, efficient automated assembly, and strong distribution will be best placed to grow.
Cigarette Lighter Manufacturing Process Flow
Understanding the process helps you plan equipment, layout, and where cost and quality are decided. The flow runs from resin drying and injection moulding of bodies and small parts through ultrasonic welding of the base, valve and filter assembly, butane filling, leak testing, fitting of the flint wheel or piezo unit and the metal hood, flame testing, printing and labelling, and packing. Moulding precision and weld quality decide whether a piece holds gas, while valve assembly and flame testing decide safety.
The Cigarette Lighter Manufacturing Process Flow
The sequence below reflects an integrated plant making disposable lighters. Assembly-only units start at the welding stage with bought-in bodies.
| Unit Operation | Key Activity |
|---|---|
| Resin Drying | Remove moisture |
| Injection Moulding | Bodies, small parts |
| Ultrasonic Welding | Seal the base |
| Valve Assembly | Valve, filter, spring |
| Gas Filling | Liquefied butane |
| Leak Testing | Water bath, sensors |
| Ignition Assembly | Flint wheel or piezo |
| Flame Testing | Height, shut-off |
| Printing & Labelling | Brand, warnings |
| Packing & Dispatch | Trays, cartons |
Two factors decide profitability across this flow. The first is rejection rate, because a single leaking weld or faulty valve means a scrapped piece and lost gas, so precise moulds, consistent welding, and inline testing directly set the cost of each good unit. The second is automation and line speed, since margins per piece are small and volumes are huge, so fast automated assembly and filling lines with few operators decide the cost per thousand pieces and the return on investment.
Raw Materials Required for Cigarette Lighter Manufacturing
The main inputs are moulding resins such as acrylonitrile styrene or acetal for bodies and parts, liquefied isobutane or butane blends as fuel, valves, filters, and springs, steel wheels and flints or piezo units for ignition, stainless steel hoods, and packaging materials such as display trays, cartons, and labels.
| Input | Role in Product | India Sourcing | % of OpEx |
|---|---|---|---|
| Moulding Resins | Body, lever, parts | Domestic producers | 25–30% |
| Butane Gas | Fuel | Refiners, gas suppliers | 8–12% |
| Metal Parts | Hood, wheel, spring | Domestic stampers | 10–14% |
| Valves & Piezo Units | Gas control, spark | Domestic, some imports | 10–14% |
| Packaging | Trays, cartons, labels | Domestic suppliers | 5–8% |
Components are the biggest supply risk now that part imports are restricted, so developing local suppliers for valves, piezo units, and flints, or making them in-house, is central to the plan.
Location, Land & Infrastructure
Site selection for a lighter plant is driven by access to plastics and metal component suppliers, a reliable butane supply, skilled moulding and assembly workers, and closeness to large consumer markets for distribution. Other factors include space for licensed gas storage with safety distances, industrial estates that accept pressurised gas handling, good road and port links, and state incentives on capital, power, and employment. Locating in an established plastics or consumer goods cluster cuts component costs and lead times.
Choosing the Best Location for Cigarette Lighter Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Tamil Nadu | Chennai, Coimbatore | Components, ports |
| Gujarat | Ahmedabad, Vapi | Plastics, gas supply |
| Uttar Pradesh | Noida, Ghaziabad | Northern demand |
| Maharashtra | Pune, Bhiwandi | Moulding cluster |
| Haryana | Manesar, Bawal | Logistics hubs |
| West Bengal | Kolkata region | Eastern markets |
Gujarat offers resin and gas supply with a deep plastics base, while Tamil Nadu and Maharashtra provide skilled moulding and component makers. The final choice should weigh component access, gas supply, labour, distribution reach, and incentives.
Quality, Safety and Environmental Systems
Every piece sold in India must meet IS/ISO 9994, which covers flame height, shut-off, resistance to drops, heat, and pressure, and burning behaviour, and must carry the BIS mark under a license. A credible plant needs inline leak and flame testing on every piece, a laboratory for drop, temperature, and pressure tests on samples from each batch, and full batch traceability, while child-resistant designs are needed for markets that require them. Safety focuses on butane storage and filling, with flameproof electricals, gas detectors, ventilation, and fire suppression in filling rooms. Environmental systems cover plastic scrap recycling, rejected units, and safe venting of gas. An experienced Cigarette Lighter Manufacturing Consultant in India can help plan capacity, product mix, automation, and BIS and PESO approvals so the plant meets regulatory and customer requirements from the start.
Infrastructure Requirements (150 Million Units a Year)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Plant Land | 3 – 5 acres | Gas safety distances |
| Built-up Area | 60,000 – 80,000 sq ft | Separate filling block |
| Power Supply | 1.5 – 2 MVA | Moulding machines |
| Butane Storage | Bullet tanks | PESO licensed |
| Filling Room | Flameproof | Gas detection |
| Utilities | Compressed air, chillers | Moulding, assembly |
| Testing Lab | Drop, heat, pressure | BIS compliance |
A licensed butane storage and flameproof filling area, a reliable power supply for moulding, and a well-equipped testing laboratory are the most important infrastructure requirements, since they decide both output and the right to sell.
Cigarette Lighter Manufacturing Machinery and Equipment
The equipment set covers moulding, welding, assembly, gas filling, testing, printing, and packing. Moulding machines and moulds, together with automated assembly lines, account for most of the investment, followed by filling, testing, and gas storage.
| Equipment | Function | Key Specification |
|---|---|---|
| Injection Moulding | Form bodies, parts | 80 – 250 Tonne |
| Multi-cavity Moulds | Shape parts | Hardened steel |
| Ultrasonic Welders | Seal bases | Automatic |
| Assembly Lines | Fit parts | Rotary, automatic |
| Gas Filling Machines | Fill butane | Multi-head |
| Leak Test Systems | Check seals | Water bath, sensors |
| Flame Testers | Check flame | Height, shut-off |
| Pad & Screen Printers | Decorate bodies | Multi-colour |
| Packing Machines | Trays, cartons | Counting, shrink |
| Gas Storage & Transfer | Hold butane | Bullets, pumps |
| Test Lab Equipment | BIS testing | Drop, heat, pressure |
Machinery should follow the project plan. An assembly unit buys moulded bodies and parts and needs welders, semi-automatic assembly, a filling machine, leak and flame testing, and packing, while an integrated plant adds a bank of moulding machines with multi-cavity moulds, fully automatic assembly lines, and larger gas storage.
Cigarette Lighter Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for an integrated plant making about 150 million pieces a year in India. The final Cigarette Lighter Investment Cost for your project will depend on capacity, product mix, level of automation, in-house component making, gas storage, land cost, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Moulding & Moulds | 25–30% | Machines, moulds |
| Assembly Lines | 20–25% | Welders, assembly |
| Filling & Testing | 10–14% | Fillers, testers |
| Gas Storage & Safety | 6–10% | Bullets, detection |
| Land & Buildings | 15–20% | Plant, filling block |
| Pre-operatives & Working Capital | 6–10% | Stock, BIS, fees |
Moulding and assembly make up most of the capital, and gas safety systems are essential rather than optional. Because of this, a detailed Cigarette Lighter Business Plan should model resin, butane, and component prices, rejection rates by stage, line speeds and shifts, product mix, ex-factory prices and distributor margins, BIS and testing costs, export volumes, receivables, and financing costs together, so that funding supports the plant through ramp-up.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Materials & Components | 60–70% | Resin, gas, parts |
| Power & Utilities | 10–15% | Moulding load |
| Labour | 8–12% | Operators, testers |
| Packing & Freight | 4–6% | Cartons, transport |
| Maintenance & Moulds | 3–5% | Spares, upkeep |
| Overheads & Certification | 3–5% | BIS, insurance |
With materials making up most of the cost, margins depend on buying well, rejection rates, and line efficiency. A good operating model tracks material cost per thousand pieces, rejections by stage, gas loss, line uptime, and realised prices by channel, and tests results against higher resin or component prices, slower sales, or a tighter BIS audit.
Financial Analysis and Profitability
Based on analysis of a 150 million unit integrated plant, the financial profile combines moderate capital needs with healthy margins in a protected domestic market, though returns depend on component supply, automation, and distribution. The profitability of Cigarette Lighter manufacturing business in India improves markedly with in-house moulding, local component sourcing, high-speed automated lines, low rejection rates, a mix that includes electronic, refillable, and utility models, strong distribution, and exports.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 35–45% | Protected market |
| Net Profit Margin | 15–20% | After depreciation, taxes |
| Payback Period | 3–5 Years | Moderate capital |
| IRR (Internal Rate of Return) | 20–28% | Volume dependent |
| Capacity Utilization (stable ops) | 70–85% | After ramp-up |
| Break-even Capacity Utilization | 40–50% | Fixed line costs |
Distribution reach and rejection rates decide where a plant lands within these ranges. Plants with strong distributor networks and well-tuned automated lines earn the higher returns, while those relying on a few traders or semi-manual assembly sit at the lower end.
Returns can be strengthened by making valves and piezo units in-house, adding utility and refillable models, taking promotional and private label orders, exporting to Africa and the Gulf, and recycling moulding scrap.
Key Risks and Mitigation
The main risks are component shortages, gas fires, product recalls, price competition from other domestic producers, changes in trade rules, and distribution credit. Component risk is reduced by local suppliers and in-house making; fire risk by flameproof design and training; recall risk by inline testing and BIS discipline; price risk by automation and product mix; policy risk by building cost advantages that do not depend on import curbs; and credit risk by careful distributor selection. Promoters often work with a Cigarette Lighter Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for Cigarette Lighter Manufacturing in India
Approvals for a lighter plant centre on the BIS license, butane storage and filling, fire and factory safety, and environmental consents, along with labelling and standard business registrations. Promoters setting up a Cigarette Lighter Manufacturing Plant in India generally need the following:
- BIS License: Product certification to IS/ISO 9994 under the lighter Quality Control Order.
- Gas Storage: PESO license for butane storage, transfer, and filling.
- Pollution Control: Consent to Establish and Operate from the State Pollution Control Board.
- Factory & Fire: Factory license, building plan approval, and fire NOC.
- Packaging & Labelling: Legal Metrology registration and safety warnings.
- Export: Import Export Code and buyer-country safety certificates.
- Business & Trade Registrations: Business registration, GST, Udyam, and trademark.
The BIS license and PESO approval for gas storage are usually on the critical path, followed by fire safety and pollution consents.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, products, state pollution control categories, customer specifications, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Cigarette Lighter Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- Import ban: In June 2023, the DGFT prohibited imports of lighters with a CIF value below INR 20 per piece.
- Quality rules: In September 2024, the government amended the Quality Control Order requiring IS/ISO 9994 and the BIS mark.
- Parts curbs: In October 2024, the DGFT restricted imports of parts, which had reached USD 4.86 million in 2023-24.
- Premium segment: In January 2025, Zippo relaunched its Indian website with models priced at INR 2,000 to 10,000.
The common thread is a domestic market now reserved largely for local producers that meet BIS standards. Manufacturers who build local component supply, automated lines, and strong distribution will be best placed to grow.
How a Cigarette Lighter Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from market demand and product strategy to component sourcing, process design, plant layout, gas safety, approvals, and economics. It helps investors decide the right capacity, location, and product mix, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Cigarette Lighter Financial Model covering resin, gas, and component prices, rejection rates, line speeds, power, labour, packing and freight, maintenance, BIS and testing costs, distributor margins, working capital, depreciation, taxes, financing, debt servicing, cash flows, break-even, return on investment, and payback under different price and volume scenarios. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a Cigarette Lighter Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a lighter project, a strong DPR also clarifies the component sourcing plan, the level of automation, the product and channel mix, and the BIS and PESO approval path, which together are the factors most likely to decide success.
Frequently Asked Questions
What are the first steps to set up a cigarette lighter manufacturing plant in India?
Start by choosing your products and channels, such as disposables for retail or utility models for kitchens. Then commission a feasibility study and DPR, secure land with space for gas storage, line up component suppliers, choose moulding, assembly, and filling equipment, apply for BIS and PESO approvals, and arrange project financing.
How much does it cost to set up the cigarette lighter manufacturing plant in India?
Investment ranges from about INR 3–8 crore for an assembly unit making 20 to 50 million pieces a year to INR 35–55 crore for an integrated plant of about 150 million pieces, and INR 80–120 crore for plants above 300 million pieces.
What are the main steps in making cigarette lighter?
The flow runs from resin drying and injection moulding through ultrasonic welding, valve assembly, butane filling, leak testing, ignition assembly, flame testing, printing and labelling, and packing.
Which machinery does the cigarette lighter manufacturing plant need?
Key equipment includes injection moulding machines and multi-cavity moulds, ultrasonic welders, automated assembly lines, gas filling machines, leak and flame testers, pad and screen printers, packing machines, butane storage and transfer systems, and laboratory test equipment.
What raw materials are used for cigarette lighter manufacturing?
The main inputs are moulding resins, liquefied butane, valves, filters, springs, flints or piezo units, steel wheels and hoods, and packaging materials such as trays, cartons, and labels.
How profitable is cigarette lighter manufacturing in India?
IMARC estimates a 35 to 45% gross margin and a 15 to 20% net margin for a well-run plant, with payback in about 3 to 5 years. Profitability depends on component costs, rejection rates, automation, and distribution.
Which approvals does the cigarette lighter manufacturing plant need in India?
Typical approvals include a BIS license under the lighter Quality Control Order, a PESO license for butane, pollution board consents, factory license and fire NOC, Legal Metrology registration, and GST, Udyam, trademark, and Import Export Code registrations.
How do I get a feasibility study or DPR for the cigarette lighter manufacturing project?
A detailed feasibility study and DPR covers market and channels, component sourcing, process and automation, plant layout, gas safety, approvals, and full financials. Investors usually engage a Cigarette Lighter Manufacturing Feasibility Study Consultant with experience in consumer goods and plastics projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

The Saudi Arabia luxury apparel market has moved beyond the volume-led phase of its expansion. IMARC Group values the market at USD 752.2 Million in 2025, with a forecast of USD 1,102.8 Million by 2034, implying a CAGR of 4.34% during 2026-2034.
Cigarettes are composed of finely cut tobacco leaf rolled into a paper cylinder, often with a filter at one end. In India, the demand for domestic cigarette production has grown due to rising consumer markets and diminishing reliance on imports.
The Saudi Arabia kitchen chimney market is moving decisively upmarket, as households stop treating ventilation as a hidden utility and start specifying it as part of kitchen design, indoor air quality and resale value.
Faucets, also called taps or CP fittings, control the flow of water in kitchens, bathrooms, and commercial washrooms. Most quality faucets in India are made from brass that is forged or cast, precision machined, polished, and chrome plated, then fitted with ceramic disc cartridges, aerators, and handles, while lower-priced ranges use stainless steel, zinc, or plastic.
Toys range from moulded plastic figures, vehicles, and building blocks to ride-on cars, soft plush toys, educational and STEM kits, electronic and remote-controlled toys, board games, and puzzles.
The UK Furniture Market is experiencing a period of selective growth, where headline expansion masks significant divergence at the segment level. According to IMARC Group, the market was valued at USD 22.78 Billion in 2025 and is projected to reach USD 32.40 Billion by 2034, growing at a CAGR of 3.87% (2026–2034).
Fast moving consumer goods are everyday products that sell quickly at relatively low prices, such as detergents, dishwash products, surface cleaners, soaps, shampoos, toothpaste, packaged foods, and beverages.
Footwear covers sports shoes, sneakers, leather shoes, sandals, slippers, safety boots, and school shoes. India is the world's second-largest footwear producer, making about 2.9 billion pairs a year, or roughly 12.5% of global output, and its domestic market was valued at about USD 20.67 billion in 2025.
Washing powder is one of the most widely used household products in India, bought by almost every family for hand washing and, increasingly, for washing machines.
Energy meters measure the electricity used by every home, shop, factory, and farm connection, and they sit at the centre of India's effort to cut distribution losses and modernise its power sector.
Sanitary napkins are an essential hygiene product for hundreds of millions of women and girls in India, and one of the fastest-growing categories in personal care.
The Healthy Snacks Market has moved decisively from a niche wellness category to a mainstream pillar of the global food and beverage industry, driven by a fundamental and durable shift in how consumers around the world think about what they eat between meals.
India is one of the world's largest producers and consumers of textiles, and it generates around 7 million tonnes of textile waste every year, from cutting scraps and yarn waste in factories to old clothes and household textiles.
India has more than a billion mobile connections, creating a large and recurring market for chargers, cables, protective cases, screen guards, earbuds and other mobile accessories.
The television has quietly become the most connected screen in many Indian homes. Streaming apps, cricket in 4K, YouTube, and voice-controlled content have turned the TV into a smart device, and falling prices, a lower GST rate, and easy online buying have brought smart TVs within reach of millions of first-time buyers.
India is sleeping better, or at least spending more to try. Rising incomes, smaller urban homes, a booming hotel sector, and growing awareness of back health have pushed households away from cotton gaddas toward engineered foam, spring, and hybrid mattresses.
Setting up a Diaper Manufacturing Plant in India is a high-speed converting venture powered by rising hygiene awareness, growing disposable incomes, low current penetration, and expanding demand across baby and adult categories.
Setting up a Liquid Detergent Manufacturing Plant in India is a formulation-and-blending venture with relatively accessible entry capital, powered by rising hygiene awareness, a steady shift from powders to liquids, expanding modern retail, and growing demand across laundry, dishwash, and household cleaning categories.
Setting up a Kraft Paper Manufacturing Plant in India is a high-demand, sustainability-driven venture, powered by the country's booming e-commerce, packaging, and corrugated-box industries. Kraft paper is the base material for corrugated boxes and packaging, and demand is rising as businesses shift from plastic to recyclable paper-based packaging.
Setting up a Garment Manufacturing Plant in India is a high-demand, employment-generating venture, powered by the country's vast textile base, skilled workforce, and growing role as a global apparel sourcing hub.
The Luxury Fashion Market reached USD 261.0 Billion in 2025 and is projected to reach USD 341.0 Billion by 2034, growing at a CAGR of 3.02% (2026–2034).
Setting up a Container Manufacturing Plant in India is a capital-efficient, high-demand venture powered by the country's fast-growing food, pharmaceutical, FMCG, and industrial packaging sectors.
Bath soap is a body wash product developed primarily to provide personal care. It is made by the alkali saponification, a method that generates soap salts and glycerin in the soap via a reaction between fats or oils and an alkali, such as sodium hydroxide. Bath soaps are made by separating out dirt, sweat, excess oil and microorganisms while helping to remove dirt, sweat, excess oil and water soap from the skin to avoid dirt, extra oil and bacteria and viruses while preserving the balance of both cleansing the skin and compatibility between the application.
Waste tyre recycling can be defined as the organized collection, treatment, and recovery of end-of-life tyres (ELTs) to produce new materials, energy sources, or secondary raw materials. Tyres are made up of vulcanized rubber, steel reinforcement, textiles, and chemical compounds, making them non-biodegradable materials that cannot be easily decomposed.
Wallpaper is a decorative and practical wall covering material used to cover interior surfaces for aesthetic purposes, protection, and ambiance. It is usually made from paper, vinyl, non-woven fibers, textile backing, or a combination of materials, printed or embossed with designs, textures, or solid colors.
The Australian footwear industry is experiencing a remarkable transformation as it navigates a confluence of shifting consumer preferences, technological advancements, and sustainability imperatives.
Tennis ball production is the process of making standardized balls for the game of tennis. The process involves making balls with specific performance and bounce features. A tennis ball is made up of a hollow rubber core that is filled with pressurized air. The core is then covered with a woven felt material.
Soap is a type of cleaning agent made by the chemical reaction of fats or oils and an alkali in a process known as saponification. The chemical reaction transforms triglycerides into soap, also known as fatty acid salts, giving these substances the properties of a surfactant, allowing the substance to be used for the removal of dirt, oil, and bacteria from surfaces.
The size of the global hair oil market has undergone significant transformation with increasing consciousness among consumers to adopt hair care as part of their personal wellness, beyond the realm of mere beauty. Hair oils, being long considered one of the traditional grooming essentials, have transformed into complex formulations to suit various hair types and scalp conditions. Over the past years, lifestyle change, growing awareness related to scalp health, and the rising demand for natural beauty have significantly impacted the consumption pattern in the hair oil segment.
The global online grocery market research landscape has undergone unprecedented changes in recent years, with an upward trend marking the way consumers engage with food retail. There has been a significant expansion in the size of the online grocery market, fuelled by changing consumer preferences, technological advances, and increased convenience associated with digital shopping. Households are showing a growing reliance on online platforms for regular essentials more than ever, making the sector a cornerstone of modern retail.
The UAE’s pet food sector has emerged as one of the most dynamic and lifestyle-influenced consumer categories. While historically smaller and more niche compared to mainstream food and beverage markets, the industry has grown in relevance due to changing demographics, international influences, and shifting consumer priorities. Residents across major cities are embracing pets as companions for emotional well-being and as part of a balanced lifestyle.
The Saudi Arabia road freight transport market represents one of the key building blocks of the economic infrastructure in the Kingdom, providing for cargo movement across various domestic supply chains. It also involves road freight operations, which allow for the distribution of goods-from manufactured goods, consumer goods, and industrial supplies to agricultural produce-across its large and wide geography.
The Saudi Arabia luxury market represents one of the most dynamic and rapidly evolving segments within the Middle Eastern premium retail landscape. As the Kingdom undergoes comprehensive economic diversification and social transformation, luxury consumption patterns are experiencing unprecedented shifts that reflect changing demographics, evolving consumer preferences, and ambitious national development goals.
The Philippines retail sector has become a pluralistic and dynamic environment where old-fashioned stores coexist with high-tech contemporary formats enabled by digital strength. The Philippines retail sector market size reached USD 648.2 Billion in 2025. The market is projected to reach USD 1,223.1 Billion by 2034, exhibiting a growth rate (CAGR) of 7.31% during 2026-2034.
Polyester fabric is a type of synthetic fabric made from polyester fibers. The main source of polyester fibers is petrochemical polymers like polyethylene terephthalate. Polyester fabric is made from processing chips of polymers to produce continuous filaments and staple fibers. The processing of polymers involves heating and melting chips of polymers made from petrochemical materials to produce continuous filaments and staple fibers.
India's gaming industry is rapidly evolving into one of the largest and most dynamic markets in the world. Driven by the increasing adoption of smartphones, affordable internet, and a tech-savvy youth population, gaming is becoming a mainstream form of entertainment.
The beauty landscape in India is undergoing a major transformation propelled by creativity, research, and technology. The India cosmetics market size was valued at USD 15.46 Billion in 2025. Looking forward, the market is expected to reach USD 25.39 Billion by 2034, exhibiting a CAGR of 5.7% from 2026-2034.
The drivers for changing India's textile sector include sustainability, modernization of production, and the introduction of advanced chemical solutions. The India textile market size was valued at USD 152.40 Billion in 2025. The market is projected to reach USD 213.75 Billion by 2034, exhibiting a CAGR of 3.83% from 2026-2034. It places the India textile chemicals market at an important position in this evolution, enabling everything from fiber processing to finishing.
India's consumer landscape is experiencing a profound transformation, driven by rapid digital adoption, evolving consumer preferences, and robust infrastructure development. The shift from traditional brick-and-mortar shopping to digital platforms represents more than a mere change in purchasing channels—it signifies a fundamental restructuring of how businesses engage with consumers and how millions of Indians access goods and services.
The Saudi Arabia deodorants market size continues to evolve as consumers embrace modern grooming habits, premium personal care products, and innovative hygiene solutions. With rising awareness of body care, fragrance layering, and daily freshness, deodorants have become an essential part of both men’s and women’s personal grooming rituals.
Pet foods consist of commercially processed foods that contain nutritional requirements tailored according to their consumption by domesticated pets like dogs, cats, birds, fish, and small animals. The foods contain planned nutritional compositions, such as ingredients like protein, carbohydrate, fat, vitamins, and minerals.
Perfume is a scented liquid composition that contains a mixture of fragrance chemicals, essential oils, aroma chemicals, fixatives, and solvents that are formulated for a pleasing and distinct fragrance emission upon application on human skin or on objects.
Technological advancements and shifting consumer expectations have caused the worldwide washing machine industry to drastically change. Washing machines are becoming indispensable parts of contemporary homes, smoothly integrating into smart home ecosystems from conventional semi-automatic models to fully linked, smart appliances.
Paper plates are disposable food containers, also referred to as tableware, and are made mostly from paperboard, pulp, and materials that are derived from fibers. These plates are designed to be convenient, hygienic, and easy to handle while being moisture and grease-proof, making them ideal for packing different food varieties, ranging from dry foods to moist and greasy food items.
The GCC cigarette lighter market is undergoing a steady phase of expansion due to evolving consumer habits, sustained product demand, and widening distribution channels across the region. In 2024, the GCC cigarette lighter market was valued at USD 197 Million. A key factor shaping industry performance is the rise in convenience-led purchases, driven by widespread retail penetration, duty-free availability, and the continued popularity of smoking-related accessories.
Paint brushes are hand-operated applicator tools, designed and manufactured with great precision, utilizing the capabilities of these tools to apply, spread, and manage liquid paint, along with other forms of paint such as varnishes, stains, lacquers, and surface finishes, onto a desired surface. Paint brushes are commonly manufactured using a series of components, including a handle, a ferrule, and natural or man-made hairs, or a combination of these two. They are also manufactured and designed with different shapes and sizes, according to the viscosity and texture of the paint.
Pan masala is a ready-to-use chewing mixture that is traditionally used as a mouth freshener as well as a digestive aid and is of South Asian origin. It is prepared by mixing different components such as areca nut, catechu, slaked lime, spices, flavoring agents, sweet agents, and aroma agents in specific proportions. It is usually packed ready for use and is different from the betel quid variant that is prepared by using fresh betel leaves. Contemporary formulations of pan masala aim to achieve consistency, shelf life, and standardized flavor so that it can be mass-produced and marketed.
Paper bags can be defined as the final product made from paper-based material such as kraft paper, recycled paper, or specialty paper, used for packing or storing products. Paper bags come in different shapes and sizes with varying strength, ranging from flat-bottom paper bags, gusseted paper bags, and handled paper bags. Paper bags can be biodegradable, can be recycled, and can be made from renewable resources.
The Brazil cosmetics products market represents one of the most vibrant and diverse beauty sectors in Latin America, reflecting a deep-seated cultural emphasis on personal appearance, wellness, and self-care. The Brazilian consumer has long been known for a keen taste for grooming, fashion, and aesthetics, which logically applies to the cosmetics industry. Driven by an expanding middle-class population, an increase in urbanization, and increasing awareness about wellness-oriented lifestyles, the market continues to evolve.
The commercial landscape across the globe is undergoing a seismic shift, driven by technology, changing consumer expectations, and macroeconomic volatility. This transformation is particularly pronounced in high-density, globally connected urban centres like Singapore. Historically a powerhouse of trade and luxury commerce, the nation is now navigating an intricate matrix of digital disruption and soaring operational pressures.
The India confectionery industry has emerged as one of the most dynamic segments within the country's food and beverage sector. Driven by changing consumer preferences, rising disposable incomes, and evolving lifestyles, the market continues to witness remarkable transformation across urban and rural landscapes.
As disposable incomes rise, households are diversifying across investment-grade gold, diamond-studded jewellery, and designer ornaments. Gold, in particular, holds unmatched cultural and economic importance, sustaining demand even through economic fluctuations. Recent indicators show how this cultural attachment continues to translate into measurable investment momentum. Gold demand stood at 135 tonnes in Q2 2025, with a full-year forecast between 600 and 700 tonnes. By mid-2025, India’s total gold holdings reached 66.7 tonnes, with two tonnes added in June and nine tonnes in the first half of the year.
Mobile accessories encompass a wide range of auxiliary products that are intended to complement, protect, enhance, or extend the functional capabilities of smartphones and other portable communication devices. Examples of these accessories include protective cases, screen guards, chargers, power banks, earphones, wireless earbuds, smart wearables, mounts, portable speakers, and connectivity adapters. They enable better usability, device safety, personalization, convenience, and integration with digital ecosystems. Mobile accessories are made from a variety of materials and technologies to meet various performance, durability, and design requirements for different groups of users.
Japan boasts a long and rich culture of traditional board games such as Go and Shogi, which have long been a fundamental component of its culture. The current board game market in Japan, though, is a vibrant mix of these indigenous games and an incredibly diverse range of modern games based on both Western and domestic design schools.
The tobacco industry has long been a cornerstone in world trade and consumer culture, shaping the courses of economies, employment landscapes, and industrial practices for centuries. Even in today's world, with growing awareness regarding health and sustainability, tobacco remains an imposing force in global commerce.
The Australia sportswear industry is experiencing unprecedented momentum, transforming into a multi-billion-dollar powerhouse where fashion, fitness, and lifestyle converge. As health consciousness sweeps the continent and athleisure becomes a wardrobe staple, the Australian market leads a global revolution in performance apparel.
Japan's luxury apparel industry has traditionally been characterized by its profound respect for craftsmanship, quality, and cultural refinement. Japanese consumers have a reverence for art and nuance, preferring items that reflect precision and enduring design over short-lived trends. Over the past decade, Japanese luxury fashion has transcended conventional retailing experiences and assumed a contemporary identity that coalesces international influences with domestic sentiments.
A mattress is a cushioned structure intended to support the human body, either while sleeping, resting, or for therapeutic purposes. It is typically made up of comfort layers, including foam, latex, fiber, or gel, combined with a supportive core, like innerspring coils, high-density foam, or hybrid constructions. Mattresses are designed to evenly distribute body weight to relieve pressure points and ensure proper spinal alignment.
Liquid detergent is a formulated cleaning solution comprising surfactants, solvents, builders, enzymes, pH stabilizers, perfumes, and other additives, which are collectively used for removing dirt, stains, and oils from fabrics, dishes, and different surfaces. Unlike powdered detergents, liquid detergents dissolve immediately in water, allowing even distribution during washing and effective performance in both hot and cold water.
The Japan personal luxury goods industry stands as one of the world’s most crucial and dynamic markets, consistently ranking among the top three globally, alongside the United States and China. In 2024, Japan personal luxury goods market size reached USD 32,060.65 Million in 2024.
The luxury watch industry represents one of the most enduring segments of the global fashion and lifestyle market. Combining precision engineering with timeless craftsmanship, luxury watches continue to hold strong appeal among high-net-worth individuals, collectors, and aspirational consumers. The global luxury watch market size reached USD 29.12 Billion in 2024, reflecting steady growth driven by premiumization, rising consumer demand in emerging economies, and the enduring value of heritage timepieces.
The Vietnam athleisure market stands at a pivotal juncture, experiencing remarkable transformation driven by evolving lifestyles, rising health consciousness, and rapid urbanization. As Vietnamese people are increasingly prioritizing wellness and seeking versatile clothing that seamlessly transitions from gym workouts to casual social settings, the demand for activewear trends has surged dramatically. With lifestyle apparel Vietnam witnessing unprecedented growth and fitness clothing demand reaching new heights, both international brands and homegrown labels are competing vigorously to capture market share in this dynamic sector.
The Philippines conveyor belt market is picking up speed, powered by the country’s industrial growth and focus on automation. According to the IMARC Group, the market reached USD 31.23 Million in 2024, reflecting notable growth across manufacturing, mining, logistics, and food processing. As industries modernize, the need for efficient material handling systems is creating strong momentum for both domestic and imported conveyor solutions.
The US retail market is undergoing a profound transformation, fueled by the integration of artificial intelligence (AI) across multiple business operations. From personalized consumer engagement to predictive inventory management and dynamic pricing strategies, AI is redefining how retailers operate, compete, and deliver value. Increasing consumer expectations for seamless, personalized, and efficient shopping experiences are prompting businesses to embrace AI-driven solutions to optimize performance, reduce costs, and enhance decision-making.
The global beauty and personal care products market is undergoing a profound transformation, driven by technological innovation, evolving consumer expectations, and sustainability-focused practices. Increasing consumer awareness of health, wellness, and ethical sourcing is compelling companies to rethink traditional formulations and adopt advanced manufacturing techniques. Businesses are now integrating biotechnology, artificial intelligence, and data-driven insights into product development, distribution, and marketing strategies.
The Philippines board game market is on a winning streak, fueled by a growing passion for social play, learning, and creative pastimes. According to IMARC Group, the market reached USD 83.39 Million in 2024, reflecting how board gaming is becoming a favorite form of entertainment across generations. Family games, strategy and role-playing titles, and educational options for kids are gaining steady traction, alongside collectible and pop culture–inspired editions.
The Australian fantasy sports industry is entering a phase of heightened momentum, with market size for 2024 reaching approximately USD 810.6 Million, as detailed in a recent report. This market is forecast to grow to USD 2,180.2 Million by 2033, representing a compound annual growth rate (CAGR) of around 10.4 % from 2025 through 2033 .
Australia's textile recycling sector is experiencing a technological renaissance, with 40% of SMEs currently adopting artificial intelligence (AI), marking a 5% increase compared to the previous quarter (July-Sept 2024). The percentage of businesses unaware of how to utilize AI has decreased by 2% to 21%.
Containers are standardized, tough, watertight containers for efficient storage and transportation of goods by ship, rail, and truck without the need for handling the cargo itself. They are the lifeblood of global trade and logistics, allowing for effective intermodal transport. Constructed from high-strength steel, aluminum, or composite materials, they are designed to withstand rigorous marine and environmental elements. The most common types are dry storage containers for general cargo; however, there are also refrigerated (reefers) for perishables, tank containers for liquids and gases, open-top and flat-rack for oversized equipment, and high-cube for voluminous cargo. Standardization, mainly through ISO specifications, allows for seamless compatibility and efficiency throughout global logistics systems.
Carpet is a textile floor covering made of a pile, tufts of yarn or fiber, sewn to a backing for dimensional stability. Carpets are manufactured in various construction forms: tufted (universal across the world, yarn punched through a primary backing and treated with secondary backing), woven (Wilton and Axminster, highly valued for durability and pattern intricacy), needle-felt (bonded fibers for industrial applications), and knotted (hand-made rugs).
Aloe vera gel is a natural concentrate obtained from the parenchyma of the inner leaf of Aloe barbadensis miller, which is valued for its therapeutic, nutritional, and cosmetic uses. The gel mostly comprises water (more than 95%) and polysaccharides, vitamins, minerals, amino acids, enzymes, and antioxidants responsible for its soothing, moisturizing, and healing actions. Renowned for its anti-inflammatory, antimicrobial, and skin-rejuvenating properties, the aloe vera gel finds broad application in personal care cosmetics, pharmaceuticals, food supplements, and beverages.
Aloe vera is a perennial fleshy succulent plant of the species Aloe barbadensis miller, grown worldwide for its nutritional, medicinal, and cosmetic benefits. It has two primary constituents: the transparent inner gel consisting mainly of polysaccharides, vitamins, enzymes, and amino acids; and the yellowish latex, consisting of anthraquinones with powerful laxative properties. Aloe vera gel is highly prized for its emollient, moisturizing, and healing properties and is a common ingredient in skincare, personal care, and pharmaceutical products.
Air purifiers are appliances that enhance indoor air quality by eliminating pollutants like dust, allergens, smoke, volatile organic compounds (VOCs), and microbial particles. They work on various technologies such as HEPA (High-Efficiency Particulate Air) filters, activated carbon filters, UV-C light, ionizers, and photocatalytic oxidation. Their major components are usually fans or blowers, filter media, sensors, electronic controls, and metal or durable plastic housings. Some of the crucial characteristics of air purifiers include efficiency of filtration, airflow, noise levels, power consumption, and filter material durability.
Air coolers are evaporative coolers based on the principle of water evaporation, utilizing a fan or blower to blow cooled air, as opposed to air conditioners, which function based on refrigerant and compressor principles. Air coolers are designed to deliver low-cost and energy-efficient temperature management, mainly applicable to dry and hot climates. They generally consist of a pump, motor, cooling pads, water tank, blower/fan, and electronic control units. Main characteristics are low energy usage, environmental friendliness, portability, and low cost. Production of air coolers typically consists of combining sheet metal or plastic enclosures with motor-driven fans, water distribution networks, and cellulose or aspen cooling pads.
A4 paper, which is one of the most commonly used paper formats around the world, is 210 mm × 297 mm and forms the part of the ISO 216 system. It mainly consists of cellulose fibers obtained from wood pulp, recycled papers, or other fibrous raw materials like bagasse or bamboo. A4 paper contains crucial characteristics like smoothness, even thickness, high opacity, brightness, tensile strength, and durability, which enable it for printing, copying, and writing. The production process includes pulping raw fibers, bleaching for whiteness, refining for increasing fiber bonding, and sheet formation under regulated drying and calendaring.
The manufacturing sector is constantly changing with continuously rising demands for sustainability, innovation, and efficiency. The time comes when companies want to expand their business or venture into new markets.
India's manufacturing industry is experiencing a remarkable transformation and growth in 2025, aiming to establish the nation as a key player in global manufacturing. Supported by governmental initiatives such as the Make in India program and the Production Linked Incentive (PLI) schemes, the sector has drawn significant foreign direct investment (FDI) and encouraged innovation across multiple industries.
India's manufacturing industry is undergoing a turning point in 2025 based on strong government initiatives, a highly skilled and youthful population, and a worldwide trend towards diverse supply chains.
The global tobacco sector remains one of the most mature yet closely scrutinized industries in the world. With demand persisting across both developing and developed markets, cigarette production continues to be a high-volume, technically refined activity governed by extensive regulation and economic influence.
The global vegan cosmetics market is experiencing unprecedented growth, driven by a new wave of conscious consumers who demand beauty products that are not only effective, but also ethical, sustainable, and cruelty-free. This movement is more than just a passing trend; it's a fundamental shift in values that is reshaping the industry.
The global online grocery market has rapidly evolved from a convenience service to a mainstream retail segment, reshaping how consumers shop for everyday essentials. According to the IMARC group report, the market reached a value of USD 710.10 Billion in 2024 and is projected to witness consistent expansion.
The India textile market is picking up serious momentum, supported by smarter tech and changing user preferences. As more buyers look for eco-friendly, premium-quality products, manufacturers are stepping up with automation, digital tools, and flexible production systems.
The global toys market plays a crucial role as toys fundamentally support child development by fostering creativity, cognitive skills, and social interaction. In 2024, the global toys market was valued at USD 113.94 Billion.
The worldwide luxury watch market is poised for sustained growth, driven by rising affluence, aspirational lifestyle, and digital evolution. As consumers place greater importance on exclusivity and craftsmanship, demand for luxury watches is growing in developed as well as emerging markets.
Baby wipes are wet disposable wipes used to clean the tender skin of an infant, mostly when changing diapers. Composed of non-woven materials and embedded with delicate cleansing products, commonly made from water, mild surfactants, moisturizers such as aloe vera, and preservatives baby wipes are made to be delicate, hypoallergenic, and safe for daily use.
A tennis ball is a type of high-performance sporting ball used in both competitive and recreational tennis. On various court surfaces, its rubber core and felt covering provide the best bounce, speed, and durability. Both pressurised and non-pressurized tennis balls are available to accommodate different playing situations and ability levels. Under international regulations, they are crucial for competitions and training, and business expansion is being driven by sustainability and material innovation.
Caramel colour or E150d, is a common food and beverage colouring ingredient that is made by carefully heating food-grade carbohydrates with alkali or acid catalysts. Known as sulfite ammonia caramel, it gives baked items, sauces, soft drinks, and alcoholic beverages a rich brown colour. In food business, it is a preferred option because to its stability, solubility, and capacity to improve aesthetic appeal. Major food regulators across the world have authorised E150d and regulated it for safe consumption.
Kitchen appliances are a diverse category of electrical and mechanical devices that are essential in modern kitchens for various cooking and food preparation tasks. These appliances have revolutionized the way we prepare and cook food, making the process more efficient and convenient. For instance, refrigerators are crucial for storing perishable foods and keeping them fresh. Ovens and stoves are fundamental for baking, roasting, and cooking on open flames or electric coils. Microwaves provide quick heating, cooking, and defrosting, saving time in the kitchen. Dishwashers automate the often-tedious task of cleaning dishes, while blenders and food processors simplify chopping, pureeing, and blending ingredients.
A plastic cigarette lighter is a small portable hand-held device that gives a flame generally used for lighting cigarettes, cigars, candles, and other small things. They are mostly butane-gas fueled, which makes them easily disposable after all the fuel has been depleted. It's manufactured using polycarbonate or polypropylene plastic, so it's very lightweight and affordable.
Tissue paper, made from both virgin and recycled pulp, has become an essential part of daily life for cleaning, dusting, wrapping, and personal use. The industry's expansion is driven by luxurious tissue products, ultra-absorbent paper towels, and rising prices. Favorable factors such as growth in the IT sector, tourism, and MNCs, along with shifts in lifestyle and attitudes towards hygiene, cleanliness, and freshness, have boosted tissue consumption. Institutions like hospitals, malls, office complexes, and F&B chains are major consumers. Government support for sustainable practices has further spurred growth. West and South India are projected to be the largest consumers of tissues due to high foreign tourist influx, growing urbanization, and a hot climate that increases demand for disposable tissues.
While secondary research acts as the base of decision-making for businesses, primary research fills in the gaps that only a nuanced and personalized perspective can deliver. With enormous volumes of data being added daily on search engines, relying on obsolete and unauthentic data could cost businesses heavily. To stay ahead of the curve and make informed decisions, tapping directly into the information gathered through your customers is essential. This helps reveal the drivers of the decision-making process, unveiling unmet needs, and highlighting nascent trends before they take shape.
Consumer behavior mainly includes consumers’ mental, emotional, and behavioral responses toward the buying pattern of products. There are several factors that influence consumer behavior, such as personal, social, cultural, and psychological. Personal factors include the age, gender, and income of the consumer. Social factors like friends and family and cultural factors such as religion and tradition also play an important role in consumer buying patterns. Motivation, perception, and learning about goods and services change consumer preferences and fall under psychological factors.