Ceiling Fan Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
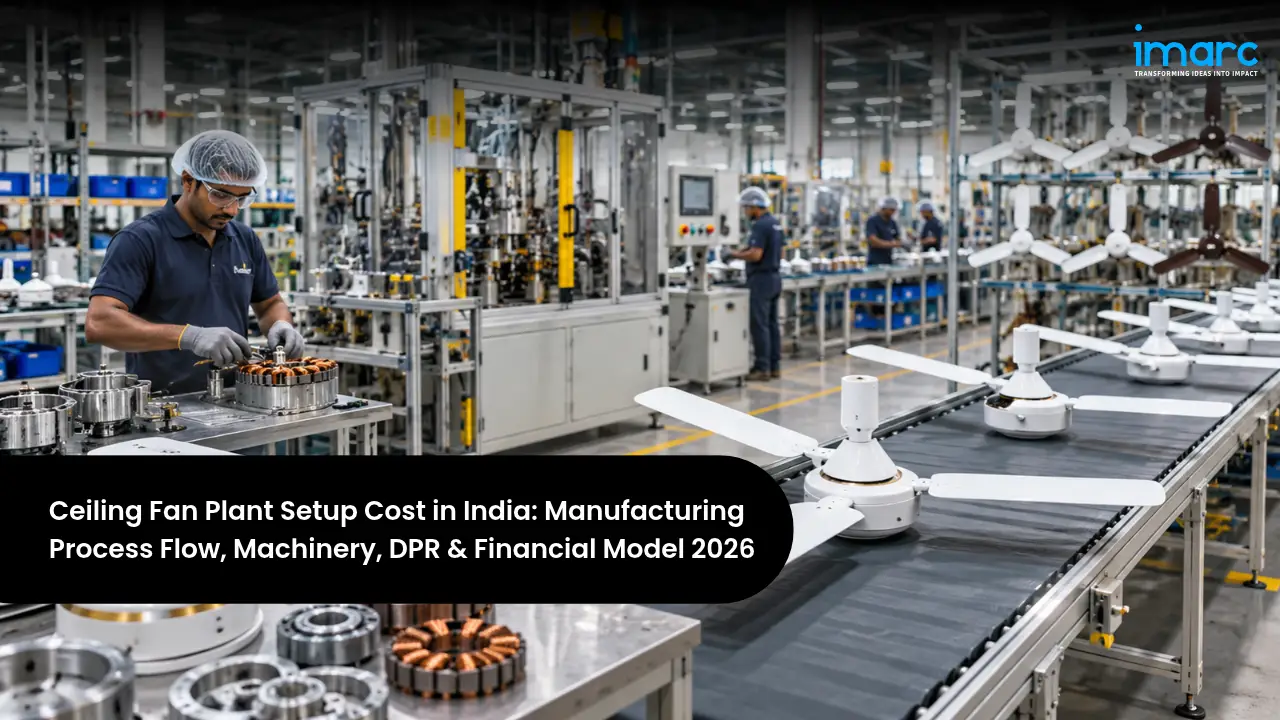
Setting up a Ceiling Fan Manufacturing Plant in India is a practical, demand-backed venture in one of the world's largest fan markets. Long summers across most of the country, steady housing construction, near-universal household electrification, and a regulatory push toward energy-efficient BLDC models keep demand both large and upgrading. A well-run unit converts copper wire, electrical steel, aluminium, and electronic components into finished, star-rated fans for homes, offices, and institutional buyers.
The total Ceiling Fan Manufacturing Plant Cost depends on capacity, the share of BLDC models in the mix, and how much of the motor is made in-house rather than bought out, with total investment for a typical unit ranging from INR 10 crore to INR 120 crore. Raw materials, led by copper, aluminium, electrical steel, and electronics, make up roughly two-thirds or more of operating costs, so metal procurement and motor efficiency are the decisions that shape margins most. At healthy capacity utilisation, a well-run Indian plant delivers a net profit margin of 6 to 12% and an IRR of 15 to 24%, with payback typically achieved within 3.5 to 5.5 years.
This guide is written for entrepreneurs and investors exploring how to start a ceiling fan manufacturing plant in India. It covers what the business involves, why demand keeps rising, the production flow, the machinery and raw materials required, location and infrastructure planning, a detailed cost and financial breakdown, the Licenses you must secure, and how a DPR turns all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| Primary Product Types | Induction, BLDC, decorative, and high-speed fans |
| Key Markets | Residential, commercial, institutional, and export |
| Demand Outlook | Steady volume growth with rapid BLDC upgrading |
| Indicative Total Investment | INR 10–120 Crore |
| Typical Payback Period | 3.5–5.5 Years |
The snapshot shows why the category draws steady investor interest: a huge installed base, near-universal household use, and a replacement cycle that regulation is now accelerating. The wide investment range reflects a real choice of scale and integration, from an assembly-led unit that buys castings and stampings to a fully integrated plant with its own stamping, die casting, winding, and powder coating. The rest of this guide unpacks that decision in detail.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Induction, BLDC, decorative, and high-speed fans |
| Total Project Investment | INR 10 – 120 Crore |
| Payback Period | 3.5 – 5.5 Years |
| Net Profit Margin | 6 – 12% |
| IRR | 15 – 24% |
| Best Locations | Uttarakhand, Uttar Pradesh, Gujarat, Tamil Nadu, West Bengal |
| Mandatory Approvals | BIS (IS 374), BEE Star Label, Factory License, SPCB, E-Waste EPR, Fire NOC |
| Key Requirement | Efficient motor design and in-house testing lab |
These indicative parameters give a realistic starting frame for early planning. Returns are attractive at scale, but they depend on controlling metal costs, designing motors that clear BEE star thresholds, and building distribution or OEM tie-ups that keep the line running through the year. A site-specific Ceiling Fan Feasibility Report tightens each of these numbers to your location, product mix, and capacity.
Table of Contents
- What is Ceiling Fan Manufacturing?
- Why is Ceiling Fan Manufacturing Growing in India?
- Ceiling Fan Manufacturing Process Flow
- Raw Materials Required for Ceiling Fan Manufacturing
- Location, Land & Infrastructure
- Ceiling Fan Manufacturing Machinery and Equipment
- Ceiling Fan Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Ceiling Fan Manufacturing in India
- Recent Developments in the India Ceiling Fan Manufacturing Industry
- How a Ceiling Fan Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Ceiling Fan Manufacturing?
Ceiling fan manufacturing is the production of electrically driven, ceiling-mounted fans by making or sourcing a motor, blades, and housing, then assembling, finishing, and testing them to meet performance and safety standards. A Ceiling Fan Manufacturing Plant typically carries out lamination stamping, aluminium die casting, stator winding, surface finishing, assembly, and air-delivery testing under one roof, although many units buy out some components and concentrate on motor building and assembly. The product is simple to use but engineering-sensitive, since air delivery, power draw, noise, and wobble all depend on motor and blade design.
From a business perspective, the appeal lies in scale and repeat demand. Almost every home, shop, classroom, and office in India uses ceiling fans, many rooms have more than one, and households typically replace or upgrade them every several years. A manufacturer offering star-rated, reliable fans at competitive prices can sell through dealers, modern retail, e-commerce, government procurement, and private-label contracts with established brands.
- Standard Induction Fans: The highest-volume segment, built around a capacitor-run induction motor and sold mainly on price and durability.
- BLDC Energy-Efficient Fans: Brushless DC motors with electronic drivers that draw far less power than conventional fans and dominate the top star bands.
- Decorative & Premium Fans: Designer finishes, wooden or ABS blades, integrated lights, and remote control aimed at urban and premium buyers.
- High-Speed & Commercial Fans: Larger sweeps and higher air delivery for shops, schools, factories, and institutions.
Main Product Categories in Ceiling Fan Production
Deciding which categories your plant will make is the foundational choice, because it drives motor design, tooling, and the level of investment required:
| Fan Type | Description | Key Property | Primary Demand |
|---|---|---|---|
| Standard Induction | Capacitor-run induction motor | Low cost, rugged | Mass residential and rural |
| BLDC | Brushless DC motor with driver board | High efficiency, remote control | Urban, star-conscious buyers |
| Decorative | Designer body and blade finishes | Aesthetics, lighting options | Premium homes, hospitality |
| High-Speed | Larger sweep, higher air delivery | Strong airflow | Commercial and institutional |
This choice shapes the factory floor. An induction-only line centres on stamping, die casting, winding, and varnishing, while a BLDC line adds driver electronics, magnets, and firmware, either assembled in-house on an SMT line or sourced from electronics suppliers. Many new entrants launch induction and BLDC ranges together, using induction for volume and BLDC for margin and star-rating compliance, then add decorative models once their distribution is in place.
Why is Ceiling Fan Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
India's ceiling fan industry is supported by structural factors that pair a vast installed base with a regulation-led shift toward efficient products. The market value is growing faster as the mix moves up the efficiency and design ladder:
- Climate and universal use: Long, hot summers make the ceiling fan the most widely owned cooling appliance in the country, running far more hours each year than air conditioners.
- Housing and electrification: New urban and rural housing, public housing programmes, and near-universal household electrification add millions of new fan points every year.
- Energy-efficiency regulation: Mandatory BEE star labelling and stricter rating tables are moving buyers from basic induction fans to BLDC models, creating a large upgrade cycle.
- Quality control and import substitution: The BIS Quality Control Order for ceiling fans bars uncertified products from the market and favours certified domestic manufacturing.
- Premiumisation and smart features: Rising incomes are lifting demand for decorative, remote-controlled, and app-connected fans at higher price points.
India-Specific Market Opportunity
| Segment | India Market Context | Manufacturing Role |
|---|---|---|
| Residential Replacement | Huge installed base of older fans | High-volume standard and BLDC supply |
| New Housing | Urban and rural construction | New fan points per dwelling |
| Energy-Efficient Upgrade | Star-rating driven shift | BLDC motors and drivers |
| Institutional & Government | Schools, offices, public tenders | Star-rated, tender-compliant volume |
| Private Label & OEM | Brands outsourcing production | Contract capacity for brand owners |
The strongest opening is a plant that makes efficient, certified fans at competitive cost and sells them through more than one channel. Contract manufacturing for established brands provides early volume and utilisation, while an own-brand range and government tenders add margin. Because regulation keeps raising efficiency expectations, a producer with solid BLDC capability is positioned on the right side of where the market is heading.
Ceiling Fan Manufacturing Process Flow
Understanding production helps you plan equipment, layout, and the main cost drivers. Fan making is a discrete engineering process in which metal parts are formed, the motor is built and wound, components are finished, and everything comes together on an assembly line that ends in performance testing. The sequence below reflects an integrated induction-motor plant; BLDC production follows the same flow with an added electronics stage.
Step-by-Step Ceiling Fan Manufacturing Process Flow
Electrical steel is first stamped and stacked into cores, aluminium parts are die cast and machined, the stator is wound and varnished, and blades and accessories are formed and coated before final assembly. A good layout keeps heavy metalworking separate from clean assembly and testing, because poor material flow raises both rejection rates and handling cost.
| Unit Operation | Key Activity |
|---|---|
| Lamination Stamping | Electrical steel stamped into stator and rotor laminations |
| Core Stacking | Laminations stacked and riveted into cores |
| Die Casting | Aluminium rotor cage and motor covers cast |
| Machining | Covers and shafts machined for bearing fits |
| Winding & Varnishing | Copper coils wound, inserted, and impregnated |
| Blade & Part Fabrication | Blades, downrods, and canopies formed |
| Surface Finishing | Pretreatment and powder coating of parts |
| Motor & Fan Assembly | Stator, rotor, bearings, capacitor or driver fitted |
| Testing & Balancing | Air delivery, power, safety, and balance checks |
| Packing & Dispatch | Cartoning and dispatch to dealers and customers |
Two factors decide profitability across this flow. First, motor quality governs everything the customer and regulator measure: lamination quality, winding precision, and air-gap control set the power draw and air delivery that fix a fan's star rating. Second, balancing and finishing protect brand reputation, since wobble, noise, and paint defects drive most warranty claims. For BLDC models, driver boards are assembled in-house or sourced, then programmed, fitted inside the motor, and tested for speed control and remote response. On every route, routine batch testing is what keeps BIS and BEE compliance intact.
Raw Materials Required for Ceiling Fan Manufacturing
The main inputs are copper winding wire, electrical steel, and aluminium, with electronics taking a larger share as the product mix moves toward BLDC. Because metals dominate cost and their prices follow global commodity markets, a reliable supplier network with sensible pricing arrangements is central to project planning.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Copper Winding Wire | Stator coils | Domestic wire manufacturers | 18–25% |
| Aluminium (ingot, sheet) | Die-cast body and blades | Domestic primary producers | 15–22% |
| CRNO Electrical Steel | Stator and rotor laminations | Domestic mills and imports | 10–15% |
| Electronics & Components | Capacitors, bearings, BLDC drivers | Domestic and imported | 12–20% |
| Powder, Paint & Packaging | Finishing and cartons | Domestic suppliers | 5–8% |
With metals making up such a large share of cost, procurement strategy is the biggest lever on profitability. Copper and aluminium prices track international benchmarks, so many manufacturers use price-linked contracts, hold buffer stock, and pass changes on to dealers with a lag. On the BLDC side, driver electronics and magnets still depend partly on imports, so qualifying more than one supplier protects both cost and continuity.
Location, Land & Infrastructure
Choosing the site is one of the first decisions in any Ceiling Fan Manufacturing Plant Setup in India, because it affects freight costs, labour availability, incentives, and proximity to component suppliers. Fans are bulky relative to their value and sold nationwide, so access to large consumption markets and an established electrical-goods supplier base usually matter more than being close to any single raw material.
Best Location for Ceiling Fan Manufacturing Plant Setup in India
| State | Why It Works | Key Advantage |
|---|---|---|
| Uttarakhand | Haridwar, Roorkee, and Rudrapur estates | Established electrical-goods cluster |
| Uttar Pradesh | Noida and Greater Noida in the NCR | Large market and component base |
| Gujarat | Strong engineering and metals base | Ports, power, and suppliers |
| Tamil Nadu | Chennai and Coimbatore motor ecosystem | Skilled labour and motor suppliers |
| West Bengal | Kolkata's long-standing fan industry | Experienced workforce, eastern market |
| Himachal Pradesh | Baddi industrial belt | Incentives and northern market access |
The strongest locations combine a large nearby market, a pool of skilled winders and machinists, ready component suppliers, and supportive state incentives. Uttarakhand and the NCR suit plants targeting North India, Tamil Nadu and Gujarat offer deep engineering ecosystems, and West Bengal brings decades of fan-making experience. Because freight on finished fans adds up quickly, many manufacturers choose a site close to their primary sales region and add a second plant or regional warehouse as they grow.
BIS, BEE and Quality Testing Requirements
Certification is not optional but foundational. Ceiling fans fall under the Electric Ceiling Type Fans (Quality Control) Order, 2023, so they cannot be manufactured, sold, or imported without a BIS License to IS 374:2019. BEE star labelling has also been mandatory since January 2023, with each model rated on its service value, the air delivered per watt consumed, and revised star tables now apply for the 2026 to 2028 labelling cycle. In practice, a plant needs an in-house laboratory with an air-delivery test chamber, power and speed measurement, high-voltage and insulation testers, and documented sampling procedures, along with accredited lab reports for every model it registers. Designing the motor to clear its target star band from the outset is far cheaper than reworking tooling after a model fails testing.
Infrastructure Requirements (Mid-Sized Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 8,000 – 20,000 sq. meters | Industrial estate or electrical cluster |
| Production Sheds | Stamping, casting, winding, assembly bays | Separate heavy and clean zones |
| Power Requirement | 500 kW – 1.5 MW | Die casting, presses, and ovens |
| Powder Coating Line | Conveyorised pretreatment and coating | Effluent handling for pretreatment |
| Testing Laboratory | Air-delivery chamber and testers | Needed for BIS and BEE compliance |
| Water & Effluent Treatment | Process water and ETP | For pretreatment and cooling |
| Warehousing | Raw material and finished-goods stores | Fans are bulky; plan generous space |
Infrastructure for a fan plant centres on robust power for die casting and presses, a well-designed powder coating line, and a credible testing laboratory. Finished fans occupy considerable space, so warehousing is easy to under-plan and often becomes a bottleneck before the summer peak, when dispatches surge. Building adequate shed, power, and storage capacity from the start supports seasonal scaling without disruption.
Ceiling Fan Manufacturing Machinery and Equipment
The equipment set spans metal forming, motor building, finishing, assembly, and testing, and the exact line-up depends on how vertically integrated the plant is. Machines must hold tight tolerances, since small variations in laminations or air gap translate directly into higher power draw. The core machinery for a fan unit, from stamping through final testing, is summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Power Press with Progressive Dies | Stamp stator and rotor laminations | High-speed precision tooling |
| High-Pressure Die Casting Machine | Cast rotor cage and motor covers | With melting and holding furnace |
| CNC Lathes and VMCs | Machine covers, shafts, bearing seats | Tight tolerance for low noise |
| Stator Winding Machine | Wind copper coils | Automatic, multi-spindle |
| Coil Inserting Machine | Insert and secure windings | Consistent slot fill |
| Varnish Impregnation System | Insulate and bond windings | With curing oven |
| Blade Forming Press Line | Blank, form, and twist blades | Repeatable blade pitch |
| Pretreatment & Powder Coating Plant | Finish covers, blades, canopies | Conveyorised with curing oven |
| Assembly Line with Dynamic Balancer | Assemble and balance fans | Conveyorised workstations |
| Air Delivery Chamber & Testers | Verify performance and safety | As per IS 374 test methods |
Equipment selection should follow your integration strategy rather than the other way around. An assembly-led unit can begin with winding, varnishing, assembly, and testing while buying castings and stampings, then add presses and die casting once volumes justify them. Testing equipment is the item most often under-budgeted, yet it is what protects star ratings, BIS License conditions, and warranty costs. Plants making BLDC fans should also budget for programming and end-of-line electronic testing, or a full SMT line if driver boards are made in-house.
Ceiling Fan Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down both the upfront capital investment and the ongoing operating costs, based on industry analysis of a mid-sized fan facility in India. The final Ceiling Fan Investment Cost for your project will depend on location, capacity, the BLDC share of output, and how much of the motor and components you make in-house.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Land, Building & Sheds | 18–28% | Land, civil works, and factory sheds |
| Plant & Machinery | 35–45% | Presses, die casting, winding, assembly |
| Tooling, Dies & Moulds | 6–10% | Lamination dies, casting and blade tools |
| Testing Lab & Quality Equipment | 3–6% | Air-delivery chamber and testers |
| Powder Coating, Utilities & ETP | 5–8% | Coating line, power, and effluent |
| Pre-operative & Contingency | 4–7% | Engineering, DPR, and buffer |
| Working Capital | 12–18% | Metal inventory and dealer credit |
Plant and machinery form the largest block, but tooling and working capital deserve equally close attention. Dies and moulds must be built for each motor and blade design, and the trade usually extends credit to dealers while metals are bought upfront, which ties up cash ahead of the summer season. These elements are modelled in detail in a Ceiling Fan Business Plan so that capacity and integration choices rest on realistic numbers.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials (metals, electronics) | 65–75% | Copper, aluminium, and steel dominate |
| Labour & Skilled Manpower | 6–9% | Winders, machinists, assembly staff |
| Warranty, Freight & Distribution | 6–10% | Bulky product and service network |
| Power & Utilities | 3–5% | Die casting and curing ovens |
| Maintenance & Overheads | 3–5% | Tooling upkeep and plant overheads |
| Quality, Testing & Certification | 1–3% | BIS, BEE, and in-house testing |
With raw materials dominating operating cost, this is fundamentally a metals-and-efficiency business. Margins move with copper and aluminium prices and with how much material each motor uses, so the model should track metal content per fan closely and stress-test returns against commodity swings. Warranty and freight are the next biggest levers, which is why build quality and plant location show up directly in profitability.
Financial Analysis and Profitability
Based on analysis of a mid-sized facility, the financial profile is sound, supported by large recurring demand, a regulation-driven upgrade cycle, and better margins on efficient models. The profitability of ceiling fan manufacturing business in India improves markedly with a higher BLDC share, efficient metal use, strong utilisation, and a blend of own-brand and contract volumes.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 22–32% | Higher with BLDC and decorative mix |
| Net Profit Margin | 6–12% | After depreciation and Indian corporate taxes |
| Payback Period | 3.5–5.5 Years | Faster with OEM contracts and own brand |
| IRR (Internal Rate of Return) | 15–24% | Higher for BLDC-led plants |
| Capacity Utilization (stable ops) | 70–85% | Seasonal peak before summer |
| Break-even Capacity Utilization | 45–60% | Contract volumes protect throughput |
Product mix and utilisation most determine outcomes. A plant selling only basic induction fans into a crowded, price-driven segment earns thin margins, while one with a strong BLDC and decorative range and steady OEM orders can run comfortably above break-even. Seasonality matters too: demand peaks in the months leading into summer, so planning production and inventory ahead of the season is part of the financial model, not an afterthought.
Returns can be strengthened in several ways: shifting the mix toward BLDC and premium models, signing private-label contracts to fill off-season capacity, reducing copper and aluminium content per fan through better motor design, bidding for government and institutional tenders, and running at high utilisation to spread fixed costs. Low warranty return rates further protect profitability.
Key Risks and Mitigation
The principal risks are metal price volatility, intense price competition from established brands, seasonality, and further tightening of efficiency norms. Metal risk is mitigated by price-linked contracts and buffer stock; competitive risk by OEM tie-ups, differentiated design, and a lean cost structure; seasonality by off-season contract work and export orders; and regulatory risk by building BLDC capability early. A manufacturer that treats procurement, motor design, and channel strategy as core priorities is far better placed to deliver the returns the model promises.
Licenses and Approvals for Ceiling Fan Manufacturing in India
Ceiling fans are a regulated electrical product, so certification is central to market access. Promoters planning a new unit generally need to obtain the following before commencing commercial sales, with BIS and BEE approvals being the most important:
- BIS Certification (ISI Mark): Product License to IS 374:2019 under the Electric Ceiling Type Fans (Quality Control) Order, 2023, including factory inspection and sample testing.
- BEE Star Labelling: Model-wise registration with the Bureau of Energy Efficiency, supported by accredited test reports, before fans can be sold.
- Factory License: Factory establishment and industrial operation approval under the Occupational Safety, Health and Working Conditions Code, 2020.
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board (CTE and CTO), covering die casting and powder coating.
- E-Waste EPR Registration: Registration on the CPCB portal under the E-Waste (Management) Rules, 2022, along with plastic packaging EPR where applicable.
- Business & Tax Registration: Company incorporation, GST registration, Udyam registration, Legal Metrology compliance, and an Import Export Code where needed.
- Fire Safety & Labour Registrations: Fire NOC, and employee welfare registrations such as EPF and ESI.
BIS and BEE approvals form the critical path and should run in parallel with plant construction, because neither can be completed without finished samples and a working test setup. Many first-time promoters engage a Ceiling Fan Manufacturing Consultant in India to sequence these approvals alongside tooling and trial runs, since a gap here can leave a completed plant unable to sell. Good sequencing can shave months off the launch timeline and help the plant catch its first summer season.
Note: The exact approvals, registrations, Licenses, and certification requirements may vary depending on factors such as plant location, product range, target markets, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Ceiling Fan Manufacturing Industry
A few structural trends give useful context for investors evaluating entry into this industry:
- Star-rating reset and BLDC shift: BEE's rescaled star tables, under which the earlier top-rated induction fans fell to the lowest band, and the revised tables for 2026 to 2028 are steadily moving the market toward BLDC motors.
- Quality control orders: Mandatory BIS certification for ceiling fans, with a quality control order for fan regulators also proposed, is curbing sub-standard imports and favouring certified domestic production.
- Smart and premium fans: Remote-controlled, app-connected, and designer fans are growing quickly, lifting realisations and rewarding manufacturers with electronics and design capability.
The common thread is a large, mature category that is being upgraded rather than simply expanded. For a new entrant, the implication is clear: plants built around efficient motor design, certified quality, and BLDC capability from day one will be best placed as norms tighten and buyers move up the value chain through the decade.
How a Ceiling Fan Manufacturing Project Report and DPR Helps Investors
A comprehensive DPR provides a structured roadmap for the facility by evaluating every aspect of the venture, from market demand and product mix to machinery selection, plant layout, and economics. It helps investors fix the right capacity and integration level, estimate capital expenditure (CapEx) and operating expenditure (OpEx), assess profitability, and flag risks before money is committed.
The report also contains a detailed Ceiling Fan Financial Model with revenue forecasts, production costs, cash flow projections, break-even analysis, return on investment (ROI), and payback calculations. These outputs let promoters, lenders, and partners judge long-term viability with confidence. Many investors bring in a Ceiling Fan Plant Project Report Consultant in India or a Ceiling Fan Manufacturing Feasibility Study Consultant to prepare and validate these documents for bank appraisal.
For a fan project specifically, a strong DPR also clarifies the induction-versus-BLDC strategy, the make-or-buy decision for stampings, castings, and electronics, the certification pathway, and the channel plan. By modelling seasonal utilisation against realistic demand and testing margins against metal price swings, the report turns a competitive but sizeable opportunity into an executable plan that lenders and partners can trust.
Frequently Asked Questions
How to start a ceiling fan manufacturing plant in India?
Start by choosing your product mix and capacity, then commission a feasibility study and DPR, secure land in an industrial estate, and arrange tooling, machinery, and component suppliers. Set up an in-house testing lab, run trial batches, and obtain BIS certification and BEE star labels before launching through dealers, e-commerce, or OEM contracts.
What is the ceiling fan manufacturing plant setup cost in India?
A typical project needs INR 10 crore to INR 120 crore, depending on capacity, BLDC share, and how much of the motor is made in-house. Plant and machinery form the largest CapEx item, followed by land and buildings and working capital.
What is the process flow for making ceiling fans?
The flow runs from lamination stamping and core stacking through aluminium die casting, machining, stator winding and varnishing, blade fabrication, powder coating, motor and fan assembly, testing and balancing, and finally packing and dispatch. BLDC fans add a driver-electronics stage.
What machinery is required for a ceiling fan manufacturing factory?
Key machines include a power press with lamination dies, a high-pressure die casting machine, CNC lathes, stator winding and coil inserting machines, a varnish impregnation system, a blade forming line, a powder coating plant, a conveyorised assembly line with dynamic balancing, and an air-delivery test chamber with electrical testers.
What raw materials are used to make ceiling fans?
The main materials are copper winding wire, aluminium for the die-cast body and blades, and CRNO electrical steel for the motor laminations. Capacitors, bearings, BLDC driver boards, powder coating, and packaging make up the rest.
Is ceiling fan manufacturing profitable in India?
Yes. At healthy utilisation, a mid-sized plant typically earns a 6 to 12% net margin and a 15 to 24% IRR, with payback in 3.5 to 5.5 years. Returns improve with a higher BLDC share, efficient metal use, and steady OEM or tender volumes, though margins track copper and aluminium prices.
What licenses are needed for a ceiling fan manufacturing plant in India?
A plant needs BIS certification to IS 374:2019, BEE star label registration for each model, a Factory License, State Pollution Control Board consents, E-Waste EPR registration, a Fire NOC, and GST, Udyam, and labour registrations.
Which state is best for setting up a ceiling fan manufacturing factory?
Uttarakhand, Uttar Pradesh, Gujarat, Tamil Nadu, and West Bengal are popular choices for their markets, supplier bases, and skilled workforce. The right site depends on your target sales region, incentive eligibility, and freight costs.
How do I get a feasibility study or DPR for a ceiling fan manufacturing plant?
A professionally prepared DPR covers market assessment, technical design, costs, and financial projections suitable for bank appraisal. Many promoters work with a Ceiling Fan Business Plan Consultant in India to prepare it and align it with lender and subsidy requirements.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Adult incontinence products, such as pant-style and tape-style diapers, underpads, and insert pads, are absorbent hygiene products made from fluff pulp and super absorbent polymer wrapped between soft nonwoven fabrics and a leak-proof backsheet, with elastics and fasteners for a secure fit.
The product is a dry, ready-to-chew blend of cut and processed areca nut with catechu, slaked lime, cardamom, flavours, and sweeteners, sold in small pouches, tins, and jars as an after-meal mouth freshener across India.
Male latex contraceptives are thin sheaths made by dipping glass formers into compounded natural rubber latex, curing the film in ovens, stripping and washing the pieces, and then testing every single one electronically for holes before lubricating and sealing it in foil.
Disposable paperboard plates are pressed from food-grade board, often laminated with silver foil paper or coated for grease and moisture resistance, and are used at weddings, festivals, religious gatherings, street food stalls, canteens, caterers, quick-service restaurants, and homes.
The US handicrafts market has moved from the margins of the hobby and gift economy into one of the more resilient corners of American consumer spending. According to IMARC Group, the market stood at USD 345.24 Billion in 2025, rose to USD 372.05 Billion in 2026, and is projected to reach USD 676.82 Billion by 2034, expanding at a CAGR of 7.77% during 2026-2034.
A pocket lighter is a small plastic or metal reservoir of liquefied butane fitted with a valve, a flame adjuster, and an ignition system, either a steel wheel striking a flint or a piezoelectric spark, that releases and lights a controlled flame at the press of a button.
The Saudi Arabia luxury apparel market has moved beyond the volume-led phase of its expansion. IMARC Group values the market at USD 752.2 Million in 2025, with a forecast of USD 1,102.8 Million by 2034, implying a CAGR of 4.34% during 2026-2034.
Cigarettes are composed of finely cut tobacco leaf rolled into a paper cylinder, often with a filter at one end. In India, the demand for domestic cigarette production has grown due to rising consumer markets and diminishing reliance on imports.
The Saudi Arabia kitchen chimney market is moving decisively upmarket, as households stop treating ventilation as a hidden utility and start specifying it as part of kitchen design, indoor air quality and resale value.
Faucets, also called taps or CP fittings, control the flow of water in kitchens, bathrooms, and commercial washrooms. Most quality faucets in India are made from brass that is forged or cast, precision machined, polished, and chrome plated, then fitted with ceramic disc cartridges, aerators, and handles, while lower-priced ranges use stainless steel, zinc, or plastic.
Toys range from moulded plastic figures, vehicles, and building blocks to ride-on cars, soft plush toys, educational and STEM kits, electronic and remote-controlled toys, board games, and puzzles.
The UK Furniture Market is experiencing a period of selective growth, where headline expansion masks significant divergence at the segment level. According to IMARC Group, the market was valued at USD 22.78 Billion in 2025 and is projected to reach USD 32.40 Billion by 2034, growing at a CAGR of 3.87% (2026–2034).
Fast moving consumer goods are everyday products that sell quickly at relatively low prices, such as detergents, dishwash products, surface cleaners, soaps, shampoos, toothpaste, packaged foods, and beverages.
Footwear covers sports shoes, sneakers, leather shoes, sandals, slippers, safety boots, and school shoes. India is the world's second-largest footwear producer, making about 2.9 billion pairs a year, or roughly 12.5% of global output, and its domestic market was valued at about USD 20.67 billion in 2025.
Washing powder is one of the most widely used household products in India, bought by almost every family for hand washing and, increasingly, for washing machines.
Energy meters measure the electricity used by every home, shop, factory, and farm connection, and they sit at the centre of India's effort to cut distribution losses and modernise its power sector.
Sanitary napkins are an essential hygiene product for hundreds of millions of women and girls in India, and one of the fastest-growing categories in personal care.
The Healthy Snacks Market has moved decisively from a niche wellness category to a mainstream pillar of the global food and beverage industry, driven by a fundamental and durable shift in how consumers around the world think about what they eat between meals.
India is one of the world's largest producers and consumers of textiles, and it generates around 7 million tonnes of textile waste every year, from cutting scraps and yarn waste in factories to old clothes and household textiles.
India has more than a billion mobile connections, creating a large and recurring market for chargers, cables, protective cases, screen guards, earbuds and other mobile accessories.
The television has quietly become the most connected screen in many Indian homes. Streaming apps, cricket in 4K, YouTube, and voice-controlled content have turned the TV into a smart device, and falling prices, a lower GST rate, and easy online buying have brought smart TVs within reach of millions of first-time buyers.
India is sleeping better, or at least spending more to try. Rising incomes, smaller urban homes, a booming hotel sector, and growing awareness of back health have pushed households away from cotton gaddas toward engineered foam, spring, and hybrid mattresses.
Setting up a Diaper Manufacturing Plant in India is a high-speed converting venture powered by rising hygiene awareness, growing disposable incomes, low current penetration, and expanding demand across baby and adult categories.
Setting up a Liquid Detergent Manufacturing Plant in India is a formulation-and-blending venture with relatively accessible entry capital, powered by rising hygiene awareness, a steady shift from powders to liquids, expanding modern retail, and growing demand across laundry, dishwash, and household cleaning categories.
Setting up a Kraft Paper Manufacturing Plant in India is a high-demand, sustainability-driven venture, powered by the country's booming e-commerce, packaging, and corrugated-box industries. Kraft paper is the base material for corrugated boxes and packaging, and demand is rising as businesses shift from plastic to recyclable paper-based packaging.
Setting up a Garment Manufacturing Plant in India is a high-demand, employment-generating venture, powered by the country's vast textile base, skilled workforce, and growing role as a global apparel sourcing hub.
The Luxury Fashion Market reached USD 261.0 Billion in 2025 and is projected to reach USD 341.0 Billion by 2034, growing at a CAGR of 3.02% (2026–2034).
Setting up a Container Manufacturing Plant in India is a capital-efficient, high-demand venture powered by the country's fast-growing food, pharmaceutical, FMCG, and industrial packaging sectors.
Bath soap is a body wash product developed primarily to provide personal care. It is made by the alkali saponification, a method that generates soap salts and glycerin in the soap via a reaction between fats or oils and an alkali, such as sodium hydroxide. Bath soaps are made by separating out dirt, sweat, excess oil and microorganisms while helping to remove dirt, sweat, excess oil and water soap from the skin to avoid dirt, extra oil and bacteria and viruses while preserving the balance of both cleansing the skin and compatibility between the application.
Waste tyre recycling can be defined as the organized collection, treatment, and recovery of end-of-life tyres (ELTs) to produce new materials, energy sources, or secondary raw materials. Tyres are made up of vulcanized rubber, steel reinforcement, textiles, and chemical compounds, making them non-biodegradable materials that cannot be easily decomposed.
Wallpaper is a decorative and practical wall covering material used to cover interior surfaces for aesthetic purposes, protection, and ambiance. It is usually made from paper, vinyl, non-woven fibers, textile backing, or a combination of materials, printed or embossed with designs, textures, or solid colors.
The Australian footwear industry is experiencing a remarkable transformation as it navigates a confluence of shifting consumer preferences, technological advancements, and sustainability imperatives.
Tennis ball production is the process of making standardized balls for the game of tennis. The process involves making balls with specific performance and bounce features. A tennis ball is made up of a hollow rubber core that is filled with pressurized air. The core is then covered with a woven felt material.
Soap is a type of cleaning agent made by the chemical reaction of fats or oils and an alkali in a process known as saponification. The chemical reaction transforms triglycerides into soap, also known as fatty acid salts, giving these substances the properties of a surfactant, allowing the substance to be used for the removal of dirt, oil, and bacteria from surfaces.
The size of the global hair oil market has undergone significant transformation with increasing consciousness among consumers to adopt hair care as part of their personal wellness, beyond the realm of mere beauty. Hair oils, being long considered one of the traditional grooming essentials, have transformed into complex formulations to suit various hair types and scalp conditions. Over the past years, lifestyle change, growing awareness related to scalp health, and the rising demand for natural beauty have significantly impacted the consumption pattern in the hair oil segment.
The global online grocery market research landscape has undergone unprecedented changes in recent years, with an upward trend marking the way consumers engage with food retail. There has been a significant expansion in the size of the online grocery market, fuelled by changing consumer preferences, technological advances, and increased convenience associated with digital shopping. Households are showing a growing reliance on online platforms for regular essentials more than ever, making the sector a cornerstone of modern retail.
The UAE’s pet food sector has emerged as one of the most dynamic and lifestyle-influenced consumer categories. While historically smaller and more niche compared to mainstream food and beverage markets, the industry has grown in relevance due to changing demographics, international influences, and shifting consumer priorities. Residents across major cities are embracing pets as companions for emotional well-being and as part of a balanced lifestyle.
The Saudi Arabia road freight transport market represents one of the key building blocks of the economic infrastructure in the Kingdom, providing for cargo movement across various domestic supply chains. It also involves road freight operations, which allow for the distribution of goods-from manufactured goods, consumer goods, and industrial supplies to agricultural produce-across its large and wide geography.
The Saudi Arabia luxury market represents one of the most dynamic and rapidly evolving segments within the Middle Eastern premium retail landscape. As the Kingdom undergoes comprehensive economic diversification and social transformation, luxury consumption patterns are experiencing unprecedented shifts that reflect changing demographics, evolving consumer preferences, and ambitious national development goals.
The Philippines retail sector has become a pluralistic and dynamic environment where old-fashioned stores coexist with high-tech contemporary formats enabled by digital strength. The Philippines retail sector market size reached USD 648.2 Billion in 2025. The market is projected to reach USD 1,223.1 Billion by 2034, exhibiting a growth rate (CAGR) of 7.31% during 2026-2034.
Polyester fabric is a type of synthetic fabric made from polyester fibers. The main source of polyester fibers is petrochemical polymers like polyethylene terephthalate. Polyester fabric is made from processing chips of polymers to produce continuous filaments and staple fibers. The processing of polymers involves heating and melting chips of polymers made from petrochemical materials to produce continuous filaments and staple fibers.
India's gaming industry is rapidly evolving into one of the largest and most dynamic markets in the world. Driven by the increasing adoption of smartphones, affordable internet, and a tech-savvy youth population, gaming is becoming a mainstream form of entertainment.
The beauty landscape in India is undergoing a major transformation propelled by creativity, research, and technology. The India cosmetics market size was valued at USD 15.46 Billion in 2025. Looking forward, the market is expected to reach USD 25.39 Billion by 2034, exhibiting a CAGR of 5.7% from 2026-2034.
The drivers for changing India's textile sector include sustainability, modernization of production, and the introduction of advanced chemical solutions. The India textile market size was valued at USD 152.40 Billion in 2025. The market is projected to reach USD 213.75 Billion by 2034, exhibiting a CAGR of 3.83% from 2026-2034. It places the India textile chemicals market at an important position in this evolution, enabling everything from fiber processing to finishing.
India's consumer landscape is experiencing a profound transformation, driven by rapid digital adoption, evolving consumer preferences, and robust infrastructure development. The shift from traditional brick-and-mortar shopping to digital platforms represents more than a mere change in purchasing channels—it signifies a fundamental restructuring of how businesses engage with consumers and how millions of Indians access goods and services.
The Saudi Arabia deodorants market size continues to evolve as consumers embrace modern grooming habits, premium personal care products, and innovative hygiene solutions. With rising awareness of body care, fragrance layering, and daily freshness, deodorants have become an essential part of both men’s and women’s personal grooming rituals.
Pet foods consist of commercially processed foods that contain nutritional requirements tailored according to their consumption by domesticated pets like dogs, cats, birds, fish, and small animals. The foods contain planned nutritional compositions, such as ingredients like protein, carbohydrate, fat, vitamins, and minerals.
Perfume is a scented liquid composition that contains a mixture of fragrance chemicals, essential oils, aroma chemicals, fixatives, and solvents that are formulated for a pleasing and distinct fragrance emission upon application on human skin or on objects.
Technological advancements and shifting consumer expectations have caused the worldwide washing machine industry to drastically change. Washing machines are becoming indispensable parts of contemporary homes, smoothly integrating into smart home ecosystems from conventional semi-automatic models to fully linked, smart appliances.
Paper plates are disposable food containers, also referred to as tableware, and are made mostly from paperboard, pulp, and materials that are derived from fibers. These plates are designed to be convenient, hygienic, and easy to handle while being moisture and grease-proof, making them ideal for packing different food varieties, ranging from dry foods to moist and greasy food items.
The GCC cigarette lighter market is undergoing a steady phase of expansion due to evolving consumer habits, sustained product demand, and widening distribution channels across the region. In 2024, the GCC cigarette lighter market was valued at USD 197 Million. A key factor shaping industry performance is the rise in convenience-led purchases, driven by widespread retail penetration, duty-free availability, and the continued popularity of smoking-related accessories.
Paint brushes are hand-operated applicator tools, designed and manufactured with great precision, utilizing the capabilities of these tools to apply, spread, and manage liquid paint, along with other forms of paint such as varnishes, stains, lacquers, and surface finishes, onto a desired surface. Paint brushes are commonly manufactured using a series of components, including a handle, a ferrule, and natural or man-made hairs, or a combination of these two. They are also manufactured and designed with different shapes and sizes, according to the viscosity and texture of the paint.
Pan masala is a ready-to-use chewing mixture that is traditionally used as a mouth freshener as well as a digestive aid and is of South Asian origin. It is prepared by mixing different components such as areca nut, catechu, slaked lime, spices, flavoring agents, sweet agents, and aroma agents in specific proportions. It is usually packed ready for use and is different from the betel quid variant that is prepared by using fresh betel leaves. Contemporary formulations of pan masala aim to achieve consistency, shelf life, and standardized flavor so that it can be mass-produced and marketed.
Paper bags can be defined as the final product made from paper-based material such as kraft paper, recycled paper, or specialty paper, used for packing or storing products. Paper bags come in different shapes and sizes with varying strength, ranging from flat-bottom paper bags, gusseted paper bags, and handled paper bags. Paper bags can be biodegradable, can be recycled, and can be made from renewable resources.
The Brazil cosmetics products market represents one of the most vibrant and diverse beauty sectors in Latin America, reflecting a deep-seated cultural emphasis on personal appearance, wellness, and self-care. The Brazilian consumer has long been known for a keen taste for grooming, fashion, and aesthetics, which logically applies to the cosmetics industry. Driven by an expanding middle-class population, an increase in urbanization, and increasing awareness about wellness-oriented lifestyles, the market continues to evolve.
The commercial landscape across the globe is undergoing a seismic shift, driven by technology, changing consumer expectations, and macroeconomic volatility. This transformation is particularly pronounced in high-density, globally connected urban centres like Singapore. Historically a powerhouse of trade and luxury commerce, the nation is now navigating an intricate matrix of digital disruption and soaring operational pressures.
The India confectionery industry has emerged as one of the most dynamic segments within the country's food and beverage sector. Driven by changing consumer preferences, rising disposable incomes, and evolving lifestyles, the market continues to witness remarkable transformation across urban and rural landscapes.
As disposable incomes rise, households are diversifying across investment-grade gold, diamond-studded jewellery, and designer ornaments. Gold, in particular, holds unmatched cultural and economic importance, sustaining demand even through economic fluctuations. Recent indicators show how this cultural attachment continues to translate into measurable investment momentum. Gold demand stood at 135 tonnes in Q2 2025, with a full-year forecast between 600 and 700 tonnes. By mid-2025, India’s total gold holdings reached 66.7 tonnes, with two tonnes added in June and nine tonnes in the first half of the year.
Mobile accessories encompass a wide range of auxiliary products that are intended to complement, protect, enhance, or extend the functional capabilities of smartphones and other portable communication devices. Examples of these accessories include protective cases, screen guards, chargers, power banks, earphones, wireless earbuds, smart wearables, mounts, portable speakers, and connectivity adapters. They enable better usability, device safety, personalization, convenience, and integration with digital ecosystems. Mobile accessories are made from a variety of materials and technologies to meet various performance, durability, and design requirements for different groups of users.
Japan boasts a long and rich culture of traditional board games such as Go and Shogi, which have long been a fundamental component of its culture. The current board game market in Japan, though, is a vibrant mix of these indigenous games and an incredibly diverse range of modern games based on both Western and domestic design schools.
The tobacco industry has long been a cornerstone in world trade and consumer culture, shaping the courses of economies, employment landscapes, and industrial practices for centuries. Even in today's world, with growing awareness regarding health and sustainability, tobacco remains an imposing force in global commerce.
The Australia sportswear industry is experiencing unprecedented momentum, transforming into a multi-billion-dollar powerhouse where fashion, fitness, and lifestyle converge. As health consciousness sweeps the continent and athleisure becomes a wardrobe staple, the Australian market leads a global revolution in performance apparel.
Japan's luxury apparel industry has traditionally been characterized by its profound respect for craftsmanship, quality, and cultural refinement. Japanese consumers have a reverence for art and nuance, preferring items that reflect precision and enduring design over short-lived trends. Over the past decade, Japanese luxury fashion has transcended conventional retailing experiences and assumed a contemporary identity that coalesces international influences with domestic sentiments.
A mattress is a cushioned structure intended to support the human body, either while sleeping, resting, or for therapeutic purposes. It is typically made up of comfort layers, including foam, latex, fiber, or gel, combined with a supportive core, like innerspring coils, high-density foam, or hybrid constructions. Mattresses are designed to evenly distribute body weight to relieve pressure points and ensure proper spinal alignment.
Liquid detergent is a formulated cleaning solution comprising surfactants, solvents, builders, enzymes, pH stabilizers, perfumes, and other additives, which are collectively used for removing dirt, stains, and oils from fabrics, dishes, and different surfaces. Unlike powdered detergents, liquid detergents dissolve immediately in water, allowing even distribution during washing and effective performance in both hot and cold water.
The Japan personal luxury goods industry stands as one of the world’s most crucial and dynamic markets, consistently ranking among the top three globally, alongside the United States and China. In 2024, Japan personal luxury goods market size reached USD 32,060.65 Million in 2024.
The luxury watch industry represents one of the most enduring segments of the global fashion and lifestyle market. Combining precision engineering with timeless craftsmanship, luxury watches continue to hold strong appeal among high-net-worth individuals, collectors, and aspirational consumers. The global luxury watch market size reached USD 29.12 Billion in 2024, reflecting steady growth driven by premiumization, rising consumer demand in emerging economies, and the enduring value of heritage timepieces.
The Vietnam athleisure market stands at a pivotal juncture, experiencing remarkable transformation driven by evolving lifestyles, rising health consciousness, and rapid urbanization. As Vietnamese people are increasingly prioritizing wellness and seeking versatile clothing that seamlessly transitions from gym workouts to casual social settings, the demand for activewear trends has surged dramatically. With lifestyle apparel Vietnam witnessing unprecedented growth and fitness clothing demand reaching new heights, both international brands and homegrown labels are competing vigorously to capture market share in this dynamic sector.
The Philippines conveyor belt market is picking up speed, powered by the country’s industrial growth and focus on automation. According to the IMARC Group, the market reached USD 31.23 Million in 2024, reflecting notable growth across manufacturing, mining, logistics, and food processing. As industries modernize, the need for efficient material handling systems is creating strong momentum for both domestic and imported conveyor solutions.
The US retail market is undergoing a profound transformation, fueled by the integration of artificial intelligence (AI) across multiple business operations. From personalized consumer engagement to predictive inventory management and dynamic pricing strategies, AI is redefining how retailers operate, compete, and deliver value. Increasing consumer expectations for seamless, personalized, and efficient shopping experiences are prompting businesses to embrace AI-driven solutions to optimize performance, reduce costs, and enhance decision-making.
The global beauty and personal care products market is undergoing a profound transformation, driven by technological innovation, evolving consumer expectations, and sustainability-focused practices. Increasing consumer awareness of health, wellness, and ethical sourcing is compelling companies to rethink traditional formulations and adopt advanced manufacturing techniques. Businesses are now integrating biotechnology, artificial intelligence, and data-driven insights into product development, distribution, and marketing strategies.
The Philippines board game market is on a winning streak, fueled by a growing passion for social play, learning, and creative pastimes. According to IMARC Group, the market reached USD 83.39 Million in 2024, reflecting how board gaming is becoming a favorite form of entertainment across generations. Family games, strategy and role-playing titles, and educational options for kids are gaining steady traction, alongside collectible and pop culture–inspired editions.
The Australian fantasy sports industry is entering a phase of heightened momentum, with market size for 2024 reaching approximately USD 810.6 Million, as detailed in a recent report. This market is forecast to grow to USD 2,180.2 Million by 2033, representing a compound annual growth rate (CAGR) of around 10.4 % from 2025 through 2033 .
Australia's textile recycling sector is experiencing a technological renaissance, with 40% of SMEs currently adopting artificial intelligence (AI), marking a 5% increase compared to the previous quarter (July-Sept 2024). The percentage of businesses unaware of how to utilize AI has decreased by 2% to 21%.
Containers are standardized, tough, watertight containers for efficient storage and transportation of goods by ship, rail, and truck without the need for handling the cargo itself. They are the lifeblood of global trade and logistics, allowing for effective intermodal transport. Constructed from high-strength steel, aluminum, or composite materials, they are designed to withstand rigorous marine and environmental elements. The most common types are dry storage containers for general cargo; however, there are also refrigerated (reefers) for perishables, tank containers for liquids and gases, open-top and flat-rack for oversized equipment, and high-cube for voluminous cargo. Standardization, mainly through ISO specifications, allows for seamless compatibility and efficiency throughout global logistics systems.
Carpet is a textile floor covering made of a pile, tufts of yarn or fiber, sewn to a backing for dimensional stability. Carpets are manufactured in various construction forms: tufted (universal across the world, yarn punched through a primary backing and treated with secondary backing), woven (Wilton and Axminster, highly valued for durability and pattern intricacy), needle-felt (bonded fibers for industrial applications), and knotted (hand-made rugs).
Aloe vera gel is a natural concentrate obtained from the parenchyma of the inner leaf of Aloe barbadensis miller, which is valued for its therapeutic, nutritional, and cosmetic uses. The gel mostly comprises water (more than 95%) and polysaccharides, vitamins, minerals, amino acids, enzymes, and antioxidants responsible for its soothing, moisturizing, and healing actions. Renowned for its anti-inflammatory, antimicrobial, and skin-rejuvenating properties, the aloe vera gel finds broad application in personal care cosmetics, pharmaceuticals, food supplements, and beverages.
Aloe vera is a perennial fleshy succulent plant of the species Aloe barbadensis miller, grown worldwide for its nutritional, medicinal, and cosmetic benefits. It has two primary constituents: the transparent inner gel consisting mainly of polysaccharides, vitamins, enzymes, and amino acids; and the yellowish latex, consisting of anthraquinones with powerful laxative properties. Aloe vera gel is highly prized for its emollient, moisturizing, and healing properties and is a common ingredient in skincare, personal care, and pharmaceutical products.
Air purifiers are appliances that enhance indoor air quality by eliminating pollutants like dust, allergens, smoke, volatile organic compounds (VOCs), and microbial particles. They work on various technologies such as HEPA (High-Efficiency Particulate Air) filters, activated carbon filters, UV-C light, ionizers, and photocatalytic oxidation. Their major components are usually fans or blowers, filter media, sensors, electronic controls, and metal or durable plastic housings. Some of the crucial characteristics of air purifiers include efficiency of filtration, airflow, noise levels, power consumption, and filter material durability.
Air coolers are evaporative coolers based on the principle of water evaporation, utilizing a fan or blower to blow cooled air, as opposed to air conditioners, which function based on refrigerant and compressor principles. Air coolers are designed to deliver low-cost and energy-efficient temperature management, mainly applicable to dry and hot climates. They generally consist of a pump, motor, cooling pads, water tank, blower/fan, and electronic control units. Main characteristics are low energy usage, environmental friendliness, portability, and low cost. Production of air coolers typically consists of combining sheet metal or plastic enclosures with motor-driven fans, water distribution networks, and cellulose or aspen cooling pads.
A4 paper, which is one of the most commonly used paper formats around the world, is 210 mm × 297 mm and forms the part of the ISO 216 system. It mainly consists of cellulose fibers obtained from wood pulp, recycled papers, or other fibrous raw materials like bagasse or bamboo. A4 paper contains crucial characteristics like smoothness, even thickness, high opacity, brightness, tensile strength, and durability, which enable it for printing, copying, and writing. The production process includes pulping raw fibers, bleaching for whiteness, refining for increasing fiber bonding, and sheet formation under regulated drying and calendaring.
The manufacturing sector is constantly changing with continuously rising demands for sustainability, innovation, and efficiency. The time comes when companies want to expand their business or venture into new markets.
India's manufacturing industry is experiencing a remarkable transformation and growth in 2025, aiming to establish the nation as a key player in global manufacturing. Supported by governmental initiatives such as the Make in India program and the Production Linked Incentive (PLI) schemes, the sector has drawn significant foreign direct investment (FDI) and encouraged innovation across multiple industries.
India's manufacturing industry is undergoing a turning point in 2025 based on strong government initiatives, a highly skilled and youthful population, and a worldwide trend towards diverse supply chains.
The global tobacco sector remains one of the most mature yet closely scrutinized industries in the world. With demand persisting across both developing and developed markets, cigarette production continues to be a high-volume, technically refined activity governed by extensive regulation and economic influence.
The global vegan cosmetics market is experiencing unprecedented growth, driven by a new wave of conscious consumers who demand beauty products that are not only effective, but also ethical, sustainable, and cruelty-free. This movement is more than just a passing trend; it's a fundamental shift in values that is reshaping the industry.
The global online grocery market has rapidly evolved from a convenience service to a mainstream retail segment, reshaping how consumers shop for everyday essentials. According to the IMARC group report, the market reached a value of USD 710.10 Billion in 2024 and is projected to witness consistent expansion.
The India textile market is picking up serious momentum, supported by smarter tech and changing user preferences. As more buyers look for eco-friendly, premium-quality products, manufacturers are stepping up with automation, digital tools, and flexible production systems.
The global toys market plays a crucial role as toys fundamentally support child development by fostering creativity, cognitive skills, and social interaction. In 2024, the global toys market was valued at USD 113.94 Billion.
The worldwide luxury watch market is poised for sustained growth, driven by rising affluence, aspirational lifestyle, and digital evolution. As consumers place greater importance on exclusivity and craftsmanship, demand for luxury watches is growing in developed as well as emerging markets.
Baby wipes are wet disposable wipes used to clean the tender skin of an infant, mostly when changing diapers. Composed of non-woven materials and embedded with delicate cleansing products, commonly made from water, mild surfactants, moisturizers such as aloe vera, and preservatives baby wipes are made to be delicate, hypoallergenic, and safe for daily use.
A tennis ball is a type of high-performance sporting ball used in both competitive and recreational tennis. On various court surfaces, its rubber core and felt covering provide the best bounce, speed, and durability. Both pressurised and non-pressurized tennis balls are available to accommodate different playing situations and ability levels. Under international regulations, they are crucial for competitions and training, and business expansion is being driven by sustainability and material innovation.
Caramel colour or E150d, is a common food and beverage colouring ingredient that is made by carefully heating food-grade carbohydrates with alkali or acid catalysts. Known as sulfite ammonia caramel, it gives baked items, sauces, soft drinks, and alcoholic beverages a rich brown colour. In food business, it is a preferred option because to its stability, solubility, and capacity to improve aesthetic appeal. Major food regulators across the world have authorised E150d and regulated it for safe consumption.
Kitchen appliances are a diverse category of electrical and mechanical devices that are essential in modern kitchens for various cooking and food preparation tasks. These appliances have revolutionized the way we prepare and cook food, making the process more efficient and convenient. For instance, refrigerators are crucial for storing perishable foods and keeping them fresh. Ovens and stoves are fundamental for baking, roasting, and cooking on open flames or electric coils. Microwaves provide quick heating, cooking, and defrosting, saving time in the kitchen. Dishwashers automate the often-tedious task of cleaning dishes, while blenders and food processors simplify chopping, pureeing, and blending ingredients.
A plastic cigarette lighter is a small portable hand-held device that gives a flame generally used for lighting cigarettes, cigars, candles, and other small things. They are mostly butane-gas fueled, which makes them easily disposable after all the fuel has been depleted. It's manufactured using polycarbonate or polypropylene plastic, so it's very lightweight and affordable.
Tissue paper, made from both virgin and recycled pulp, has become an essential part of daily life for cleaning, dusting, wrapping, and personal use. The industry's expansion is driven by luxurious tissue products, ultra-absorbent paper towels, and rising prices. Favorable factors such as growth in the IT sector, tourism, and MNCs, along with shifts in lifestyle and attitudes towards hygiene, cleanliness, and freshness, have boosted tissue consumption. Institutions like hospitals, malls, office complexes, and F&B chains are major consumers. Government support for sustainable practices has further spurred growth. West and South India are projected to be the largest consumers of tissues due to high foreign tourist influx, growing urbanization, and a hot climate that increases demand for disposable tissues.
While secondary research acts as the base of decision-making for businesses, primary research fills in the gaps that only a nuanced and personalized perspective can deliver. With enormous volumes of data being added daily on search engines, relying on obsolete and unauthentic data could cost businesses heavily. To stay ahead of the curve and make informed decisions, tapping directly into the information gathered through your customers is essential. This helps reveal the drivers of the decision-making process, unveiling unmet needs, and highlighting nascent trends before they take shape.
Consumer behavior mainly includes consumers’ mental, emotional, and behavioral responses toward the buying pattern of products. There are several factors that influence consumer behavior, such as personal, social, cultural, and psychological. Personal factors include the age, gender, and income of the consumer. Social factors like friends and family and cultural factors such as religion and tradition also play an important role in consumer buying patterns. Motivation, perception, and learning about goods and services change consumer preferences and fall under psychological factors.