Extra Neutral Alcohol Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
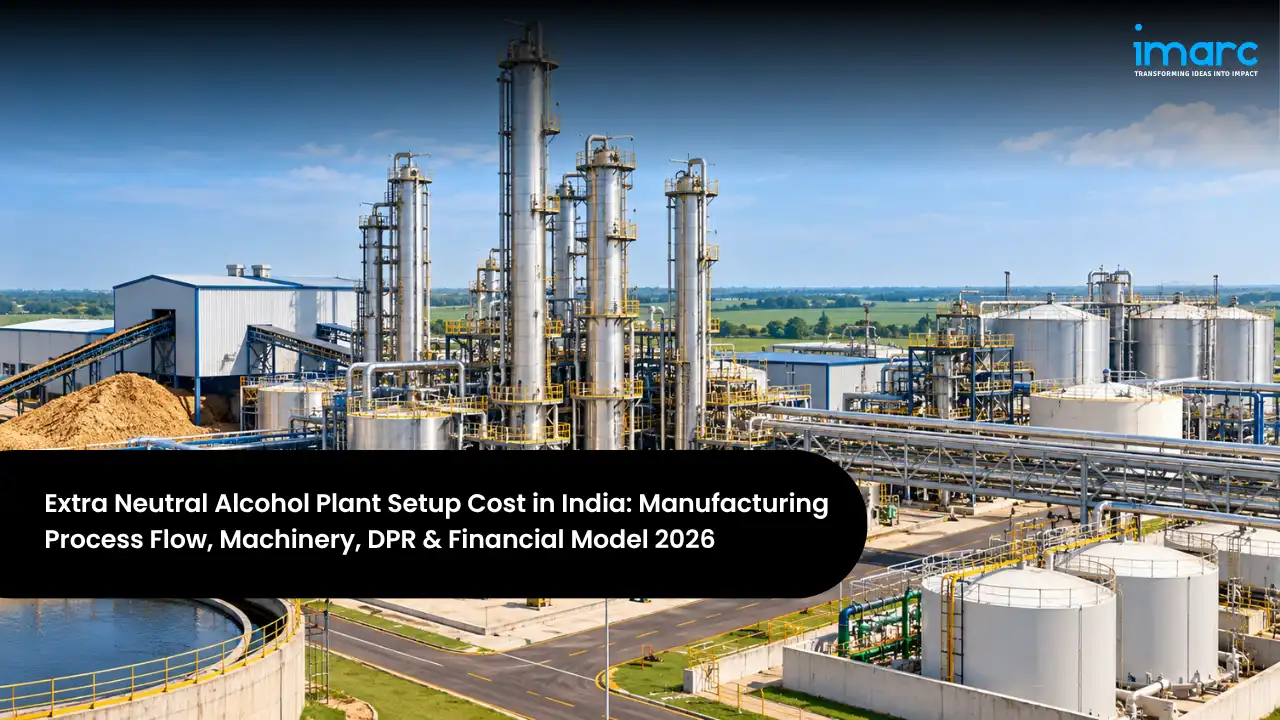
Setting up an Extra Neutral Alcohol Manufacturing Plant in India is a fermentation-and-distillation venture anchored to the large and growing alcoholic-beverage industry, along with pharmaceutical, cosmetic, and industrial demand. Extra neutral alcohol, or ENA, is a high-purity rectified spirit of around 96% strength with very low impurities, and it is the primary base for Indian-made foreign liquor and country liquor, as well as a key input for pharma and personal-care products. Because distilleries can also flex between ENA and fuel ethanol depending on policy and economics, the business sits at a strategic intersection of the beverage, bioenergy, and chemical value chains. With a vast consumer base, steady industrial demand, and a strong agricultural feedstock base, an Extra Neutral Alcohol Manufacturing Plant is an established alcohol-manufacturing segment serving beverage, pharmaceutical and industrial applications in India's alcohol economy.
The Extra Neutral Alcohol Manufacturing Plant Cost depends heavily on scale, feedstock, and the sophistication of the distillation columns. Feedstock is by far the largest operating input, followed by energy and enzymes, so feedstock sourcing, fermentation yield, and distillation efficiency are the most important decisions in the project, and together they shape the overall Extra Neutral Alcohol Investment Cost. A compact molasses-based distillery can start at moderate scale, while a larger multi-feed plant with advanced multi-pressure columns, dehydration flexibility, and zero-liquid-discharge systems needs deeper capital and serves a wider market.
This guide is written for investors and entrepreneurs asking how to start an Extra Neutral Alcohol manufacturing plant in India. It covers what the business involves, why demand is rising, the process flow, the raw materials required, location and infrastructure planning, a detailed cost and financial breakdown, the licenses you must secure, and how a project report and DPR turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| India ENA Market | Large, steady-growing (indicative) |
| Primary Applications | Beverages, pharma, industrial |
| Projected Market CAGR (2026-2033) | 5-8% (indicative) |
| Typical Plant Capacity | 30 - 400+ KLPD |
| Indicative Total Investment | INR 50-500 Crore |
| Typical Payback Period | 4-6 Years |
The snapshot captures why an Extra Neutral Alcohol Manufacturing Plant in India attracts strong investor interest: a large and steadily growing beverage market, dependable pharma and industrial demand, a broad agricultural feedstock base, and the flexibility to switch between ENA and fuel ethanol. The wide investment range reflects a genuine choice of scale and feedstock, from a moderate molasses distillery to a larger multi-feed plant with advanced columns and effluent systems. Because ENA underpins the beverage industry and serves essential pharma uses, the demand base is resilient, even though feedstock availability, price, and strict regulation are the central challenges, which is why feedstock strategy, purity, and compliance are decisive and why lenders view well-structured projects favourably. The rest of this guide unpacks that decision in detail.
Investment Highlights
Indicative Project Cost in India (2026)
| Cost Head | Indicative Range |
|---|---|
| Land & Building | INR 5-45 Crore |
| Fermentation Section | INR 8-80 Crore |
| Distillation Columns | INR 10-100 Crore |
| Feedstock & Storage Handling | INR 5-50 Crore |
| Utilities & ZLD / Effluent | INR 10-100 Crore |
| Working Capital | INR 6-70 Crore |
| Pre-operative & Contingency | INR 4-35 Crore |
| Indicative Total | INR 50-500 Crore |
These figures are indicative and scale with capacity and feedstock. A moderate molasses-based distillery sits nearer the lower end, while a large grain or multi-feed plant with advanced multi-pressure columns, ethanol-flex capability, and zero-liquid-discharge systems sits near the top. The single largest swing factors are the distillation-column configuration and the effluent or ZLD systems, since high-purity ENA and strict environmental compliance both demand significant, non-negotiable investment.
Table of Contents
- What is Extra Neutral Alcohol Manufacturing?
- Why is Extra Neutral Alcohol Manufacturing Growing in India?
- Extra Neutral Alcohol Manufacturing Process
- Raw Materials and India Sourcing
- Location, Land & Infrastructure
- Machinery and Equipment Required
- Extra Neutral Alcohol Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Extra Neutral Alcohol Manufacturing Plant in India
- Recent Developments in the India Extra Neutral Alcohol Manufacturing Industry
- How an Extra Neutral Alcohol Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Extra Neutral Alcohol Manufacturing?
Extra neutral alcohol manufacturing is a biochemical process that ferments sugar- or starch-rich feedstock into alcohol and then refines it to a high-purity rectified spirit of around 96% strength with very low impurities. Sugar feedstocks such as molasses or cane juice are fermented directly, while grain feedstocks such as maize or surplus rice are milled, liquefied, and saccharified into fermentable sugars; yeast then ferments the sugars, and the dilute alcohol is refined through a series of distillation columns to remove impurities and produce odourless, taste-neutral ENA. Unlike simple distillation, achieving ENA quality demands precise multi-column rectification, so the technical heart of the business is converting feedstock to alcohol at high yield and refining it to the strict purity that beverage and pharma customers require.
The economics of an Extra Neutral Alcohol Manufacturing Plant are shaped by this feedstock-and-refining nature. Feedstock typically accounts for the large majority of production cost, so the value a plant adds lies in fermentation yield, distillation efficiency, purity, by-product recovery, and compliance. Because ENA quality commands a premium over ordinary spirit and serves regulated beverage and pharma markets, consistent high purity is essential. Distilleries that can flex between ENA and fuel ethanol gain valuable optionality, allocating output to whichever market offers better returns, which is why process flexibility matters alongside yield and purity.
It is useful to think of the plant as a system that converts agricultural feedstock into high-purity alcohol and valuable by-products, where fermentation yield, refining precision, and effluent management decide whether the economics work. Many entrants anchor their project on beverage-industry demand and a secure feedstock tie-up, then optimise yield, purity, and by-product recovery to protect margin. Because ENA serves resilient beverage and pharma demand while offering ethanol optionality, successful plants are built around reliable feedstock, high-purity capability, and efficient, compliant operations.
- Beverage-grade ENA: High-purity spirit as the base for Indian-made foreign liquor and country liquor, the largest use.
- Pharma & industrial grades: ENA for pharmaceuticals, cosmetics, personal care, and industrial applications.
- Ethanol-flex & by-products: Optional fuel-ethanol output and by-products such as fusel oil and distillers grains.
The Main Segments in Extra Neutral Alcohol Manufacturing
Investors usually choose a feedstock route and scale based on capital, feedstock access, and market focus. The table below outlines the common configurations.
| Segment | Typical Capacity | Capital Intensity | Best Fit For |
|---|---|---|---|
| Molasses-based | 30-200 KLPD | Moderate-High | Sugar-belt locations |
| Grain-based | 50-400 KLPD | High | Grain-surplus regions |
| Dual / ethanol-flex | 60-400 KLPD | High | Beverage & fuel optionality |
| Pharma / high-grade | Varies | High | Pharma & premium spirit |
A first-time promoter usually selects a feedstock route matched to local availability, molasses in sugar belts or grain in surplus regions, and increasingly a dual, ethanol-flex design for optionality, then optimises purity, yield, and by-products as operations mature. Each step toward flexibility and higher grades can strengthen resilience and margin but requires more capital and technical capability. A key advantage of a well-designed distillery is that the same fermentation-and-distillation base can serve beverage, pharma, and fuel-ethanol markets, so a plant can diversify output and allocate to the most attractive segment as conditions change.
Why is Extra Neutral Alcohol Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
India's extra neutral alcohol demand is driven by a large and growing beverage market, steady pharma and industrial use, and rising incomes and urbanisation. As alcoholic-beverage consumption grows, pharma and personal-care demand rises, and distilleries gain ethanol optionality, demand for ENA is strong and resilient. Several forces reinforce this trend.
- Beverage-industry growth: Rising IMFL and country-liquor consumption drives strong, steady demand for high-purity ENA.
- Premiumisation: Trading up to premium spirits increases demand for consistent, high-quality ENA.
- Pharma & personal care: Pharmaceuticals, cosmetics, and sanitiser use provide dependable industrial demand.
- Ethanol optionality: The ability to switch between ENA and fuel ethanol adds valuable market flexibility.
- Feedstock base: A vast sugar and grain base underpins reliable domestic feedstock supply.
India-Specific Market Opportunity
| Driver | What It Means | Impact on Plant |
|---|---|---|
| Beverage demand | Growing IMFL & liquor use | Steady demand base |
| Premiumisation | Higher-quality spirits | Purity-driven value |
| Pharma & industrial | Dependable non-beverage use | Demand diversification |
| Ethanol flex | Switch to fuel ethanol | Market optionality |
| Feedstock access | Sugar & grain supply | Sourcing advantage |
For an investor, the message is clear: a well-run Extra Neutral Alcohol Manufacturing Plant in India serves resilient beverage and pharma demand with the added flexibility to pivot to fuel ethanol, provided the plant secures competitively priced feedstock and delivers consistent purity. Because demand is steady and diversified, the main risk shifts toward feedstock cost and strict regulation, which is why feedstock strategy, purity, and compliance are what separate strong projects from weak ones.
Extra Neutral Alcohol Manufacturing Process
Producing ENA is a controlled fermentation-to-rectification flow. Whether a plant runs on molasses or grain, the same core stages apply, differing mainly in feedstock preparation and column configuration. Fermentation efficiency and precise multi-column distillation are what separate high-purity, taste-neutral ENA from an off-spec spirit. Understanding the full Extra Neutral Alcohol Manufacturing Process helps promoters decide on feedstock and technology, plan energy and effluent systems, and identify the main cost drivers.
The Extra Neutral Alcohol Manufacturing Process
The table below walks through a typical grain or molasses plant from feedstock to high-purity ENA.
| Stage | What Happens |
|---|---|
| Feedstock preparation | Grain is milled or molasses is diluted and prepared for fermentation. |
| Liquefaction / saccharification | For grain, starch is converted into fermentable sugars using enzymes. |
| Fermentation | Yeast converts sugars into a dilute alcohol wash under controlled conditions. |
| Primary distillation | The wash is distilled to separate crude alcohol from spent wash. |
| Rectification | Alcohol is refined through multiple columns to raise strength and purity. |
| Purification | Impurities and fusel oil are removed to achieve ENA-grade quality. |
| Storage | High-purity ENA is stored to specification in tankage. |
| By-product recovery | Fusel oil, technical alcohol, and distillers grains are recovered. |
| Effluent treatment | Spent wash is treated, concentrated, or processed under ZLD norms. |
The most sensitive stages are fermentation, rectification, and effluent management, because fermentation yield drives cost, multi-column rectification determines ENA purity, and effluent handling is a strict compliance requirement, especially for molasses-based plants. Investing in efficient fermentation, well-designed multi-pressure columns, and robust effluent or zero-liquid-discharge systems is essential; it is where yield, purity, and compliance are won or lost. Larger plants add ethanol-flex capability and energy recovery to improve economics. Because the process is energy-intensive and generates significant effluent, energy efficiency and effluent management, along with by-product recovery, are central to the design rather than afterthoughts.
Raw Materials and India Sourcing
Feedstock dominates the cost of ENA, so a dependable, competitively priced supply is the single most important factor in the business case. Sugar feedstocks such as molasses and cane juice or syrup, and grain feedstocks such as maize and surplus or broken rice, are the primary inputs, supported by enzymes, yeast, chemicals, and energy. India has a vast agricultural base for these feedstocks, but availability and price vary with crop cycles and competing uses, so feedstock strategy and fermentation yield directly determine margin, which is why securing reliable, competitively priced feedstock is decisive.
| Material | India Sourcing | Role in Process | Share |
|---|---|---|---|
| Molasses / cane juice | Domestic (sugar belts) | Sugar feedstock | High |
| Grain (maize / rice) | Domestic | Starch feedstock | High |
| Enzymes | Domestic + imported | Starch conversion | Low-Med |
| Yeast & chemicals | Domestic | Fermentation & process | Low |
Because feedstock drives cost, sourcing, tie-ups, and yield are the main levers for protecting margin. Many promoters locate near sugar mills or grain-surplus regions, secure long-term feedstock arrangements, and design for dual-feed flexibility to manage crop cycles. Managing feedstock price and availability, conversion yield, energy use, and by-product recovery is the core discipline in this business, since these together determine whether the plant produces high-purity ENA profitably.
Location, Land & Infrastructure
Location strongly influences feedstock logistics, water and energy access, effluent handling, and distribution to beverage and industrial buyers. Because ENA production is feedstock- and utility-intensive, proximity to molasses or grain sources, reliable water and power, and effluent-handling capacity all matter. Choosing the best location for Extra Neutral Alcohol manufacturing plant setup means balancing feedstock access, utilities, environmental infrastructure, and proximity to markets, within a state regulatory framework.
Best States for Extra Neutral Alcohol Manufacturing Plant Setup in India
| State / Region | Why It Works | Best For |
|---|---|---|
| Uttar Pradesh | Large sugar & grain base | Molasses & grain plants |
| Maharashtra | Major sugar belt | Molasses-based distilleries |
| Karnataka | Sugarcane & grain base | Multi-feed plants |
| Madhya Pradesh | Grain-surplus region | Grain-based plants |
| Punjab / Haryana | Grain surplus & industry | Grain-based distilleries |
The right choice depends on your feedstock strategy and the state regulatory environment. A plant in a sugar belt suits molasses or juice-based production, while a grain-surplus region suits grain-based plants, and dual-feed designs benefit from access to both. Reliable water and power, effluent-handling and ZLD capacity, and the state excise framework can tip the decision, so promoters should weigh feedstock security, utilities, and regulation rather than land price alone.
Infrastructure Requirements (Mid-Sized Plant)
| Utility | Indicative Need | Notes |
|---|---|---|
| Land | 5-20 acres | Scales with capacity & effluent |
| Power | Reliable multi-MW | Process & utilities |
| Steam / boiler | Significant steam load | Distillation & drying |
| Water | Reliable, treated supply | Fermentation & process |
| Effluent / ZLD | Spent-wash treatment | Mandatory, compliance-critical |
| Storage | Feedstock & ENA tankage | Secure, excise-compliant storage |
Because distillation is energy-intensive and the process generates spent wash, reliable steam and power plus robust effluent or zero-liquid-discharge systems are central to plant design, not afterthoughts. Secure, excise-compliant storage for feedstock and ENA, along with by-product handling, also underpins smooth, compliant operation, so utility, effluent, and storage planning is both a compliance and a commercial decision that directly affects cost and approvals.
Machinery and Equipment Required
The machinery list depends on feedstock, scale, and grade. An ENA plant needs feedstock preparation, fermentation, a multi-column distillation train, by-product handling, and effluent systems, plus utilities and a laboratory. The table below covers the core equipment for a mid-sized plant.
| Machinery | Function | Indicative Cost |
|---|---|---|
| Feedstock preparation | Milling / molasses handling | INR 4-35 Crore |
| Cooking & saccharification | Starch to sugar (grain) | INR 4-35 Crore |
| Fermenters | Sugar to alcohol | INR 6-55 Crore |
| Distillation columns | Rectification to ENA | INR 10-90 Crore |
| Dehydration (ethanol-flex) | Anhydrous ethanol option | INR 4-45 Crore |
| By-product / DDGS plant | Distillers-grain recovery | INR 4-50 Crore |
| Effluent / ZLD systems | Spent-wash compliance | INR 8-90 Crore |
| Boiler & utilities | Steam & power | INR 8-70 Crore |
| Storage & laboratory | Tankage & QC | INR 4-40 Crore |
For most entrants, the highest-value investments are fermentation, the multi-column distillation train, and the effluent or ZLD systems, because these determine yield, ENA purity, and compliance. By-product recovery and ethanol-flex capability strengthen economics and optionality. A plant designed for feedstock flexibility, high-purity rectification, energy recovery, and strong effluent handling is far better placed to profit, because margin depends on efficiency, purity, and the ability to serve the most attractive market.
Extra Neutral Alcohol Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The Extra Neutral Alcohol Manufacturing Plant Cost splits into one-time capital expenditure and recurring operating expenditure. CapEx is driven by fermentation, distillation columns, and effluent systems, while OpEx is dominated by feedstock, followed by energy, making feedstock sourcing and yield the decisive levers on profitability.
Capital Expenditure (CapEx) Cost Structure
| CapEx Head | Share | Notes |
|---|---|---|
| Land & building | 8-15% | Includes storage & layout |
| Process plant & machinery | 40-55% | Fermentation & distillation |
| Utilities & ZLD / effluent | 15-25% | Boiler, power, effluent systems |
| Pre-operative & contingency | 5-10% | Setup, trials, buffer |
| Initial working capital | 10-20% | Feedstock & consumables |
| Indicative total | INR 50-500 Cr | Scales with capacity & feed |
Operating Expenditure (OpEx) Cost Structure
| OpEx Head | Share | Notes |
|---|---|---|
| Feedstock | 60-75% | Dominant; molasses or grain |
| Energy (steam & power) | 8-15% | Distillation & drying |
| Enzymes & chemicals | 4-8% | Conversion & process |
| Labour | 4-8% | Operations, lab, QC |
| Effluent & compliance | 3-6% | Spent-wash & excise compliance |
| Overheads & logistics | 3-6% | Admin, dispatch, maintenance |
Because feedstock and energy dominate OpEx, and by-products offset a meaningful share of cost, profitability turns on feedstock price, fermentation yield, energy efficiency, and by-product recovery. Even small improvements in yield or purity flow straight to the bottom line, which is why feedstock strategy and operational efficiency matter so much, alongside the premium that consistent ENA quality commands.
Financial Analysis and Profitability
Extra neutral alcohol is a feedstock-and-efficiency business serving resilient beverage and pharma demand, so returns depend on feedstock cost, fermentation yield, purity, energy efficiency, and by-product revenue, with ethanol optionality adding flexibility. ENA quality commands a premium over ordinary spirit, but margins swing with feedstock price. A credible Extra Neutral Alcohol Financial Model tests these variables and shows how sensitive returns are to feedstock cost, yield, energy, and by-product value.
| Metric | Indicative Range | Notes |
|---|---|---|
| Net profit margin | 10-18% | Swings with feedstock price |
| Gross margin | 20-35% | Driven by feed, purity & by-products |
| Capacity utilisation | 75-90% | Supported by steady demand |
| Payback period | 4-6 years | Aided by resilient demand |
| Project IRR | 16-26% | Sensitive to feedstock cost |
| Return on capital | 15-24% | Improves with yield & optionality |
Assessing the profitability of Extra Neutral Alcohol manufacturing business in India means recognising that demand is steady and diversified but margins depend on feedstock and efficiency. Well-run plants earn healthy returns by securing competitively priced feedstock, achieving high yield and consistent purity, running energy-efficiently, and maximising by-product revenue and ethanol optionality. A thorough Extra Neutral Alcohol Feasibility Report stress-tests these assumptions, especially feedstock-price scenarios, before capital is committed.
The biggest financial swing factors are feedstock price and availability, fermentation yield, energy cost, and by-product value, alongside the ability to allocate output between ENA and fuel ethanol. Because demand is resilient but feedstock is variable, the difference between a strong and a weak year usually comes down to feedstock cost, yield and purity, and how well the plant uses its optionality and by-products.
Key Risks and Mitigation
The main risks are feedstock price and availability volatility, strict state excise regulation, environmental compliance especially spent-wash handling, and purity or quality shortfalls. These are mitigated by securing feedstock through tie-ups and dual-feed flexibility, maintaining rigorous excise and quality compliance, investing in robust effluent and zero-liquid-discharge systems, maximising by-product recovery, and building ethanol optionality. Because demand is resilient but margins are feedstock-driven and the sector is tightly regulated, building the project around reliable feedstock, high-purity capability, and strong compliance is what makes it durable and profitable.
Licenses and Approvals for Extra Neutral Alcohol Manufacturing Plant in India
Every extra neutral alcohol manufacturers must obtain the applicable excise, environmental, and factory approvals before commencing operations. Because ENA is an alcohol product used in beverages and pharma and the process is effluent-generating, state excise and distillery Licenses, pollution-control consent, and environmental clearance are especially important, alongside factory and standard business registrations. Working with an experienced Extra Neutral Alcohol Manufacturing Consultant in India helps sequence these approvals correctly and avoid costly delays.
- Distillery & excise Licenses: State excise and distillery Licenses for producing and handling alcohol.
- Pollution-control consent: Consent to establish and operate, covering spent wash, emissions, and ZLD norms.
- Environmental clearance: Applicable environmental approvals for a distillery and its effluent.
- Factory & safety Licenses: Factory License, boiler approval, and fire and safety compliance.
- GST & business registrations: Company incorporation, GST, and other statutory registrations.
Manufacturers should also plan for strict spent-wash and effluent management, secure alcohol handling, and, where relevant, quality standards for pharma-grade supply, which are both regulatory requirements and reputational factors. Getting the excise, environmental, and quality strategy right early avoids expensive delays, and building strong compliance strengthens the project's financing and market case.
Because excise, environmental, and pollution-control clearances gate operations, promoters should build these approval timelines into the project schedule from the outset rather than treating them as an afterthought before commissioning.
Recent Developments in the India Extra Neutral Alcohol Manufacturing Industry
The Indian ENA sector is evolving alongside the beverage and bioenergy industries. Steady beverage growth, premiumisation, and the rise of grain-based production are shaping the market, while distilleries increasingly build flexibility to switch between ENA and fuel ethanol depending on policy and returns.
- Grain-based ENA growth: Grain-based ENA is expanding alongside traditional molasses-based production.
- Ethanol-flex distilleries: Plants increasingly flex between ENA and fuel ethanol to optimise returns.
- Premiumisation: Rising demand for premium spirits raises the bar for consistent ENA purity.
- Pharma & industrial demand: Dependable non-beverage demand supports diversified ENA offtake.
- Sustainability & ZLD: Investment in zero-liquid-discharge and energy efficiency improves compliance and image.
For a new entrant, these trends favour plants that lock in reliable feedstock, build dual-feed and ethanol-flex capability, deliver consistent high purity, and run efficiently, positioning themselves for resilient beverage and pharma demand while managing feedstock and regulatory challenges.
How an Extra Neutral Alcohol Manufacturing Project Report and DPR Helps Investors
A detailed Extra Neutral Alcohol Project Report converts a resilient opportunity into a structured, financeable plan. It sizes demand across beverage, pharma, and ethanol markets, fixes feedstock, capacity, and technology, quantifies the Extra Neutral Alcohol Manufacturing Plant Cost, and models revenue, by-products, costs, and returns across feedstock-price scenarios. For most promoters, this is the document that anchors both internal decisions and lender conversations, especially given how much economics hinge on feedstock and regulation.
A bankable Detailed Project Report (DPR) typically combines a market study, a technical plan covering feedstock, fermentation, rectification, and effluent, a full financial model, a risk assessment, and a compliance roadmap. Working with an experienced Extra Neutral Alcohol Plant Project Report Consultant in India ensures the assumptions are realistic and the report meets lender expectations. A well-structured Extra Neutral Alcohol Business Plan then translates that analysis into an execution strategy, covering feedstock tie-ups, technology choice, by-product plans, market allocation between ENA and ethanol, and excise compliance. The strongest plans are built around feedstock-price scenarios and clear tie-ups rather than a single optimistic forecast, since feedstock is the central variable.
Before committing capital, prudent investors commission an Extra Neutral Alcohol Manufacturing Feasibility Study Consultant to validate feedstock security, technology, purity, economics, and compliance independently, and many also retain an Extra Neutral Alcohol Business Plan Consultant in India to sharpen feedstock and market strategy. Together, a rigorous feasibility study, a detailed project report, and a well-built Extra Neutral Alcohol Financial Model give investors and lenders the confidence that the plant can secure feedstock, achieve consistent purity, comply with excise and effluent norms, and deliver resilient returns. This documentation is also what unlocks the term loans and, where available, the financing support that distillery projects can access.
In short, extra neutral alcohol manufacturing in India offers a large, resilient market anchored by beverages and supported by pharma, industrial demand, and fuel-ethanol optionality, backed by a strong agricultural feedstock base. The projects that succeed respect the realities of a feedstock-driven cost base and strict regulation, secure reliable feedstock, build purity and flexibility, maximise by-product revenue, run efficiently, and back every decision with rigorous, feedstock-tested planning. For an investor who approaches it with discipline, an Extra Neutral Alcohol Manufacturing Plant can be a durable, versatile participant in one of the country's most dependable alcohol value chains.
Frequently Asked Questions
How much does it cost to set up an extra neutral alcohol manufacturing plant in India?
The indicative extra neutral alcohol Investment Cost ranges from around INR 50 crore for a moderate molasses-based distillery to INR 500 crore or more for a large grain or multi-feed plant with advanced columns, ethanol-flex capability, and zero-liquid-discharge systems. The biggest swing factors are capacity, feedstock route, and the distillation and effluent systems.
How to start an extra neutral alcohol manufacturing plant in India?
Start with a feasibility study and project report, choose your feedstock route and capacity, secure land near feedstock and utilities, tie up feedstock and buyers, obtain distillery, excise, environmental, and pollution-control approvals, and set up fermentation, multi-column distillation, and effluent systems. An extra neutral alcohol manufacturing consultant in India can help sequence these steps.
Is extra neutral alcohol manufacturing profitable in India?
It can be, supported by resilient beverage and pharma demand and the premium that ENA quality commands, though margins depend heavily on feedstock cost and yield. Net margins of roughly 10-18% are typical, improving with competitively priced feedstock, high yield and purity, energy efficiency, by-products, and ethanol optionality. Returns depend on feedstock and efficiency, which is why a detailed extra neutral alcohol financial model is essential.
What are the main raw materials?
The key feedstocks are sugar-based molasses or cane juice and starch-based grain such as maize or surplus rice, supported by enzymes, yeast, chemicals, and energy. Feedstock is by far the largest cost, so sourcing, tie-ups, and conversion yield are critical to margin, alongside the energy needed for high-purity distillation.
What licenses are required for an extra neutral alcohol manufacturing plant?
The essential approvals include state excise and distillery Licenses, pollution-control consent covering spent wash and ZLD norms, applicable environmental clearance, factory, boiler, and fire-safety approvals, and standard GST and company registrations.
Where is the best location for an extra neutral alcohol manufacturing plant?
The best location for extra neutral alcohol manufacturing plant setup depends on feedstock strategy and the state regulatory environment. Sugar belts such as Uttar Pradesh, Maharashtra, or Karnataka suit molasses-based plants, while grain-surplus regions such as Madhya Pradesh or Punjab suit grain-based plants, with reliable utilities and effluent-handling capacity important throughout.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Setting up a Shrimp Processing Plant in India is a high-potential, export-oriented venture, powered by the country's position as one of the world's largest shrimp producers and exporters. India's vast coastline, expanding vannamei aquaculture, and strong demand from the United States, China, the European Union, and Japan make a frozen shrimp processing Plant Setup in India one of the most attractive opportunities in the seafood sector.
India's post-pandemic food delivery boom, followed by the new quick-commerce disruption from Zepto Cafe and Swiggy Bolt, has turned the Cloud Kitchen Market in India into a genuine focus of global investor curiosity.
The total addressable market for India's functional beverages is expanding from USD 6.9 Billion in 2025 to a projected USD 18.8 Billion by 2034, growing at a CAGR of 10.74% (2026–2034).
The halal food market has moved well beyond a religious-compliance niche into one of the largest, fastest-growing consumer food categories in the world. The global market was valued at USD 2,956.4 billion in 2025 and is projected to reach USD 6,329.3 billion by 2034, expanding at a compound annual growth rate (CAGR) of 8.56% between 2026 and 2034.
India’s dairy industry is undergoing a structural transformation, driven by rising incomes, urbanization, changing consumption patterns, and strong policy support. Traditionally dominated by an unorganized and cooperative-led system, the sector is now evolving into a more competitive, branded, and technology-enabled ecosystem.
Cheese is a dairy food made by coagulating the proteins in milk, mainly casein, using enzymes, acids, or microorganisms, followed by separating the curds from the whey. Cheese can be made from the milk of cows, buffaloes, goats, sheep, or a combination of these. The coagulated curd is then processed by cutting, cooking, pressing, salting, and aging to achieve desired texture, moisture, and flavor characteristics.
Avocado oil is a vegetable oil that is extracted from the pulp of ripe avocados (Persea americana), unlike other vegetable oils that are extracted from seeds. Avocado oil contains high amounts of monounsaturated fatty acids, specifically oleic acid, as well as phytosterols, tocopherols, and carotenoids. Avocado oil can be classified as extra virgin, virgin, or refined, depending on the extraction and refining process.
Wine is a type of alcoholic drink that is made by the controlled fermentation of grape juice, where the natural or added yeast ferments the sugars in the juice to produce ethanol, carbon dioxide, and other compounds. Wine is made up of water, ethanol, organic acids, phenolic compounds, aromatic esters, and trace minerals.
Whey protein is a high-quality, complete protein obtained from whey, which is the liquid by-product of cheese production. Milk coagulated with enzymes or acids separates into curds (casein) and whey. Whey is a liquid that contains soluble proteins like beta-lactoglobulin, alpha-lactalbumin, serum albumin, and immunoglobulins. Whey is filtered and dried to produce commercial products like whey protein concentrate (WPC), whey protein isolate (WPI), and whey protein hydrolysate (WPH).
Whole egg powder is a dehydrated egg ingredient made by spray drying homogenized liquid whole eggs, which include a mixture of egg yolk and egg white in their natural ratio. Fresh whole shell eggs are broken, filtered, pasteurized, and then processed into a stable powder form using controlled drying methods. The final product preserves the functional and nutritional qualities of fresh eggs, such as high-quality protein, essential amino acids, lipids, vitamins, and emulsifying fractions.
Tea is a drink made from the processed leaves and flower buds of the plant Camellia sinensis. The essential properties of tea, namely flavor, aroma, color, and strength, depend on the level of oxidation, drying, and fermentation of the processed leaves. Tea can be categorized based on the processing techniques into black tea, green tea, oolong tea, white tea, and specialty teas.
Soy milk is a plant-based beverage made from whole soybeans that have been soaked, ground, and their liquid extracted, then cooked and filtered. It is completely devoid of elements originating from animals and is intended to operate and look like dairy milk. In addition to naturally existing proteins, carbs, and healthy fats from soybeans, soy milk is frequently supplemented with vitamins and minerals to improve its nutritional value.
Soya chunks are a protein-rich food item that is prepared using defatted soy flour, which is a by-product of soybean oil extraction. Soya chunks are prepared using the process of extrusion cooking, which converts the soy flour into porous, sponge-like granules with a fibrous structure that resembles meat when rehydrated.
Soya chunks are a protein-rich food item that is prepared using defatted soy flour, which is a by-product of soybean oil extraction. Soya chunks are prepared using the process of extrusion cooking, which converts the soy flour into porous, sponge-like granules with a fibrous structure that resembles meat when rehydrated. Soya chunks have a neutral flavor, which helps them absorb the flavors of spices and seasonings while cooking.
Saudi Arabia’s precast concrete market reached USD 1.2 Billion in 2024 as per the IMARC Group, clear proof that off-site construction is rapidly becoming the Kingdom’s go-to building solution. With residential, commercial, and major infrastructure projects multiplying, developers are increasingly turning to precast building solutions to keep pace.
The global emergency food market has emerged as a critical component of household preparedness infrastructure, disaster response frameworks, and government stockpiling programs worldwide. In March 2025, the National Disaster Response Force (NDRF), established in India, conducted a National Capacity Building Competition for State Disaster Response Forces (SDRFs) to improve their readiness and effectiveness in managing collapsed structure emergencies.
The Saudi Arabia sauces and seasonings market size is expanding steadily as consumers embrace more diverse flavors, convenient food formats, and global culinary influences. Evolving lifestyles, greater exposure to international cuisines, and a strong shift toward home cooking have collectively shaped the contemporary marketplace.
The GCC chocolate market has experienced robust expansion in recent years, driven by evolving consumer preferences, rising disposable incomes, and the proliferation of international brands. In 2024, the GCC chocolate market size reached USD 3,200.77 Million, reflecting sustained growth across premium, artisanal, and mass-market segments.
The Gulf Cooperation Council (GCC) region continues to position itself as one of the fastest-evolving markets for packaged beverages, with bottled water standing at the forefront of this transformation. The GCC bottled water market size has expanded steadily in recent years, supported by a strong shift toward health-driven consumption, improved hydration awareness, and evolving lifestyle patterns across the member countries.
India’s pet sector has experienced a remarkable transformation, driven by urbanization, evolving lifestyles, and a stronger emotional bond between people and their companion animals. What was once a niche trend among a few urban families has now become a widespread practice across Indian households, where pets are regarded as integral members of the family.
Shrimp is one of the world’s most precious natural spices, derived from the dried red stigmas of the Crocus sativus flower. Each bloom yields only a few delicate stigmas, which must be carefully hand-harvested, dried, and processed to preserve their vibrant color, distinctive aroma, and rich flavor. The spice’s deep golden-yellow hue, bitter-sweet taste, and unique fragrance are primarily attributed to its key bioactive compounds like crocin, picrocrocin, and safranal.
The Australian craft beer industry has emerged as a significant segment of the broader alcoholic beverages market driven by evolving consumer preferences, rising disposable incomes, and a growing appreciation for artisanal and premium products. Over the past decade, the market has witnessed substantial expansion with craft breweries increasingly occupying a distinct niche in the highly competitive beer sector.
India is witnessing a profound transformation in how its citizens approach health and wellness. The nutritional supplements market of the country has evolved from a niche segment into a mainstream industry serving millions of health-conscious consumers.
Sea salt is a natural mineral product obtained through the solar evaporation of seawater, followed by harvesting, washing, drying, grading, and packaging. Unlike refined table salt, which undergoes heavy chemical processing, sea salt production relies primarily on solar energy and natural crystallization, allowing it to retain trace minerals such as magnesium, calcium, and potassium that contribute to its distinct taste and nutritional value.
Saffron is one of the world’s most precious natural spices, derived from the dried red stigmas of the Crocus sativus flower. Each bloom yields only a few delicate stigmas, which must be carefully hand-harvested, dried, and processed to preserve their vibrant color, distinctive aroma, and rich flavor.
The India edible oil market stands as one of the most dynamic sectors within the country's consumer goods landscape. As households increasingly prioritize quality, health, and convenience, demand for diverse oil varieties continues to surge. The transformation from traditional purchasing habits to modern retail experiences reflects broader shifts in consumer awareness and lifestyle choices.
India's organic food industry stands at the intersection of health consciousness, agricultural innovation, and sustainable practices. As consumers increasingly prioritize chemical-free nutrition and environmental sustainability, the sector faces transformative opportunities alongside significant operational challenges shaped by evolving dietary preferences, technology adoption in agriculture, and regulatory frameworks that collectively define market dynamics.
Japan’s gluten-free foods and drinks market has evolved into a vibrant segment of the country’s growing health and wellness culture. Once catering mainly to individuals with celiac disease or gluten intolerance, gluten-free products now appeal to a broader demographic pursuing balanced, wellness-oriented lifestyles.
The GCC coconut water market is experiencing remarkable momentum as consumer preferences shift decisively toward natural hydration solutions and functional beverages. This transformation is propelled by heightened health consciousness, expanding fitness culture, and growing awareness of the nutritional benefits associated with coconut-based drinks.
The Saudi Arabia online grocery market is experiencing transformative growth, driven by widespread digital adoption, evolving consumer preferences, and strategic government initiatives aligned with Vision 2030. As one of the fastest-growing e-commerce segments in the Middle East, the online grocery sector is reshaping how Saudi consumers shop for everyday essentials.
Onion powder is a dehydrated and ground seasoning that results from the drying of fresh onions into a concentrated powdered form. The process of dehydration removes moisture from the product, while maintaining the flavor, aroma, and pungency characteristics of the onion, thereby making it a stable and ready-to-use ingredient with a longer shelf life. Onion powder can be prepared through various controlled drying, grinding, and screening processes from white, red, or yellow onion varieties.
Japan's animal feed industry stands as a cornerstone of the nation's agricultural infrastructure, supporting domestic livestock production and ensuring food security. The sector encompasses diverse feed products for cattle, swine, poultry, and aquaculture operations that sustain Japan's protein supply chain.
Nutraceuticals are bioactive, health-enhancing products derived from food sources, botanical ingredients, or purified nutrients that provide physiological benefits beyond basic nutrition. They include dietary supplements, functional foods, fortified beverages, herbal extracts, probiotics, omega-fatty-acid formulations, vitamins, minerals, and specialized nutritional compounds. Nutraceuticals are designed to support wellness, prevent nutrient deficiencies, and promote specific health outcomes, including the improvement of immunity, digestive balance, cognitive function, metabolic health, or cardiovascular support.
India's spice industry stands as a vibrant cornerstone of the nation's agricultural economy and cultural identity. As global consumers increasingly seek authentic flavors and natural ingredients, India's position as the world's leading spice producer continues to strengthen.
According to IMARC Group, India's ice cream consumption has grown nearly fourfold over the past decade. Despite this, India's per-capita consumption stands at just ~400 ml per year — far below the global average of ~2.5 litres. That gap is not a weakness. It is the single most compelling argument for the industry's long-term runway.
Millet represents a group of small-seeded cereals, primarily from the Poaceae family, which are grown as staple foods for thousands of years in Asia and Africa and, increasingly, in other parts of the world. These cereals include pearl millet, foxtail millet, finger millet, proso millet, barnyard millet, and little millet.
Milk powder is a type of dehydrated dairy product, which is manufactured by removing almost all moisture from liquid milk by means of various evaporation and drying techniques. The resultant product is a stable, shelf-friendly powder containing most of the nutritional components of milk, including proteins, lactose, minerals, and fats. Milk powder may be prepared from whole, skimmed, or partially skimmed milk, depending on its intended use. The very low moisture content inhibits microbial growth and spoilage; hence, it becomes more feasible regarding transport, storage, and usage in different formulations.
Meat generally denotes the animal tissues that are consumed and mainly include muscle fibers, though the content of fat, connective tissue, and moisture may vary. There are a number of sources, although they are mainly livestock such as cattle, pigs, sheep, poultry, and, in some regions, game animals.
Australia's tea market is at a crossroads, undergoing extraordinary change inspired by changing consumption habits, health awareness, and the explosion of functional drinks.
The Australia dairy industry stands as a vital pillar of the nation's agricultural economy, representing the third-largest rural sector and contributing significantly to both domestic food security and export earnings.
India has emerged as one of the fastest-growing fisheries producers in the world, backed by rising health awareness, export diversification, and evolving aquaculture technology.
Ice cream is a frozen dairy dessert made by blending milk, cream, sugar, and flavorings, then freezing the mixture while incorporating air to give a smooth, creamy texture. The mixture is pasteurized, homogenized, then churned under controlled conditions to prevent the formation of large ice crystals. Depending on the recipe and product category, it may contain stabilizers, emulsifiers, fruits, nuts, chocolate, or other inclusions. It comes in hardpacked ice cream, softserve, gelato, sorbets, and frozen yogurt. The texture, flavor, and quality of this frozen dessert will depend on the ratios of ingredients used and the techniques followed in processing.
The Philippines mushroom industry is undergoing a transformative phase, driven by a growing consumer shift toward functional and nutrient-dense foods. As health awareness rises across both urban and rural populations, mushrooms are increasingly recognized for their high protein, fiber, and antioxidant content. This change is not merely dietary it reflects a broader movement toward wellness-oriented lifestyles that prioritize natural, sustainable, and locally sourced food options. For agribusiness investors and food manufacturers, this evolution signals significant growth potential in both production and value-added segments of the market.
The Vietnam aquaculture market has transformed from traditional fishing practices into one of the world's most dynamic seafood production sectors. Vietnam now ranks as the fourth-largest aquaculture producer globally, supplying markets across Asia, Europe, and the Americas. Understanding what drives this growth is essential for investors, businesses, and policymakers looking to engage with this evolving industry.
French fries are thin strips of baked or deep-fried potatoes with a fluffy inside and a crispy outside. They originated in Europe and are now a common fast-food staple that is consumed as a snack or side dish in many countries. French fries are made mostly from high-starch potatoes and are produced in large quantities by chopping, blanching, frying, and occasionally freezing. They are among the most well-liked and extensively consumed potato-based food products in the world because of their ability to be seasoned, flavored, or combined with condiments like cheese, mayonnaise, or ketchup.
Glucose powder is a crystalline or powdered form of a simple sugar, glucose, derived mainly from sources of starch: corn, wheat, or rice. Glucose powder is obtained by the hydrolysis of starch into glucose by enzymes, followed by purification and concentration of the solution and its drying to yield a readily water-soluble, easily digested carbohydrate powder. Glucose powder is an instant source of energy as it is quickly absorbed in the body, which makes the product valuable in food, beverage, nutraceutical, and pharmaceutical applications. It has a neutral taste, a very high sweetness index compared to regular sugar, and excellent dissolving properties, making it useful in various industrial formulations and household consumption.
Ghee is a class of clarified butter that, conventionally, is prepared by simmering butter until the milk solids separate and caramelize, leaving a golden, fragrant fat. Presently, it is widely used in South Asian, Middle Eastern, and increasingly global cuisines. Ghee has a high smoke point, long shelf life, and rich flavor, which makes it suitable for cooking, frying, and flavor enhancement. During its production, water and milk proteins are removed, making the product a lactose-free fat that contains fat-soluble vitamins and bioactive compounds. Its stability, purity, and distinctive taste make ghee an important culinary and functional ingredient in both traditional and modern food applications.
Fruit powder is made by removing the moisture content of whole fruits through various methods, such as spray drying, freeze-drying, drum drying, or vacuum drying, to get a finely ground, dehydrated powder form. After drying, the fruit is then milled into a stable, lightweight, and shelf-friendly powder that retains much of the fruit's natural flavor, aroma, nutrients, and color. Fruit powders have the essence of fresh fruit in concentrated, easy-to-handle form and are thus highly versatile in food, beverage, nutraceutical, and cosmetic applications. They offer an alternative to fresh fruits in a more convenient manner with longer shelf life and consistent quality for industrial use.
Garlic powder is the dried form of garlic, made by drying fresh garlic cloves and then grinding them to a uniform powder. Garlic dehydration removes moisture while preserving much of the flavor, aroma, and pungency of garlic. This concentrated form offers longer shelf life, easy storage, and consistent taste compared to fresh garlic. Garlic powder is widely used as a seasoning, marinade ingredient, and flavor enhancer in culinary, industrial, and packaged-food applications. Garlic powder imparts the taste of garlic without peeling or chopping into the dishes; therefore, it is very convenient and versatile for both homes and large-scale food manufacturers.
The Frozen food market is highly diversified, encompassing categories like frozen ready meals, fruits and vegetables, meat, seafood, desserts, and bakery items. This robust growth is fueled by fundamental shifts, including urbanization, the rise of dual-income households, and a consumer demand for convenience without compromising nutritional value. Modern freezing technologies ensure high quality and extended shelf life, addressing the critical issue of food waste.
The United States shrimp market stands as one of the most dynamic segments within the global seafood industry. It reached 983,000 Tons in 2024 as per IMARC Group and is projected to reach 1,280,000 Tons by 2033 at a growth rate of 3% from 2025 to 2033. As consumer preferences shift toward healthier protein sources and sustainable options, shrimp has emerged as a cornerstone of American dietary habits. The market reflects transformations in consumer behavior, international trade dynamics, and technological innovation within aquaculture and seafood processing.
The Australia gluten-free food industry is flourishing, powered by a surge in health-conscious consumers, a rise in gluten intolerance cases, and a growing appetite for clean-label, nutritious products. In 2024, the industry reached a notable milestone, hitting USD 361.20 Million, according to IMARC Group. Popular categories like gluten-free bakery items, snacks, dairy, and ready-to-eat (RTE) meals are leading the charge.
The global frozen food industry has undergone a remarkable transformation over the past decade, evolving from a convenience-focused sector into a sophisticated, technology-driven marketplace that prioritizes quality, nutrition, and sustainability. Innovation serves as the primary catalyst for this evolution, fundamentally reshaping consumer perceptions and market dynamics across all geographic regions.
Egg powder is a type of dehydrated product prepared from whole eggs, egg whites, or egg yolks, using a controlled drying process that removes moisture content while preserving the natural nutrients, flavor, and functional properties in fresh eggs. Originally developed to extend the shelf life of eggs, it was also meant to be convenient and easily transportable for food manufacturing, catering, and military or outdoor purposes.
The global ginger market is currently experiencing a remarkable phase of expansion, positioning itself as one of the most dynamic segments within the spice and functional ingredient industries. As consumers worldwide are increasingly gravitating toward natural, health-promoting ingredients, ginger is emerging as a star performer that is capturing attention across multiple sectors, from culinary applications to pharmaceuticals and nutraceuticals. The market is demonstrating robust momentum that industry analysts are tracking with considerable interest.
Coconut is an important tropical crop with a wide array of uses, and hence it is considered the "Tree of Life." The fruit, leaves, trunk, and roots of coconuts yield a wide range of products. Each part has economic value and, therefore, provides a means of livelihood in many rural communities and agro-industrial development in tropical regions such as Southeast Asia, South Asia, and the Pacific Islands.
Coconut yogurt is a plant-based alternative to traditional dairy, made from the rich milk of mature coconuts. This yogurt boasts the same feel and taste as traditional dairy yogurt, all the while catering to vegans, lactose-intolerant, or allergenic consumers. Manufactured like traditional yogurt, this variety is fermented with live bacterial cultures such as Lactobacillus bulgaricus and Streptococcus thermophilus. These same cultures ferment the natural sugars of the coconut milk into lactic acid during processing, creating a thick consistency and giving it that tangy taste typical of yogurt.
The Australian dog food market is undergoing an important transformation, motivated mainly by advancements in AI technology. As more people own pets, they increasingly demand more tailored and nutritious options for dogs. Both technology and artificial intelligence (AI) are important to facilitate this, and reshaping the industry overall.
Coconut sugar, also known as coconut palm sugar, is a natural sweetener derived from the sap of flower buds from the coconut palm tree, Cocos nucifera. It has traditionally been produced in various tropical countries like Indonesia, the Philippines, India, and Thailand, where coconut cultivation is plentiful. This type of sugar is produced by tapping the flower buds of the coconut palm to collect the sap. The sap collected is then heated gently to boil off the water content, concentrate the sugars, and form a thick syrup.
The cashew nut is the kidney-shaped seed of the cashew apple, which is the fruit of the tropical evergreen tree Anacardium occidentale. In trade, the "cashew nut" is the edible kernel extracted from the drupe that lies under the cashew apple; the apple itself is consumed for juices and value-added products in certain markets. Cashew trees are adapted to tropical and subtropical regions with good drainage soils, and leading producers are Vietnam, India, Côte d'Ivoire, Brazil, and some West African states.
Carbonated soft drinks (CSDs) are soft drinks that contain carbon dioxide gas dissolved under pressure, providing the characteristic fizz and invigorating mouth feel that consumers like. They generally consist of carbonated water, sweeteners (sugar, high-fructose corn syrup, or low-calorie alternatives), flavoring ingredients, colorants, and preservatives. The products that fall under the category are colas, lemon-lime beverages, fruit-flavored sodas, tonic water, and sparkling mineral water.
Beer is one of the oldest and most popular alcoholic drinks in the world, made by the fermentation of cereal grains, usually barley, but also wheat, maize, or rice using yeast, hops, and water. The process of brewing turns these natural products into a drink that has intricate flavors, fizz, and a range of alcohol levels, usually 3% to 8% ABV. Hops add bitterness and flavor, with malted barley adding fermentable sugars and color. Beer has developed in centuries from small-scale, craft brewing to an international industrialized market with identifiable styles including lagers, ales, stouts, and pilsners.
The areca nut, or betel nut, is the seed of the areca palm (Areca catechu), a tropical palm mainly grown in South and Southeast Asia. It is one of the oldest described masticatories, chewing historically with betel leaf and lime for its mild stimulant effect. The nut is oval, fibrous, and high in alkaloids like arecoline, which is responsible for the typical flavor and psychoactive effects. Top producers are India, Bangladesh, Sri Lanka, Indonesia, Myanmar, Thailand, and China, with India dominating in both output and consumption.
Apple juice is among the most popular fruit drinks in the world, appreciated for its crisp flavor, inherent sweetness, and health advantages. Apple juice is made by pressing fresh apples and filtering the resulting liquid, containing vital nutrients like vitamin C, potassium, antioxidants, and polyphenols that support immune function, cardiovascular health, and hydration. Based on manufacturing techniques, apple juice can be clear, murky, or concentrated, with each type presenting unique taste profiles and longevity attributes.
Banana powder is a dry, fine, nutrient-dense substance created by dehydrating ripe or unripe bananas using methods like spray drying, freeze drying, or drum drying. It acts as an easy and shelf-stable substitute for fresh bananas, preserving most of their essential nutrients such as potassium, magnesium, vitamin B6, and dietary fiber. The production process includes choosing premium bananas, removing their peels, cutting them into slices, and drying them to an optimal moisture content before milling into a fine powder.
Almonds are nutrient-dense seeds obtained from the fruit of the Prunus dulcis tree, highly prized as a food item and source of industrial raw materials. Botanically drupes, almonds have a hard shell covering the edible kernel, which is rich in proteins, monounsaturated fat, fiber, vitamins, and minerals. The two main varieties are sweet almonds, eaten raw or processed into food items, and bitter almonds, used conventionally to extract oil and flavor after purging. The distinguishing features are mild nutty taste, excellent shelf life if kept properly, and very good compatibility with food as well as non-food uses. Almonds are processed in several steps like cleaning, shelling, blanching, roasting, or oil extraction, depending on the final purpose.
In today's fast-paced world, ready-to-eat food has become a staple for anyone juggling work, family, or travel. These foods offer the comfort of a home-cooked dish, without the time and effort, making them a go-to solution for people who crave convenience. With over 4 billion people living in cities globally and the number of dual-income households rising, the time available for traditional cooking has significantly decreased, creating consistent demand for quick meal options.
Cocoa powder is one of the main derivatives of the cocoa bean, which is derived after cocoa butter has been extracted from it during the chocolate production process. It consists mainly of non-fat cocoa solids, which contain a high content of polyphenols, flavonoids, and alkaloids like theobromine. Famous for its intense color, bitter-sweet taste, and antioxidant activity, cocoa powder comes in natural and alkalized (Dutch-processed) grades, each with distinctive taste profiles and functional characteristics.
Cassava starch or tapioca starch is a white, odorless, fine powder extracted from the cassava plant's roots (Manihot esculenta). Cassava starch has diverse applications in food, pharmaceutical, textile, paper, and adhesives industries because of its unbeatable thickening, gelling, binding, and stabilizing properties. In the food industry, cassava starch finds its applications in bakery, confectionery, dairy, beverages, and gluten-free foods as a substitute for wheat and corn-based starches.
The global vegan yogurt market was valued at USD 3.40 Billion in 2024 and is projected to reach USD 12.21 Billion by 2033, growing at a CAGR of 14.51% from 2025 to 2033. This expansion is marked by ongoing innovation, enhanced consumer personalization, and a deeper commitment to sustainability.
The guacamole market is experiencing a notable change, primarily fueled by an increasing consumer preference for healthy, convenient, and natural food choices. In 2024, the market was valued at USD 1379.9 Million. Guacamole is a creamy avocado-based dip originating from Mexican cuisine has grown into a globally popular food product recognized for its nutritional value and versatility.
Corn starch tableware is a new and ecofriendly solution to traditional plastic disposable items, which aims at solving the increasing environmental issues linked to plastic waste. Comprising mostly of corn starch, a plant-based and renewable resource, the products range from plates, bowls, cups, cutlery, and food containers, all of which are completely biodegradable and compostable.
Artificial Intelligence (AI) is transforming India's beer market at a rapid pace by balancing art with advanced technology. Right from brewing to branding, AI makes fermentation precise, temperature adjustment accurate, and ingredient control efficient, guaranteeing consistent quality and innovation in taste.
Soybean oil is a major vegetable oil used as food obtained from the seeds of the soybean crop. It ranks among the world's most significant edible oils, widely utilized in the preparation of foods, processed food items, industrial purposes, and increasingly in biofuels. High in polyunsaturated fats, especially omega-6 fatty acids, soybean oil has applications in non-food industries such as the production of biodiesel, cosmetics, naphthas, and lubricants.
A bun is a small, round or oval-shaped, soft-textured bread product that can be slightly sweet or savory in taste. Made chiefly of wheat flour, yeast, sugar, salt, water, and fat, buns are found in most cuisines around the globe.
The global dairy market is presently experiencing a profound transformation. This is largely accredited to the strategic integration of artificial intelligence (AI), a technology poised to redefine established paradigms of efficiency and innovation within the industry.
People’s relationship with food is undergoing a profound transformation. No longer just a source of fuel, what individuals eat is now seen as a cornerstone of the overall well-being—a tool to boost immunity, sharpen focus, support digestion, and build long-term resilience. This evolution in consumer consciousness is creating a powerful demand for foods that are functional, organic, and transparently made with real ingredients.
Tequila, once confined to regional consumption in Mexico, has now become a popular spirit worldwide, known for its rich heritage, skilled craftsmanship, and premium quality. Made from blue agave, tequila has attracted international consumers for its distinct flavor, artisanal qualities, and cocktail versatility.
Avocado oil is a nutritious oil pressed from the pulp of avocados (Persea americana), in contrast with most oils, which are seed derived. Avocado oil is valued for its rich content of monounsaturated fats, especially oleic acid, in addition to necessary vitamins like E, A, and D. Avocado oil has a mild, buttery taste and very high smoke point and is used both in food preparation and cosmetics.
Biscuits are dry, baked foods made from flour and usually crisp in texture and flat in shape, eaten frequently as a snack or with a meal. They consist mostly of wheat flour, sugar, fat (butter or vegetable oil), and leavening agents such as baking powder. Flavors and variety may be added using ingredients like milk solids, chocolate, spices, or dried fruits. Biscuits come in sweet and savory forms, varying from cookies and cream-filled to salted crackers. Their shelf life, which is lengthy, convenient packaging, and broad taste appeal have made them a household staple, school staple, and workplace staple worldwide.
Nutritional powders have become essential nutritional supplements created to address the specific health needs of vulnerable demographics, including diabetic patients, the aged, and the sick. When regular food intake is inadequate or compromised, these powders, which are made with specially designed compositions and are high in vital vitamins, minerals, protein, and carbs, offer balanced nourishment. Specialized baby formulas guarantee the best possible growth and development in the early years of life.
Vegetable oils remain among the world’s most widely used agricultural products, essential to food manufacturing, biofuels, cosmetics, and industrial goods.
Learn key financial strategies, operational and capital cost planning essentials for starting a profitable livestock feed production business in 2025.
World Tea Day, celebrated every year on May 21st, is an opportunity to appreciate the rich history, cultural significance, and economic impact of tea. From its origins in ancient China to its status as a global commodity, tea continues to connect people, cultures, and economies.
Mango pulp is the thick, smooth, and semi-liquid product yielded by crushing or pulping ripened mangoes. It is the inner flesh of the mango fruit extracted, without the skin and seeds. Mango pulp is widely utilized as a base for many food items, including mango juice, nectar, drinks, smoothies, ice creams, desserts, and as a topping for pancakes or yogurt. Mango juice is a cool drink prepared from ripe mangoes' juice. To make mango juice, the ripe mangoes are normally peeled, pitted, and the flesh of the mango is squeezed to get the pulp. The pulp is further treated to remove the juice from any remaining fibers or solids.
Soy sauce is a liquid condiment used extensively in cooking and seasoning food. Produced from fermented soybeans, wheat, salt, and water, it provides a deep umami taste that can be used to enhance different foods. It is a common ingredient in Asian cooking and has become popular worldwide in marinades, stir-fries, dips, and processed foods. Come in various forms including light, dark, and low-sodium, soy sauce meets the different consumer tastes and nutritional requirements, rendering it a vital ingredient in the food industry.
Instant coffee is a quick and easy-to-brew coffee beverage that is produced by brewing coffee beans into a liquid that concentrates and evaporates into powder or grain form. It rapidly dissolves in hot water, so it's highly sought after by customers demanding fast and easy coffee brewing. It has a long storage life and is inexpensive, making it popular in homes, offices, and food service establishments. It is fueled by urbanization, hectic lifestyles, and growing demand for convenience drinks.
Glucose syrup and sorbitol syrup are versatile sweeteners widely used across the food and beverage industry. Their ability to enhance texture, retain moisture, and extend shelf life makes them essential ingredients in confectionery, bakery, dairy, and beverage products. Beyond their functional benefits, these syrups contribute to taste enhancement and product stability, catering to consumer preferences for smooth, consistent formulations.
Potato flakes are a highly adaptable food ingredient created by processing cooked potatoes into thin, dehydrated slices. They are often used in soups, snacks, baked goods, and fast meals and are well-known for their usefulness, taste, and simplicity of usage. These flakes provide a reliable and effective option for home cooking, foodservice, and commercial food production while preserving the natural flavour, texture, and nutritional value of fresh potatoes. They are indispensable in a variety of culinary applications due to their lengthy shelf life, lightweight design, and easy rehydration method. Their ability to be used in a variety of recipes, from thickened stews to crispy coatings, further solidifies their position as a basic component of the world's food industry.
Industrial enzymes are biological catalysts that fast-track the chemical process that is involved during the industrial processes. Their use is mainly seen in the food and beverage, pharmaceutical, textile, biofuel, and detergent industries. This enzyme is very effective as it is energy efficient and has cleaner and greener production. Its stability and specificity make it a wonderful tool for breaking complex molecules while improving product quality and yield. Industrial enzymes can enhance the texture of bread, benefit dairy processing, assist in the production of biofuels, and clean wastewater. All these phenomena illustrate that industrial enzymes are a mandatory requirement to manufacture many more products with sustainability and cost effectiveness for multiple industries.
Sorbitol is a sugar alcohol widely used as a sweetener, humectant, and stabilizer in food, pharmaceuticals, and cosmetics. It is made commercially by hydrogenating glucose and is naturally present in fruits like apples and pears. Because of its mild sweetness, low glycaemic index, and ability to retain moisture, sorbitol is a popular ingredient in skincare, dental care, and sugar-free goods. It is also an essential component of industrial processes and a laxative in medical applications.
Inedible beef tallow, a byproduct of the meat processing industry, is derived from beef suet and serves various industrial and commercial purposes. This versatile substance undergoes rendering, a process that separates the fat from solid components. Inedible beef tallow's primary application is in animal feed, as it provides essential fats and energy for livestock, particularly in pet food and livestock supplements. Additionally, it finds use in the cosmetics and personal care industry, contributing to the production of candles, soaps, and skin-care products.
Vitamin C supplements are typically made by extracting ascorbic acid from various sources, such as citrus fruits, or synthesizing it in a laboratory setting. The extracted or synthesized ascorbic acid is then processed and formulated into different types of supplements, including tablets, capsules, chewable, and powdered forms. One of the primary advantages of Vitamin C supplements is their ability to support a healthy immune system.
Over the recent decade, the online food and grocery delivery business in India has witnessed exponential growth. This expansion is attributed to the increasing penetration of smartphones, the affordability and convenience offered by food delivery app services, and the growing availability of low-cost internet services. The industry has become progressively competitive, with numerous local and international players competing for a significant market share. Nonetheless, despite the extreme competition, global players are continuing to make significant investments in India on account of its significant market share in the global online food delivery market.
‘World Food Day’ is celebrated on October 16th as a global responsibility to abolish hunger. 2024’s theme for the day is ‘Right to foods for a better life and a better future’. This theme highlights the significance of enabling access to nutritious food for all, particularly in the face of global challenges, including poverty, climate change, and conflict. In line with this theme, in October 2024, India and the United Arab Emirates (UAE) announced plans for developing a food corridor between the two nations, with an initial investment of over USD 2 Billion (INR 17,000 Crore) in food processing and logistics for food parks. This project significantly reinforces the UAE's food security while providing support to Indian farmers. The initiative is part of a bigger investment strategy targeting over USD100 Billion across key sectors, including manufacturing, infrastructure, and logistics.
A vegan, or a plant-based diet, focuses mainly on consuming fruits, vegetables, grains, legumes, nuts, and seeds. It excludes all animal-derived products and ingredients, including meat, poultry, fish, dairy, eggs, and honey. Nowadays, people are shifting toward vegan diets for a variety of reasons, such as ethical concerns for animal welfare, environmental sustainability, health benefits, and personal preferences.
Functional foods promote overall well-being and offer specific health benefits beyond daily nutrient intake. These benefits encompass enhanced bone health, effective cholesterol management, improved heart health, and eye health. Functional foods include probiotic yoghurt, omega-3 enriched eggs, fortified milk, antioxidant-rich berries, and functional beverages.
Fusion cuisine and beverages blend different ingredients, flavors, or techniques from various culinary or cultural backgrounds to create unique and innovative flavor profiles in dishes and drinks. Fusion beverages encompass both alcoholic and non-alcoholic options, including cocktails, mocktails, smoothies, teas, and more. These beverages span a spectrum from simple combinations to complex and inventive concoctions. Changing taste preferences and global connectivity are the main reasons for the increasing adoption of fusion beverages. They are available in various product types, such as carbonated drinks, fused teas and coffees, fruit juices, fusion alcoholic beverages, energy drinks, sports drinks, and more. These beverages are accessible through off-trade outlets (hypermarkets, supermarkets, discounters, grocery stores, off-license stores, alcohol and confectionery stores, highly specialized retailers, and online stores), as well as on-trade establishments (pubs, bars, cafés, restaurants, clubs, discos, hotels, mass events, and others). Examples of fusion beverages include fruit-infused tea, Asian-inspired cocktails, spicy margaritas, bubble tea creations, mojito variations, and infused waters. Furthermore, fusion cuisine merges elements from diverse culinary traditions, such as Asian, European, African, or Latin American, to craft new and exciting dishes. Examples of fusion cuisine include sushi burritos, Thai basil pizza, kimchi tacos, and more.