Used Oil Recycling Plant Setup Cost in India: Process Flow, Machinery, DPR & Financial Model 2026
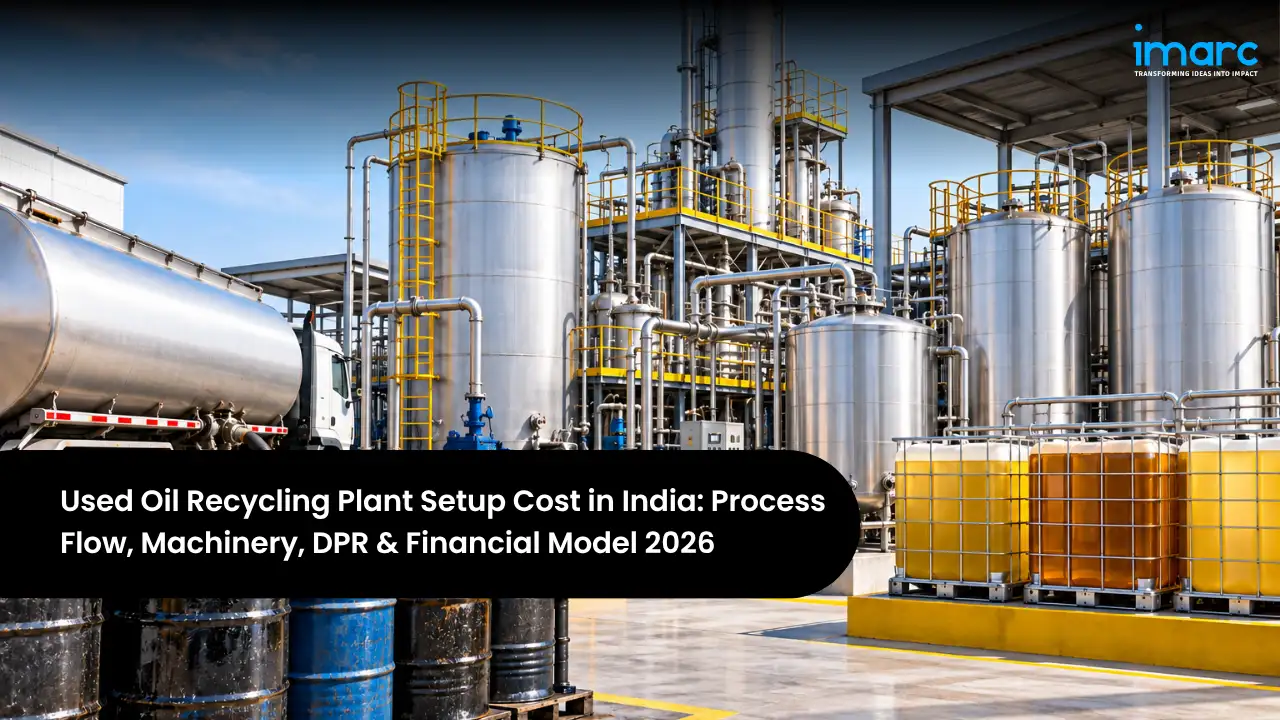
Every year, India's vehicles, machinery, and industries consume around 3 million tonnes of lubricants, making the country one of the world's largest lubricant markets. Once used, these oils are classified as hazardous waste. Much of the collected used oil has historically been burned as low-grade fuel or handled informally, causing pollution and wasting a valuable resource. Re-refining can turn used oil back into high-quality base oil that can be blended into new lubricants again and again. Since April 2024, Extended Producer Responsibility rules have required lubricant producers and importers to ensure that a rising share of used oil is re-refined, creating assured demand for registered recyclers. This makes Used Oil Recycling Manufacturing Plant Setup in India a timely, policy-backed opportunity in the circular economy.
Investment depends on capacity, the re-refining technology, and the quality of base oil produced. Older acid–clay processes are low in cost but generate hazardous acid sludge and are being discouraged. Modern plants use dehydration, vacuum distillation, thin-film or wiped-film evaporation, and finishing by hydrotreating, solvent extraction, or clay polishing. The Used Oil Recycling Manufacturing Plant Cost ranges from about INR 10–40 crore for a vacuum distillation plant of 10,000 to 20,000 kilolitres a year to INR 150–400 crore for a large hydrotreating plant producing higher-grade base oils. Used oil feedstock is the largest single cost, followed by energy and collection logistics, so collection networks, yield, and product quality are the decisions that shape profitability, alongside revenue from EPR certificates. At healthy utilisation, a well-run plant can deliver a gross margin of 20 to 28% and a net profit margin of 7 to 14%.
This guide is written for investors trying to understand how to start a Used Oil Recycling manufacturing plant in India. It covers the main products and their markets, the regulatory drivers, the process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, the approvals involved, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| India Lubricant Demand | About 3 Million Tonnes a year |
| Re-Refined Base Oil Produced (2022) | About 27 kilotonnes, under 1% of lubricant sales |
| Registered Re-Refining Units | Over 400, widely dispersed |
| EPR Rules Effective From | April 1, 2024 |
| EPR Re-Refining Target | 5% in 2024-25, rising to 50% by 2030-31 |
| Indicative Total Investment | INR 10–400 Crore |
The snapshot shows a large lubricant market with a very small formal re-refining output and a rapidly rising regulatory requirement. Although India has hundreds of re-refining units and substantial theoretical capacity, actual production of re-refined base oil has been very low because of fragmented collection, informal diversion of used oil to fuel, and quality limitations. EPR targets that rise to 50% by 2030-31 are designed to change this. The wide investment range reflects a genuine choice between a mid-sized vacuum distillation plant producing Group I base oils and a large hydrotreating plant producing higher-quality base oils for premium lubricant blenders. The sections below work through that choice.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Re-refined base oils, light fuel oil, asphalt extender, and EPR certificates |
| Total Project Investment | INR 10 – 400 Crore (technology and scale dependent) |
| Payback Period | 3 – 5 Years |
| Net Profit Margin | 7 – 14% |
| IRR | 16 – 24% |
| Preferred States | Gujarat, Maharashtra, Haryana, Uttar Pradesh, Tamil Nadu, Telangana |
| Key Approvals | SPCB consents, hazardous waste authorisation, CPCB EPR registration, PESO license |
| Key Requirement | Reliable used oil collection and environmentally sound technology |
These ranges provide a realistic frame for early planning, but actual returns depend on the cost and quality of used oil collected, base oil yield, the grade of base oil produced, energy costs, EPR certificate prices, and success in selling to lubricant blenders. A site-specific Used Oil Recycling Feasibility Report narrows each of these assumptions to your chosen technology, capacity, collection region, and customers.
Table of Contents
- What is Used Oil Recycling?
- Why is Used Oil Recycling Manufacturing Growing in India?
- Used Oil Recycling Manufacturing Process Flow
- Raw Materials Required for Used Oil Recycling Manufacturing
- Location, Land & Infrastructure
- Used Oil Recycling Manufacturing Machinery and Equipment
- Used Oil Recycling Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Used Oil Recycling Manufacturing in India
- Recent Developments in the India Used Oil Recycling Manufacturing Industry
- How a Used Oil Recycling Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Used Oil Recycling?
Used lubricating oil loses its usefulness not because the base oil wears out, but because it becomes contaminated with water, fuel, dirt, metal particles, oxidation products, and spent additives. Re-refining removes these contaminants and recovers the base oil. Typically, the used oil is dehydrated to remove water and light fuel, distilled under vacuum to separate clean lube oil fractions from heavy residues, and then finished by hydrotreating, solvent extraction, or clay treatment to remove remaining sulphur, nitrogen, and colour bodies. The resulting re-refined base oil can be blended with additives to make new lubricants. Good feedstock control, vacuum distillation performance, and effective finishing determine base oil yield and quality.
Commercially, the business combines a recycling service with base oil production. A Used Oil Recycling Manufacturing Plant collects used oil from workshops, fleet operators, factories, and authorised collectors, sells re-refined base oils to lubricant blenders and manufacturers, sells by-products such as light fuel oil and asphalt extenders, and generates EPR certificates that lubricant producers and importers buy to meet their obligations. EPR certificate income has become an important part of the economics of compliant re-refiners.
- Lubricant Blenders: Re-refined base oil for automotive, industrial, and process lubricants.
- Lubricant Producers & Importers: EPR certificates to meet re-refining obligations.
- Fuel & Energy Users: Light fuel fractions recovered during dehydration and distillation.
- Road & Construction Sector: Distillation residue used as asphalt extender or bitumen modifier.
The Main Products and Technologies
Choosing the re-refining technology and product quality is the most important commercial decision, because it determines capital cost, yield, base oil grade, and customers:
| Product / Technology | Description | Key Property | Primary Demand |
|---|---|---|---|
| Vacuum Distillation + Clay Finishing | Distillation with clay polishing | Moderate capex, Group I oils | General lubricant blenders |
| Thin-Film / Wiped-Film Evaporation | Short residence time distillation | Less thermal cracking, better yield | Mid-grade base oils |
| Hydrotreating | Hydrogen finishing of distillates | Low sulphur, Group II-quality oils | Premium lubricant makers |
| Solvent Extraction | Removal of aromatics with solvents | Improved colour and stability | Quality-focused blenders |
| By-Products & EPR Certificates | Light fuel, asphalt extender, certificates | Additional revenue streams | Fuel users, road sector, producers |
These choices shape the whole plant. Vacuum distillation with clay or solvent finishing is the most common route for mid-sized plants and produces Group I base oils suitable for many lubricants. Hydrotreating requires hydrogen supply and much higher capital but produces low-sulphur base oils that meet the needs of modern engine oils and command premium prices. Many new entrants start with vacuum distillation and wiped-film evaporation with a clean finishing step, then consider hydrotreating as volumes, feedstock quality, and customer demand for higher-grade oils grow.
Why is Used Oil Recycling Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
Growth is driven mainly by regulation, supported by resource and environmental benefits:
- EPR obligations: Lubricant producers and importers must meet re-refining targets that rise from 5% in 2024-25 to 50% by 2030-31.
- Large lubricant market: India’s large and growing vehicle fleet and industrial base generate substantial volumes of used oil.
- Import substitution: Re-refined base oil reduces reliance on imported base oils and crude-derived products.
- Environmental protection: Proper recycling prevents used oil from being burned as dirty fuel, dumped, or used to adulterate fuels.
- Sustainability goals: Lubricant brands and industrial users increasingly seek recycled content and circular solutions.
India-Specific Market Opportunity
| Segment | India Market Context | Manufacturing Role |
|---|---|---|
| Lubricant Producers & Importers | Rising EPR obligations | EPR certificates from re-refining |
| Lubricant Blenders | Large base oil demand | Re-refined base oil supply |
| Automotive Workshops & Fleets | Large, dispersed used oil sources | Organised collection services |
| Industries & Utilities | Hydraulic, turbine, and process oils | Collection and re-refining |
| Road & Fuel Markets | Demand for asphalt extenders and fuels | By-product sales |
The strongest opportunity lies in building an organised, compliant collection network in a high-density region and pairing it with clean, efficient re-refining technology. Producers need credible EPR certificates, and blenders need consistent base oil quality, so plants that can deliver both, with transparent documentation, are well placed as EPR targets rise sharply over the coming years.
Used Oil Recycling Manufacturing Process Flow
Understanding the process helps you plan equipment, safety systems, and where yield and quality are decided. Re-refining runs from used oil collection and testing through pre-treatment, dehydration, vacuum distillation, finishing, and fractionation, with by-products recovered along the way. Feedstock testing, vacuum performance, and finishing quality determine base oil yield and grade.
The Used Oil Recycling Manufacturing Process Flow
The sequence below reflects a modern vacuum distillation plant with wiped-film evaporation and hydrotreating or clay finishing. Simpler plants may use clay polishing only, while advanced plants add hydrotreating and fractionation into multiple base oil grades.
| Unit Operation | Key Activity |
|---|---|
| Collection & Receipt Testing | Used oil tested for water, chlorine, and contaminants |
| Storage & Settling | Oil stored and settled to remove free water and sludge |
| Pre-Treatment & Filtration | Solids removed and oil conditioned |
| Dehydration & Light Ends Removal | Water and light fuel fractions flashed off |
| Vacuum Distillation / Wiped-Film Evaporation | Lube fractions separated from heavy residue |
| Finishing (Hydrotreating, Solvent, or Clay) | Sulphur, colour, and impurities removed |
| Fractionation | Base oil separated into viscosity grades |
| Quality Testing | Viscosity, flash point, colour, and sulphur tested |
| By-Product Handling | Light fuel and asphalt extender stored and sold |
| Storage, Dispatch & EPR Reporting | Products dispatched; quantities reported for EPR |
Two factors decide profitability across this flow. The first is base oil yield and quality: careful feedstock selection, effective dehydration, and deep vacuum distillation with minimal thermal cracking maximise the share of used oil recovered as saleable base oil, while good finishing determines the grade and price. The second is energy and environmental performance, because distillation and finishing consume significant heat and power, and residues and wastewater must be handled safely; heat integration, efficient vacuum systems, and clean finishing technologies reduce costs and simplify compliance.
Raw Materials Required for Used Oil Recycling Manufacturing
The main input is used lubricating oil from engines, gearboxes, hydraulic systems, turbines, and industrial machinery. Depending on the technology, the plant also uses hydrogen and catalysts for hydrotreating, solvents for extraction, or bleaching clay for polishing, along with chemicals for pre-treatment and wastewater treatment. Because feedstock quality and supply drive both yield and cost, a reliable, well-documented collection system is central to project planning.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Used Lubricating Oil | Main feedstock | Workshops, fleets, industries, collectors | 30–38% |
| Hydrogen & Catalysts / Clay / Solvents | Finishing of base oil | Domestic suppliers or on-site generation | 2–4% |
| Pre-Treatment & ETP Chemicals | Conditioning and wastewater treatment | Domestic suppliers | 1–2% |
| Packaging & Drums | Product dispatch | Domestic suppliers | 1–2% |
Used oil is generated across thousands of workshops, fleet depots, factories, and power plants, so collection is the most challenging part of the business. Informal buyers who sell used oil as fuel have often paid competitive prices, but EPR rules are steadily formalising the market. Registered collection agents, contracts with fleet operators, industrial generators, and lubricant brands' service networks, and transparent testing and pricing all help secure steady, good-quality feedstock. Segregating automotive and industrial oils, and keeping out contaminants such as chlorinated solvents, improves yield and protects equipment.
Location, Land & Infrastructure
Site selection for a re-refining plant is shaped by the density of used oil generation within an economic collection radius, proximity to lubricant blenders, access to industrial areas where hazardous waste recycling can be approved, reliable power and fuel, and availability of hydrogen if hydrotreating is planned.
Choosing the Best Location for Used Oil Recycling Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Gujarat (Ankleshwar, Vapi & Dahej) | Large industrial base and chemical estates | Feedstock, approvals infrastructure, ports |
| Maharashtra (Taloja & Pune) | Major vehicle fleets and industries | Feedstock and lubricant blenders |
| Haryana & Delhi-NCR | Dense vehicle population and logistics hubs | High used oil generation |
| Uttar Pradesh | Large transport and industrial base | Feedstock and northern markets |
| Tamil Nadu (Chennai region) | Automotive manufacturing and fleets | Feedstock and southern blenders |
| Telangana (Hyderabad region) | Growing industry and logistics | Land and central location |
Gujarat and Maharashtra offer large industrial and transport bases, established chemical estates with infrastructure for hazardous waste processing, and proximity to lubricant blenders and ports. The Delhi-NCR region, Uttar Pradesh, and Tamil Nadu generate large volumes of automotive used oil from dense vehicle populations and fleets, while Telangana provides a central location for southern and central India. The final choice should weigh collection density, blender proximity, approval timelines, and utilities.
Environmentally Sound Technology and Quality
Regulators expect re-refiners to use environmentally sound technology that avoids hazardous acid sludge, controls emissions, and safely manages residues and wastewater. A credible plant needs closed handling of used oil, vacuum systems with vapour treatment, safe management of distillation residues, an effluent treatment plant, and fire safety systems suited to petroleum products. Lubricant blenders expect consistent base oil specifications backed by laboratory testing. An experienced Used Oil Recycling Manufacturing Consultant in India can help select compliant technology, design collection and quality systems, and navigate registration and EPR processes so the plant operates smoothly and earns certificate revenue from the start.
Infrastructure Requirements (Mid-Sized Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 3 – 10 acres | Space for tank farm and safety distances |
| Tank Farm | Used oil, product, and by-product storage | PESO-compliant layout |
| Process Plant | Dehydration, distillation, finishing | Vacuum and heating systems |
| Thermic Fluid Heaters & Utilities | Process heat, cooling, compressed air | Efficient fuel use |
| ETP & Residue Handling | Wastewater and residue management | Critical for consent |
| Power Requirement | 0.5 – 3 MW | Stable supply with backup |
| Laboratory & Weighbridge | Feedstock and product testing | Supports EPR documentation |
A tank farm laid out to petroleum safety rules, a process plant with dehydration, vacuum distillation, and finishing, thermic fluid heating, an effluent treatment plant, and a laboratory are the defining infrastructure needs. Accurate weighing and documentation of every incoming and outgoing load are essential, since EPR certificates depend on verified quantities.
Used Oil Recycling Manufacturing Machinery and Equipment
The equipment set covers receipt and storage, pre-treatment, dehydration, vacuum distillation, finishing, fractionation, utilities, and environmental systems. Distillation units, evaporators, vacuum systems, and finishing equipment account for most of the machinery budget. The main items are summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Receiving & Storage Tanks | Store used oil and products | Heated, PESO-compliant |
| Decanters, Centrifuges & Filters | Remove water and solids | Continuous separation |
| Dehydration Column & Flash Drum | Remove water and light ends | Controlled heating |
| Vacuum Distillation Column | Separate lube fractions | Deep vacuum operation |
| Thin-Film / Wiped-Film Evaporator | Distil with minimal cracking | Short residence time |
| Vacuum System | Maintain low pressure | Steam ejectors or vacuum pumps |
| Hydrotreating Reactor or Clay / Solvent Units | Finish base oil | Technology-specific design |
| Thermic Fluid Heaters & Heat Exchangers | Provide and recover heat | Heat integration |
| Fractionation & Blending Tanks | Separate and blend grades | Accurate product control |
| ETP & Vapour Treatment | Treat wastewater and off-gases | Meets discharge norms |
| Quality Control Laboratory | Test feedstock and products | Viscosity, flash point, sulphur, colour |
Machinery should follow the technology and capacity plan. Wiped-film evaporators improve yield and quality by reducing thermal cracking, while hydrotreating adds reactors, hydrogen supply, and gas treatment but produces superior base oils. Good heat integration, reliable vacuum systems, and automated controls reduce energy use and improve consistency across varying feedstock.
Used Oil Recycling Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a mid-sized used oil re-refining plant in India. The final Used Oil Recycling Investment Cost for your project will depend on capacity, re-refining technology, finishing route, tank farm size, environmental systems, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Plant & Machinery | 45–55% | Dehydration, distillation, evaporation, finishing |
| Tank Farm & Piping | 10–15% | Feedstock, product, and by-product storage |
| Utilities & Heating Systems | 6–10% | Thermic fluid heaters, cooling, power |
| Environmental & Safety Systems | 6–10% | ETP, vapour treatment, fire protection |
| Land & Civil Works | 8–12% | Land, foundations, buildings, roads |
| Collection Fleet, Lab & Pre-operative | 4–7% | Tankers, testing, DPR, commissioning |
| Working Capital | 8–12% | Feedstock stocks and receivables |
Process machinery and the tank farm dominate the capital budget, while environmental and safety systems are significant because the plant handles hazardous waste and petroleum products. Working capital is needed for feedstock stocks, products in storage, and receivables from blenders and certificate buyers. A detailed Used Oil Recycling Business Plan should model feedstock collection costs, base oil yield and prices, EPR certificate volumes and prices, by-product revenue, and payment terms together, so that funding matches the real cash cycle of the business.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Raw Materials (used oil, finishing inputs) | 35–45% | Feedstock price affected by informal demand |
| Utilities (fuel, power, steam) | 18–25% | Distillation and finishing are energy-intensive |
| Collection & Logistics | 8–12% | Tankers and collection network |
| Labour & Technical Staff | 6–9% | Operators, chemists, and collection staff |
| Environmental & Compliance | 4–6% | ETP, residue handling, and EPR reporting |
| Maintenance & Overheads | 4–6% | Equipment upkeep and administration |
With feedstock, energy, and collection logistics making up most of the cost, margins depend on securing used oil at reasonable prices, maximising base oil yield, and operating efficiently. A good operating model tracks feedstock cost per kilolitre, base oil yield, energy use per kilolitre, collection cost per kilolitre, and certificate revenue, and tests how margins respond when feedstock prices rise, when base oil prices fall with crude oil, or when certificate prices change.
Financial Analysis and Profitability
Based on analysis of a mid-sized re-refining plant, the financial profile is attractive for compliant operators, supported by mandatory EPR demand, a large feedstock pool, and multiple revenue streams. The profitability of the Used Oil Recycling manufacturing business in India improves markedly with a strong collection network, high base oil yield, higher-grade finishing, efficient energy use, and steady EPR certificate sales to lubricant producers.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 20–28% | Supported by EPR certificate income |
| Net Profit Margin | 7–14% | After depreciation and Indian corporate taxes |
| Payback Period | 3–5 Years | Faster with assured feedstock |
| IRR (Internal Rate of Return) | 16–24% | Higher with hydrotreated base oils |
| Capacity Utilization (stable ops) | 60–85% | Depends on collection success |
| Break-even Capacity Utilization | 40–50% | Moderate fixed costs |
Feedstock access and product quality decide where a plant lands within these ranges. Plants that secure steady used oil supply can run at high utilisation and spread fixed costs, while those competing with informal buyers for scattered feedstock struggle to fill capacity. Higher-grade base oils sell at better prices, and EPR certificates add a valuable income stream, although certificate prices depend on how the market develops as targets rise.
Returns can be strengthened by building collection partnerships with fleets, industries, workshops, and lubricant brands, investing in wiped-film evaporation and hydrotreating for better yield and quality, selling by-products effectively, integrating heat recovery, and maintaining transparent documentation that makes certificates attractive to producers. Consistent base oil quality and reliable compliance are what earn long-term relationships with lubricant companies.
Key Risks and Mitigation
The main risks are feedstock competition from informal buyers, variable feedstock quality, base oil price movements linked to crude oil, uncertainty in EPR certificate prices, and environmental or safety incidents. Feedstock risk is reduced through collection contracts and partnerships; quality risk by testing and segregation; price risk by long-term offtake with blenders; certificate risk by agreements with producers; and environmental risk by compliant technology and strong safety systems. Promoters often work with a Used Oil Recycling Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for Used Oil Recycling Manufacturing in India
Approvals for a re-refining plant centre on hazardous waste rules, EPR registration, and petroleum safety, alongside environmental and industrial permissions. Promoters setting up a Used Oil Recycling Manufacturing Plant in India generally need the following:
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, with conditions for emissions, effluents, and residues.
- Hazardous Waste Authorisation: Authorisation for collection, storage, and recycling of used oil under the Hazardous and Other Wastes Rules, using environmentally sound technology.
- CPCB EPR Registration: Registration as a recycler on the CPCB EPR portal to process used oil and generate EPR certificates, with regular reporting.
- Petroleum Storage License: PESO license for storage of petroleum products and adherence to safety distances.
- Environmental Clearance: Environmental clearance where applicable to the process and capacity.
- Factory, Boiler & Fire Approvals: Factory license, boiler registration where applicable, and a Fire NOC.
- Business & Tax Registration: Company incorporation, GST, Udyam, and EPF and ESI registrations.
Pollution consent, hazardous waste authorisation, and PESO approval are usually on the critical path, and EPR registration is needed before the plant can generate certificates. Collection agents working for the plant must also be properly registered. Planning technology approval, safety design, and EPR documentation alongside construction shortens the time to full commercial operation.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, re-refining technology, products, collection arrangements, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Used Oil Recycling Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- EPR now in force: Extended Producer Responsibility for used oil took effect on April 1, 2024, under amendments to the Hazardous and Other Wastes Rules.
- Rising targets: Producers must ensure re-refining of 5% of oil sold in 2024-25 and 10% in 2025-26, rising progressively to 50% from 2030-31.
- Certificate market structure: EPR certificates are traded through the CPCB portal, with minimum and maximum prices linked to environmental compensation for non-compliance.
- Large capacity gap: India produced only about 27 kilotonnes of re-refined base oil in 2022, under 1% of lubricant sales, despite much larger installed capacity.
The common thread is a market being transformed by regulation, with demand for compliant re-refining set to rise sharply. New entrants who build reliable collection networks, use clean and efficient technology, and produce consistent base oil will be best placed as EPR targets increase through the decade.
How a Used Oil Recycling Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from feedstock availability and technology selection to plant design, collection logistics, approvals, and economics. It helps investors decide the right technology, capacity, and collection region, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Used Oil Recycling Financial Model covering feedstock collection volumes and costs, base oil yield and prices, by-product revenue, EPR certificate volumes and prices, energy and logistics costs, working capital, cash flows, break-even, return on investment, and payback. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a Used Oil Recycling Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a re-refining project, a strong DPR also clarifies the collection strategy, the technology and product quality plan, the EPR certificate approach, and the environmental and safety design, which together are the factors most likely to decide success. By testing margins against feedstock competition, crude-linked base oil prices, and certificate price scenarios, the report turns a regulation-driven opportunity into a plan that lenders and partners can trust.
Frequently Asked Questions
What are the first steps to set up a used oil recycling manufacturing plant in India?
Start by assessing used oil availability in your target region and choosing your technology, capacity, and products. Then commission a feasibility study and DPR, secure land in an industrial area, obtain pollution consent, hazardous waste authorisation, and PESO approval, build the tank farm, process plant, and environmental systems, set up collection arrangements, register on the CPCB EPR portal, and build relationships with lubricant blenders and producers.
How much does it cost to set up a used oil recycling manufacturing plant in India?
Investment ranges from about INR 10–40 crore for a vacuum distillation plant of 10,000 to 20,000 kilolitres a year to INR 150–400 crore for a large hydrotreating plant producing higher-grade base oils. Process machinery, the tank farm, environmental systems, and working capital are the largest components.
What are the main steps in used oil recycling manufacturing?
The flow runs from collection and receipt testing through storage and settling, pre-treatment and filtration, dehydration and light ends removal, vacuum distillation or wiped-film evaporation, finishing by hydrotreating, solvent extraction, or clay, fractionation, quality testing, by-product handling, and storage, dispatch, and EPR reporting.
Which machinery does a used oil recycling manufacturing plant need?
Key equipment includes receiving and storage tanks, decanters, centrifuges and filters, a dehydration column, vacuum distillation columns, thin-film or wiped-film evaporators, vacuum systems, hydrotreating reactors or clay and solvent units, thermic fluid heaters and heat exchangers, fractionation and blending tanks, effluent and vapour treatment, and a quality control laboratory.
What raw materials are used in used oil recycling?
The main input is used lubricating oil from vehicles and industry, together with hydrogen and catalysts, solvents, or bleaching clay for finishing, chemicals for pre-treatment and wastewater treatment, and packaging for products.
How profitable is used oil recycling in India?
A well-run plant typically earns a 20 to 28% gross margin and a 7 to 14% net margin, with payback in 3 to 5 years. Profitability depends on feedstock collection, base oil yield and quality, energy costs, by-product sales, and EPR certificate revenue.
Which approvals does a used oil recycling manufacturing plant need in India?
Typical approvals include State Pollution Control Board consents, hazardous waste authorisation for used oil recycling, CPCB EPR registration as a recycler, a PESO petroleum storage license, environmental clearance where applicable, a factory license and Fire NOC, and GST, Udyam, and labour registrations.
How do I get a feasibility study or DPR for a used oil recycling manufacturing project?
A detailed feasibility study and DPR covers feedstock availability, technology and product strategy, collection logistics, approvals, EPR economics, and full financials. Investors usually engage a Used Oil Recycling Manufacturing Feasibility Study Consultant with experience in petroleum and waste recycling projects to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Indian wine has come a long way from a niche curiosity to a genuine lifestyle category. Young urban consumers, growing interest in food pairing, wine tourism in regions such as Nashik and Nandi Valley, and supportive state grape policies have given domestic wineries room to grow, while producers have steadily improved quality and won international recognition.
Setting up an Extra Neutral Alcohol Manufacturing Plant in India is a fermentation-and-distillation venture anchored to the large and growing alcoholic-beverage industry, along with pharmaceutical, cosmetic, and industrial demand.
Setting up a Shrimp Processing Plant in India is a high-potential, export-oriented venture, powered by the country's position as one of the world's largest shrimp producers and exporters. India's vast coastline, expanding vannamei aquaculture, and strong demand from the United States, China, the European Union, and Japan make a frozen shrimp processing Plant Setup in India one of the most attractive opportunities in the seafood sector.
India's post-pandemic food delivery boom, followed by the new quick-commerce disruption from Zepto Cafe and Swiggy Bolt, has turned the Cloud Kitchen Market in India into a genuine focus of global investor curiosity.
The total addressable market for India's functional beverages is expanding from USD 6.9 Billion in 2025 to a projected USD 18.8 Billion by 2034, growing at a CAGR of 10.74% (2026–2034).
The halal food market has moved well beyond a religious-compliance niche into one of the largest, fastest-growing consumer food categories in the world. The global market was valued at USD 2,956.4 billion in 2025 and is projected to reach USD 6,329.3 billion by 2034, expanding at a compound annual growth rate (CAGR) of 8.56% between 2026 and 2034.
India’s dairy industry is undergoing a structural transformation, driven by rising incomes, urbanization, changing consumption patterns, and strong policy support. Traditionally dominated by an unorganized and cooperative-led system, the sector is now evolving into a more competitive, branded, and technology-enabled ecosystem.
Cheese is a dairy food made by coagulating the proteins in milk, mainly casein, using enzymes, acids, or microorganisms, followed by separating the curds from the whey. Cheese can be made from the milk of cows, buffaloes, goats, sheep, or a combination of these. The coagulated curd is then processed by cutting, cooking, pressing, salting, and aging to achieve desired texture, moisture, and flavor characteristics.
Avocado oil is a vegetable oil that is extracted from the pulp of ripe avocados (Persea americana), unlike other vegetable oils that are extracted from seeds. Avocado oil contains high amounts of monounsaturated fatty acids, specifically oleic acid, as well as phytosterols, tocopherols, and carotenoids. Avocado oil can be classified as extra virgin, virgin, or refined, depending on the extraction and refining process.
Wine is a type of alcoholic drink that is made by the controlled fermentation of grape juice, where the natural or added yeast ferments the sugars in the juice to produce ethanol, carbon dioxide, and other compounds. Wine is made up of water, ethanol, organic acids, phenolic compounds, aromatic esters, and trace minerals.
Whey protein is a high-quality, complete protein obtained from whey, which is the liquid by-product of cheese production. Milk coagulated with enzymes or acids separates into curds (casein) and whey. Whey is a liquid that contains soluble proteins like beta-lactoglobulin, alpha-lactalbumin, serum albumin, and immunoglobulins. Whey is filtered and dried to produce commercial products like whey protein concentrate (WPC), whey protein isolate (WPI), and whey protein hydrolysate (WPH).
Whole egg powder is a dehydrated egg ingredient made by spray drying homogenized liquid whole eggs, which include a mixture of egg yolk and egg white in their natural ratio. Fresh whole shell eggs are broken, filtered, pasteurized, and then processed into a stable powder form using controlled drying methods. The final product preserves the functional and nutritional qualities of fresh eggs, such as high-quality protein, essential amino acids, lipids, vitamins, and emulsifying fractions.
Tea is a drink made from the processed leaves and flower buds of the plant Camellia sinensis. The essential properties of tea, namely flavor, aroma, color, and strength, depend on the level of oxidation, drying, and fermentation of the processed leaves. Tea can be categorized based on the processing techniques into black tea, green tea, oolong tea, white tea, and specialty teas.
Soy milk is a plant-based beverage made from whole soybeans that have been soaked, ground, and their liquid extracted, then cooked and filtered. It is completely devoid of elements originating from animals and is intended to operate and look like dairy milk. In addition to naturally existing proteins, carbs, and healthy fats from soybeans, soy milk is frequently supplemented with vitamins and minerals to improve its nutritional value.
Soya chunks are a protein-rich food item that is prepared using defatted soy flour, which is a by-product of soybean oil extraction. Soya chunks are prepared using the process of extrusion cooking, which converts the soy flour into porous, sponge-like granules with a fibrous structure that resembles meat when rehydrated.
Soya chunks are a protein-rich food item that is prepared using defatted soy flour, which is a by-product of soybean oil extraction. Soya chunks are prepared using the process of extrusion cooking, which converts the soy flour into porous, sponge-like granules with a fibrous structure that resembles meat when rehydrated. Soya chunks have a neutral flavor, which helps them absorb the flavors of spices and seasonings while cooking.
Saudi Arabia’s precast concrete market reached USD 1.2 Billion in 2024 as per the IMARC Group, clear proof that off-site construction is rapidly becoming the Kingdom’s go-to building solution. With residential, commercial, and major infrastructure projects multiplying, developers are increasingly turning to precast building solutions to keep pace.
The global emergency food market has emerged as a critical component of household preparedness infrastructure, disaster response frameworks, and government stockpiling programs worldwide. In March 2025, the National Disaster Response Force (NDRF), established in India, conducted a National Capacity Building Competition for State Disaster Response Forces (SDRFs) to improve their readiness and effectiveness in managing collapsed structure emergencies.
The Saudi Arabia sauces and seasonings market size is expanding steadily as consumers embrace more diverse flavors, convenient food formats, and global culinary influences. Evolving lifestyles, greater exposure to international cuisines, and a strong shift toward home cooking have collectively shaped the contemporary marketplace.
The GCC chocolate market has experienced robust expansion in recent years, driven by evolving consumer preferences, rising disposable incomes, and the proliferation of international brands. In 2024, the GCC chocolate market size reached USD 3,200.77 Million, reflecting sustained growth across premium, artisanal, and mass-market segments.
The Gulf Cooperation Council (GCC) region continues to position itself as one of the fastest-evolving markets for packaged beverages, with bottled water standing at the forefront of this transformation. The GCC bottled water market size has expanded steadily in recent years, supported by a strong shift toward health-driven consumption, improved hydration awareness, and evolving lifestyle patterns across the member countries.
India’s pet sector has experienced a remarkable transformation, driven by urbanization, evolving lifestyles, and a stronger emotional bond between people and their companion animals. What was once a niche trend among a few urban families has now become a widespread practice across Indian households, where pets are regarded as integral members of the family.
Shrimp is one of the world’s most precious natural spices, derived from the dried red stigmas of the Crocus sativus flower. Each bloom yields only a few delicate stigmas, which must be carefully hand-harvested, dried, and processed to preserve their vibrant color, distinctive aroma, and rich flavor. The spice’s deep golden-yellow hue, bitter-sweet taste, and unique fragrance are primarily attributed to its key bioactive compounds like crocin, picrocrocin, and safranal.
The Australian craft beer industry has emerged as a significant segment of the broader alcoholic beverages market driven by evolving consumer preferences, rising disposable incomes, and a growing appreciation for artisanal and premium products. Over the past decade, the market has witnessed substantial expansion with craft breweries increasingly occupying a distinct niche in the highly competitive beer sector.
India is witnessing a profound transformation in how its citizens approach health and wellness. The nutritional supplements market of the country has evolved from a niche segment into a mainstream industry serving millions of health-conscious consumers.
Sea salt is a natural mineral product obtained through the solar evaporation of seawater, followed by harvesting, washing, drying, grading, and packaging. Unlike refined table salt, which undergoes heavy chemical processing, sea salt production relies primarily on solar energy and natural crystallization, allowing it to retain trace minerals such as magnesium, calcium, and potassium that contribute to its distinct taste and nutritional value.
Saffron is one of the world’s most precious natural spices, derived from the dried red stigmas of the Crocus sativus flower. Each bloom yields only a few delicate stigmas, which must be carefully hand-harvested, dried, and processed to preserve their vibrant color, distinctive aroma, and rich flavor.
The India edible oil market stands as one of the most dynamic sectors within the country's consumer goods landscape. As households increasingly prioritize quality, health, and convenience, demand for diverse oil varieties continues to surge. The transformation from traditional purchasing habits to modern retail experiences reflects broader shifts in consumer awareness and lifestyle choices.
India's organic food industry stands at the intersection of health consciousness, agricultural innovation, and sustainable practices. As consumers increasingly prioritize chemical-free nutrition and environmental sustainability, the sector faces transformative opportunities alongside significant operational challenges shaped by evolving dietary preferences, technology adoption in agriculture, and regulatory frameworks that collectively define market dynamics.
Japan’s gluten-free foods and drinks market has evolved into a vibrant segment of the country’s growing health and wellness culture. Once catering mainly to individuals with celiac disease or gluten intolerance, gluten-free products now appeal to a broader demographic pursuing balanced, wellness-oriented lifestyles.
The GCC coconut water market is experiencing remarkable momentum as consumer preferences shift decisively toward natural hydration solutions and functional beverages. This transformation is propelled by heightened health consciousness, expanding fitness culture, and growing awareness of the nutritional benefits associated with coconut-based drinks.
The Saudi Arabia online grocery market is experiencing transformative growth, driven by widespread digital adoption, evolving consumer preferences, and strategic government initiatives aligned with Vision 2030. As one of the fastest-growing e-commerce segments in the Middle East, the online grocery sector is reshaping how Saudi consumers shop for everyday essentials.
Onion powder is a dehydrated and ground seasoning that results from the drying of fresh onions into a concentrated powdered form. The process of dehydration removes moisture from the product, while maintaining the flavor, aroma, and pungency characteristics of the onion, thereby making it a stable and ready-to-use ingredient with a longer shelf life. Onion powder can be prepared through various controlled drying, grinding, and screening processes from white, red, or yellow onion varieties.
Japan's animal feed industry stands as a cornerstone of the nation's agricultural infrastructure, supporting domestic livestock production and ensuring food security. The sector encompasses diverse feed products for cattle, swine, poultry, and aquaculture operations that sustain Japan's protein supply chain.
Nutraceuticals are bioactive, health-enhancing products derived from food sources, botanical ingredients, or purified nutrients that provide physiological benefits beyond basic nutrition. They include dietary supplements, functional foods, fortified beverages, herbal extracts, probiotics, omega-fatty-acid formulations, vitamins, minerals, and specialized nutritional compounds. Nutraceuticals are designed to support wellness, prevent nutrient deficiencies, and promote specific health outcomes, including the improvement of immunity, digestive balance, cognitive function, metabolic health, or cardiovascular support.
India's spice industry stands as a vibrant cornerstone of the nation's agricultural economy and cultural identity. As global consumers increasingly seek authentic flavors and natural ingredients, India's position as the world's leading spice producer continues to strengthen.
According to IMARC Group, India's ice cream consumption has grown nearly fourfold over the past decade. Despite this, India's per-capita consumption stands at just ~400 ml per year — far below the global average of ~2.5 litres. That gap is not a weakness. It is the single most compelling argument for the industry's long-term runway.
Millet represents a group of small-seeded cereals, primarily from the Poaceae family, which are grown as staple foods for thousands of years in Asia and Africa and, increasingly, in other parts of the world. These cereals include pearl millet, foxtail millet, finger millet, proso millet, barnyard millet, and little millet.
Milk powder is a type of dehydrated dairy product, which is manufactured by removing almost all moisture from liquid milk by means of various evaporation and drying techniques. The resultant product is a stable, shelf-friendly powder containing most of the nutritional components of milk, including proteins, lactose, minerals, and fats. Milk powder may be prepared from whole, skimmed, or partially skimmed milk, depending on its intended use. The very low moisture content inhibits microbial growth and spoilage; hence, it becomes more feasible regarding transport, storage, and usage in different formulations.
Meat generally denotes the animal tissues that are consumed and mainly include muscle fibers, though the content of fat, connective tissue, and moisture may vary. There are a number of sources, although they are mainly livestock such as cattle, pigs, sheep, poultry, and, in some regions, game animals.
Australia's tea market is at a crossroads, undergoing extraordinary change inspired by changing consumption habits, health awareness, and the explosion of functional drinks.
The Australia dairy industry stands as a vital pillar of the nation's agricultural economy, representing the third-largest rural sector and contributing significantly to both domestic food security and export earnings.
India has emerged as one of the fastest-growing fisheries producers in the world, backed by rising health awareness, export diversification, and evolving aquaculture technology.
Ice cream is a frozen dairy dessert made by blending milk, cream, sugar, and flavorings, then freezing the mixture while incorporating air to give a smooth, creamy texture. The mixture is pasteurized, homogenized, then churned under controlled conditions to prevent the formation of large ice crystals. Depending on the recipe and product category, it may contain stabilizers, emulsifiers, fruits, nuts, chocolate, or other inclusions. It comes in hardpacked ice cream, softserve, gelato, sorbets, and frozen yogurt. The texture, flavor, and quality of this frozen dessert will depend on the ratios of ingredients used and the techniques followed in processing.
The Philippines mushroom industry is undergoing a transformative phase, driven by a growing consumer shift toward functional and nutrient-dense foods. As health awareness rises across both urban and rural populations, mushrooms are increasingly recognized for their high protein, fiber, and antioxidant content. This change is not merely dietary it reflects a broader movement toward wellness-oriented lifestyles that prioritize natural, sustainable, and locally sourced food options. For agribusiness investors and food manufacturers, this evolution signals significant growth potential in both production and value-added segments of the market.
The Vietnam aquaculture market has transformed from traditional fishing practices into one of the world's most dynamic seafood production sectors. Vietnam now ranks as the fourth-largest aquaculture producer globally, supplying markets across Asia, Europe, and the Americas. Understanding what drives this growth is essential for investors, businesses, and policymakers looking to engage with this evolving industry.
French fries are thin strips of baked or deep-fried potatoes with a fluffy inside and a crispy outside. They originated in Europe and are now a common fast-food staple that is consumed as a snack or side dish in many countries. French fries are made mostly from high-starch potatoes and are produced in large quantities by chopping, blanching, frying, and occasionally freezing. They are among the most well-liked and extensively consumed potato-based food products in the world because of their ability to be seasoned, flavored, or combined with condiments like cheese, mayonnaise, or ketchup.
Glucose powder is a crystalline or powdered form of a simple sugar, glucose, derived mainly from sources of starch: corn, wheat, or rice. Glucose powder is obtained by the hydrolysis of starch into glucose by enzymes, followed by purification and concentration of the solution and its drying to yield a readily water-soluble, easily digested carbohydrate powder. Glucose powder is an instant source of energy as it is quickly absorbed in the body, which makes the product valuable in food, beverage, nutraceutical, and pharmaceutical applications. It has a neutral taste, a very high sweetness index compared to regular sugar, and excellent dissolving properties, making it useful in various industrial formulations and household consumption.
Ghee is a class of clarified butter that, conventionally, is prepared by simmering butter until the milk solids separate and caramelize, leaving a golden, fragrant fat. Presently, it is widely used in South Asian, Middle Eastern, and increasingly global cuisines. Ghee has a high smoke point, long shelf life, and rich flavor, which makes it suitable for cooking, frying, and flavor enhancement. During its production, water and milk proteins are removed, making the product a lactose-free fat that contains fat-soluble vitamins and bioactive compounds. Its stability, purity, and distinctive taste make ghee an important culinary and functional ingredient in both traditional and modern food applications.
Fruit powder is made by removing the moisture content of whole fruits through various methods, such as spray drying, freeze-drying, drum drying, or vacuum drying, to get a finely ground, dehydrated powder form. After drying, the fruit is then milled into a stable, lightweight, and shelf-friendly powder that retains much of the fruit's natural flavor, aroma, nutrients, and color. Fruit powders have the essence of fresh fruit in concentrated, easy-to-handle form and are thus highly versatile in food, beverage, nutraceutical, and cosmetic applications. They offer an alternative to fresh fruits in a more convenient manner with longer shelf life and consistent quality for industrial use.
Garlic powder is the dried form of garlic, made by drying fresh garlic cloves and then grinding them to a uniform powder. Garlic dehydration removes moisture while preserving much of the flavor, aroma, and pungency of garlic. This concentrated form offers longer shelf life, easy storage, and consistent taste compared to fresh garlic. Garlic powder is widely used as a seasoning, marinade ingredient, and flavor enhancer in culinary, industrial, and packaged-food applications. Garlic powder imparts the taste of garlic without peeling or chopping into the dishes; therefore, it is very convenient and versatile for both homes and large-scale food manufacturers.
The Frozen food market is highly diversified, encompassing categories like frozen ready meals, fruits and vegetables, meat, seafood, desserts, and bakery items. This robust growth is fueled by fundamental shifts, including urbanization, the rise of dual-income households, and a consumer demand for convenience without compromising nutritional value. Modern freezing technologies ensure high quality and extended shelf life, addressing the critical issue of food waste.
The United States shrimp market stands as one of the most dynamic segments within the global seafood industry. It reached 983,000 Tons in 2024 as per IMARC Group and is projected to reach 1,280,000 Tons by 2033 at a growth rate of 3% from 2025 to 2033. As consumer preferences shift toward healthier protein sources and sustainable options, shrimp has emerged as a cornerstone of American dietary habits. The market reflects transformations in consumer behavior, international trade dynamics, and technological innovation within aquaculture and seafood processing.
The Australia gluten-free food industry is flourishing, powered by a surge in health-conscious consumers, a rise in gluten intolerance cases, and a growing appetite for clean-label, nutritious products. In 2024, the industry reached a notable milestone, hitting USD 361.20 Million, according to IMARC Group. Popular categories like gluten-free bakery items, snacks, dairy, and ready-to-eat (RTE) meals are leading the charge.
The global frozen food industry has undergone a remarkable transformation over the past decade, evolving from a convenience-focused sector into a sophisticated, technology-driven marketplace that prioritizes quality, nutrition, and sustainability. Innovation serves as the primary catalyst for this evolution, fundamentally reshaping consumer perceptions and market dynamics across all geographic regions.
Egg powder is a type of dehydrated product prepared from whole eggs, egg whites, or egg yolks, using a controlled drying process that removes moisture content while preserving the natural nutrients, flavor, and functional properties in fresh eggs. Originally developed to extend the shelf life of eggs, it was also meant to be convenient and easily transportable for food manufacturing, catering, and military or outdoor purposes.
The global ginger market is currently experiencing a remarkable phase of expansion, positioning itself as one of the most dynamic segments within the spice and functional ingredient industries. As consumers worldwide are increasingly gravitating toward natural, health-promoting ingredients, ginger is emerging as a star performer that is capturing attention across multiple sectors, from culinary applications to pharmaceuticals and nutraceuticals. The market is demonstrating robust momentum that industry analysts are tracking with considerable interest.
Coconut is an important tropical crop with a wide array of uses, and hence it is considered the "Tree of Life." The fruit, leaves, trunk, and roots of coconuts yield a wide range of products. Each part has economic value and, therefore, provides a means of livelihood in many rural communities and agro-industrial development in tropical regions such as Southeast Asia, South Asia, and the Pacific Islands.
Coconut yogurt is a plant-based alternative to traditional dairy, made from the rich milk of mature coconuts. This yogurt boasts the same feel and taste as traditional dairy yogurt, all the while catering to vegans, lactose-intolerant, or allergenic consumers. Manufactured like traditional yogurt, this variety is fermented with live bacterial cultures such as Lactobacillus bulgaricus and Streptococcus thermophilus. These same cultures ferment the natural sugars of the coconut milk into lactic acid during processing, creating a thick consistency and giving it that tangy taste typical of yogurt.
The Australian dog food market is undergoing an important transformation, motivated mainly by advancements in AI technology. As more people own pets, they increasingly demand more tailored and nutritious options for dogs. Both technology and artificial intelligence (AI) are important to facilitate this, and reshaping the industry overall.
Coconut sugar, also known as coconut palm sugar, is a natural sweetener derived from the sap of flower buds from the coconut palm tree, Cocos nucifera. It has traditionally been produced in various tropical countries like Indonesia, the Philippines, India, and Thailand, where coconut cultivation is plentiful. This type of sugar is produced by tapping the flower buds of the coconut palm to collect the sap. The sap collected is then heated gently to boil off the water content, concentrate the sugars, and form a thick syrup.
The cashew nut is the kidney-shaped seed of the cashew apple, which is the fruit of the tropical evergreen tree Anacardium occidentale. In trade, the "cashew nut" is the edible kernel extracted from the drupe that lies under the cashew apple; the apple itself is consumed for juices and value-added products in certain markets. Cashew trees are adapted to tropical and subtropical regions with good drainage soils, and leading producers are Vietnam, India, Côte d'Ivoire, Brazil, and some West African states.
Carbonated soft drinks (CSDs) are soft drinks that contain carbon dioxide gas dissolved under pressure, providing the characteristic fizz and invigorating mouth feel that consumers like. They generally consist of carbonated water, sweeteners (sugar, high-fructose corn syrup, or low-calorie alternatives), flavoring ingredients, colorants, and preservatives. The products that fall under the category are colas, lemon-lime beverages, fruit-flavored sodas, tonic water, and sparkling mineral water.
Beer is one of the oldest and most popular alcoholic drinks in the world, made by the fermentation of cereal grains, usually barley, but also wheat, maize, or rice using yeast, hops, and water. The process of brewing turns these natural products into a drink that has intricate flavors, fizz, and a range of alcohol levels, usually 3% to 8% ABV. Hops add bitterness and flavor, with malted barley adding fermentable sugars and color. Beer has developed in centuries from small-scale, craft brewing to an international industrialized market with identifiable styles including lagers, ales, stouts, and pilsners.
The areca nut, or betel nut, is the seed of the areca palm (Areca catechu), a tropical palm mainly grown in South and Southeast Asia. It is one of the oldest described masticatories, chewing historically with betel leaf and lime for its mild stimulant effect. The nut is oval, fibrous, and high in alkaloids like arecoline, which is responsible for the typical flavor and psychoactive effects. Top producers are India, Bangladesh, Sri Lanka, Indonesia, Myanmar, Thailand, and China, with India dominating in both output and consumption.
Apple juice is among the most popular fruit drinks in the world, appreciated for its crisp flavor, inherent sweetness, and health advantages. Apple juice is made by pressing fresh apples and filtering the resulting liquid, containing vital nutrients like vitamin C, potassium, antioxidants, and polyphenols that support immune function, cardiovascular health, and hydration. Based on manufacturing techniques, apple juice can be clear, murky, or concentrated, with each type presenting unique taste profiles and longevity attributes.
Banana powder is a dry, fine, nutrient-dense substance created by dehydrating ripe or unripe bananas using methods like spray drying, freeze drying, or drum drying. It acts as an easy and shelf-stable substitute for fresh bananas, preserving most of their essential nutrients such as potassium, magnesium, vitamin B6, and dietary fiber. The production process includes choosing premium bananas, removing their peels, cutting them into slices, and drying them to an optimal moisture content before milling into a fine powder.
Almonds are nutrient-dense seeds obtained from the fruit of the Prunus dulcis tree, highly prized as a food item and source of industrial raw materials. Botanically drupes, almonds have a hard shell covering the edible kernel, which is rich in proteins, monounsaturated fat, fiber, vitamins, and minerals. The two main varieties are sweet almonds, eaten raw or processed into food items, and bitter almonds, used conventionally to extract oil and flavor after purging. The distinguishing features are mild nutty taste, excellent shelf life if kept properly, and very good compatibility with food as well as non-food uses. Almonds are processed in several steps like cleaning, shelling, blanching, roasting, or oil extraction, depending on the final purpose.
In today's fast-paced world, ready-to-eat food has become a staple for anyone juggling work, family, or travel. These foods offer the comfort of a home-cooked dish, without the time and effort, making them a go-to solution for people who crave convenience. With over 4 billion people living in cities globally and the number of dual-income households rising, the time available for traditional cooking has significantly decreased, creating consistent demand for quick meal options.
Cocoa powder is one of the main derivatives of the cocoa bean, which is derived after cocoa butter has been extracted from it during the chocolate production process. It consists mainly of non-fat cocoa solids, which contain a high content of polyphenols, flavonoids, and alkaloids like theobromine. Famous for its intense color, bitter-sweet taste, and antioxidant activity, cocoa powder comes in natural and alkalized (Dutch-processed) grades, each with distinctive taste profiles and functional characteristics.
Cassava starch or tapioca starch is a white, odorless, fine powder extracted from the cassava plant's roots (Manihot esculenta). Cassava starch has diverse applications in food, pharmaceutical, textile, paper, and adhesives industries because of its unbeatable thickening, gelling, binding, and stabilizing properties. In the food industry, cassava starch finds its applications in bakery, confectionery, dairy, beverages, and gluten-free foods as a substitute for wheat and corn-based starches.
The global vegan yogurt market was valued at USD 3.40 Billion in 2024 and is projected to reach USD 12.21 Billion by 2033, growing at a CAGR of 14.51% from 2025 to 2033. This expansion is marked by ongoing innovation, enhanced consumer personalization, and a deeper commitment to sustainability.
The guacamole market is experiencing a notable change, primarily fueled by an increasing consumer preference for healthy, convenient, and natural food choices. In 2024, the market was valued at USD 1379.9 Million. Guacamole is a creamy avocado-based dip originating from Mexican cuisine has grown into a globally popular food product recognized for its nutritional value and versatility.
Corn starch tableware is a new and ecofriendly solution to traditional plastic disposable items, which aims at solving the increasing environmental issues linked to plastic waste. Comprising mostly of corn starch, a plant-based and renewable resource, the products range from plates, bowls, cups, cutlery, and food containers, all of which are completely biodegradable and compostable.
Artificial Intelligence (AI) is transforming India's beer market at a rapid pace by balancing art with advanced technology. Right from brewing to branding, AI makes fermentation precise, temperature adjustment accurate, and ingredient control efficient, guaranteeing consistent quality and innovation in taste.
Soybean oil is a major vegetable oil used as food obtained from the seeds of the soybean crop. It ranks among the world's most significant edible oils, widely utilized in the preparation of foods, processed food items, industrial purposes, and increasingly in biofuels. High in polyunsaturated fats, especially omega-6 fatty acids, soybean oil has applications in non-food industries such as the production of biodiesel, cosmetics, naphthas, and lubricants.
A bun is a small, round or oval-shaped, soft-textured bread product that can be slightly sweet or savory in taste. Made chiefly of wheat flour, yeast, sugar, salt, water, and fat, buns are found in most cuisines around the globe.
The global dairy market is presently experiencing a profound transformation. This is largely accredited to the strategic integration of artificial intelligence (AI), a technology poised to redefine established paradigms of efficiency and innovation within the industry.
People’s relationship with food is undergoing a profound transformation. No longer just a source of fuel, what individuals eat is now seen as a cornerstone of the overall well-being—a tool to boost immunity, sharpen focus, support digestion, and build long-term resilience. This evolution in consumer consciousness is creating a powerful demand for foods that are functional, organic, and transparently made with real ingredients.
Tequila, once confined to regional consumption in Mexico, has now become a popular spirit worldwide, known for its rich heritage, skilled craftsmanship, and premium quality. Made from blue agave, tequila has attracted international consumers for its distinct flavor, artisanal qualities, and cocktail versatility.
Avocado oil is a nutritious oil pressed from the pulp of avocados (Persea americana), in contrast with most oils, which are seed derived. Avocado oil is valued for its rich content of monounsaturated fats, especially oleic acid, in addition to necessary vitamins like E, A, and D. Avocado oil has a mild, buttery taste and very high smoke point and is used both in food preparation and cosmetics.
Biscuits are dry, baked foods made from flour and usually crisp in texture and flat in shape, eaten frequently as a snack or with a meal. They consist mostly of wheat flour, sugar, fat (butter or vegetable oil), and leavening agents such as baking powder. Flavors and variety may be added using ingredients like milk solids, chocolate, spices, or dried fruits. Biscuits come in sweet and savory forms, varying from cookies and cream-filled to salted crackers. Their shelf life, which is lengthy, convenient packaging, and broad taste appeal have made them a household staple, school staple, and workplace staple worldwide.
Nutritional powders have become essential nutritional supplements created to address the specific health needs of vulnerable demographics, including diabetic patients, the aged, and the sick. When regular food intake is inadequate or compromised, these powders, which are made with specially designed compositions and are high in vital vitamins, minerals, protein, and carbs, offer balanced nourishment. Specialized baby formulas guarantee the best possible growth and development in the early years of life.
Vegetable oils remain among the world’s most widely used agricultural products, essential to food manufacturing, biofuels, cosmetics, and industrial goods.
Learn key financial strategies, operational and capital cost planning essentials for starting a profitable livestock feed production business in 2025.
World Tea Day, celebrated every year on May 21st, is an opportunity to appreciate the rich history, cultural significance, and economic impact of tea. From its origins in ancient China to its status as a global commodity, tea continues to connect people, cultures, and economies.
Mango pulp is the thick, smooth, and semi-liquid product yielded by crushing or pulping ripened mangoes. It is the inner flesh of the mango fruit extracted, without the skin and seeds. Mango pulp is widely utilized as a base for many food items, including mango juice, nectar, drinks, smoothies, ice creams, desserts, and as a topping for pancakes or yogurt. Mango juice is a cool drink prepared from ripe mangoes' juice. To make mango juice, the ripe mangoes are normally peeled, pitted, and the flesh of the mango is squeezed to get the pulp. The pulp is further treated to remove the juice from any remaining fibers or solids.
Soy sauce is a liquid condiment used extensively in cooking and seasoning food. Produced from fermented soybeans, wheat, salt, and water, it provides a deep umami taste that can be used to enhance different foods. It is a common ingredient in Asian cooking and has become popular worldwide in marinades, stir-fries, dips, and processed foods. Come in various forms including light, dark, and low-sodium, soy sauce meets the different consumer tastes and nutritional requirements, rendering it a vital ingredient in the food industry.
Instant coffee is a quick and easy-to-brew coffee beverage that is produced by brewing coffee beans into a liquid that concentrates and evaporates into powder or grain form. It rapidly dissolves in hot water, so it's highly sought after by customers demanding fast and easy coffee brewing. It has a long storage life and is inexpensive, making it popular in homes, offices, and food service establishments. It is fueled by urbanization, hectic lifestyles, and growing demand for convenience drinks.
Glucose syrup and sorbitol syrup are versatile sweeteners widely used across the food and beverage industry. Their ability to enhance texture, retain moisture, and extend shelf life makes them essential ingredients in confectionery, bakery, dairy, and beverage products. Beyond their functional benefits, these syrups contribute to taste enhancement and product stability, catering to consumer preferences for smooth, consistent formulations.
Potato flakes are a highly adaptable food ingredient created by processing cooked potatoes into thin, dehydrated slices. They are often used in soups, snacks, baked goods, and fast meals and are well-known for their usefulness, taste, and simplicity of usage. These flakes provide a reliable and effective option for home cooking, foodservice, and commercial food production while preserving the natural flavour, texture, and nutritional value of fresh potatoes. They are indispensable in a variety of culinary applications due to their lengthy shelf life, lightweight design, and easy rehydration method. Their ability to be used in a variety of recipes, from thickened stews to crispy coatings, further solidifies their position as a basic component of the world's food industry.
Industrial enzymes are biological catalysts that fast-track the chemical process that is involved during the industrial processes. Their use is mainly seen in the food and beverage, pharmaceutical, textile, biofuel, and detergent industries. This enzyme is very effective as it is energy efficient and has cleaner and greener production. Its stability and specificity make it a wonderful tool for breaking complex molecules while improving product quality and yield. Industrial enzymes can enhance the texture of bread, benefit dairy processing, assist in the production of biofuels, and clean wastewater. All these phenomena illustrate that industrial enzymes are a mandatory requirement to manufacture many more products with sustainability and cost effectiveness for multiple industries.
Sorbitol is a sugar alcohol widely used as a sweetener, humectant, and stabilizer in food, pharmaceuticals, and cosmetics. It is made commercially by hydrogenating glucose and is naturally present in fruits like apples and pears. Because of its mild sweetness, low glycaemic index, and ability to retain moisture, sorbitol is a popular ingredient in skincare, dental care, and sugar-free goods. It is also an essential component of industrial processes and a laxative in medical applications.
Inedible beef tallow, a byproduct of the meat processing industry, is derived from beef suet and serves various industrial and commercial purposes. This versatile substance undergoes rendering, a process that separates the fat from solid components. Inedible beef tallow's primary application is in animal feed, as it provides essential fats and energy for livestock, particularly in pet food and livestock supplements. Additionally, it finds use in the cosmetics and personal care industry, contributing to the production of candles, soaps, and skin-care products.
Vitamin C supplements are typically made by extracting ascorbic acid from various sources, such as citrus fruits, or synthesizing it in a laboratory setting. The extracted or synthesized ascorbic acid is then processed and formulated into different types of supplements, including tablets, capsules, chewable, and powdered forms. One of the primary advantages of Vitamin C supplements is their ability to support a healthy immune system.
Over the recent decade, the online food and grocery delivery business in India has witnessed exponential growth. This expansion is attributed to the increasing penetration of smartphones, the affordability and convenience offered by food delivery app services, and the growing availability of low-cost internet services. The industry has become progressively competitive, with numerous local and international players competing for a significant market share. Nonetheless, despite the extreme competition, global players are continuing to make significant investments in India on account of its significant market share in the global online food delivery market.
‘World Food Day’ is celebrated on October 16th as a global responsibility to abolish hunger. 2024’s theme for the day is ‘Right to foods for a better life and a better future’. This theme highlights the significance of enabling access to nutritious food for all, particularly in the face of global challenges, including poverty, climate change, and conflict. In line with this theme, in October 2024, India and the United Arab Emirates (UAE) announced plans for developing a food corridor between the two nations, with an initial investment of over USD 2 Billion (INR 17,000 Crore) in food processing and logistics for food parks. This project significantly reinforces the UAE's food security while providing support to Indian farmers. The initiative is part of a bigger investment strategy targeting over USD100 Billion across key sectors, including manufacturing, infrastructure, and logistics.
A vegan, or a plant-based diet, focuses mainly on consuming fruits, vegetables, grains, legumes, nuts, and seeds. It excludes all animal-derived products and ingredients, including meat, poultry, fish, dairy, eggs, and honey. Nowadays, people are shifting toward vegan diets for a variety of reasons, such as ethical concerns for animal welfare, environmental sustainability, health benefits, and personal preferences.
Functional foods promote overall well-being and offer specific health benefits beyond daily nutrient intake. These benefits encompass enhanced bone health, effective cholesterol management, improved heart health, and eye health. Functional foods include probiotic yoghurt, omega-3 enriched eggs, fortified milk, antioxidant-rich berries, and functional beverages.
Fusion cuisine and beverages blend different ingredients, flavors, or techniques from various culinary or cultural backgrounds to create unique and innovative flavor profiles in dishes and drinks. Fusion beverages encompass both alcoholic and non-alcoholic options, including cocktails, mocktails, smoothies, teas, and more. These beverages span a spectrum from simple combinations to complex and inventive concoctions. Changing taste preferences and global connectivity are the main reasons for the increasing adoption of fusion beverages. They are available in various product types, such as carbonated drinks, fused teas and coffees, fruit juices, fusion alcoholic beverages, energy drinks, sports drinks, and more. These beverages are accessible through off-trade outlets (hypermarkets, supermarkets, discounters, grocery stores, off-license stores, alcohol and confectionery stores, highly specialized retailers, and online stores), as well as on-trade establishments (pubs, bars, cafés, restaurants, clubs, discos, hotels, mass events, and others). Examples of fusion beverages include fruit-infused tea, Asian-inspired cocktails, spicy margaritas, bubble tea creations, mojito variations, and infused waters. Furthermore, fusion cuisine merges elements from diverse culinary traditions, such as Asian, European, African, or Latin American, to craft new and exciting dishes. Examples of fusion cuisine include sushi burritos, Thai basil pizza, kimchi tacos, and more.