Cashew Nut Shell Oil Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
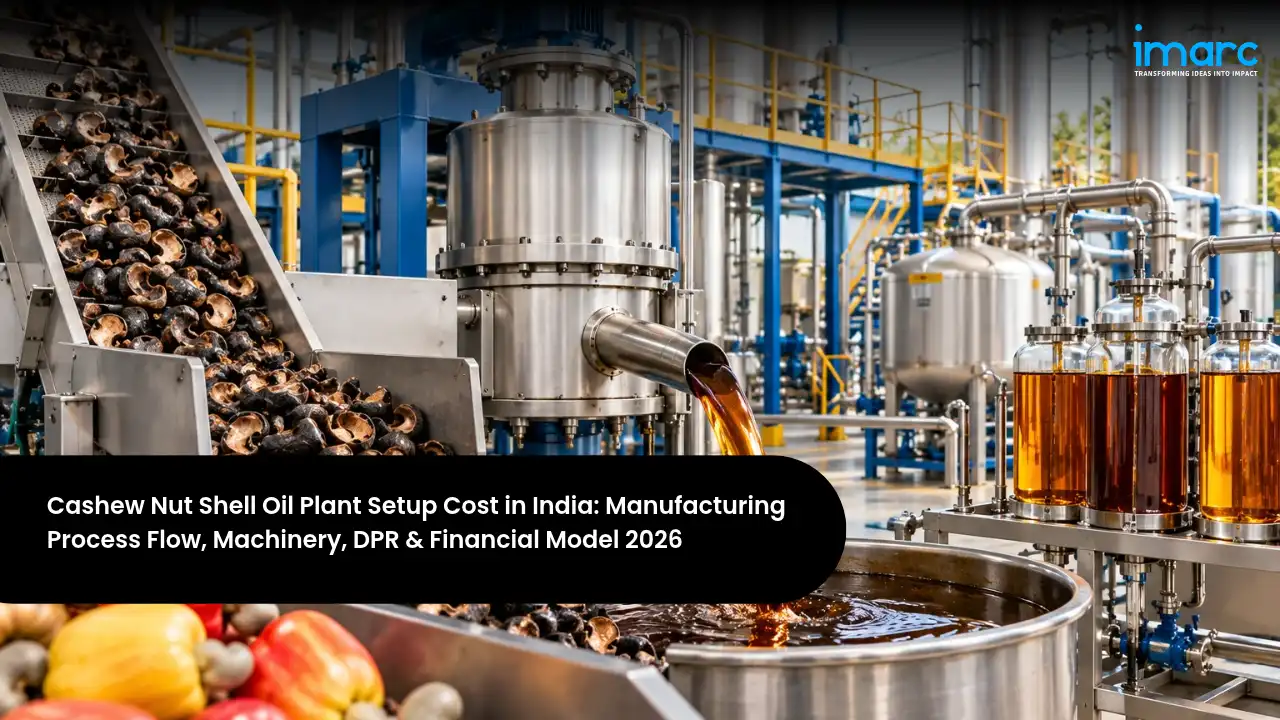
CNSL, the dark, viscous liquid held in the honeycomb of the cashew shell, is recovered by pressing shells left over from kernel processing and then heating the crude liquid so that its anacardic acid turns into cardanol. The result is one of the few renewable industrial phenols, used as a binder in brake linings and clutch facings, in phenolic and epoxy resins, epoxy curing agents, coatings, laminates, surfactants, and as a fuel oil. India processes a large share of the world's raw cashew, importing about 12.5 lakh tonnes in 2024 on top of its own crop, so Cashew Nut Shell Oil Manufacturing Plant Setup in India turns a plentiful agro-waste into a valuable bio-based chemical.
Investment depends mainly on daily shell intake, whether the plant uses only screw expellers or adds solvent extraction for the residual liquid, whether it sells technical grade or distils cardanol, the heat treatment and fume control systems, and the size of shell storage needed to ride out the seasons. The Cashew Nut Shell Oil Manufacturing Plant Cost ranges from about INR 1.5–3 crore for an expeller unit handling 5 to 10 tonnes of shell a day, to INR 6–10 crore for a plant of about 30 tonnes a day with heat treatment, and INR 30–50 crore for large integrated plants with solvent extraction and vacuum distillation. Shells make up 70 to 80% of operating cost, so buying them well decides competitiveness. At mid-2026 prices of about INR 18 per kg for shells, INR 55 per kg for the liquid, and INR 12.5 per kg for de-oiled cake sold as fuel, a well-run expeller plant typically earns a gross margin of 15 to 25% and a net margin of 6 to 10%, with distilled grades lifting returns.
This guide is written for investors exploring how to start a Cashew Nut Shell Oil manufacturing plant in India. It focuses on a plant processing about 30 tonnes of shell a day, roughly 9,000 tonnes a year, producing around 2,000 tonnes a year of technical-grade liquid and about 6,500 tonnes of de-oiled cake for boiler fuel, buying shells from kernel processors and selling to friction material, resin, and coatings makers. It also explains small expeller units and large integrated plants. It covers products and markets, the demand outlook, the production process flow, machinery and raw materials, location and infrastructure, a detailed cost and financial breakdown, certification and approvals, and how a DPR and financial model turn all of this into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| India Raw Cashew Imports (2024) | About 12.5 Lakh Tonnes |
| Liquid Yield from Shell | About 22 – 23% |
| Shell / Liquid Price (2026) | INR 18 / INR 55 per Kg |
| Indicative Total Investment | INR 1.5 Crore to 50 Crore |
The snapshot shows a niche but fast-growing bio-based chemical market, where India has a natural advantage because it processes huge volumes of raw cashew every year. The spread between shell cost and liquid and cake prices is narrow for plain expeller units, so scale, yield, and moving into refined grades decide how much value a plant captures.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Technical CNSL, cardanol, shell cake |
| Plant Capacity | 5 – 100 Tonnes of Shell Per Day |
| Total Project Investment | INR 1.5–3 Crore (small unit) to 6–10 Crore (30 TPD plant) |
| Payback Period | 4 – 6 Years |
| Net Profit Margin | 6 – 10% |
| IRR | 15 – 20% |
| Preferred States | Kerala, Tamil Nadu, Karnataka, Maharashtra, Andhra Pradesh, Odisha |
| Key Requirement | Shell supply, fume control, buyers |
These ranges provide a realistic frame for early planning, but actual returns depend on shell prices through the cashew processing season, liquid yield and quality, the price of de-oiled cake as fuel, the share of output sold as distilled cardanol, export demand, power and labour costs, pollution control spending, and the working capital tied up in shell stocks. A site-specific Cashew Nut Shell Oil Feasibility Report narrows each of these assumptions to your chosen capacity, location, product mix, and buyers.
Table of Contents
- What is Cashew Nut Shell Oil Manufacturing?
- Why is Cashew Nut Shell Oil Manufacturing Growing in India?
- Cashew Nut Shell Oil Manufacturing Process Flow
- Raw Materials Required for Cashew Nut Shell Oil Manufacturing
- Location, Land & Infrastructure
- Cashew Nut Shell Oil Manufacturing Machinery and Equipment
- Cashew Nut Shell Oil Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Cashew Nut Shell Oil Manufacturing in India
- Recent Developments in the India Cashew Nut Shell Oil Manufacturing Industry
- How a Cashew Nut Shell Oil Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Cashew Nut Shell Oil Manufacturing?
Cashew nut shell liquid, widely called CNSL, makes up roughly a quarter of the weight of the shell and is a mixture of natural phenols. In its raw state it is mostly anacardic acid, with some cardol and cardanol. When heated, the anacardic acid loses carbon dioxide and becomes cardanol, giving technical CNSL, which is about two-thirds cardanol and is the main grade traded. Vacuum distillation then separates light-coloured cardanol from cardol and a heavy polymeric residue. Cardanol content, viscosity, moisture, ash, and colour decide value.
Commercially, the liquid is sold to brake lining and clutch facing makers, phenolic and epoxy resin producers, paint, coating, and varnish companies, laminate and adhesive makers, surfactant and specialty chemical firms, rubber compounders, and fuel users, while the pressed shell cake is sold as boiler fuel. A Cashew Nut Shell Oil Manufacturing Plant can serve all these buyers from one shell supply, with technical grade for volume and distilled cardanol for higher-value customers. Buyers value consistent cardanol content, low moisture and ash, reliable supply, and stable pricing.
- Friction: Brake linings, clutch facings.
- Resins: Phenolic and epoxy systems.
- Coatings: Paints, varnishes, laminates.
- Fuel: Liquid fuel and shell cake.
The Main Products and Applications
Choosing the product mix is the most important commercial decision, because it determines the process route, equipment, and margins:
| Product | Description | Key Property | Primary Demand |
|---|---|---|---|
| Natural CNSL | Cold-pressed | Anacardic acid rich | Further processing |
| Technical CNSL | Heat treated | Mostly cardanol | Friction, resins |
| Distilled Cardanol | Vacuum distilled | Light colour | Coatings, surfactants |
| Cardol & Residue | Distillation bottoms | Reactive phenols | Resins, binders |
| Friction Dust | Cured resin | Heat resistant | Brake linings |
| De-oiled Cake | Pressed shell | High heat value | Boiler fuel |
These choices shape the whole project. Technical grade and shell cake give steady volume with a simple expeller and heating setup, while distilled cardanol, friction dust, and resins earn premiums but need vacuum distillation, reactors, and close work with customers.
Why is Cashew Nut Shell Oil Manufacturing Growing in India?
Key Growth Drivers in India and Export Markets
Demand is supported by the shift to bio-based chemicals, vehicle production, and India's large cashew processing base:
- Bio-based phenols: Cardanol replaces petroleum phenol in resins and coatings.
- Automotive: Rising vehicle output needs more brake linings and clutch facings.
- Coatings: Epoxy curing agents from cardanol suit marine and floor coatings.
- Waste value: Processors want to earn more from shells than as low-grade fuel.
- Exports: Buyers in Europe, the US, China, and Japan import Indian grades.
India-Specific Market Opportunity
| Segment | Market Context | Manufacturing Role |
|---|---|---|
| Friction Materials | Vehicle growth | Technical grade, dust |
| Resins & Adhesives | Bio-based push | Cardanol supply |
| Paints & Coatings | Curing agents | Distilled grades |
| Fuel Users | Boilers, kilns | Shell cake, liquid |
The strongest opportunity for new entrants lies in reliable supply of consistent technical grade to friction and resin makers, in distilled cardanol for coatings and specialty chemicals, and in long-term shell contracts with kernel processors. Producers that secure shells at good prices, keep yields high, and move into refined grades will be best placed to grow.
Cashew Nut Shell Oil Manufacturing Process Flow
Understanding the process helps you plan equipment, layout, and where cost and quality are decided. The flow runs from shell receiving and drying through conditioning, pressing in screw expellers, settling and filtration of the crude liquid, heat treatment to convert anacardic acid into cardanol, handling of the pressed cake, optional vacuum distillation, testing, and storage and dispatch in drums or tankers. Shell moisture and expeller settings decide yield, while heat treatment temperature and time decide cardanol content and viscosity.
The Cashew Nut Shell Oil Manufacturing Process Flow
The sequence below reflects a 30 TPD expeller plant making technical grade. Integrated plants add solvent extraction of the cake and vacuum distillation.
| Unit Operation | Key Activity |
|---|---|
| Shell Receiving | Moisture, quality check |
| Drying | Reduce moisture |
| Conditioning | Warm shells |
| Expeller Pressing | Squeeze out liquid |
| Settling & Filtration | Remove solids |
| Heat Treatment | Decarboxylation |
| Cake Handling | Fuel or extraction |
| Vacuum Distillation | Cardanol, optional |
| Testing | Viscosity, moisture |
| Storage & Dispatch | Drums, tankers |
Two factors decide profitability across this flow. The first is yield, because shells make up most of the cost, so drying shells properly, setting expellers well, recovering residual liquid from the cake, and avoiding losses in settling directly set the cost of each kg sold. The second is product value, since the spread on plain technical grade is thin, so consistent quality, steady contracts, and moving part of the output into distilled cardanol or resins decide the return on investment.
Raw Materials Required for Cashew Nut Shell Oil Manufacturing
The main raw material is cashew shell left after kernel extraction, bought from processing units in Kerala, Tamil Nadu, Karnataka, Andhra Pradesh, Odisha, and the Konkan. Other inputs include hexane where solvent extraction is used, filter media and process chemicals for clarifying the liquid, fuel for heat treatment, which usually comes from the plant's own cake, and drums or tankers for dispatch.
| Raw Material | Role in Product | India Sourcing | % of OpEx |
|---|---|---|---|
| Cashew Shells | Main feedstock | Kernel processors | 70–80% |
| Hexane | Extract residual liquid | Domestic suppliers | 1–2% |
| Filter Media | Clarify liquid | Domestic suppliers | Under 1% |
| Heat Source | Heat treatment | Own shell cake | Under 1% |
| Drums & Tankers | Dispatch | Domestic suppliers | 2–3% |
Shells are by far the largest cost, and their price rises and falls with the kernel processing season and with demand from boiler users, so stocking shells in season and long-term contracts with processors are essential.
Location, Land & Infrastructure
Site selection for a shell processing plant is driven by closeness to cashew processing clusters, because shells are bulky and freight quickly erodes the thin spread. Other factors include space for covered shell storage, distance from homes because of odour and fumes, reliable power for expellers, road access for heavy trucks, nearby boiler users for the cake, and state pollution and industrial policies. Locating inside or near a processing cluster gives year-round shells, lower freight, and ready buyers for cake.
Choosing the Best Location for Cashew Nut Shell Oil Manufacturing Plant Setup
| State / Region | Why It Works | Key Advantage |
|---|---|---|
| Kerala | Kollam cluster | Shells, ports |
| Tamil Nadu | Panruti, Ariyalur | Shells, buyers |
| Karnataka | Mangaluru, Udupi | 250+ processors |
| Maharashtra | Sindhudurg, Ratnagiri | Konkan cashew |
| Andhra Pradesh | Palasa, Srikakulam | Large cluster |
| Odisha | Ganjam, Gajapati | Low-cost shells |
Karnataka's coastal belt alone has more than 250 kernel processing units, while Kollam, Panruti, and Palasa are other major hubs with steady shell supply and port access. The final choice should weigh shell availability, freight, environmental approval, buyer location, and incentives.
Quality, Safety and Environmental Systems
Buyers expect test certificates for cardanol content, viscosity, moisture, ash, specific gravity, and iodine value with every batch, and friction and resin makers often run their own approval trials before signing contracts. A credible plant needs a laboratory with viscometers, moisture analysers, and access to chromatography for cardanol content, along with ISO 9001 systems for larger buyers. Safety focuses on the liquid itself, which can cause severe skin burns, so workers need gloves, aprons, and face shields, together with fire protection for heated oil and good ventilation. Environmental systems cover fumes and odour from heat treatment, stack emissions from cake firing, oily runoff, and spill containment. An experienced Cashew Nut Shell Oil Manufacturing Consultant in India can help plan capacity, process route, pollution control, and buyer approvals so the plant meets regulatory and customer requirements from the start.
Infrastructure Requirements (30 TPD Shell Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Plant Land | 1.5 – 2.5 acres | Away from homes |
| Built-up Area | 10,000 – 15,000 sq ft | Covered press shed |
| Shell Storage | 1,000 – 1,500 tonnes | Seasonal stocking |
| Power Supply | 250 – 400 kVA | Expellers, pumps |
| Thermic Fluid Heater | Cake fired | Heat treatment |
| Fume Control | Scrubber, stack | Pollution norms |
| Liquid Storage | Mild steel tanks | Bulk dispatch |
Covered shell storage large enough to buy in season, a reliable heat source for treatment, and effective fume and odour control are the most important infrastructure requirements, since they decide both cost and the right to operate.
Cashew Nut Shell Oil Manufacturing Machinery and Equipment
The equipment set covers shell handling, drying, pressing, clarification, heat treatment, heating utilities, fume control, and storage, with optional solvent extraction and distillation. Expellers and the heat treatment system account for most of the machinery cost in a basic plant, while distillation adds the most in an integrated one.
| Equipment | Function | Key Specification |
|---|---|---|
| Shell Dryer | Reduce moisture | Hot air |
| Conveyors & Elevators | Move shells | Enclosed |
| Screw Expellers | Press shells | Heavy duty |
| Settling Tanks | Separate solids | Heated |
| Filter Press | Clarify liquid | Plate type |
| Heat Treatment Reactor | Make cardanol | Agitated vessel |
| Thermic Fluid Heater | Supply heat | Cake fired |
| Fume Scrubber | Clean exhaust | Wet type |
| Storage Tanks & Pumps | Hold product | Gear pumps |
| Solvent Extraction | Recover residue | Optional |
| Vacuum Distillation | Purify cardanol | Optional |
Machinery should follow the project plan. A small unit uses a few expellers, settling tanks, a simple heating kettle, and drum filling, while a 30 TPD plant adds shell drying, a filter press, a heat treatment reactor with a thermic fluid heater, fume scrubbing, and bulk tanks, and an integrated plant adds solvent extraction and vacuum distillation.
Cashew Nut Shell Oil Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below break down capital and operating costs for a plant processing about 30 tonnes of shell a day in India. The final Cashew Nut Shell Oil Investment Cost for your project will depend on capacity, process route, product mix, pollution control, shell storage, land cost, and location.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Expellers & Pressing | 20–25% | Dryer, expellers |
| Heat Treatment & Filtration | 15–20% | Reactor, filter |
| Thermic Fluid & Utilities | 10–14% | Heater, power |
| Land & Buildings | 20–25% | Shed, storage |
| Tanks & Pollution Control | 10–14% | Tanks, scrubber |
| Pre-operatives & Working Capital | 8–12% | Shell stock, fees |
Pressing and heat treatment make up most of the plant cost, while shell stocks tie up significant working capital. Because of this, a detailed Cashew Nut Shell Oil Business Plan should model seasonal shell prices and stocking, liquid and cake yields, technical and distilled grade prices, cake sales as fuel, power and labour, pollution control, export demand, receivables, and financing costs together, so that funding supports the plant through ramp-up.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Cashew Shells | 70–80% | Seasonal prices |
| Power | 4–6% | Expellers, pumps |
| Labour | 5–8% | Operators, loaders |
| Packing & Freight | 4–6% | Drums, tankers |
| Maintenance & Consumables | 2–4% | Worm shafts, filters |
| Overheads & Compliance | 2–4% | Insurance, testing |
With shells making up most of the cost, margins depend on the spread between shell prices and the combined value of liquid and cake. A good operating model tracks shell cost per tonne, liquid and cake yield, cardanol content, cake realisation, and prices by buyer, and tests results against shell price spikes, lower yields from wet shells, or weaker friction and resin demand.
Financial Analysis and Profitability
Based on analysis of a 30 TPD shell plant, the financial profile combines low capital needs with thin but steady margins on technical grade, high working capital in shell stocks, and good upside from refined grades. The profitability of Cashew Nut Shell Oil manufacturing business in India improves markedly with location inside a processing cluster, long-term shell contracts, high expeller yields, solvent recovery of residual liquid, steady sales of cake as fuel, and a growing share of distilled cardanol, friction dust, or resins.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 15–25% | Shell cost driven |
| Net Profit Margin | 6–10% | After depreciation, taxes |
| Payback Period | 4–6 Years | Low capital |
| IRR (Internal Rate of Return) | 15–20% | Mix dependent |
| Capacity Utilization (stable ops) | 70–85% | Seasonal shells |
| Break-even Capacity Utilization | 50–60% | Thin spreads |
Shell cost and product mix decide where a plant lands within these ranges. Plants selling only technical grade and cake sit at the lower end, while those with distillation and approved specialty customers earn much higher returns.
Returns can be strengthened by adding solvent extraction to lift yield, distilling cardanol, making friction dust or resins, selling cake under contract to boiler users, exporting to Europe and East Asia, and partnering with kernel processors for captive shells.
Key Risks and Mitigation
The main risks are shell price and supply swings, thin spreads, odour and pollution complaints, worker burns and fire, quality variation, and competition from Vietnamese and established Indian producers. Supply risk is reduced by long-term contracts and seasonal stocking; spread risk by refined grades; pollution risk by scrubbers and good siting; safety risk by protective equipment and fire systems; quality risk by testing and blending; and competition by consistent quality and service. Promoters often work with a Cashew Nut Shell Oil Business Plan Consultant in India to test these scenarios before committing capital.
Licenses and Approvals for Cashew Nut Shell Oil Manufacturing in India
Approvals for a shell processing plant centre on environmental consents, fire and factory safety, and handling of solvents and heated oil, along with export and standard business registrations. Promoters setting up a Cashew Nut Shell Oil Manufacturing Plant in India generally need the following:
- Pollution Control: Consent to Establish and Operate covering fumes, stack, and effluent.
- Factory & Fire: Factory license, building plan approval, and fire NOC.
- Solvent Storage: PESO license where hexane is stored above set limits.
- Boiler & Heater: Registration under boiler rules where applicable.
- Quality Certification: ISO 9001 and buyer approvals for friction and resin grades.
- Export: Import Export Code and registration with the export council.
- Business & Trade Registrations: Business registration, GST, Udyam, and trademark.
Pollution consents and siting away from homes are usually on the critical path, followed by fire safety and buyer approvals.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, capacity, products, state pollution control categories, customer specifications, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Cashew Nut Shell Oil Manufacturing Industry
Several recent developments give useful context for investors considering this market:
- New capacity: In June 2026, NFP Sampoorna Foods announced a CNSL unit at Neemrana, Rajasthan, to process up to 1,000 tonnes of shells a month.
- Raw cashew imports: In 2025 up to October, India imported about 12.92 lakh tonnes of raw cashew.
- Port volumes: From April to October 2025, raw cashew imports through New Mangalore Port rose 44% to about 3.45 lakh tonnes.
The common thread is rising raw cashew processing in India and growing interest in turning shells into higher-value chemicals. Producers who secure shells, keep yields high, and move into refined grades will be best placed to grow.
How a Cashew Nut Shell Oil Manufacturing Project Report and DPR Helps Investors
A detailed DPR provides a structured roadmap for the venture, from market demand and product strategy to shell sourcing, process selection, plant design, pollution control, approvals, and economics. It helps investors decide the right capacity, location, and product mix, estimate capital and operating expenditure, assess profitability, and identify risks before committing funds.
At its core is a detailed Cashew Nut Shell Oil Financial Model covering seasonal shell prices and stocking, liquid and cake yields, grade-wise selling prices, cake revenue, power, labour, packing and freight, maintenance, pollution control, working capital, depreciation, taxes, financing, debt servicing, cash flows, break-even, return on investment, and payback under different shell price and demand scenarios. Banks and investors rely on this model to judge long-term viability, which is why many promoters appoint a Cashew Nut Shell Oil Plant Project Report Consultant in India to prepare the report and validate its assumptions against current market data.
For a shell processing project, a strong DPR also clarifies the shell sourcing plan, the process route, the product mix and target buyers, and the pollution control design, which together are the factors most likely to decide success.
Frequently Asked Questions
What are the first steps to set up a cashew nut shell oil manufacturing plant in India?
Start by securing shell supply from kernel processors and identifying buyers among friction, resin, and coatings makers. Then commission a feasibility study and DPR, secure land near a processing cluster and away from homes, choose expellers and heat treatment equipment, obtain pollution and fire approvals, and arrange project financing.
How much does it cost to set up the cashew nut shell oil manufacturing plant in India?
Investment ranges from about INR 1.5–3 crore for a 5 to 10 tonne a day expeller unit to INR 6–10 crore for a 30 tonne a day plant with heat treatment, and INR 30–50 crore for integrated plants with solvent extraction and distillation.
What are the main steps in making cashew nut shell oil?
The flow runs from shell receiving and drying through conditioning, expeller pressing, settling and filtration, heat treatment, cake handling, optional vacuum distillation, testing, and storage and dispatch.
Which machinery does the cashew nut shell oil manufacturing plant need?
Key equipment includes shell dryers, conveyors and elevators, screw expellers, settling tanks, a filter press, a heat treatment reactor, a thermic fluid heater, a fume scrubber, storage tanks and pumps, and optional solvent extraction and vacuum distillation units.
How much liquid comes from a tonne of shells?
Expeller pressing typically recovers about 22 to 23% of the shell weight as liquid, with around 72 to 73% left as de-oiled cake for fuel, and solvent extraction of the cake can recover a little more.
How profitable is cashew nut shell oil manufacturing in India?
At current shell, liquid, and cake prices, a well-run expeller plant typically earns a 15 to 25% gross margin and a 6 to 10% net margin, with payback in about 4 to 6 years. Distilled grades and long-term contracts raise returns.
Which approvals does the cashew nut shell oil manufacturing plant need in India?
Typical approvals include pollution board consents, factory license and fire NOC, PESO approval for solvent storage where applicable, boiler registration where applicable, ISO and buyer approvals, and Import Export Code, GST, Udyam, and trademark registrations.
How do I get a feasibility study or DPR for the cashew nut shell oil manufacturing project?
A detailed feasibility study and DPR covers market and buyers, shell sourcing, process route, plant layout, pollution control, approvals, and full financials. Investors usually engage a Cashew Nut Shell Oil Manufacturing Feasibility Study Consultant with experience in agro-processing and bio-based chemicals to prepare the report and validate it for lenders.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

Ground spices and blended masalas turn whole chilli, turmeric, coriander, cumin, pepper, and other spices into clean, safe, ready-to-use powders and mixes for homes, restaurants, food processors, and export buyers.
Fishmeal is a brown, protein-rich powder made by cooking, pressing, drying, and grinding small oily fish and fish processing waste, with fish oil recovered as a valuable co-product.
Dried banana ingredients are made by washing, peeling, and slicing fresh fruit, treating it to prevent browning, drying it in belt, tray, or spray dryers, and milling it into a fine, shelf-stable product.
Dried egg is made by breaking fresh eggs, pasteurising the liquid whole egg, yolk, or white, and spray drying it into a fine powder that keeps for a year or more without refrigeration.
Whey is the liquid left after milk is made into cheese or paneer, and it contains high-quality proteins that can be separated by membrane filtration and spray dried into concentrates and isolates.
The pectin market has moved from the back of the ingredient label to the centre of product development strategy. As food manufacturers strip out synthetic gelling agents, stabilisers and thickeners, pectin has become one of the few hydrocolloids that can deliver texture and shelf stability while still reading as a familiar, fruit-derived ingredient.
Poultry processing turns live broilers into hygienically slaughtered, chilled, cut, and packed meat, ready for retail shelves, restaurants, quick-service chains, caterers, and export. India produced about 10.5 million tonnes of meat in 2024-25, and poultry made up roughly half of it at 5.18 million tonnes, yet around 85% of birds are still sold live or slaughtered in small wet-market shops.
The global tomato ketchup market reached USD 20.8 Billion in 2025 and is projected to reach USD 26.3 Billion by 2034, growing at a CAGR of 2.68% during 2026-2034, according to IMARC Group. Those numbers describe a mature, high-volume condiment category rather than a fast-growing one.
Coconut shell powder is made by cleaning, drying, crushing, and finely grinding the hard inner shell of the coconut into a uniform powder. Because the shell is dense, rich in lignin, low in ash, and slightly oily, the powder is an excellent natural filler.
Dextrins are modified starches made by heating dry starch, usually with a small amount of acid, so that its long molecules break into shorter ones. The result is a powder that dissolves easily in water and forms strong, quick-drying adhesive films.
Fruit powders are made by drying fruit pulp or juice into a fine, free-flowing powder that keeps the flavour, colour, and much of the nutrition of fresh fruit while lasting months without refrigeration.
Yeast is a living microorganism that makes bread rise, ferments beer, wine, and spirits, turns sugar into fuel ethanol, and supplies protein, vitamins, and flavour to food, feed, and nutrition products.
The global champagne market is entering a phase where value growth matters more than volume growth. IMARC Group values the market at USD 6.6 Billion in 2025 and projects it to reach USD 8.1 Billion by 2034, expanding at a CAGR of 2.25% during 2026-2034.
India is one of the world's leading coffee producers and exporters, growing shade-grown arabica and robusta in the hills of Karnataka, Kerala, and Tamil Nadu and supplying green, roasted, and instant coffee to more than 100 countries.
The Australia Online Grocery Industry has crossed the point where volume growth is the scarce commodity. What is scarce now is profitable volume. According to IMARC Group, the market reached USD 17.22 Billion in 2025 and USD 21.91 Billion in 2026, and is projected to reach USD 96.59 Billion by 2034, expanding at a CAGR of 20.37% (2026–2034), a more than five-fold expansion in under a decade. That growth is unfolding inside one of the most closely regulated grocery markets in the developed world.
Baby formula, also known as infant formula, is a manufactured food product designed to serve as a substitute for or supplement to human breast milk for infants and young children up to three years of age.
Palm oil is the world's most widely used vegetable oil, extracted from the fruit of the oil palm and used in cooking oils, vanaspati, bakery fats, snacks, soaps, cosmetics, and oleochemicals, while the kernel yields palm kernel oil and cake.
Beer is one of the world's most widely consumed drinks, brewed from malted barley, water, hops, and yeast, often with rice or maize as adjuncts. In India, beer accounts for only a small share of alcohol consumption compared with most countries, but that is changing as a young, urban, and increasingly female consumer base embraces lighter drinks, premium lagers, wheat beers, and craft styles.
Bread, buns, rusk, cakes, cookies, and biscuits are part of daily meals and snacking in almost every Indian household, from metro cities to small towns.
Makhana has moved from a pond crop traded through village aggregators into a branded snack with its own export code and a national board behind it. According to IMARC Group, the India makhana market was valued at INR 9.29 Billion in 2025 and is projected to reach INR 19.95 Billion by 2034, growing at a CAGR of 8.85% (2026–2034).
Packaged drinking water has become an everyday essential in India, sold at railway stations, highway dhabas, offices, weddings, hotels, and homes. Concerns about groundwater contamination, rising incomes, travel and tourism, and hot summers keep demand growing year after year, and the market is worth more than USD 8 billion.
Every year, India's vehicles, machinery, and industries consume around 3 million tonnes of lubricants, making the country one of the world's largest lubricant markets.
Indian wine has come a long way from a niche curiosity to a genuine lifestyle category. Young urban consumers, growing interest in food pairing, wine tourism in regions such as Nashik and Nandi Valley, and supportive state grape policies have given domestic wineries room to grow, while producers have steadily improved quality and won international recognition.
Setting up an Extra Neutral Alcohol Manufacturing Plant in India is a fermentation-and-distillation venture anchored to the large and growing alcoholic-beverage industry, along with pharmaceutical, cosmetic, and industrial demand.
Setting up a Shrimp Processing Plant in India is a high-potential, export-oriented venture, powered by the country's position as one of the world's largest shrimp producers and exporters. India's vast coastline, expanding vannamei aquaculture, and strong demand from the United States, China, the European Union, and Japan make a frozen shrimp processing Plant Setup in India one of the most attractive opportunities in the seafood sector.
India's post-pandemic food delivery boom, followed by the new quick-commerce disruption from Zepto Cafe and Swiggy Bolt, has turned the Cloud Kitchen Market in India into a genuine focus of global investor curiosity.
The total addressable market for India's functional beverages is expanding from USD 6.9 Billion in 2025 to a projected USD 18.8 Billion by 2034, growing at a CAGR of 10.74% (2026–2034).
The halal food market has moved well beyond a religious-compliance niche into one of the largest, fastest-growing consumer food categories in the world. The global market was valued at USD 2,956.4 billion in 2025 and is projected to reach USD 6,329.3 billion by 2034, expanding at a compound annual growth rate (CAGR) of 8.56% between 2026 and 2034.
India’s dairy industry is undergoing a structural transformation, driven by rising incomes, urbanization, changing consumption patterns, and strong policy support. Traditionally dominated by an unorganized and cooperative-led system, the sector is now evolving into a more competitive, branded, and technology-enabled ecosystem.
Cheese is a dairy food made by coagulating the proteins in milk, mainly casein, using enzymes, acids, or microorganisms, followed by separating the curds from the whey. Cheese can be made from the milk of cows, buffaloes, goats, sheep, or a combination of these. The coagulated curd is then processed by cutting, cooking, pressing, salting, and aging to achieve desired texture, moisture, and flavor characteristics.
Avocado oil is a vegetable oil that is extracted from the pulp of ripe avocados (Persea americana), unlike other vegetable oils that are extracted from seeds. Avocado oil contains high amounts of monounsaturated fatty acids, specifically oleic acid, as well as phytosterols, tocopherols, and carotenoids. Avocado oil can be classified as extra virgin, virgin, or refined, depending on the extraction and refining process.
Wine is a type of alcoholic drink that is made by the controlled fermentation of grape juice, where the natural or added yeast ferments the sugars in the juice to produce ethanol, carbon dioxide, and other compounds. Wine is made up of water, ethanol, organic acids, phenolic compounds, aromatic esters, and trace minerals.
Whey protein is a high-quality, complete protein obtained from whey, which is the liquid by-product of cheese production. Milk coagulated with enzymes or acids separates into curds (casein) and whey. Whey is a liquid that contains soluble proteins like beta-lactoglobulin, alpha-lactalbumin, serum albumin, and immunoglobulins. Whey is filtered and dried to produce commercial products like whey protein concentrate (WPC), whey protein isolate (WPI), and whey protein hydrolysate (WPH).
Whole egg powder is a dehydrated egg ingredient made by spray drying homogenized liquid whole eggs, which include a mixture of egg yolk and egg white in their natural ratio. Fresh whole shell eggs are broken, filtered, pasteurized, and then processed into a stable powder form using controlled drying methods. The final product preserves the functional and nutritional qualities of fresh eggs, such as high-quality protein, essential amino acids, lipids, vitamins, and emulsifying fractions.
Tea is a drink made from the processed leaves and flower buds of the plant Camellia sinensis. The essential properties of tea, namely flavor, aroma, color, and strength, depend on the level of oxidation, drying, and fermentation of the processed leaves. Tea can be categorized based on the processing techniques into black tea, green tea, oolong tea, white tea, and specialty teas.
Soy milk is a plant-based beverage made from whole soybeans that have been soaked, ground, and their liquid extracted, then cooked and filtered. It is completely devoid of elements originating from animals and is intended to operate and look like dairy milk. In addition to naturally existing proteins, carbs, and healthy fats from soybeans, soy milk is frequently supplemented with vitamins and minerals to improve its nutritional value.
Soya chunks are a protein-rich food item that is prepared using defatted soy flour, which is a by-product of soybean oil extraction. Soya chunks are prepared using the process of extrusion cooking, which converts the soy flour into porous, sponge-like granules with a fibrous structure that resembles meat when rehydrated.
Soya chunks are a protein-rich food item that is prepared using defatted soy flour, which is a by-product of soybean oil extraction. Soya chunks are prepared using the process of extrusion cooking, which converts the soy flour into porous, sponge-like granules with a fibrous structure that resembles meat when rehydrated. Soya chunks have a neutral flavor, which helps them absorb the flavors of spices and seasonings while cooking.
Saudi Arabia’s precast concrete market reached USD 1.2 Billion in 2024 as per the IMARC Group, clear proof that off-site construction is rapidly becoming the Kingdom’s go-to building solution. With residential, commercial, and major infrastructure projects multiplying, developers are increasingly turning to precast building solutions to keep pace.
The global emergency food market has emerged as a critical component of household preparedness infrastructure, disaster response frameworks, and government stockpiling programs worldwide. In March 2025, the National Disaster Response Force (NDRF), established in India, conducted a National Capacity Building Competition for State Disaster Response Forces (SDRFs) to improve their readiness and effectiveness in managing collapsed structure emergencies.
The Saudi Arabia sauces and seasonings market size is expanding steadily as consumers embrace more diverse flavors, convenient food formats, and global culinary influences. Evolving lifestyles, greater exposure to international cuisines, and a strong shift toward home cooking have collectively shaped the contemporary marketplace.
The GCC chocolate market has experienced robust expansion in recent years, driven by evolving consumer preferences, rising disposable incomes, and the proliferation of international brands. In 2024, the GCC chocolate market size reached USD 3,200.77 Million, reflecting sustained growth across premium, artisanal, and mass-market segments.
The Gulf Cooperation Council (GCC) region continues to position itself as one of the fastest-evolving markets for packaged beverages, with bottled water standing at the forefront of this transformation. The GCC bottled water market size has expanded steadily in recent years, supported by a strong shift toward health-driven consumption, improved hydration awareness, and evolving lifestyle patterns across the member countries.
India’s pet sector has experienced a remarkable transformation, driven by urbanization, evolving lifestyles, and a stronger emotional bond between people and their companion animals. What was once a niche trend among a few urban families has now become a widespread practice across Indian households, where pets are regarded as integral members of the family.
Shrimp is one of the world’s most precious natural spices, derived from the dried red stigmas of the Crocus sativus flower. Each bloom yields only a few delicate stigmas, which must be carefully hand-harvested, dried, and processed to preserve their vibrant color, distinctive aroma, and rich flavor. The spice’s deep golden-yellow hue, bitter-sweet taste, and unique fragrance are primarily attributed to its key bioactive compounds like crocin, picrocrocin, and safranal.
The Australian craft beer industry has emerged as a significant segment of the broader alcoholic beverages market driven by evolving consumer preferences, rising disposable incomes, and a growing appreciation for artisanal and premium products. Over the past decade, the market has witnessed substantial expansion with craft breweries increasingly occupying a distinct niche in the highly competitive beer sector.
India is witnessing a profound transformation in how its citizens approach health and wellness. The nutritional supplements market of the country has evolved from a niche segment into a mainstream industry serving millions of health-conscious consumers.
Sea salt is a natural mineral product obtained through the solar evaporation of seawater, followed by harvesting, washing, drying, grading, and packaging. Unlike refined table salt, which undergoes heavy chemical processing, sea salt production relies primarily on solar energy and natural crystallization, allowing it to retain trace minerals such as magnesium, calcium, and potassium that contribute to its distinct taste and nutritional value.
Saffron is one of the world’s most precious natural spices, derived from the dried red stigmas of the Crocus sativus flower. Each bloom yields only a few delicate stigmas, which must be carefully hand-harvested, dried, and processed to preserve their vibrant color, distinctive aroma, and rich flavor.
The India edible oil market stands as one of the most dynamic sectors within the country's consumer goods landscape. As households increasingly prioritize quality, health, and convenience, demand for diverse oil varieties continues to surge. The transformation from traditional purchasing habits to modern retail experiences reflects broader shifts in consumer awareness and lifestyle choices.
India's organic food industry stands at the intersection of health consciousness, agricultural innovation, and sustainable practices. As consumers increasingly prioritize chemical-free nutrition and environmental sustainability, the sector faces transformative opportunities alongside significant operational challenges shaped by evolving dietary preferences, technology adoption in agriculture, and regulatory frameworks that collectively define market dynamics.
Japan’s gluten-free foods and drinks market has evolved into a vibrant segment of the country’s growing health and wellness culture. Once catering mainly to individuals with celiac disease or gluten intolerance, gluten-free products now appeal to a broader demographic pursuing balanced, wellness-oriented lifestyles.
The GCC coconut water market is experiencing remarkable momentum as consumer preferences shift decisively toward natural hydration solutions and functional beverages. This transformation is propelled by heightened health consciousness, expanding fitness culture, and growing awareness of the nutritional benefits associated with coconut-based drinks.
The Saudi Arabia online grocery market is experiencing transformative growth, driven by widespread digital adoption, evolving consumer preferences, and strategic government initiatives aligned with Vision 2030. As one of the fastest-growing e-commerce segments in the Middle East, the online grocery sector is reshaping how Saudi consumers shop for everyday essentials.
Onion powder is a dehydrated and ground seasoning that results from the drying of fresh onions into a concentrated powdered form. The process of dehydration removes moisture from the product, while maintaining the flavor, aroma, and pungency characteristics of the onion, thereby making it a stable and ready-to-use ingredient with a longer shelf life. Onion powder can be prepared through various controlled drying, grinding, and screening processes from white, red, or yellow onion varieties.
Japan's animal feed industry stands as a cornerstone of the nation's agricultural infrastructure, supporting domestic livestock production and ensuring food security. The sector encompasses diverse feed products for cattle, swine, poultry, and aquaculture operations that sustain Japan's protein supply chain.
Nutraceuticals are bioactive, health-enhancing products derived from food sources, botanical ingredients, or purified nutrients that provide physiological benefits beyond basic nutrition. They include dietary supplements, functional foods, fortified beverages, herbal extracts, probiotics, omega-fatty-acid formulations, vitamins, minerals, and specialized nutritional compounds. Nutraceuticals are designed to support wellness, prevent nutrient deficiencies, and promote specific health outcomes, including the improvement of immunity, digestive balance, cognitive function, metabolic health, or cardiovascular support.
India's spice industry stands as a vibrant cornerstone of the nation's agricultural economy and cultural identity. As global consumers increasingly seek authentic flavors and natural ingredients, India's position as the world's leading spice producer continues to strengthen.
According to IMARC Group, India's ice cream consumption has grown nearly fourfold over the past decade. Despite this, India's per-capita consumption stands at just ~400 ml per year — far below the global average of ~2.5 litres. That gap is not a weakness. It is the single most compelling argument for the industry's long-term runway.
Millet represents a group of small-seeded cereals, primarily from the Poaceae family, which are grown as staple foods for thousands of years in Asia and Africa and, increasingly, in other parts of the world. These cereals include pearl millet, foxtail millet, finger millet, proso millet, barnyard millet, and little millet.
Milk powder is a type of dehydrated dairy product, which is manufactured by removing almost all moisture from liquid milk by means of various evaporation and drying techniques. The resultant product is a stable, shelf-friendly powder containing most of the nutritional components of milk, including proteins, lactose, minerals, and fats. Milk powder may be prepared from whole, skimmed, or partially skimmed milk, depending on its intended use. The very low moisture content inhibits microbial growth and spoilage; hence, it becomes more feasible regarding transport, storage, and usage in different formulations.
Meat generally denotes the animal tissues that are consumed and mainly include muscle fibers, though the content of fat, connective tissue, and moisture may vary. There are a number of sources, although they are mainly livestock such as cattle, pigs, sheep, poultry, and, in some regions, game animals.
Australia's tea market is at a crossroads, undergoing extraordinary change inspired by changing consumption habits, health awareness, and the explosion of functional drinks.
The Australia dairy industry stands as a vital pillar of the nation's agricultural economy, representing the third-largest rural sector and contributing significantly to both domestic food security and export earnings.
India has emerged as one of the fastest-growing fisheries producers in the world, backed by rising health awareness, export diversification, and evolving aquaculture technology.
Ice cream is a frozen dairy dessert made by blending milk, cream, sugar, and flavorings, then freezing the mixture while incorporating air to give a smooth, creamy texture. The mixture is pasteurized, homogenized, then churned under controlled conditions to prevent the formation of large ice crystals. Depending on the recipe and product category, it may contain stabilizers, emulsifiers, fruits, nuts, chocolate, or other inclusions. It comes in hardpacked ice cream, softserve, gelato, sorbets, and frozen yogurt. The texture, flavor, and quality of this frozen dessert will depend on the ratios of ingredients used and the techniques followed in processing.
The Philippines mushroom industry is undergoing a transformative phase, driven by a growing consumer shift toward functional and nutrient-dense foods. As health awareness rises across both urban and rural populations, mushrooms are increasingly recognized for their high protein, fiber, and antioxidant content. This change is not merely dietary it reflects a broader movement toward wellness-oriented lifestyles that prioritize natural, sustainable, and locally sourced food options. For agribusiness investors and food manufacturers, this evolution signals significant growth potential in both production and value-added segments of the market.
The Vietnam aquaculture market has transformed from traditional fishing practices into one of the world's most dynamic seafood production sectors. Vietnam now ranks as the fourth-largest aquaculture producer globally, supplying markets across Asia, Europe, and the Americas. Understanding what drives this growth is essential for investors, businesses, and policymakers looking to engage with this evolving industry.
French fries are thin strips of baked or deep-fried potatoes with a fluffy inside and a crispy outside. They originated in Europe and are now a common fast-food staple that is consumed as a snack or side dish in many countries. French fries are made mostly from high-starch potatoes and are produced in large quantities by chopping, blanching, frying, and occasionally freezing. They are among the most well-liked and extensively consumed potato-based food products in the world because of their ability to be seasoned, flavored, or combined with condiments like cheese, mayonnaise, or ketchup.
Glucose powder is a crystalline or powdered form of a simple sugar, glucose, derived mainly from sources of starch: corn, wheat, or rice. Glucose powder is obtained by the hydrolysis of starch into glucose by enzymes, followed by purification and concentration of the solution and its drying to yield a readily water-soluble, easily digested carbohydrate powder. Glucose powder is an instant source of energy as it is quickly absorbed in the body, which makes the product valuable in food, beverage, nutraceutical, and pharmaceutical applications. It has a neutral taste, a very high sweetness index compared to regular sugar, and excellent dissolving properties, making it useful in various industrial formulations and household consumption.
Ghee is a class of clarified butter that, conventionally, is prepared by simmering butter until the milk solids separate and caramelize, leaving a golden, fragrant fat. Presently, it is widely used in South Asian, Middle Eastern, and increasingly global cuisines. Ghee has a high smoke point, long shelf life, and rich flavor, which makes it suitable for cooking, frying, and flavor enhancement. During its production, water and milk proteins are removed, making the product a lactose-free fat that contains fat-soluble vitamins and bioactive compounds. Its stability, purity, and distinctive taste make ghee an important culinary and functional ingredient in both traditional and modern food applications.
Fruit powder is made by removing the moisture content of whole fruits through various methods, such as spray drying, freeze-drying, drum drying, or vacuum drying, to get a finely ground, dehydrated powder form. After drying, the fruit is then milled into a stable, lightweight, and shelf-friendly powder that retains much of the fruit's natural flavor, aroma, nutrients, and color. Fruit powders have the essence of fresh fruit in concentrated, easy-to-handle form and are thus highly versatile in food, beverage, nutraceutical, and cosmetic applications. They offer an alternative to fresh fruits in a more convenient manner with longer shelf life and consistent quality for industrial use.
Garlic powder is the dried form of garlic, made by drying fresh garlic cloves and then grinding them to a uniform powder. Garlic dehydration removes moisture while preserving much of the flavor, aroma, and pungency of garlic. This concentrated form offers longer shelf life, easy storage, and consistent taste compared to fresh garlic. Garlic powder is widely used as a seasoning, marinade ingredient, and flavor enhancer in culinary, industrial, and packaged-food applications. Garlic powder imparts the taste of garlic without peeling or chopping into the dishes; therefore, it is very convenient and versatile for both homes and large-scale food manufacturers.
The Frozen food market is highly diversified, encompassing categories like frozen ready meals, fruits and vegetables, meat, seafood, desserts, and bakery items. This robust growth is fueled by fundamental shifts, including urbanization, the rise of dual-income households, and a consumer demand for convenience without compromising nutritional value. Modern freezing technologies ensure high quality and extended shelf life, addressing the critical issue of food waste.
The United States shrimp market stands as one of the most dynamic segments within the global seafood industry. It reached 983,000 Tons in 2024 as per IMARC Group and is projected to reach 1,280,000 Tons by 2033 at a growth rate of 3% from 2025 to 2033. As consumer preferences shift toward healthier protein sources and sustainable options, shrimp has emerged as a cornerstone of American dietary habits. The market reflects transformations in consumer behavior, international trade dynamics, and technological innovation within aquaculture and seafood processing.
The Australia gluten-free food industry is flourishing, powered by a surge in health-conscious consumers, a rise in gluten intolerance cases, and a growing appetite for clean-label, nutritious products. In 2024, the industry reached a notable milestone, hitting USD 361.20 Million, according to IMARC Group. Popular categories like gluten-free bakery items, snacks, dairy, and ready-to-eat (RTE) meals are leading the charge.
The global frozen food industry has undergone a remarkable transformation over the past decade, evolving from a convenience-focused sector into a sophisticated, technology-driven marketplace that prioritizes quality, nutrition, and sustainability. Innovation serves as the primary catalyst for this evolution, fundamentally reshaping consumer perceptions and market dynamics across all geographic regions.
Egg powder is a type of dehydrated product prepared from whole eggs, egg whites, or egg yolks, using a controlled drying process that removes moisture content while preserving the natural nutrients, flavor, and functional properties in fresh eggs. Originally developed to extend the shelf life of eggs, it was also meant to be convenient and easily transportable for food manufacturing, catering, and military or outdoor purposes.
The global ginger market is currently experiencing a remarkable phase of expansion, positioning itself as one of the most dynamic segments within the spice and functional ingredient industries. As consumers worldwide are increasingly gravitating toward natural, health-promoting ingredients, ginger is emerging as a star performer that is capturing attention across multiple sectors, from culinary applications to pharmaceuticals and nutraceuticals. The market is demonstrating robust momentum that industry analysts are tracking with considerable interest.
Coconut is an important tropical crop with a wide array of uses, and hence it is considered the "Tree of Life." The fruit, leaves, trunk, and roots of coconuts yield a wide range of products. Each part has economic value and, therefore, provides a means of livelihood in many rural communities and agro-industrial development in tropical regions such as Southeast Asia, South Asia, and the Pacific Islands.
Coconut yogurt is a plant-based alternative to traditional dairy, made from the rich milk of mature coconuts. This yogurt boasts the same feel and taste as traditional dairy yogurt, all the while catering to vegans, lactose-intolerant, or allergenic consumers. Manufactured like traditional yogurt, this variety is fermented with live bacterial cultures such as Lactobacillus bulgaricus and Streptococcus thermophilus. These same cultures ferment the natural sugars of the coconut milk into lactic acid during processing, creating a thick consistency and giving it that tangy taste typical of yogurt.
The Australian dog food market is undergoing an important transformation, motivated mainly by advancements in AI technology. As more people own pets, they increasingly demand more tailored and nutritious options for dogs. Both technology and artificial intelligence (AI) are important to facilitate this, and reshaping the industry overall.
Coconut sugar, also known as coconut palm sugar, is a natural sweetener derived from the sap of flower buds from the coconut palm tree, Cocos nucifera. It has traditionally been produced in various tropical countries like Indonesia, the Philippines, India, and Thailand, where coconut cultivation is plentiful. This type of sugar is produced by tapping the flower buds of the coconut palm to collect the sap. The sap collected is then heated gently to boil off the water content, concentrate the sugars, and form a thick syrup.
The cashew nut is the kidney-shaped seed of the cashew apple, which is the fruit of the tropical evergreen tree Anacardium occidentale. In trade, the "cashew nut" is the edible kernel extracted from the drupe that lies under the cashew apple; the apple itself is consumed for juices and value-added products in certain markets. Cashew trees are adapted to tropical and subtropical regions with good drainage soils, and leading producers are Vietnam, India, Côte d'Ivoire, Brazil, and some West African states.
Carbonated soft drinks (CSDs) are soft drinks that contain carbon dioxide gas dissolved under pressure, providing the characteristic fizz and invigorating mouth feel that consumers like. They generally consist of carbonated water, sweeteners (sugar, high-fructose corn syrup, or low-calorie alternatives), flavoring ingredients, colorants, and preservatives. The products that fall under the category are colas, lemon-lime beverages, fruit-flavored sodas, tonic water, and sparkling mineral water.
Beer is one of the oldest and most popular alcoholic drinks in the world, made by the fermentation of cereal grains, usually barley, but also wheat, maize, or rice using yeast, hops, and water. The process of brewing turns these natural products into a drink that has intricate flavors, fizz, and a range of alcohol levels, usually 3% to 8% ABV. Hops add bitterness and flavor, with malted barley adding fermentable sugars and color. Beer has developed in centuries from small-scale, craft brewing to an international industrialized market with identifiable styles including lagers, ales, stouts, and pilsners.
The areca nut, or betel nut, is the seed of the areca palm (Areca catechu), a tropical palm mainly grown in South and Southeast Asia. It is one of the oldest described masticatories, chewing historically with betel leaf and lime for its mild stimulant effect. The nut is oval, fibrous, and high in alkaloids like arecoline, which is responsible for the typical flavor and psychoactive effects. Top producers are India, Bangladesh, Sri Lanka, Indonesia, Myanmar, Thailand, and China, with India dominating in both output and consumption.
Apple juice is among the most popular fruit drinks in the world, appreciated for its crisp flavor, inherent sweetness, and health advantages. Apple juice is made by pressing fresh apples and filtering the resulting liquid, containing vital nutrients like vitamin C, potassium, antioxidants, and polyphenols that support immune function, cardiovascular health, and hydration. Based on manufacturing techniques, apple juice can be clear, murky, or concentrated, with each type presenting unique taste profiles and longevity attributes.
Banana powder is a dry, fine, nutrient-dense substance created by dehydrating ripe or unripe bananas using methods like spray drying, freeze drying, or drum drying. It acts as an easy and shelf-stable substitute for fresh bananas, preserving most of their essential nutrients such as potassium, magnesium, vitamin B6, and dietary fiber. The production process includes choosing premium bananas, removing their peels, cutting them into slices, and drying them to an optimal moisture content before milling into a fine powder.
Almonds are nutrient-dense seeds obtained from the fruit of the Prunus dulcis tree, highly prized as a food item and source of industrial raw materials. Botanically drupes, almonds have a hard shell covering the edible kernel, which is rich in proteins, monounsaturated fat, fiber, vitamins, and minerals. The two main varieties are sweet almonds, eaten raw or processed into food items, and bitter almonds, used conventionally to extract oil and flavor after purging. The distinguishing features are mild nutty taste, excellent shelf life if kept properly, and very good compatibility with food as well as non-food uses. Almonds are processed in several steps like cleaning, shelling, blanching, roasting, or oil extraction, depending on the final purpose.
In today's fast-paced world, ready-to-eat food has become a staple for anyone juggling work, family, or travel. These foods offer the comfort of a home-cooked dish, without the time and effort, making them a go-to solution for people who crave convenience. With over 4 billion people living in cities globally and the number of dual-income households rising, the time available for traditional cooking has significantly decreased, creating consistent demand for quick meal options.
Cocoa powder is one of the main derivatives of the cocoa bean, which is derived after cocoa butter has been extracted from it during the chocolate production process. It consists mainly of non-fat cocoa solids, which contain a high content of polyphenols, flavonoids, and alkaloids like theobromine. Famous for its intense color, bitter-sweet taste, and antioxidant activity, cocoa powder comes in natural and alkalized (Dutch-processed) grades, each with distinctive taste profiles and functional characteristics.
Cassava starch or tapioca starch is a white, odorless, fine powder extracted from the cassava plant's roots (Manihot esculenta). Cassava starch has diverse applications in food, pharmaceutical, textile, paper, and adhesives industries because of its unbeatable thickening, gelling, binding, and stabilizing properties. In the food industry, cassava starch finds its applications in bakery, confectionery, dairy, beverages, and gluten-free foods as a substitute for wheat and corn-based starches.
The global vegan yogurt market was valued at USD 3.40 Billion in 2024 and is projected to reach USD 12.21 Billion by 2033, growing at a CAGR of 14.51% from 2025 to 2033. This expansion is marked by ongoing innovation, enhanced consumer personalization, and a deeper commitment to sustainability.
The guacamole market is experiencing a notable change, primarily fueled by an increasing consumer preference for healthy, convenient, and natural food choices. In 2024, the market was valued at USD 1379.9 Million. Guacamole is a creamy avocado-based dip originating from Mexican cuisine has grown into a globally popular food product recognized for its nutritional value and versatility.
Corn starch tableware is a new and ecofriendly solution to traditional plastic disposable items, which aims at solving the increasing environmental issues linked to plastic waste. Comprising mostly of corn starch, a plant-based and renewable resource, the products range from plates, bowls, cups, cutlery, and food containers, all of which are completely biodegradable and compostable.
Artificial Intelligence (AI) is transforming India's beer market at a rapid pace by balancing art with advanced technology. Right from brewing to branding, AI makes fermentation precise, temperature adjustment accurate, and ingredient control efficient, guaranteeing consistent quality and innovation in taste.
Soybean oil is a major vegetable oil used as food obtained from the seeds of the soybean crop. It ranks among the world's most significant edible oils, widely utilized in the preparation of foods, processed food items, industrial purposes, and increasingly in biofuels. High in polyunsaturated fats, especially omega-6 fatty acids, soybean oil has applications in non-food industries such as the production of biodiesel, cosmetics, naphthas, and lubricants.
A bun is a small, round or oval-shaped, soft-textured bread product that can be slightly sweet or savory in taste. Made chiefly of wheat flour, yeast, sugar, salt, water, and fat, buns are found in most cuisines around the globe.
The global dairy market is presently experiencing a profound transformation. This is largely accredited to the strategic integration of artificial intelligence (AI), a technology poised to redefine established paradigms of efficiency and innovation within the industry.
People’s relationship with food is undergoing a profound transformation. No longer just a source of fuel, what individuals eat is now seen as a cornerstone of the overall well-being—a tool to boost immunity, sharpen focus, support digestion, and build long-term resilience. This evolution in consumer consciousness is creating a powerful demand for foods that are functional, organic, and transparently made with real ingredients.
Tequila, once confined to regional consumption in Mexico, has now become a popular spirit worldwide, known for its rich heritage, skilled craftsmanship, and premium quality. Made from blue agave, tequila has attracted international consumers for its distinct flavor, artisanal qualities, and cocktail versatility.
Avocado oil is a nutritious oil pressed from the pulp of avocados (Persea americana), in contrast with most oils, which are seed derived. Avocado oil is valued for its rich content of monounsaturated fats, especially oleic acid, in addition to necessary vitamins like E, A, and D. Avocado oil has a mild, buttery taste and very high smoke point and is used both in food preparation and cosmetics.
Biscuits are dry, baked foods made from flour and usually crisp in texture and flat in shape, eaten frequently as a snack or with a meal. They consist mostly of wheat flour, sugar, fat (butter or vegetable oil), and leavening agents such as baking powder. Flavors and variety may be added using ingredients like milk solids, chocolate, spices, or dried fruits. Biscuits come in sweet and savory forms, varying from cookies and cream-filled to salted crackers. Their shelf life, which is lengthy, convenient packaging, and broad taste appeal have made them a household staple, school staple, and workplace staple worldwide.
Nutritional powders have become essential nutritional supplements created to address the specific health needs of vulnerable demographics, including diabetic patients, the aged, and the sick. When regular food intake is inadequate or compromised, these powders, which are made with specially designed compositions and are high in vital vitamins, minerals, protein, and carbs, offer balanced nourishment. Specialized baby formulas guarantee the best possible growth and development in the early years of life.
Vegetable oils remain among the world’s most widely used agricultural products, essential to food manufacturing, biofuels, cosmetics, and industrial goods.
Learn key financial strategies, operational and capital cost planning essentials for starting a profitable livestock feed production business in 2025.
World Tea Day, celebrated every year on May 21st, is an opportunity to appreciate the rich history, cultural significance, and economic impact of tea. From its origins in ancient China to its status as a global commodity, tea continues to connect people, cultures, and economies.
Mango pulp is the thick, smooth, and semi-liquid product yielded by crushing or pulping ripened mangoes. It is the inner flesh of the mango fruit extracted, without the skin and seeds. Mango pulp is widely utilized as a base for many food items, including mango juice, nectar, drinks, smoothies, ice creams, desserts, and as a topping for pancakes or yogurt. Mango juice is a cool drink prepared from ripe mangoes' juice. To make mango juice, the ripe mangoes are normally peeled, pitted, and the flesh of the mango is squeezed to get the pulp. The pulp is further treated to remove the juice from any remaining fibers or solids.
Soy sauce is a liquid condiment used extensively in cooking and seasoning food. Produced from fermented soybeans, wheat, salt, and water, it provides a deep umami taste that can be used to enhance different foods. It is a common ingredient in Asian cooking and has become popular worldwide in marinades, stir-fries, dips, and processed foods. Come in various forms including light, dark, and low-sodium, soy sauce meets the different consumer tastes and nutritional requirements, rendering it a vital ingredient in the food industry.
Instant coffee is a quick and easy-to-brew coffee beverage that is produced by brewing coffee beans into a liquid that concentrates and evaporates into powder or grain form. It rapidly dissolves in hot water, so it's highly sought after by customers demanding fast and easy coffee brewing. It has a long storage life and is inexpensive, making it popular in homes, offices, and food service establishments. It is fueled by urbanization, hectic lifestyles, and growing demand for convenience drinks.
Glucose syrup and sorbitol syrup are versatile sweeteners widely used across the food and beverage industry. Their ability to enhance texture, retain moisture, and extend shelf life makes them essential ingredients in confectionery, bakery, dairy, and beverage products. Beyond their functional benefits, these syrups contribute to taste enhancement and product stability, catering to consumer preferences for smooth, consistent formulations.
Potato flakes are a highly adaptable food ingredient created by processing cooked potatoes into thin, dehydrated slices. They are often used in soups, snacks, baked goods, and fast meals and are well-known for their usefulness, taste, and simplicity of usage. These flakes provide a reliable and effective option for home cooking, foodservice, and commercial food production while preserving the natural flavour, texture, and nutritional value of fresh potatoes. They are indispensable in a variety of culinary applications due to their lengthy shelf life, lightweight design, and easy rehydration method. Their ability to be used in a variety of recipes, from thickened stews to crispy coatings, further solidifies their position as a basic component of the world's food industry.
Industrial enzymes are biological catalysts that fast-track the chemical process that is involved during the industrial processes. Their use is mainly seen in the food and beverage, pharmaceutical, textile, biofuel, and detergent industries. This enzyme is very effective as it is energy efficient and has cleaner and greener production. Its stability and specificity make it a wonderful tool for breaking complex molecules while improving product quality and yield. Industrial enzymes can enhance the texture of bread, benefit dairy processing, assist in the production of biofuels, and clean wastewater. All these phenomena illustrate that industrial enzymes are a mandatory requirement to manufacture many more products with sustainability and cost effectiveness for multiple industries.
Sorbitol is a sugar alcohol widely used as a sweetener, humectant, and stabilizer in food, pharmaceuticals, and cosmetics. It is made commercially by hydrogenating glucose and is naturally present in fruits like apples and pears. Because of its mild sweetness, low glycaemic index, and ability to retain moisture, sorbitol is a popular ingredient in skincare, dental care, and sugar-free goods. It is also an essential component of industrial processes and a laxative in medical applications.
Inedible beef tallow, a byproduct of the meat processing industry, is derived from beef suet and serves various industrial and commercial purposes. This versatile substance undergoes rendering, a process that separates the fat from solid components. Inedible beef tallow's primary application is in animal feed, as it provides essential fats and energy for livestock, particularly in pet food and livestock supplements. Additionally, it finds use in the cosmetics and personal care industry, contributing to the production of candles, soaps, and skin-care products.
Vitamin C supplements are typically made by extracting ascorbic acid from various sources, such as citrus fruits, or synthesizing it in a laboratory setting. The extracted or synthesized ascorbic acid is then processed and formulated into different types of supplements, including tablets, capsules, chewable, and powdered forms. One of the primary advantages of Vitamin C supplements is their ability to support a healthy immune system.
Over the recent decade, the online food and grocery delivery business in India has witnessed exponential growth. This expansion is attributed to the increasing penetration of smartphones, the affordability and convenience offered by food delivery app services, and the growing availability of low-cost internet services. The industry has become progressively competitive, with numerous local and international players competing for a significant market share. Nonetheless, despite the extreme competition, global players are continuing to make significant investments in India on account of its significant market share in the global online food delivery market.
‘World Food Day’ is celebrated on October 16th as a global responsibility to abolish hunger. 2024’s theme for the day is ‘Right to foods for a better life and a better future’. This theme highlights the significance of enabling access to nutritious food for all, particularly in the face of global challenges, including poverty, climate change, and conflict. In line with this theme, in October 2024, India and the United Arab Emirates (UAE) announced plans for developing a food corridor between the two nations, with an initial investment of over USD 2 Billion (INR 17,000 Crore) in food processing and logistics for food parks. This project significantly reinforces the UAE's food security while providing support to Indian farmers. The initiative is part of a bigger investment strategy targeting over USD100 Billion across key sectors, including manufacturing, infrastructure, and logistics.
A vegan, or a plant-based diet, focuses mainly on consuming fruits, vegetables, grains, legumes, nuts, and seeds. It excludes all animal-derived products and ingredients, including meat, poultry, fish, dairy, eggs, and honey. Nowadays, people are shifting toward vegan diets for a variety of reasons, such as ethical concerns for animal welfare, environmental sustainability, health benefits, and personal preferences.
Functional foods promote overall well-being and offer specific health benefits beyond daily nutrient intake. These benefits encompass enhanced bone health, effective cholesterol management, improved heart health, and eye health. Functional foods include probiotic yoghurt, omega-3 enriched eggs, fortified milk, antioxidant-rich berries, and functional beverages.
Fusion cuisine and beverages blend different ingredients, flavors, or techniques from various culinary or cultural backgrounds to create unique and innovative flavor profiles in dishes and drinks. Fusion beverages encompass both alcoholic and non-alcoholic options, including cocktails, mocktails, smoothies, teas, and more. These beverages span a spectrum from simple combinations to complex and inventive concoctions. Changing taste preferences and global connectivity are the main reasons for the increasing adoption of fusion beverages. They are available in various product types, such as carbonated drinks, fused teas and coffees, fruit juices, fusion alcoholic beverages, energy drinks, sports drinks, and more. These beverages are accessible through off-trade outlets (hypermarkets, supermarkets, discounters, grocery stores, off-license stores, alcohol and confectionery stores, highly specialized retailers, and online stores), as well as on-trade establishments (pubs, bars, cafés, restaurants, clubs, discos, hotels, mass events, and others). Examples of fusion beverages include fruit-infused tea, Asian-inspired cocktails, spicy margaritas, bubble tea creations, mojito variations, and infused waters. Furthermore, fusion cuisine merges elements from diverse culinary traditions, such as Asian, European, African, or Latin American, to craft new and exciting dishes. Examples of fusion cuisine include sushi burritos, Thai basil pizza, kimchi tacos, and more.