Almond Milk Plant Setup Cost in India: Manufacturing Process Flow, Machinery, DPR & Financial Model 2026
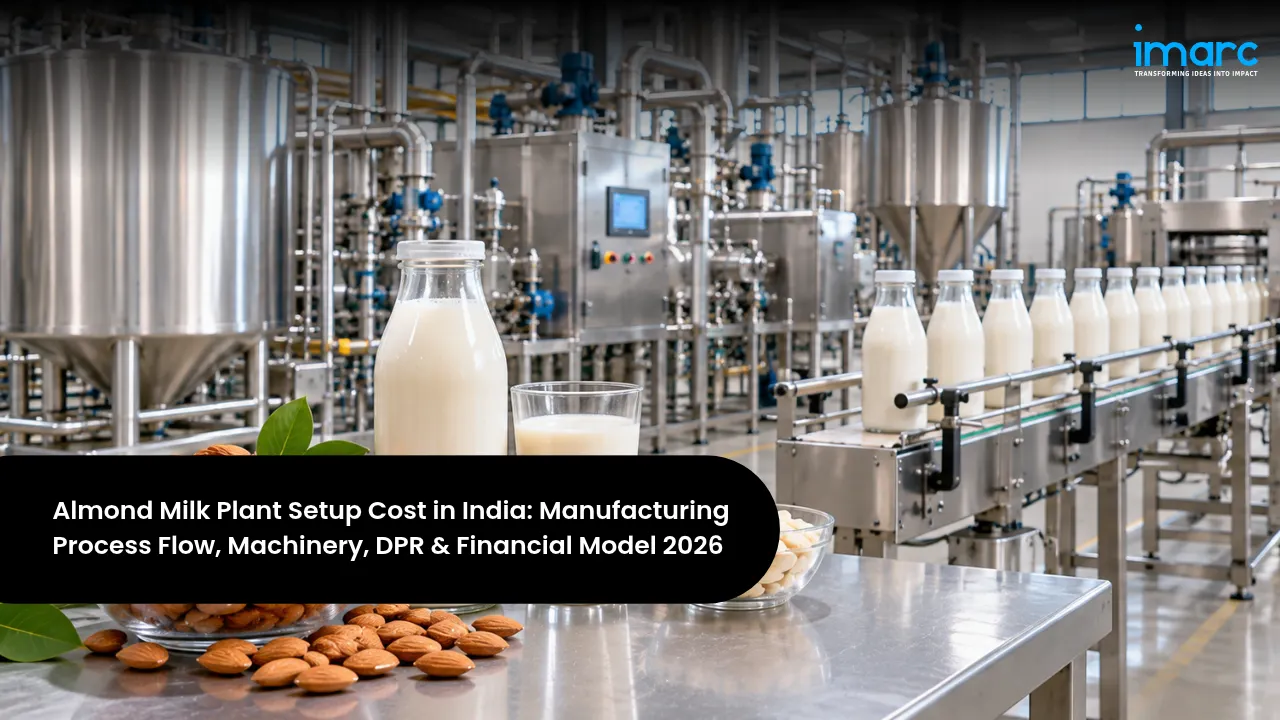
An Almond Milk Manufacturing Plant Setup in India produces a creamy, plant-based beverage made by grinding almonds with water, filtering, blending, and heat-treating the mixture. Almond beverages are naturally lactose-free and cholesterol-free, low in calories in unsweetened form, and suitable for vegan and dairy-free diets, and they are increasingly fortified with calcium and vitamins D and B12. Rising lactose intolerance awareness, vegan and fitness trends, café culture, and quick-commerce growth are expanding demand in India's metro and Tier 1 cities. Under FSSAI's position on dairy terminology, these products are generally labelled as almond beverages or almond-based drinks on pack.
The overall Almond Milk Manufacturing Plant Cost depends mainly on capacity, whether the product is shelf-stable UHT or chilled pasteurised, almond preparation and extraction equipment, homogenisers, UHT and aseptic filling systems, CIP and utilities, hygienic buildings, and working capital for imported almonds and packaging. A UHT plant producing about 5 million litres of almond beverage a year typically needs INR 25 crore to INR 40 crore in fixed assets, or about INR 30 crore to INR 50 crore including working capital, while a smaller chilled almond drink unit of 0.5 to 1 million litres a year in PET bottles can start at around INR 3 crore to INR 6 crore. IMARC Group puts typical capacities at 5 to 10 million litres a year, with gross margins of 35 to 45% and net margins of 15 to 20%.
This guide is written for dairy and beverage companies, plant-based food start-ups, dry fruit processors and importers, FMCG brands, contract manufacturers, and investors exploring how to start a Almond Milk manufacturing plant in India. It explains product types and end uses, demand drivers, the production flow, machinery and raw materials, site selection near almond supply and urban markets, a detailed cost and returns breakdown, the food safety, labelling, and other approvals involved, and how a DPR pulls these elements into a bankable plan.
India Market Snapshot
| Key Facts | Details |
|---|---|
| India Almond Milk Market (2025) | USD 422.1 Million |
| India Market Outlook | USD 1,141.3 Million by 2034, 11.33% CAGR |
| Global Almond Milk Market | USD 12.91 Billion (2025) to USD 36.69 Billion (2034) |
| Typical Plant Capacity | 5–10 Million Litres a year |
| Indicative Total Investment | INR 30–50 Crore (5 Million litres/year, incl. working capital) |
The snapshot shows a fast-growing Indian almond beverage market, which IMARC Group expects to more than double to USD 1,141.3 million by 2034. India imports most of its almonds, largely from the United States, and the India–US interim trade framework of February 2026 includes cuts on tree nut tariffs.
Investment Highlights
Indicative Project Cost in India (2026)
| Parameter | Value |
|---|---|
| Product Range | Unsweetened, sweetened, and flavoured almond beverages; barista blends; UHT cartons and chilled bottles |
| Total Project Investment | INR 30 – 50 Crore incl. working capital (5 Million L/year UHT); INR 3 – 6 Crore (chilled, 0.5–1 Million L/year) |
| Payback Period | 4 – 5 Years |
| Net Profit Margin | 15 – 20% (IMARC benchmark) |
| IRR | 18 – 24% |
| Best Locations | Maharashtra, Haryana (Delhi NCR), Punjab, Karnataka, Gujarat, Jammu & Kashmir |
| Mandatory Approvals | FSSAI License, Legal Metrology, SPCB Consents, Factory License, Packaging EPR, IEC |
| Key Requirement | Quality almonds at good prices, shelf-stable processing, compliant labelling, and strong distribution |
These figures offer a practical frame for early evaluation. Returns depend on sourcing almonds at competitive prices and managing import duties and currency risk, achieving smooth texture and stable products without separation, controlling packaging costs, complying with FSSAI labelling, and building strong distribution. A capacity- and format-specific Almond Milk Feasibility Report refines these numbers before capital is committed.
Table of Contents
- What is Almond Milk Manufacturing?
- Why is Almond Milk Manufacturing Growing in India?
- Almond Milk Manufacturing Process Flow
- Raw Materials Required for Almond Milk Manufacturing
- Location, Land & Infrastructure
- Almond Milk Manufacturing Machinery and Equipment
- Almond Milk Manufacturing Plant Setup Cost in India (CapEx & OpEx)
- Financial Analysis and Profitability
- Licenses and Approvals for Almond Milk Manufacturing in India
- Recent Developments in the India Almond Milk Manufacturing Industry
- How Almond Milk Manufacturing Project Report and DPR Helps Investors
- Frequently Asked Questions
What is Almond Milk Manufacturing?
Almond beverages are made by extracting the nutrients and flavour of almonds into water. Almond kernels are cleaned, sorted, tested for aflatoxins, soaked, and sometimes blanched to remove skins. They are then wet-ground with water in colloid mills to form a fine slurry, and the solids, known as almond pulp, are separated by decanters, separators, or filters. Some producers instead rehydrate almond paste, which simplifies processing. The almond base is blended with sweeteners, flavours, stabilisers, emulsifiers, and fortificants such as calcium and vitamins, then homogenised for a smooth, stable texture. Shelf-stable products are UHT-treated and aseptically filled into cartons, while chilled products are pasteurised and filled into PET or glass bottles. An Almond Milk Manufacturing Plant therefore combines almond preparation, grinding, extraction, blending, homogenisation, heat treatment, filling, packing, and quality testing.
Products are sold through supermarkets and hypermarkets, quick-commerce and e-commerce platforms, cafés, coffee chains, and hotels, gyms and health stores, D2C subscriptions, institutional buyers, and private label and contract manufacturing for FMCG brands. Buyers expect a pleasant, consistent taste, creamy texture without separation, clean labels, good nutrition and fortification, safe and stable shelf life, compliant labelling, and competitive pricing.
- Unsweetened Almond Beverages: Low-calorie options for health-conscious consumers.
- Sweetened and Flavoured Drinks: Chocolate, vanilla, and kesar badam variants.
- Barista Blends: Foamable almond beverages for coffee and tea.
- Co-Products: Almond pulp for bakery, snacks, and flour.
Main Product Types in Almond Beverage Production
The product mix shapes processing, packaging, and margins:
| Product Type | Description | Key Feature | Primary Market |
|---|---|---|---|
| Unsweetened UHT Beverage | Shelf-stable carton | Low calorie, long shelf life | Modern retail, quick commerce |
| Flavoured Beverages | Chocolate, vanilla, kesar badam | Mass appeal | Retail, kids, on-the-go |
| Barista Blend | Higher fat, foam stability | Café performance | Coffee chains, HoReCa |
| Chilled Fresh Beverage | Pasteurised, short shelf life | Premium fresh positioning | D2C, premium stores |
| Almond Pulp & Ingredients | By-product of extraction | Additional revenue | Bakery, snacks, flour |
Many new entrants start with chilled almond drinks in bottles or with contract manufacturing for established brands, which need lower investment, then move into UHT cartons, barista blends, and flavoured ranges as volumes and distribution grow. Barista blends, premium fortified products, and branded retail earn better margins than private label supply.
Why is Almond Milk Manufacturing Growing in India?
Key Growth Drivers in the Indian Market
Demand for almond beverages in India is driven by health, lifestyle, and retail changes. IMARC Group expects the Indian almond milk market to grow at 11.33% a year from 2026 to 2034:
- Lactose intolerance awareness: Many Indians are lactose intolerant, and awareness of dairy-free options is rising.
- Vegan and fitness trends: Urban consumers are adopting vegan, flexitarian, and high-protein diets.
- Café and coffee culture: Coffee chains and cafés offer almond-based options in drinks.
- Quick commerce and e-commerce: Online grocery platforms make premium beverages widely available.
- Lower almond tariffs: The India–US interim trade framework includes cuts on tree nut tariffs, which could reduce almond costs.
End-Use Market Opportunity
| End Use | Demand Driver | Product Role |
|---|---|---|
| Household Consumption | Health and lactose intolerance | Unsweetened and flavoured cartons |
| Cafés & Coffee Chains | Plant-based menu options | Barista blends |
| Gyms & Health Stores | Fitness and vegan diets | Fortified and protein variants |
| Food Processors | Dairy-free desserts and bakery | Almond base and pulp |
| Private Label & Contract | FMCG brand expansion | Contract manufacturing |
The strongest position for an Almond Milk Manufacturing Plant in India combines reliable access to quality almonds, smooth and stable product formulations, UHT and aseptic capability for shelf-stable products, compliant labelling, efficient packaging, and strong distribution through modern retail, quick commerce, cafés, and brand partnerships. Producers that also offer oat, soy, or other plant-based beverages on the same line can improve utilisation.
Almond Milk Manufacturing Process Flow
Understanding the Almond Milk Manufacturing Process helps promoters plan almond preparation, extraction, formulation, heat treatment, filling, layout, staffing, and quality control. Product quality depends on almond quality and freshness, soaking and grinding, particle size, extraction efficiency, stabiliser system, homogenisation pressure, heat treatment, and hygienic filling. The flow below reflects a typical UHT plant with a chilled product option.
Step-by-Step Almond Beverage Production Flow
Almonds are cleaned, tested, soaked, and ground with water, and the pulp is separated. The almond base is blended with ingredients, homogenised, and UHT-treated or pasteurised, then filled aseptically into cartons or into bottles, coded, packed, and stored.
| Unit Operation | Key Activity |
|---|---|
| Almond Receiving & Testing | Sorting, aflatoxin and quality checks |
| Soaking & Blanching | Hydrate and optionally peel almonds |
| Wet Grinding | Colloid mills create almond slurry |
| Extraction & Filtration | Separate almond pulp |
| Blending | Add sweeteners, flavours, stabilisers, fortificants |
| Homogenisation | Create smooth, stable texture |
| UHT or Pasteurisation | Heat treatment for safety and shelf life |
| Aseptic or Clean Filling | Cartons or PET bottles |
| Coding & Packing | Batch coding, shrink wrapping |
| Storage & Dispatch | Ambient or chilled distribution |
Two factors decide profitability. The first is almond cost and content: almonds are the most expensive ingredient and are largely imported, so purchase price, import duties, exchange rates, and the almond percentage in each product strongly influence margins. The second is packaging and distribution efficiency: aseptic cartons and bottles are a large share of cost, and reaching consumers through modern retail, quick commerce, and cafés requires strong distribution, so efficient packaging formats and high line utilisation are essential.
Raw Materials Required for Almond Milk Manufacturing
The main inputs are almonds and water, supported by sweeteners, flavours, stabilisers, fortificants, and packaging. IMARC Group estimates raw materials, mainly almonds, at 70 to 80% of operating cost and utilities at 10 to 15%.
| Raw Material | Role in Process | India Sourcing | % of OpEx |
|---|---|---|---|
| Almond Kernels or Paste | Main ingredient | Imported (mainly US), some Kashmir almonds | 35–45% |
| Sweeteners & Flavours | Taste and variants | Sugar, dates, cocoa, natural flavours | 3–6% |
| Stabilisers, Emulsifiers & Fortificants | Texture, stability, nutrition | Calcium, vitamins, gums, lecithin | 3–5% |
| Treated Water | Base liquid | RO-treated on site | About 1% |
| Packaging (Aseptic Cartons, Bottles, Caps) | Product protection | Aseptic packaging suppliers, PET converters | 20–28% |
India imports most of its almonds, mainly from the United States, with smaller domestic production in Jammu and Kashmir. Almond prices move with global harvests, exchange rates, and import duties, so producers should contract supply ahead, consider almond paste for consistency, test every lot for aflatoxins and quality, and store almonds in cool, dry conditions. Aseptic packaging materials are often supplied with filling systems, so packaging contracts should be negotiated together with equipment.
Location, Land & Infrastructure
Location shapes almond logistics, packaging supply, and access to consumers. The best location for Almond Milk manufacturing plant setup lies close to major urban markets and distribution hubs, with good access to almond importers and dry fruit trading centres, reliable power and clean water, and availability of food technologists and packaging suppliers.
Preferred States for Almond Beverage Plants in India
| State | Why It Works | Key Advantage |
|---|---|---|
| Maharashtra | Mumbai and Pune markets, JNPT port | Large urban demand, almond imports |
| Haryana (Delhi NCR) | Delhi dry fruit trade, NCR market | Almond sourcing and consumers |
| Punjab | Amritsar dry fruit processing hub | Almond handling expertise |
| Karnataka | Bengaluru health-conscious market | Premium and café demand |
| Gujarat | Food parks, Mundra port | Infrastructure and imports |
| Jammu & Kashmir | Domestic almond production | Local almond supply |
Maharashtra and Haryana place producers next to India's largest urban markets and major almond import and trading hubs, while Punjab has long experience in almond handling and processing. Karnataka offers a strong health-conscious and café market around Bengaluru, Gujarat provides food parks and port access, and Jammu and Kashmir offers domestic almond supply. Because almond beverages are often sold chilled or in premium channels, proximity to metro markets reduces distribution cost.
Product Quality, Safety and Labelling Requirements
Almond beverages must meet FSSAI standards for food safety, additives, fortification, and labelling. FSSAI has objected to the use of dairy terms such as "milk" for plant-based products, and although this has been contested in court, most brands label their packs as almond beverages or almond-based drinks. Products must also carry allergen declarations for tree nuts. Key controls include almond aflatoxin testing, water quality, process temperature and pressure records, UHT validation, aseptic integrity tests, microbiological testing, sensory checks, and batch traceability.
Infrastructure Requirements (5 Million Litres/Year UHT Plant)
| Infrastructure Element | Specification | India-Specific Note |
|---|---|---|
| Total Land Area | 1.5 – 3 acres | Or plot in a food park |
| Processing Building | 2,500 – 4,000 m² | Hygienic zones, high-care filling area |
| Power | 500 – 900 kW connected load | UHT, homogeniser, filling, chillers |
| Steam | Boiler for UHT and CIP | Fuel-efficient design |
| Water | 80 – 150 KLD | RO-treated process water, CIP |
| Effluent Treatment | ETP for CIP and wash water | SPCB compliance |
| Warehouses & Laboratory | Almond cold store, FG warehouse, QC lab | Quality and dispatch |
Infrastructure for an almond beverage plant centres on almond storage, a preparation and soaking area, grinding and extraction, blending and homogenisation, UHT or pasteurisation, a high-care aseptic or clean filling area, packing, finished goods storage, utilities such as RO water, boilers, chillers, and compressed air, CIP systems, an effluent treatment plant, and a quality laboratory. Planning space for additional plant-based beverage lines from the outset supports growth.
Almond Milk Manufacturing Machinery and Equipment
Grinding, extraction, blending, and CIP equipment are available from Indian food machinery suppliers, while UHT systems, homogenisers, and aseptic carton fillers are often sourced from global packaging and processing companies. The main equipment is summarised below.
| Equipment | Function | Key Specification |
|---|---|---|
| Almond Sorters & Soaking Tanks | Clean and hydrate almonds | Food-grade stainless steel |
| Blancher & Peeler (optional) | Remove almond skins | Gentle handling |
| Wet Grinders / Colloid Mills | Make almond slurry | Fine particle size |
| Decanter, Separator or Filter | Separate almond pulp | High extraction yield |
| Blending Tanks & High-Shear Mixers | Mix ingredients | Uniform dispersion |
| Homogeniser | Stabilise emulsion | High-pressure, two-stage |
| UHT Plant / Pasteuriser | Heat treatment | Validated time and temperature |
| Aseptic Carton Filler / PET Filling Line | Fill and seal packs | Aseptic or clean filling |
| CIP System | Clean equipment | Automated cleaning cycles |
| RO Plant, Boiler, Chiller & QC Lab | Utilities and testing | Micro and aflatoxin testing |
Equipment selection should follow format and capacity. The homogeniser, UHT system, and aseptic filler largely determine product stability, shelf life, and packaging options, while extraction equipment determines almond yield and texture. Many promoters begin with chilled bottled products or contract UHT processing, then invest in their own UHT and aseptic lines as volumes justify the cost.
Almond Milk Manufacturing Plant Setup Cost in India (CapEx & OpEx)
The tables below summarise the capital and operating cost structure of a UHT almond beverage plant producing about 5 million litres a year in India. The final Almond Milk Investment Cost for a specific project depends on capacity, shelf-stable or chilled format, extraction and processing equipment, UHT and aseptic filling systems, utilities, hygienic building design, land and building costs, and working capital for almonds, packaging, and receivables.
Capital Expenditure (CapEx) Cost Structure
| CapEx Component | % of Total CapEx | What It Covers |
|---|---|---|
| Almond Preparation & Extraction | 10–14% | Soaking, grinding, separation |
| Blending & Homogenisation | 8–10% | Tanks, mixers, homogeniser |
| UHT & Aseptic Filling | 30–35% | UHT plant, aseptic carton filler |
| CIP & Utilities | 10–12% | CIP, boiler, chiller, RO, ETP |
| Packing & QC Laboratory | 4–6% | Packing lines, testing equipment |
| Land & Buildings | 15–18% | Site, hygienic buildings, stores |
| Working Capital | 10–14% | Almonds, packaging, receivables |
UHT processing and aseptic filling form the largest share of investment, followed by buildings, utilities, and extraction. An Almond Milk Business Plan models these components so that capacity, product format, and financing rest on realistic almond prices, almond content per litre, packaging costs, channel margins, and selling prices.
Operating Expenditure (OpEx) Cost Structure
| OpEx Component | % of Total OpEx | India-Specific Note |
|---|---|---|
| Almonds | 35–45% | Mostly imported |
| Packaging | 20–28% | Aseptic cartons, bottles, caps |
| Other Ingredients | 6–10% | Sweeteners, stabilisers, fortificants |
| Utilities | 8–12% | Steam, power, water, chilling |
| Labour | 4–6% | Operators, food technologists, QA |
| Logistics & Distribution | 4–6% | Ambient or cold chain delivery |
With almonds and packaging forming most of operating cost, profitability depends on almond sourcing, almond content, packaging efficiency, utilisation, and channel margins. A sound financial model should test margins against higher almond prices or duties, rupee depreciation, packaging cost increases, higher retail and quick-commerce commissions, slower category growth, and labelling or regulatory changes.
Financial Analysis and Profitability
Almond beverage manufacturing offers attractive returns for producers with good sourcing and strong channels. The profitability of Almond Milk manufacturing business in India improves with competitive almond procurement, optimised almond content and recipes, high utilisation of UHT and filling lines, a mix of branded, barista, and contract products, efficient packaging, strong presence in quick commerce, modern retail, and cafés, and use of almond pulp as a co-product.
| Financial Metric | Indicative Value | India Context |
|---|---|---|
| Gross Profit Margin | 35–45% | IMARC benchmark |
| Net Profit Margin | 15–20% | After depreciation and Indian corporate taxes |
| Payback Period | 4–5 Years | Moderate capital needs |
| IRR (Internal Rate of Return) | 18–24% | Sensitive to almond prices and channel costs |
| Capacity Utilization (stable ops) | 55–75% | Linked to brand and contract volumes |
| Break-even Capacity Utilization | 40–50% | Packaging and marketing overheads |
Sourcing and distribution are the decisive factors. Almond beverages sell at premium prices, but almond and packaging costs are high and brand building takes investment, so producers that combine efficient sourcing with strong distribution or contract manufacturing earn the best returns. Running other plant-based beverages on the same line improves utilisation and spreads fixed costs.
Returns can be strengthened by contracting almonds ahead of harvest, using almond paste for consistency, optimising recipes for taste and cost, offering contract manufacturing and private label, launching barista blends for cafés, adding oat and other plant-based beverages, selling almond pulp to bakeries and snack makers, and building direct and quick-commerce channels.
Key Risks and Mitigation
The main risks are almond price volatility and import dependence, currency movements, packaging cost increases, regulatory uncertainty over dairy terminology, competition from established brands and imported products, high retail and quick-commerce commissions, and product stability or food safety issues. Sourcing risk is reduced through contracts and diversified supply; regulatory risk through compliant labelling; competition through quality, taste, and innovation; channel risk through diversified distribution; and safety risk through validated processes and testing.
Licenses and Approvals for Almond Milk Manufacturing in India
An almond beverage unit requires food safety, labelling, environmental, industrial, and business approvals. Promoters typically need the following before starting commercial production:
- FSSAI License: A Central or State FSSAI license based on capacity and product category, with compliance with food safety, additive, fortification, and labelling regulations.
- Labelling Compliance: Product names and claims that follow FSSAI guidance on dairy terminology, along with allergen, nutrition, and veg logo declarations.
- Legal Metrology Registration: Registration for pre-packaged products with correct declarations of net quantity, MRP, and manufacturer details.
- Pollution Control Consents: Consent to Establish and Consent to Operate from the State Pollution Control Board, covering wash water and CIP effluent.
- Factory, Boiler and Fire Approvals: Factory license, boiler registration, and fire safety approval.
- Packaging EPR and Certifications: Plastic packaging EPR registration, with FSSC 22000 or ISO 22000 often required by retailers and export buyers.
- Business and Import Registrations: Company registration, GST, Udyam, and an Import Export Code for importing almonds and equipment.
FSSAI licensing, labelling compliance, and pollution consents usually sit on the critical path. Engaging an Almond Milk Manufacturing Consultant in India can help promoters develop formulations, select processing and filling technology, secure almond supply, design compliant labels, obtain approvals, and build retail, café, and contract manufacturing channels.
Note: The exact approvals, registrations, licenses, and certification requirements may vary depending on factors such as plant location, product range, capacity, target customers, and applicable regulations. Businesses are advised to undertake a detailed regulatory assessment during the project planning stage to ensure full compliance and timely implementation.
Recent Developments in the India Almond Milk Manufacturing Industry
Several recent developments are shaping almond beverage demand in India and globally:
- New Indian almond beverage launches: In September 2024, Maiva Fresh launched an unsweetened almond beverage fortified with vitamins B12 and D, reflecting continued product innovation in India's plant-based segment.
- Global innovation in almond drinks: In August 2025, Califia Farms launched organic seasonal almond creamers and a rice-and-almond horchata drink, showing the global shift toward café and indulgent almond formats.
- Tree nut tariff cuts in India–US trade framework: In February 2026, India and the United States announced an interim trade framework under which tariffs on tree nuts, including almonds, are set to be cut, potentially lowering almond costs for Indian processors.
Together these point to rising product innovation and potentially lower raw material costs. For new entrants, success depends on sourcing, taste, compliant labelling, and distribution.
How Almond Milk Manufacturing Project Report and DPR Helps Investors
A detailed Almond Milk Project Report gives investors a structured roadmap covering demand by channel and region, consumer preferences, product mix, almond sourcing, formulation, process design, machinery, packaging, utilities, approvals, labelling, distribution, and economics. It helps promoters choose the right capacity, format, and product range, estimate capital expenditure (CapEx) and operating expenditure (OpEx), assess profitability, and identify risks before implementation.
At the core of the DPR is an Almond Milk Financial Model covering almond prices and content per litre, ingredient and packaging costs, utilities, labour, channel margins and commissions, marketing, logistics, working capital, cash flow projections, break-even, return on investment (ROI), and payback. Because almond prices, packaging, and channel costs drive returns, lenders expect detailed sensitivity analysis, which is why many promoters engage an Almond Milk Plant Project Report Consultant in India to prepare bank-ready documents.
For an almond beverage project specifically, a strong DPR also answers the questions that matter most: whether to start with chilled or shelf-stable products, how much almond content to use, how lower almond tariffs would change costs, which channels and partners to build first, and how returns hold up if almond or packaging prices rise. An experienced Almond Milk Manufacturing Feasibility Study Consultant tests these scenarios so that the final plan is one lenders and partners can back with confidence.
Frequently Asked Questions
How do I set up an almond milk manufacturing unit in India?
Start by defining products, formats, and target channels, and commission a feasibility study and DPR. Choose a site near urban markets and almond suppliers, install almond preparation, grinding, extraction, blending, homogenisation, UHT or pasteurisation, and filling equipment, obtain FSSAI, Legal Metrology, pollution, and factory approvals, design compliant labels, and build retail, café, and contract channels.
What is the cost of setting up an almond milk manufacturing plant in India?
A UHT plant producing about 5 million litres a year typically needs INR 25 crore to INR 40 crore in fixed assets, or about INR 30 crore to INR 50 crore including working capital. A smaller chilled unit of 0.5 to 1 million litres a year can start at around INR 3 crore to INR 6 crore.
How is almond beverage made?
Almonds are cleaned, tested, soaked, and ground with water, and the pulp is separated. The almond base is blended with sweeteners, flavours, stabilisers, and fortificants, homogenised, UHT-treated or pasteurised, and filled into cartons or bottles.
What machinery is needed for an almond milk manufacturing plant?
Key equipment includes almond sorters, soaking tanks, blanchers, wet grinders or colloid mills, decanters or separators, blending tanks, high-shear mixers, homogenisers, UHT plants or pasteurisers, aseptic carton fillers or PET filling lines, CIP systems, RO plants, boilers, chillers, and a quality laboratory.
What raw materials are used for almond milk manufacturing?
The main inputs are almond kernels or paste and treated water, along with sweeteners, flavours, stabilisers, emulsifiers, calcium and vitamin fortificants, and packaging such as aseptic cartons, bottles, and caps.
Is almond milk manufacturing profitable in India?
Benchmark figures point to a 15 to 20% net margin and an IRR of around 18 to 24%, with payback in 4 to 5 years. Profitability depends mainly on almond prices and content, packaging costs, channel margins, utilisation, and brand strength.
What licenses are needed for an almond milk manufacturing unit in India?
A unit typically needs an FSSAI license, labelling that complies with FSSAI guidance, Legal Metrology registration, State Pollution Control Board consents, a Factory License, boiler registration, Fire NOC, packaging EPR registration, GST, and an Import Export Code for almond imports.
Which state is best for an almond milk manufacturing plant?
Maharashtra, Haryana, Punjab, Karnataka, Gujarat, and Jammu and Kashmir are strong options. The best site combines access to almond supply with proximity to large urban markets and distribution hubs.
How do I get a feasibility study or DPR for an almond milk manufacturing plant?
A professionally prepared DPR covers market and channel assessment, formulation and technical design, approvals, costs, and financial projections for bank appraisal. Many promoters work with an Almond Milk Business Plan Consultant in India to prepare it and align it with lender requirements.
Our Clients
Contact Us
Have a question or need assistance?
Please complete the form with your inquiry or reach out to us at
Phone Number
+91-120-433-0800+1-201-971-6302
+44-113-547-7077
Previous Post

A Pea Protein Powder Manufacturing Plant Setup in India extracts high-quality protein from yellow and field peas for sports nutrition, protein supplements, dairy alternatives, meat analogues, bakery, beverages, infant and clinical nutrition, and pet food.
An Edible Vegetable Oil Manufacturing Plant Setup in India produces one of the country's most essential food staples. Edible oils such as palm, soybean, sunflower, mustard, groundnut, rice bran, and cottonseed oil are used in every household kitchen and by restaurants, caterers, bakeries, snack and namkeen makers, and packaged food companies.
An Olive Manufacturing Plant Setup in India turns raw or bulk-brined olives into ready-to-eat table olives and related products for India's fast-growing pizza, restaurant, retail, and online grocery markets.
Food safety testing rarely makes the news, yet it is one of the steadiest growth markets in food. According to IMARC Group, the global food safety testing market was valued at USD 27.16 Billion in 2025 and is expected to reach USD 53.62 Billion by 2034, growing at a CAGR of 7.85% during 2026-2034. That is roughly USD 26.5 Billion of new annual value in under a decade.
The tequila market is moving from a regional specialty to a mainstream global spirits category, with value increasingly concentrated in premium, additive-free and cocktail-led products. IMARC Group estimates the global tequila market at USD 20.3 Billion in 2025, and projects it to reach USD 47.8 Billion by 2034, expanding at a CAGR of 9.99% during 2026-2034.
A Guar Gum Processing Plant Setup in India builds on one of the country's most distinctive agricultural advantages. Guar gum is a natural polysaccharide obtained from the endosperm of the guar bean, grown mainly in the arid regions of Rajasthan, Gujarat, Haryana, and Punjab.
A Banana Wine Manufacturing Plant Setup in India links the world's largest banana crop with one of the country's fastest-growing alcoholic beverage categories.
A Food Processing Plant Setup in India gives investors access to one of the country's largest and most resilient industries. India is among the world's biggest producers of milk, fruits, vegetables, grains, pulses, and spices, yet only a part of this output is processed before it reaches consumers.
An Oleoresin Manufacturing Plant Setup in India builds on the country's position as the world's largest producer and exporter of spices and spice extracts.
A Fish processing Plant Setup in India links one of the world's largest fish producing nations with fast-growing domestic and global demand for safe, convenient seafood.
The India microgreens market is moving from a niche urban farming category into a mainstream fresh produce line, and the redistribution of demand toward quick commerce and online grocery is doing much of the pushing. According to IMARC Group, the market stood at USD 87.67 Million in 2026 and is projected to reach USD 158.56 Million by 2034, expanding at a CAGR of 7.69% during 2026-2034.
A Coconut Processing Plant Setup in India builds on the country's position as the world's largest coconut producer. Modern coconut processing turns fresh nuts into higher-value products such as desiccated coconut, virgin coconut oil, coconut milk and cream, and packaged coconut water, while shells and husks become feedstock for charcoal, activated carbon, coir, and coco peat.
A Castor Oil Processing Plant Setup in India builds on one of the country's clearest global leadership positions. India grows most of the world's castor seed and supplies the large majority of internationally traded castor oil, with production concentrated in North Gujarat and neighbouring Rajasthan.
A Baby Food and Infant Formula Manufacturing Plant Setup in India is one of the most demanding food processing projects, because the products feed the most vulnerable consumers.
A Gelato Manufacturing Plant Setup in India targets the premium end of one of the country's fastest-growing food categories.
A Whiskey Manufacturing Plant Setup in India places investors in the world's largest whiskey market by volume. Whiskey dominates India's spirits consumption, ranging from mass-market blends to premium Indian single malts that now win international awards and compete with Scotch on the shelf.
The global coffee packaging market size reached USD 910.9 Million in 2025 and is projected to climb to USD 1,388.1 Million by 2034, registering a CAGR of 4.65% during 2026-2034. That trajectory is moderate by consumer-packaging standards, but it understates how much structural change is compressed into it.
A Potato Starch Manufacturing Plant Setup in India builds on the country's position as the world's second-largest potato producer. Potato starch is a fine, white, neutral-tasting powder extracted from potatoes, valued for its high viscosity, clear gels, binding strength, and clean flavour.
A Mineral Water Processing Plant Setup in India serves one of the most essential and fastest-growing consumer categories in the country.
Setting up a Sugar Manufacturing Plant in India means entering one of the country's largest and most policy-shaped agro-industries.
A Ghee Manufacturing Plant Setup in India builds on one of the country's most trusted and widely consumed dairy products. Ghee, or clarified butter, is made by heating butter or cream until the water evaporates and the milk solids separate, leaving a golden, aromatic fat with a long shelf life.
A Cashew Nut Manufacturing Plant Setup in India builds on one of the country's oldest and most export-oriented agro-processing industries.
Setting up a Whey Protein Powder Manufacturing Plant in India addresses a striking gap in the world's largest milk-producing nation. India produces close to 250 million tonnes of milk a year, yet it imports an estimated 80 to 90% of the supplement-grade whey used by its fast-growing sports nutrition and protein brands.
The Indian animal feed market is being reshaped less by what happens inside a feed mill than by what appears on Indian dinner plates. According to IMARC Group, the market was valued at INR 1,186.30 Billion in 2025 and is projected to reach INR 2,112.96 Billion by 2034, expanding at a CAGR of 6.6% over 2026-2034.
Setting up a Pectin Manufacturing Plant in India is a timely, import-substitution opportunity in a fast-growing food ingredients segment.
Peanut spread is a smooth or crunchy paste made by roasting, skinning, and grinding groundnuts, often with a little salt, sugar, and a stabiliser. It is rich in protein and healthy fats, and in India it has moved from a niche import to an everyday breakfast and fitness food sold through supermarkets, pharmacies, gyms, and online stores.
The organic and natural pet food market has moved from a specialist shelf in independent pet stores to a structural growth engine inside global pet care. According to IMARC Group, the global natural pet food market reached USD 33.6 Billion in 2025 and is projected to reach USD 59.4 Billion by 2034, expanding at a CAGR of 6.33% during 2026-2034.
Edible oils are produced by pressing and solvent-extracting oilseeds such as soybean, mustard, groundnut, and sunflower, or by importing crude palm, soybean, and sunflower oil, and then refining them through degumming, bleaching, and deodorisation to remove impurities, colour, and odour before packing them for homes, restaurants, and food processors.
Club soda is purified water chilled and charged with food-grade carbon dioxide under pressure, then filled into PET bottles, glass bottles, or cans and sealed so that it keeps its fizz until opened.
Ice cream is a frozen dairy dessert made by pasteurising and homogenising a mix of milk, cream, sugar, stabilisers, and flavours, then freezing it while whipping in air and hardening it at very low temperatures.
CNSL, the dark, viscous liquid held in the honeycomb of the cashew shell, is recovered by pressing shells left over from kernel processing and then heating the crude liquid so that its anacardic acid turns into cardanol.
Ground spices and blended masalas turn whole chilli, turmeric, coriander, cumin, pepper, and other spices into clean, safe, ready-to-use powders and mixes for homes, restaurants, food processors, and export buyers.
Fishmeal is a brown, protein-rich powder made by cooking, pressing, drying, and grinding small oily fish and fish processing waste, with fish oil recovered as a valuable co-product.
Dried banana ingredients are made by washing, peeling, and slicing fresh fruit, treating it to prevent browning, drying it in belt, tray, or spray dryers, and milling it into a fine, shelf-stable product.
Dried egg is made by breaking fresh eggs, pasteurising the liquid whole egg, yolk, or white, and spray drying it into a fine powder that keeps for a year or more without refrigeration.
Whey is the liquid left after milk is made into cheese or paneer, and it contains high-quality proteins that can be separated by membrane filtration and spray dried into concentrates and isolates.
The pectin market has moved from the back of the ingredient label to the centre of product development strategy. As food manufacturers strip out synthetic gelling agents, stabilisers and thickeners, pectin has become one of the few hydrocolloids that can deliver texture and shelf stability while still reading as a familiar, fruit-derived ingredient.
Poultry processing turns live broilers into hygienically slaughtered, chilled, cut, and packed meat, ready for retail shelves, restaurants, quick-service chains, caterers, and export. India produced about 10.5 million tonnes of meat in 2024-25, and poultry made up roughly half of it at 5.18 million tonnes, yet around 85% of birds are still sold live or slaughtered in small wet-market shops.
The global tomato ketchup market reached USD 20.8 Billion in 2025 and is projected to reach USD 26.3 Billion by 2034, growing at a CAGR of 2.68% during 2026-2034, according to IMARC Group. Those numbers describe a mature, high-volume condiment category rather than a fast-growing one.
Coconut shell powder is made by cleaning, drying, crushing, and finely grinding the hard inner shell of the coconut into a uniform powder. Because the shell is dense, rich in lignin, low in ash, and slightly oily, the powder is an excellent natural filler.
Dextrins are modified starches made by heating dry starch, usually with a small amount of acid, so that its long molecules break into shorter ones. The result is a powder that dissolves easily in water and forms strong, quick-drying adhesive films.
Fruit powders are made by drying fruit pulp or juice into a fine, free-flowing powder that keeps the flavour, colour, and much of the nutrition of fresh fruit while lasting months without refrigeration.
Yeast is a living microorganism that makes bread rise, ferments beer, wine, and spirits, turns sugar into fuel ethanol, and supplies protein, vitamins, and flavour to food, feed, and nutrition products.
The global champagne market is entering a phase where value growth matters more than volume growth. IMARC Group values the market at USD 6.6 Billion in 2025 and projects it to reach USD 8.1 Billion by 2034, expanding at a CAGR of 2.25% during 2026-2034.
India is one of the world's leading coffee producers and exporters, growing shade-grown arabica and robusta in the hills of Karnataka, Kerala, and Tamil Nadu and supplying green, roasted, and instant coffee to more than 100 countries.
The Australia Online Grocery Industry has crossed the point where volume growth is the scarce commodity. What is scarce now is profitable volume. According to IMARC Group, the market reached USD 17.22 Billion in 2025 and USD 21.91 Billion in 2026, and is projected to reach USD 96.59 Billion by 2034, expanding at a CAGR of 20.37% (2026–2034), a more than five-fold expansion in under a decade. That growth is unfolding inside one of the most closely regulated grocery markets in the developed world.
Baby formula, also known as infant formula, is a manufactured food product designed to serve as a substitute for or supplement to human breast milk for infants and young children up to three years of age.
Palm oil is the world's most widely used vegetable oil, extracted from the fruit of the oil palm and used in cooking oils, vanaspati, bakery fats, snacks, soaps, cosmetics, and oleochemicals, while the kernel yields palm kernel oil and cake.
Beer is one of the world's most widely consumed drinks, brewed from malted barley, water, hops, and yeast, often with rice or maize as adjuncts. In India, beer accounts for only a small share of alcohol consumption compared with most countries, but that is changing as a young, urban, and increasingly female consumer base embraces lighter drinks, premium lagers, wheat beers, and craft styles.
Bread, buns, rusk, cakes, cookies, and biscuits are part of daily meals and snacking in almost every Indian household, from metro cities to small towns.
Makhana has moved from a pond crop traded through village aggregators into a branded snack with its own export code and a national board behind it. According to IMARC Group, the India makhana market was valued at INR 9.29 Billion in 2025 and is projected to reach INR 19.95 Billion by 2034, growing at a CAGR of 8.85% (2026–2034).
Packaged drinking water has become an everyday essential in India, sold at railway stations, highway dhabas, offices, weddings, hotels, and homes. Concerns about groundwater contamination, rising incomes, travel and tourism, and hot summers keep demand growing year after year, and the market is worth more than USD 8 billion.
Every year, India's vehicles, machinery, and industries consume around 3 million tonnes of lubricants, making the country one of the world's largest lubricant markets.
Indian wine has come a long way from a niche curiosity to a genuine lifestyle category. Young urban consumers, growing interest in food pairing, wine tourism in regions such as Nashik and Nandi Valley, and supportive state grape policies have given domestic wineries room to grow, while producers have steadily improved quality and won international recognition.
Setting up an Extra Neutral Alcohol Manufacturing Plant in India is a fermentation-and-distillation venture anchored to the large and growing alcoholic-beverage industry, along with pharmaceutical, cosmetic, and industrial demand.
Setting up a Shrimp Processing Plant in India is a high-potential, export-oriented venture, powered by the country's position as one of the world's largest shrimp producers and exporters. India's vast coastline, expanding vannamei aquaculture, and strong demand from the United States, China, the European Union, and Japan make a frozen shrimp processing Plant Setup in India one of the most attractive opportunities in the seafood sector.
India's post-pandemic food delivery boom, followed by the new quick-commerce disruption from Zepto Cafe and Swiggy Bolt, has turned the Cloud Kitchen Market in India into a genuine focus of global investor curiosity.
The total addressable market for India's functional beverages is expanding from USD 6.9 Billion in 2025 to a projected USD 18.8 Billion by 2034, growing at a CAGR of 10.74% (2026–2034).
The halal food market has moved well beyond a religious-compliance niche into one of the largest, fastest-growing consumer food categories in the world. The global market was valued at USD 2,956.4 billion in 2025 and is projected to reach USD 6,329.3 billion by 2034, expanding at a compound annual growth rate (CAGR) of 8.56% between 2026 and 2034.
India’s dairy industry is undergoing a structural transformation, driven by rising incomes, urbanization, changing consumption patterns, and strong policy support. Traditionally dominated by an unorganized and cooperative-led system, the sector is now evolving into a more competitive, branded, and technology-enabled ecosystem.
Cheese is a dairy food made by coagulating the proteins in milk, mainly casein, using enzymes, acids, or microorganisms, followed by separating the curds from the whey. Cheese can be made from the milk of cows, buffaloes, goats, sheep, or a combination of these. The coagulated curd is then processed by cutting, cooking, pressing, salting, and aging to achieve desired texture, moisture, and flavor characteristics.
Avocado oil is a vegetable oil that is extracted from the pulp of ripe avocados (Persea americana), unlike other vegetable oils that are extracted from seeds. Avocado oil contains high amounts of monounsaturated fatty acids, specifically oleic acid, as well as phytosterols, tocopherols, and carotenoids. Avocado oil can be classified as extra virgin, virgin, or refined, depending on the extraction and refining process.
Wine is a type of alcoholic drink that is made by the controlled fermentation of grape juice, where the natural or added yeast ferments the sugars in the juice to produce ethanol, carbon dioxide, and other compounds. Wine is made up of water, ethanol, organic acids, phenolic compounds, aromatic esters, and trace minerals.
Whey protein is a high-quality, complete protein obtained from whey, which is the liquid by-product of cheese production. Milk coagulated with enzymes or acids separates into curds (casein) and whey. Whey is a liquid that contains soluble proteins like beta-lactoglobulin, alpha-lactalbumin, serum albumin, and immunoglobulins. Whey is filtered and dried to produce commercial products like whey protein concentrate (WPC), whey protein isolate (WPI), and whey protein hydrolysate (WPH).
Whole egg powder is a dehydrated egg ingredient made by spray drying homogenized liquid whole eggs, which include a mixture of egg yolk and egg white in their natural ratio. Fresh whole shell eggs are broken, filtered, pasteurized, and then processed into a stable powder form using controlled drying methods. The final product preserves the functional and nutritional qualities of fresh eggs, such as high-quality protein, essential amino acids, lipids, vitamins, and emulsifying fractions.
Tea is a drink made from the processed leaves and flower buds of the plant Camellia sinensis. The essential properties of tea, namely flavor, aroma, color, and strength, depend on the level of oxidation, drying, and fermentation of the processed leaves. Tea can be categorized based on the processing techniques into black tea, green tea, oolong tea, white tea, and specialty teas.
Soy milk is a plant-based beverage made from whole soybeans that have been soaked, ground, and their liquid extracted, then cooked and filtered. It is completely devoid of elements originating from animals and is intended to operate and look like dairy milk. In addition to naturally existing proteins, carbs, and healthy fats from soybeans, soy milk is frequently supplemented with vitamins and minerals to improve its nutritional value.
Soya chunks are a protein-rich food item that is prepared using defatted soy flour, which is a by-product of soybean oil extraction. Soya chunks are prepared using the process of extrusion cooking, which converts the soy flour into porous, sponge-like granules with a fibrous structure that resembles meat when rehydrated.
Soya chunks are a protein-rich food item that is prepared using defatted soy flour, which is a by-product of soybean oil extraction. Soya chunks are prepared using the process of extrusion cooking, which converts the soy flour into porous, sponge-like granules with a fibrous structure that resembles meat when rehydrated. Soya chunks have a neutral flavor, which helps them absorb the flavors of spices and seasonings while cooking.
Saudi Arabia’s precast concrete market reached USD 1.2 Billion in 2024 as per the IMARC Group, clear proof that off-site construction is rapidly becoming the Kingdom’s go-to building solution. With residential, commercial, and major infrastructure projects multiplying, developers are increasingly turning to precast building solutions to keep pace.
The global emergency food market has emerged as a critical component of household preparedness infrastructure, disaster response frameworks, and government stockpiling programs worldwide. In March 2025, the National Disaster Response Force (NDRF), established in India, conducted a National Capacity Building Competition for State Disaster Response Forces (SDRFs) to improve their readiness and effectiveness in managing collapsed structure emergencies.
The Saudi Arabia sauces and seasonings market size is expanding steadily as consumers embrace more diverse flavors, convenient food formats, and global culinary influences. Evolving lifestyles, greater exposure to international cuisines, and a strong shift toward home cooking have collectively shaped the contemporary marketplace.
The GCC chocolate market has experienced robust expansion in recent years, driven by evolving consumer preferences, rising disposable incomes, and the proliferation of international brands. In 2024, the GCC chocolate market size reached USD 3,200.77 Million, reflecting sustained growth across premium, artisanal, and mass-market segments.
The Gulf Cooperation Council (GCC) region continues to position itself as one of the fastest-evolving markets for packaged beverages, with bottled water standing at the forefront of this transformation. The GCC bottled water market size has expanded steadily in recent years, supported by a strong shift toward health-driven consumption, improved hydration awareness, and evolving lifestyle patterns across the member countries.
India’s pet sector has experienced a remarkable transformation, driven by urbanization, evolving lifestyles, and a stronger emotional bond between people and their companion animals. What was once a niche trend among a few urban families has now become a widespread practice across Indian households, where pets are regarded as integral members of the family.
Shrimp is one of the world’s most precious natural spices, derived from the dried red stigmas of the Crocus sativus flower. Each bloom yields only a few delicate stigmas, which must be carefully hand-harvested, dried, and processed to preserve their vibrant color, distinctive aroma, and rich flavor. The spice’s deep golden-yellow hue, bitter-sweet taste, and unique fragrance are primarily attributed to its key bioactive compounds like crocin, picrocrocin, and safranal.
The Australian craft beer industry has emerged as a significant segment of the broader alcoholic beverages market driven by evolving consumer preferences, rising disposable incomes, and a growing appreciation for artisanal and premium products. Over the past decade, the market has witnessed substantial expansion with craft breweries increasingly occupying a distinct niche in the highly competitive beer sector.
India is witnessing a profound transformation in how its citizens approach health and wellness. The nutritional supplements market of the country has evolved from a niche segment into a mainstream industry serving millions of health-conscious consumers.
Sea salt is a natural mineral product obtained through the solar evaporation of seawater, followed by harvesting, washing, drying, grading, and packaging. Unlike refined table salt, which undergoes heavy chemical processing, sea salt production relies primarily on solar energy and natural crystallization, allowing it to retain trace minerals such as magnesium, calcium, and potassium that contribute to its distinct taste and nutritional value.
Saffron is one of the world’s most precious natural spices, derived from the dried red stigmas of the Crocus sativus flower. Each bloom yields only a few delicate stigmas, which must be carefully hand-harvested, dried, and processed to preserve their vibrant color, distinctive aroma, and rich flavor.
The India edible oil market stands as one of the most dynamic sectors within the country's consumer goods landscape. As households increasingly prioritize quality, health, and convenience, demand for diverse oil varieties continues to surge. The transformation from traditional purchasing habits to modern retail experiences reflects broader shifts in consumer awareness and lifestyle choices.
India's organic food industry stands at the intersection of health consciousness, agricultural innovation, and sustainable practices. As consumers increasingly prioritize chemical-free nutrition and environmental sustainability, the sector faces transformative opportunities alongside significant operational challenges shaped by evolving dietary preferences, technology adoption in agriculture, and regulatory frameworks that collectively define market dynamics.
Japan’s gluten-free foods and drinks market has evolved into a vibrant segment of the country’s growing health and wellness culture. Once catering mainly to individuals with celiac disease or gluten intolerance, gluten-free products now appeal to a broader demographic pursuing balanced, wellness-oriented lifestyles.
The GCC coconut water market is experiencing remarkable momentum as consumer preferences shift decisively toward natural hydration solutions and functional beverages. This transformation is propelled by heightened health consciousness, expanding fitness culture, and growing awareness of the nutritional benefits associated with coconut-based drinks.
The Saudi Arabia online grocery market is experiencing transformative growth, driven by widespread digital adoption, evolving consumer preferences, and strategic government initiatives aligned with Vision 2030. As one of the fastest-growing e-commerce segments in the Middle East, the online grocery sector is reshaping how Saudi consumers shop for everyday essentials.
Onion powder is a dehydrated and ground seasoning that results from the drying of fresh onions into a concentrated powdered form. The process of dehydration removes moisture from the product, while maintaining the flavor, aroma, and pungency characteristics of the onion, thereby making it a stable and ready-to-use ingredient with a longer shelf life. Onion powder can be prepared through various controlled drying, grinding, and screening processes from white, red, or yellow onion varieties.
Japan's animal feed industry stands as a cornerstone of the nation's agricultural infrastructure, supporting domestic livestock production and ensuring food security. The sector encompasses diverse feed products for cattle, swine, poultry, and aquaculture operations that sustain Japan's protein supply chain.
Nutraceuticals are bioactive, health-enhancing products derived from food sources, botanical ingredients, or purified nutrients that provide physiological benefits beyond basic nutrition. They include dietary supplements, functional foods, fortified beverages, herbal extracts, probiotics, omega-fatty-acid formulations, vitamins, minerals, and specialized nutritional compounds. Nutraceuticals are designed to support wellness, prevent nutrient deficiencies, and promote specific health outcomes, including the improvement of immunity, digestive balance, cognitive function, metabolic health, or cardiovascular support.
India's spice industry stands as a vibrant cornerstone of the nation's agricultural economy and cultural identity. As global consumers increasingly seek authentic flavors and natural ingredients, India's position as the world's leading spice producer continues to strengthen.
According to IMARC Group, India's ice cream consumption has grown nearly fourfold over the past decade. Despite this, India's per-capita consumption stands at just ~400 ml per year — far below the global average of ~2.5 litres. That gap is not a weakness. It is the single most compelling argument for the industry's long-term runway.
Millet represents a group of small-seeded cereals, primarily from the Poaceae family, which are grown as staple foods for thousands of years in Asia and Africa and, increasingly, in other parts of the world. These cereals include pearl millet, foxtail millet, finger millet, proso millet, barnyard millet, and little millet.
Milk powder is a type of dehydrated dairy product, which is manufactured by removing almost all moisture from liquid milk by means of various evaporation and drying techniques. The resultant product is a stable, shelf-friendly powder containing most of the nutritional components of milk, including proteins, lactose, minerals, and fats. Milk powder may be prepared from whole, skimmed, or partially skimmed milk, depending on its intended use. The very low moisture content inhibits microbial growth and spoilage; hence, it becomes more feasible regarding transport, storage, and usage in different formulations.
Meat generally denotes the animal tissues that are consumed and mainly include muscle fibers, though the content of fat, connective tissue, and moisture may vary. There are a number of sources, although they are mainly livestock such as cattle, pigs, sheep, poultry, and, in some regions, game animals.
Australia's tea market is at a crossroads, undergoing extraordinary change inspired by changing consumption habits, health awareness, and the explosion of functional drinks.
The Australia dairy industry stands as a vital pillar of the nation's agricultural economy, representing the third-largest rural sector and contributing significantly to both domestic food security and export earnings.
India has emerged as one of the fastest-growing fisheries producers in the world, backed by rising health awareness, export diversification, and evolving aquaculture technology.
Ice cream is a frozen dairy dessert made by blending milk, cream, sugar, and flavorings, then freezing the mixture while incorporating air to give a smooth, creamy texture. The mixture is pasteurized, homogenized, then churned under controlled conditions to prevent the formation of large ice crystals. Depending on the recipe and product category, it may contain stabilizers, emulsifiers, fruits, nuts, chocolate, or other inclusions. It comes in hardpacked ice cream, softserve, gelato, sorbets, and frozen yogurt. The texture, flavor, and quality of this frozen dessert will depend on the ratios of ingredients used and the techniques followed in processing.
The Philippines mushroom industry is undergoing a transformative phase, driven by a growing consumer shift toward functional and nutrient-dense foods. As health awareness rises across both urban and rural populations, mushrooms are increasingly recognized for their high protein, fiber, and antioxidant content. This change is not merely dietary it reflects a broader movement toward wellness-oriented lifestyles that prioritize natural, sustainable, and locally sourced food options. For agribusiness investors and food manufacturers, this evolution signals significant growth potential in both production and value-added segments of the market.
The Vietnam aquaculture market has transformed from traditional fishing practices into one of the world's most dynamic seafood production sectors. Vietnam now ranks as the fourth-largest aquaculture producer globally, supplying markets across Asia, Europe, and the Americas. Understanding what drives this growth is essential for investors, businesses, and policymakers looking to engage with this evolving industry.
French fries are thin strips of baked or deep-fried potatoes with a fluffy inside and a crispy outside. They originated in Europe and are now a common fast-food staple that is consumed as a snack or side dish in many countries. French fries are made mostly from high-starch potatoes and are produced in large quantities by chopping, blanching, frying, and occasionally freezing. They are among the most well-liked and extensively consumed potato-based food products in the world because of their ability to be seasoned, flavored, or combined with condiments like cheese, mayonnaise, or ketchup.
Glucose powder is a crystalline or powdered form of a simple sugar, glucose, derived mainly from sources of starch: corn, wheat, or rice. Glucose powder is obtained by the hydrolysis of starch into glucose by enzymes, followed by purification and concentration of the solution and its drying to yield a readily water-soluble, easily digested carbohydrate powder. Glucose powder is an instant source of energy as it is quickly absorbed in the body, which makes the product valuable in food, beverage, nutraceutical, and pharmaceutical applications. It has a neutral taste, a very high sweetness index compared to regular sugar, and excellent dissolving properties, making it useful in various industrial formulations and household consumption.
Ghee is a class of clarified butter that, conventionally, is prepared by simmering butter until the milk solids separate and caramelize, leaving a golden, fragrant fat. Presently, it is widely used in South Asian, Middle Eastern, and increasingly global cuisines. Ghee has a high smoke point, long shelf life, and rich flavor, which makes it suitable for cooking, frying, and flavor enhancement. During its production, water and milk proteins are removed, making the product a lactose-free fat that contains fat-soluble vitamins and bioactive compounds. Its stability, purity, and distinctive taste make ghee an important culinary and functional ingredient in both traditional and modern food applications.
Fruit powder is made by removing the moisture content of whole fruits through various methods, such as spray drying, freeze-drying, drum drying, or vacuum drying, to get a finely ground, dehydrated powder form. After drying, the fruit is then milled into a stable, lightweight, and shelf-friendly powder that retains much of the fruit's natural flavor, aroma, nutrients, and color. Fruit powders have the essence of fresh fruit in concentrated, easy-to-handle form and are thus highly versatile in food, beverage, nutraceutical, and cosmetic applications. They offer an alternative to fresh fruits in a more convenient manner with longer shelf life and consistent quality for industrial use.
Garlic powder is the dried form of garlic, made by drying fresh garlic cloves and then grinding them to a uniform powder. Garlic dehydration removes moisture while preserving much of the flavor, aroma, and pungency of garlic. This concentrated form offers longer shelf life, easy storage, and consistent taste compared to fresh garlic. Garlic powder is widely used as a seasoning, marinade ingredient, and flavor enhancer in culinary, industrial, and packaged-food applications. Garlic powder imparts the taste of garlic without peeling or chopping into the dishes; therefore, it is very convenient and versatile for both homes and large-scale food manufacturers.
The Frozen food market is highly diversified, encompassing categories like frozen ready meals, fruits and vegetables, meat, seafood, desserts, and bakery items. This robust growth is fueled by fundamental shifts, including urbanization, the rise of dual-income households, and a consumer demand for convenience without compromising nutritional value. Modern freezing technologies ensure high quality and extended shelf life, addressing the critical issue of food waste.
The United States shrimp market stands as one of the most dynamic segments within the global seafood industry. It reached 983,000 Tons in 2024 as per IMARC Group and is projected to reach 1,280,000 Tons by 2033 at a growth rate of 3% from 2025 to 2033. As consumer preferences shift toward healthier protein sources and sustainable options, shrimp has emerged as a cornerstone of American dietary habits. The market reflects transformations in consumer behavior, international trade dynamics, and technological innovation within aquaculture and seafood processing.
The Australia gluten-free food industry is flourishing, powered by a surge in health-conscious consumers, a rise in gluten intolerance cases, and a growing appetite for clean-label, nutritious products. In 2024, the industry reached a notable milestone, hitting USD 361.20 Million, according to IMARC Group. Popular categories like gluten-free bakery items, snacks, dairy, and ready-to-eat (RTE) meals are leading the charge.
The global frozen food industry has undergone a remarkable transformation over the past decade, evolving from a convenience-focused sector into a sophisticated, technology-driven marketplace that prioritizes quality, nutrition, and sustainability. Innovation serves as the primary catalyst for this evolution, fundamentally reshaping consumer perceptions and market dynamics across all geographic regions.
Egg powder is a type of dehydrated product prepared from whole eggs, egg whites, or egg yolks, using a controlled drying process that removes moisture content while preserving the natural nutrients, flavor, and functional properties in fresh eggs. Originally developed to extend the shelf life of eggs, it was also meant to be convenient and easily transportable for food manufacturing, catering, and military or outdoor purposes.
The global ginger market is currently experiencing a remarkable phase of expansion, positioning itself as one of the most dynamic segments within the spice and functional ingredient industries. As consumers worldwide are increasingly gravitating toward natural, health-promoting ingredients, ginger is emerging as a star performer that is capturing attention across multiple sectors, from culinary applications to pharmaceuticals and nutraceuticals. The market is demonstrating robust momentum that industry analysts are tracking with considerable interest.
Coconut is an important tropical crop with a wide array of uses, and hence it is considered the "Tree of Life." The fruit, leaves, trunk, and roots of coconuts yield a wide range of products. Each part has economic value and, therefore, provides a means of livelihood in many rural communities and agro-industrial development in tropical regions such as Southeast Asia, South Asia, and the Pacific Islands.
Coconut yogurt is a plant-based alternative to traditional dairy, made from the rich milk of mature coconuts. This yogurt boasts the same feel and taste as traditional dairy yogurt, all the while catering to vegans, lactose-intolerant, or allergenic consumers. Manufactured like traditional yogurt, this variety is fermented with live bacterial cultures such as Lactobacillus bulgaricus and Streptococcus thermophilus. These same cultures ferment the natural sugars of the coconut milk into lactic acid during processing, creating a thick consistency and giving it that tangy taste typical of yogurt.
The Australian dog food market is undergoing an important transformation, motivated mainly by advancements in AI technology. As more people own pets, they increasingly demand more tailored and nutritious options for dogs. Both technology and artificial intelligence (AI) are important to facilitate this, and reshaping the industry overall.
Coconut sugar, also known as coconut palm sugar, is a natural sweetener derived from the sap of flower buds from the coconut palm tree, Cocos nucifera. It has traditionally been produced in various tropical countries like Indonesia, the Philippines, India, and Thailand, where coconut cultivation is plentiful. This type of sugar is produced by tapping the flower buds of the coconut palm to collect the sap. The sap collected is then heated gently to boil off the water content, concentrate the sugars, and form a thick syrup.
The cashew nut is the kidney-shaped seed of the cashew apple, which is the fruit of the tropical evergreen tree Anacardium occidentale. In trade, the "cashew nut" is the edible kernel extracted from the drupe that lies under the cashew apple; the apple itself is consumed for juices and value-added products in certain markets. Cashew trees are adapted to tropical and subtropical regions with good drainage soils, and leading producers are Vietnam, India, Côte d'Ivoire, Brazil, and some West African states.
Carbonated soft drinks (CSDs) are soft drinks that contain carbon dioxide gas dissolved under pressure, providing the characteristic fizz and invigorating mouth feel that consumers like. They generally consist of carbonated water, sweeteners (sugar, high-fructose corn syrup, or low-calorie alternatives), flavoring ingredients, colorants, and preservatives. The products that fall under the category are colas, lemon-lime beverages, fruit-flavored sodas, tonic water, and sparkling mineral water.
Beer is one of the oldest and most popular alcoholic drinks in the world, made by the fermentation of cereal grains, usually barley, but also wheat, maize, or rice using yeast, hops, and water. The process of brewing turns these natural products into a drink that has intricate flavors, fizz, and a range of alcohol levels, usually 3% to 8% ABV. Hops add bitterness and flavor, with malted barley adding fermentable sugars and color. Beer has developed in centuries from small-scale, craft brewing to an international industrialized market with identifiable styles including lagers, ales, stouts, and pilsners.
The areca nut, or betel nut, is the seed of the areca palm (Areca catechu), a tropical palm mainly grown in South and Southeast Asia. It is one of the oldest described masticatories, chewing historically with betel leaf and lime for its mild stimulant effect. The nut is oval, fibrous, and high in alkaloids like arecoline, which is responsible for the typical flavor and psychoactive effects. Top producers are India, Bangladesh, Sri Lanka, Indonesia, Myanmar, Thailand, and China, with India dominating in both output and consumption.
Apple juice is among the most popular fruit drinks in the world, appreciated for its crisp flavor, inherent sweetness, and health advantages. Apple juice is made by pressing fresh apples and filtering the resulting liquid, containing vital nutrients like vitamin C, potassium, antioxidants, and polyphenols that support immune function, cardiovascular health, and hydration. Based on manufacturing techniques, apple juice can be clear, murky, or concentrated, with each type presenting unique taste profiles and longevity attributes.
Banana powder is a dry, fine, nutrient-dense substance created by dehydrating ripe or unripe bananas using methods like spray drying, freeze drying, or drum drying. It acts as an easy and shelf-stable substitute for fresh bananas, preserving most of their essential nutrients such as potassium, magnesium, vitamin B6, and dietary fiber. The production process includes choosing premium bananas, removing their peels, cutting them into slices, and drying them to an optimal moisture content before milling into a fine powder.
Almonds are nutrient-dense seeds obtained from the fruit of the Prunus dulcis tree, highly prized as a food item and source of industrial raw materials. Botanically drupes, almonds have a hard shell covering the edible kernel, which is rich in proteins, monounsaturated fat, fiber, vitamins, and minerals. The two main varieties are sweet almonds, eaten raw or processed into food items, and bitter almonds, used conventionally to extract oil and flavor after purging. The distinguishing features are mild nutty taste, excellent shelf life if kept properly, and very good compatibility with food as well as non-food uses. Almonds are processed in several steps like cleaning, shelling, blanching, roasting, or oil extraction, depending on the final purpose.
In today's fast-paced world, ready-to-eat food has become a staple for anyone juggling work, family, or travel. These foods offer the comfort of a home-cooked dish, without the time and effort, making them a go-to solution for people who crave convenience. With over 4 billion people living in cities globally and the number of dual-income households rising, the time available for traditional cooking has significantly decreased, creating consistent demand for quick meal options.
Cocoa powder is one of the main derivatives of the cocoa bean, which is derived after cocoa butter has been extracted from it during the chocolate production process. It consists mainly of non-fat cocoa solids, which contain a high content of polyphenols, flavonoids, and alkaloids like theobromine. Famous for its intense color, bitter-sweet taste, and antioxidant activity, cocoa powder comes in natural and alkalized (Dutch-processed) grades, each with distinctive taste profiles and functional characteristics.
Cassava starch or tapioca starch is a white, odorless, fine powder extracted from the cassava plant's roots (Manihot esculenta). Cassava starch has diverse applications in food, pharmaceutical, textile, paper, and adhesives industries because of its unbeatable thickening, gelling, binding, and stabilizing properties. In the food industry, cassava starch finds its applications in bakery, confectionery, dairy, beverages, and gluten-free foods as a substitute for wheat and corn-based starches.
The global vegan yogurt market was valued at USD 3.40 Billion in 2024 and is projected to reach USD 12.21 Billion by 2033, growing at a CAGR of 14.51% from 2025 to 2033. This expansion is marked by ongoing innovation, enhanced consumer personalization, and a deeper commitment to sustainability.
The guacamole market is experiencing a notable change, primarily fueled by an increasing consumer preference for healthy, convenient, and natural food choices. In 2024, the market was valued at USD 1379.9 Million. Guacamole is a creamy avocado-based dip originating from Mexican cuisine has grown into a globally popular food product recognized for its nutritional value and versatility.
Corn starch tableware is a new and ecofriendly solution to traditional plastic disposable items, which aims at solving the increasing environmental issues linked to plastic waste. Comprising mostly of corn starch, a plant-based and renewable resource, the products range from plates, bowls, cups, cutlery, and food containers, all of which are completely biodegradable and compostable.
Artificial Intelligence (AI) is transforming India's beer market at a rapid pace by balancing art with advanced technology. Right from brewing to branding, AI makes fermentation precise, temperature adjustment accurate, and ingredient control efficient, guaranteeing consistent quality and innovation in taste.
Soybean oil is a major vegetable oil used as food obtained from the seeds of the soybean crop. It ranks among the world's most significant edible oils, widely utilized in the preparation of foods, processed food items, industrial purposes, and increasingly in biofuels. High in polyunsaturated fats, especially omega-6 fatty acids, soybean oil has applications in non-food industries such as the production of biodiesel, cosmetics, naphthas, and lubricants.
A bun is a small, round or oval-shaped, soft-textured bread product that can be slightly sweet or savory in taste. Made chiefly of wheat flour, yeast, sugar, salt, water, and fat, buns are found in most cuisines around the globe.
The global dairy market is presently experiencing a profound transformation. This is largely accredited to the strategic integration of artificial intelligence (AI), a technology poised to redefine established paradigms of efficiency and innovation within the industry.
People’s relationship with food is undergoing a profound transformation. No longer just a source of fuel, what individuals eat is now seen as a cornerstone of the overall well-being—a tool to boost immunity, sharpen focus, support digestion, and build long-term resilience. This evolution in consumer consciousness is creating a powerful demand for foods that are functional, organic, and transparently made with real ingredients.
Tequila, once confined to regional consumption in Mexico, has now become a popular spirit worldwide, known for its rich heritage, skilled craftsmanship, and premium quality. Made from blue agave, tequila has attracted international consumers for its distinct flavor, artisanal qualities, and cocktail versatility.
Avocado oil is a nutritious oil pressed from the pulp of avocados (Persea americana), in contrast with most oils, which are seed derived. Avocado oil is valued for its rich content of monounsaturated fats, especially oleic acid, in addition to necessary vitamins like E, A, and D. Avocado oil has a mild, buttery taste and very high smoke point and is used both in food preparation and cosmetics.
Biscuits are dry, baked foods made from flour and usually crisp in texture and flat in shape, eaten frequently as a snack or with a meal. They consist mostly of wheat flour, sugar, fat (butter or vegetable oil), and leavening agents such as baking powder. Flavors and variety may be added using ingredients like milk solids, chocolate, spices, or dried fruits. Biscuits come in sweet and savory forms, varying from cookies and cream-filled to salted crackers. Their shelf life, which is lengthy, convenient packaging, and broad taste appeal have made them a household staple, school staple, and workplace staple worldwide.
Nutritional powders have become essential nutritional supplements created to address the specific health needs of vulnerable demographics, including diabetic patients, the aged, and the sick. When regular food intake is inadequate or compromised, these powders, which are made with specially designed compositions and are high in vital vitamins, minerals, protein, and carbs, offer balanced nourishment. Specialized baby formulas guarantee the best possible growth and development in the early years of life.
Vegetable oils remain among the world’s most widely used agricultural products, essential to food manufacturing, biofuels, cosmetics, and industrial goods.
Learn key financial strategies, operational and capital cost planning essentials for starting a profitable livestock feed production business in 2025.
World Tea Day, celebrated every year on May 21st, is an opportunity to appreciate the rich history, cultural significance, and economic impact of tea. From its origins in ancient China to its status as a global commodity, tea continues to connect people, cultures, and economies.
Mango pulp is the thick, smooth, and semi-liquid product yielded by crushing or pulping ripened mangoes. It is the inner flesh of the mango fruit extracted, without the skin and seeds. Mango pulp is widely utilized as a base for many food items, including mango juice, nectar, drinks, smoothies, ice creams, desserts, and as a topping for pancakes or yogurt. Mango juice is a cool drink prepared from ripe mangoes' juice. To make mango juice, the ripe mangoes are normally peeled, pitted, and the flesh of the mango is squeezed to get the pulp. The pulp is further treated to remove the juice from any remaining fibers or solids.
Soy sauce is a liquid condiment used extensively in cooking and seasoning food. Produced from fermented soybeans, wheat, salt, and water, it provides a deep umami taste that can be used to enhance different foods. It is a common ingredient in Asian cooking and has become popular worldwide in marinades, stir-fries, dips, and processed foods. Come in various forms including light, dark, and low-sodium, soy sauce meets the different consumer tastes and nutritional requirements, rendering it a vital ingredient in the food industry.
Instant coffee is a quick and easy-to-brew coffee beverage that is produced by brewing coffee beans into a liquid that concentrates and evaporates into powder or grain form. It rapidly dissolves in hot water, so it's highly sought after by customers demanding fast and easy coffee brewing. It has a long storage life and is inexpensive, making it popular in homes, offices, and food service establishments. It is fueled by urbanization, hectic lifestyles, and growing demand for convenience drinks.
Glucose syrup and sorbitol syrup are versatile sweeteners widely used across the food and beverage industry. Their ability to enhance texture, retain moisture, and extend shelf life makes them essential ingredients in confectionery, bakery, dairy, and beverage products. Beyond their functional benefits, these syrups contribute to taste enhancement and product stability, catering to consumer preferences for smooth, consistent formulations.
Potato flakes are a highly adaptable food ingredient created by processing cooked potatoes into thin, dehydrated slices. They are often used in soups, snacks, baked goods, and fast meals and are well-known for their usefulness, taste, and simplicity of usage. These flakes provide a reliable and effective option for home cooking, foodservice, and commercial food production while preserving the natural flavour, texture, and nutritional value of fresh potatoes. They are indispensable in a variety of culinary applications due to their lengthy shelf life, lightweight design, and easy rehydration method. Their ability to be used in a variety of recipes, from thickened stews to crispy coatings, further solidifies their position as a basic component of the world's food industry.
Industrial enzymes are biological catalysts that fast-track the chemical process that is involved during the industrial processes. Their use is mainly seen in the food and beverage, pharmaceutical, textile, biofuel, and detergent industries. This enzyme is very effective as it is energy efficient and has cleaner and greener production. Its stability and specificity make it a wonderful tool for breaking complex molecules while improving product quality and yield. Industrial enzymes can enhance the texture of bread, benefit dairy processing, assist in the production of biofuels, and clean wastewater. All these phenomena illustrate that industrial enzymes are a mandatory requirement to manufacture many more products with sustainability and cost effectiveness for multiple industries.
Sorbitol is a sugar alcohol widely used as a sweetener, humectant, and stabilizer in food, pharmaceuticals, and cosmetics. It is made commercially by hydrogenating glucose and is naturally present in fruits like apples and pears. Because of its mild sweetness, low glycaemic index, and ability to retain moisture, sorbitol is a popular ingredient in skincare, dental care, and sugar-free goods. It is also an essential component of industrial processes and a laxative in medical applications.
Inedible beef tallow, a byproduct of the meat processing industry, is derived from beef suet and serves various industrial and commercial purposes. This versatile substance undergoes rendering, a process that separates the fat from solid components. Inedible beef tallow's primary application is in animal feed, as it provides essential fats and energy for livestock, particularly in pet food and livestock supplements. Additionally, it finds use in the cosmetics and personal care industry, contributing to the production of candles, soaps, and skin-care products.
Vitamin C supplements are typically made by extracting ascorbic acid from various sources, such as citrus fruits, or synthesizing it in a laboratory setting. The extracted or synthesized ascorbic acid is then processed and formulated into different types of supplements, including tablets, capsules, chewable, and powdered forms. One of the primary advantages of Vitamin C supplements is their ability to support a healthy immune system.
Over the recent decade, the online food and grocery delivery business in India has witnessed exponential growth. This expansion is attributed to the increasing penetration of smartphones, the affordability and convenience offered by food delivery app services, and the growing availability of low-cost internet services. The industry has become progressively competitive, with numerous local and international players competing for a significant market share. Nonetheless, despite the extreme competition, global players are continuing to make significant investments in India on account of its significant market share in the global online food delivery market.
‘World Food Day’ is celebrated on October 16th as a global responsibility to abolish hunger. 2024’s theme for the day is ‘Right to foods for a better life and a better future’. This theme highlights the significance of enabling access to nutritious food for all, particularly in the face of global challenges, including poverty, climate change, and conflict. In line with this theme, in October 2024, India and the United Arab Emirates (UAE) announced plans for developing a food corridor between the two nations, with an initial investment of over USD 2 Billion (INR 17,000 Crore) in food processing and logistics for food parks. This project significantly reinforces the UAE's food security while providing support to Indian farmers. The initiative is part of a bigger investment strategy targeting over USD100 Billion across key sectors, including manufacturing, infrastructure, and logistics.
A vegan, or a plant-based diet, focuses mainly on consuming fruits, vegetables, grains, legumes, nuts, and seeds. It excludes all animal-derived products and ingredients, including meat, poultry, fish, dairy, eggs, and honey. Nowadays, people are shifting toward vegan diets for a variety of reasons, such as ethical concerns for animal welfare, environmental sustainability, health benefits, and personal preferences.
Functional foods promote overall well-being and offer specific health benefits beyond daily nutrient intake. These benefits encompass enhanced bone health, effective cholesterol management, improved heart health, and eye health. Functional foods include probiotic yoghurt, omega-3 enriched eggs, fortified milk, antioxidant-rich berries, and functional beverages.
Fusion cuisine and beverages blend different ingredients, flavors, or techniques from various culinary or cultural backgrounds to create unique and innovative flavor profiles in dishes and drinks. Fusion beverages encompass both alcoholic and non-alcoholic options, including cocktails, mocktails, smoothies, teas, and more. These beverages span a spectrum from simple combinations to complex and inventive concoctions. Changing taste preferences and global connectivity are the main reasons for the increasing adoption of fusion beverages. They are available in various product types, such as carbonated drinks, fused teas and coffees, fruit juices, fusion alcoholic beverages, energy drinks, sports drinks, and more. These beverages are accessible through off-trade outlets (hypermarkets, supermarkets, discounters, grocery stores, off-license stores, alcohol and confectionery stores, highly specialized retailers, and online stores), as well as on-trade establishments (pubs, bars, cafés, restaurants, clubs, discos, hotels, mass events, and others). Examples of fusion beverages include fruit-infused tea, Asian-inspired cocktails, spicy margaritas, bubble tea creations, mojito variations, and infused waters. Furthermore, fusion cuisine merges elements from diverse culinary traditions, such as Asian, European, African, or Latin American, to craft new and exciting dishes. Examples of fusion cuisine include sushi burritos, Thai basil pizza, kimchi tacos, and more.